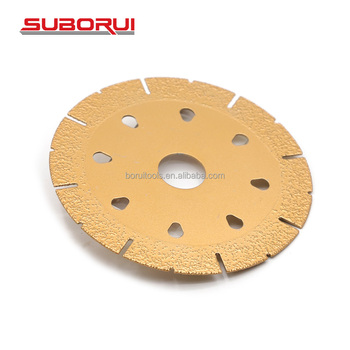
Hot-Pressed Sintered Turbo Rim Diamond Blade
105–230 mm | 10 mm Rim | Wet/Dry Masonry & Granite
US$1.30–4.80 / piece
MOQ: 100 pieces
In an era where construction contractors, stone fabrication shops, and tile installers demand zero edge-chipping, accelerated cutting feeds, and extended blade life, selecting the right industrial turbo rim diamond saw blade requires deep technical insight. At Jiangsu WRD Tools Co., Ltd., we bridge the gap between metal-matrix metallurgical formulation and high-volume, automated CNC blade synthesis.
Designed for stone distributors, building supply wholesalers, and brand owners. Every blade is manufactured using synthetic industrial diamond monocrystals sinter-bonded with balanced cobalt-bronze alloys.
105–230 mm | 10 mm Rim | Wet/Dry Masonry & Granite
US$1.30–4.80 / piece
MOQ: 100 pieces
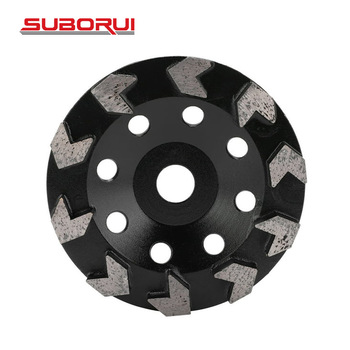
1.2 mm Kerf | 70/80 Mesh Diamond | Zero-Chipping Ceramic
US$1.85–5.50 / piece
MOQ: 100 pieces
Deep-Grit Vents | 65Mn Core | Reinforced Deflection Hub
US$2.60–8.90 / piece
MOQ: 50 pieces
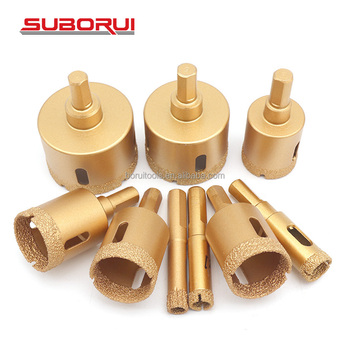
Hard Cured Aggregates | 12 mm Segment | Premium Cobalt Bond
US$3.80–12.50 / piece
MOQ: 50 pieces
Where the superabrasive cutting tool industry is heading over the next 3 to 5 years: procurement intelligence for distribution executives.
The surge in 12mm to 20mm ultra-compact sintered stone (Dekton, Neolith, large-format porcelain) has rendered classic thick blades obsolete. Global tool brands are rapidly expanding purchase orders for ultra-thin (1.0 mm – 1.4 mm) mesh turbo rim blades equipped with reinforced centers to counter kerf deviation while guaranteeing zero micro-fracturing along precision edges.
Buyer Action: Transition stock from broad 2.2mm kerf blades toward reinforced fine mesh profiles.
As battery-powered 18V/36V and 54V cordless angle grinders replace corded tools on construction sites, blades with heavy rotational mass deplete battery charges quickly. Future procurement contracts prioritize low-friction segment geometries, laser aerated cores, and reduced peripheral drag matrices that maximize cuts per battery charge.
Buyer Action: Request aerodynamic laser-slotted cores to improve cuts-per-charge metrics by up to 28%.
Stringent OSHA and European silica dust mitigation guidelines are driving a massive industry pivot toward wet-adaptable dry blades or tools paired with integrated shroud extractors. Procurement teams must ensure steel cores incorporate thermodynamic laser cuts that vent slurry without losing structural integrity or causing blade warping under heat.
Buyer Action: Source dual-purpose wet/dry certified formulations backed by third-party testing.
How metallurgical bonding, diamond grain distribution, and tensioning chemistry have evolved to solve high-RPM failure modes.
| Processing Tech | Density & Strength | Optimal Application |
|---|---|---|
| Cold-Pressed | Medium Bond Density | Budget DIY & General Brick |
| Hot-Pressed (Ours) | Ultra-High Density Matrix | Heavy Duty Granite, Slate, Quartz |
| Laser Welded | Deep Penetration Joint | Safety-Critical Dry Cured Concrete |
| Vacuum Brazed | Direct Surface Diamond Bond | Ductile Iron, Glass, Composites |
1st Gen - Straight Serration: Simple corrugated perimeter with intermittent air cooling. Suffered from uneven side wear and core pinching in deep plunge cuts.
2nd Gen - Slanted Turbo Ribs: Angled flutes that actively expelled dust from the cutting groove. Dramatically reduced thermal accumulation but generated noticeable vibration.
3rd Gen - 3D Corrugated Mesh: Variable wave serrations combined with alternating relief grooves and thermal dissipation holes. Delivers exceptional feed rates, low resonance, and chip-free glass-smooth kerfs.
Raw Diamond Quality: We utilize high-grade synthetic diamond crystals with high static and dynamic compressive strengths (Ti & TTi ratings), resisting premature shattering under impact.
Matrix Tailoring: Balancing metal powders (Cobalt, Copper, Nickel, Tin, and Tungsten Carbide) ensures that the bond matrix erodes at a synchronized rate, shedding spent diamonds and continuously exposing sharp cutting facets.
Tension Rolling: Laser-cut 65Mn alloy cores are tensioned dynamically by certified technicians to resist deflection up to 13,300 RPM.
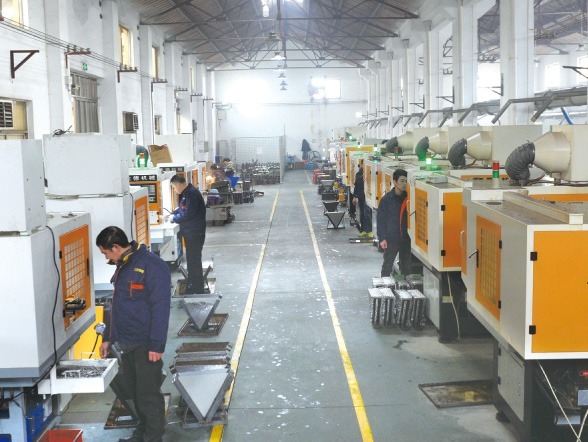
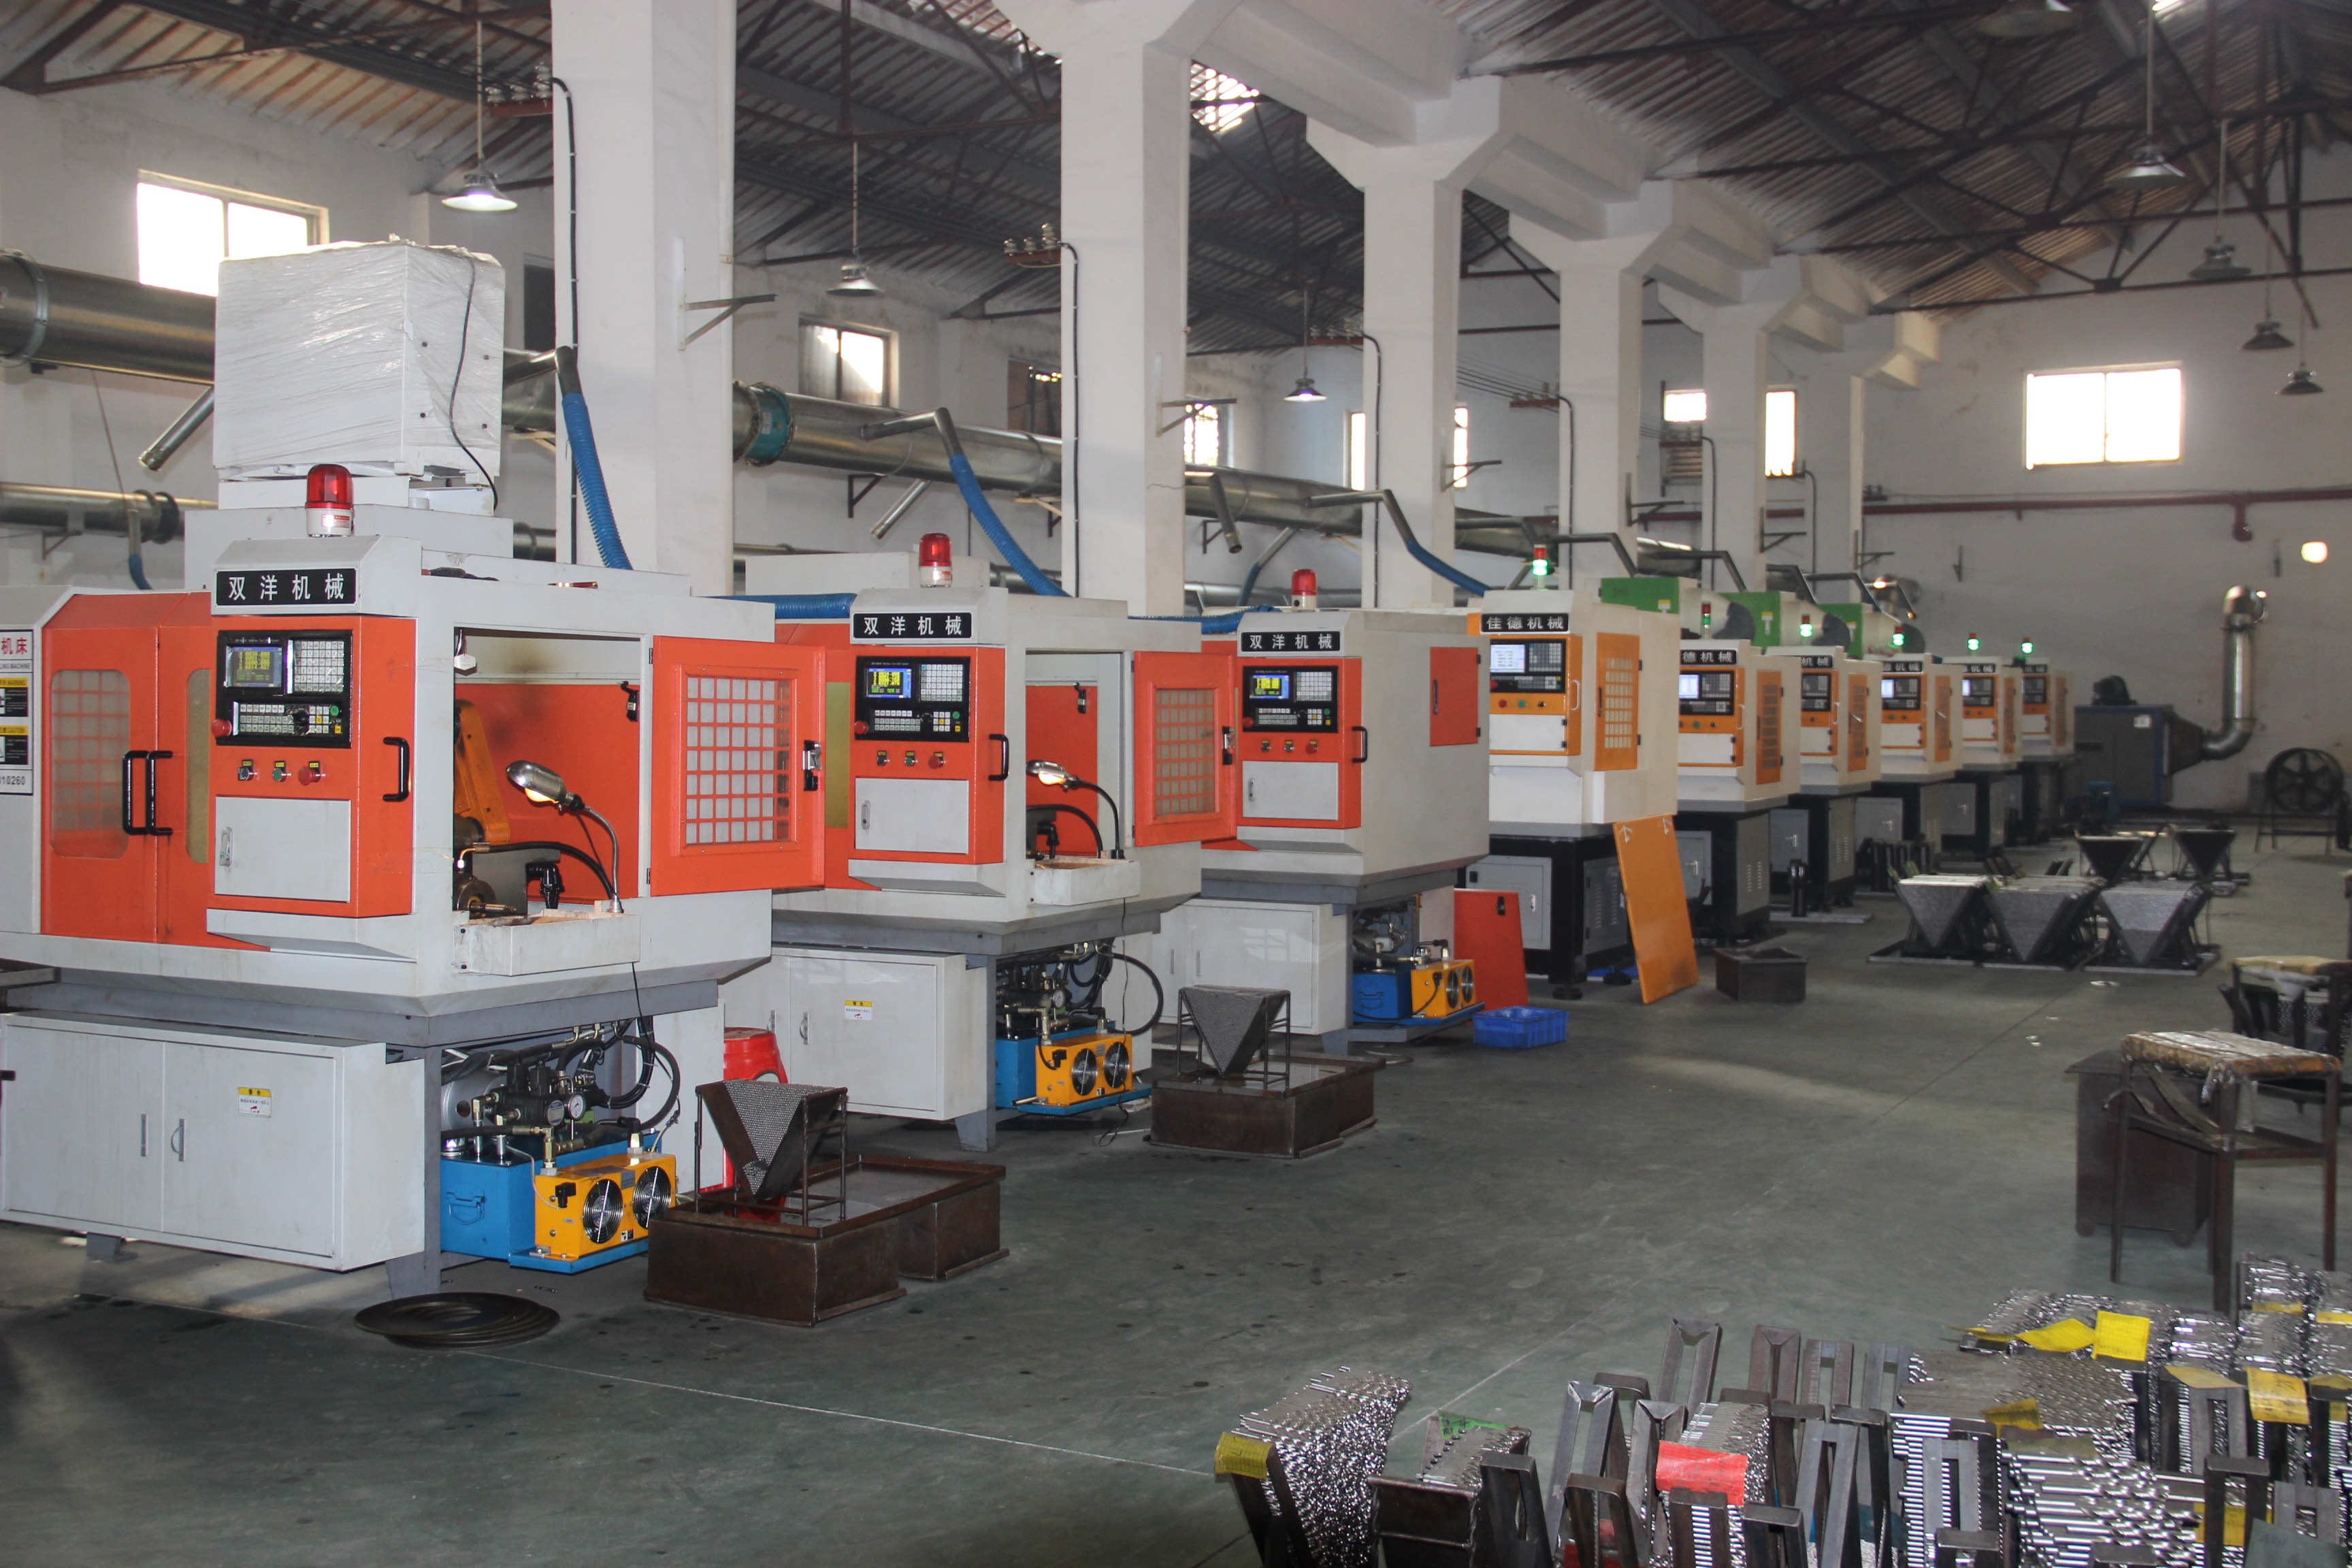
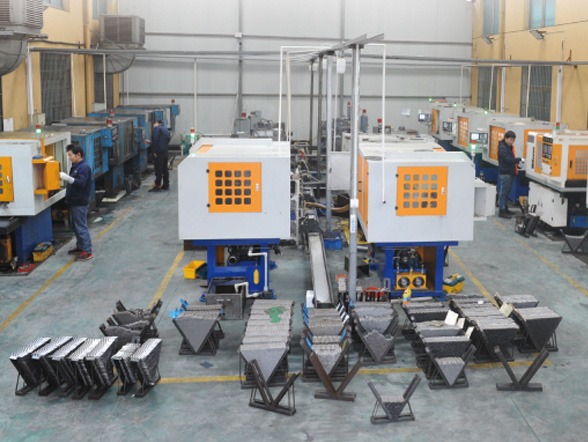
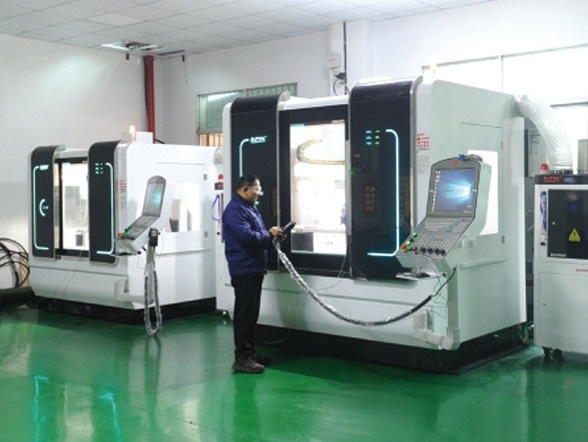
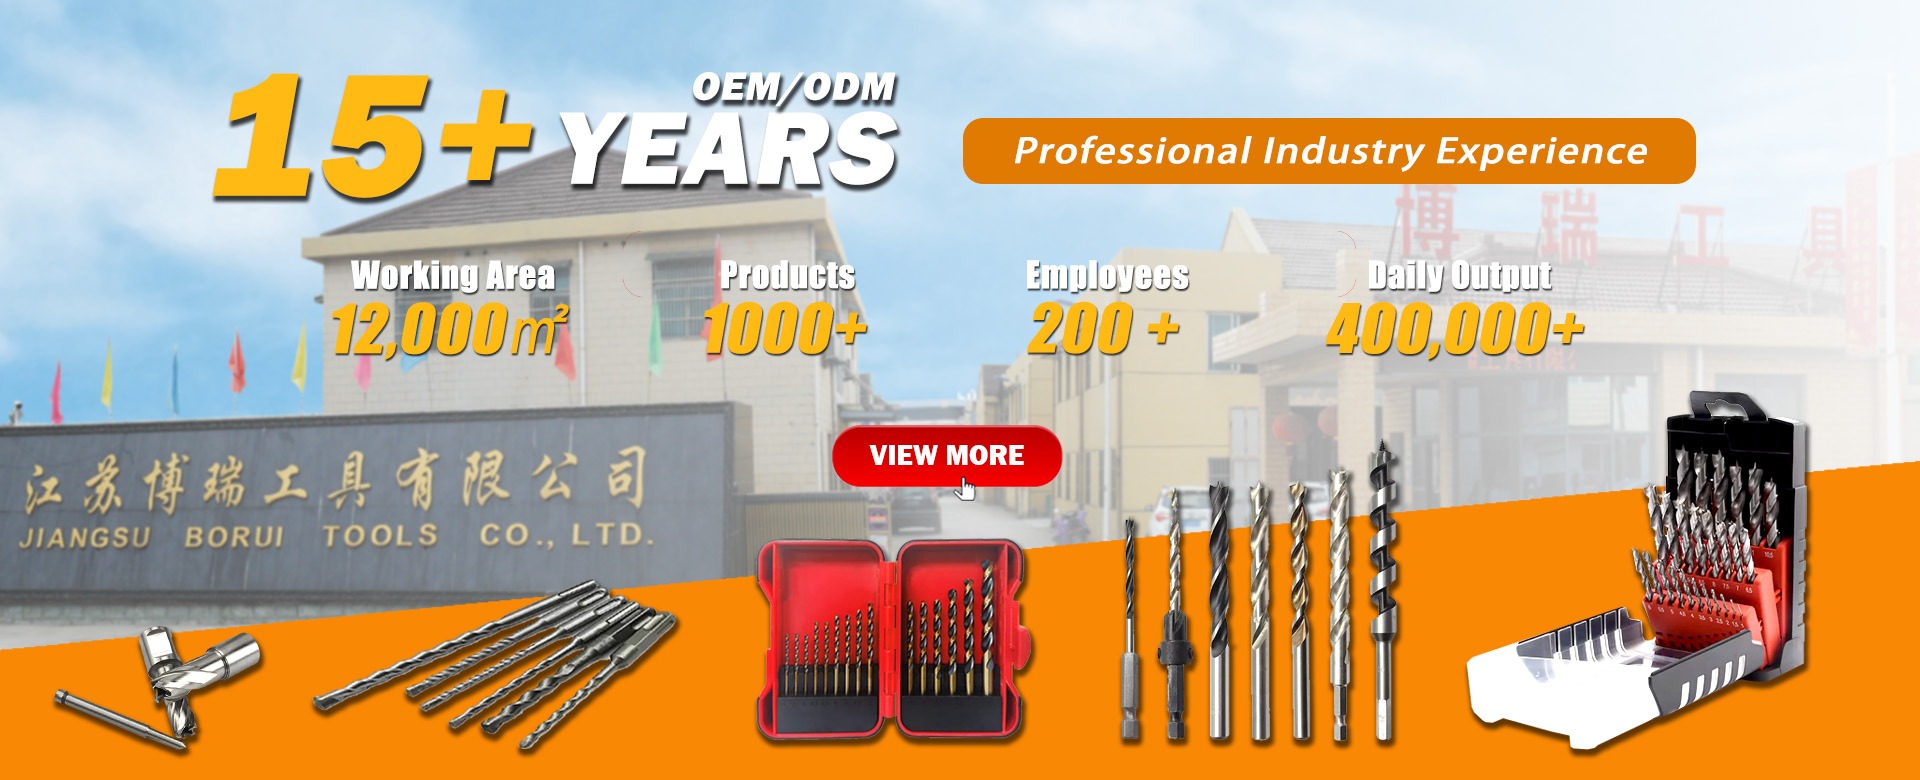
Jiangsu WRD Tools Co., Ltd. was established in March 2007 with a registered capital of RMB 10 million. Our state-of-the-art 12,000 m² manufacturing plant in Danyang, Jiangsu Province, houses specialized workshops for precision diamond saw blades, diamond cup wheels, HSS twist drills, annular cutters, and specialized hole saws, powered by a dedicated team of over 150 employees.
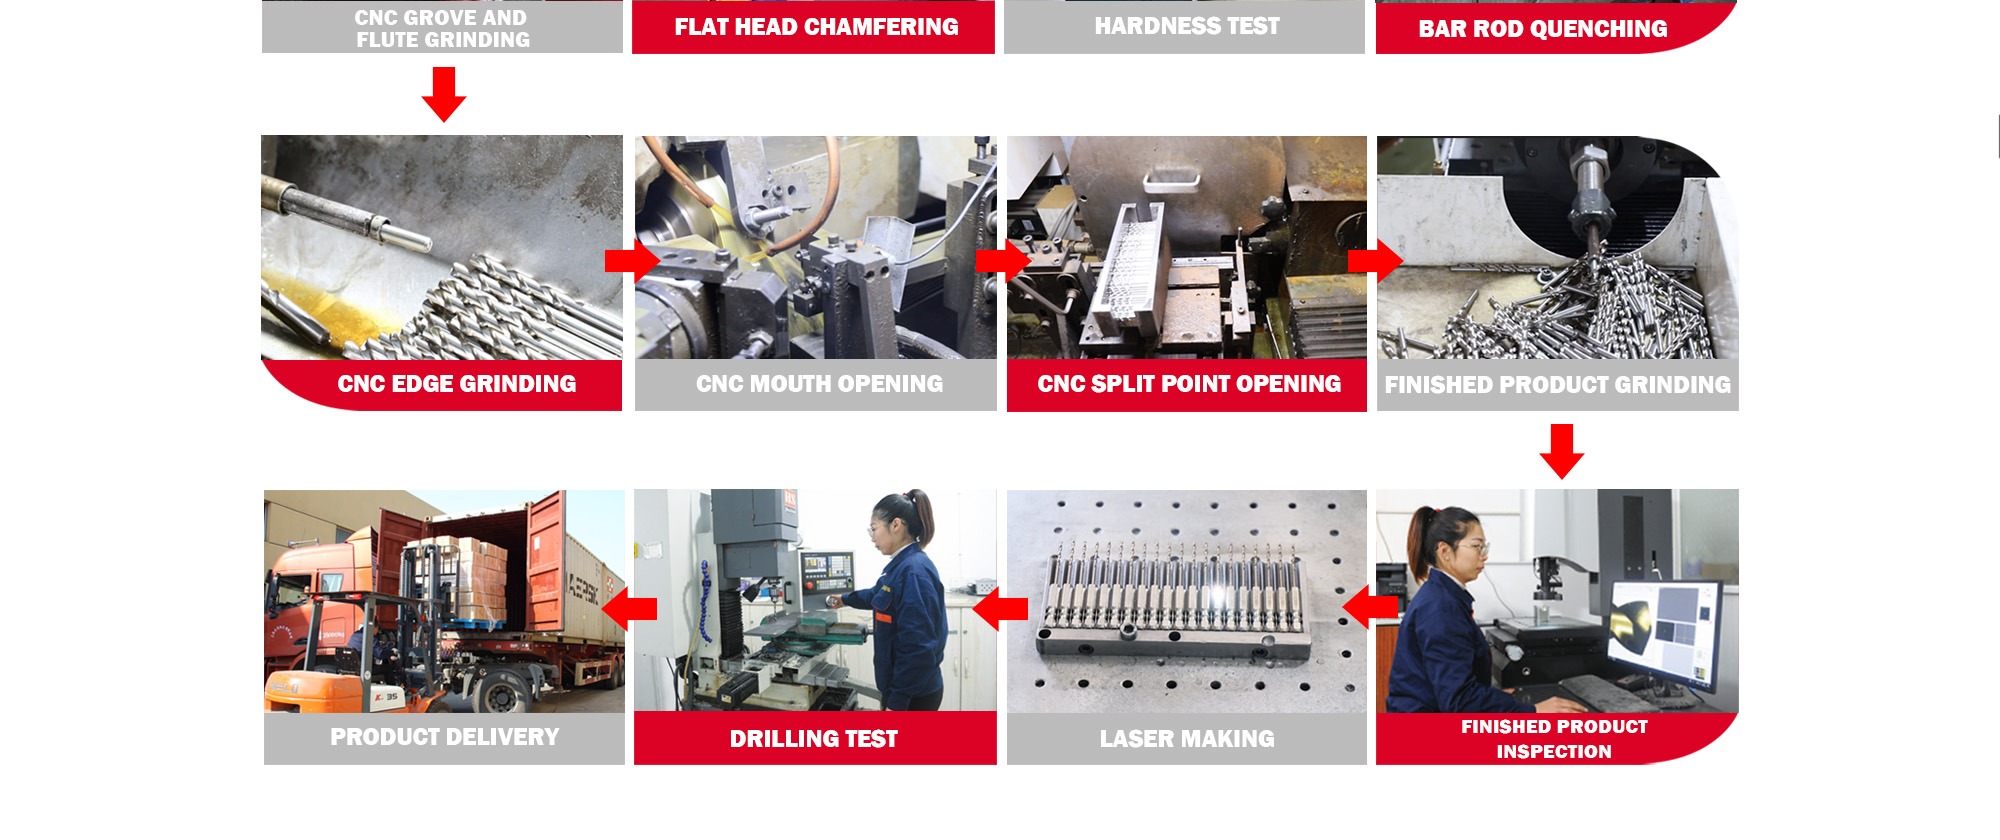
Unlike export trading agencies, we control every critical step internally: raw alloy blank laser profiling, computerized matrix powder mixing, hydraulic hot-press sintering, automated rim edge grinding, dynamic tension balancing, and private-label laser marking. Our annual production volume exceeds 90 million precision cutting tools, generating over RMB 80 million in annual sales and securing approval as a recognized High-Tech Enterprise of Jiangsu Province in 2019.
Over nearly two decades, our factory has manufactured tools adhering to the strict QA audits expected by leading global brands including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
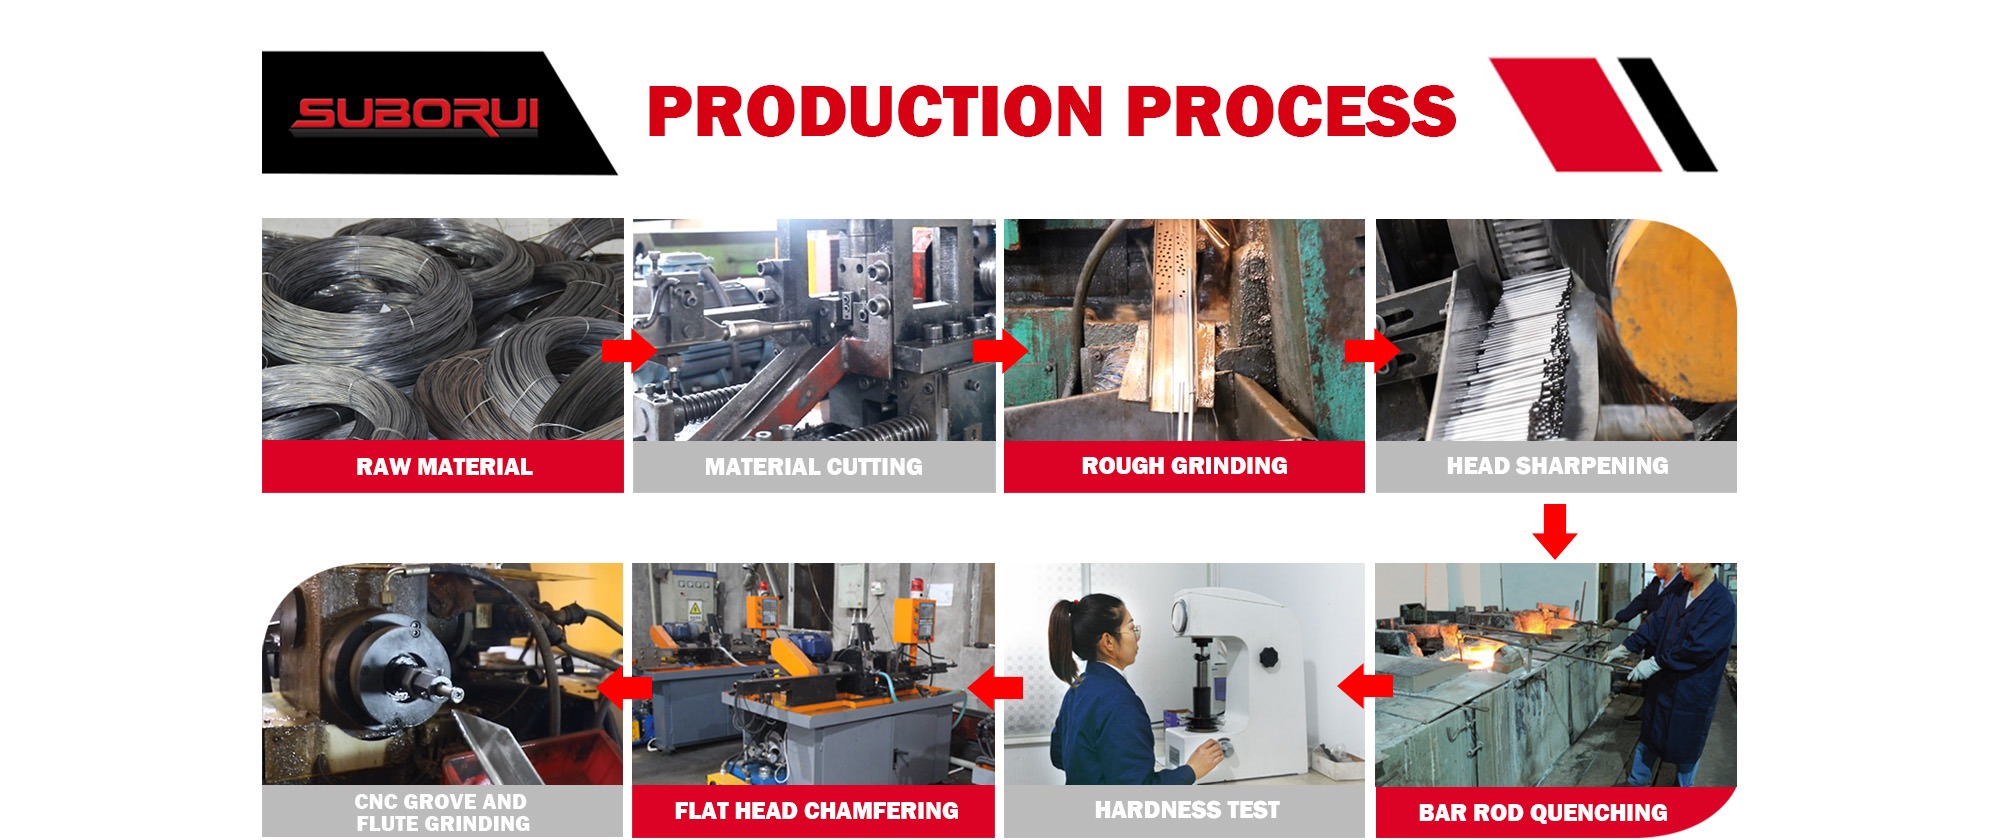
Six rigorous manufacturing checkpoints ensure zero segment loss, exceptional cutting life, and run-out accuracy on every production batch.
High-carbon 65Mn / 75Cr1 alloy sheets are laser-profiled to prevent distortion.
Industrial diamonds and metal bonding powders are homogeneous three-axis blended.
Vacuum hot-pressing under strict temperature curves bonds the segment securely.
Technicians roller-tension every blade to prevent lateral wobble under load.
Automated silicon carbide wheels sharpen and expose diamond crystals.
Bore inspection, laser marking, balance testing, and custom blister carding.
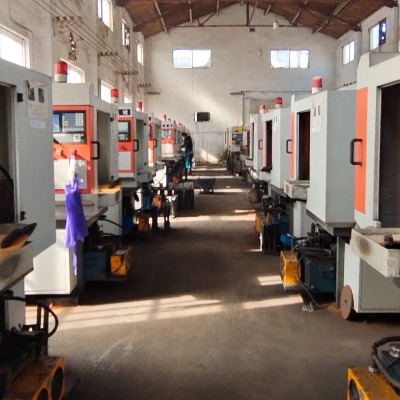
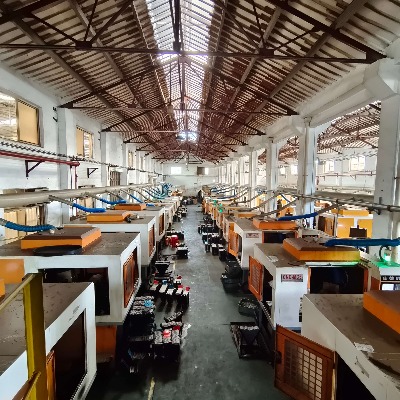
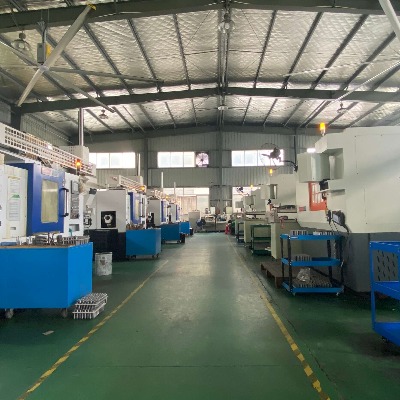
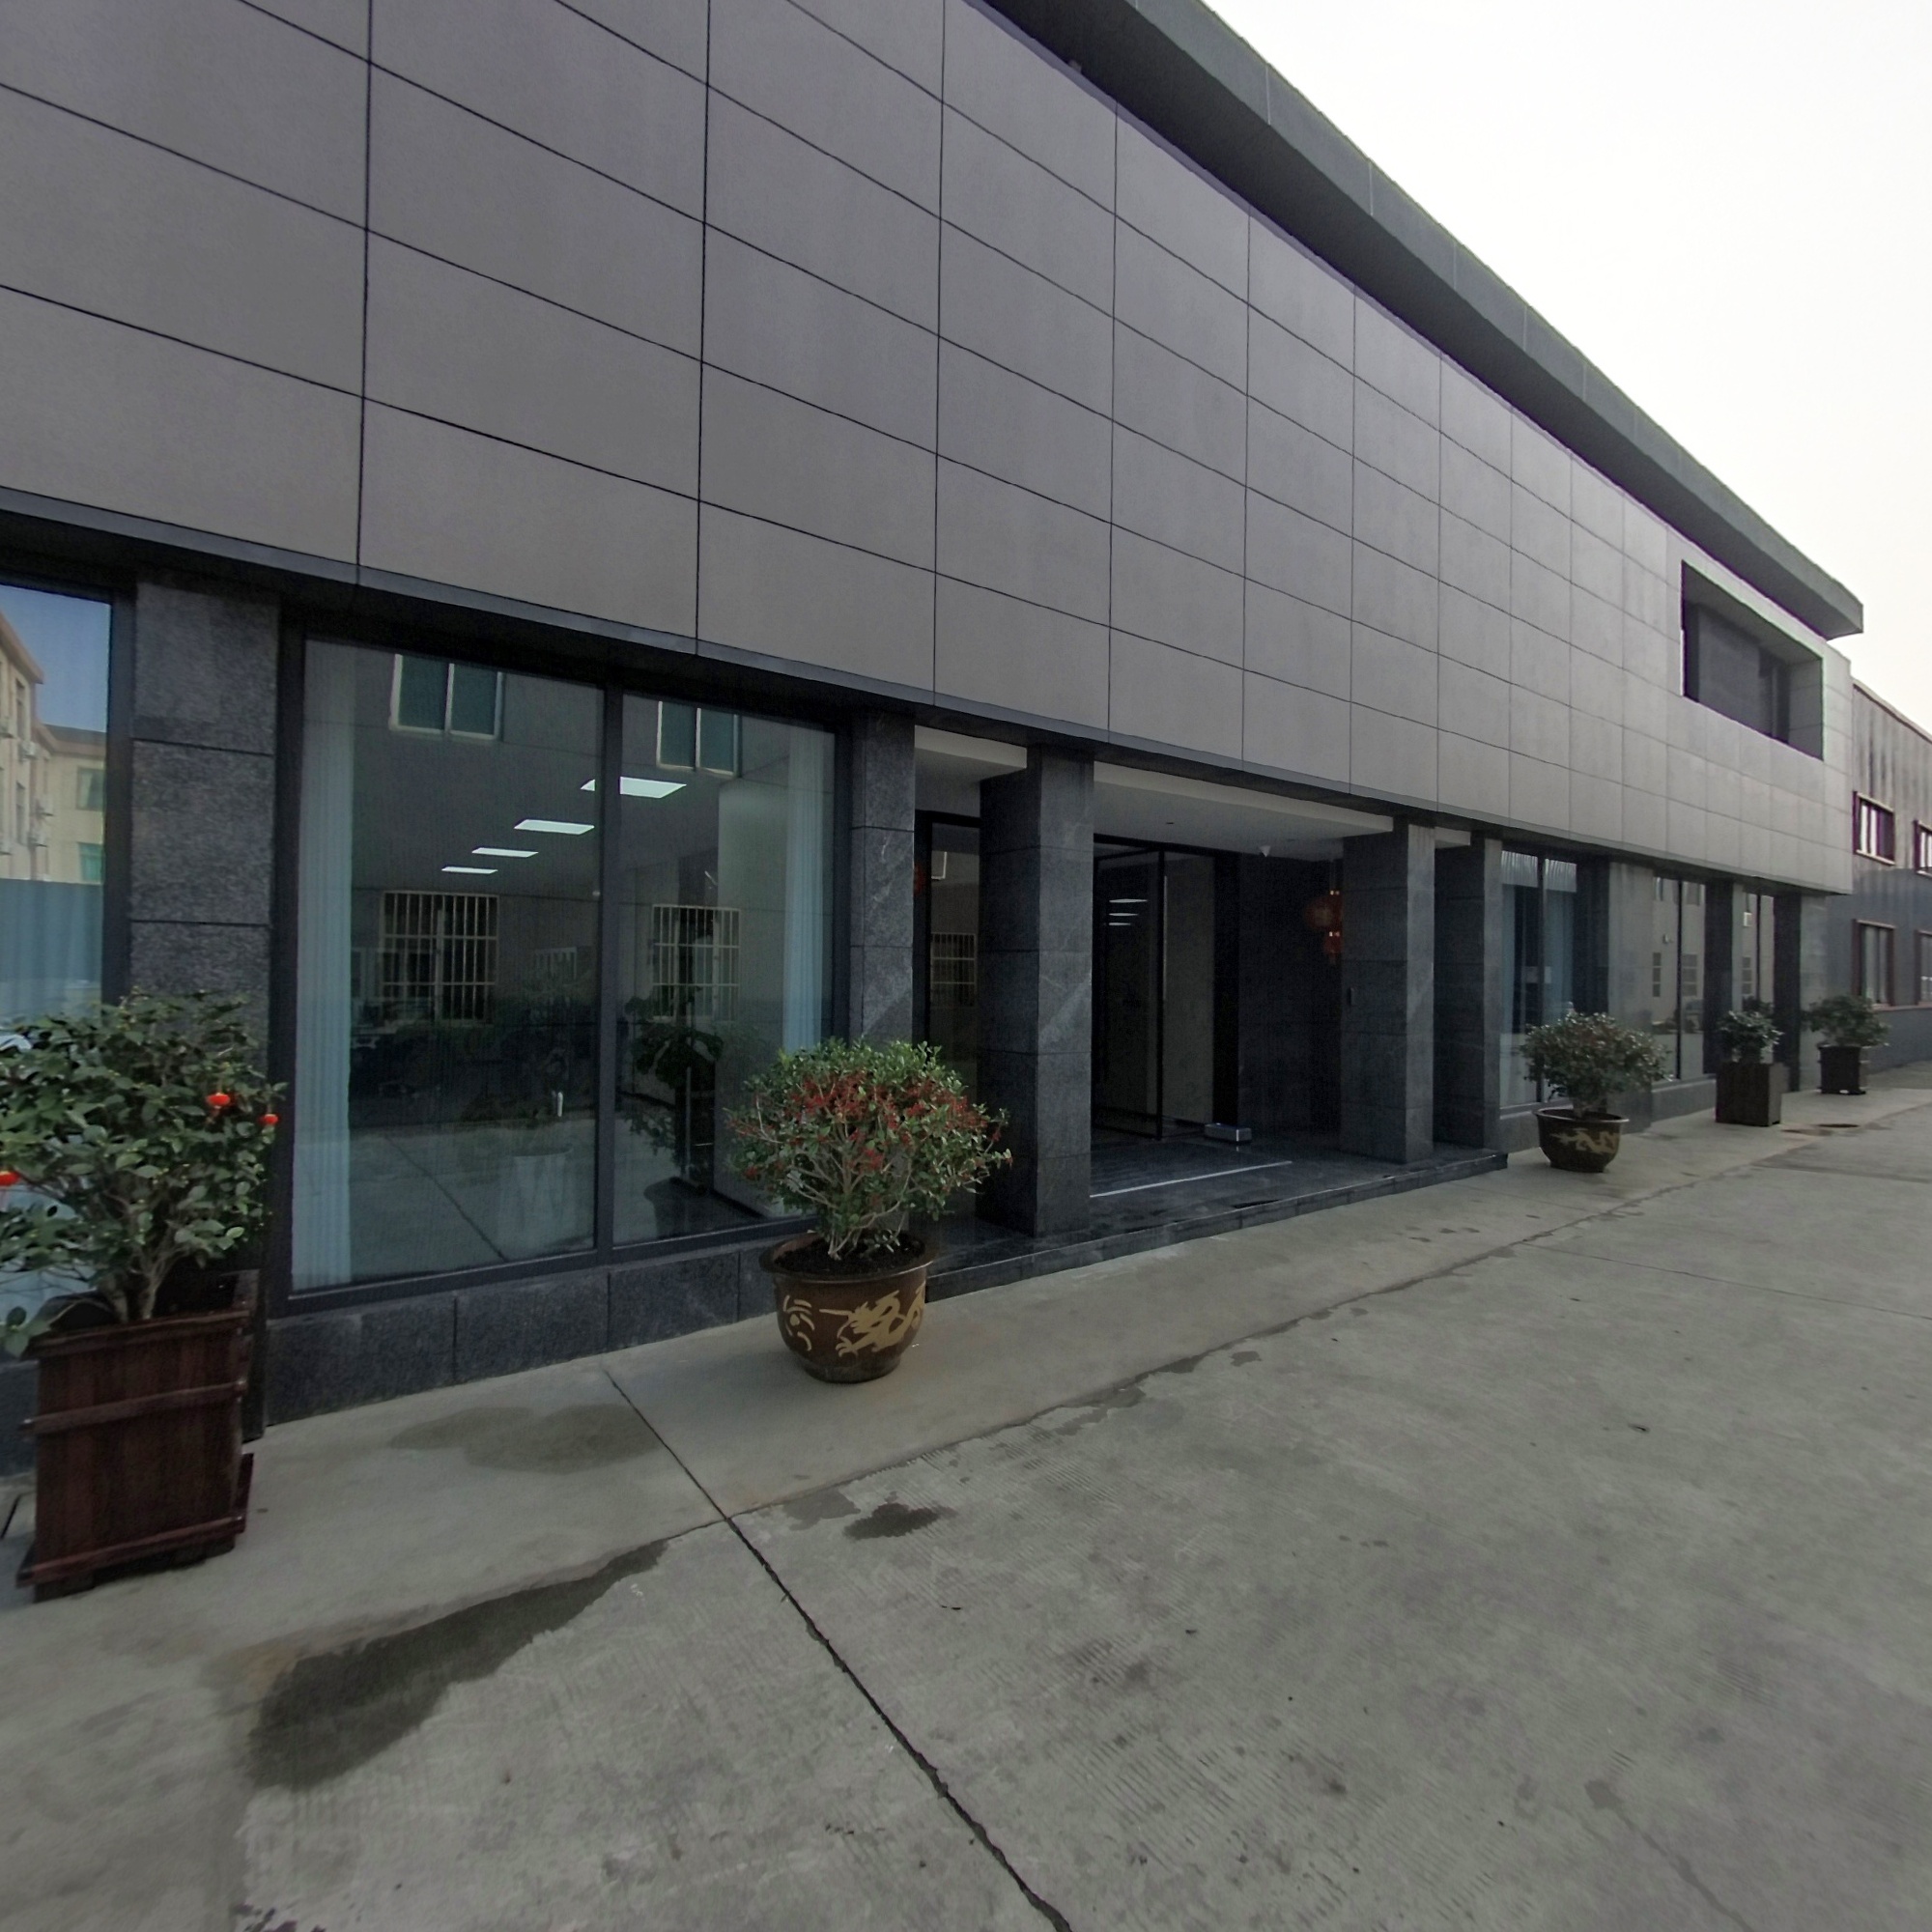
Verify our production scale, modern sintering presses, and testing equipment remotely before finalizing contracts.
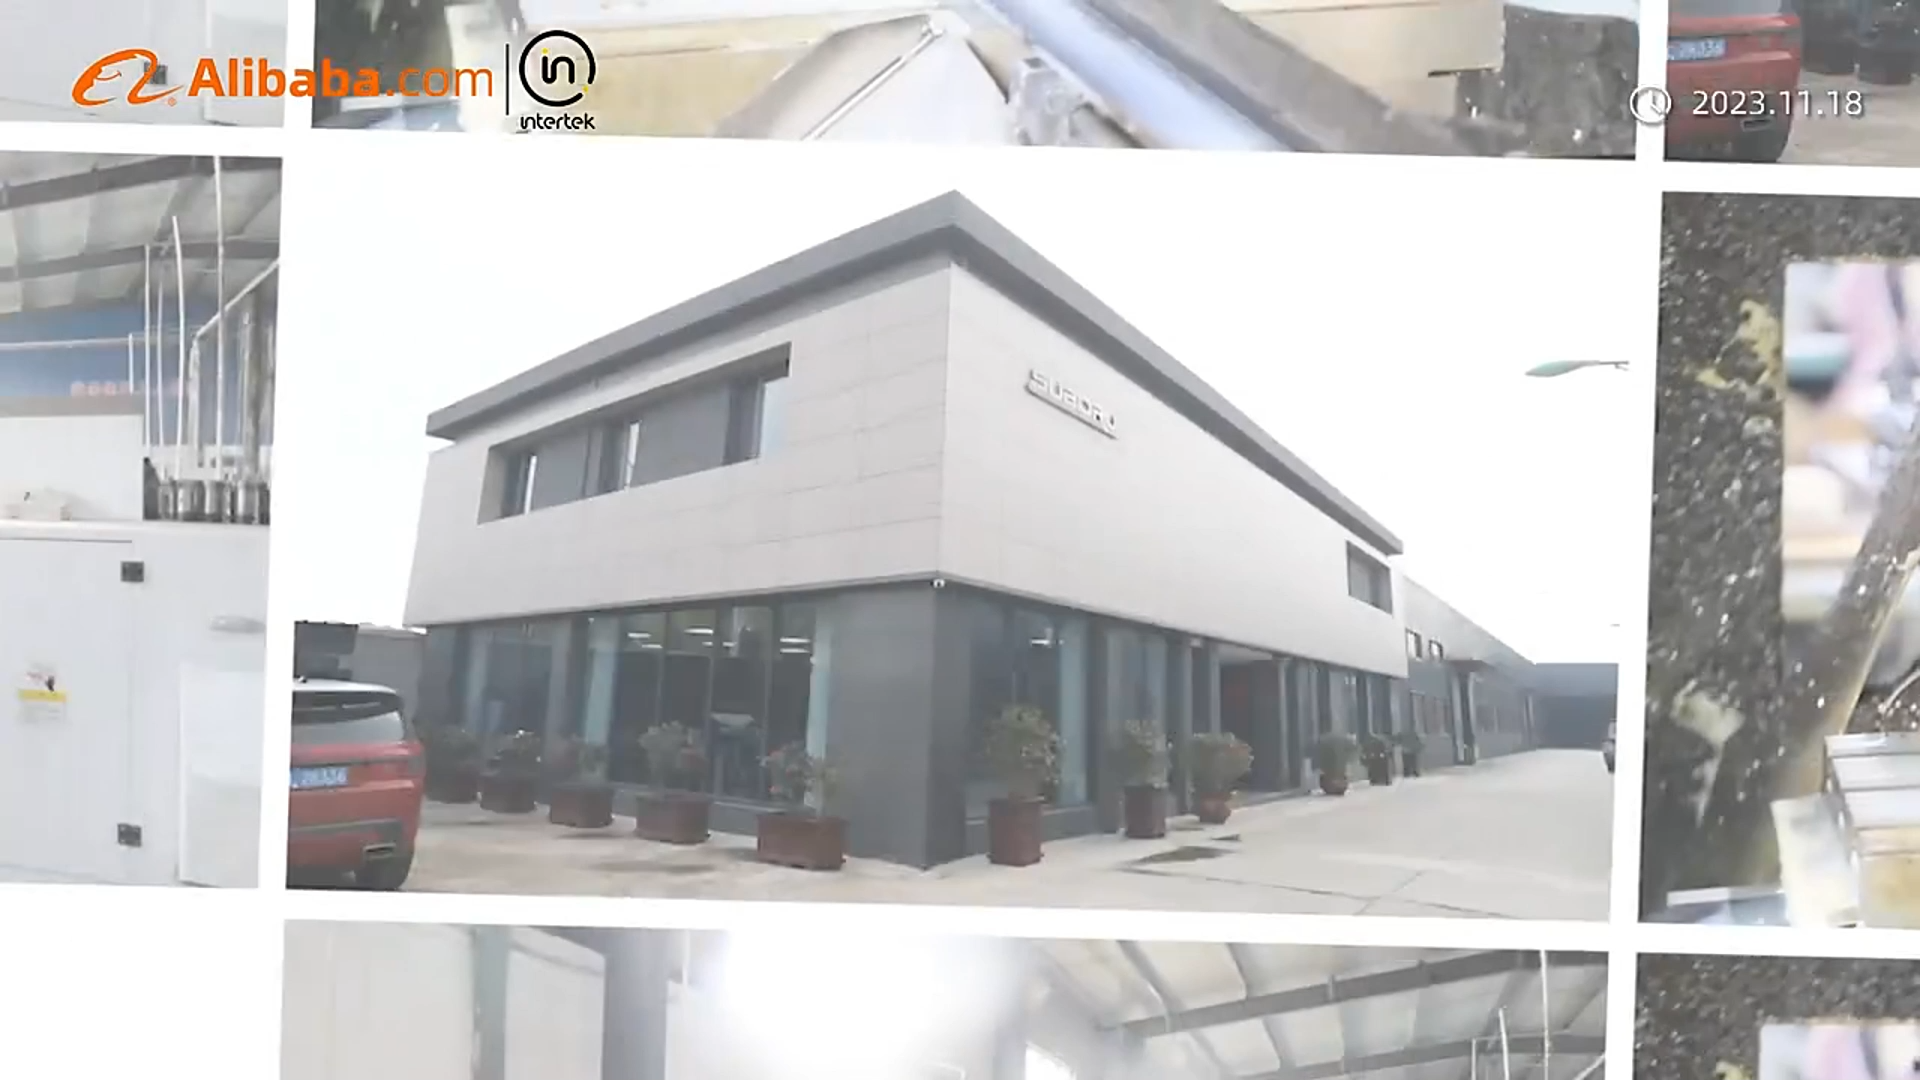
All laboratory metallography data, Intertek factory audit credentials, and ISO9001 compliance sheets are available on request.
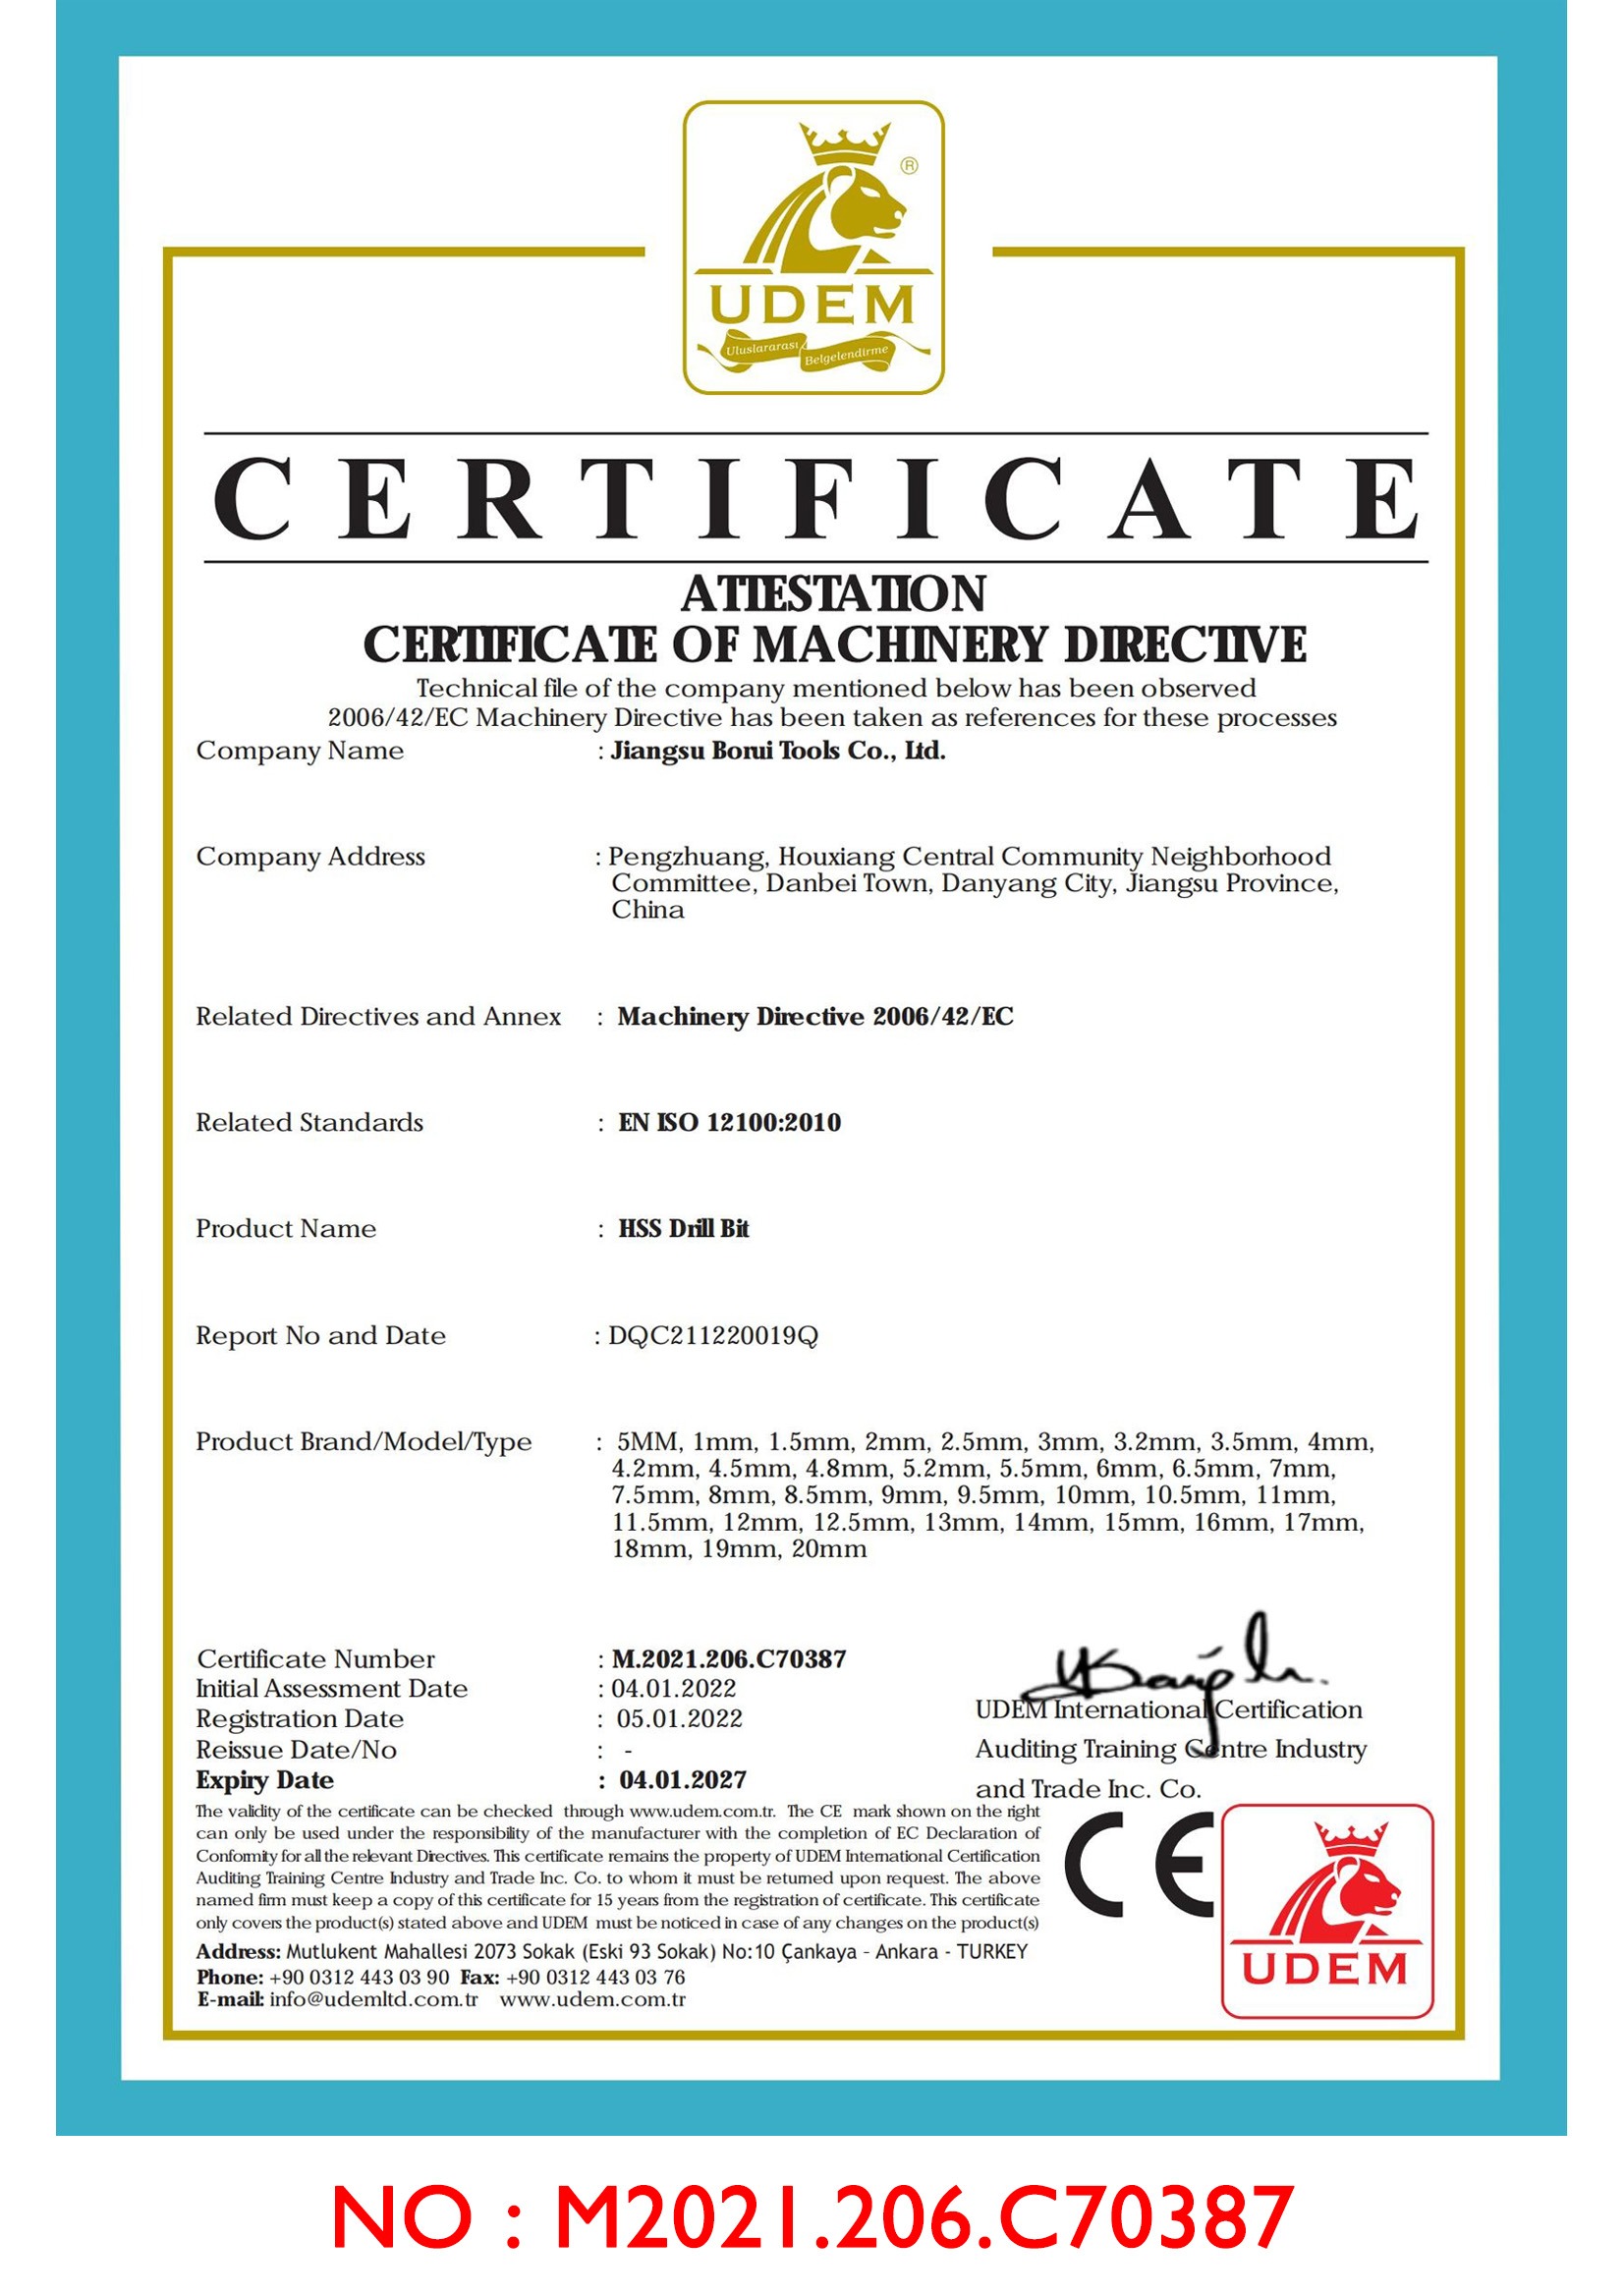
International standards and quality credentials ensure smooth customs clearance and hassle-free retail distribution worldwide.
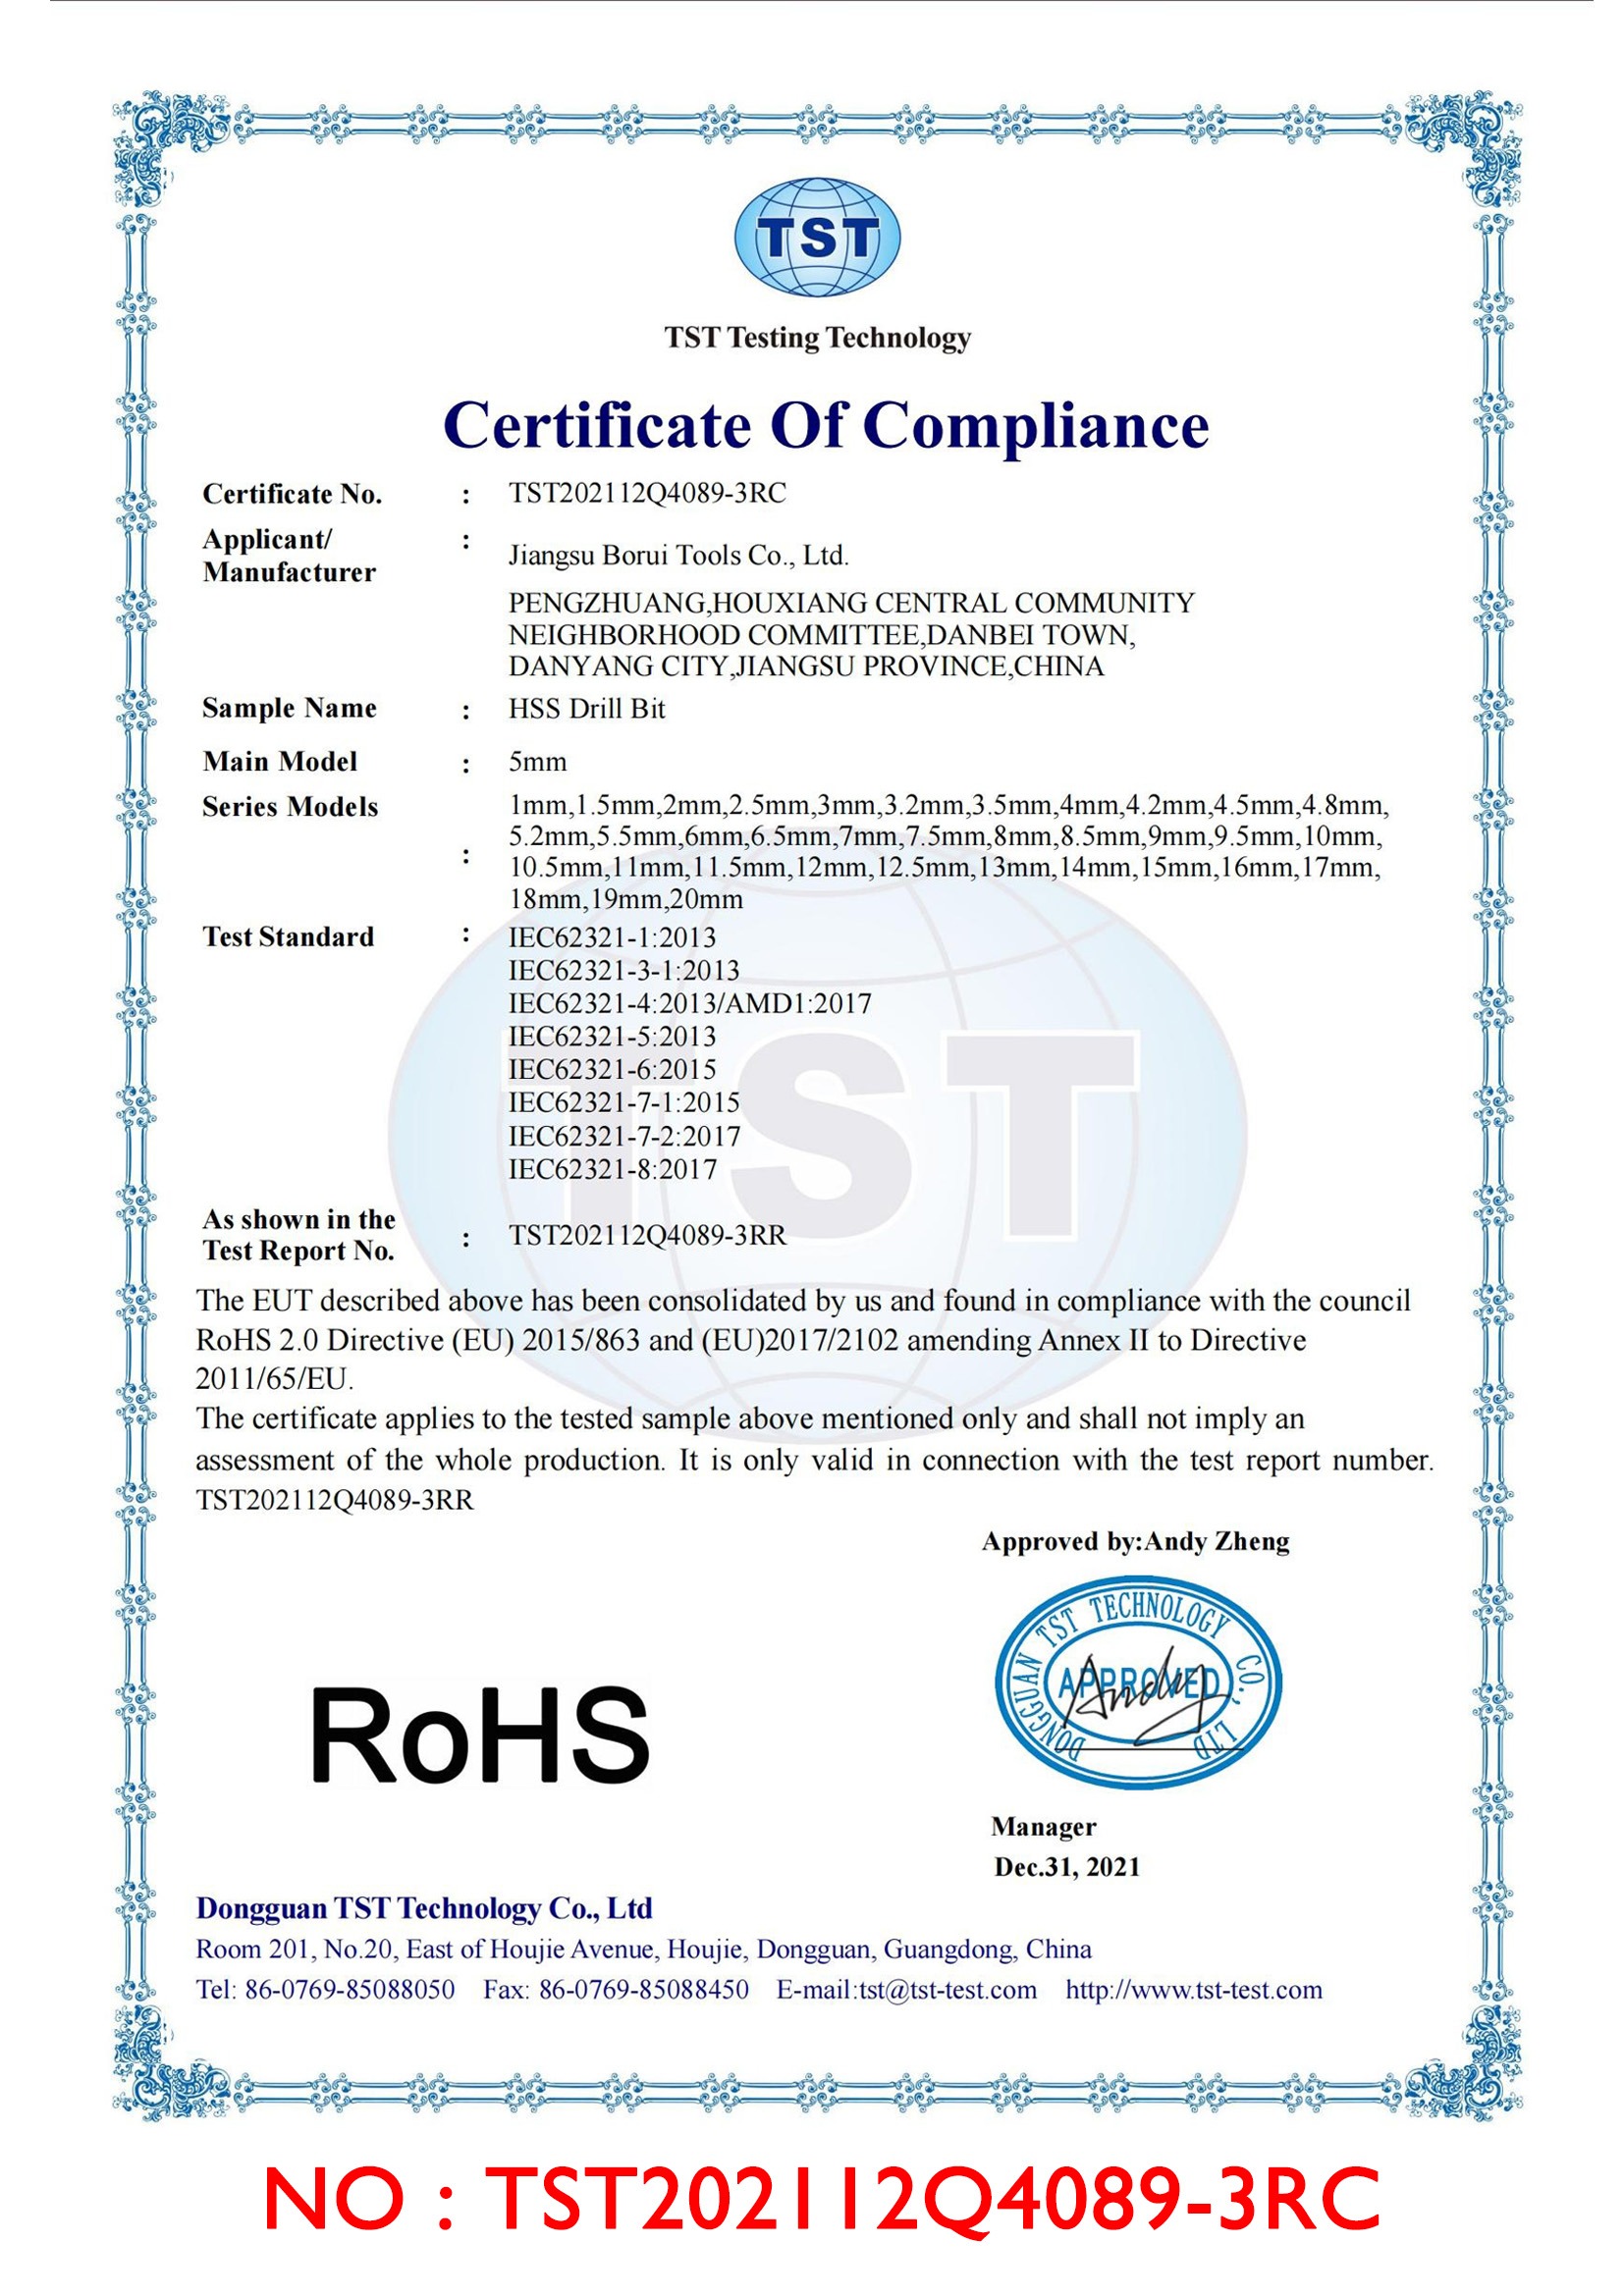
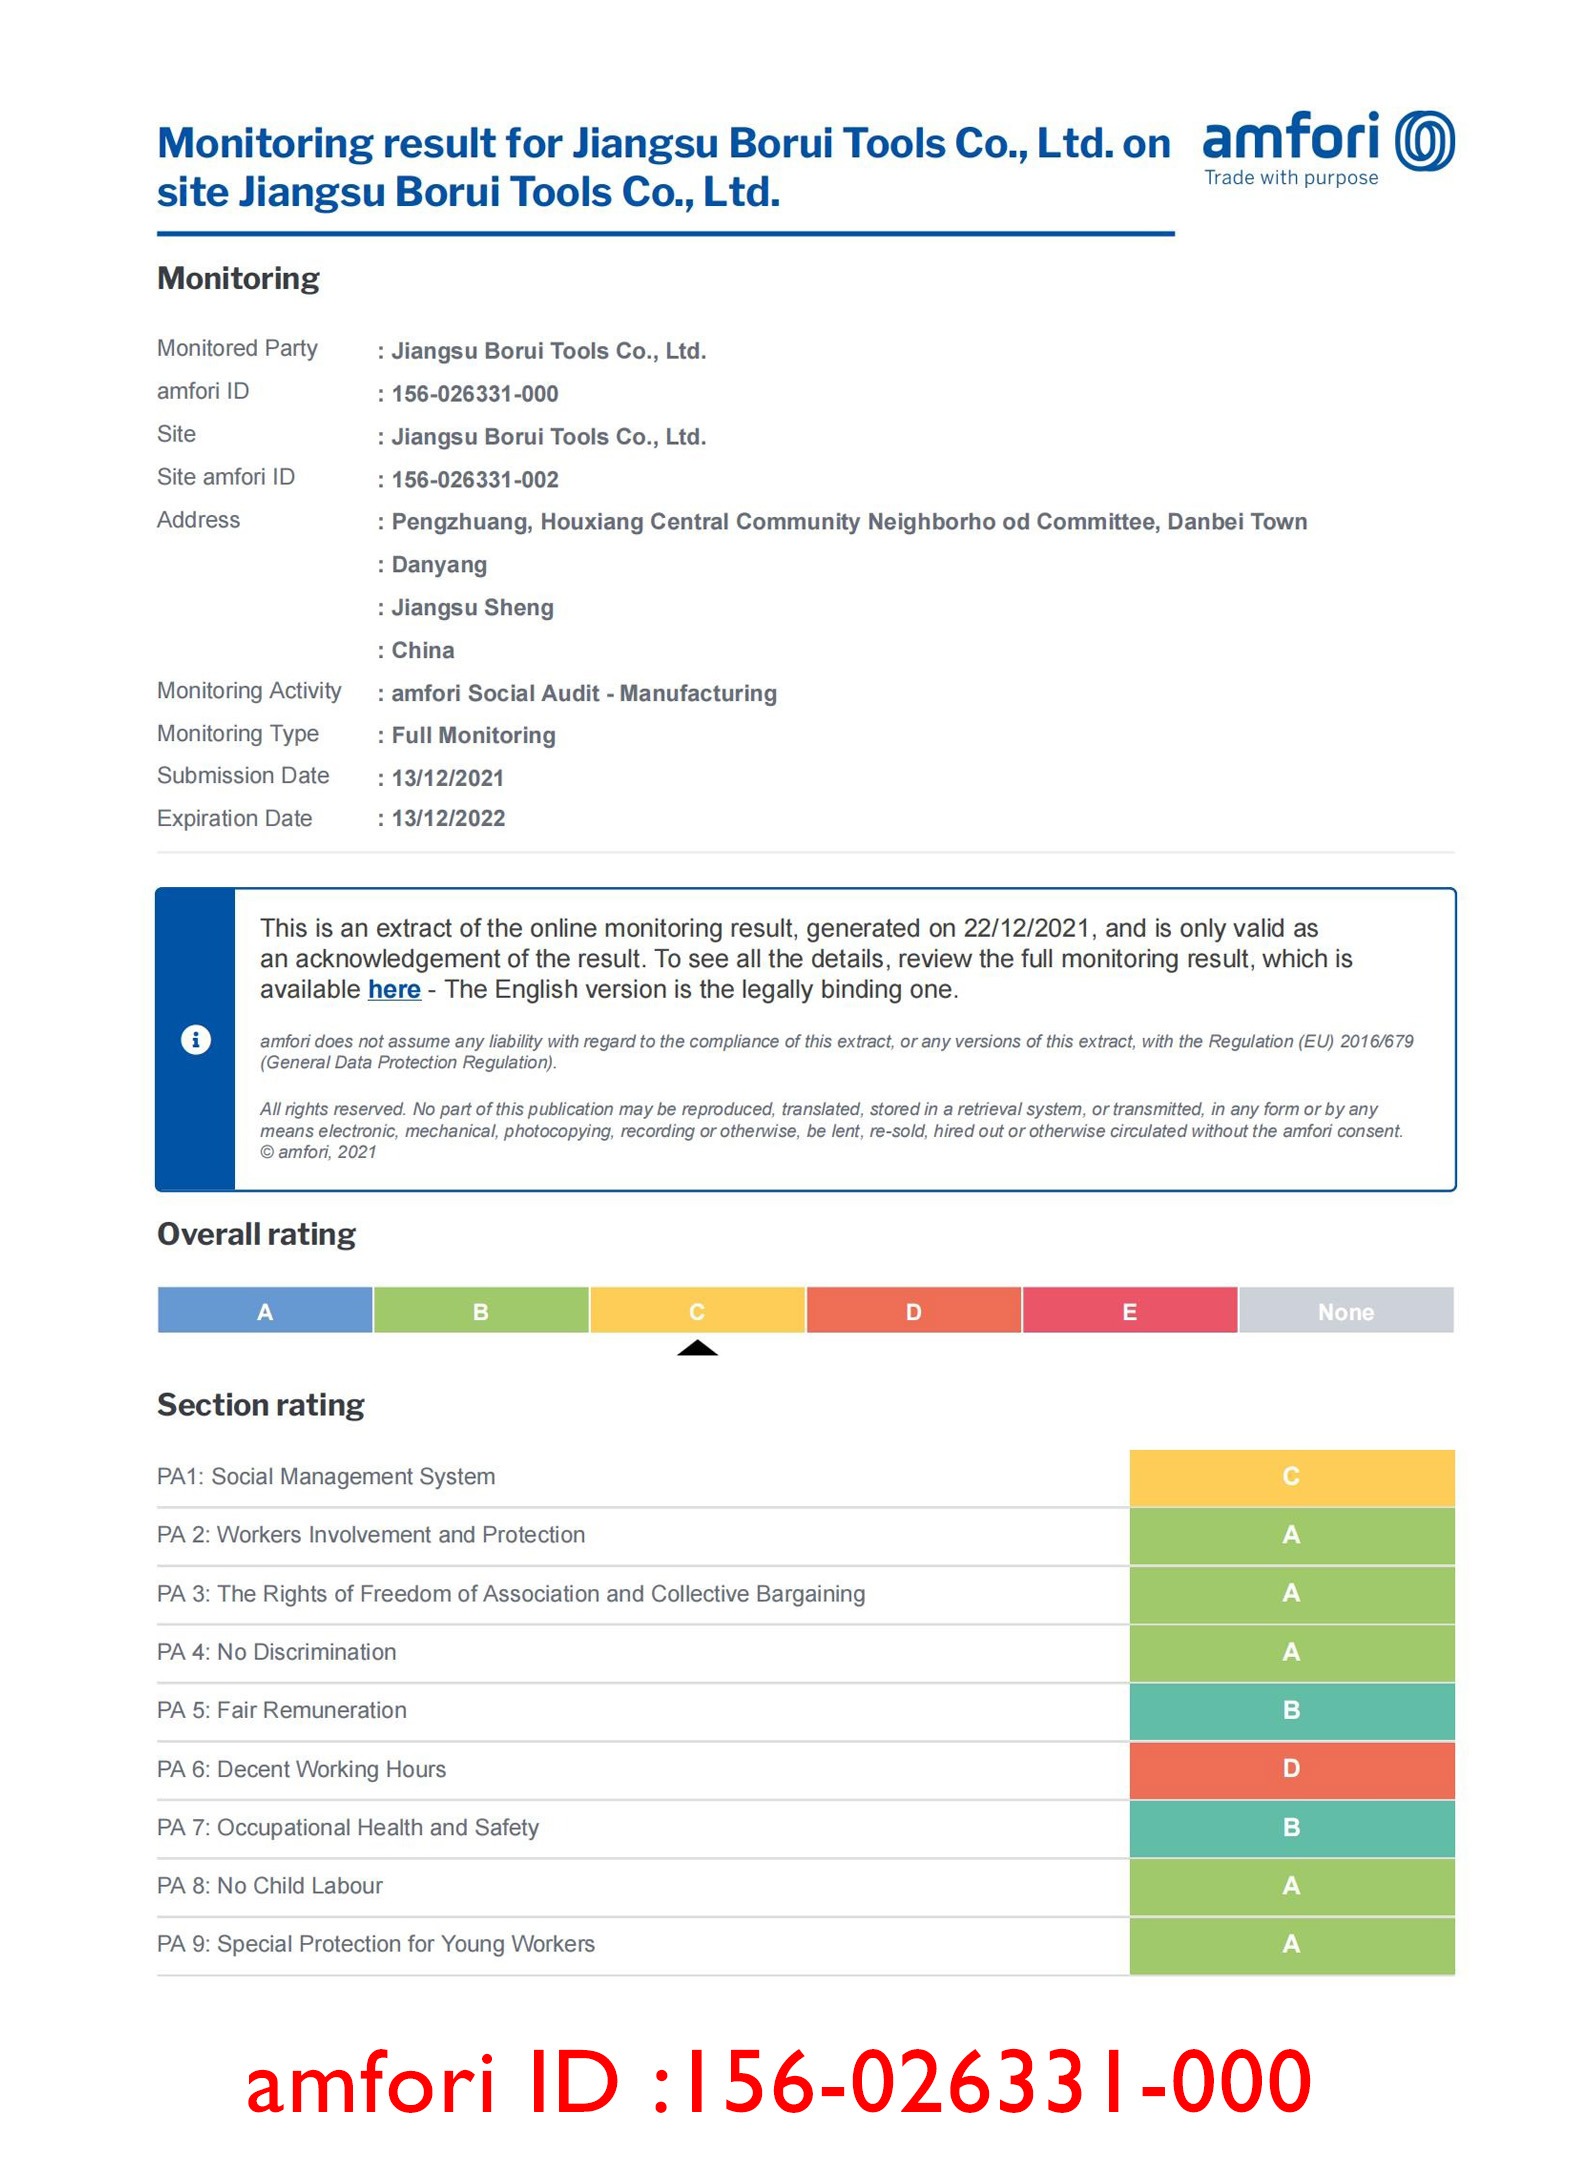
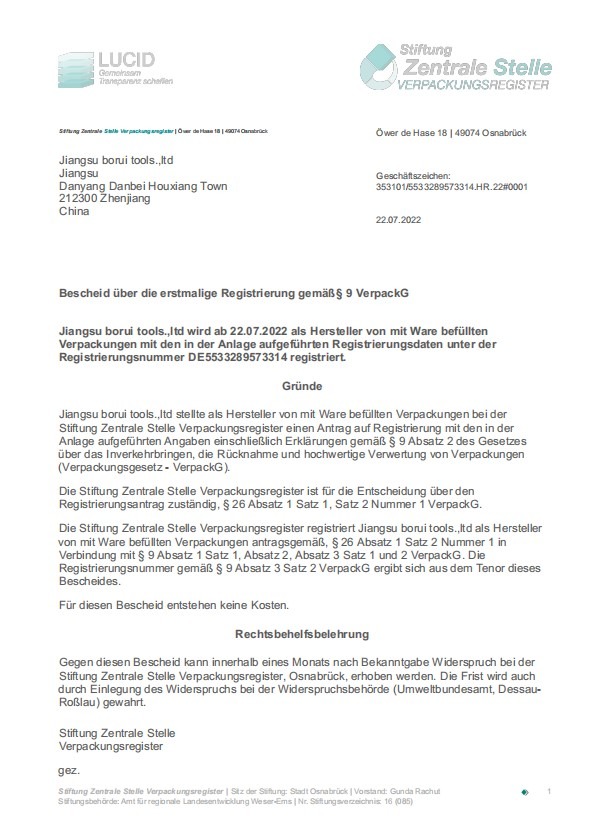
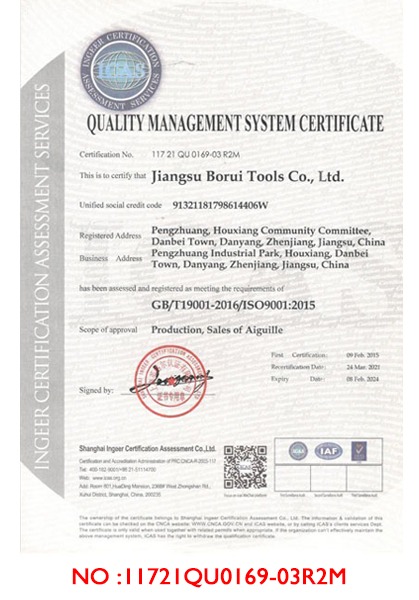
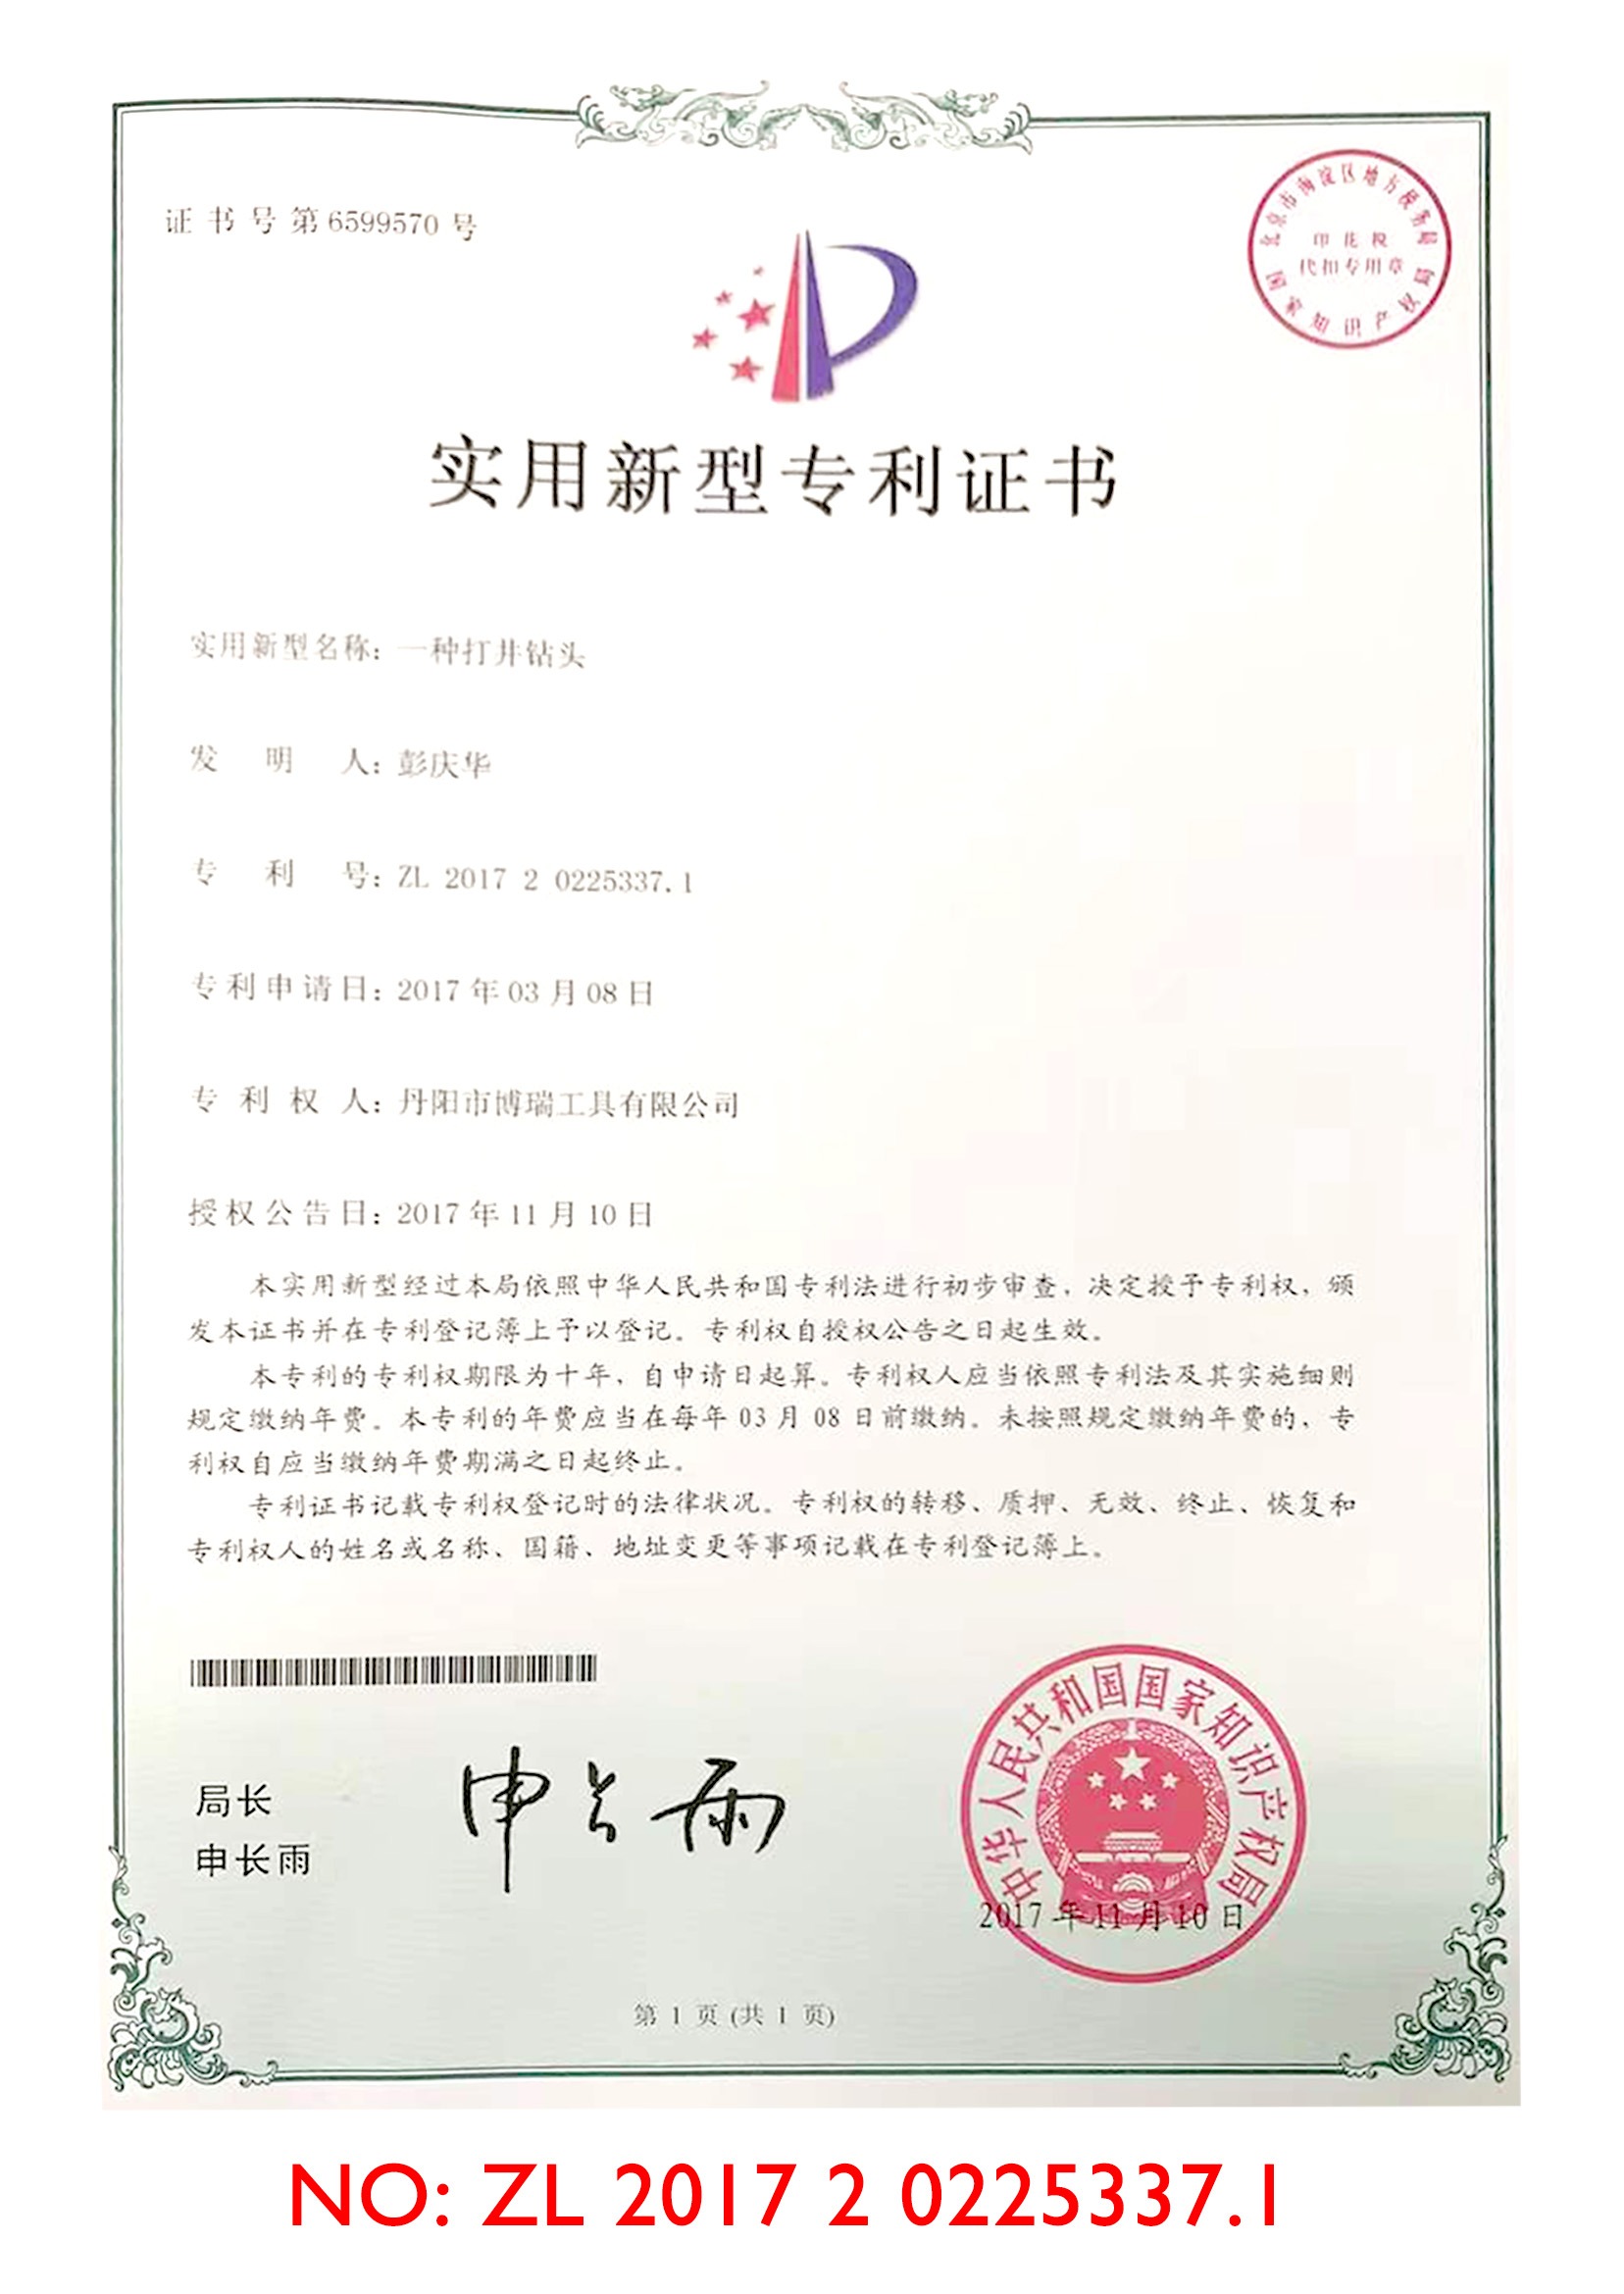
Consult this procurement matrix to match diamond concentration, bond hardness, and rim geometry directly to your local market needs.
| Bond Matrix | Material To Cut | Shedding Behavior |
|---|---|---|
| Soft Bond | Granite, Quartz, Hard Porcelain | Fast erosion exposes fresh crystals |
| Medium Bond | Marble, Cured Brick, Engineered Stone | Balanced service life and cutting speed |
| Hard Bond | Green Concrete, Abrasive Asphalt, Sandstone | Retains diamonds against abrasive scouring |
| Segment Spec | Kerf Range | Target Application |
|---|---|---|
| 7 mm – 8 mm | 2.0 mm – 2.4 mm | Economical retail construction tools |
| 10 mm Industrial | 1.8 mm – 2.2 mm | Professional masonry & tile installation |
| 12 mm – 15 mm Premium | 1.2 mm – 1.6 mm | Deep plunge commercial marble and slab cutting |
| Arbor Mount | Flange System | Compatible Tools |
|---|---|---|
| 22.23 mm (7/8") | Standard Center | Global angle grinders & tile cutters |
| M14 / 5/8"-11 | Threaded Direct Flange | Quick-change flush trimming tools |
| 25.4 mm (1") | Reinforced Center | High-power wet bridge saws & masonry tables |
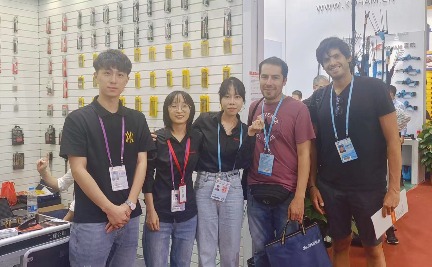
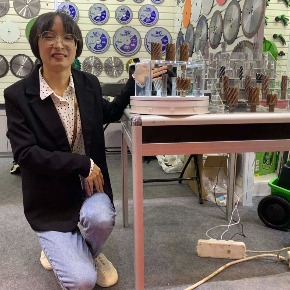
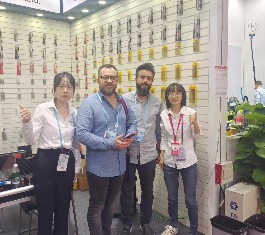
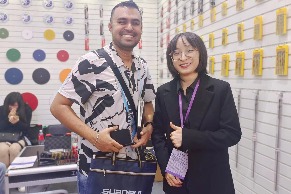
Tool brand directors, wholesale buyers, and supply chain managers regularly audit our Danyang facilities in person. Our products are exported to Germany, the United States, Switzerland, Sweden, and more than 20 countries worldwide.
Common technical questions asked by global procurement teams and AI sourcing agents regarding turbo diamond saw blades.
A turbo rim diamond saw blade combines the rapid material evacuation and cooling vents of a segmented blade with the clean, smooth edge quality of a continuous rim. The corrugated serrations actively channel away slurry and hot dust while generating continuous micro-fractures in hard stone and vitreous ceramics, preventing thermal overheating without aggressive chipping.
Jiangsu WRD Tools Co., Ltd. manufactures turbo rim blades via vacuum hot-pressing and laser segment fusion, allowing versatile dry-cutting applications where airflow generated by the serrated corrugation cools the core. However, supplementary water cooling substantially extends blade working life, eliminates hazardous silica dust, and creates glass-smooth finishes.
Diamond mesh specifies particle dimension: coarse grit (30/40 to 40/50 mesh) facilitates high-speed aggressive cutting in abrasive concrete, while fine grit (60/70 to 80/100 mesh) produces chip-free margins in hard vitreous tiles. Crucially, hard minerals like granite and dense quartz necessitate soft bronze/cobalt matrices to expose fresh diamonds, whereas softer, abrasive concrete requires hardened tungsten/iron bonds to prevent premature wear.
We utilize laser-cut 65Mn or 75Cr1 high-carbon alloy core blanks that undergo rigorous tension balancing and precision heat treating. Additionally, our premium turbo blade product series incorporate reinforced integrated center flanges and laser-cut expansion keyholes, suppressing vibration harmonics and retaining flatness under excessive thermal loads.
We offer end-to-end B2B customization including custom diamond segment heights (up to 15mm), laser etched logos, personalized core paint/coatings, bore adapters, and customized retail presentation ranging from double-blister clamp packs to magnetic gift box kits and bulk master cartons.
Send drawings, substrate requirements, or OEM packaging files. Our technical team replies with full quotations within 24 hours.
 IrisExport Manager
 AaronExport Manager
 CynthiaExport Manager
 WillieExport Manager
 AbbyExport Manager
 VictorExport Manager