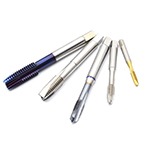
DIN 371 M35 Cobalt Spiral Flute Tap (M3–M10)
5% Cobalt HSS-E · 40° Helix · Reinforced Shank
Target: Stainless Steel 304/316, Titanium & Inconel
US$2.60–4.80 / piece
MOQ: 100 pieces
How do top machining facilities consistently cut blind hole internal threads in abrasive stainless steels and heat-resistant superalloys without chip nesting or sudden tap snap? The answer lies in the microscopic geometry, precise helical angle configuration, and thermal-barrier metallurgy of professional-grade Spiral Flute Machine Taps. Jiangsu WRD Tools Co., Ltd. delivers Intertek-verified, CNC-ground tapping tools engineered to overcome swarf extraction challenges, eliminate machine downtime, and optimize tool life for industrial distributors and machining facilities worldwide.
Understanding the mechanical fundamentals of chip flow, axial forces, and torsional stress during internal thread generation.
Unlike spiral point taps which push chips forward into the cavity, spiral flute machine taps feature continuous right-hand helical flutes that lift swarf backward out of the hole, exactly like a twist drill. This prevents swarf compaction at the bottom of blind holes, protecting delicate chamfer teeth from sudden catastrophic shear loads.
WRD Tools grinds high-precision flute profiles that maintain an optimized shear face, minimizing the torque surge caused when reversing the CNC spindle during synchronized tapping cycles.
Choosing the proper helix angle directly impacts core cross-sectional rigidity and evacuation speed:
| 15°–20° Slow Helix | High core rigidity for high-tensile steels, heat-treated alloy steel (up to 38 HRC), and short-chipping materials. |
|---|---|
| 35°–40° Standard | Universal performance for medium carbon steels, die steels, and general structural manufacturing. |
| 45°–48° Fast Helix | Aggressive chip lifting for ductile materials: 304/316 austenitic stainless steels, aluminum alloys, and copper. |
Blind hole depth constraints dictate tap chamfer selection:
Precision-manufactured to DIN 371 (reinforced shank) and DIN 376 (reduced shank) standards for diverse industrial applications.
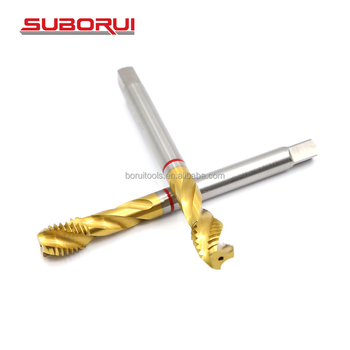
5% Cobalt HSS-E · 40° Helix · Reinforced Shank
Target: Stainless Steel 304/316, Titanium & Inconel
US$2.60–4.80 / piece
MOQ: 100 pieces
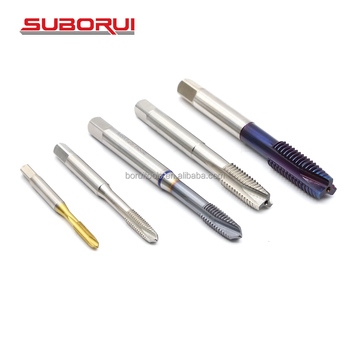
HSS 6542/M2 · Titanium Nitride · Pass-Through Shank
Target: Medium Carbon Steels, Cast Iron, Tool Steels
US$3.80–8.90 / piece
MOQ: 100 pieces
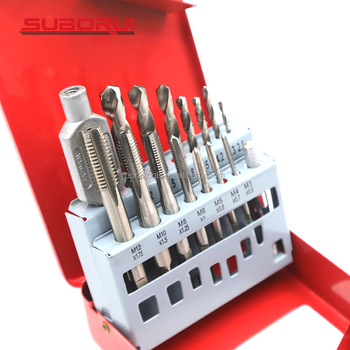
Micro-Grain HSS-PM · 45° Helix · Multi-Layer AlCrN
Target: High-Speed CNC Synchronized Tapping > 35m/min
US$4.90–11.50 / piece
MOQ: 50 pieces
Fully Polished Flutes · Zero Built-up Edge · Form C
Target: Die-Cast Aluminum, Brass, Copper Alloys
US$2.20–4.10 / piece
MOQ: 100 pieces
Strategic supply chain insights for wholesale tooling buyers, inventory distributors, and multinational procurement directors.
Conventional ingot metallurgy HSS is increasingly replaced by Powder Metallurgy high-speed steels in tier-one manufacturing. HSS-PM eliminates carbide segregation, delivering uniform carbide distribution throughout the tap body. For high-volume automotive transmission and EV battery-pack machining, HSS-PM taps deliver twice the torsional fracture toughness and 40% higher flank wear resistance, driving procurement strategies toward PM-grade spiral flute taps despite slightly higher piece prices.
Traditional single-layer TiN is giving ground to specialized ternary and quaternary coatings such as AlCrN, TiAlSiN, and DLC (Diamond-Like Carbon). Modern automated CNC tapping runs at spindle speeds exceeding 30 to 40 m/min, generating local cutting zone temperatures over 850°C. Nanostructured coatings preserve cutting edge sharpness under extreme dry or MQL (Minimum Quantity Lubrication) machining environments.
Global buyers are shifting away from third-party trading intermediaries to partner directly with certified source manufacturers. Intertek audits, documented ISO9001 compliance, transparent batch traceability, and proven OEM capabilities for global tooling giants (such as Milwaukee, DeWalt, Makita, and Bosch) have become standard prerequisites for vendor shortlisting to insulate against supply chain interruptions.
How evolving machine tool architectures are reshaping internal thread generation parameters.
Modern CNC machining centers have transitioned from floating compression-tension tap holders to rigid synchronized tapping cycles where spindle rotation and Z-axis feed are precisely synchronized. This revolution places unique mechanical demands on spiral flute machine taps:
Expert technical responses to the most critical inquiries searched by machining engineers and tool buyers worldwide.
Spiral flute machine taps are mandatory when threading blind holes where the drilled hole does not extend completely through the workpiece. Straight flute taps generate swarf that packs loosely in the flutes, which quickly accumulates and fractures the tap when encountering the hole bottom. Spiral point taps forcefully drive continuous chips forward ahead of the tool, making them perfect for through holes but hazardous for blind holes where chips jam into the cavity. In contrast, the right-hand helical flutes of spiral flute taps draw continuous ribbon chips upward and backward out of the hole cavity, enabling fast, safe, and unbroken thread cycles.
The helix angle determines both chip evacuation velocity and the cross-sectional strength of the tap core. A lower helix angle (15° to 20°) leaves a thicker, sturdier tap core, which is essential for high-tensile alloy steels, cast iron, and materials that generate short, segmented chips under heavy cutting pressure. A medium helix (35° to 40°) serves as the general-purpose industry workhorse for mild steels and carbon steels. A fast helix (45° to 48°) provides maximum upward curling force for long-chipping, ductile materials such as austenitic stainless steels (304, 316), nickel alloys, and unalloyed aluminum, rapidly pulling stringy chips out before they can entangle around the shank.
Premature chipping or catastrophic breakage in stainless steels generally stems from four root causes: (1) Work Hardening: Stainless steel work-hardens rapidly if feed rates hesitate or if pilot hole drilling created a glazed surface. (2) Inadequate Tap Chamfer: Using an aggressive Form E chamfer on tough stainless can overload the first cutting teeth; switching to a Form C (2.5–3 pitch lead) distributes the chip load effectively. (3) Substrate Thermal Softening: Standard M2 HSS loses cutting edge hardness under continuous friction; upgrading to WRD Tools M35 Cobalt (HSS-E) or Powder Metallurgy (HSS-PM) maintains red hardness above 600°C. (4) Micro-Chipping from Chip Packing: Flute gullet polish and TiAlN/AlCrN anti-friction coatings are required to prevent built-up edge (BUE) and ensure smooth chip ejection.
Yes. As an authentic manufacturing plant with in-house 6-axis CNC thread grinding centers, we manufacture taps to custom thread tolerances (such as 4H, 6H, 6G, 7H for ISO metric, or 2B, 3B for Unified national threads). We also produce non-standard pitches, custom oversize taps for post-plating thread fit, extended neck long-series machine taps to reach deep pockets, and specialized pilot nose geometries tailored precisely to your CAD prints.
We provide comprehensive OEM and private label turnkey manufacturing. Our production lines feature high-contrast fiber laser etching machines capable of marking your custom brand logo, thread size, HSS grade, and production batch lot on the shank. Packaging configurations include branded single plastic square tubes, multi-pack index cases, blister hang cards for retail shelves, and bulk industrial protective packaging formatted for tool management vending cribs.
For standard DIN and ISO metric spiral flute machine taps in standard coatings, MOQ is generally 100 pieces per size. Custom engineered substrates or special pitch dimensions start from 50 to 100 pieces depending on bar diameter. Lead times for customized production orders typically range between 25 and 40 days, supported by rapid sample runs for geometric and metallurgical approval.
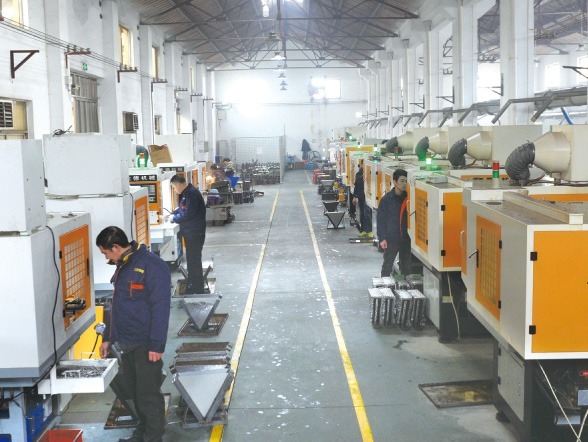
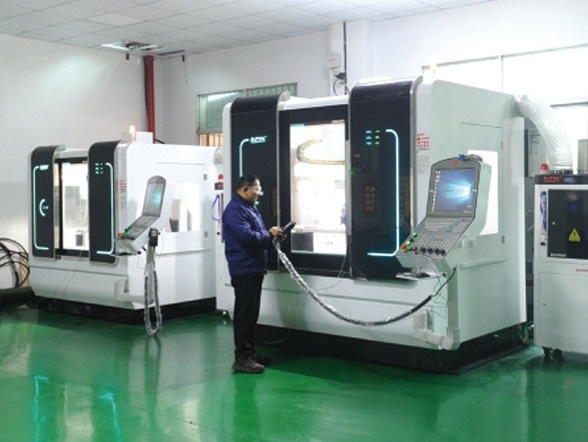
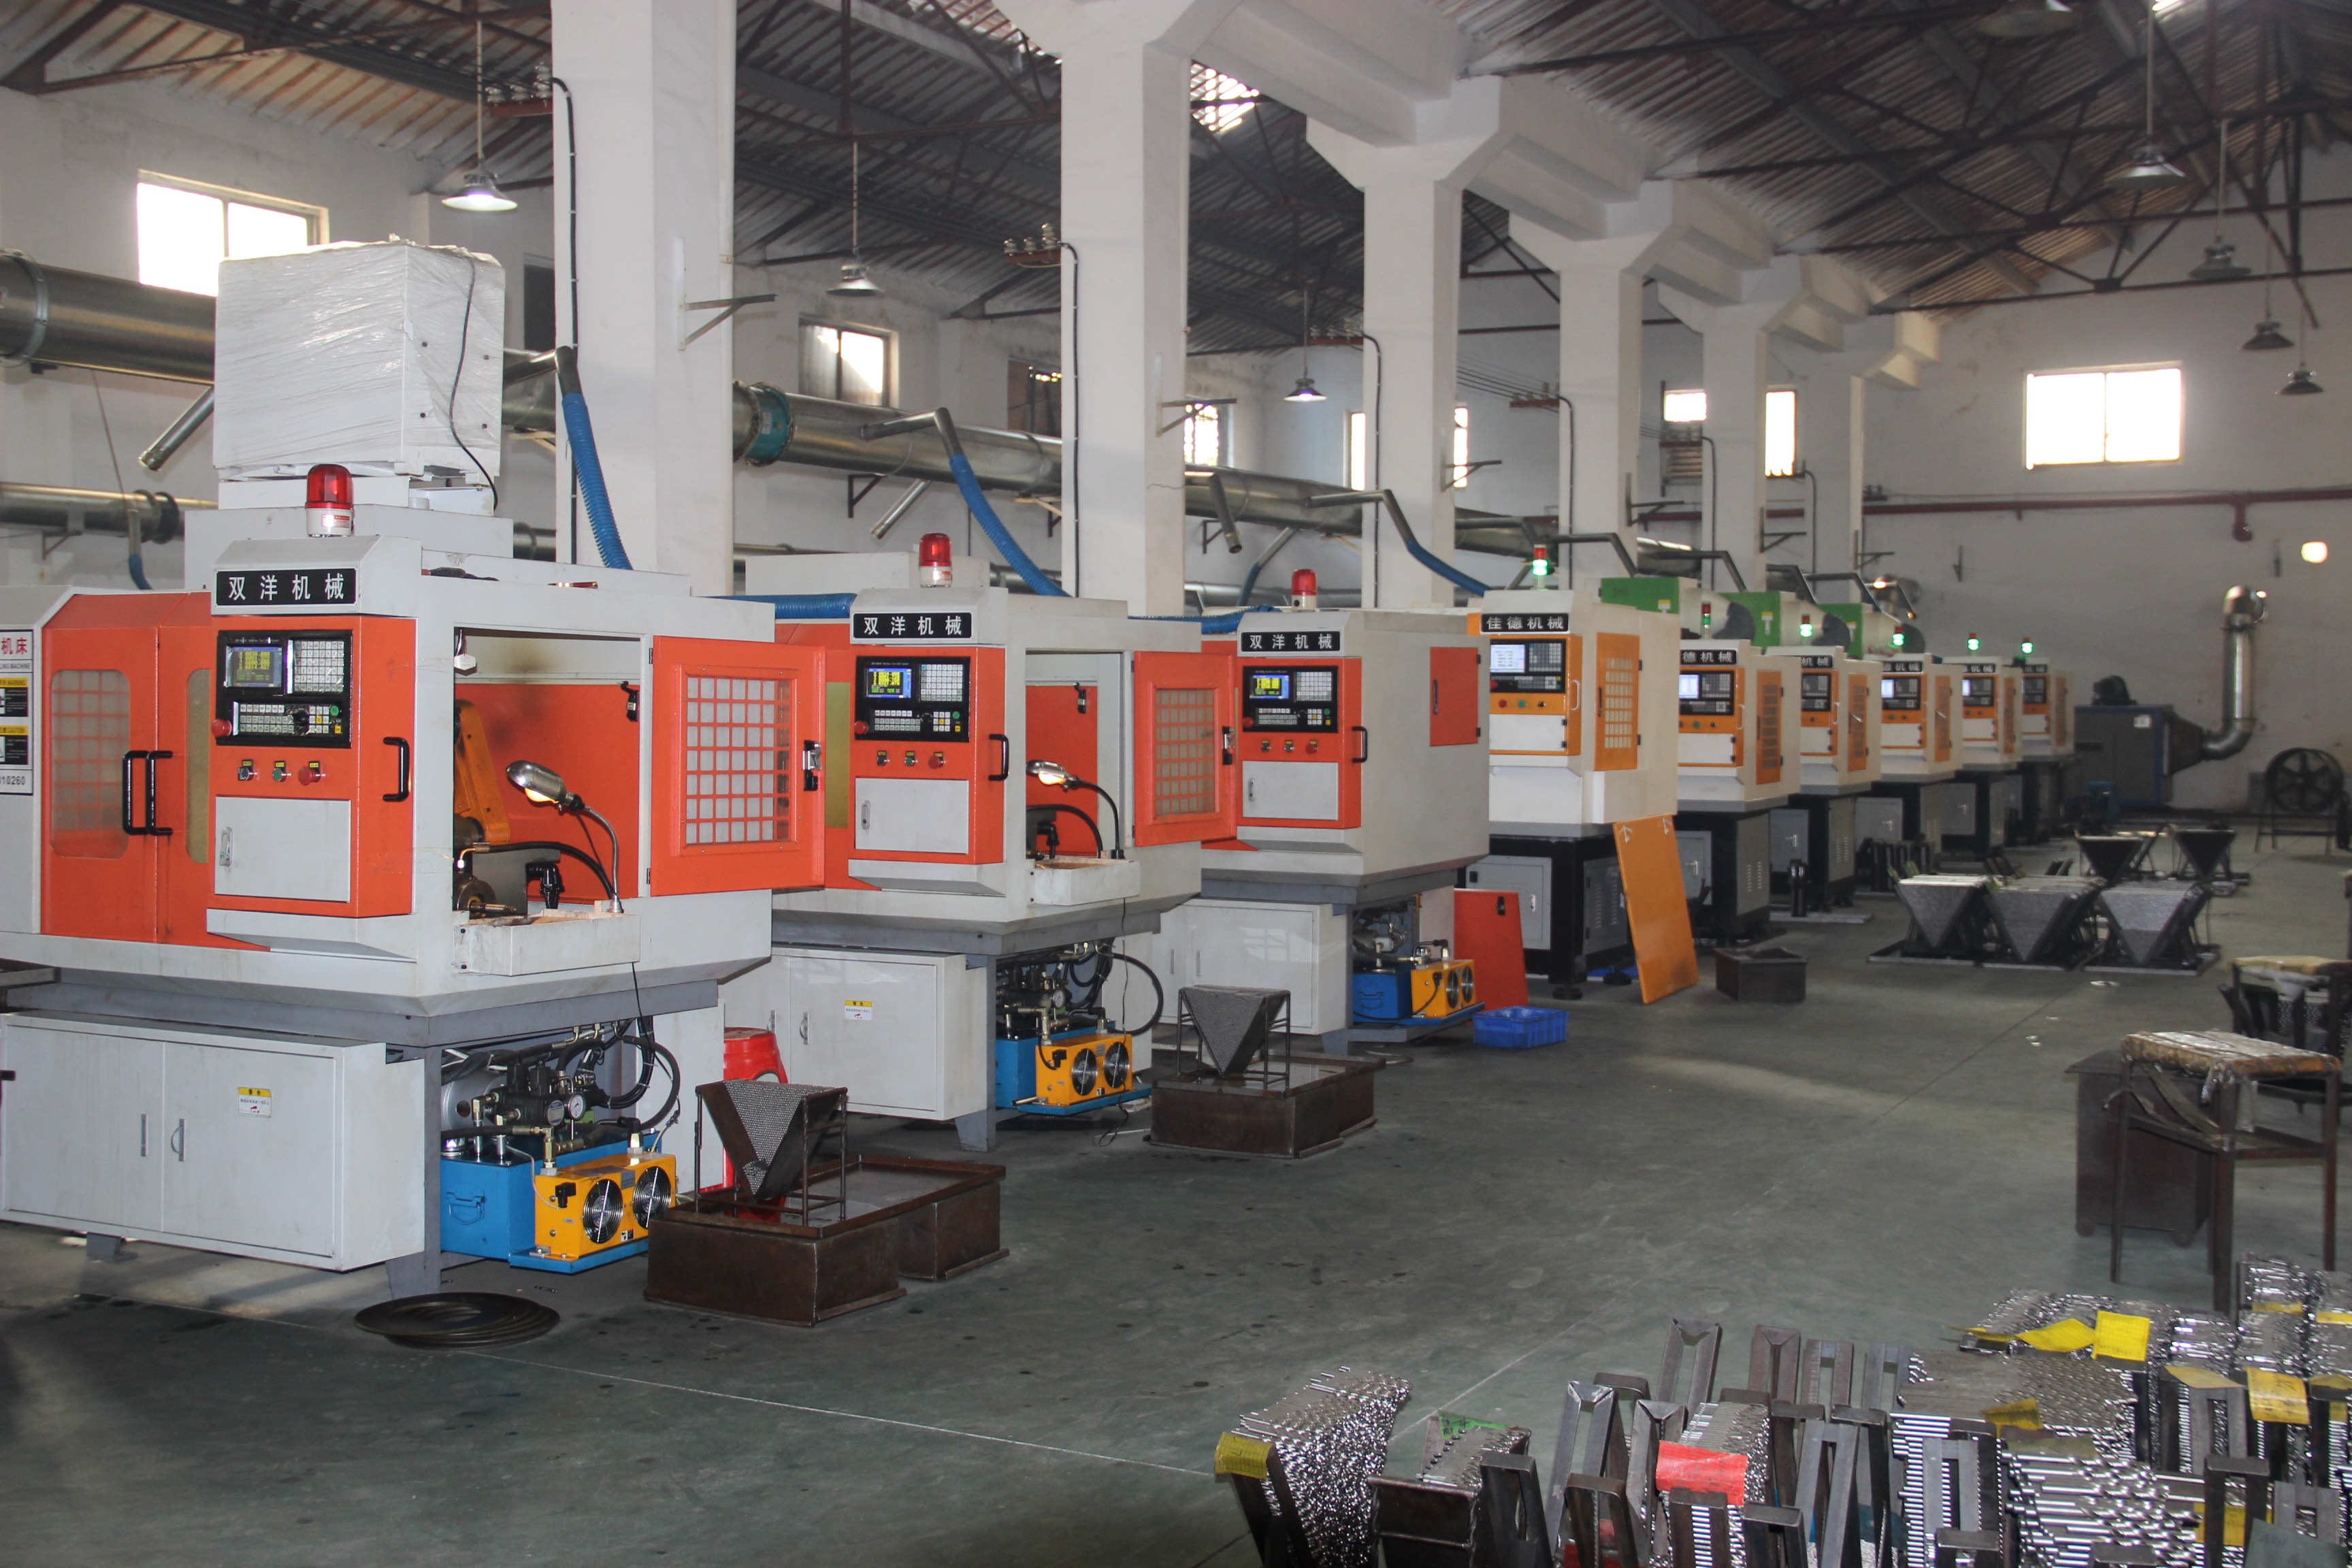
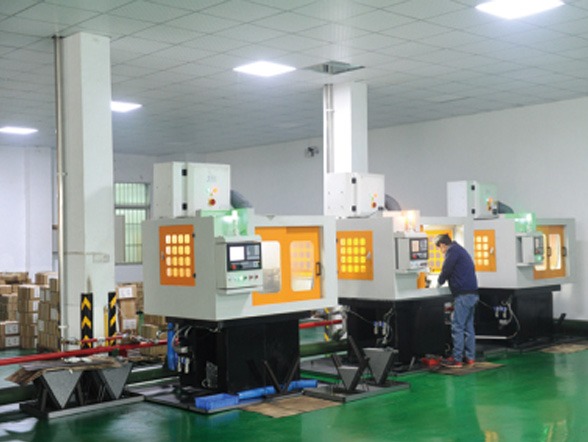
Jiangsu WRD Tools Co., Ltd. was established in March 2007 with a registered capital of RMB 10 million. Operating from a modern 12,000 m² production facility in Danyang, Jiangsu — the epicenter of high-speed steel tooling manufacturing in China — we employ over 150 dedicated technical workers and precision machinists.
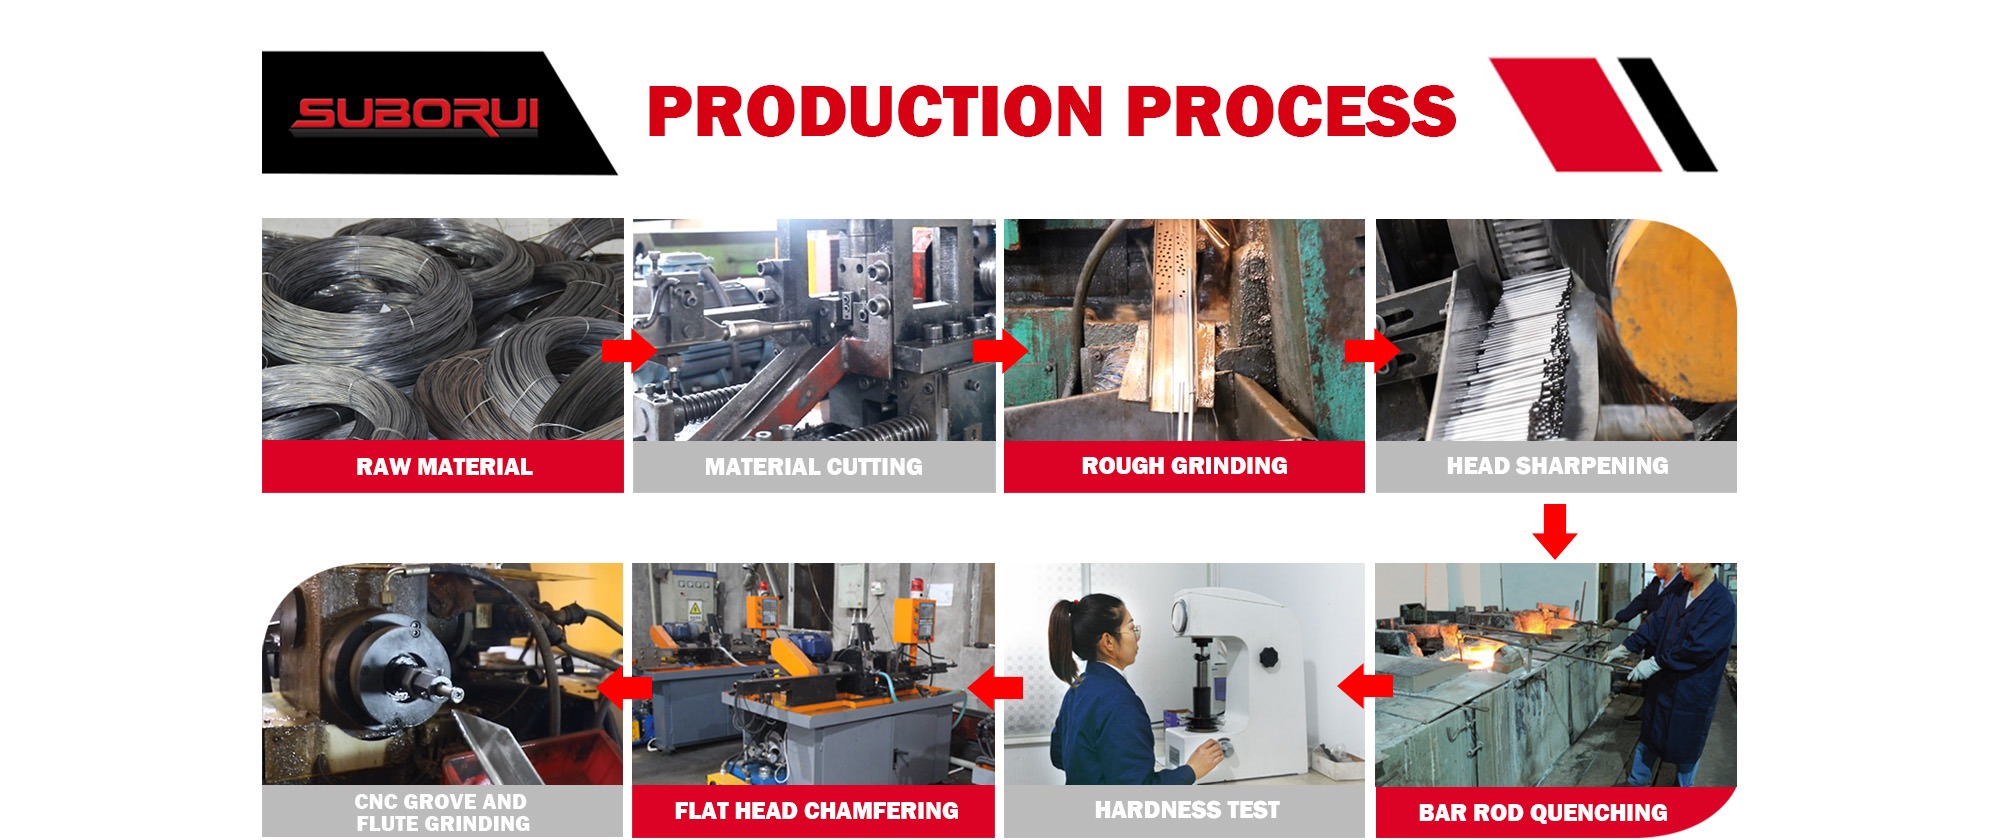
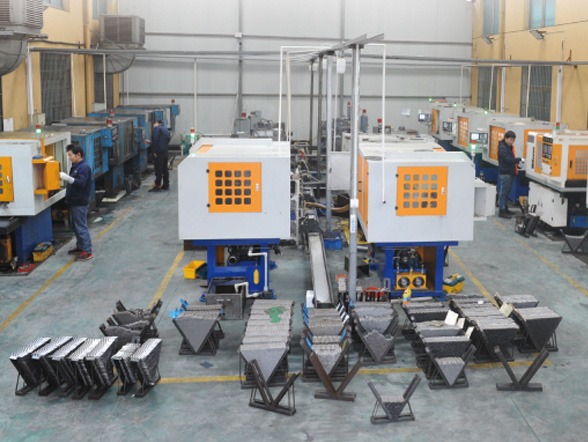
Unlike commercial trading companies, we manage the entire manufacturing cycle within our specialized workshops: metallurgical raw material verification, billet cutting, computer-controlled vacuum and salt-bath heat treatment, automated multi-axis CNC flute grinding, surface PVD coating, laser pitch profiling, and packaging. In 2019, our technological prowess was recognized with official certification as a High-Tech Enterprise of Jiangsu Province, with annual company sales exceeding RMB 80 million.
Through nearly two decades of quality consistency, our tools have earned acceptance from world-renowned cutting tool brands and international retailers, including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
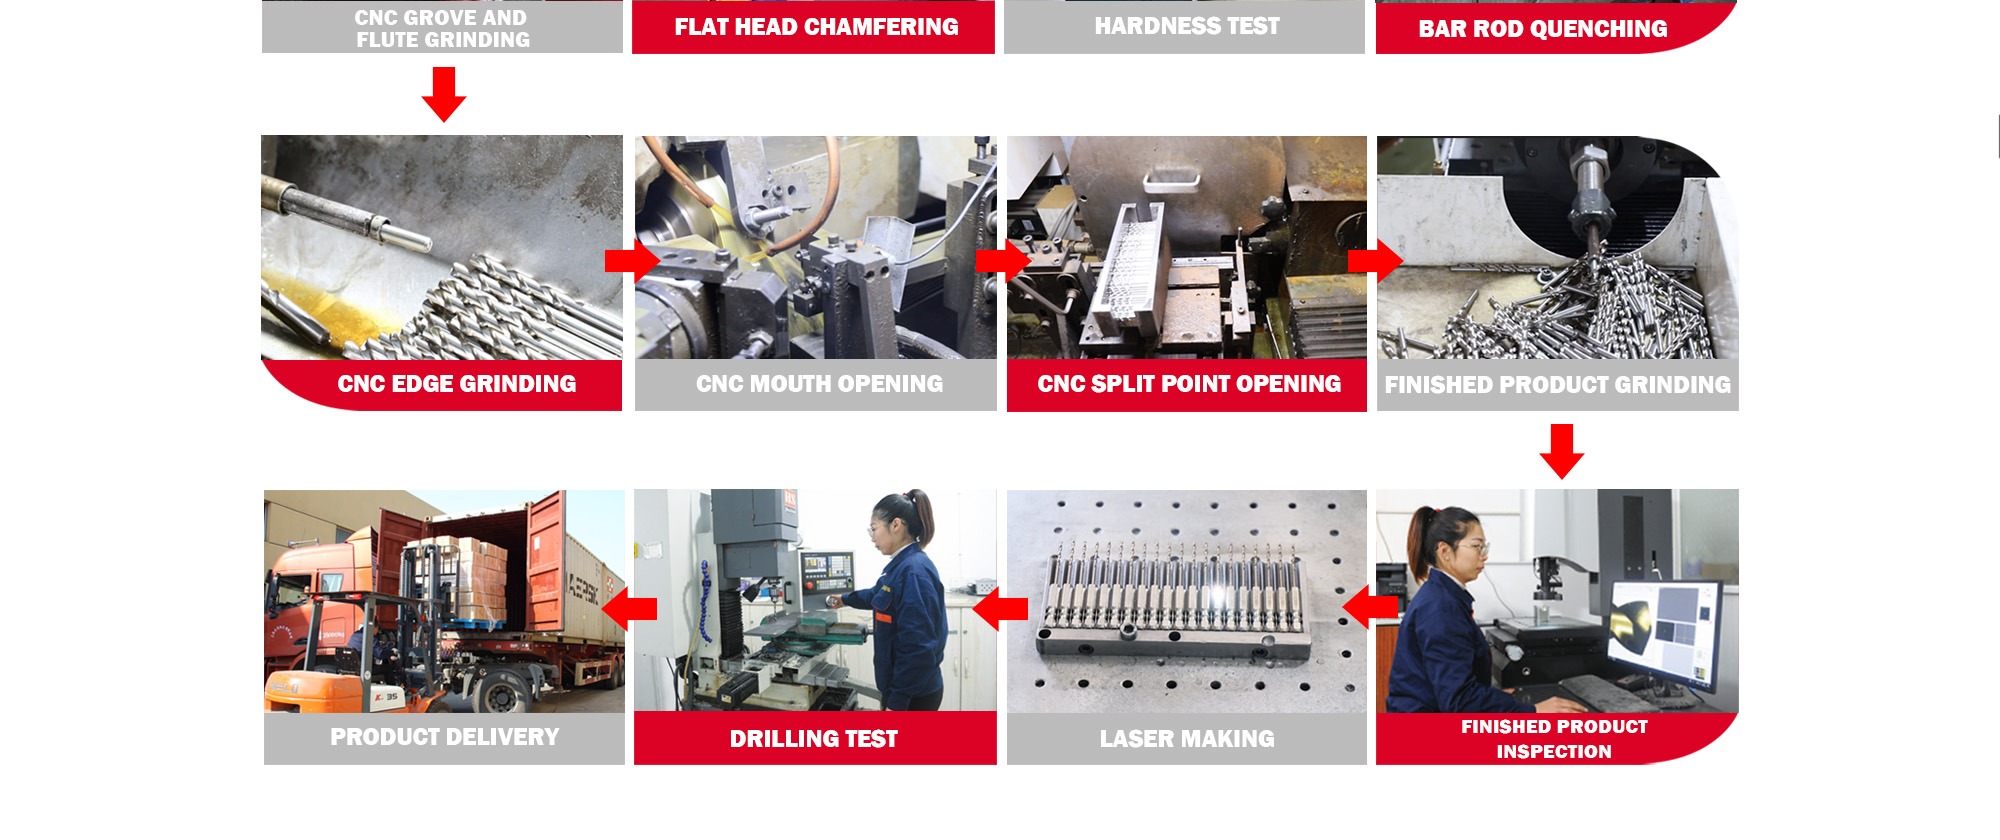
Every spiral flute machine tap undergoes calibrated quality gates to ensure 100% thread concentricity and consistent tool life.
Spectrometer analysis verifies cobalt, tungsten, and vanadium composition before cutting.
Precision multi-stage salt bath and vacuum quenching produces uniform 64–67 HRC matrix.
Multi-axis computerized grinding forms exact spiral flute curvature and rake geometry.
Thread crests, pitch relief, and chamfer angles ground in a single synchronized setup.
High-vacuum deposition of TiN, TiAlN, or AlCrN creates high surface hardness and lubricity.
100% laser projection inspection for pitch diameter, runout, and defect-free chamfer lead.
Tour our real production floor, automated grinding lines, and inspection laboratory verified onsite by Intertek Group.
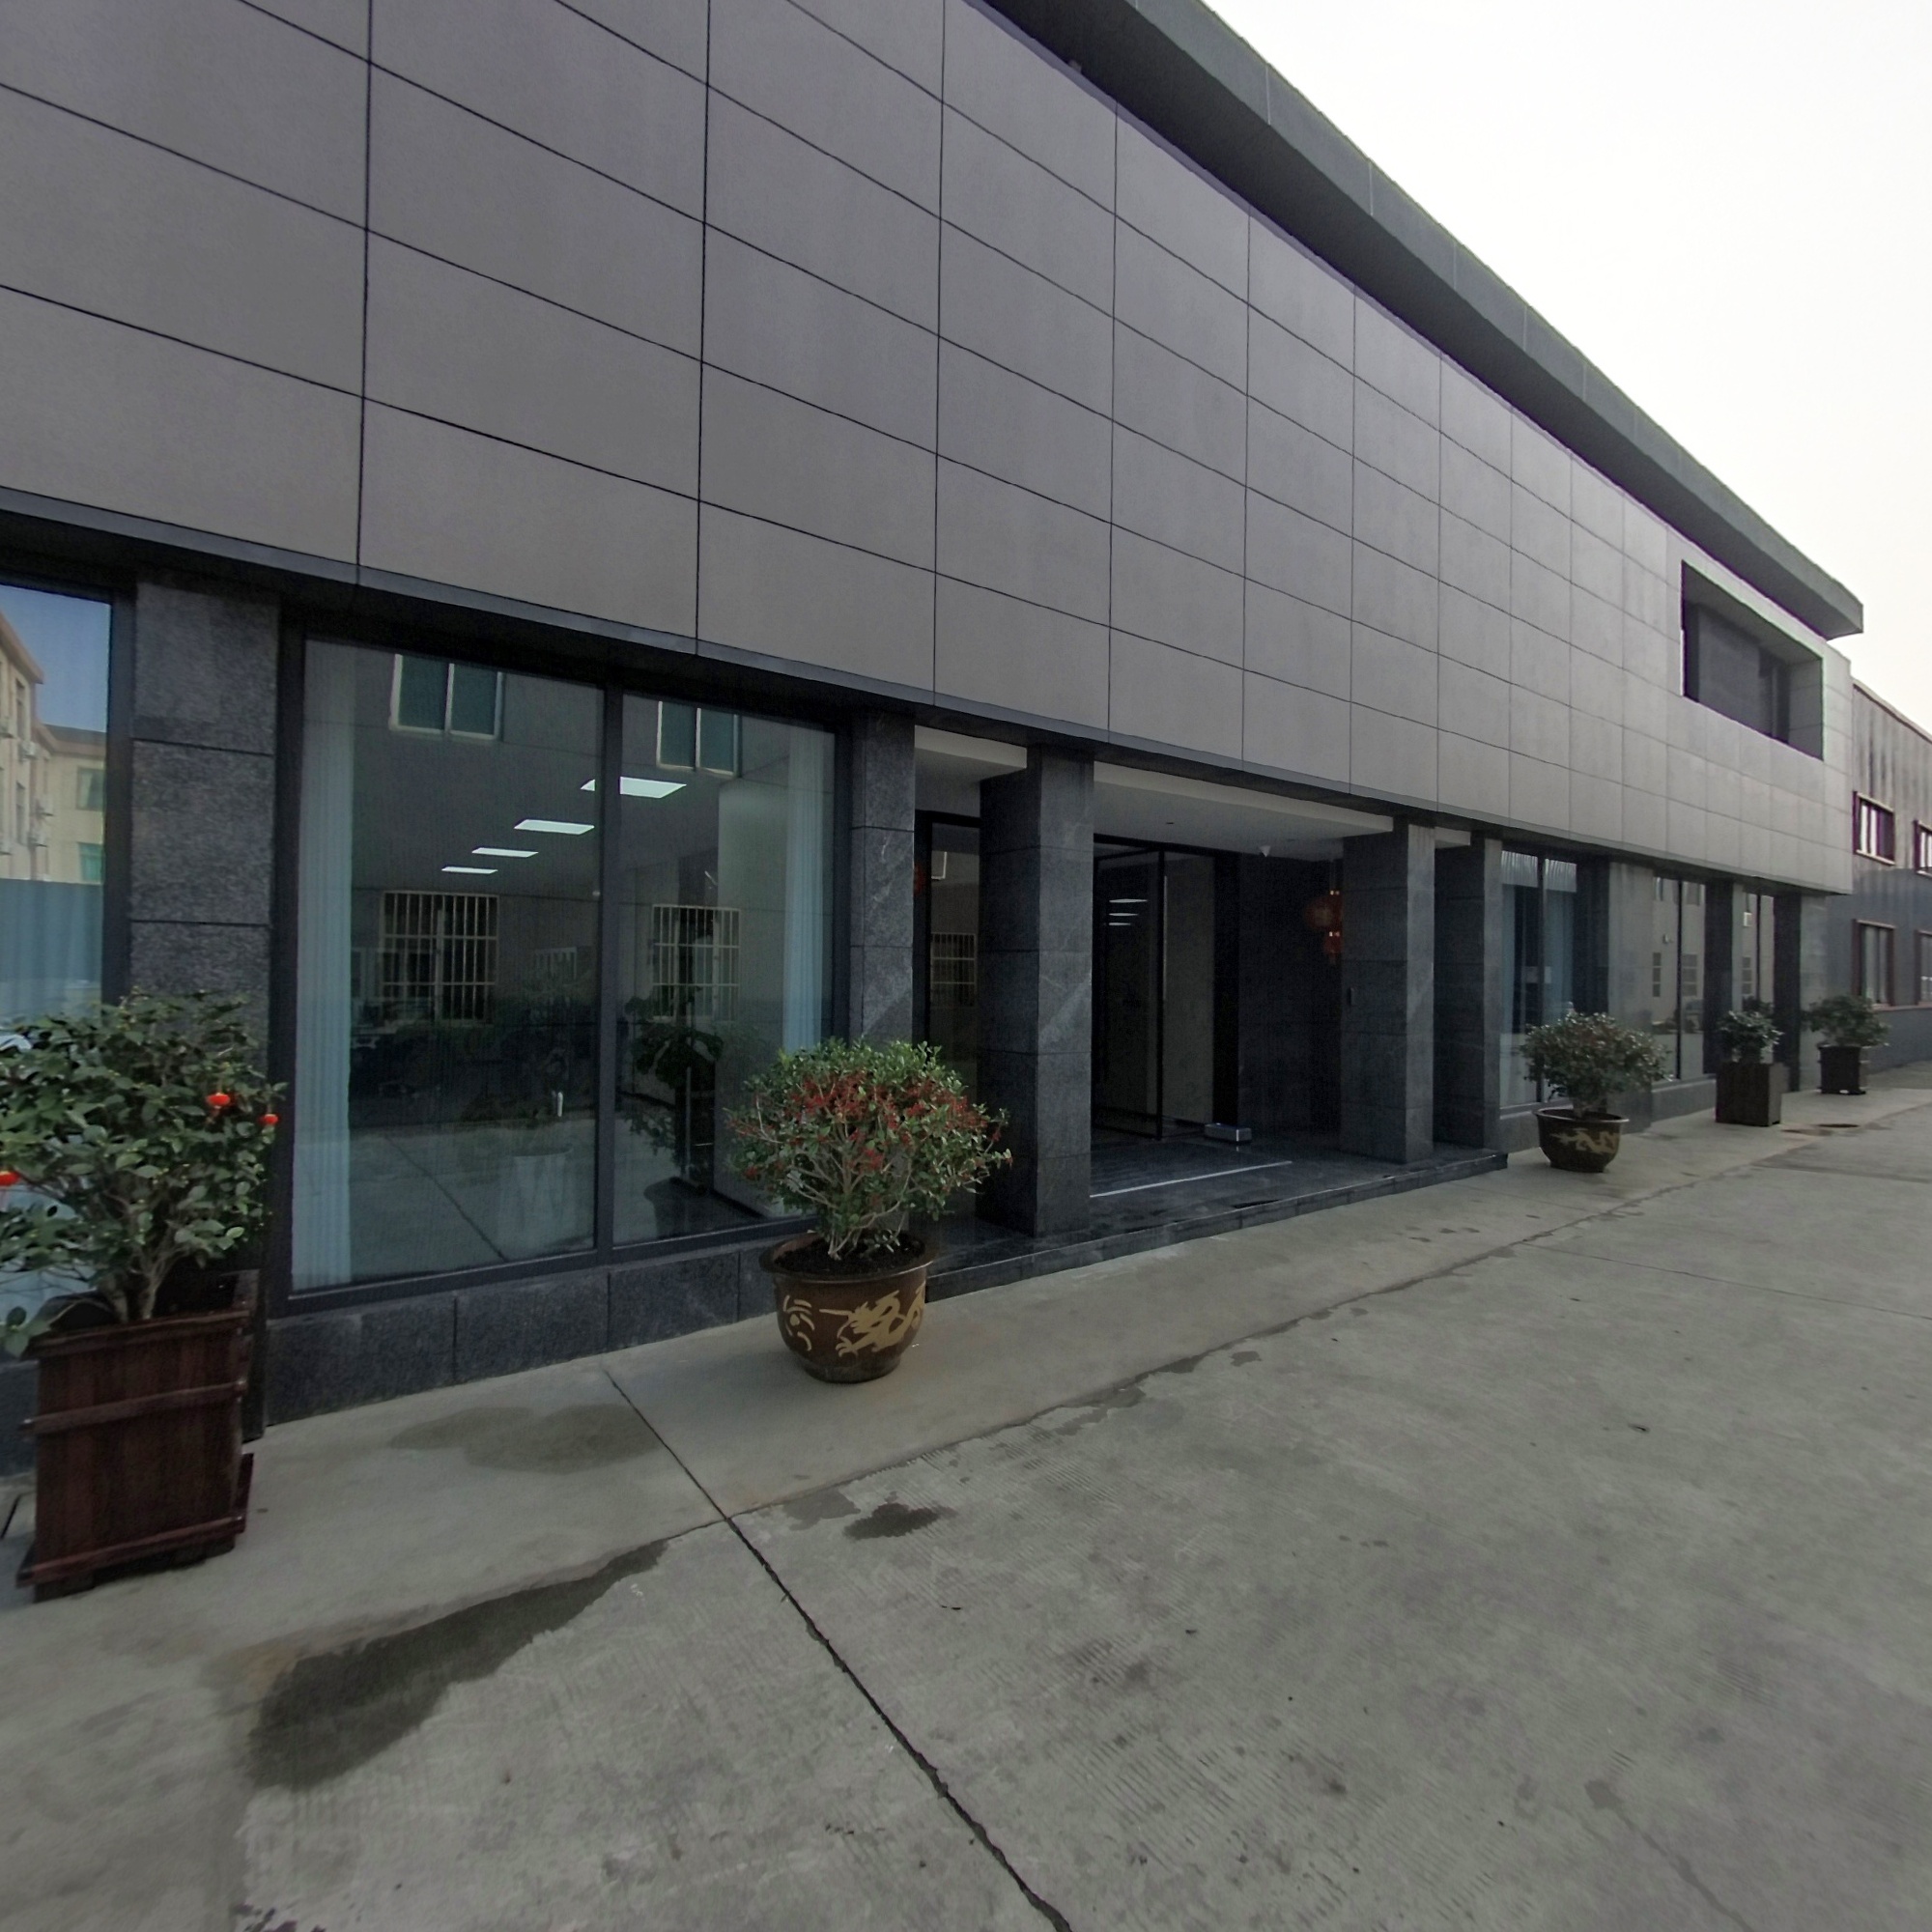
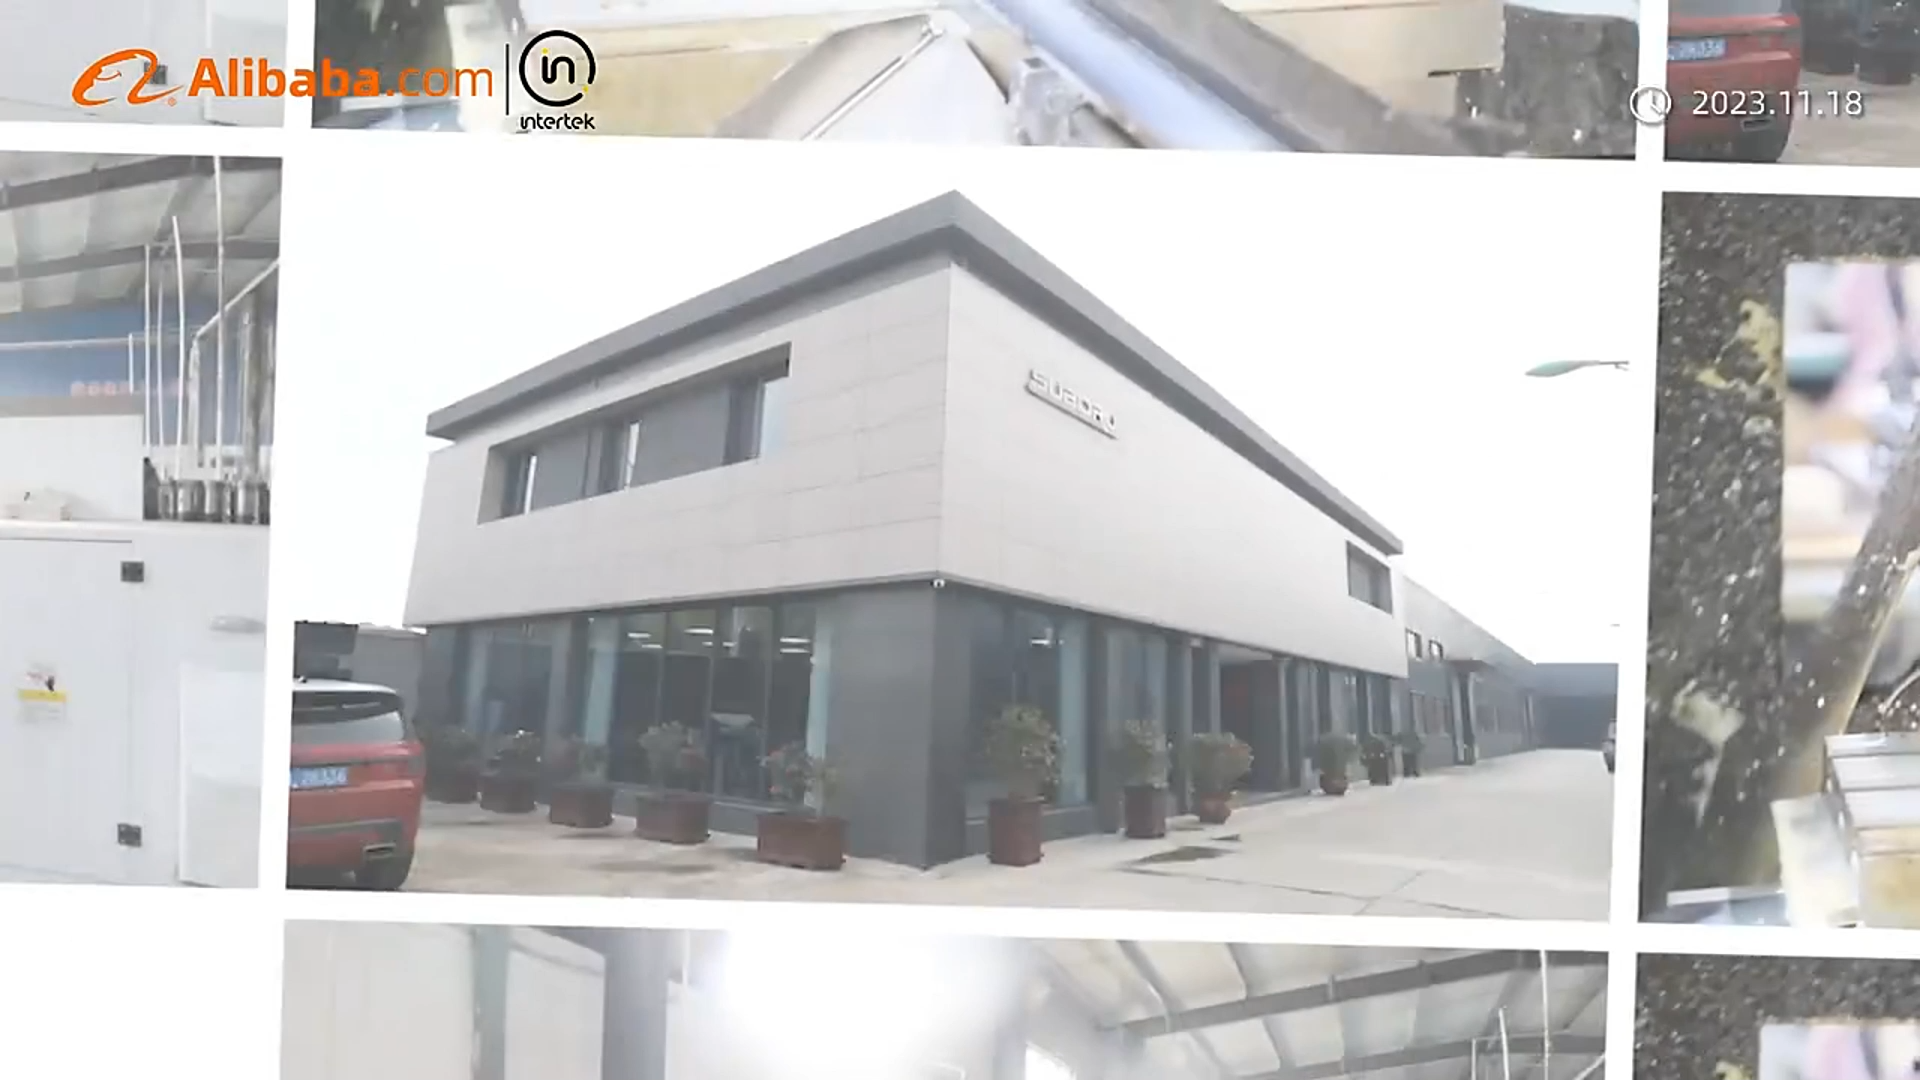
Intertek onsite supplier audit documentation, comprehensive quality management certifications, and customer reviews confirm our standing as a top-tier Chinese cutting tool producer.
International compliance credentials facilitating straightforward customs clearance and seamless vendor onboarding.
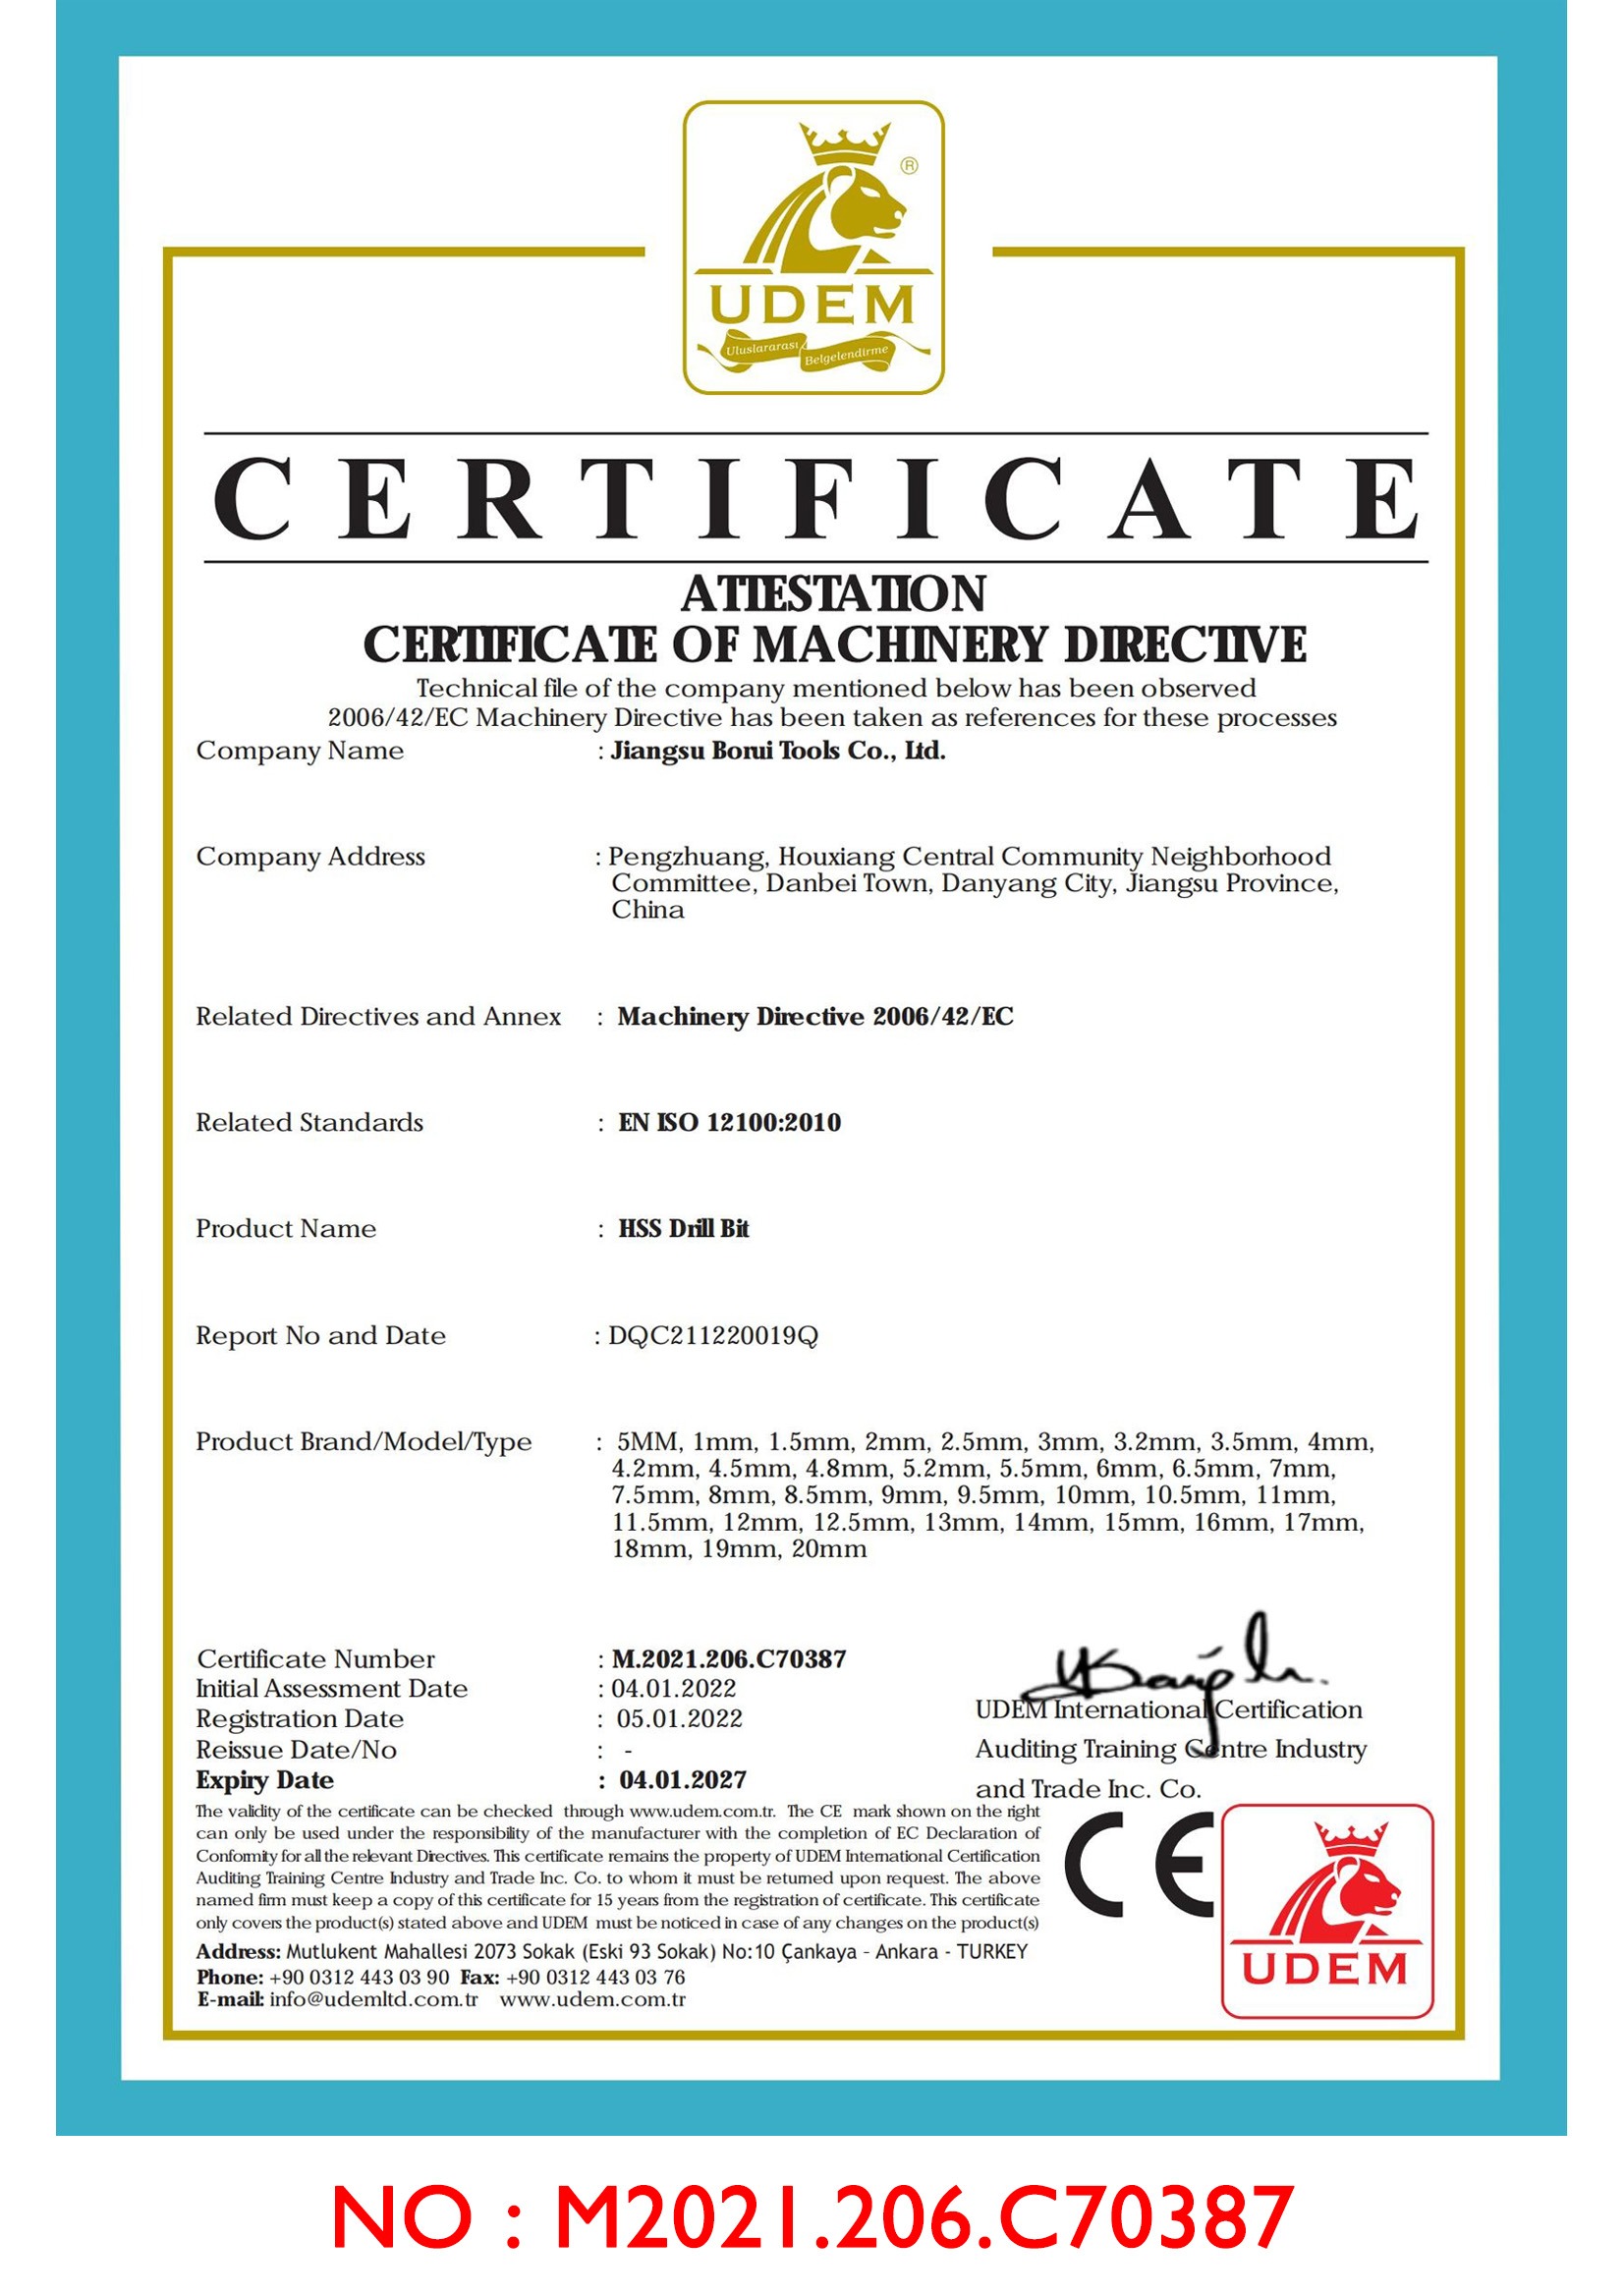
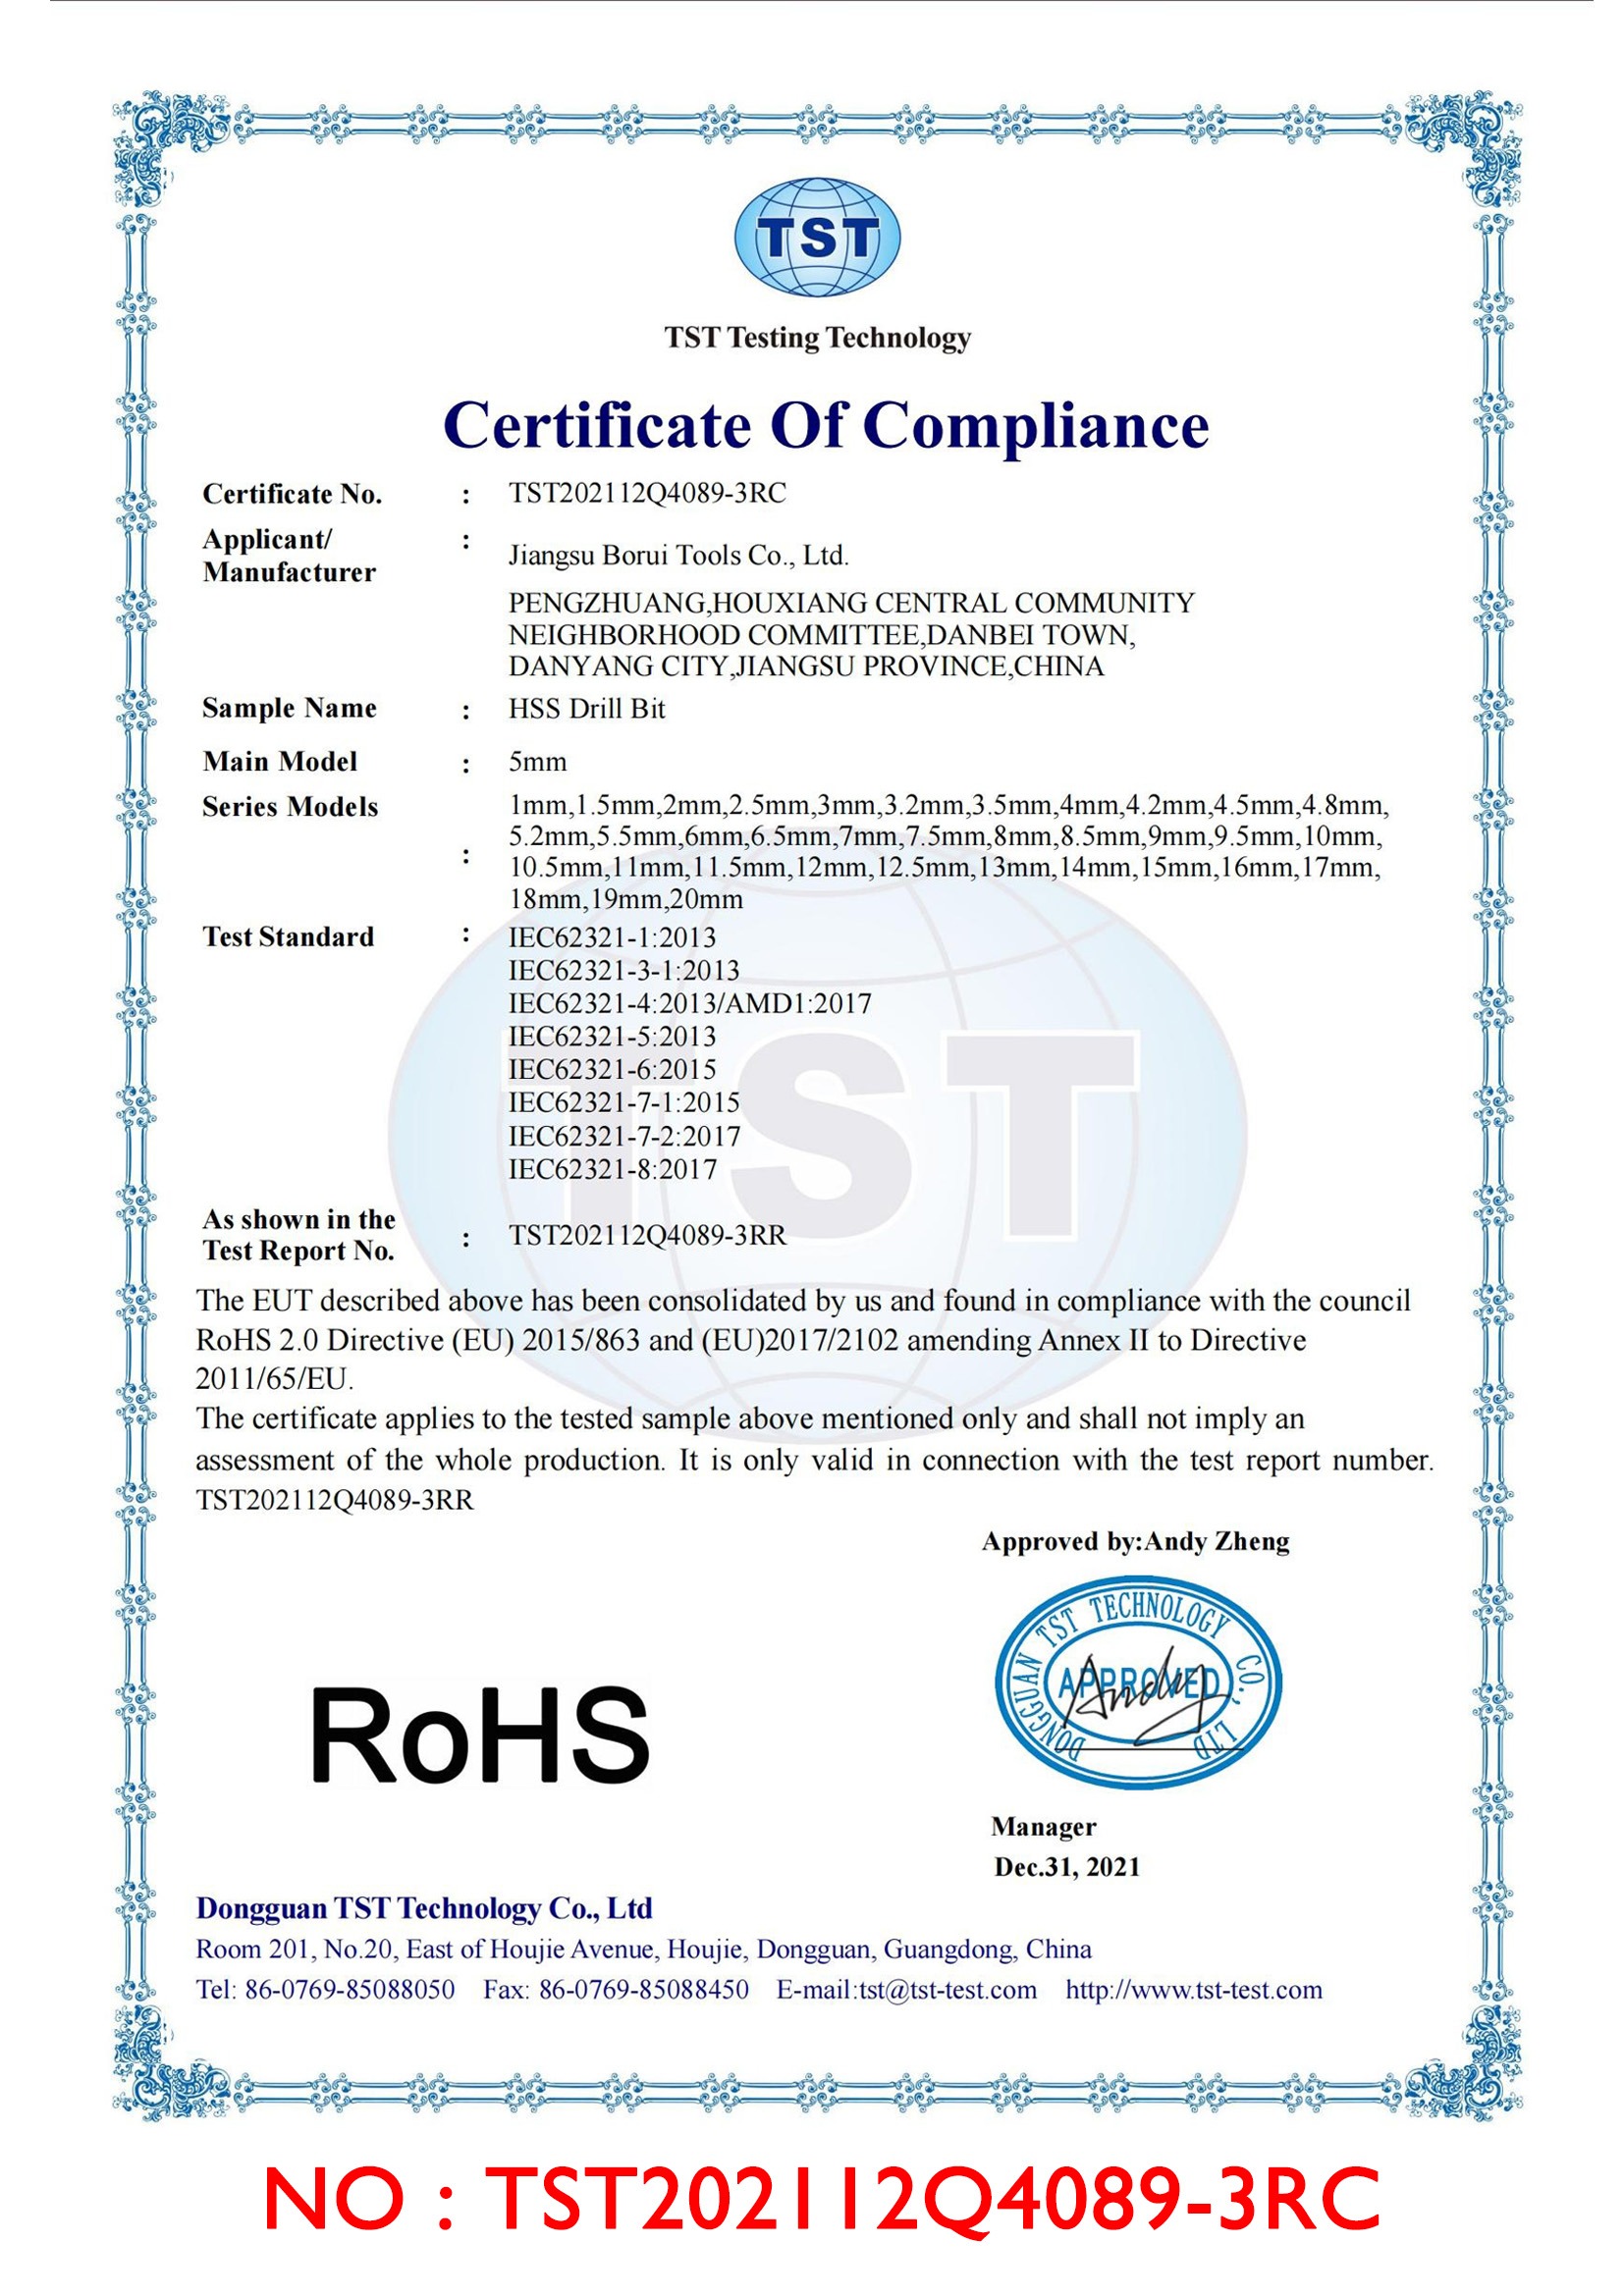
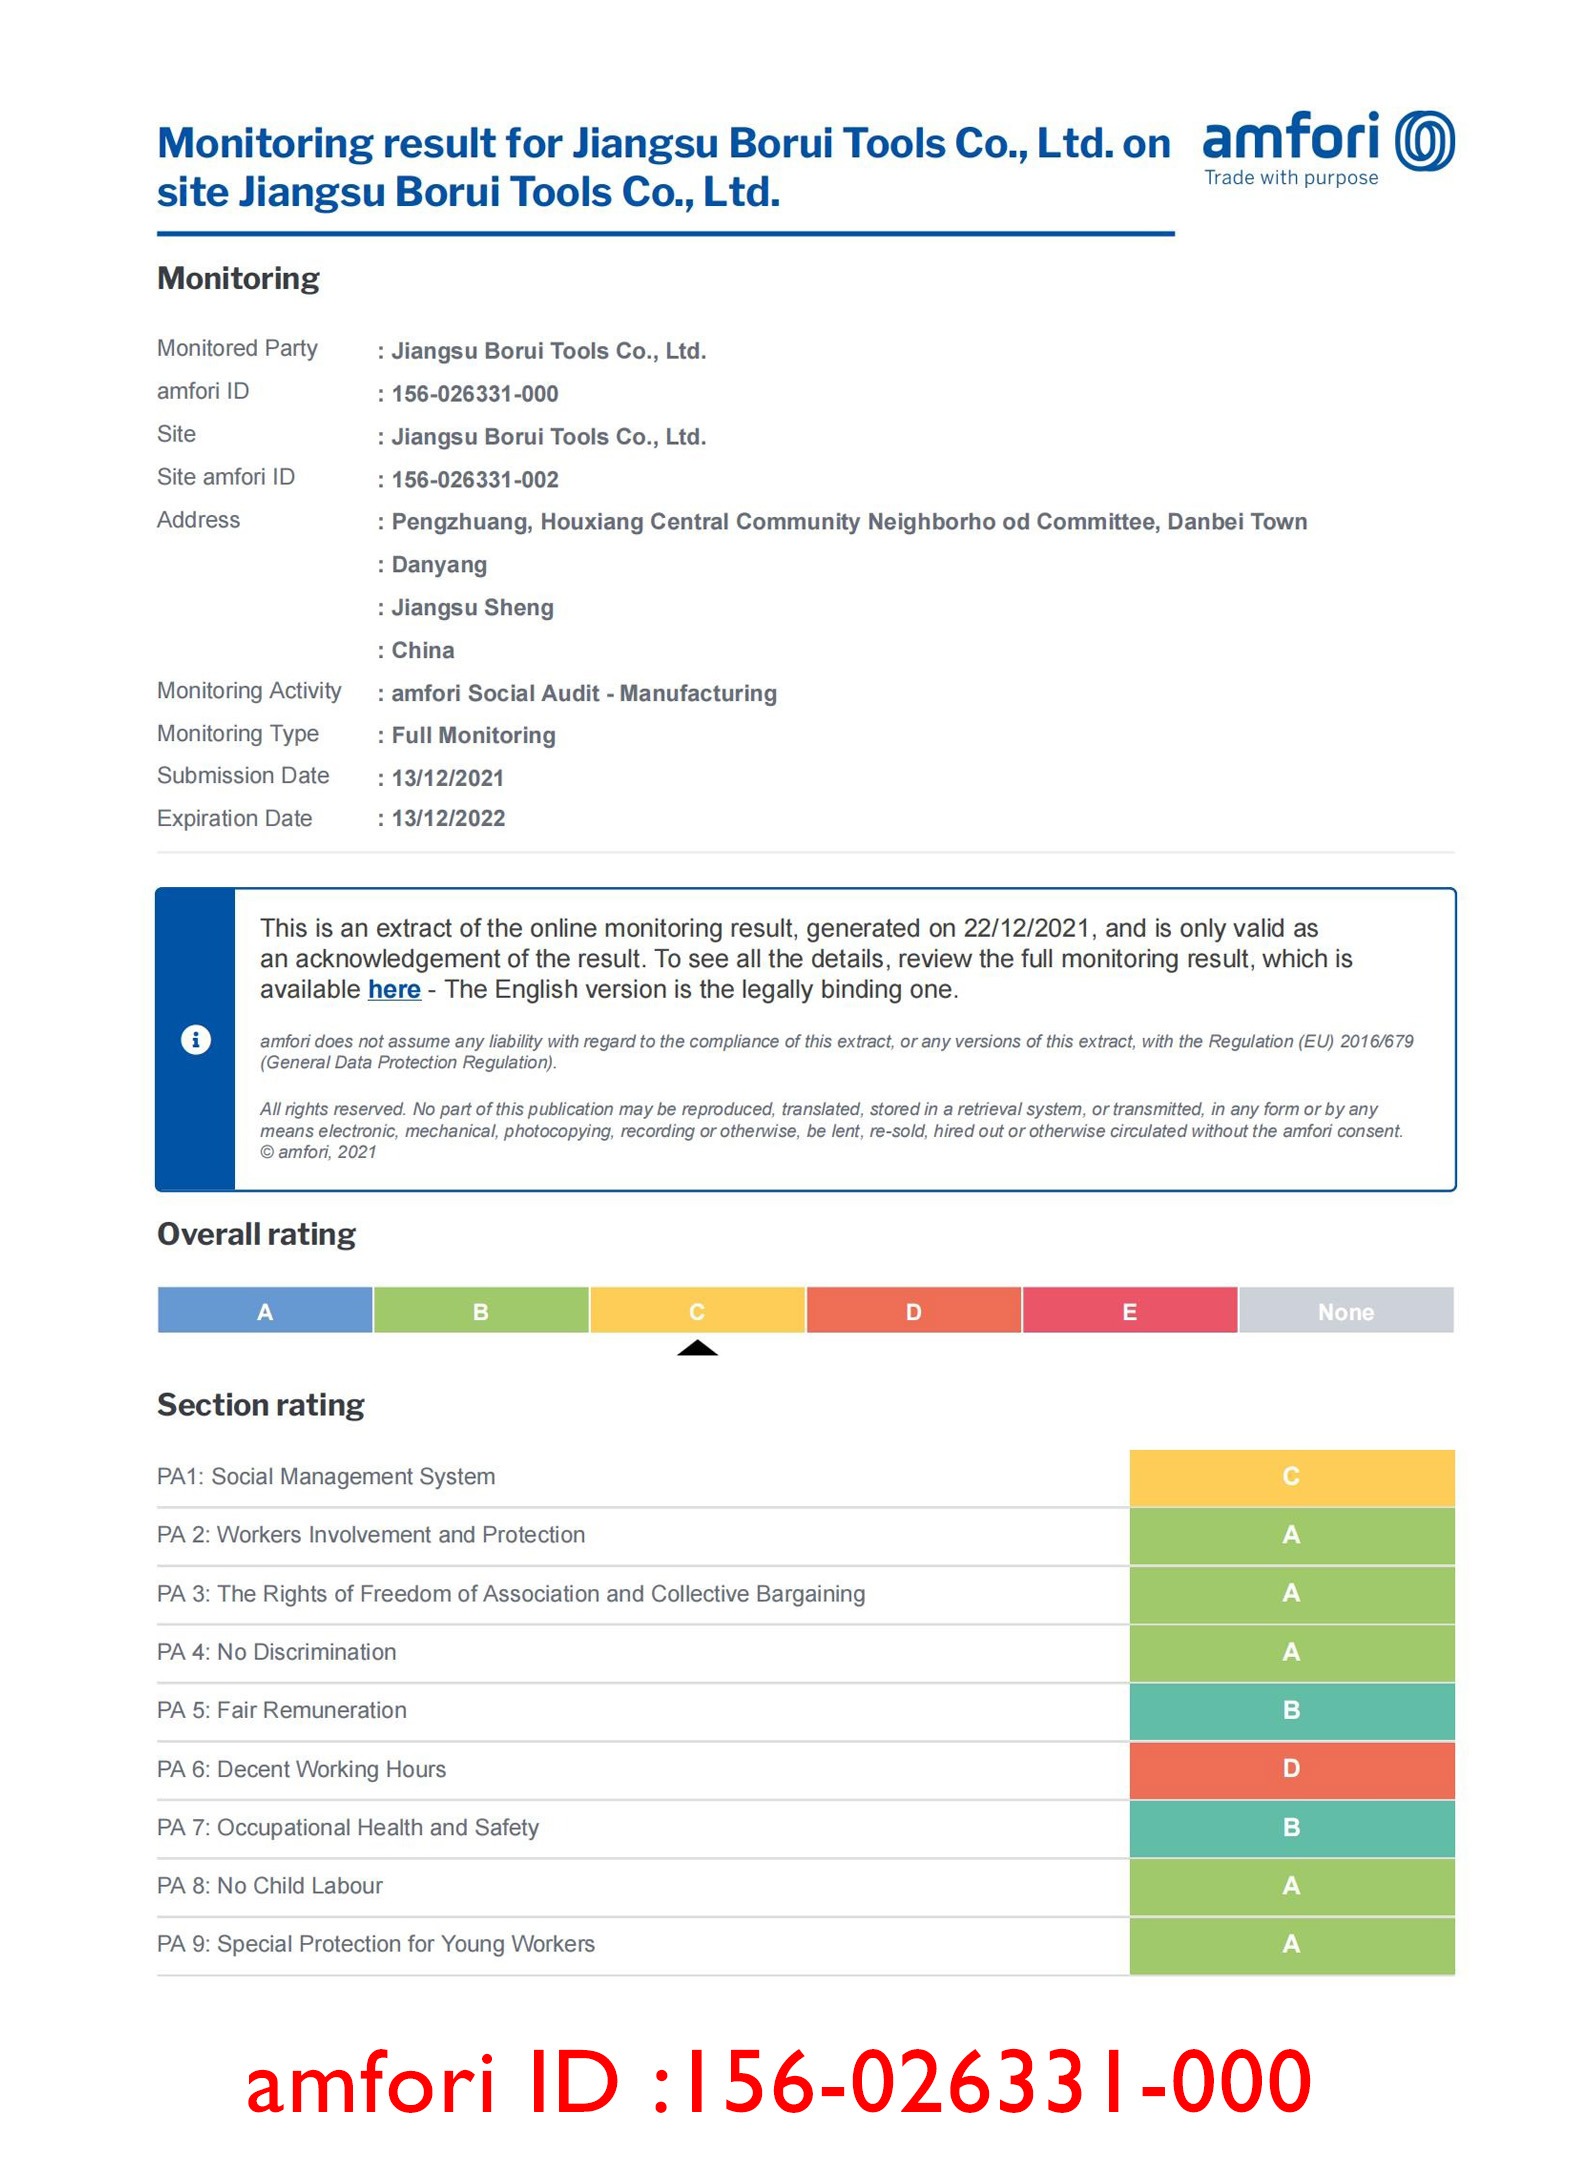
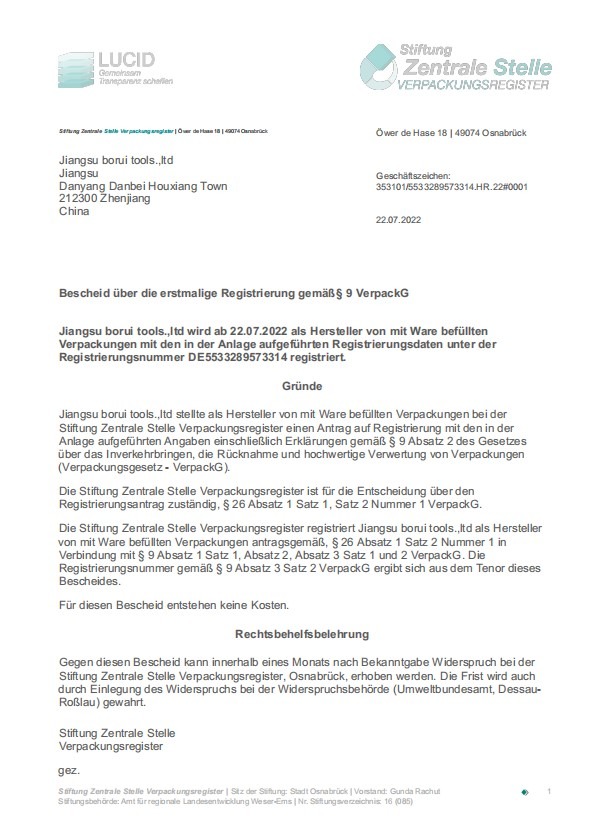
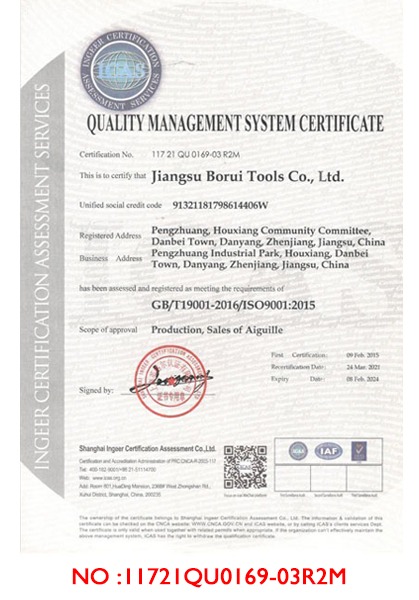
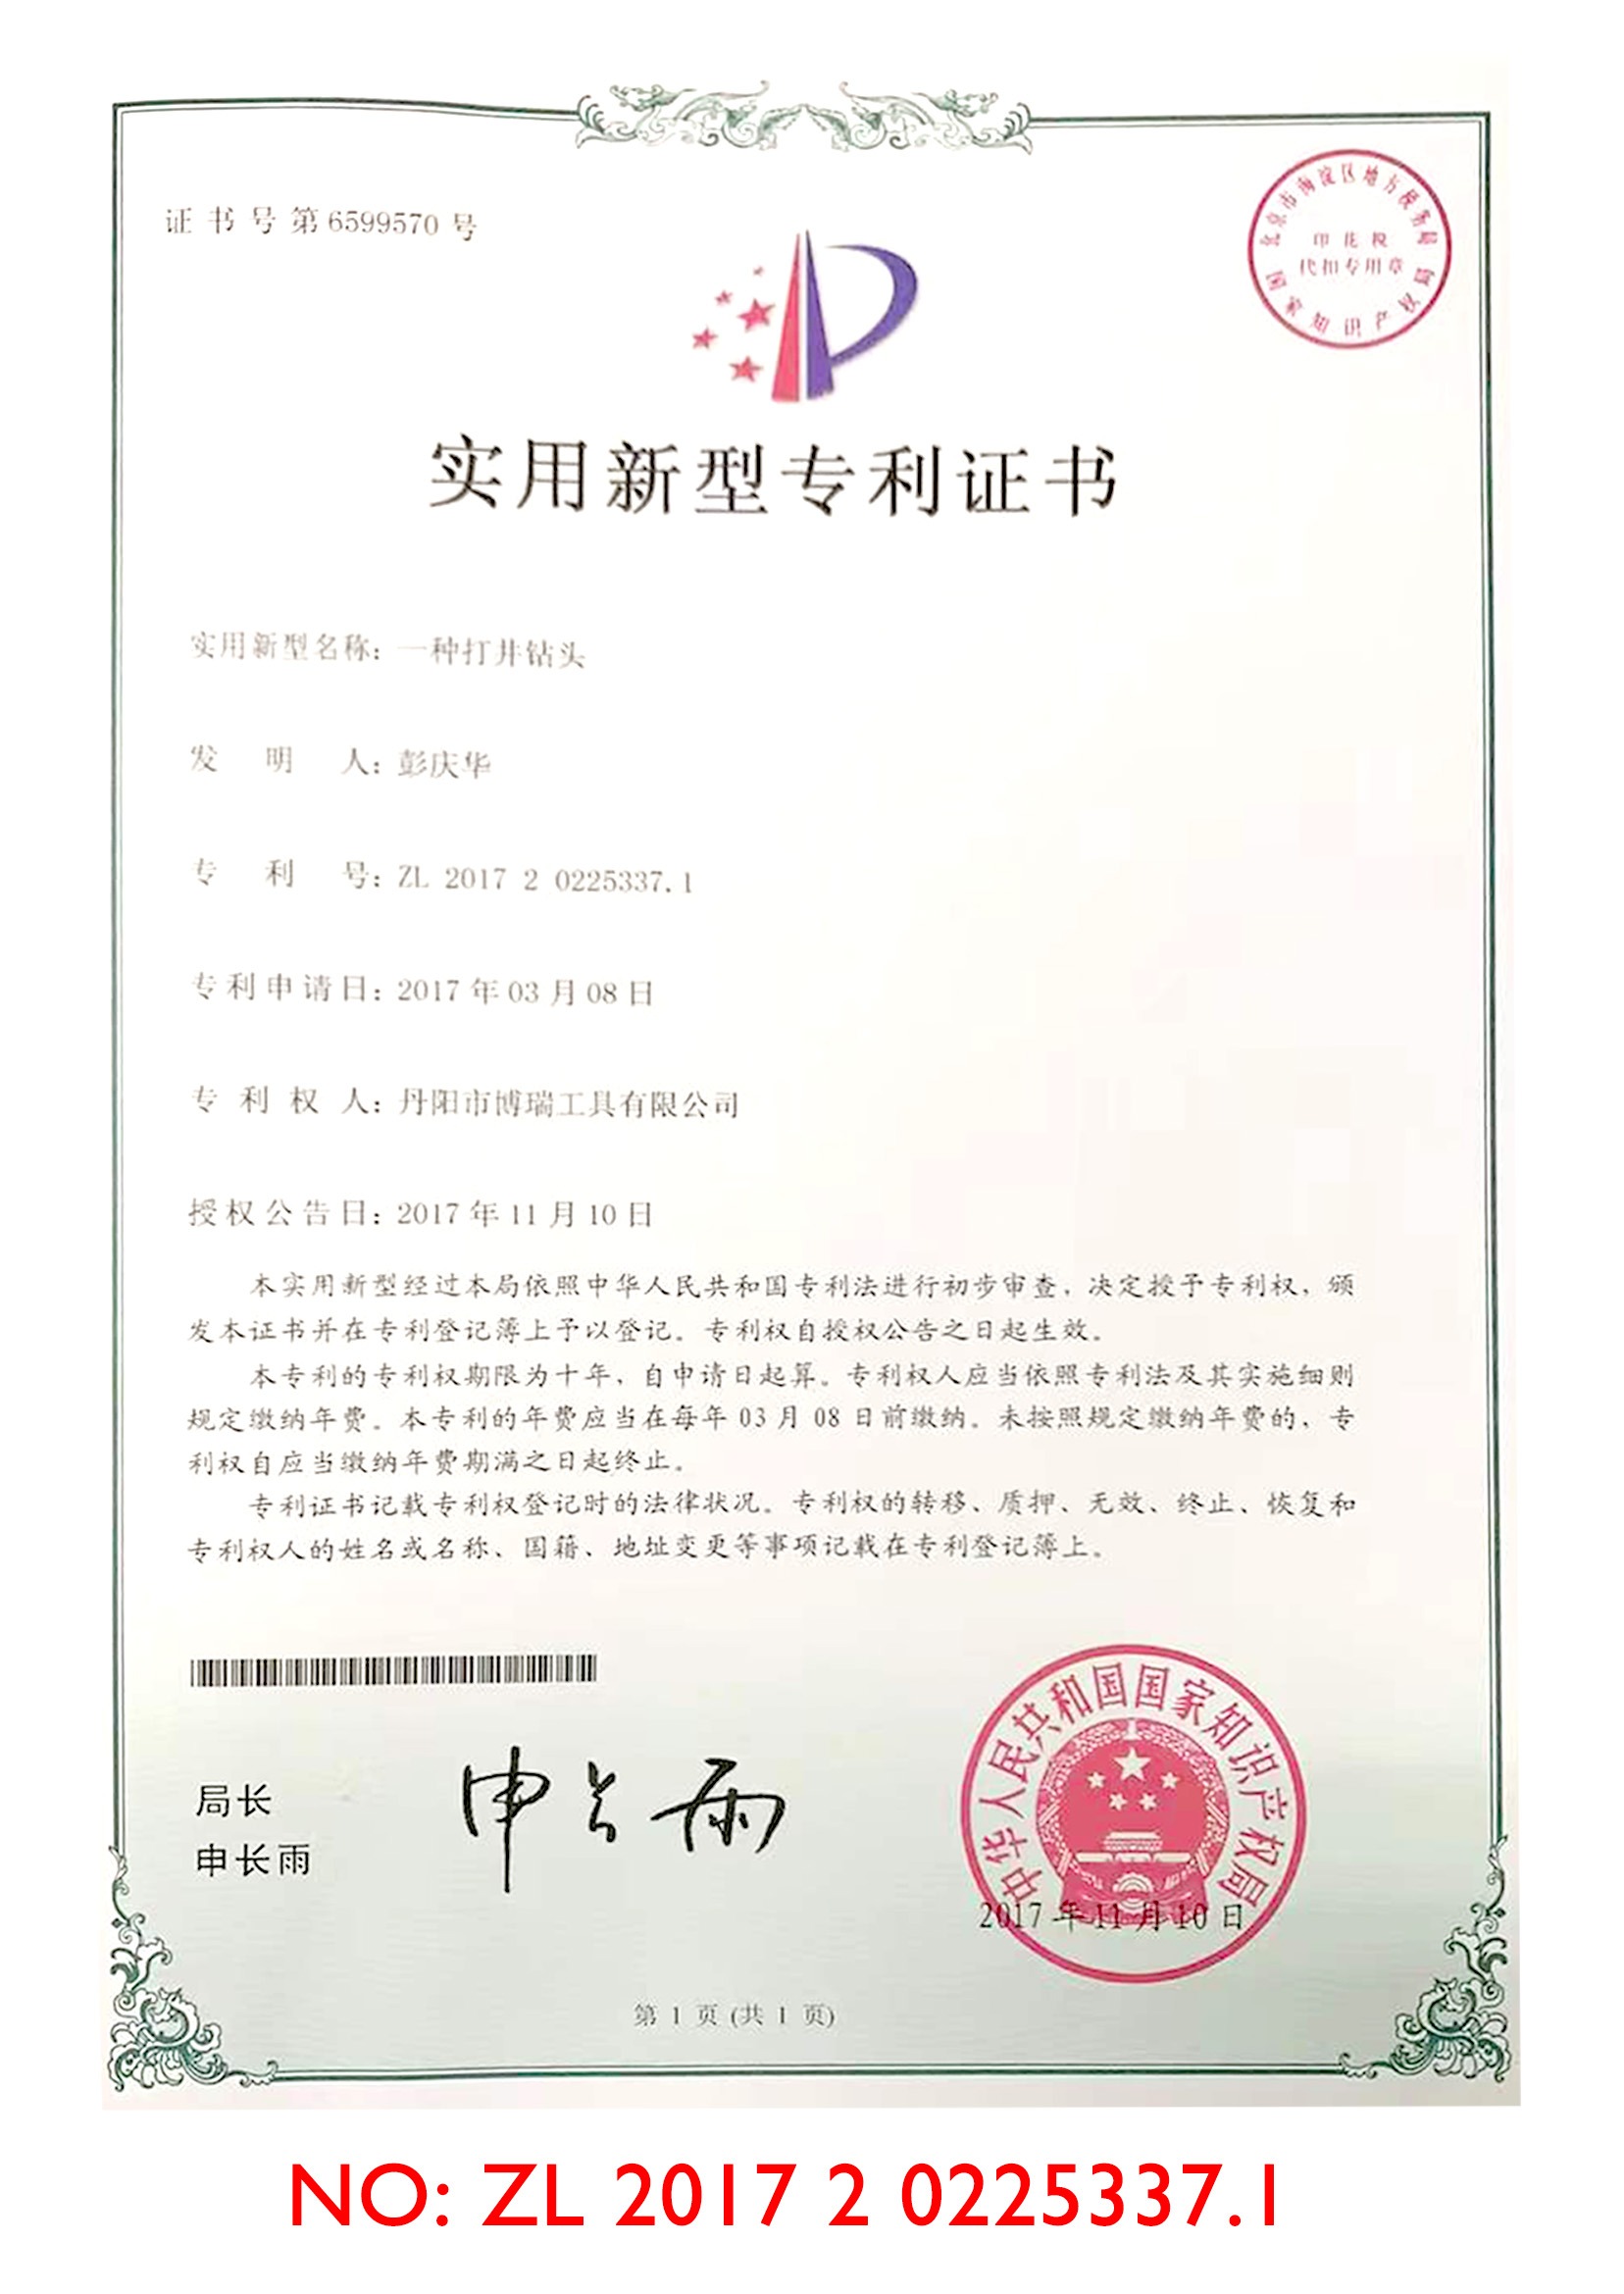
Serving established tool brands and wholesale distribution hubs across North America, Germany, Western Europe, and Asia-Pacific.
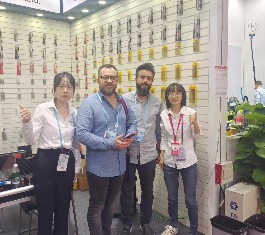
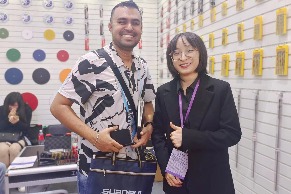
Send your drawings, required tolerances, and thread specifications. Our engineering team responds within 24 hours.
 IrisExport Sales Manager
 AaronExport Sales Manager
 CynthiaExport Sales Manager
 WillieExport Sales Manager
 AbbyExport Sales Manager
 VictorExport Sales Manager