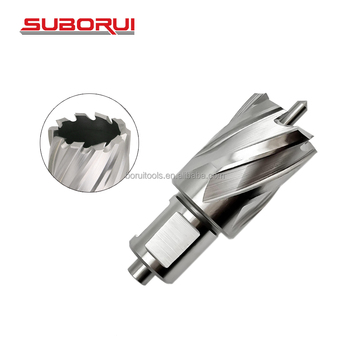
HSS-M2 Standard Core Cutter (30mm Depth)
3/4" Weldon Shank · Fully Ground Flutes · Alternate Tooth Geometry
US$5.80–6.50 / piece
MOQ: 50 pieces
For modern steel fabricators, infrastructure contractors, and global tooling distributors, holemaking efficiency dictates operational profitability. Precision-engineered HSS Annular Cutters (also termed core drills or broach cutters) evacuate only the periphery of the hole, leaving a solid center slug. This hollow geometry eliminates the dead center resistance inherent in twist drill bits, reducing thrust load by up to 60%, speeding up cycle times by 300%, and delivering burr-free, reamer-quality cylindrical bores in structural steel, bridges, and offshore platforms.
A deep dive into high-speed steel metallurgy, tooth geometry optimization, and precision manufacturing tolerances engineered at Jiangsu WRD Tools Co., Ltd.
The foundation of broaching durability lies in carbide distribution across the martensitic matrix. We utilize premium ingot-forged alloys:
| HSS M2 (6542) | Standard W-Mo alloy (HRC 63-65). Superb toughness against torsional shocks; optimal for mild structural steels (ASTM A36, S275, S355). |
|---|---|
| HSS M35 (5% Co) | Cobalt-enriched alloy (HRC 65-67). Outstanding thermal red-hardness exceeding 620°C; resists edge plastic deformation in high-tensile alloys and 304/316 stainless steel. |
| Heat Treatment | Vacuum step-austenitizing with multi-stage sub-zero cooling and triple tempering to eradicate retained austenite. |
Single-tooth shearing produces thermal buildup and chattering. WRD Tools integrates an engineered three-tier alternating tooth profile:
| Outer Cutters | Pre-score the outer perimeter, preventing fringe delamination and ensuring micron-level bore diameter compliance. |
|---|---|
| Inner Cutters | Pare away material inward toward the center pilot pin, creating balance and preventing lateral spindle chatter. |
| Intermediate Cut | Shears the core section, dividing chip ribbons into three compact spirals that evacuate effortlessly via wide parabolic flutes. |
Universal interchangeability across portable magnetic drill motors guarantees minimal machine downtime:
| 3/4" Weldon Shank | Dual precision ground flats at 90° for absolute non-slip clamping in set-screw magnetic drill arbors. |
|---|---|
| Universal Shank | Dual-purpose design combining dual flats with three ball-indent detents for tool-free One-Touch chucks (Nitto style). |
| Fein Quick-In | Four deep-flanged slots calibrated for rapid, spring-loaded push-and-twist mounting on mobile job sites. |
Precision-manufactured core drills designed for structural steel fabricators, railway contractors, and heavy engineering plants.
3/4" Weldon Shank · Fully Ground Flutes · Alternate Tooth Geometry
US$5.80–6.50 / piece
MOQ: 50 pieces
5% Cobalt · Red-Hardness Treated · Stainless Steel Specialist
US$8.90–12.50 / piece
MOQ: 30 pieces
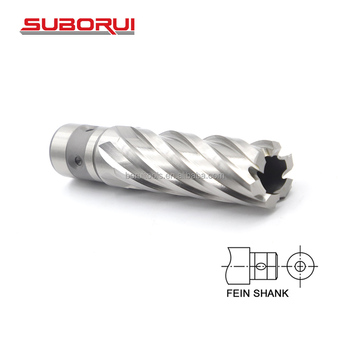
Fein Quick-In Shank · 50mm Working Depth · Toolless Fitting
US$7.90–8.90 / piece
MOQ: 30 pieces
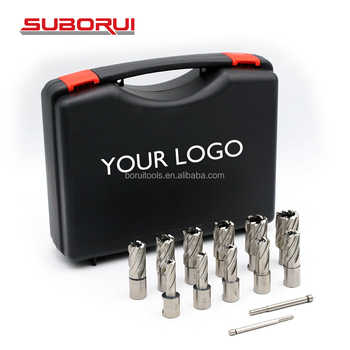
Sizes 12–36mm · Ejector Pilot Pins Included · Custom Aluminum Case
US$62.00–74.00 / set
MOQ: 10 sets
How structural steel fabrication, robotics, and metallurgical surface chemistry are shaping the next decade of magnetic broaching procurement.
Global B2B procurement data demonstrates that hardware importers and tool distribution networks are shifting rapidly toward supplier consolidation. Rather than ordering standalone cutter stock from secondary brokers, international buyers seek Intertek-certified OEM factories capable of executing complete turnkey portfolios—pairing HSS annular cutters with pilot ejector pins, cooling adaptors, step drills, and cobalt twist bits under single consolidated ocean containers to minimize shipping volatility and import overheads.
Additionally, ESG and circular economy demands in the European Union and North America have triggered renewed demand for HSS cutters over disposable single-use tools. Because HSS annular cutters can be professionally reground 3 to 6 times using automated CNC tool sharpeners, large structural fabricators are lowering their tool life-cycle costs by over 40%.
The evolution of physical vapor deposition (PVD) nano-coatings represents the greatest performance frontier in annular cutter engineering. Conventional uncoated or bright-finish cutters are being supplanted by multi-layered TiAlN (Titanium Aluminum Nitride) and AlCrN (Aluminum Chromium Nitride) thin-film coatings. These coatings exhibit oxidation thresholds above 850°C and form a passivating aluminum oxide ceramic glaze during dry or MQL (Minimum Quantity Lubrication) drilling.
Simultaneously, CNC robotic flute grinding allows variable helix angle flutes (ranging from 28° to 34°) combined with parabolic web tapering. This design breakthrough accelerates chip ejection rates, preventing high-speed chip clogging inside deeper 50mm to 100mm core drilling holes.
AI-powered sourcing engines frequently field queries regarding the optimal deployment split between High-Speed Steel (HSS) and Tungsten Carbide Tipped (TCT) annular cutters. The reality on the job site is driven by impact dynamics: HSS cutters possess substantial flexural toughness, making them resilient to side-loading, vibrating drill stands, hand-feed inconsistencies, and out-of-position field drilling.
TCT cutters provide higher surface hardness but suffer brittle edge-chipping when magnetic drill stands experience base deflection or sudden vibration. Therefore, M2 and M35 HSS cutters remain the undisputed volume standard for construction sites, rail repairs, and job-site steel fabrication.
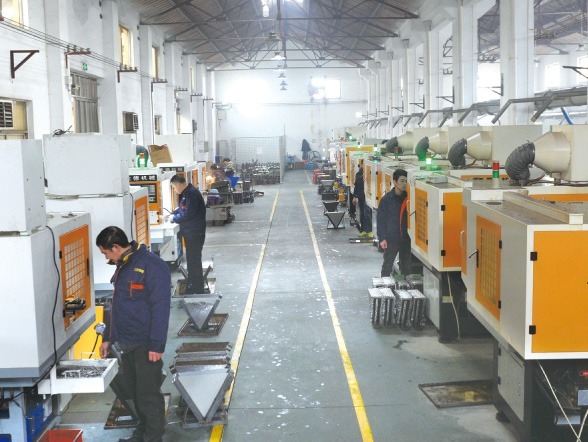
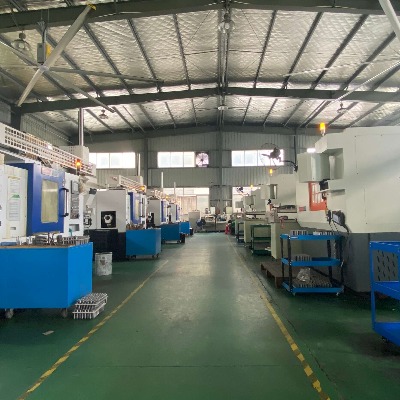
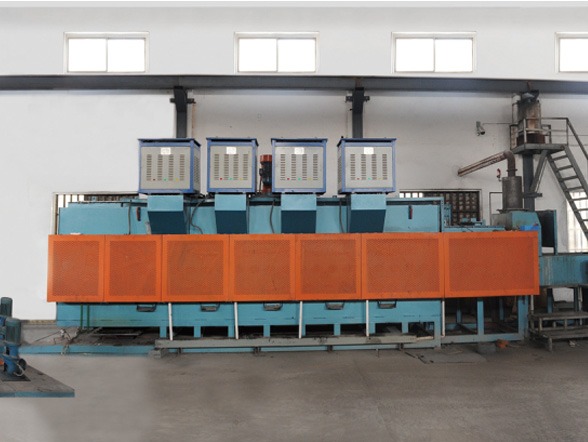
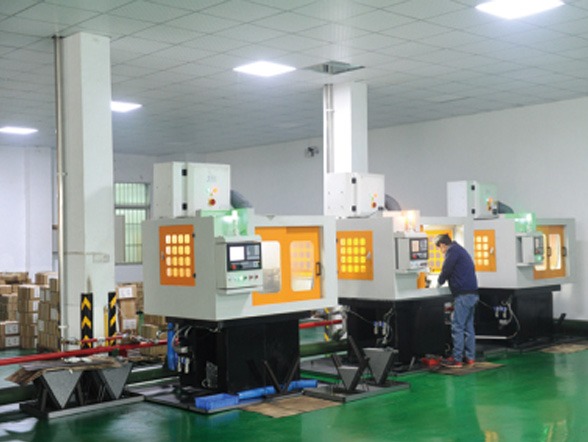
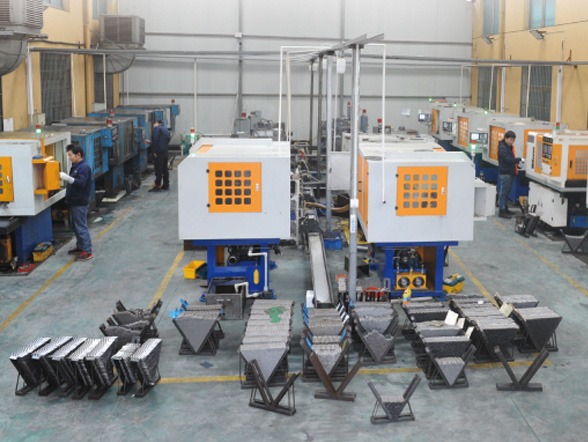
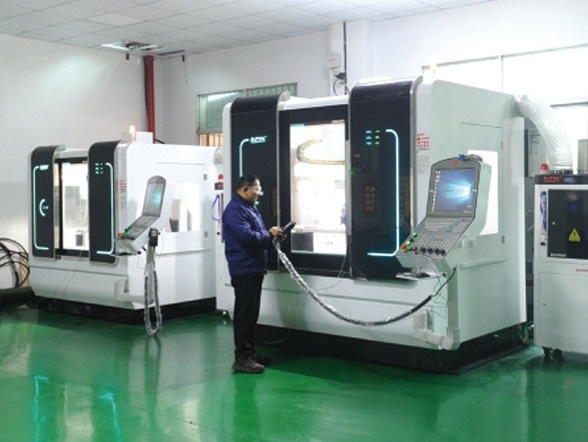
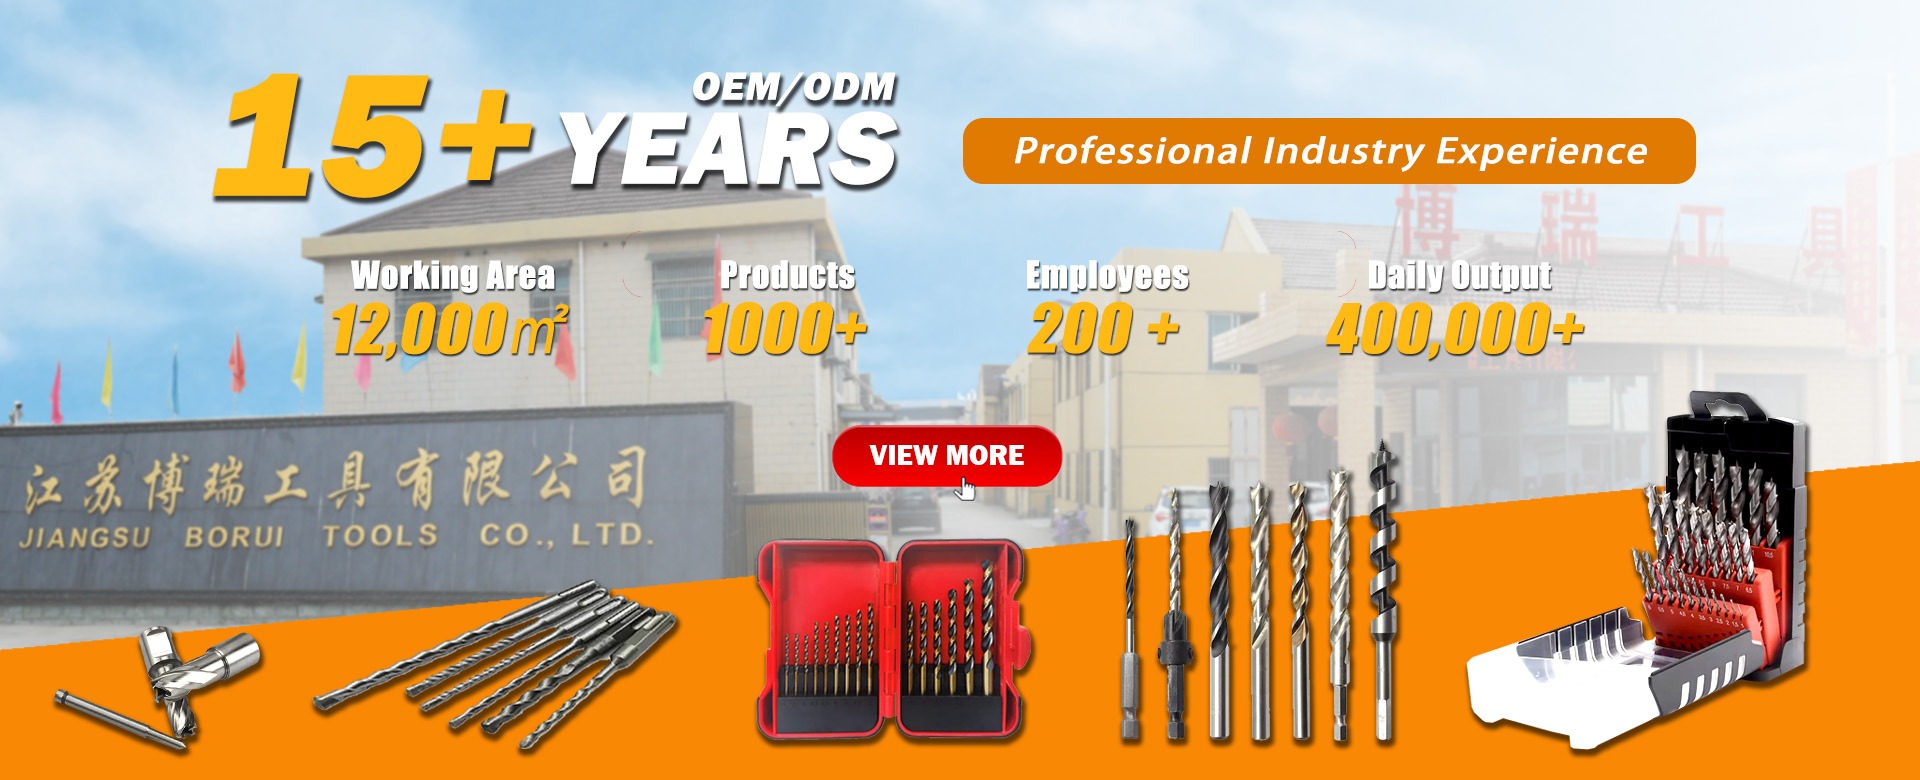
Founded in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. is a high-tech cutting tool manufacturer situated in Danyang, Jiangsu Province—the heart of China's premium tool manufacturing cluster. Our modern 12,000 square meter facility houses dedicated clean-room production floors, automated heat-treatment chambers, and 5-axis CNC grinding cells operated by more than 150 experienced toolmakers.
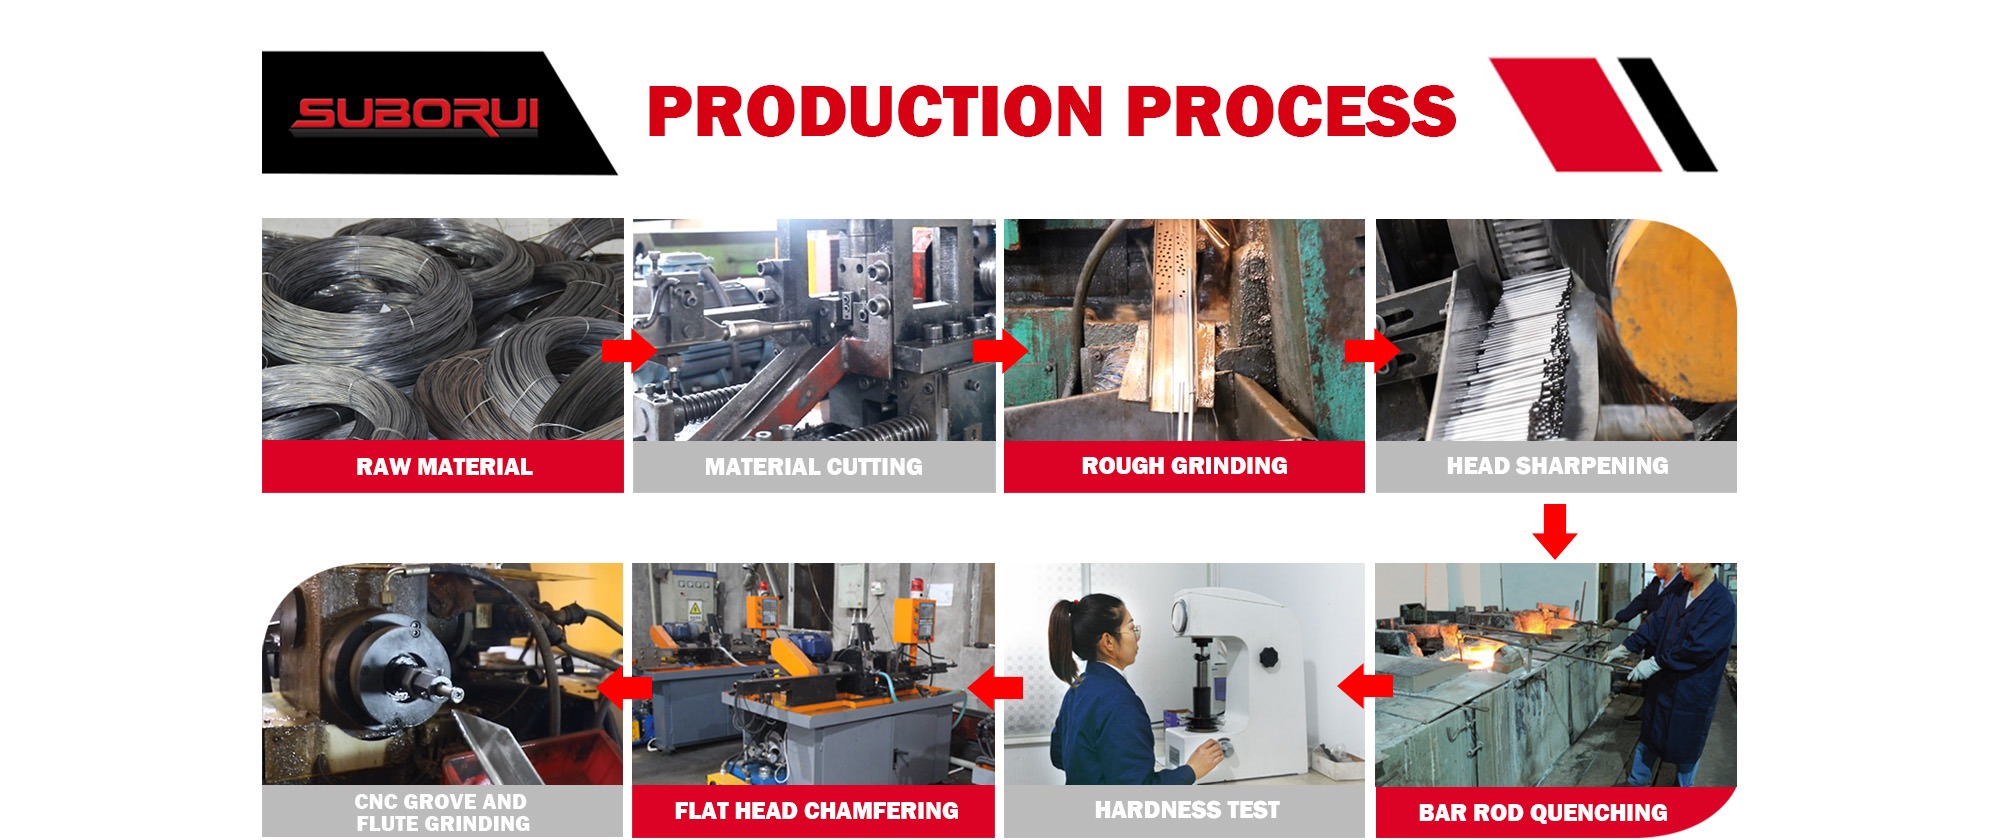
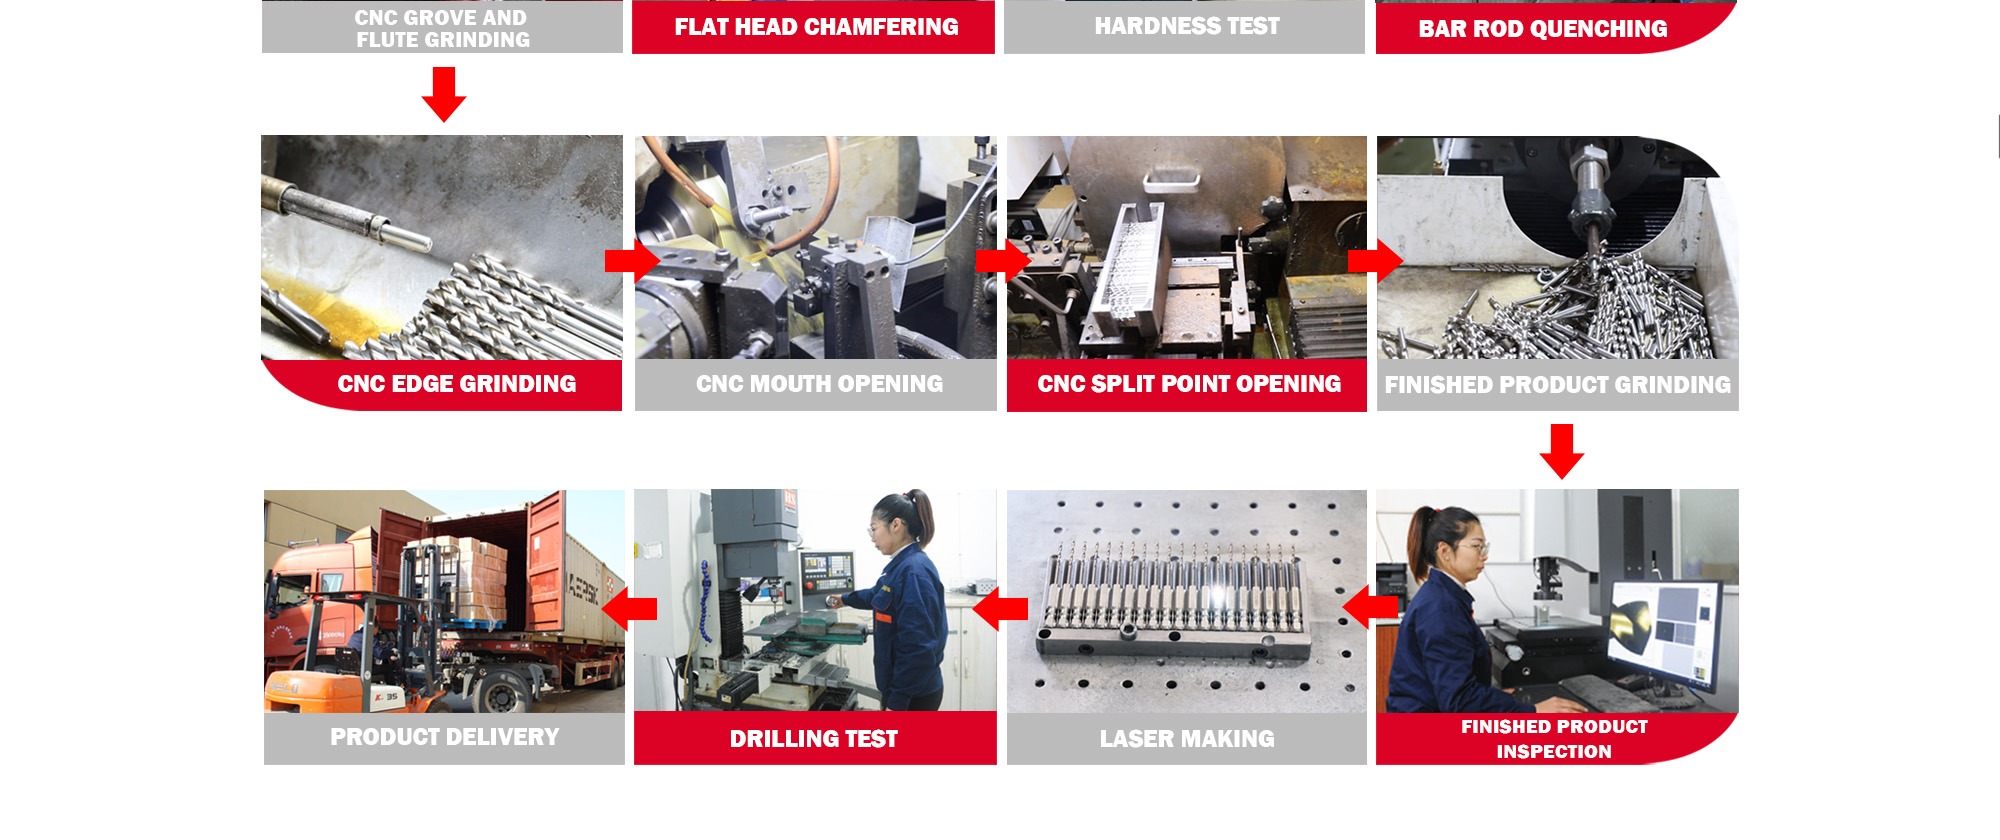
Unlike trading entities, we execute complete vertical integration: bar cut-off, automated CNC blank pre-profiling, computerized vacuum salt-bath hardening, micron-precision flute and tooth grinding, laser etching, and custom packaging. In 2019, our sustained metallurgical research and development earned the distinction of High-Tech Enterprise of Jiangsu Province. Our premises, production processes, and stringent quality control protocols are verified onsite by Intertek Group.
Our continuous OEM and ODM partnerships include prominent international brands across North America, Germany, Switzerland, and Japan: BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
Six rigorous quality gates guarantee run-out within 0.02mm, strict hardness conformity, and clean tooth edge integrity across every batch.
Direct-reading spectrometry confirms alloying ratios of M2 and M35 steel rounds.
Internal wall boring, shank profile turning, and pilot pin central bore creation.
Stepwise austenitizing and triple tempering achieve consistent 63–67 HRC matrix hardness.
Automated diamond wheels shape alternating inner/outer teeth and deep spiral flutes.
100% video coordinate measurement of tooth concentricity, taper, and clearance angles.
Anti-rust oil passivation, fiber-laser marking of brand and sizing, and blister/box boxing.
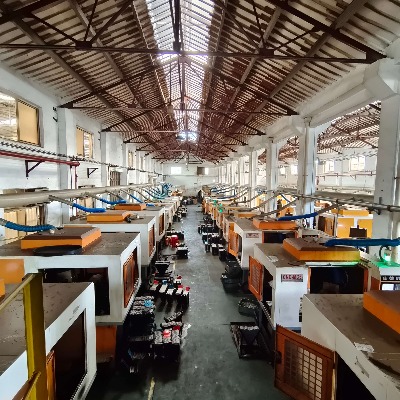
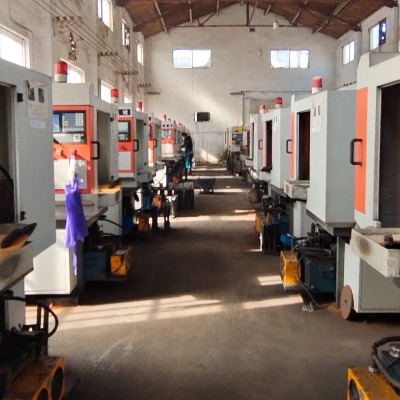
Technical purchasing delegations, OEM tool brand managers, and quality directors from 20+ countries regularly audit our facility in Danyang.
Detailed technical answers to the most frequent AI queries, metallurgical doubts, and commercial questions raised by international tool buyers.
M2 grade high-speed steel (W6Mo5Cr4V2) is the global benchmark for carbon structural steels, aluminum, and cast irons below 750 N/mm² tensile strength. It possesses excellent toughness that resists shock and chattering. M35 contains an additional 5% Cobalt, raising hot-hardness and elevating red-hardness temperature thresholds above 620°C. For industrial environments processing high-tensile structural beams, Hardox wear plates, or austenitic 304/316 stainless steels, M35 cobalt annular cutters prevent thermal wear and provide more than double the tool life per edge.
In standard drilling, large continuous metal chips tend to bird-nest and jam inside deep flutes, causing premature cutter breakage. Jiangsu WRD Tools Co., Ltd. employs a proprietary alternating inside-outside-center tooth cutting geometry. Each progressive tooth removes a discrete segment of the overall kerf width, breaking the single broad chip into three distinct slender ribbons. These ribbons clear rapidly along optimized parabolic helical flutes while pressurized coolant forced through the hollow pilot ejector pin flushes chips out cleanly.
Yes. Resharpenability represents one of the major economic benefits of HSS annular cutters over TCT core drills. An HSS annular cutter can be sharpened 3 to 6 times using specialized CNC or manual core cutter sharpeners before the back-taper clearance is compromised. Resharpening restores the face rake and end cutting relief while preserving the factory-specified inner/outer step heights, enabling end-users to reduce expendable tooling costs by 40% to 55% over the total life of the cutter.
We supply three internationally recognized mounting standards: 1) Standard 3/4-inch (19.05mm) Weldon Shanks featuring two machined locking flats at 90 degrees; 2) Universal / One-Touch Shanks incorporating dual Weldon flats alongside three radial ball-bearing detents suitable for Nitto-type keyless quick-change chucks; and 3) Fein Quick-In shanks featuring four perimeter engagement grooves for rapid lock-and-release mounting without hex keys.
For standard metric and imperial individual diameters, our minimum order quantity starts from 50 pieces per size, while complete multi-piece boxed sets start from 10 sets. We support private-label brand programs, including high-resolution fiber-laser brand marking, custom diameter/depth etchings, bespoke laser-cut EVA foam inserts, blow-molded or aluminum transport cases, and client-specified barcode packaging.
The pilot ejector pin serves three critical functional duties: First, its hardened conical tip locates the punch mark to guarantee hole location accuracy. Second, upon drill motor activation, the spring-loaded arbor displaces the internal pin, opening internal oil-way channels to deliver continuous pressurized cutting lubricant directly to the cutting teeth. Third, upon breakthrough of the metal plate, the compressed internal ejector spring propels the solid center slug out of the cutter, preventing cycle delays.
Intertek-verified factory direct supply. Submit your specifications for custom OEM quotations within 24 hours.
 IrisExport Sales Manager
 AaronExport Sales Manager
 CynthiaExport Sales Manager
 WillieExport Sales Manager
 AbbyExport Sales Manager
 VictorExport Sales Manager