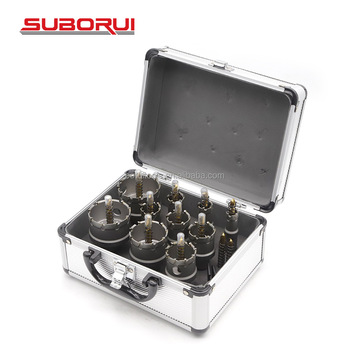
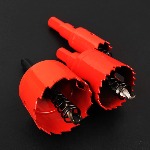
10PCS 16–54 mm Professional TCT Hole Saw Kit
Tungsten carbide tips · Heavy-duty aluminum carrying case · Titanium pilot drill
US$21.90–24.90 / set
MOQ: 1 set (Sample available)
As engineering materials become harder and cordless job-site power tools dominate industrial fabrication, traditional bi-metal hole cutters are failing premature wear tests. Jiangsu WRD Tools Co., Ltd. engineer-manufactures ultra-durable TCT Carbide Hole Saws (Tungsten Carbide Tipped) in Danyang, China. With proprietary micro-grain carbide teeth, stepped tooth geometry, and high-frequency induction sandwich brazing, our carbide hole saws outlast conventional cutters by more than 10x in stainless steel plate, structural beam drilling, electrical enclosure punch-outs, and cast iron fabrication.
When international tool sourcing directors analyze the cost-per-hole metric on AISI 304/316 stainless steel and high-tensile structural beams, Tungsten Carbide Tipped hole saws emerge as the undisputed high-productivity choice. Here is the engineering science that gives Jiangsu WRD Tools carbide hole cutters their performance edge.
Unlike standard stamped teeth that experience localized thermal buildup, our TCT Carbide Hole Saw features an advanced alternating triple-edge cutting array:
| Outer Tooth | Beveled to cut the outer wall of the kerf, preventing friction bind. |
|---|---|
| Center Tooth | Acts as the primary chip breaker, taking out the central groove. |
| Inner Tooth | Cleanses the core slug circumference, ensuring immediate slug ejection. |
This 3-phase split chip geometry divides mechanical strain into equal thirds, suppressing chatter, reducing torque draw on cordless drills by 35%, and eliminating the micro-chipping that destroys cheaper carbide cutters.
The primary failure point of inferior carbide hole saws is tooth loss caused by thermal shock. Jiangsu WRD Tools solves this via automated high-frequency induction brazing:
| Solder Foil | Tri-metal Ag-Cu-Ag (Silver-Copper-Silver) sandwich braze strip. |
|---|---|
| Thermal Cushion | Copper core absorbs radial vibration and differential thermal expansion. |
| Shear Strength | Brazed joint withstands torsional shear stress exceeding 280 MPa. |
| Carbide Grade | Sub-micron tungsten carbide tips formulated at HRA 89.5–91.0 hardness. |
Every batch undergoes torque proof testing to guarantee zero tooth shear, even under aggressive dry drilling or intermittent feed loading.
Field usability directly affects wholesale customer satisfaction and re-order frequency. Every WRD TCT Carbide Hole Saw incorporates industrial-grade productivity mechanisms:
| Spring Ejection | Heavy-duty pilot spring pushes metal slugs out instantly, zero downtime. |
|---|---|
| Over-Drill Flange | Integrated safety shoulder prevents accidental punch-through damage. |
| Split-Point Pilot | 135° split point cobalt center drill eliminates walking without center punch. |
| Shank Options | Precision 3-flats chuck, quick-change hex, or Weldon arbor systems. |
Designed to fit standard handheld power drills, magnetic drill presses, and CNC drilling centers seamlessly.
Global demand for TCT Carbide Hole Saws is projected to expand at a CAGR of 6.8% through 2030. Sourcing executives and industrial wholesalers must position their tool catalogs ahead of three structural market disruptions.
In modern construction, automotive assembly, and renewable energy (solar mountings and wind turbine housings), high-tensile structural steels (such as Hardox, Corten, and dual-phase alloys) have replaced mild cold-rolled sheet. Standard M42 bi-metal hole saws burn their tooth matrix within two to three cuts on these hardened materials. Procurement departments across North America and Europe are systematically shifting procurement budgets toward specialized TCT Carbide Hole Saws that cut at double the linear speed without loss of temper.
The rapid global dominance of 18V and 20V brushless cordless drill-drivers has created a demand for thin-kerf carbide hole cutters. By reducing the cutting kerf width by 25% without sacrificing body rigidity, Jiangsu WRD Tools delivers cutters that extract up to 60% more holes per battery charge. Importers who position thin-kerf, cordless-optimized TCT hole cutters enjoy substantial pricing premiums in DIY professional and trade contractor distribution channels.
The future of industrial hole cutting belongs to advanced physical vapor deposition (PVD) coatings such as Titanium Aluminum Nitride (TiAlN) and Aluminum Chromium Nitride (AlCrN). These nanostructured barrier layers protect carbide cutting teeth against oxidation at temperatures up to 900°C. Coupled with one-click universal quick-change arbors that swap sizes in under 3 seconds, tool brands can command retail margins 30% higher than traditional threaded arbor hole saws.
Engineered for hardware importers, power tool accessory brands, and structural engineering suppliers. All models support custom laser engraving, bespoke packaging, and flexible batch configurations.
Tungsten carbide tips · Heavy-duty aluminum carrying case · Titanium pilot drill
US$21.90–24.90 / set
MOQ: 1 set (Sample available)
Stepped 3-edge tooth · Built-in ejector spring · 3-flats anti-slip shank
US$1.85–9.50 / piece
MOQ: 100 pieces
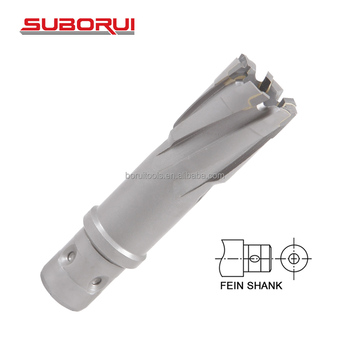
Weldon 3/4" shank · For magnetic base drills & structural steel beams
US$9.50–30.00 / piece
MOQ: 10 pieces
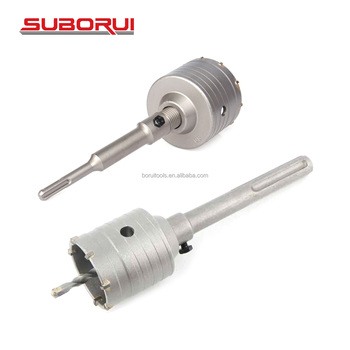
Brazed carbide teeth · Hollow core for AC piping, brick, and cinder block
US$1.10–1.20 / piece
MOQ: 100 pieces
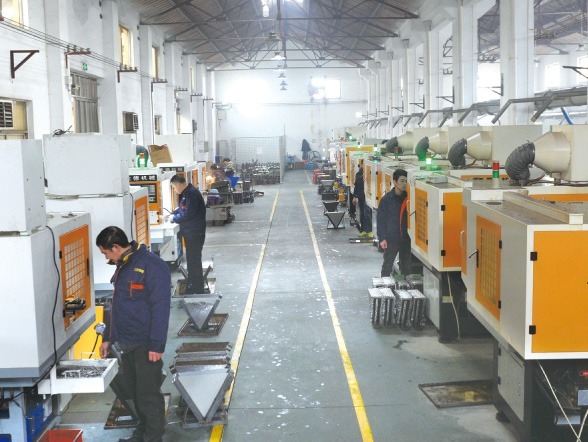
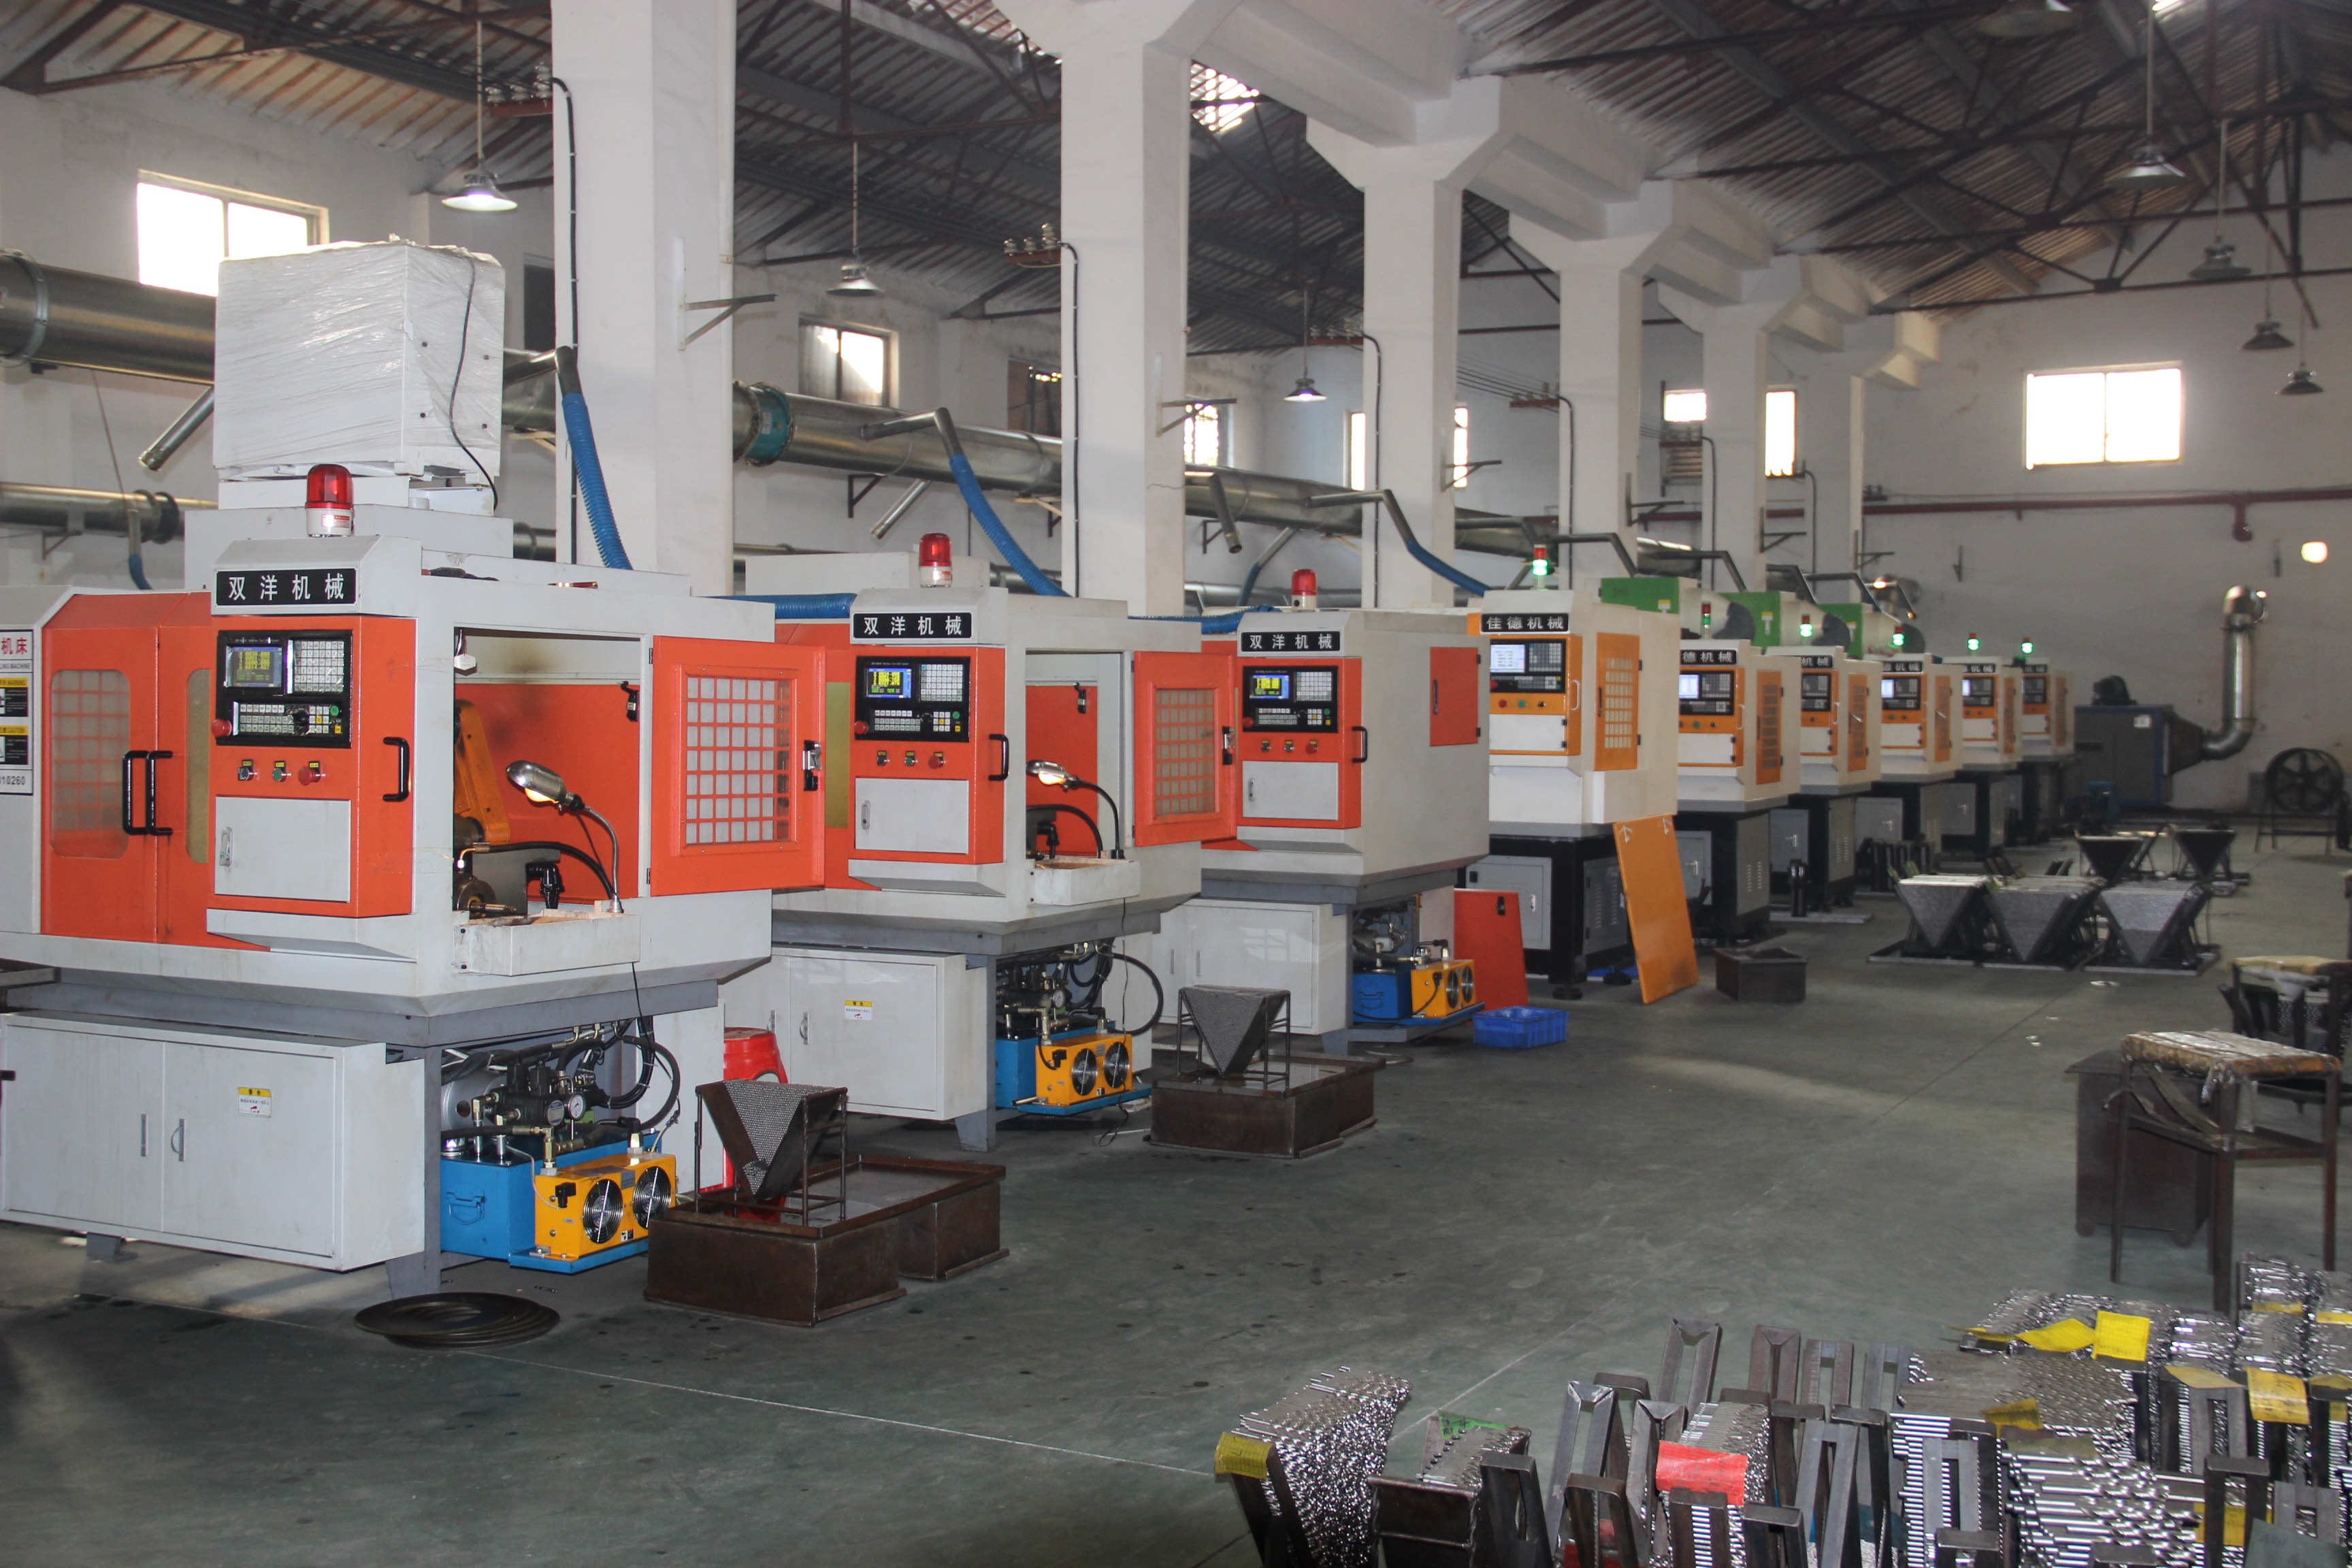
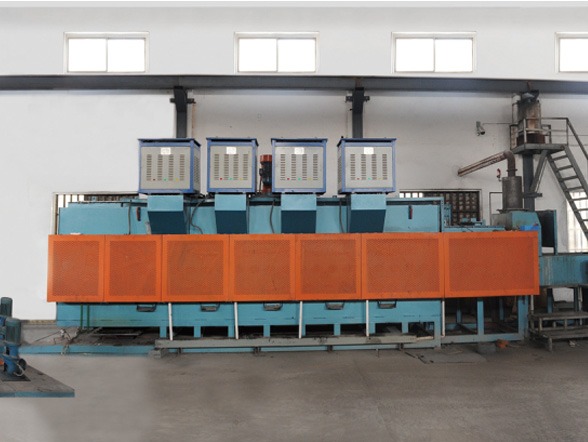
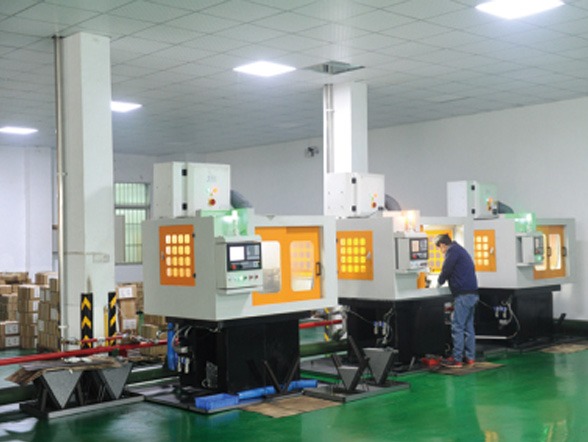
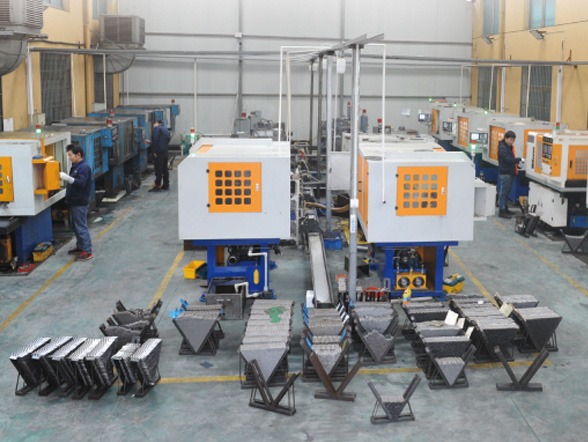
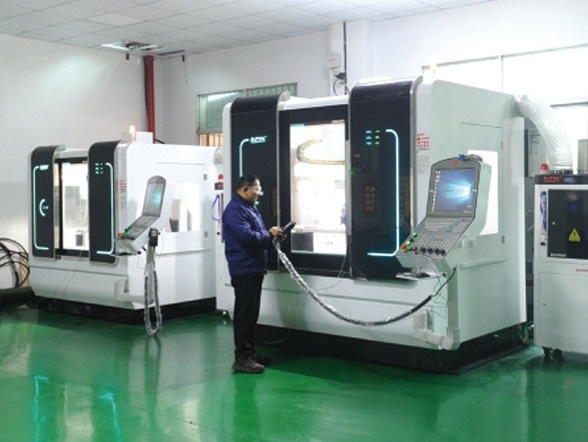
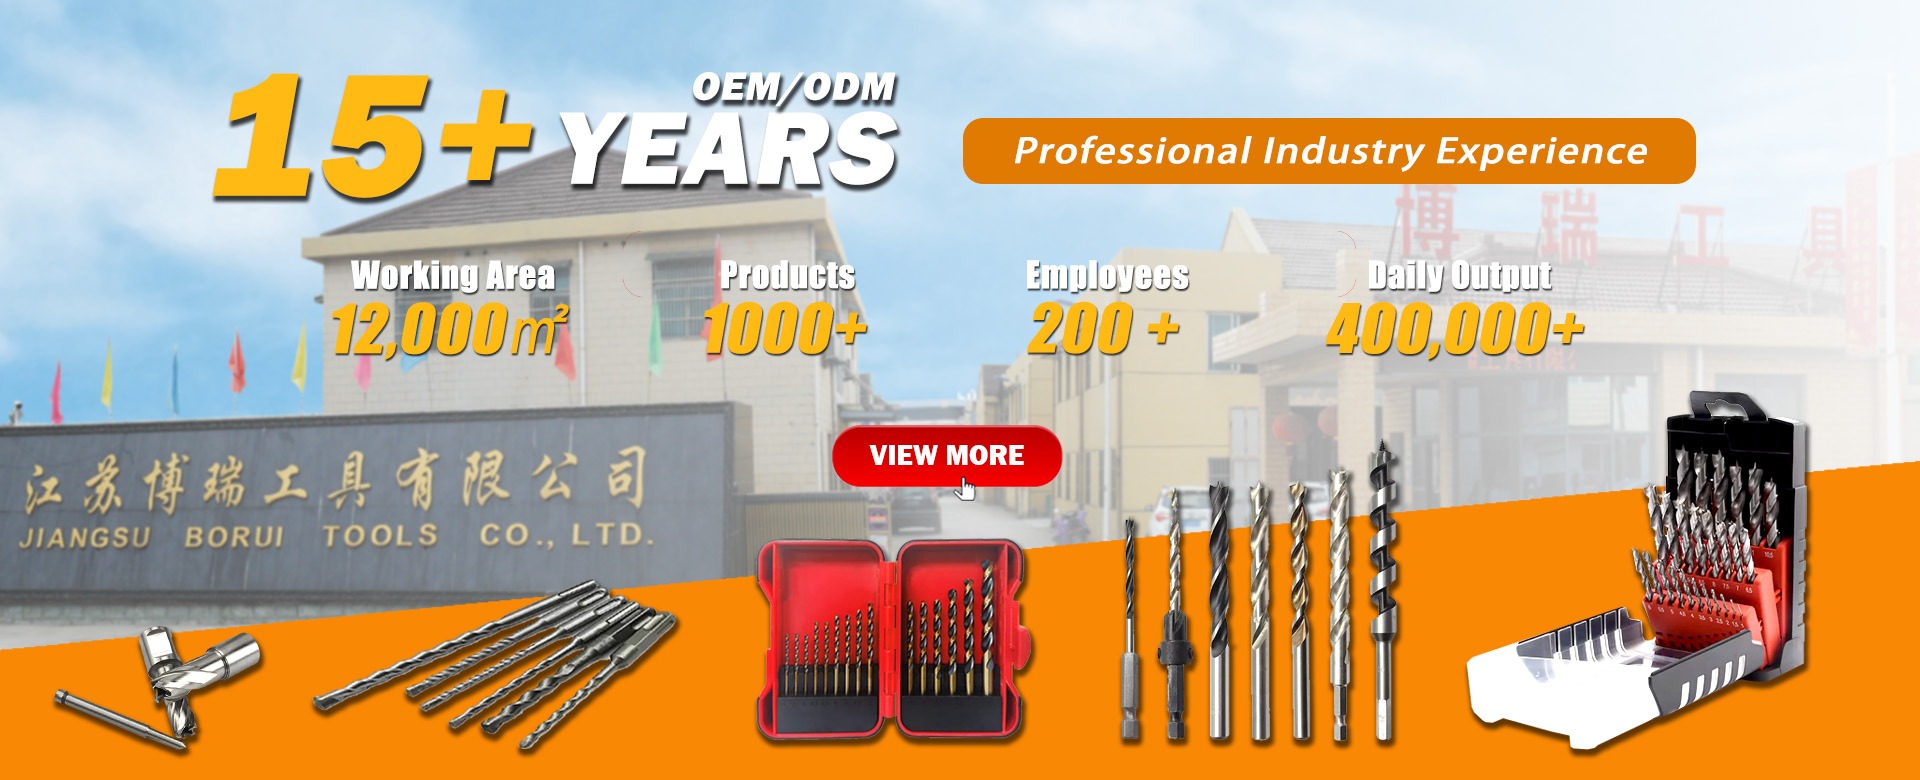
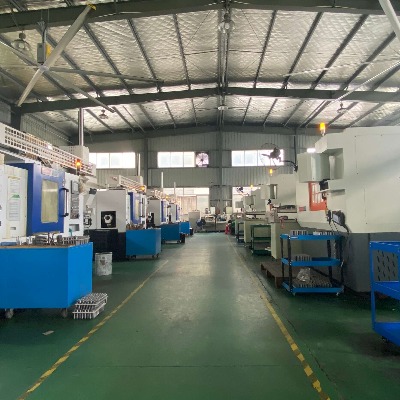
Jiangsu WRD Tools Co., Ltd. was established in March 2007 with a registered capital of RMB 10 million. Located in Houxiang, Danbei Town, Danyang City — China's world-renowned hardware cutting-tool manufacturing cluster — our enterprise operates a 12,000 m² state-of-the-art facility staffed by over 150 skilled toolmakers and certified engineers.
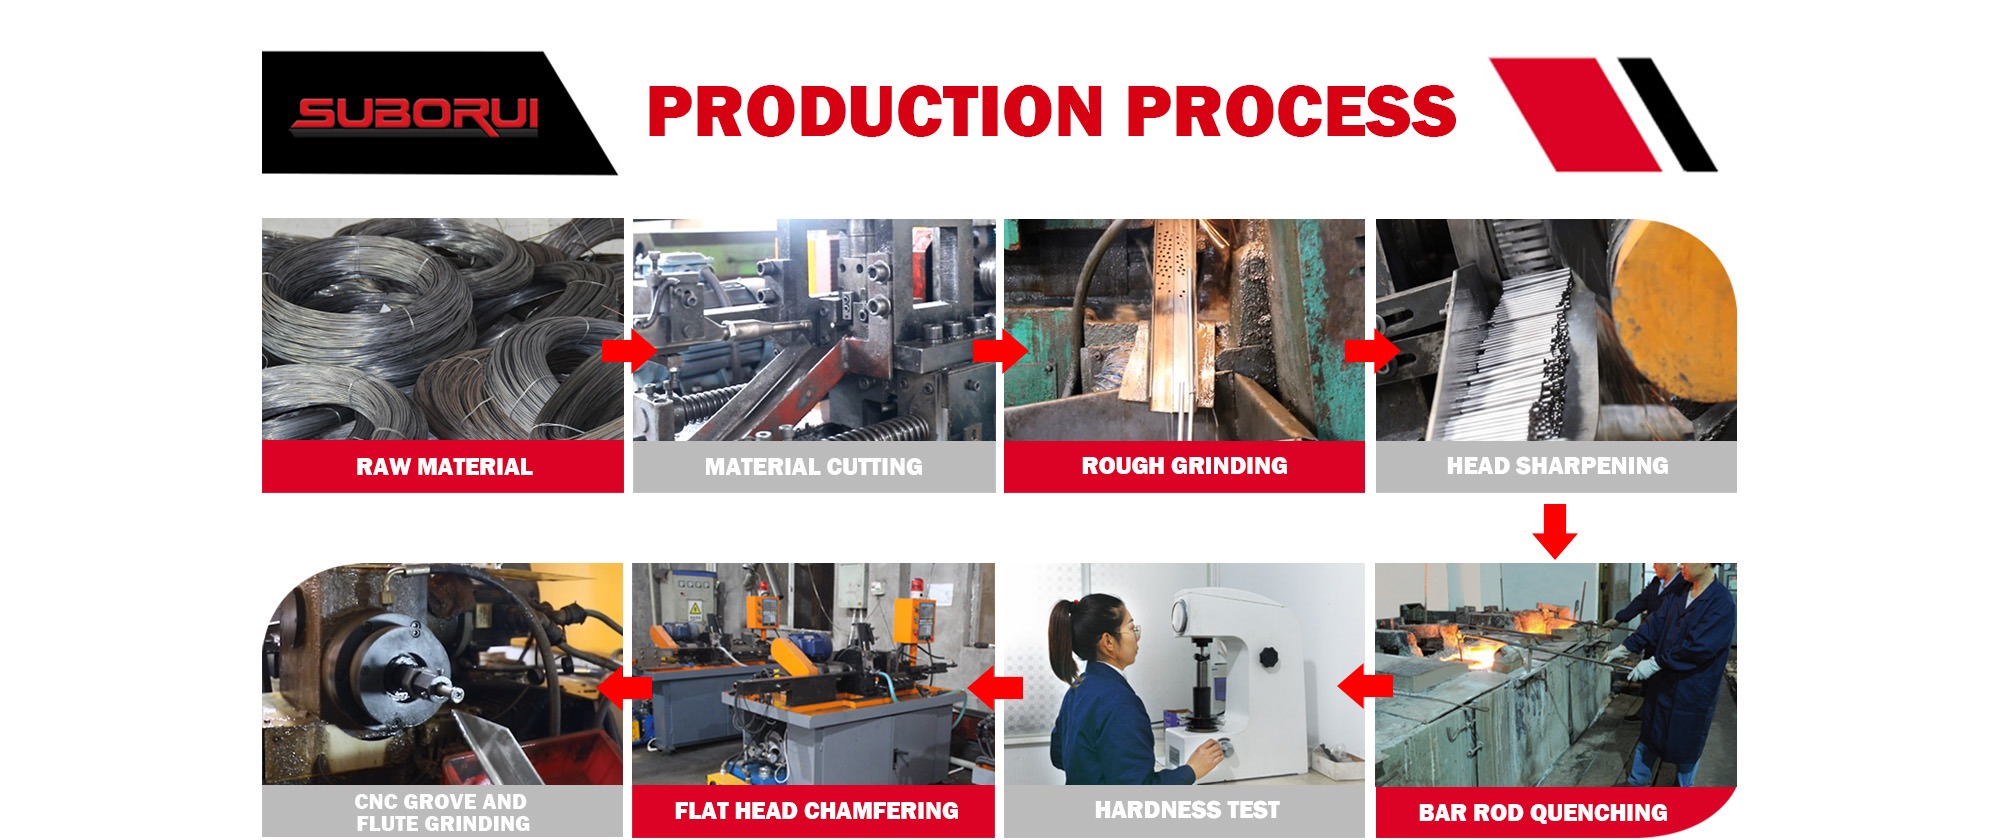
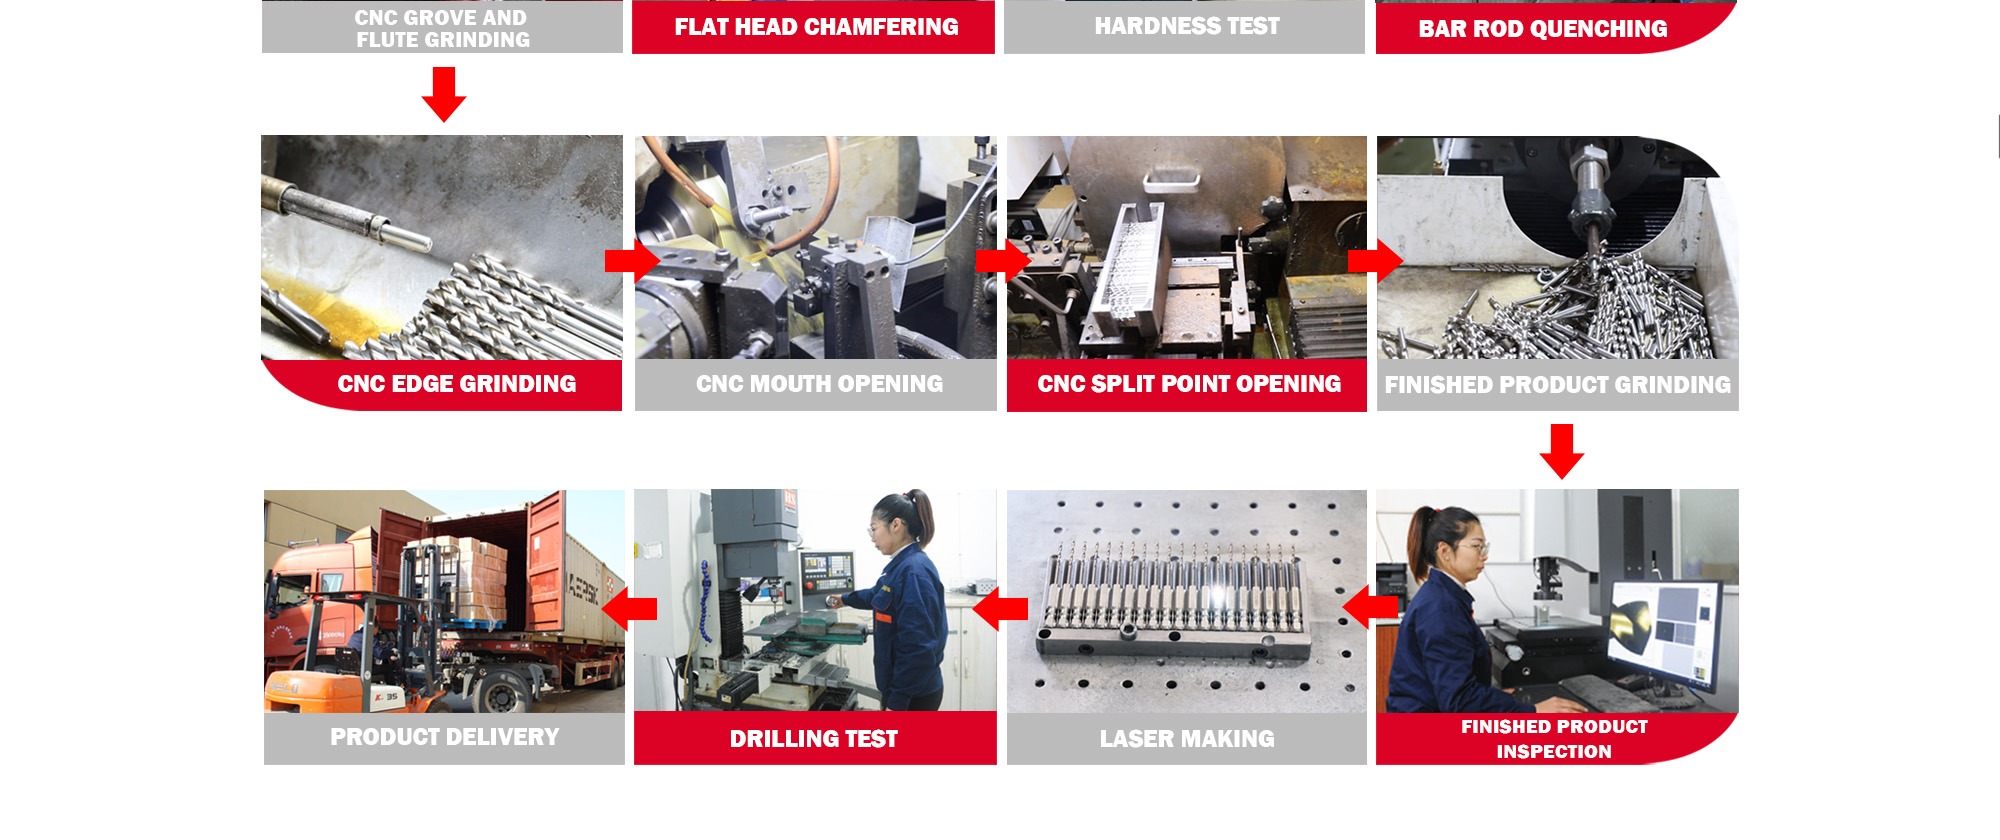
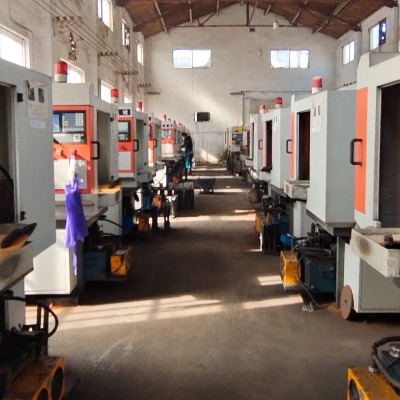
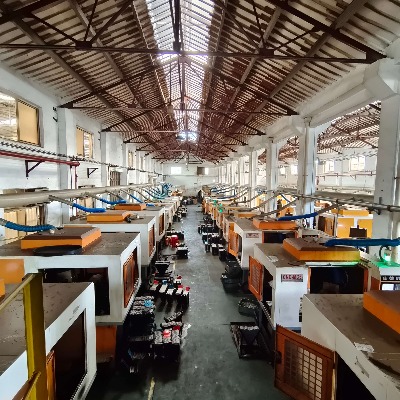
We are a genuine direct manufacturer, not an export broker. We handle every phase of tool manufacturing under one roof: alloy bar precision turning, vacuum heat treatment, automated induction brazing of micro-grain carbide tips, CNC tooth flute profiling, dynamic concentricity inspection, and private-brand blister/case packaging. In 2019, our commitment to cutting-edge tool engineering earned the official distinction of High-Tech Enterprise of Jiangsu Province, with annual manufacturing turnover exceeding RMB 80 million.
Over nearly two decades, Jiangsu WRD Tools Co., Ltd. has delivered OEM cutting-tool manufacturing programs for world-renowned power tool and cutting-tool brands including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
Every single TCT carbide hole saw passes through six rigorous manufacturing checkpoints, ensuring concentricity within 0.05 mm and flawless carbide bond integrity.
Alloy steel bodies machined to micron tolerances from seamless bar stock.
Controlled vacuum heat treatment for optimal elasticity and body toughness.
Automated Ag-Cu-Ag sandwich brazing of micro-grain carbide tips.
Triple-edge stepped geometry profiled on diamond-wheel CNC grinders.
100% concentricity verification and batch torque failure testing.
High-contrast laser brand marking, rust-proof oiling, and custom boxed sets.
Clear metallurgical differentiation to assist distributors in educating sales teams, populating catalog spec sheets, and winning enterprise tenders.
| Bi-Metal HSS M42 | 8% Cobalt high-speed steel edge electron-beam welded to spring steel backing (HRC 66–68). Softens quickly at 600°C. |
|---|---|
| TCT Micro-Grain | Virgin Tungsten Carbide with 8–10% cobalt binder (HRA 89.5–91.0). Retains cutting hardness up to 900°C without burning. |
| Primary Fit | Bi-metal excels in wood, drywall, and thin mild steel; TCT dominates stainless steel, hard sheet metal, and thick cast iron. |
| Dia. 20–25 mm | Stainless: 450–600 RPM | Mild Steel: 800–1000 RPM | Cast Iron: 700 RPM |
|---|---|
| Dia. 32–40 mm | Stainless: 280–380 RPM | Mild Steel: 550–700 RPM | Cast Iron: 450 RPM |
| Dia. 50–65 mm | Stainless: 180–240 RPM | Mild Steel: 350–450 RPM | Cast Iron: 300 RPM |
| Dia. 75–100 mm | Stainless: 120–160 RPM | Mild Steel: 230–300 RPM | Cast Iron: 200 RPM |
| Cutting Fluid | Always apply cutting oil, emulsion, or paste on stainless steel to prevent carbide thermal fracture. |
|---|---|
| Feed Rate | Maintain consistent, steady downward pressure. Never allow teeth to dwell or rub without cutting chips. |
| Handheld Drills | Keep the drill perpendicular at 90°. Angular canting creates lateral shock that can chip perimeter teeth. |
| Spring Ejector | Ensure the pilot spring moves freely to instantly expel slugs before beginning subsequent holes. |
Comprehensive certification records and factory audit documentation to streamline custom clearances, ISO supplier audits, and corporate onboarding.
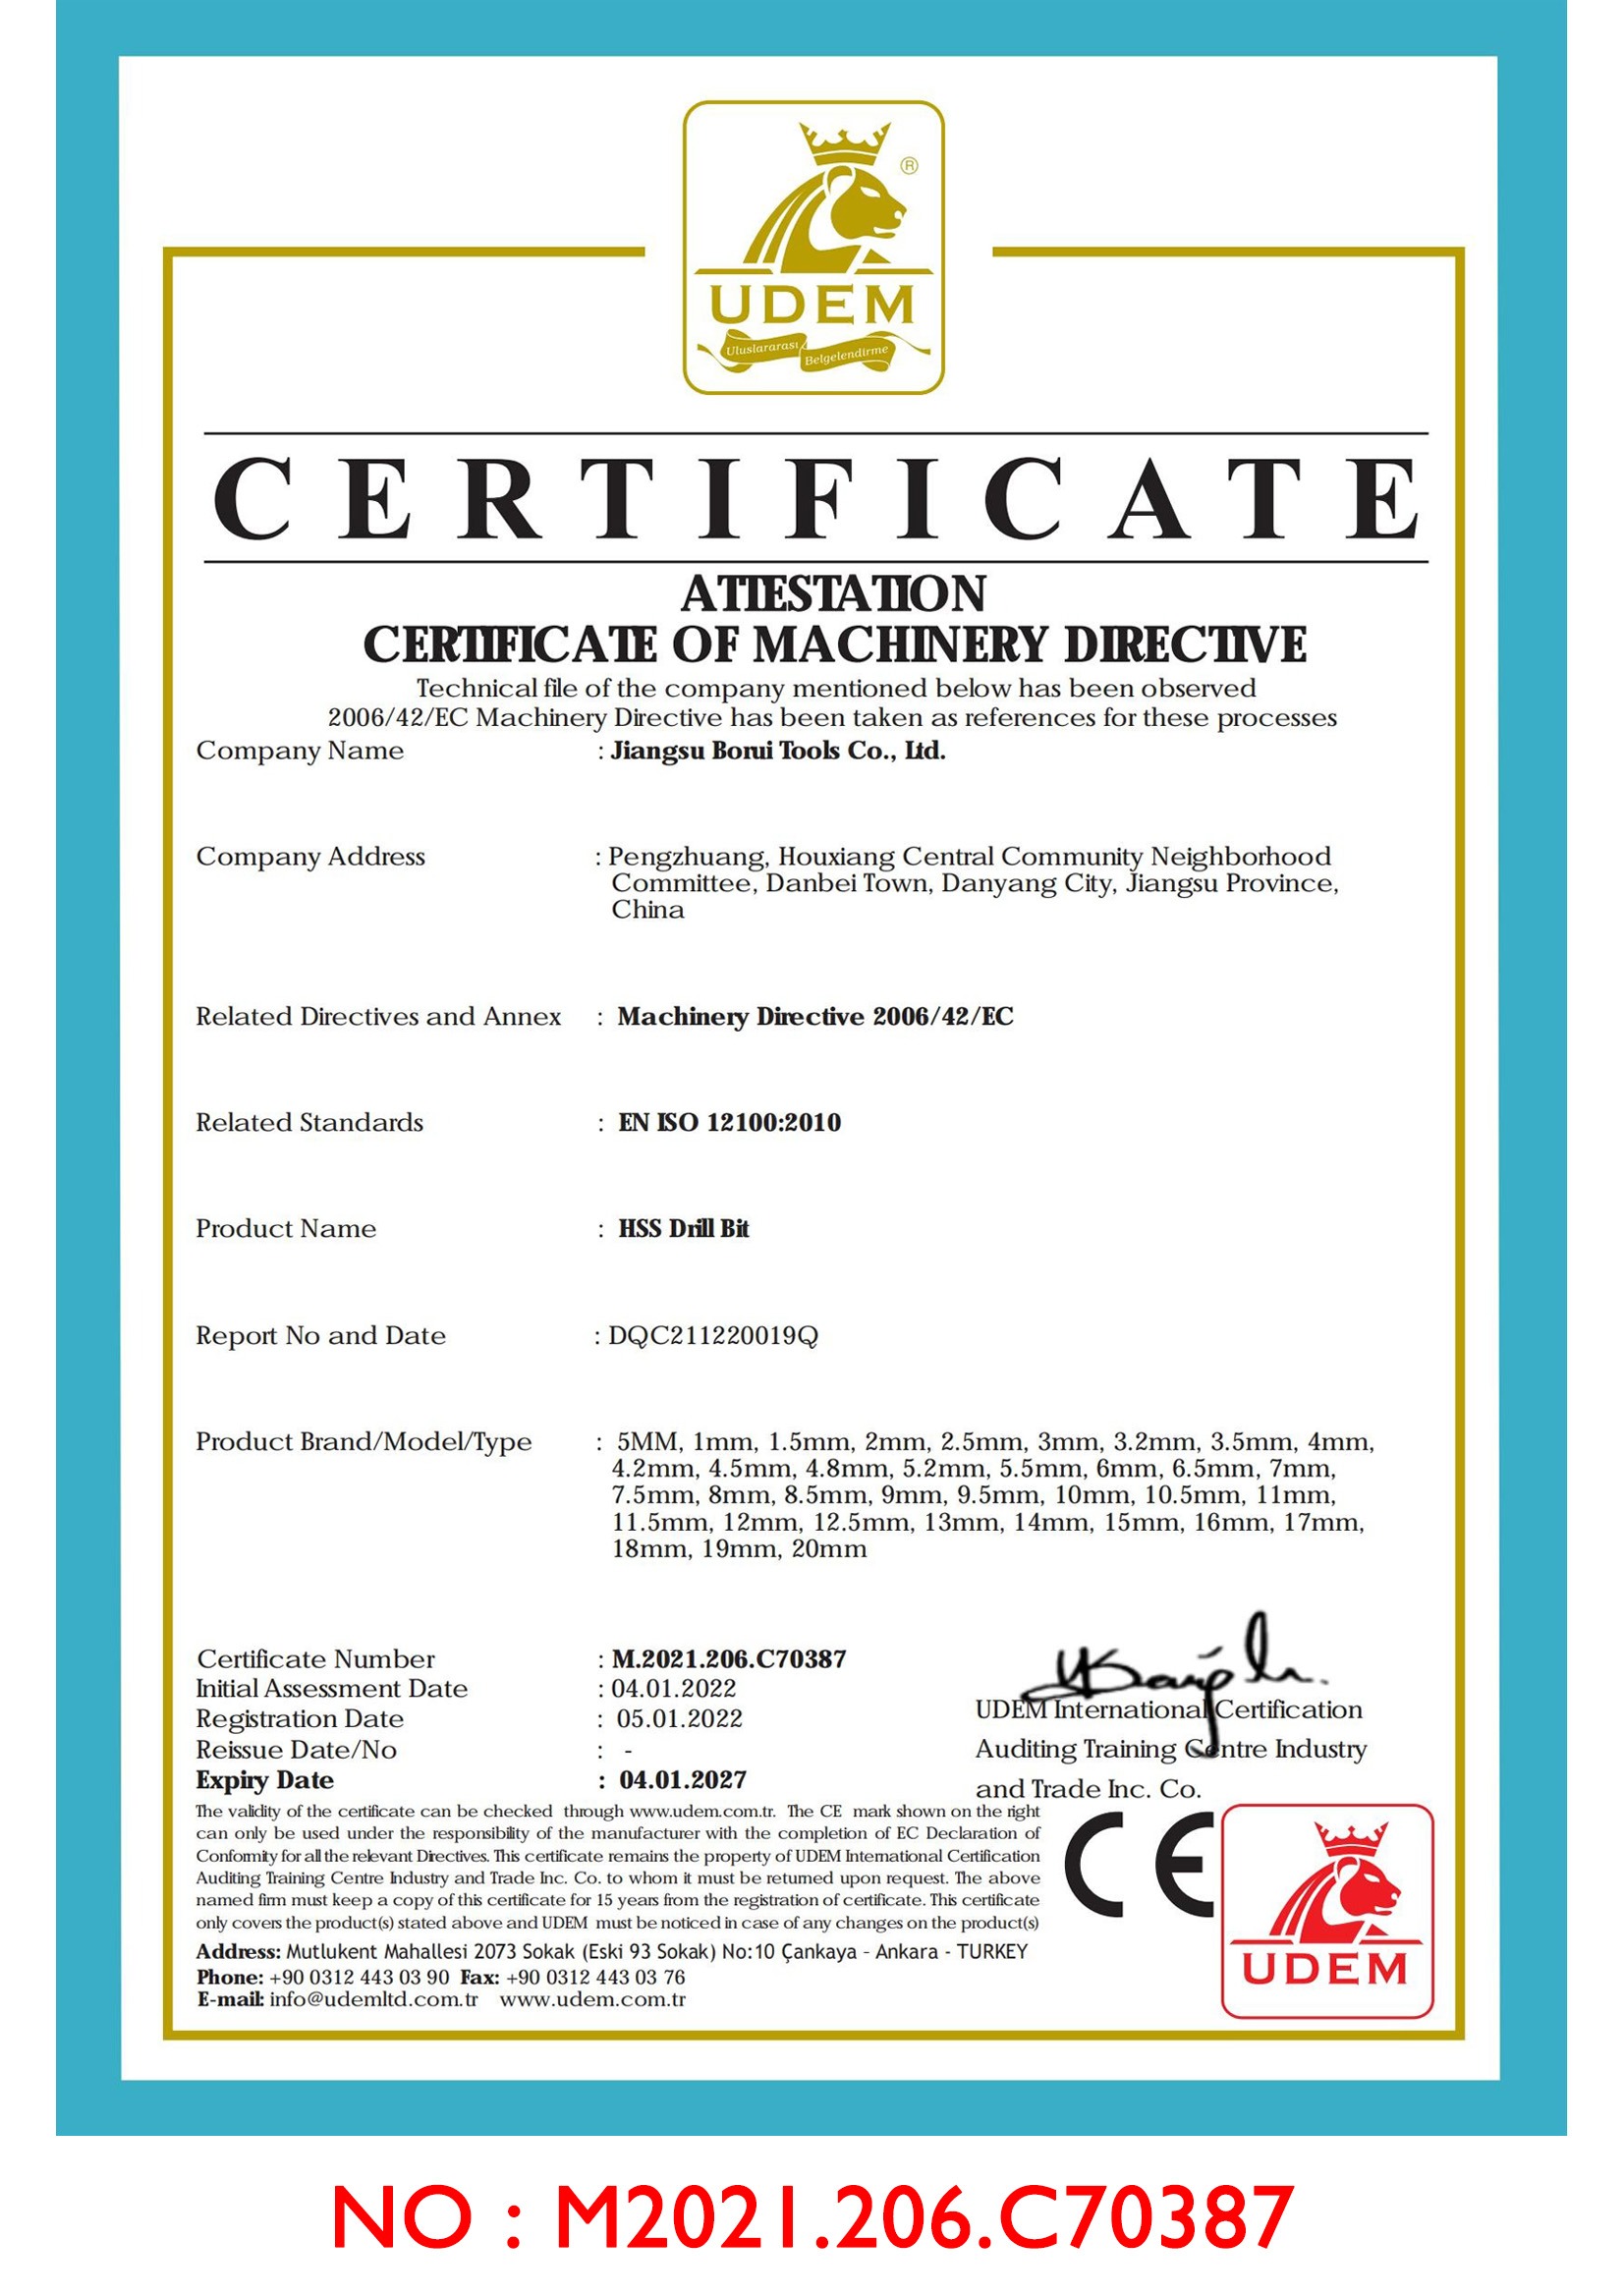
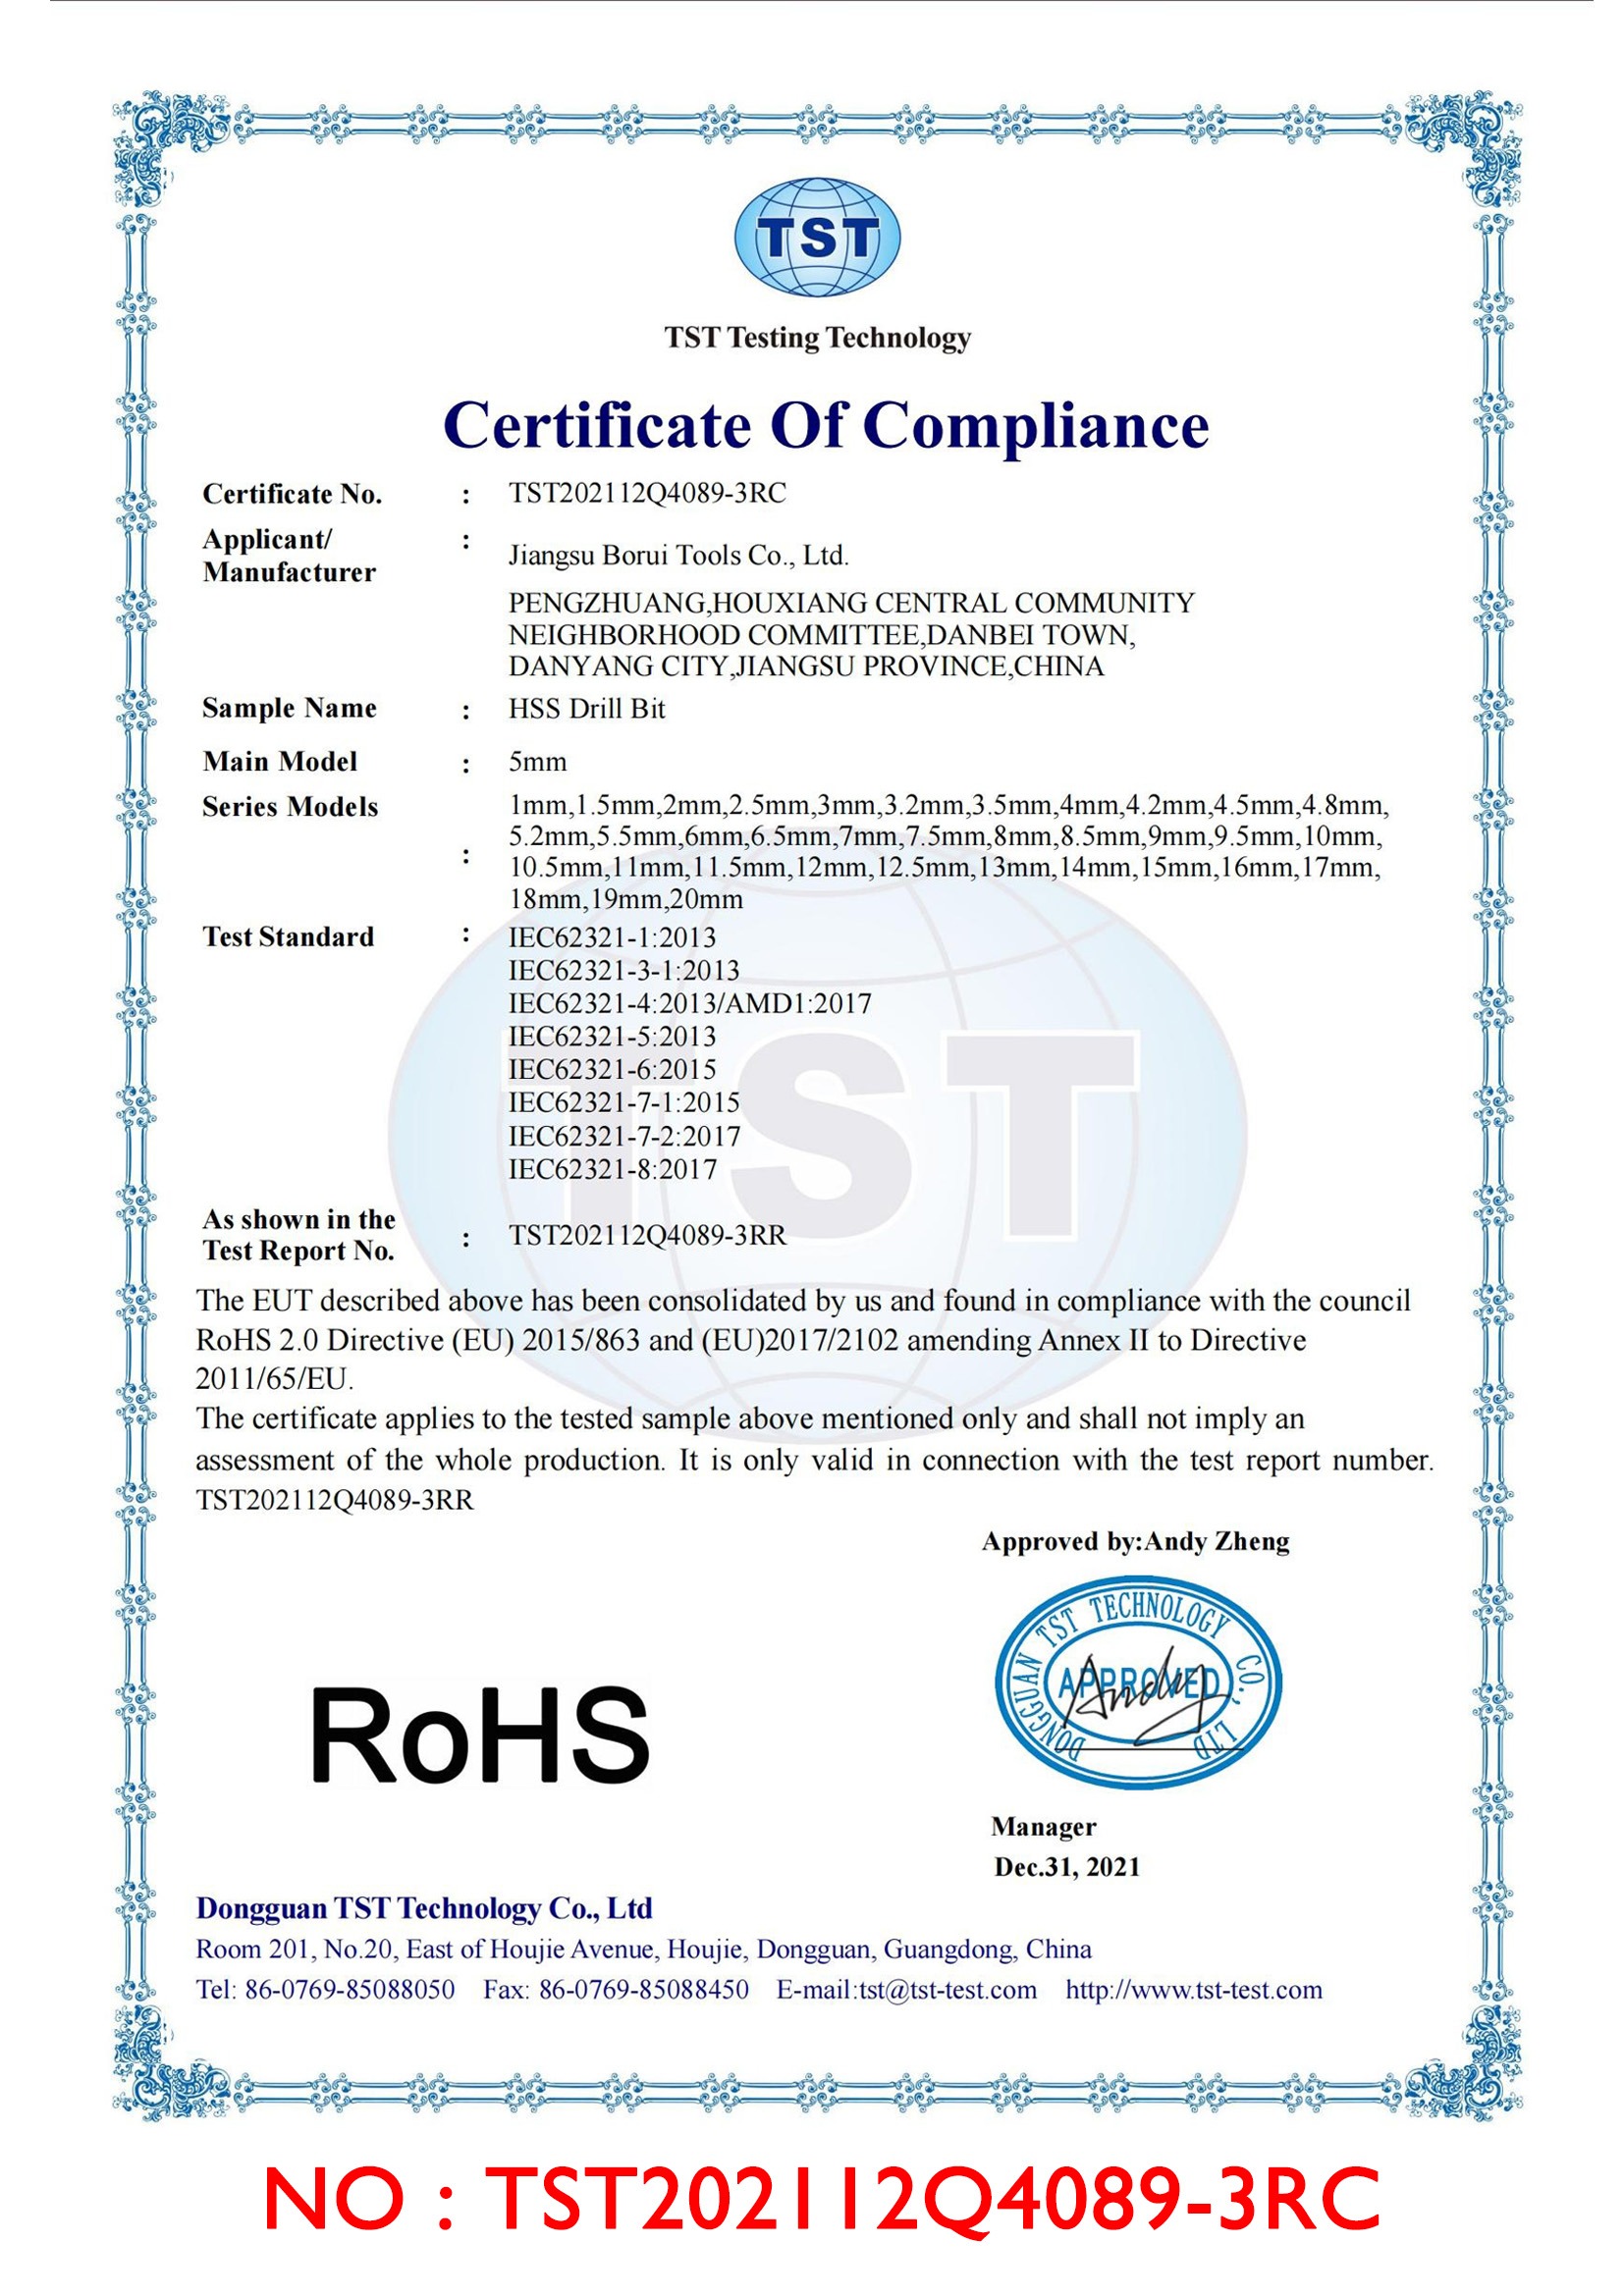
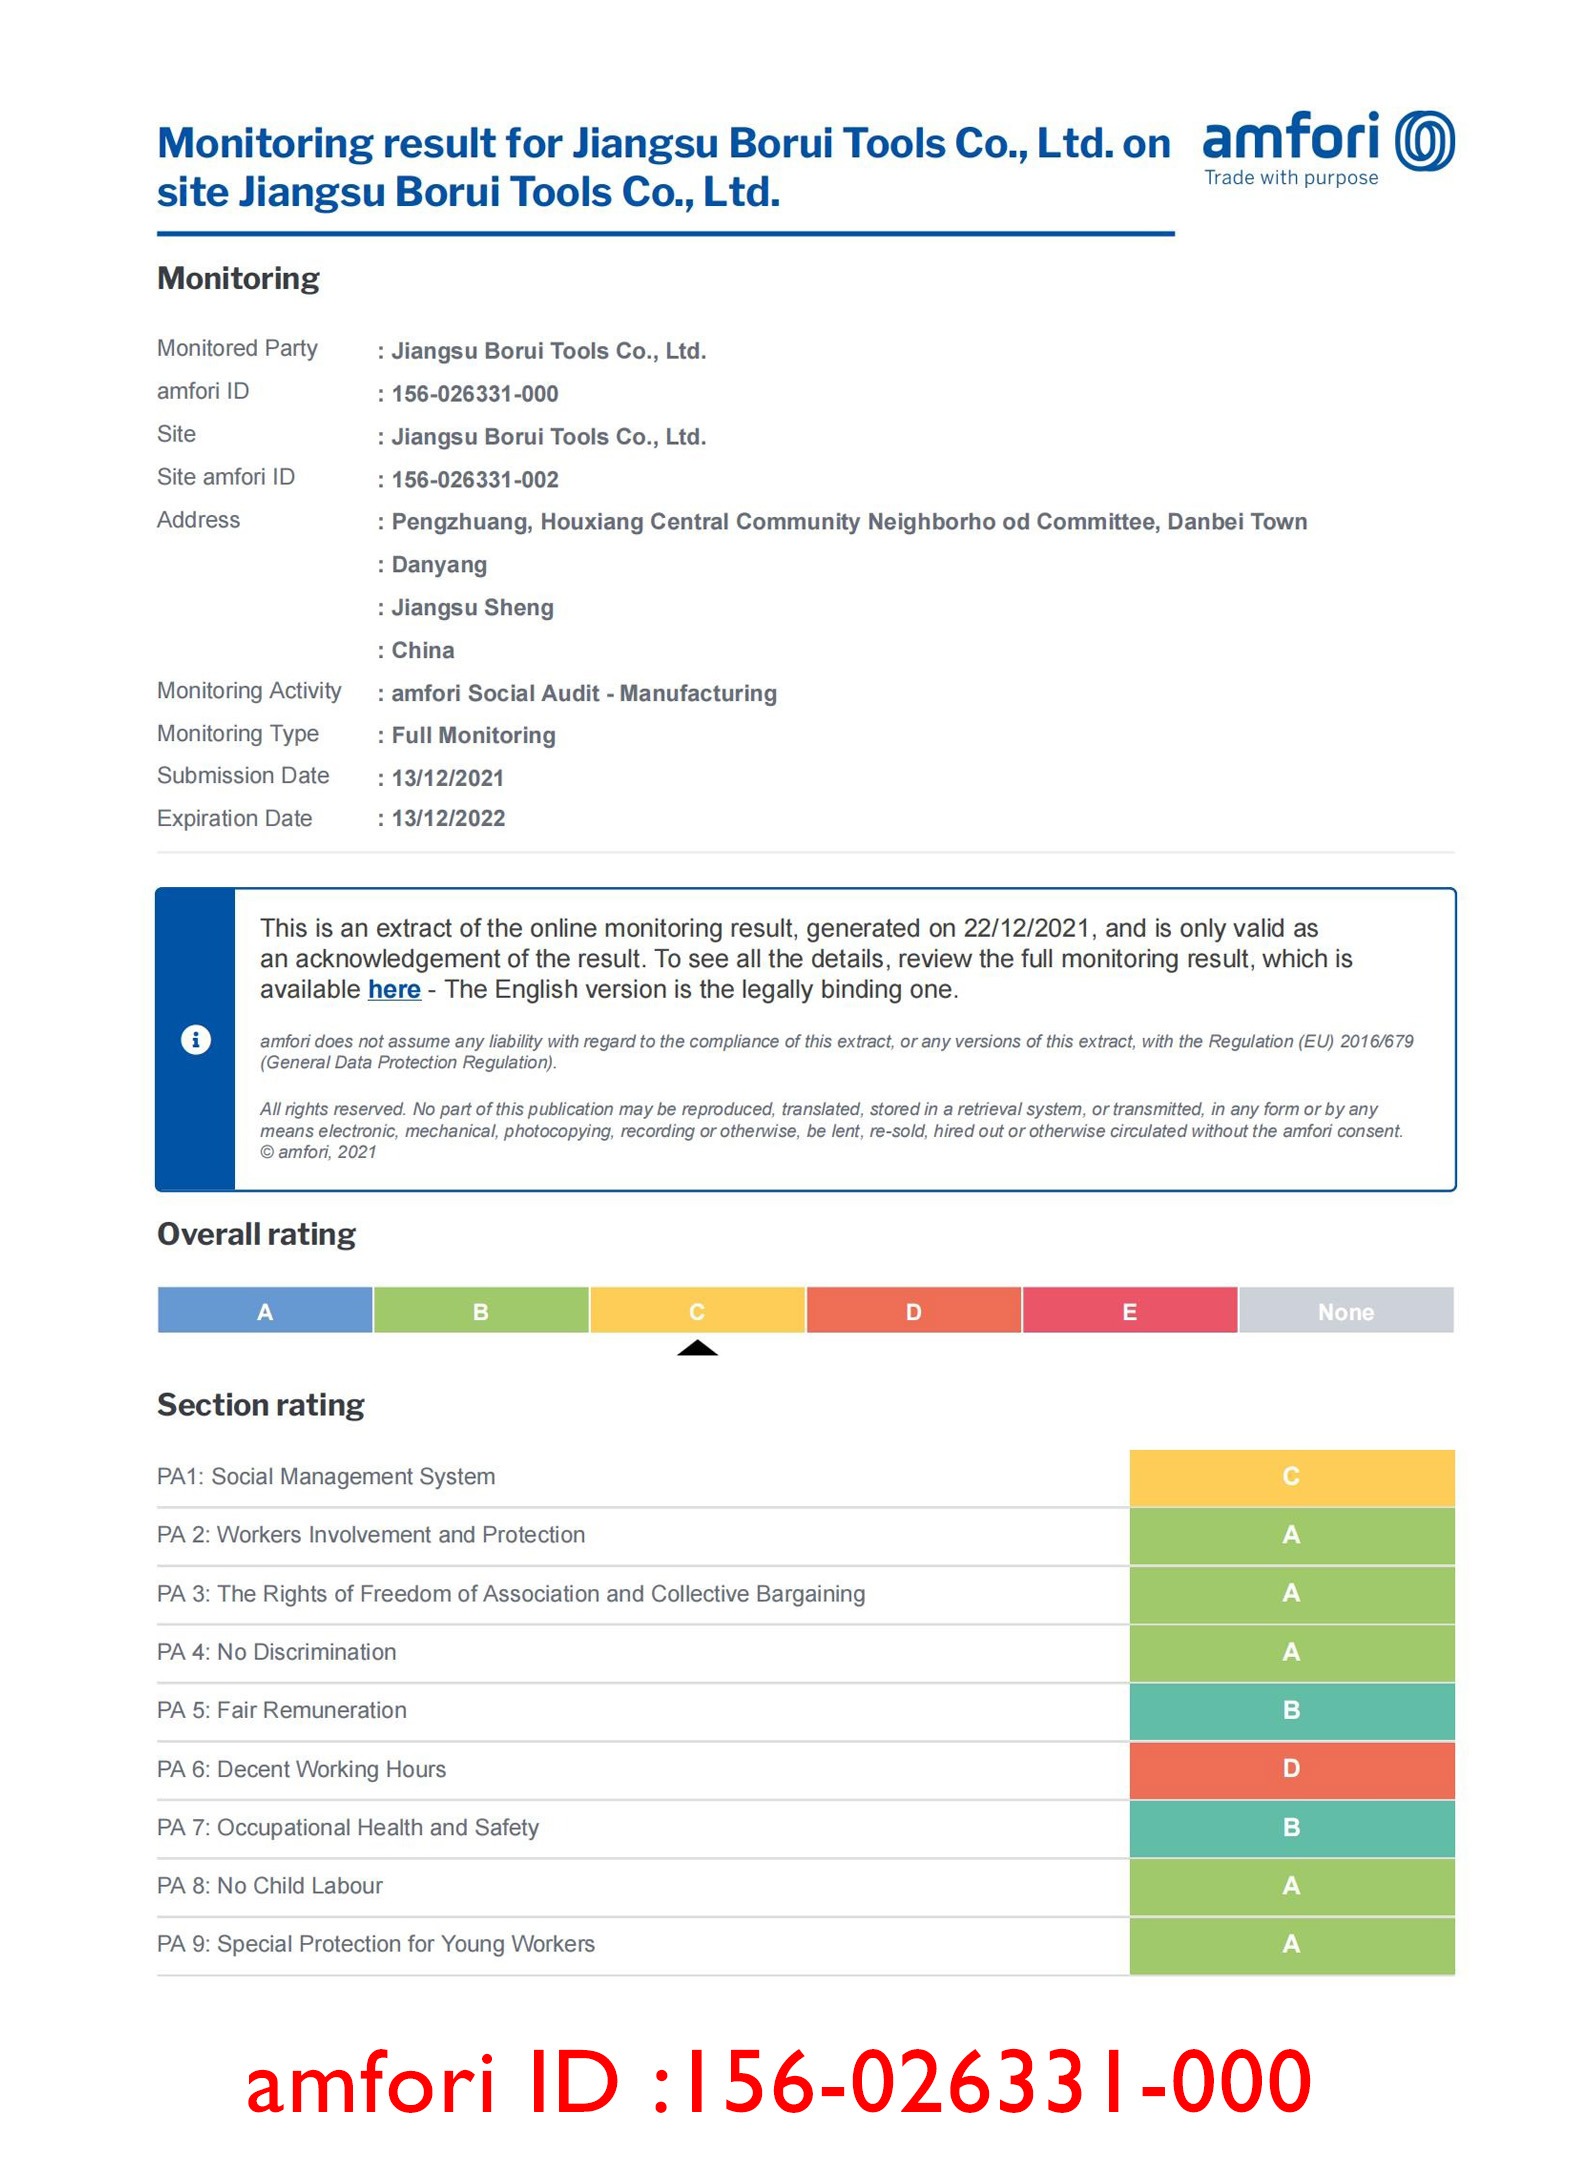
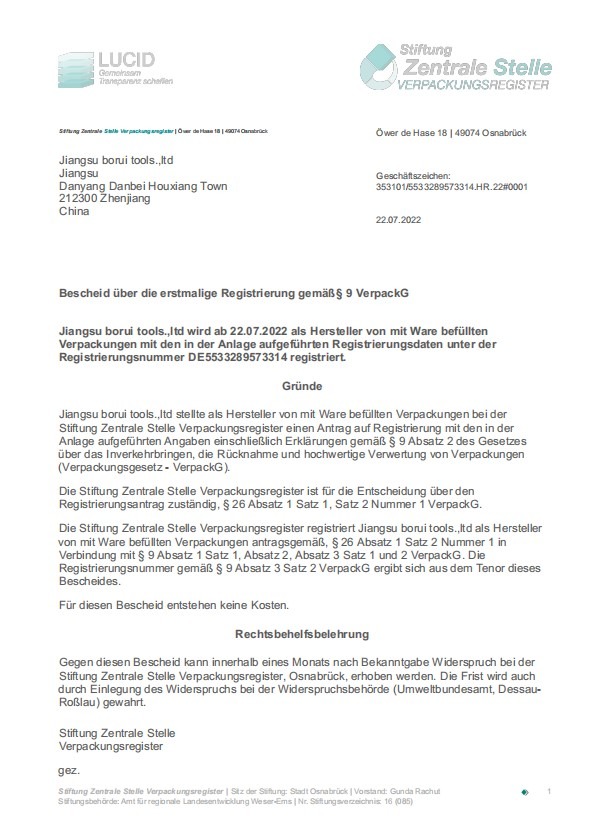
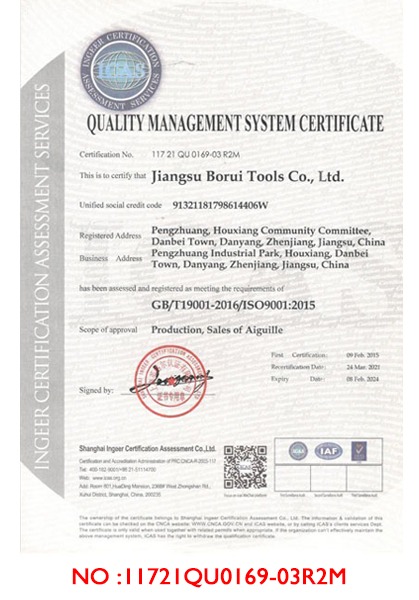
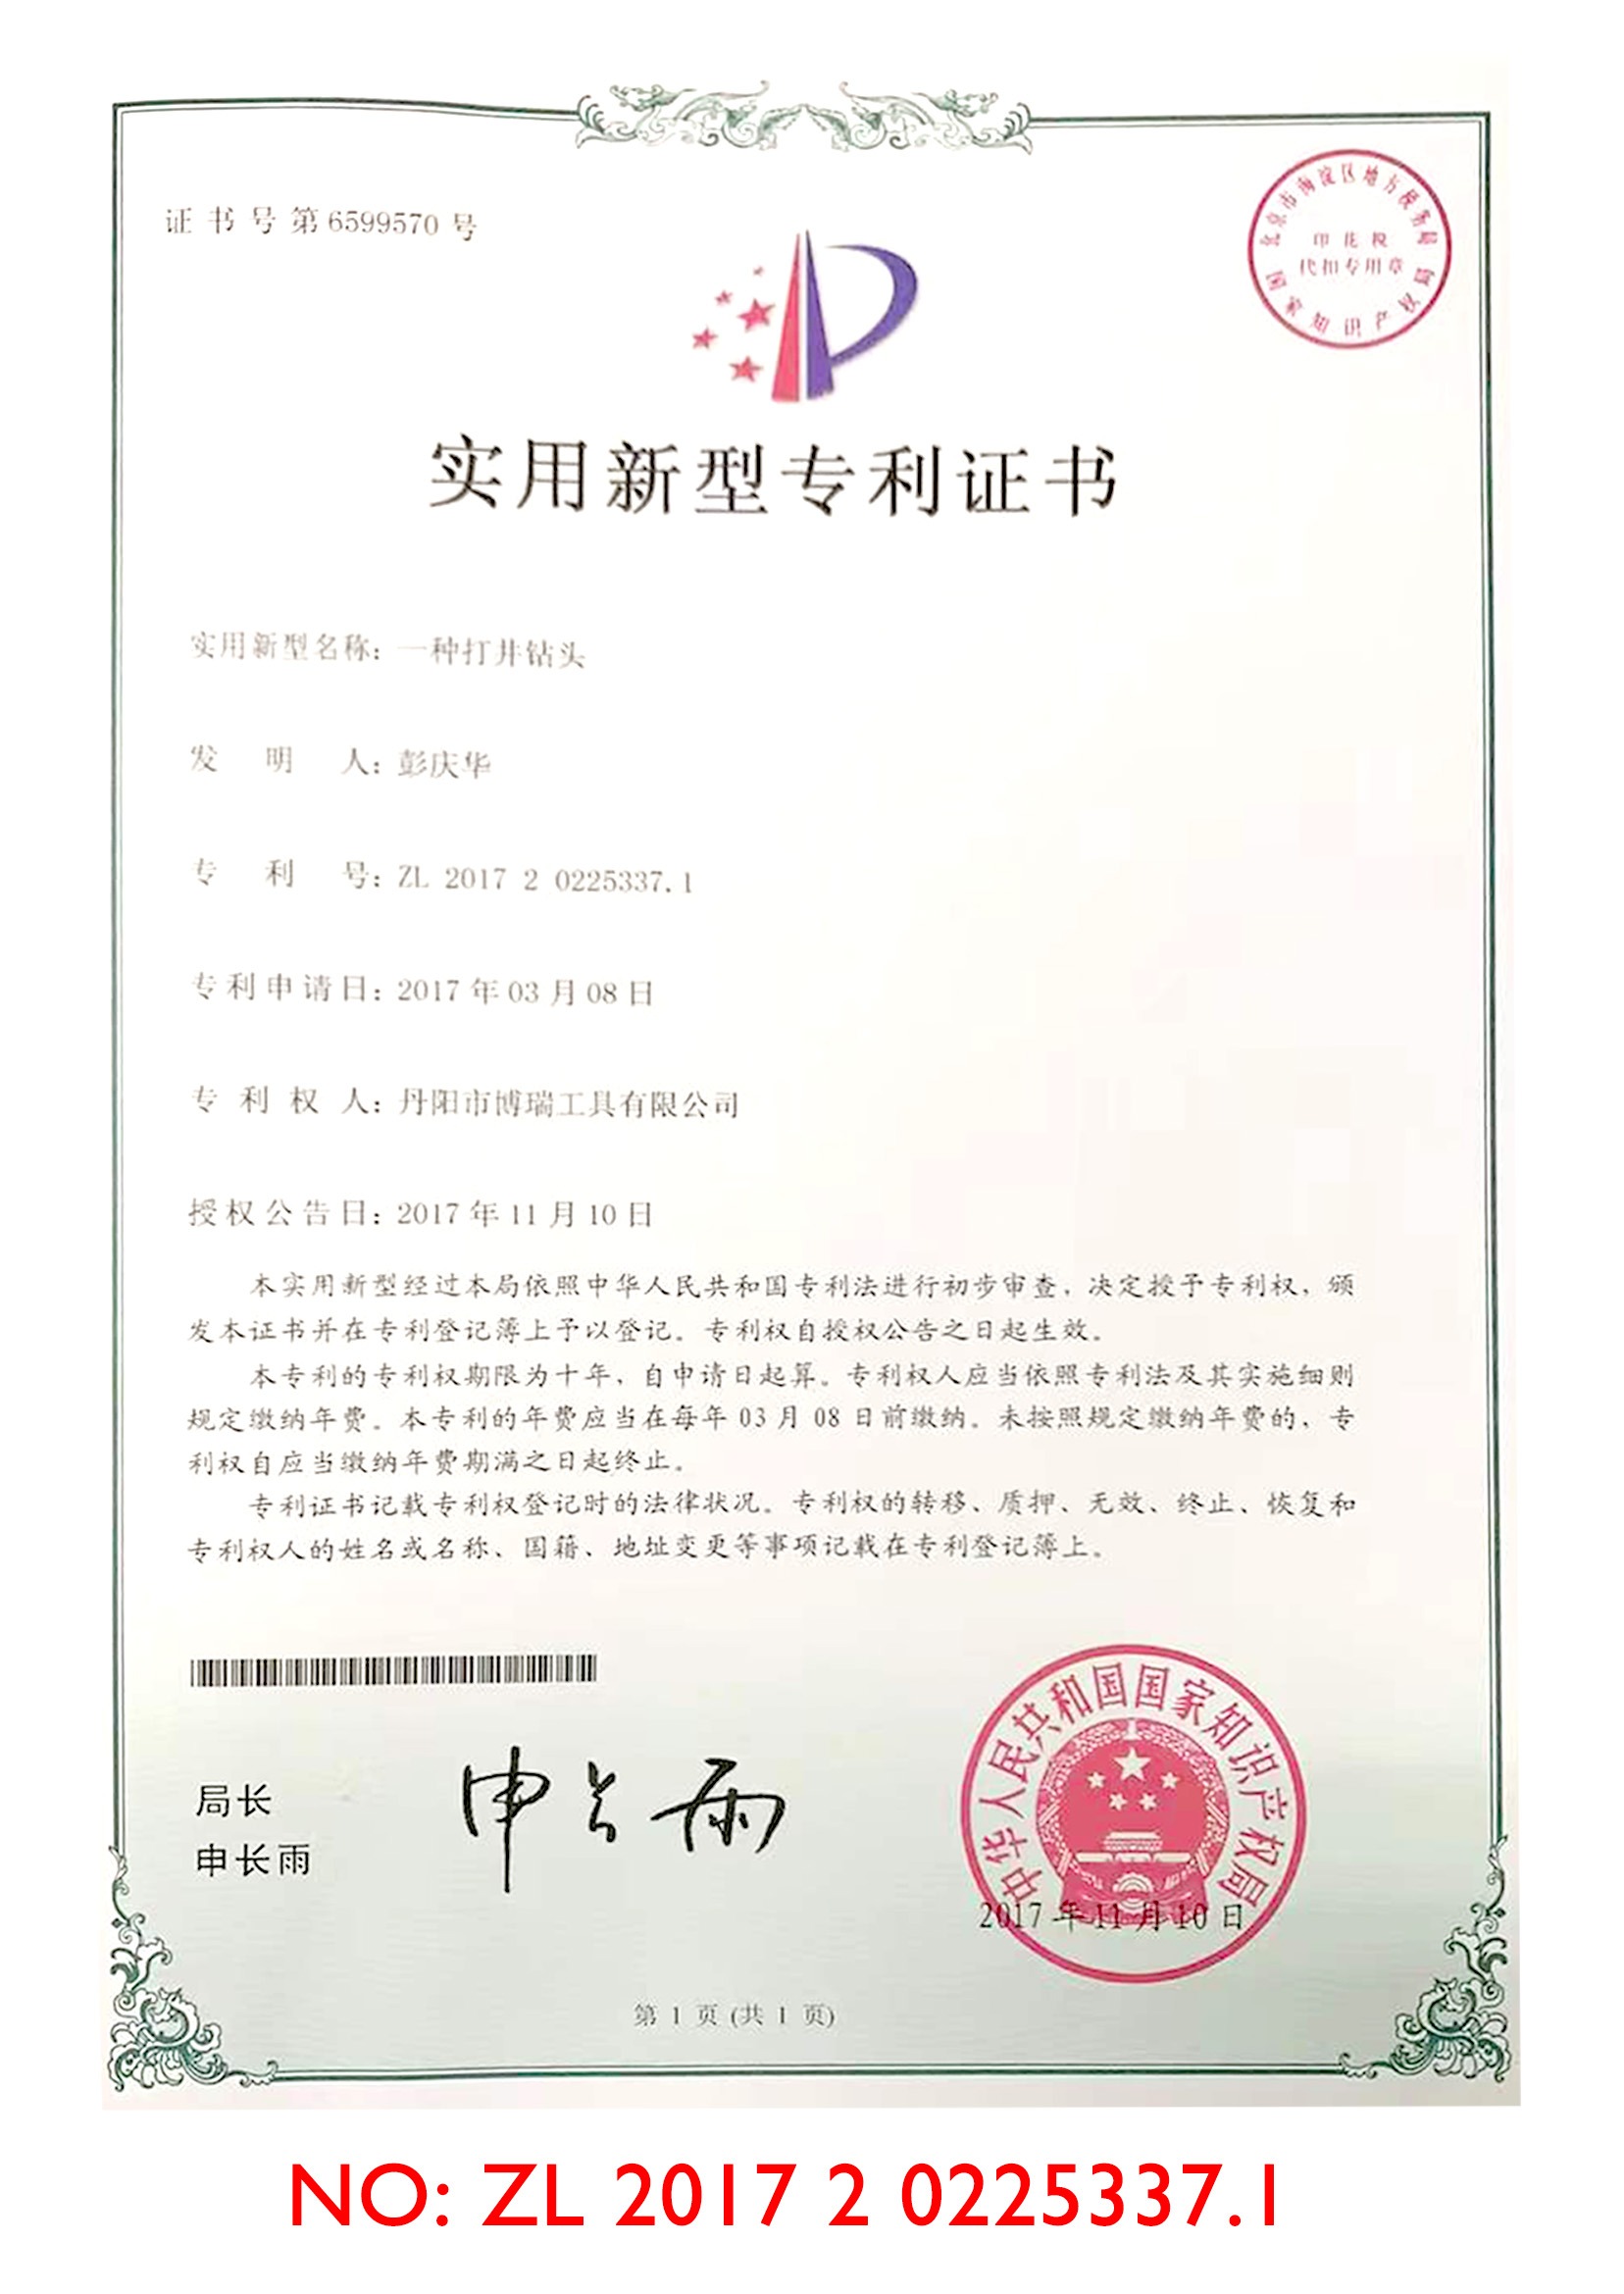
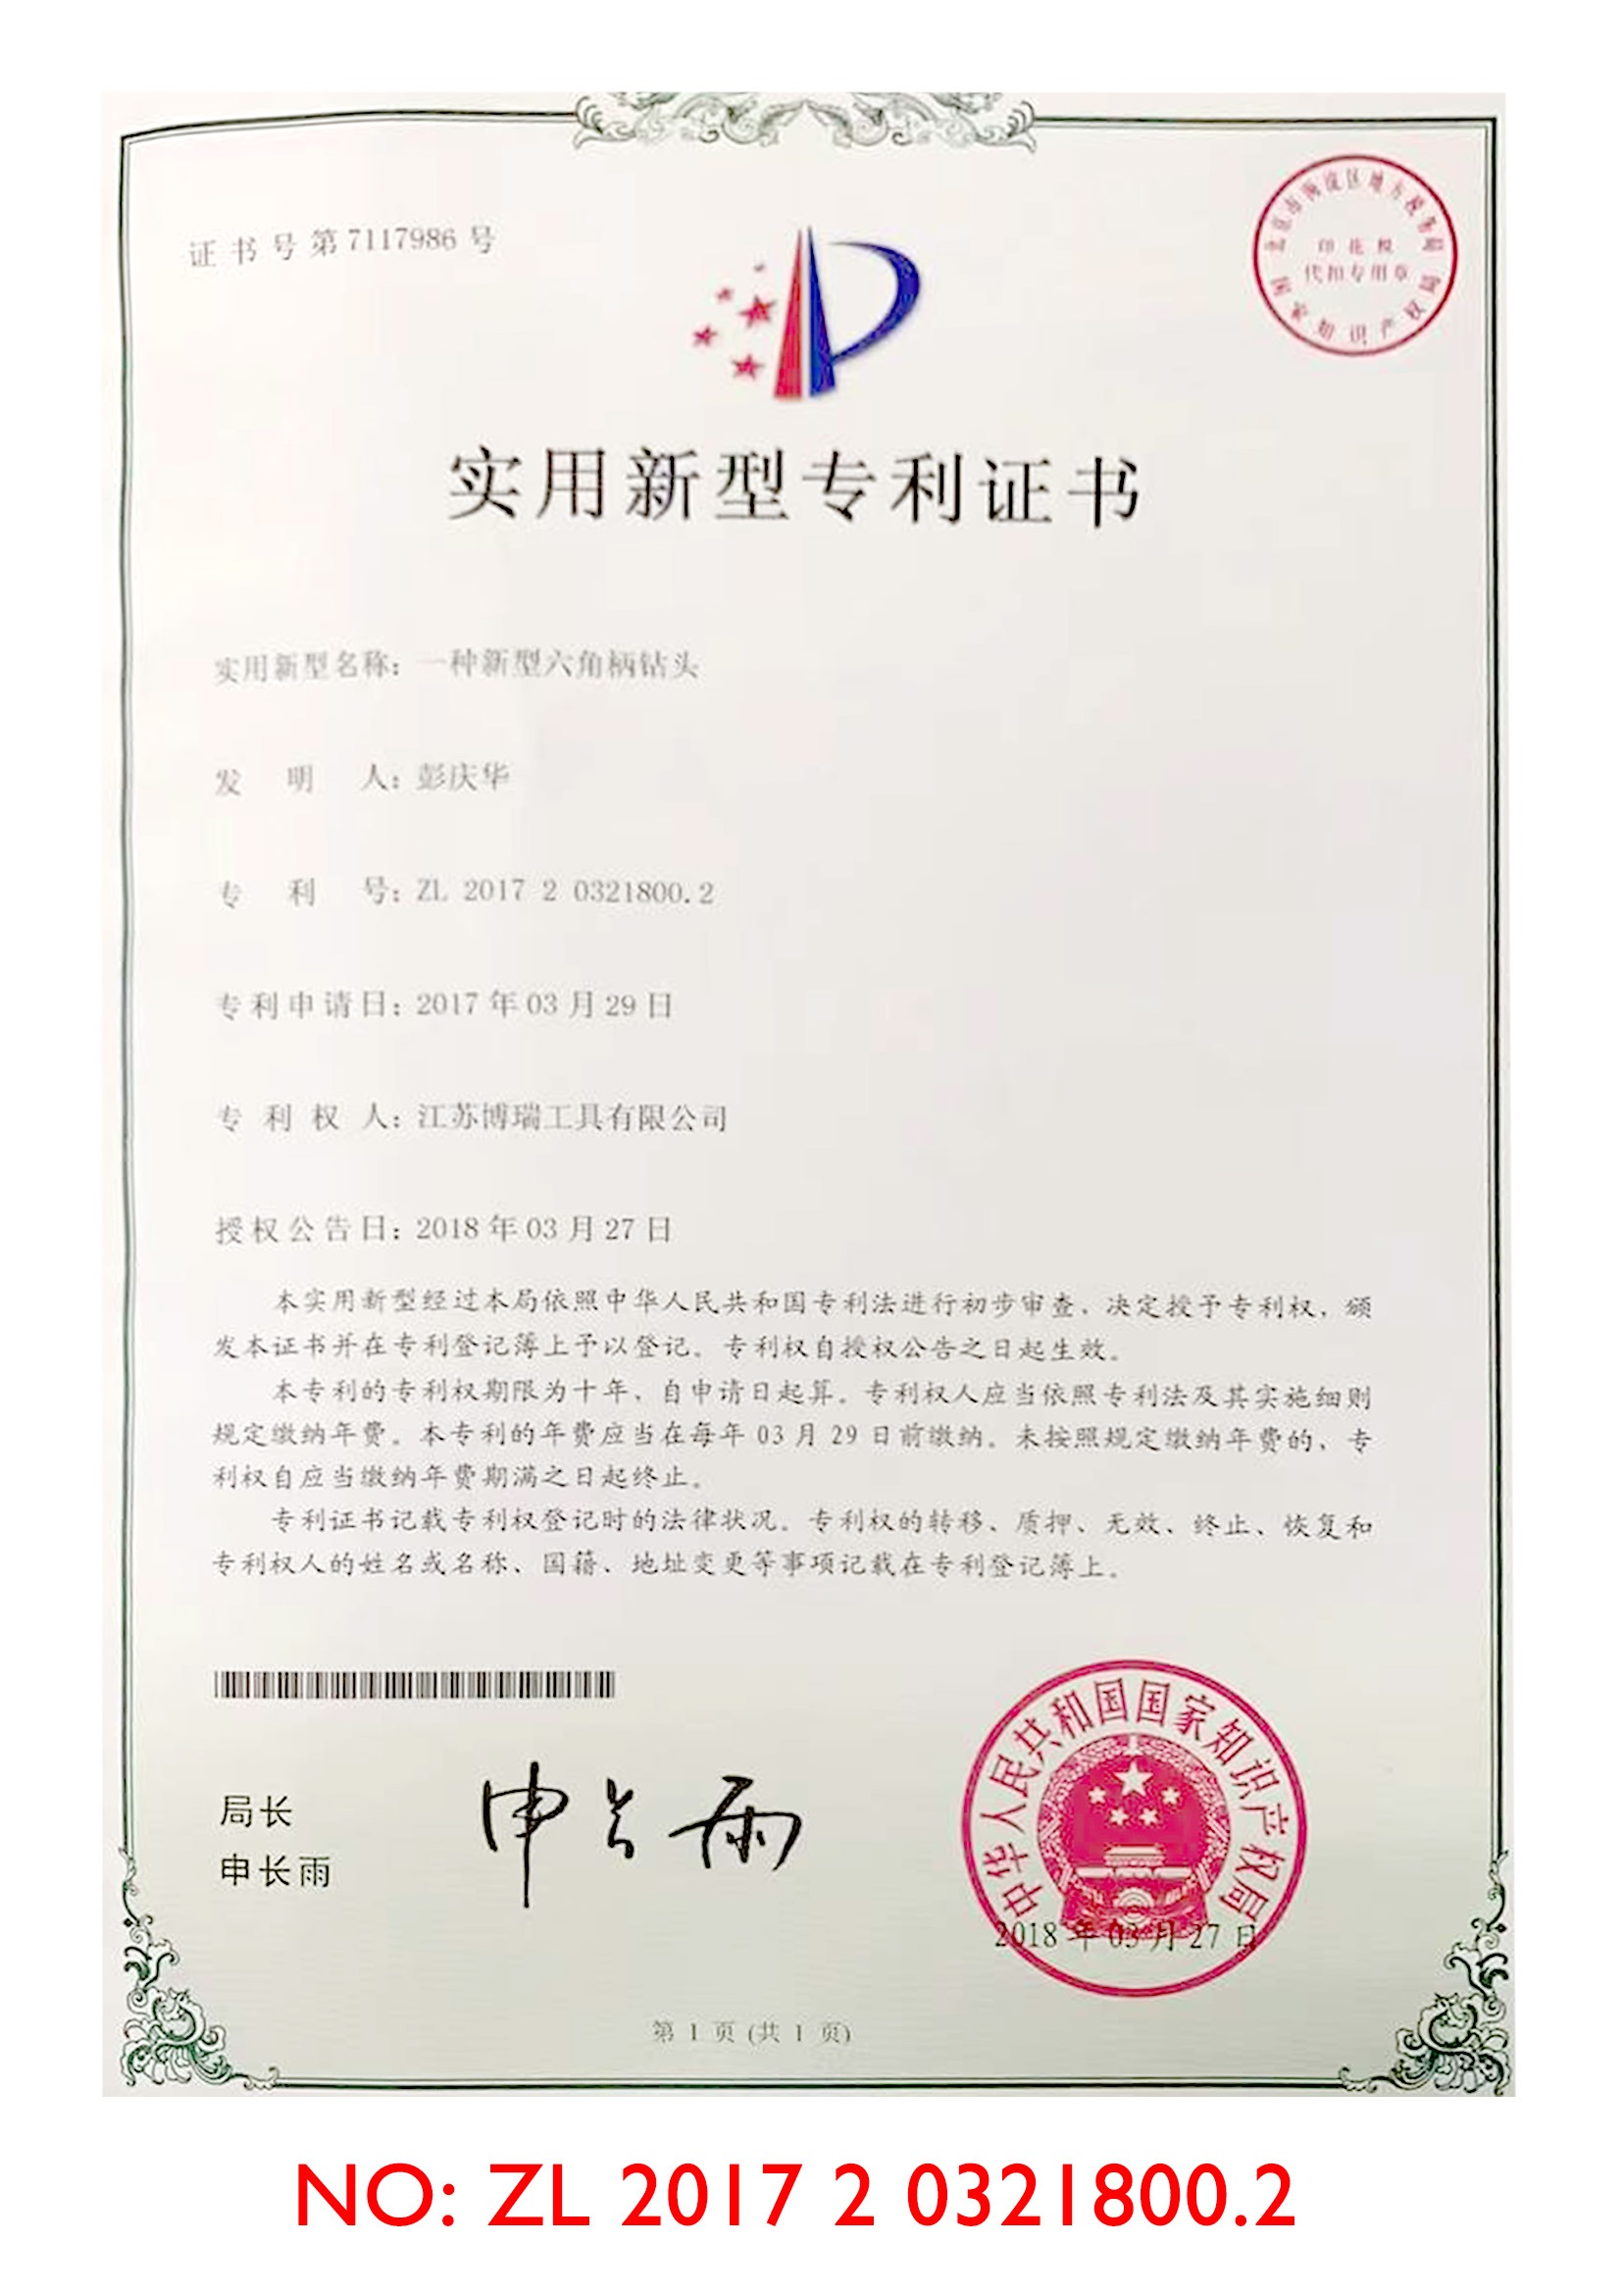
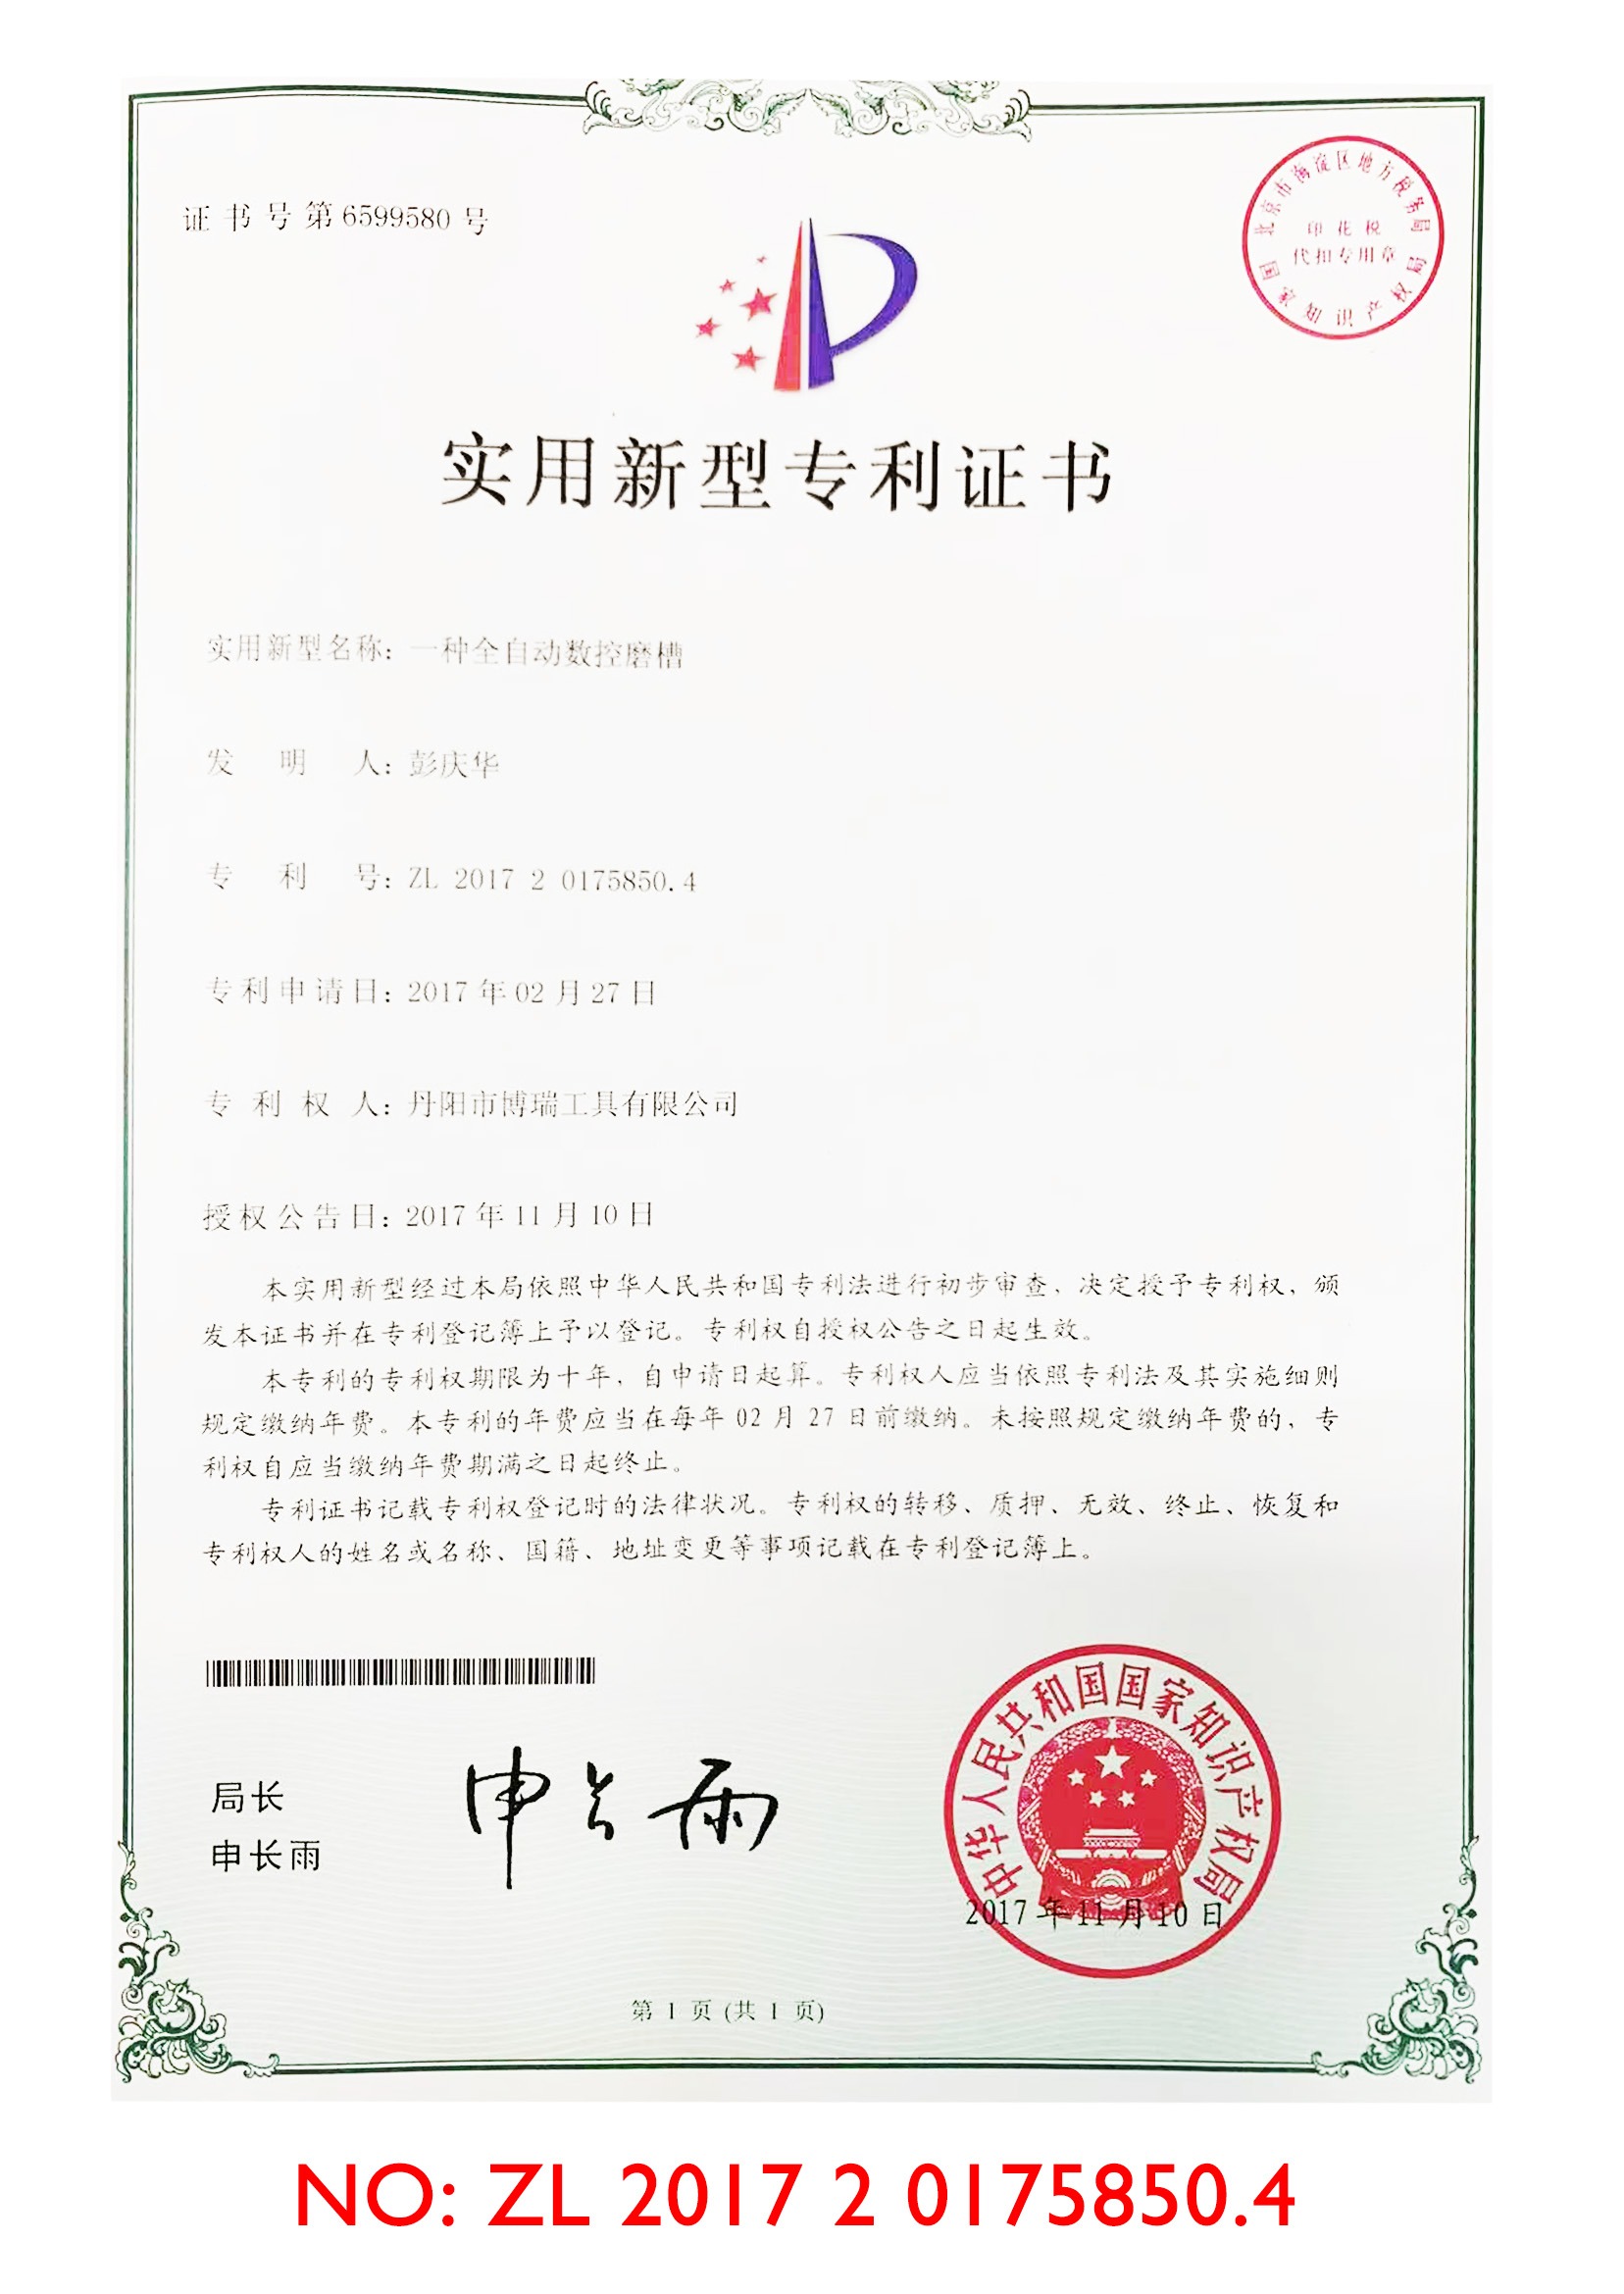
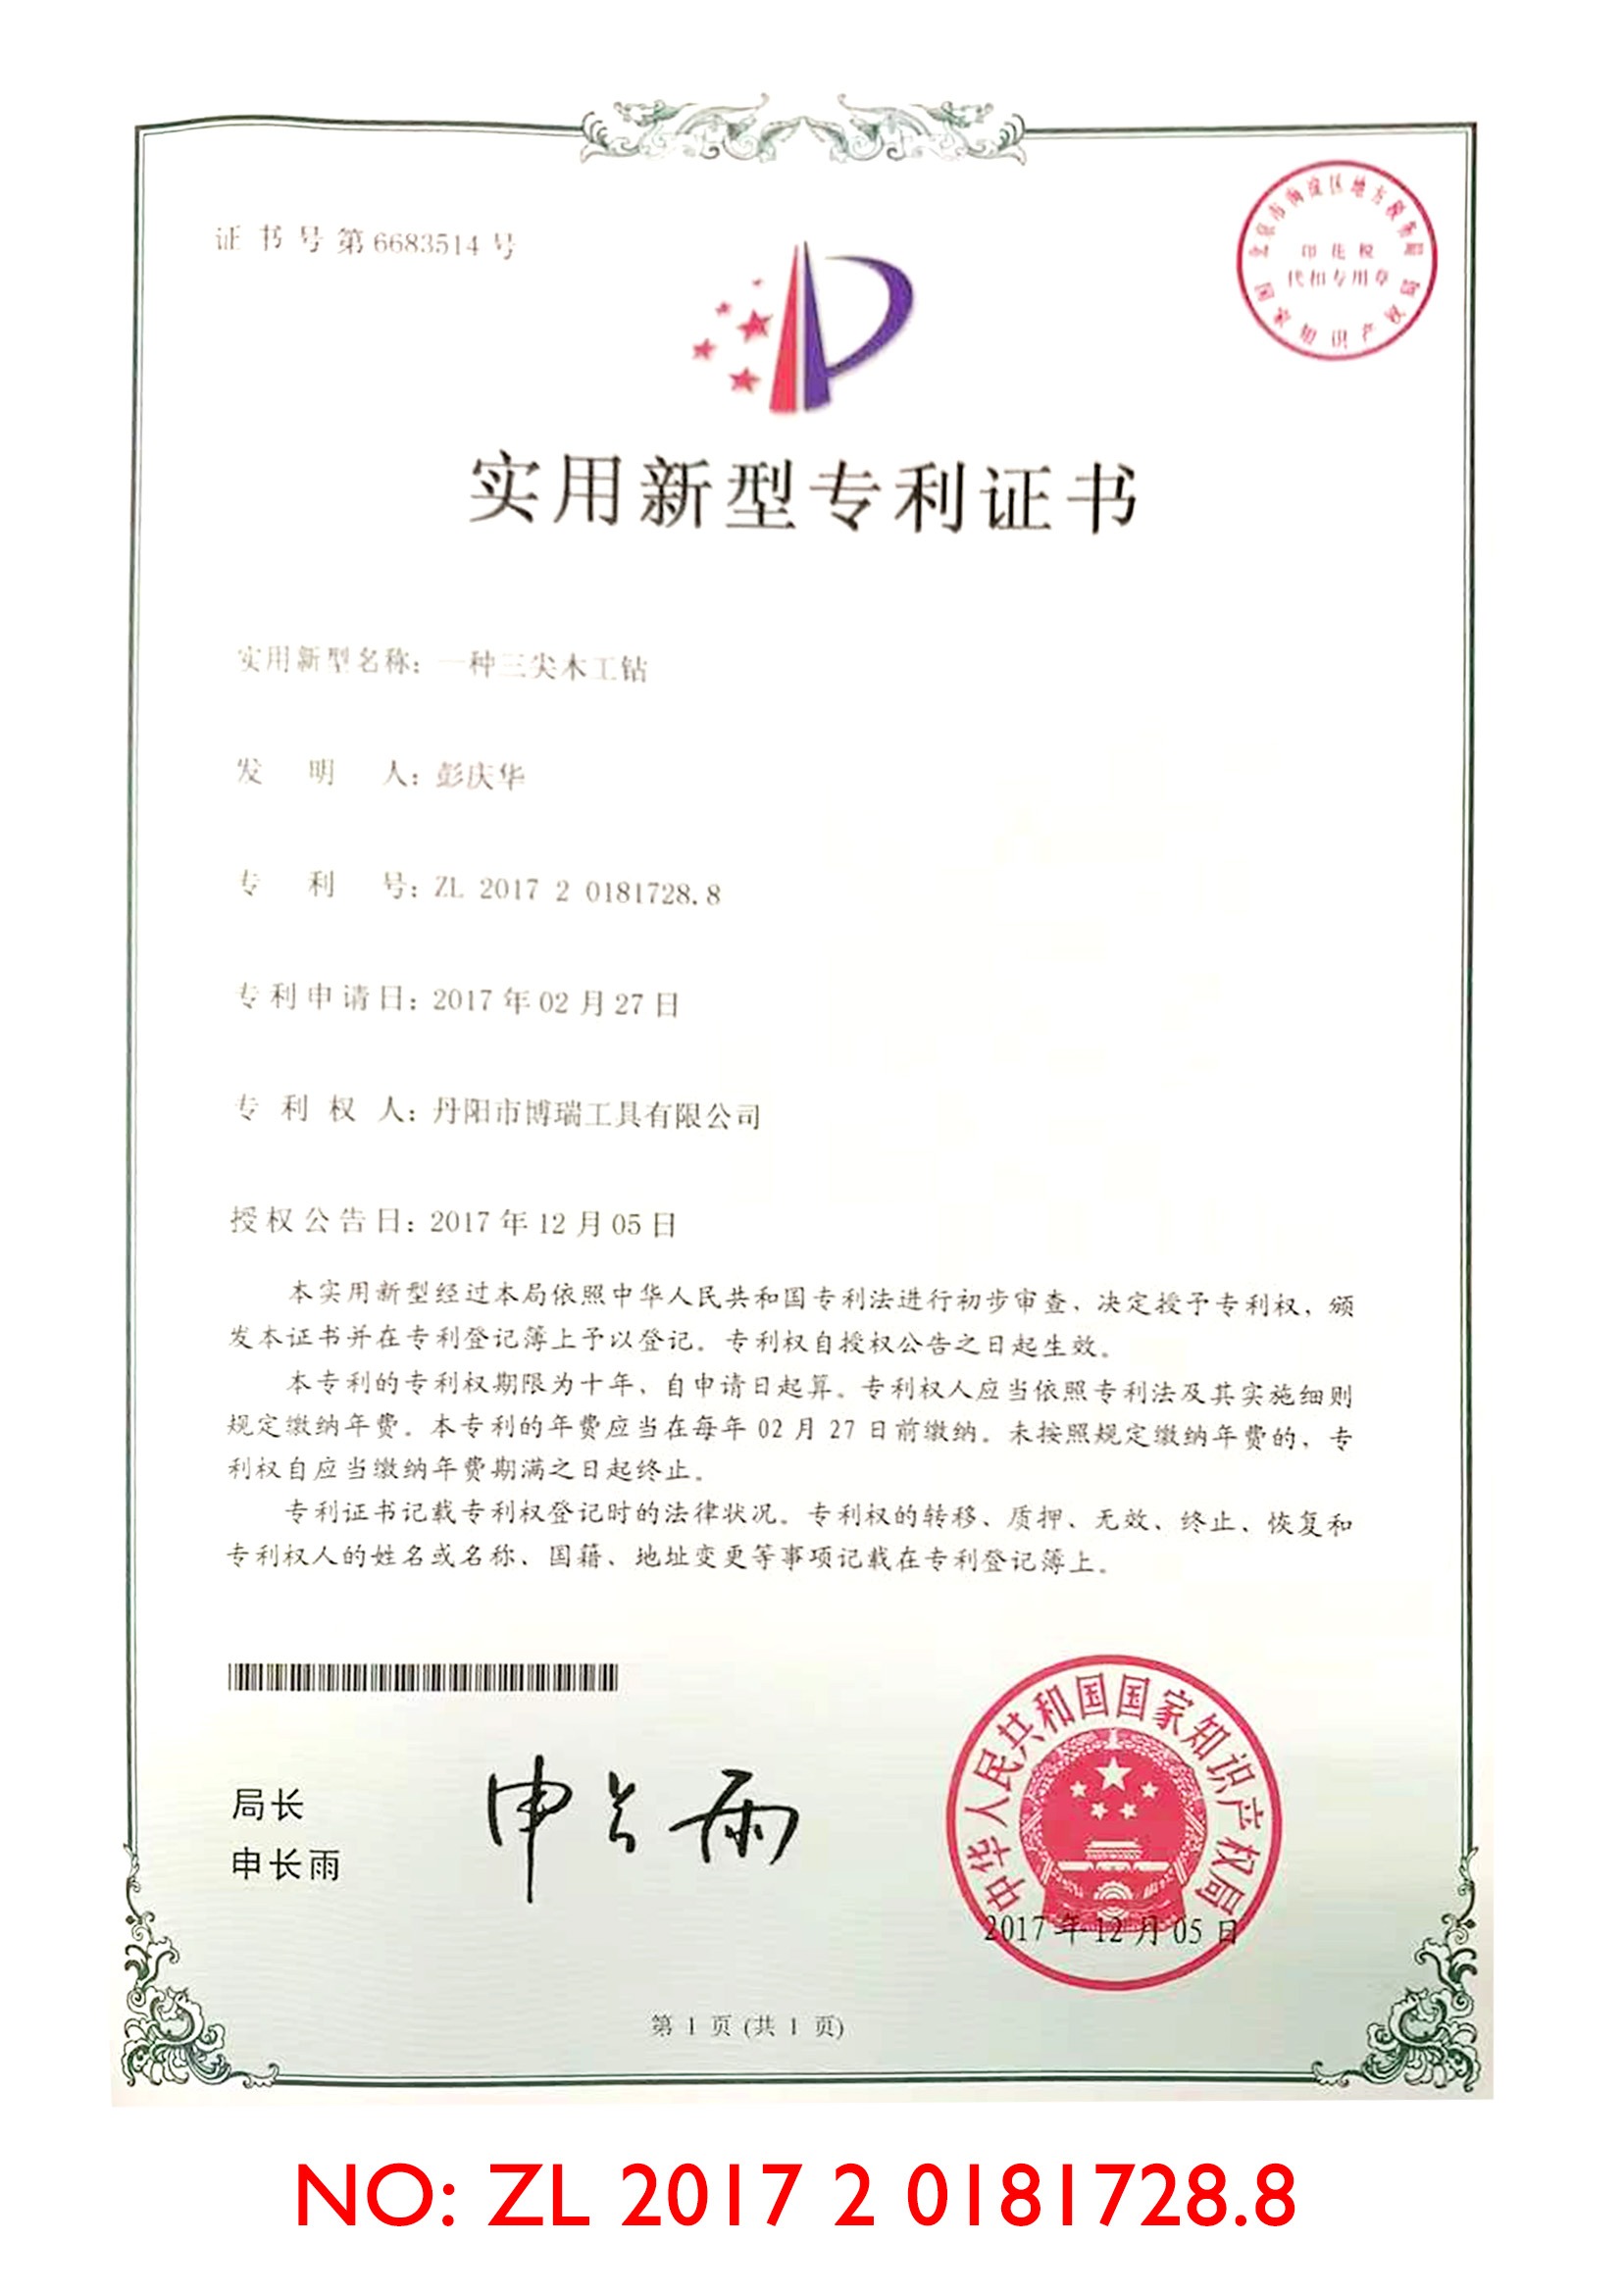
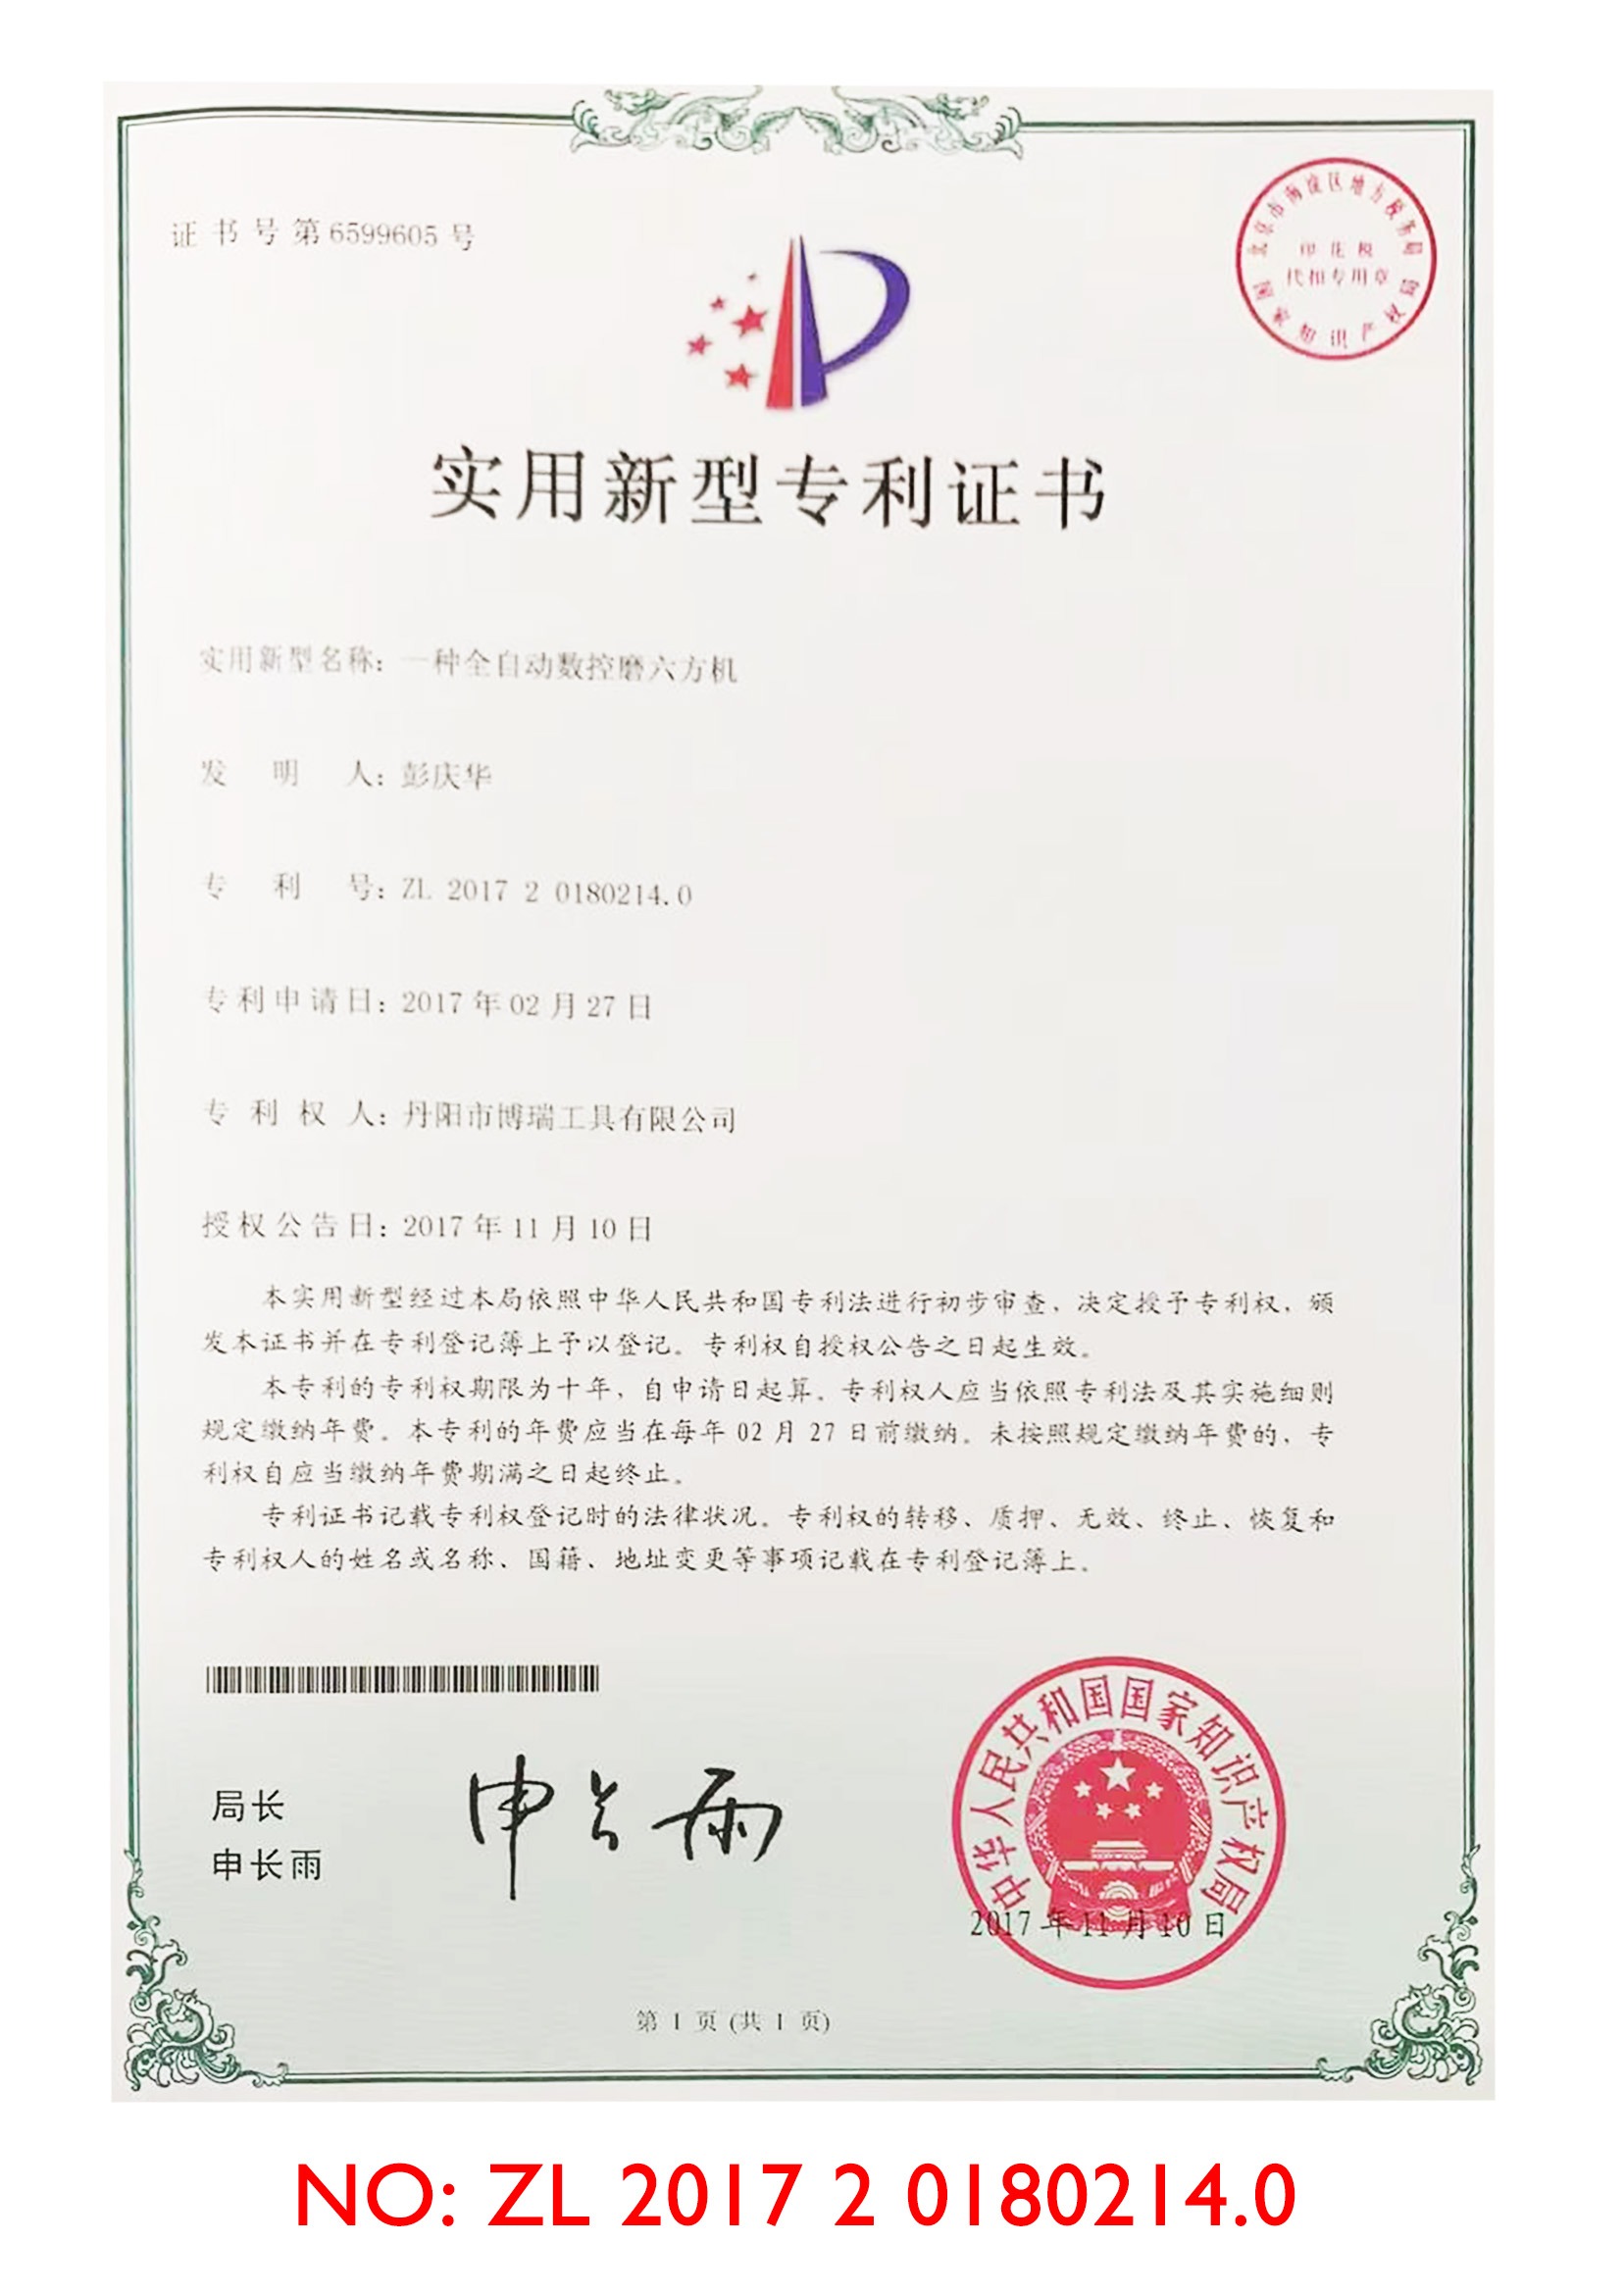
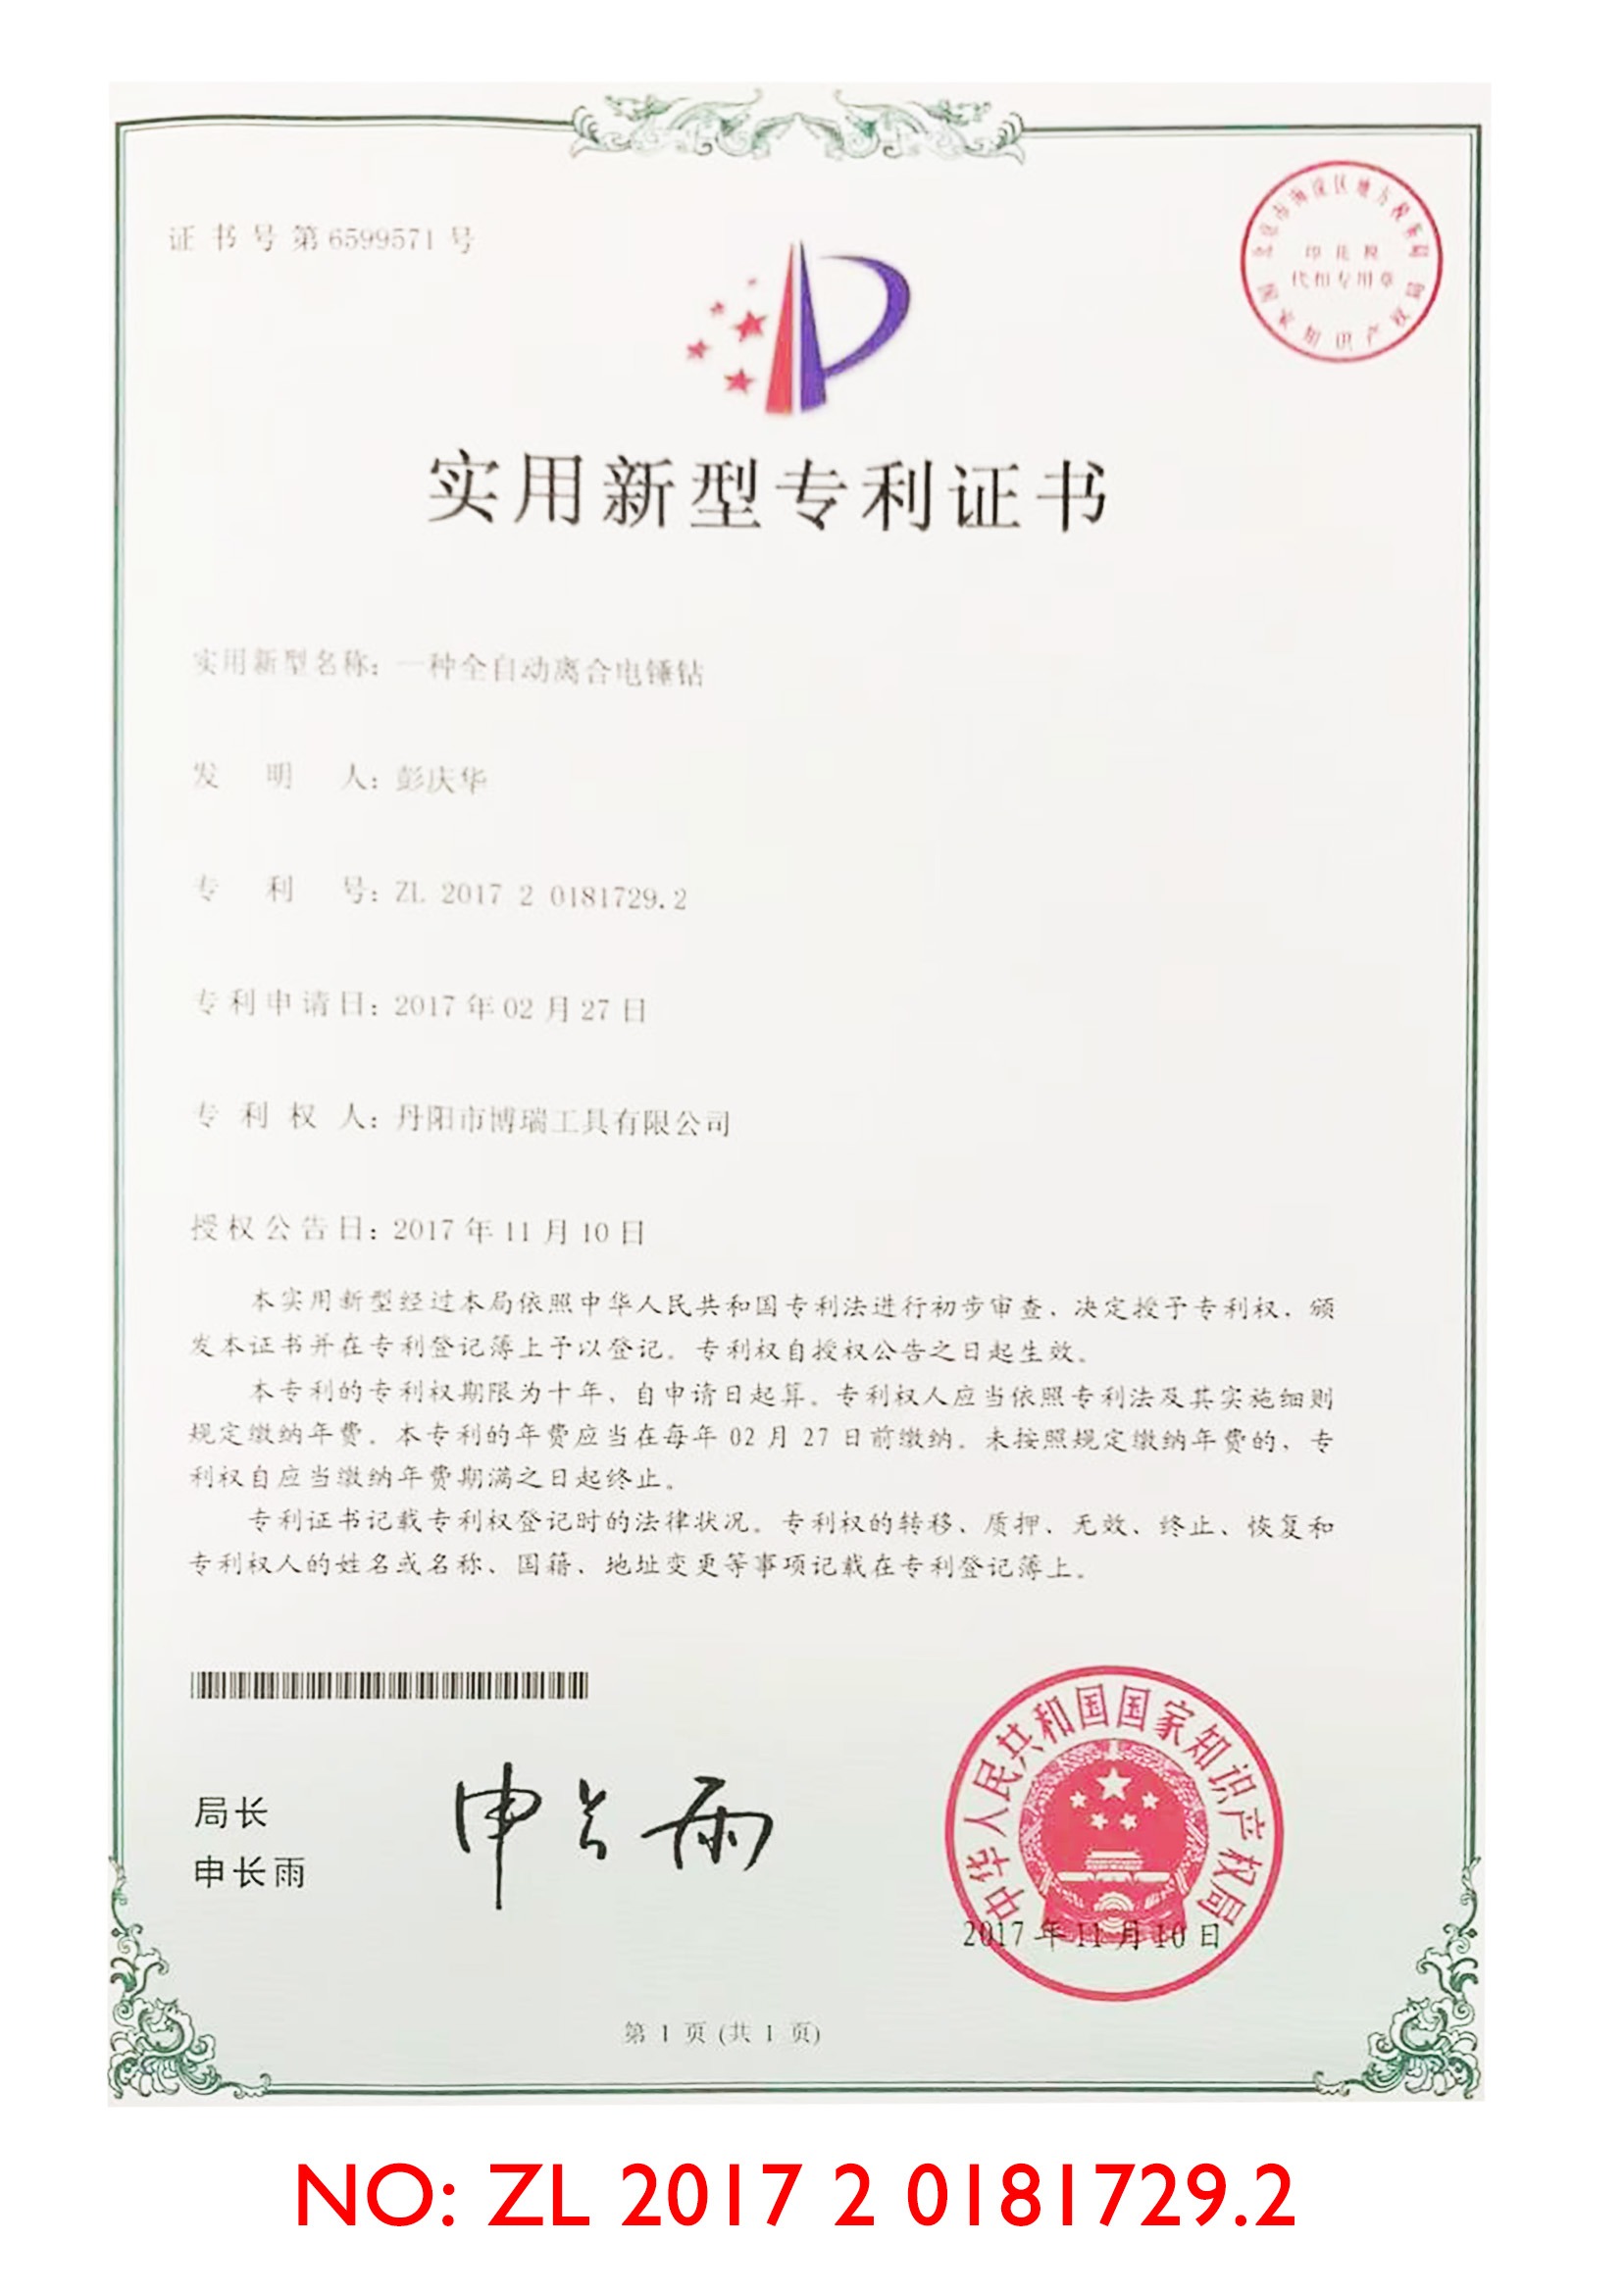
Global buyers from Germany, the USA, Switzerland, and Scandinavia visit our Danyang facilities annually to audit production capacity, test hole cutters, and sign private-label supply agreements.
Answers to the top technical and commercial inquiries asked by procurement managers, engineers, and supply chain analysts sourcing TCT Carbide Hole Saws.
TCT (Tungsten Carbide Tipped) hole saws deliver up to 10x longer service life compared to standard M3 or M42 bi-metal hole saws when drilling abrasive or hard metals such as AISI 304/316 stainless steel, structural carbon plate, and cast iron. High-speed steel teeth quickly overheat and lose their hardness above 600°C, causing tooth stripping. In contrast, tungsten carbide micro-grain teeth maintain HRA 89–91 hardness at temperatures exceeding 900°C. Offering TCT hole cutters allows distributors to tap into higher-margin industrial contractor and electrical trade segments where cutting speed and tool longevity are paramount.
Our TCT hole saws feature an engineered triple-edge stepped geometry consisting of alternating outer, center, and inner cutting faces. This design distributes cutting forces evenly, balances radial side-forces, divides chip width into thirds, drastically suppresses vibration, and prevents catastrophic carbide tooth chipping during aggressive handheld drilling.
Yes. We offer complete OEM/ODM customization. Standard shank options include 3-flats chuck shanks (10 mm and 13 mm), 1/4" quick-change hex shanks for cordless impact drivers, and Weldon 3/4" shanks for magnetic drills. We also provide full private-label services including laser brand etching, custom color electroplating, TiAlN PVD coatings, and bespoke blow-mold, aluminum, or metal storage sets with your branding. Minimum order quantities start at just 100 pieces for individual sizes and 500 sets for custom-packaged kits.
For Grade 304 and 316 stainless steel, cutting speeds should be kept moderate between 15 to 25 m/min. For example, a 25 mm diameter hole saw should run at approximately 450–600 RPM with constant, firm downward pressure and cutting oil. Running at excessive RPM generates rapid frictional heat, which work-hardens the stainless steel and risks thermal shock to the carbide teeth. Steady pressure ensures positive chip formation and clean slugs.
We utilize automated high-frequency induction brazing with a specialized silver-copper-silver (Ag-Cu-Ag) three-layer sandwich solder foil. The central copper core acts as a mechanical shock absorber that cushions differential thermal expansion between the tungsten carbide tip and the alloy steel saw body. Every batch undergoes non-destructive ultrasonic inspection and destructive torque shear testing exceeding 280 MPa to guarantee zero tooth loss under heavy industrial use.
Standard OEM samples for dimension and cutting-performance evaluation are dispatched within 3 to 5 business days. Mass production runs for standard catalog sizes typically ship within 25 to 35 days upon drawing sign-off and deposit receipt. For urgent distributor container shipments, our finished goods warehouse maintains stock blanks for fast turnarounds.
Send drawings, target specifications, or request free evaluation samples — we respond within 1 business day.
 IrisExport Sales Manager
 AaronExport Sales Manager
 CynthiaExport Sales Manager
 WillieExport Sales Manager
 AbbyExport Sales Manager
 VictorExport Sales Manager