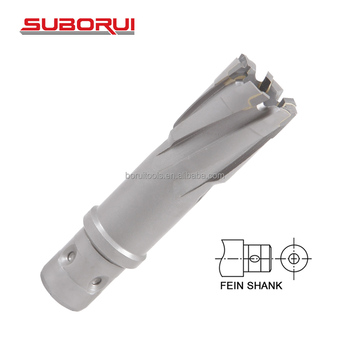
Standard 19.05mm (3/4") Weldon Shank TCT Cutter
Dia 12–100 mm | Depth: 35mm, 50mm, 75mm
Tri-tooth cutting geometry for mild & stainless plate
US$9.50–30.00 / piece
MOQ: 10 pieces
Engineered for extreme structural steelwork, stainless alloys, and railway profile drilling, Tungsten Carbide Tipped (TCT) annular cutters deliver unmatched speed, heat dissipation, and hole concentricity. Jiangsu WRD Tools Co., Ltd. provides direct manufacturing precision from China's premier cutting-tool belt in Danyang.
Explore factory-direct core drill configurations optimized for magnetic base drills, radial drill presses, and CNC machine centers across heavy engineering applications.
Dia 12–100 mm | Depth: 35mm, 50mm, 75mm
Tri-tooth cutting geometry for mild & stainless plate
US$9.50–30.00 / piece
MOQ: 10 pieces
Specialized for 900A/1100 rail profiles & manganese alloy
Impact-absorbing braze seam, negative rake carbide
US$16.00–45.00 / piece
MOQ: 10 pieces
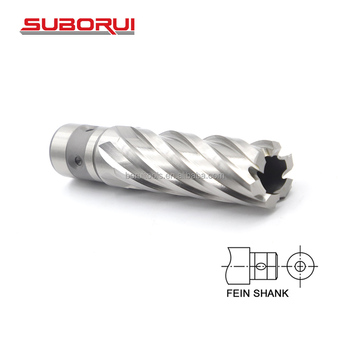
Dual-fit shank for Nitto Kohki & standard Weldon arbors
Tool-free quick changeover for jobsite mag-drills
US$11.50–34.00 / piece
MOQ: 10 pieces
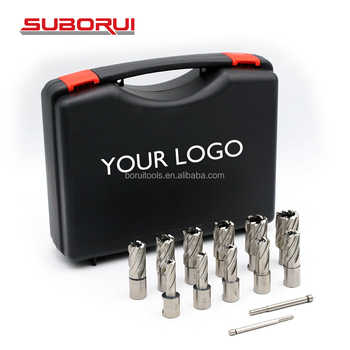
Popular metric/imperial diameters + centering ejector pins
Heavy-duty aluminum flight case, customized laser foam
US$75.00–140.00 / set
MOQ: 5 sets
A deep-dive technical briefing for tool distributors, procurement heads, and EPC project managers navigating global infrastructure expansion.
Global structural steel fabrication is undergoing an accelerated shift away from traditional mild structural steels toward Thermo-Mechanically Rolled Steels (such as S460, S690QL, and Hardox wear-plates). Traditional High-Speed Steel (HSS) annular cutters encounter rapid edge thermal breakdown when encountering tensile strengths above 850 MPa. Consequently, Tier-1 structural fabricators are re-allocating up to 70% of their tool budgets exclusively to TCT annular cutters to prevent catastrophic downtime and repeated tool swap-outs.
While bare carbide provides exceptional baseline hardness, modern dry and high-speed CNC magnetic drilling demands extreme heat resistance. The adoption of advanced PVD nanocomposite coatings—specifically Aluminium Titanium Nitride (AlTiN) and Titanium Silicon Nitride (TiSiN)—has surged. These nano-coatings generate an amorphous aluminium oxide passivating layer during high-friction cutting, raising maximum oxidation barriers up to 1,100°C while drastically lowering coefficient of friction in gummy materials.
Western distributors and regional hardware giants are streamlining vendor portfolios, consolidating twist drill, hole saw, and annular cutter procurement under certified direct manufacturing partners. Sourcing models demand agile OEM capabilities: customized laser-etched imperial and metric dimensions, branded CNC fluting geometries, dual-hardness carbide braze testing, and private-label blow-molded carrying packaging delivered with predictable lead times.
The core technological advantage of a TCT annular cutter lies in its segmented cutting crown. Unlike a standard drill bit that converts the entire core volume into chips, an annular cutter cuts exclusively along the hole perimeter, ejecting a solid metal slug. However, carbide's inherent brittleness requires unique tooth architecture:
At Jiangsu WRD Tools Co., Ltd., each tooth on our TCT cutter is precision ground with a multi-angle profile consisting of three distinctive cutters: Outer Tooth (defining exact hole diameter), Intermediate Tooth (clearing the central kerf), and Inner Tooth (governing core clearance and preventing core clamping). This three-ply cut spreads the cutting force evenly, dampens harmonic vibration, eliminates chip congestion, and prevents sudden tip shatter.
Comprehensive engineering and commercial answers to frequent questions queried by global tool importers, buyers, and technical engineers.
TCT (Tungsten Carbide Tipped) cutters utilize micro-grain cemented carbide tooth inserts induction-brazed onto a high-alloy spring steel body. While standard High-Speed Steel (M2/M35) begins losing hardness around 500°C–600°C, tungsten carbide maintains exceptional hot hardness past 900°C. In heavy structural I-beams, stainless steels (304/316), abrasive cast iron, and high-tensile railway tracks, TCT cuts at more than twice the peripheral surface speed (SFM) of HSS with 3x to 5x greater overall tool lifespan, dramatically reducing machine downtime and labor per hole.
Carbide tips possess outstanding compressive strength and abrasive resistance but low tensile/impact ductility. Premature breakage is usually triggered by three common culprits: 1) Weak magnetic holding base or unstable workpieces allowing the drill press to rock during cutting; 2) Inconsistent manual feed pressure causing tooth snatching; or 3) Ejection failure of the center slug at cycle completion. To prevent damage, ensure a minimum 12mm flat steel surface for magnetic chuck adherence, maintain continuous internal pressurized coolant through the center pilot pin, and ease off feed pressure slightly upon penetration breakthrough.
Jiangsu WRD Tools Co., Ltd. manufactures four core arbor connections: 1) Standard 19.05 mm (3/4") Weldon Shank with two grub-screw flats—compatible with majority magnetic drills globally; 2) 31.75 mm (1-1/4") Weldon Shank for heavy-bore cutters above 65 mm; 3) Universal One-Touch Shank featuring 3 ball detents and 1 drive flat—allowing fast tool-free chucking in Nitto Kohki machines while maintaining full compatibility with regular Weldon arbors; and 4) 4-spoke Quick-In shanks customized for Fein magnetic drills.
Yes. Although re-sharpening TCT annular cutters requires precise CNC tool and cutter grinders equipped with resinoid diamond wheels and designated indexing cams to preserve the alternating triple-cut rake and relief angles, cutters can routinely be re-sharpened 3 to 5 times. As long as the carbide insert is not fractured across the braze line or worn down to less than 0.8 mm thickness, re-sharpening delivers substantial cost savings over complete tool replacement.
For standard stocked sizes, our minimum order quantity starts at just 10 pieces or 5-piece boxed sets. For custom OEM branding, we accommodate private laser engraving (logos, custom part numbering, and sizing), custom depth specifications (35 mm, 50 mm, 75 mm, 100 mm), advanced protective coatings (TiN, TiAlN), and branded high-impact plastic or aluminum cases with custom molded foam. Sample orders are dispatched within 5–7 days, with commercial container orders completed in 30–35 days.
Internal lubrication via the spring-loaded center pilot pin is essential. The pilot pin serves a dual mechanical function: it accurately aligns the cutter over the center punch mark before drilling, and during cutting, retracts inward to open the internal arbor coolant valve. Pressurized cutting oil flows directly across the internal flutes to the carbide cutting edges, cooling the braze joint and flushing chips away. Upon complete breakthrough, the pilot spring expands forcefully, violently ejecting the solid waste slug to prepare the drill immediately for the next cycle.
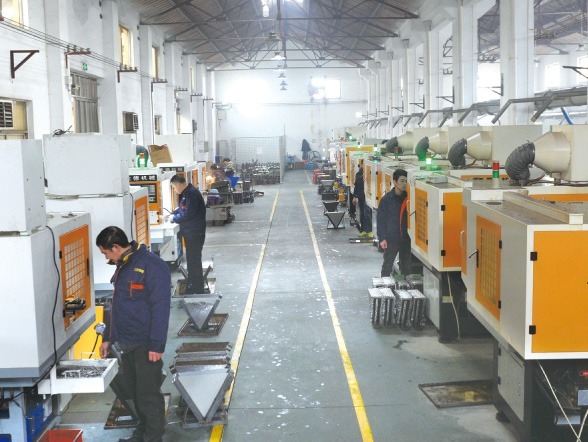
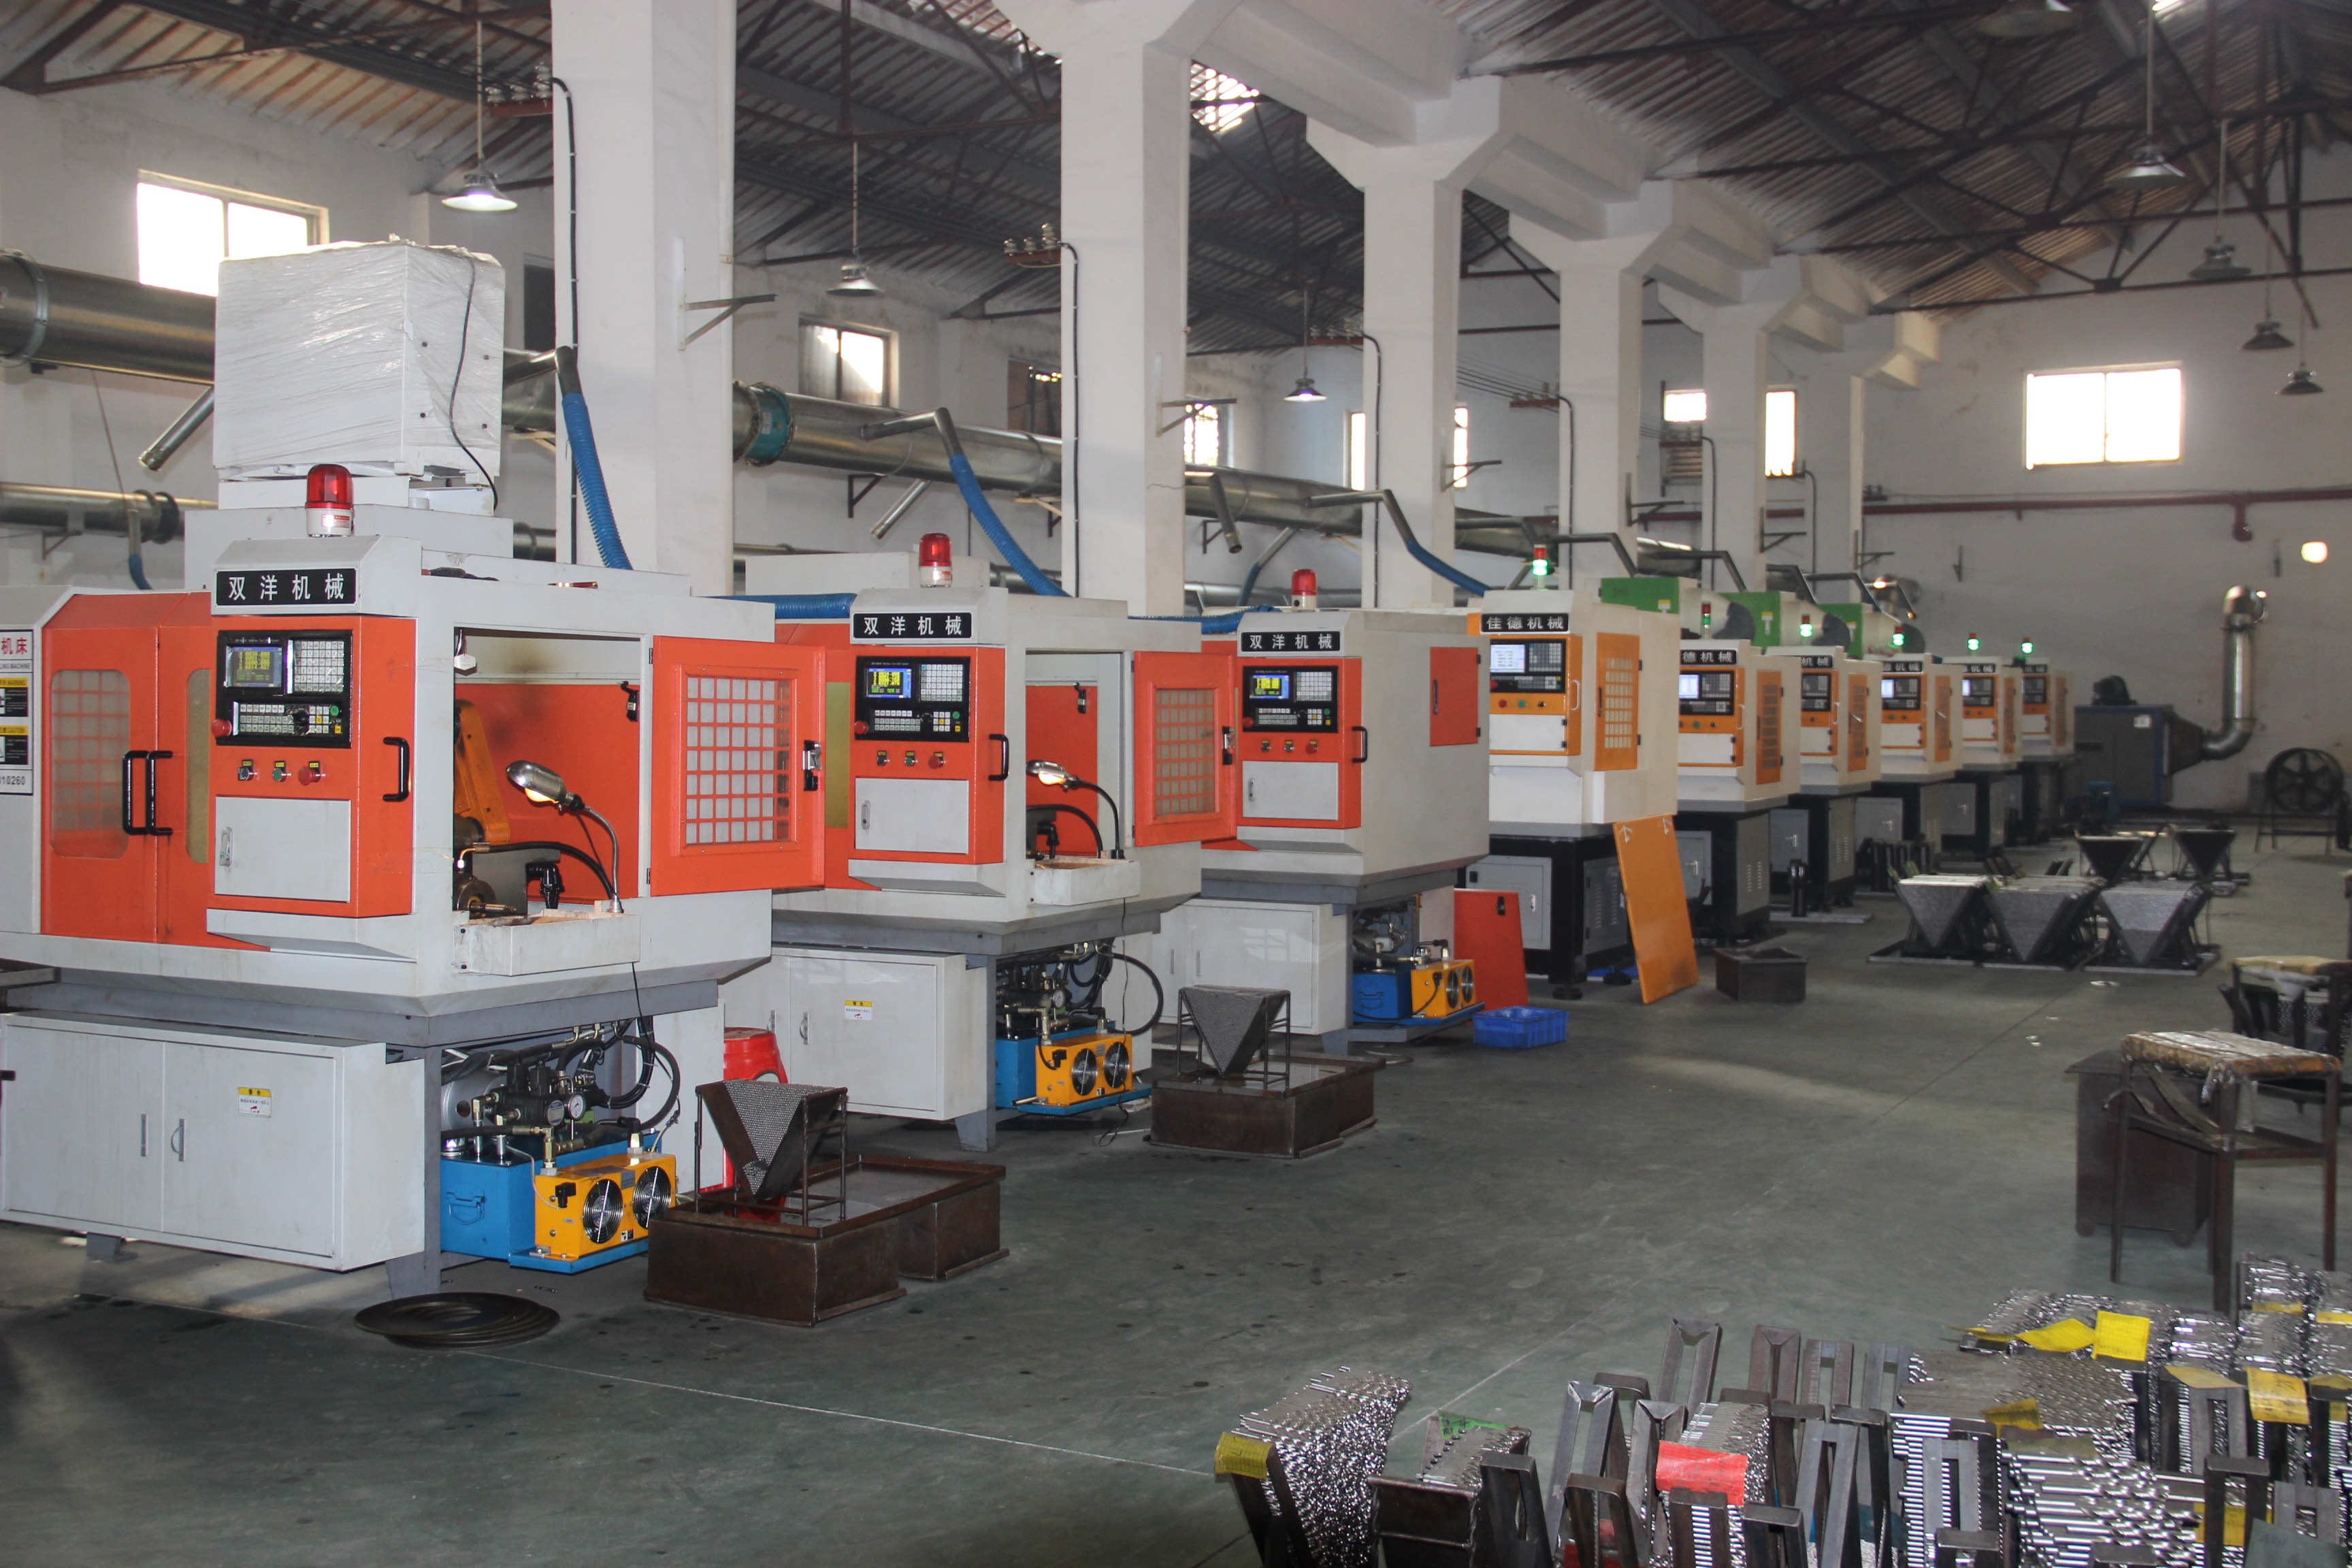
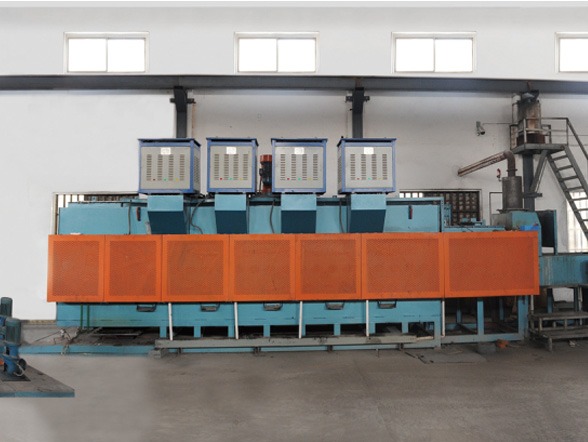
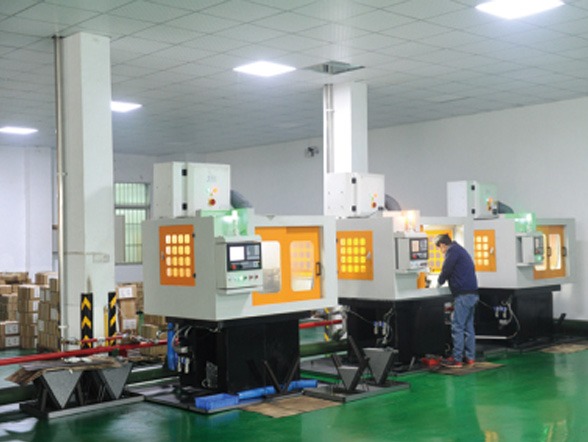
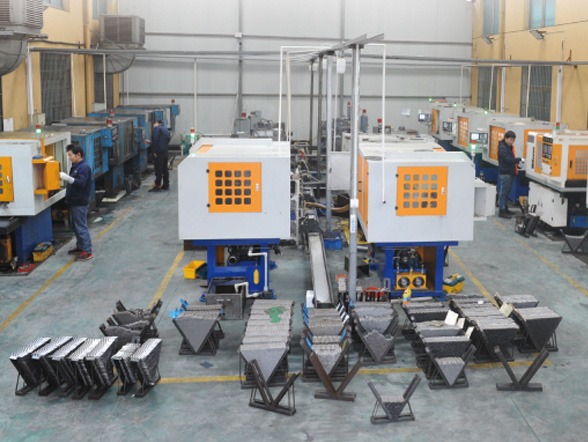
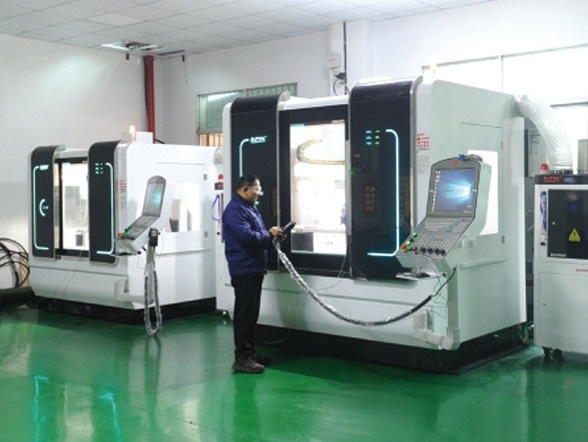
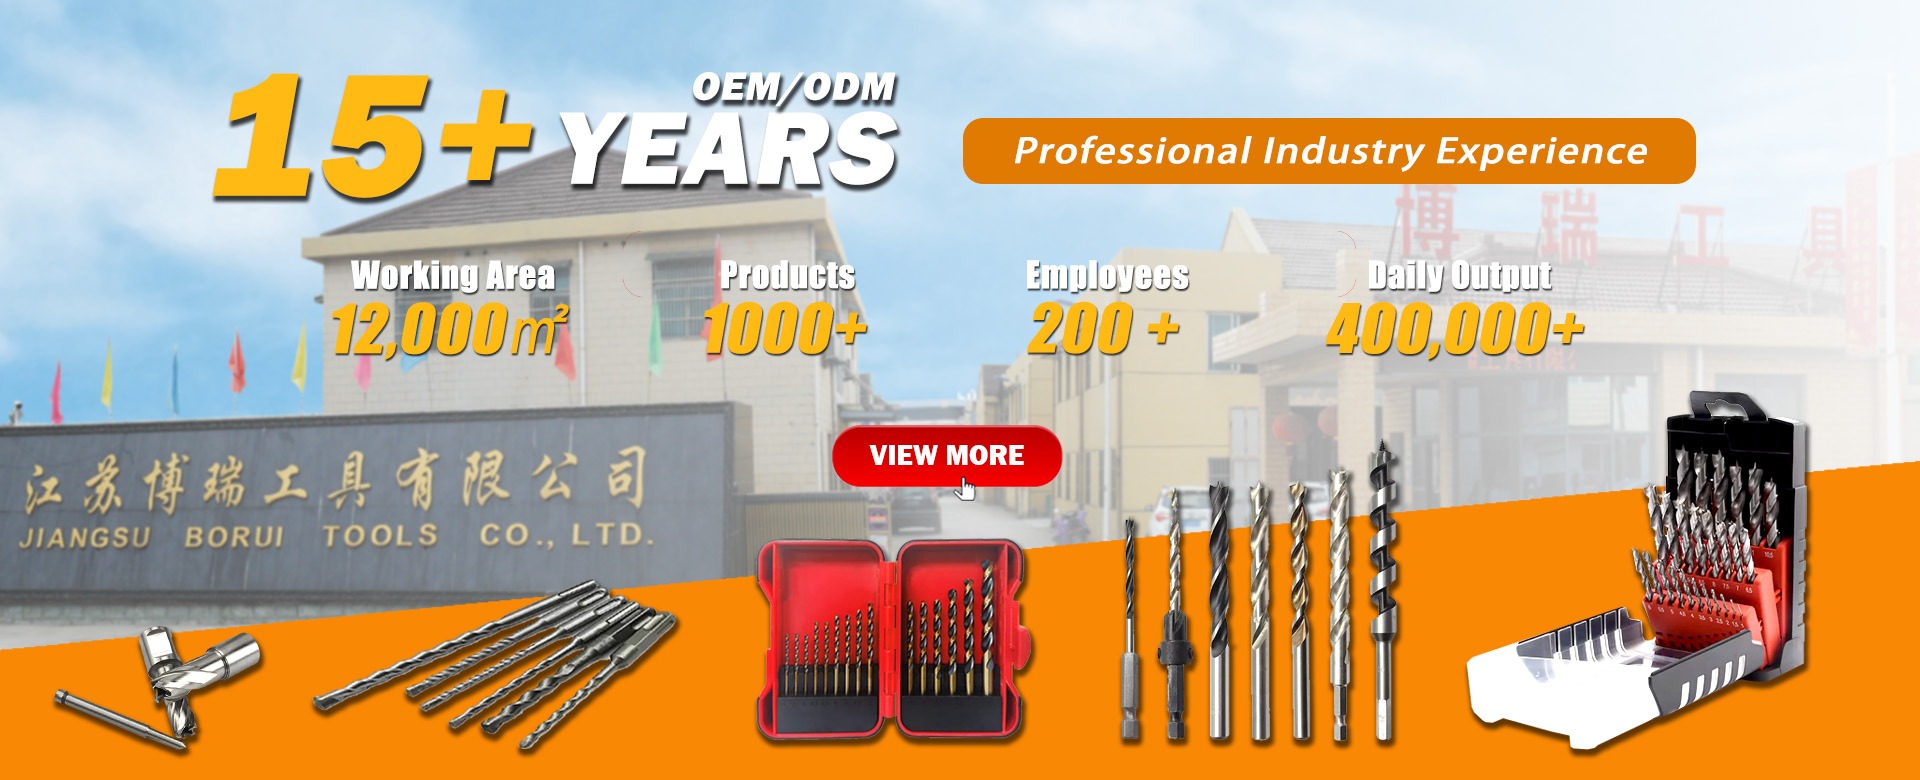
Jiangsu WRD Tools Co., Ltd. was established in March 2007 with a registered capital of RMB 10 million. Strategically located across a 12,000 m² state-of-the-art manufacturing campus in Danyang, Jiangsu Province, we operate dedicated specialized workshops for annular cutters, HSS twist drills, taps, hole saws, and wood bits powered by over 150 skilled machinists, metallurgists, and QA technicians.
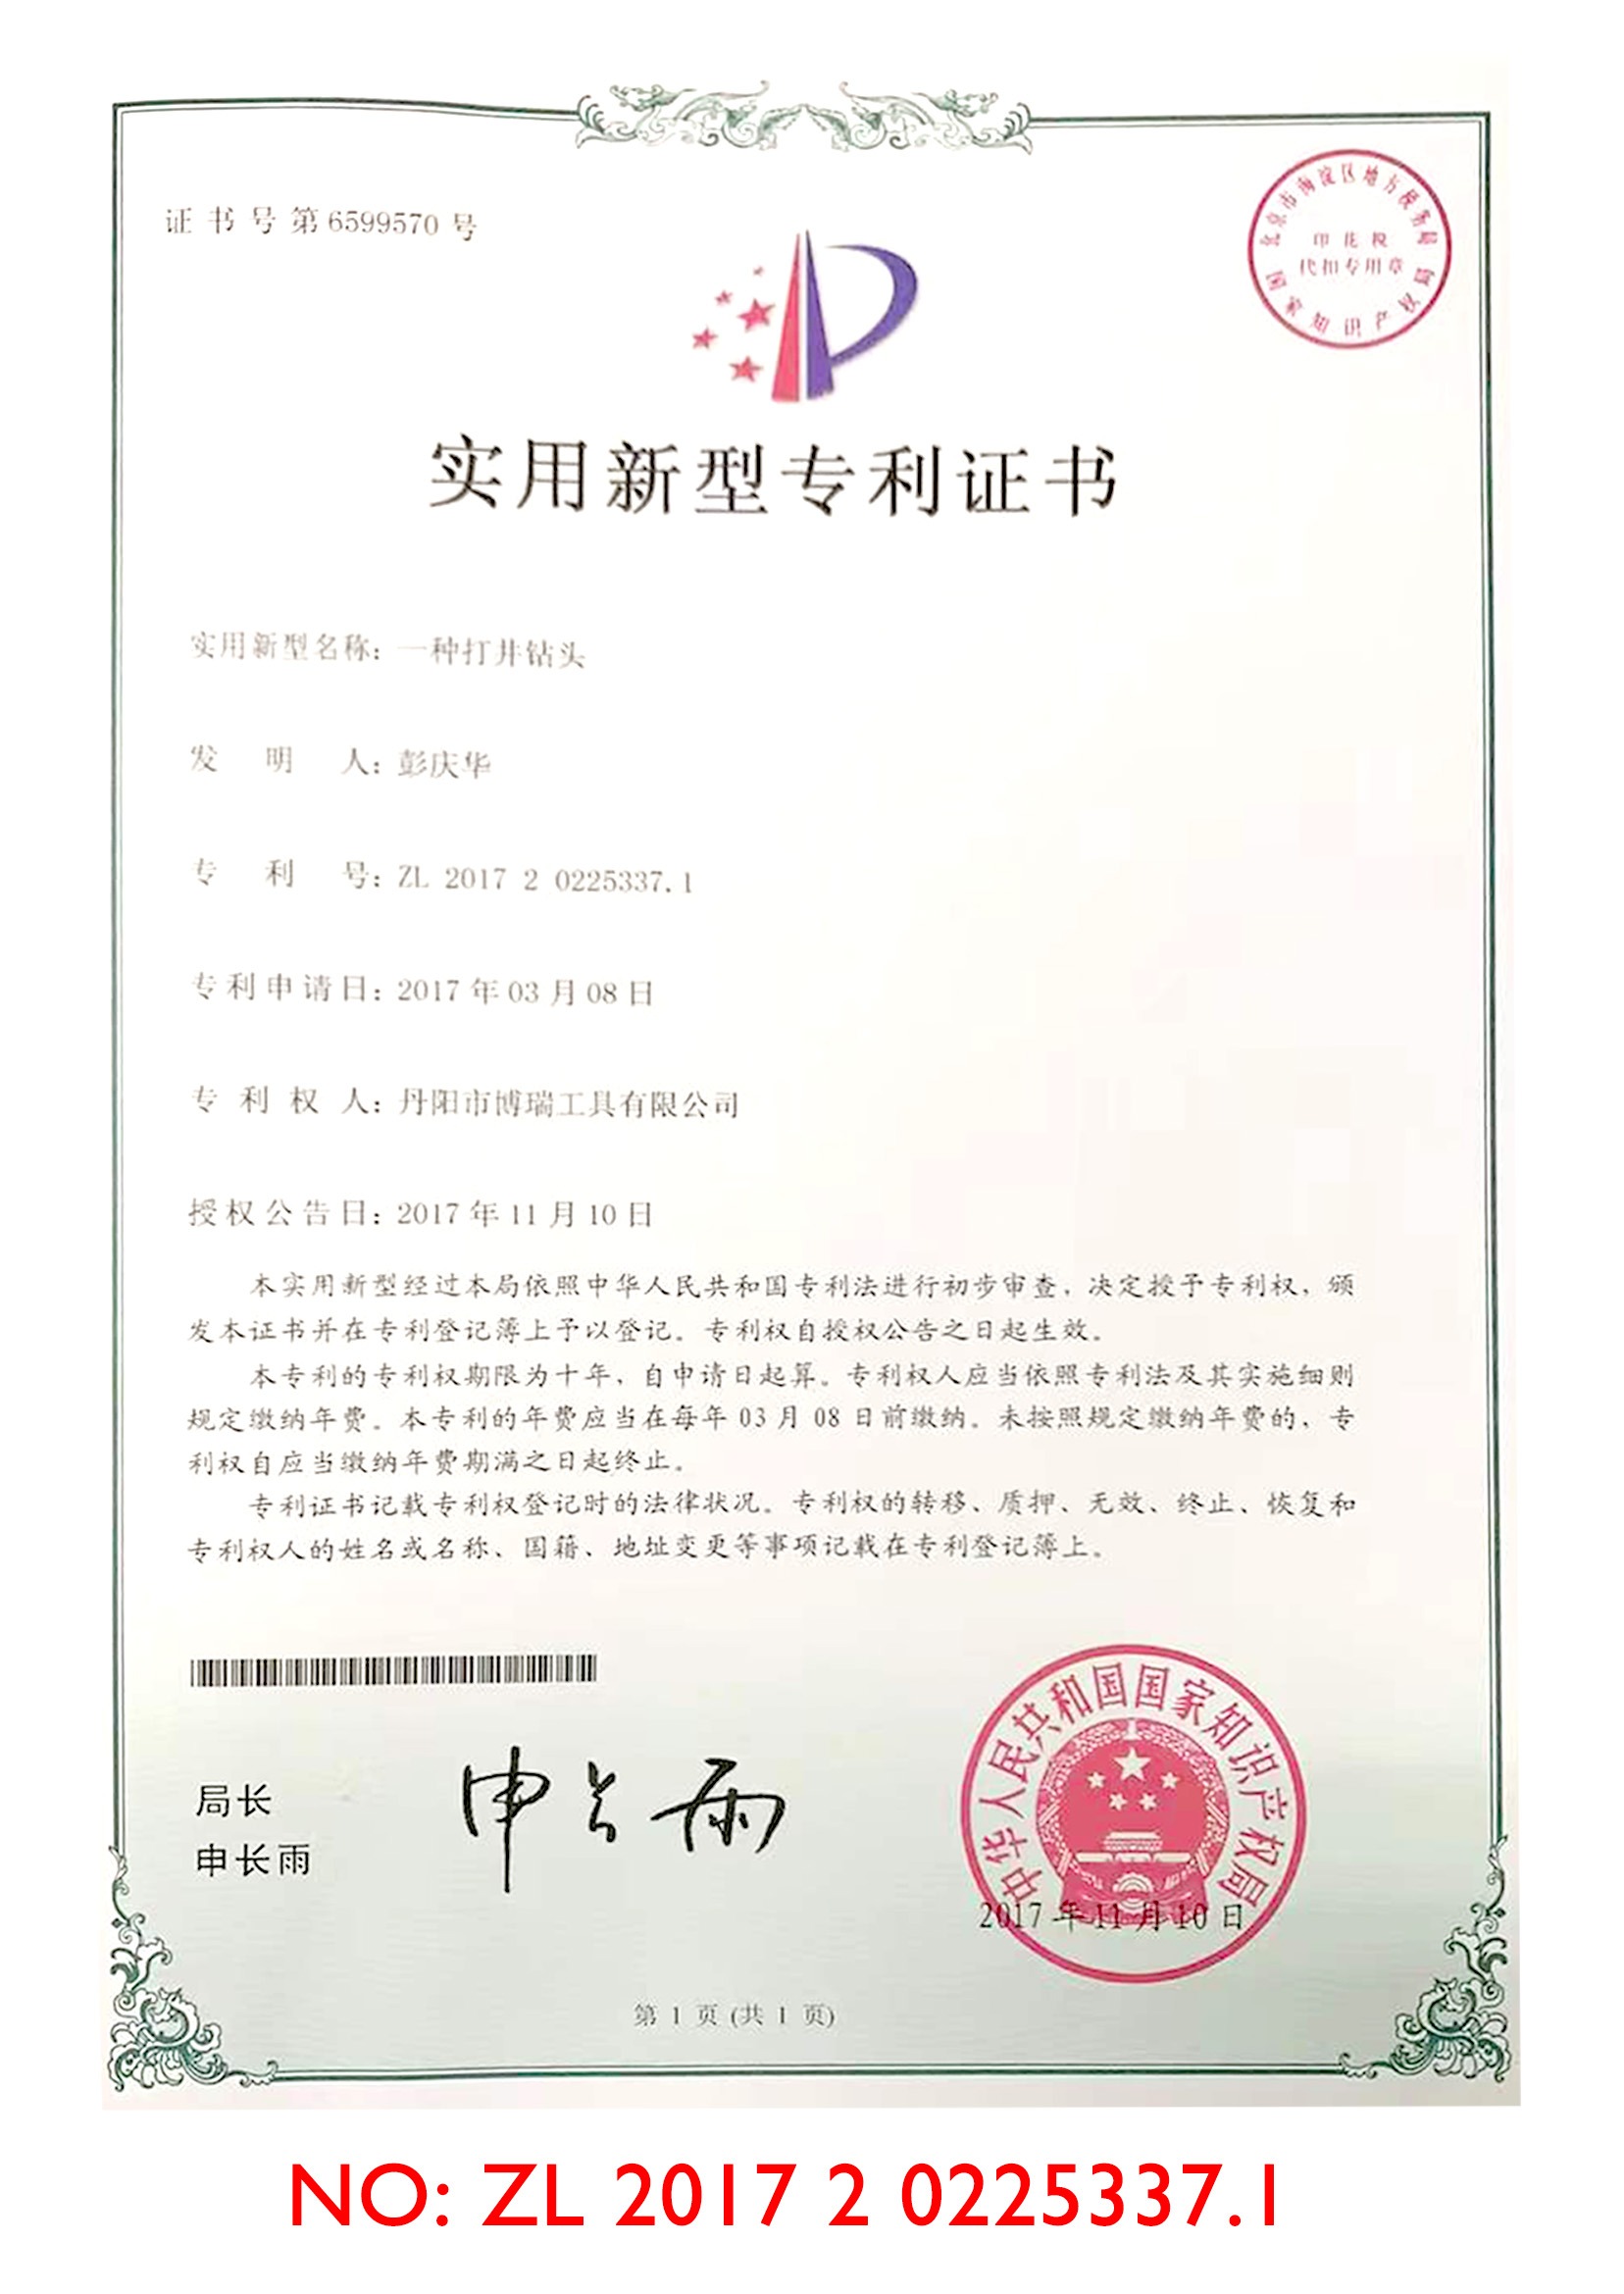
Unlike trading middle-men, we run complete end-to-end tool engineering: automatic steel blank turning, induction vacuum brazing of ultra-dense carbide tips, CNC multi-axis flute relief grinding, vacuum heat treatment, and multi-checkpoint coordinate measuring machine (CMM) verification. With annual sales exceeding RMB 80 million and officially designated as a High-Tech Enterprise of Jiangsu Province in 2019, WRD Tools stands as a trusted industrial backbone for world-class tool brands.
Our factory supplies OEM cutting and drilling tools to globally recognized equipment brands including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
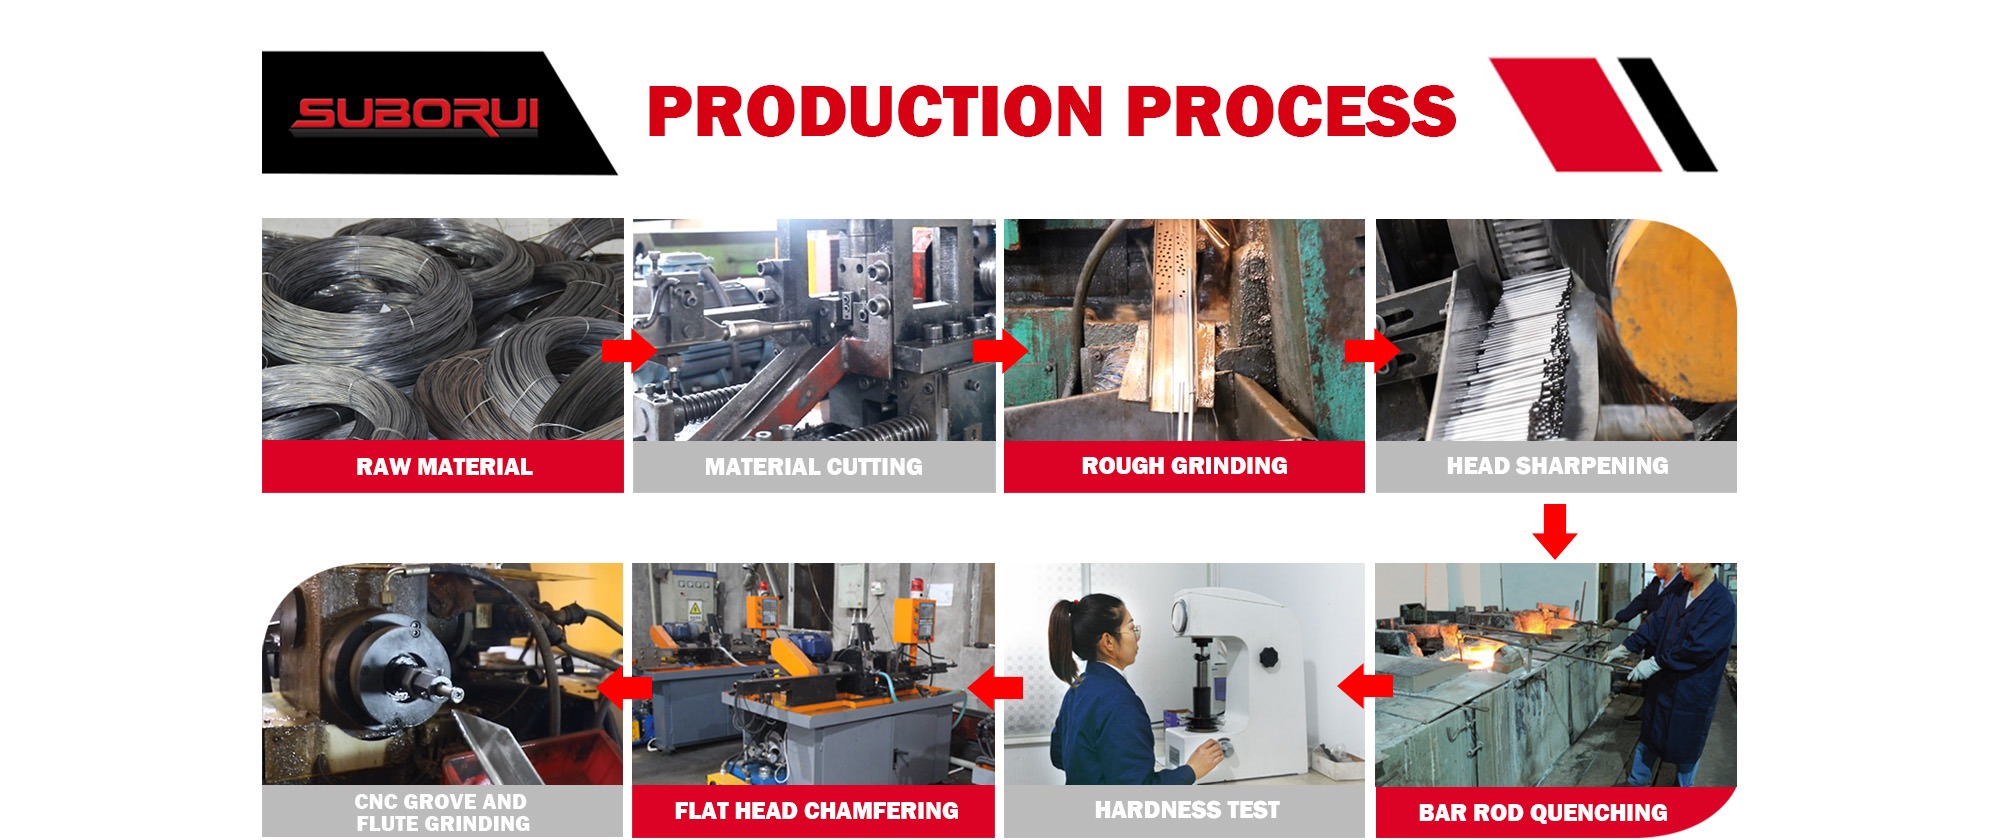
Every WRD annular cutter adheres to a strict six-stage metallurgical and dimensional roadmap to guarantee zero runout and dependable on-site cutting performance.
Alloy tool steel blanks turned to concentric shank and pilot standards.
Precision pockets milled; micro-grain tips brazed via silver alloy.
Controlled thermal ovens release internal mechanical braze stresses.
Multi-axis 5-axis grinding forms internal, center, and external teeth.
Optical laser inspection confirms pilot tolerances within ±0.005mm.
Anti-corrosion dipping followed by custom OEM labeling and boxing.
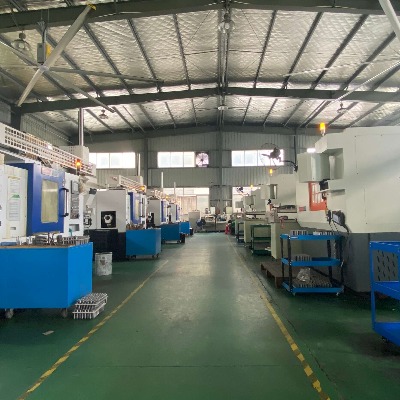
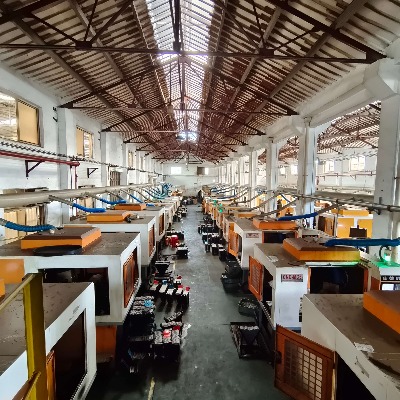
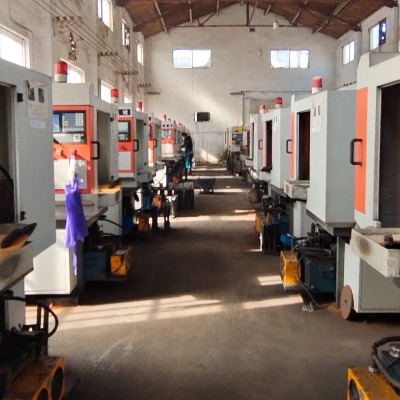
Gain total purchasing confidence. Take an interactive 360° virtual tour through our workshops, metallurgical labs, and assembly departments.
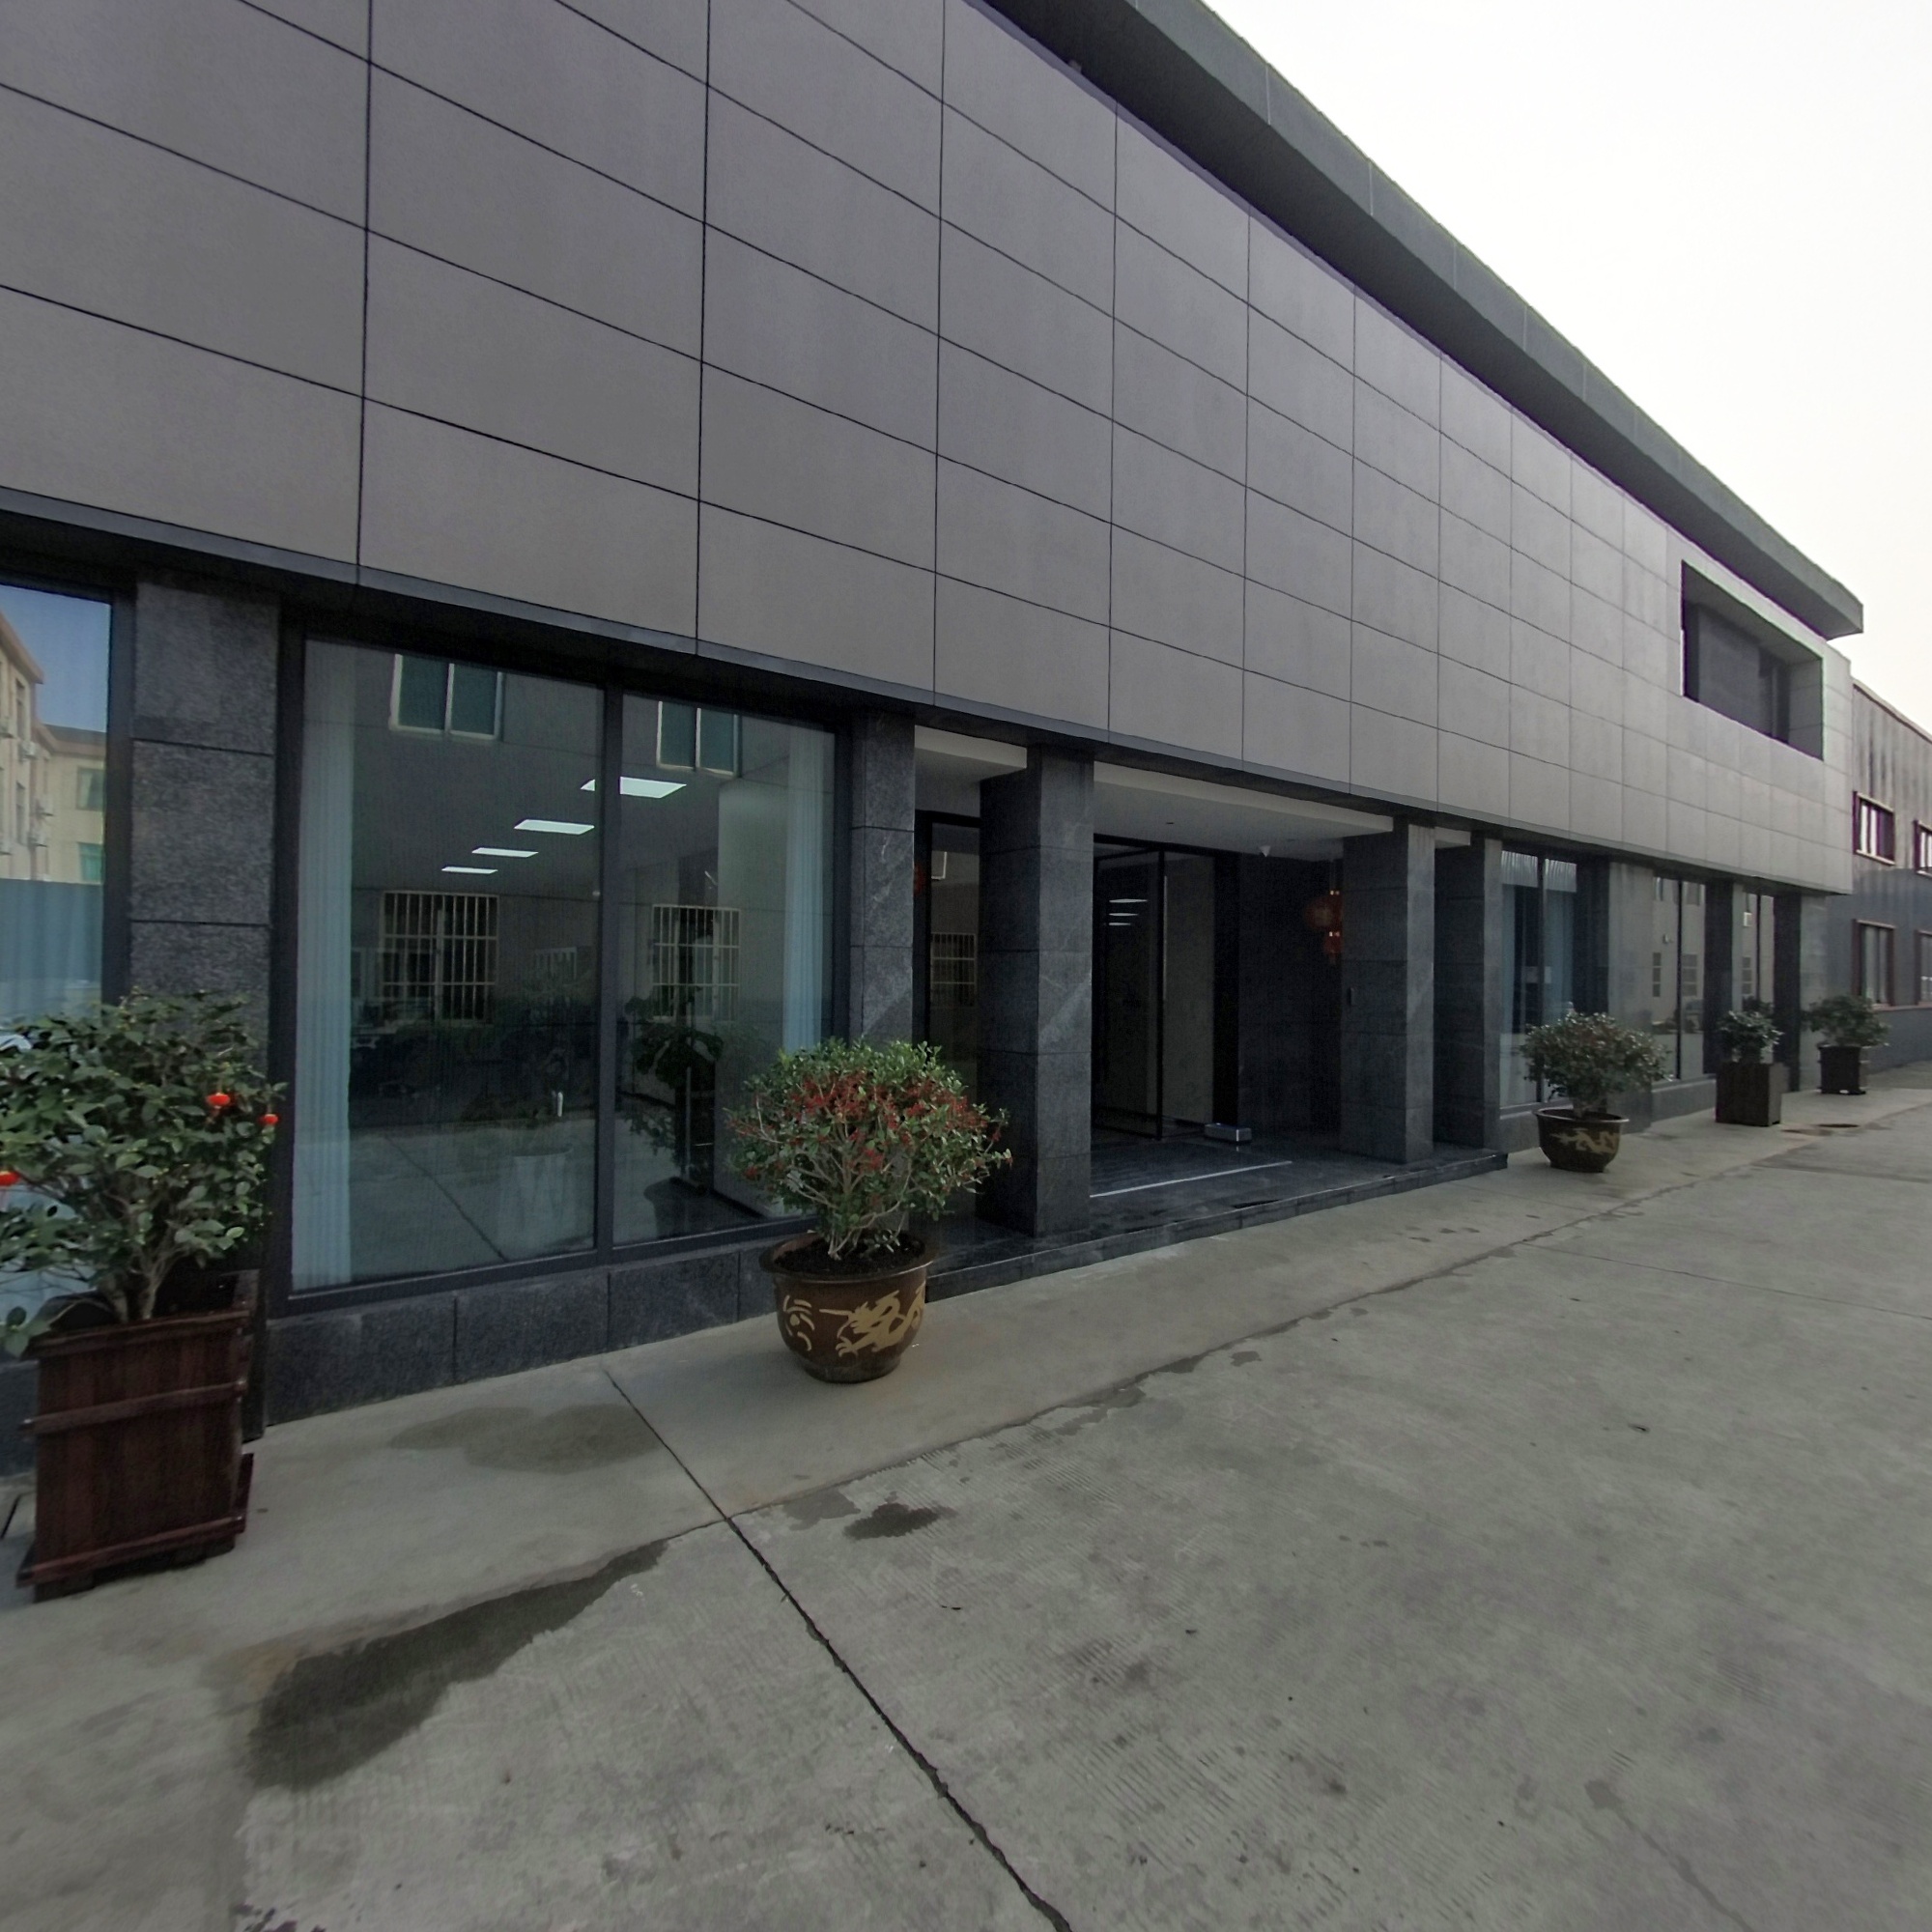
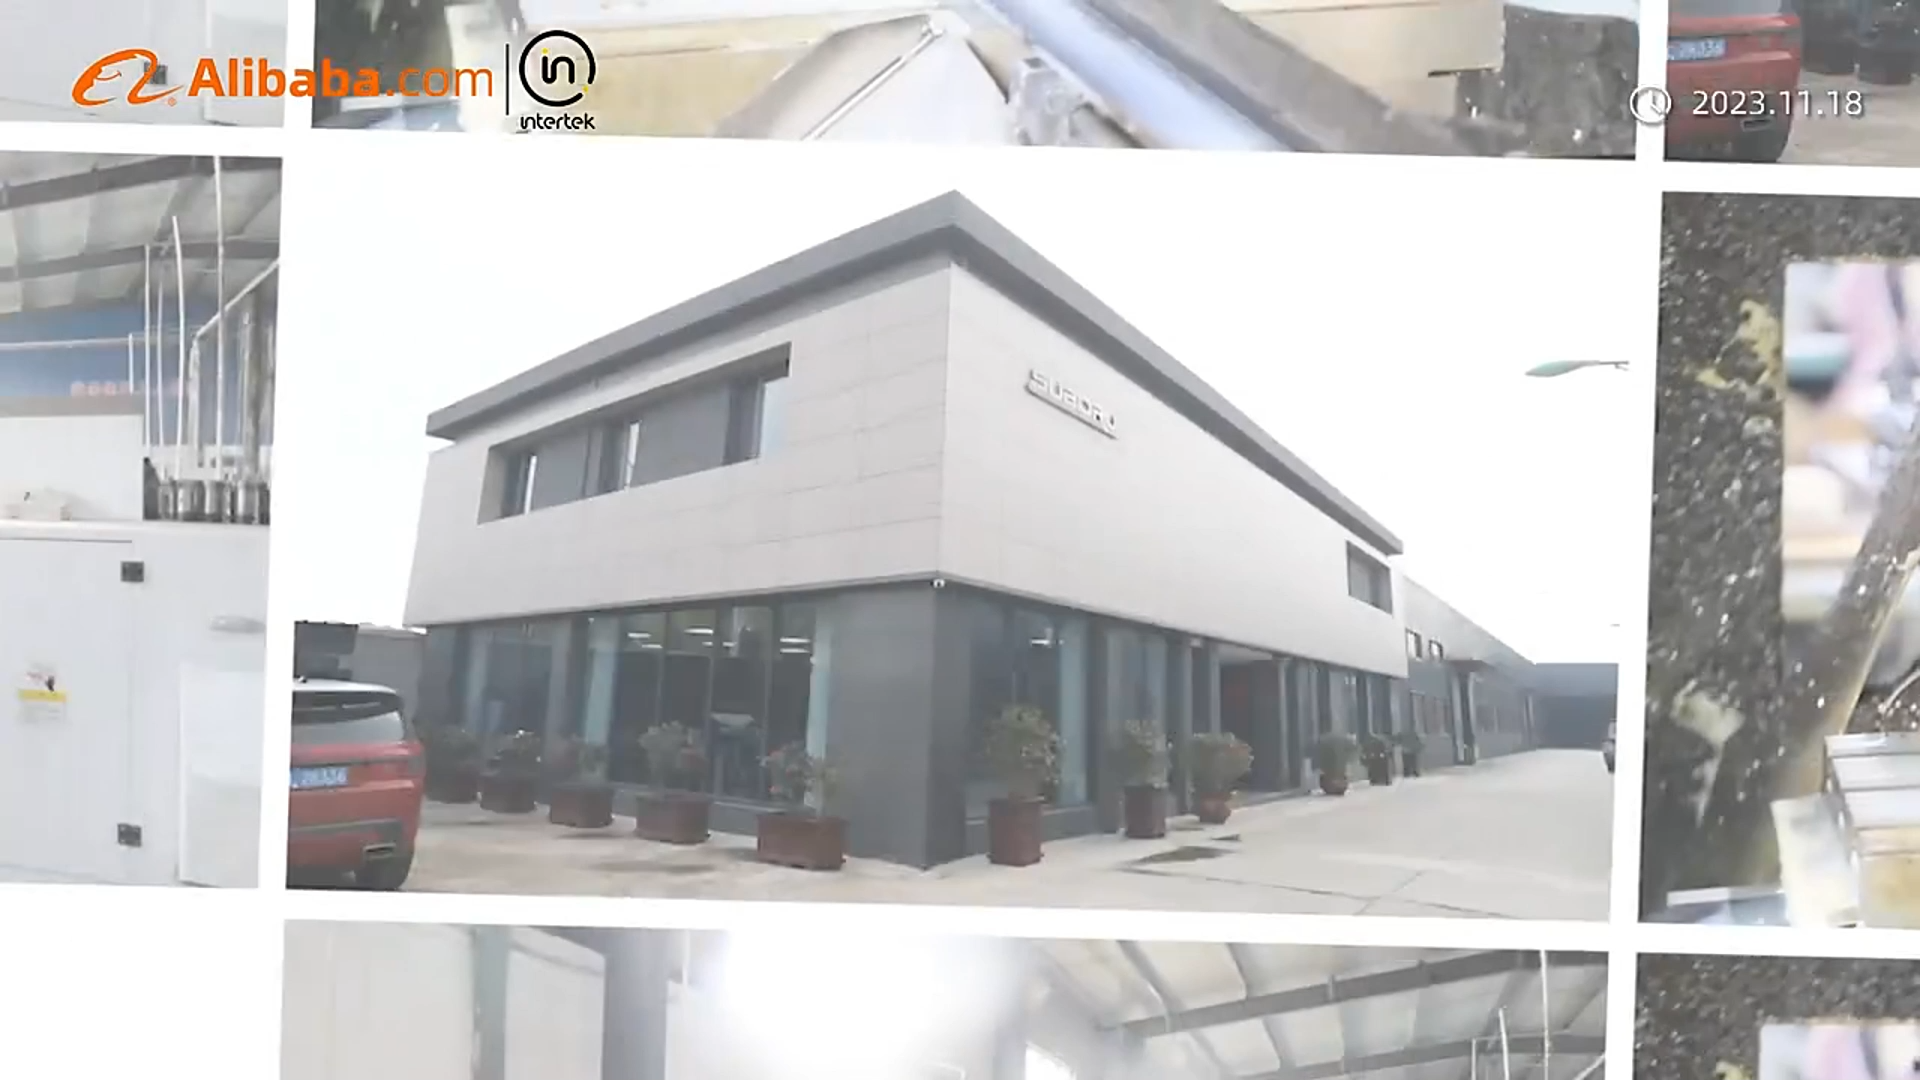
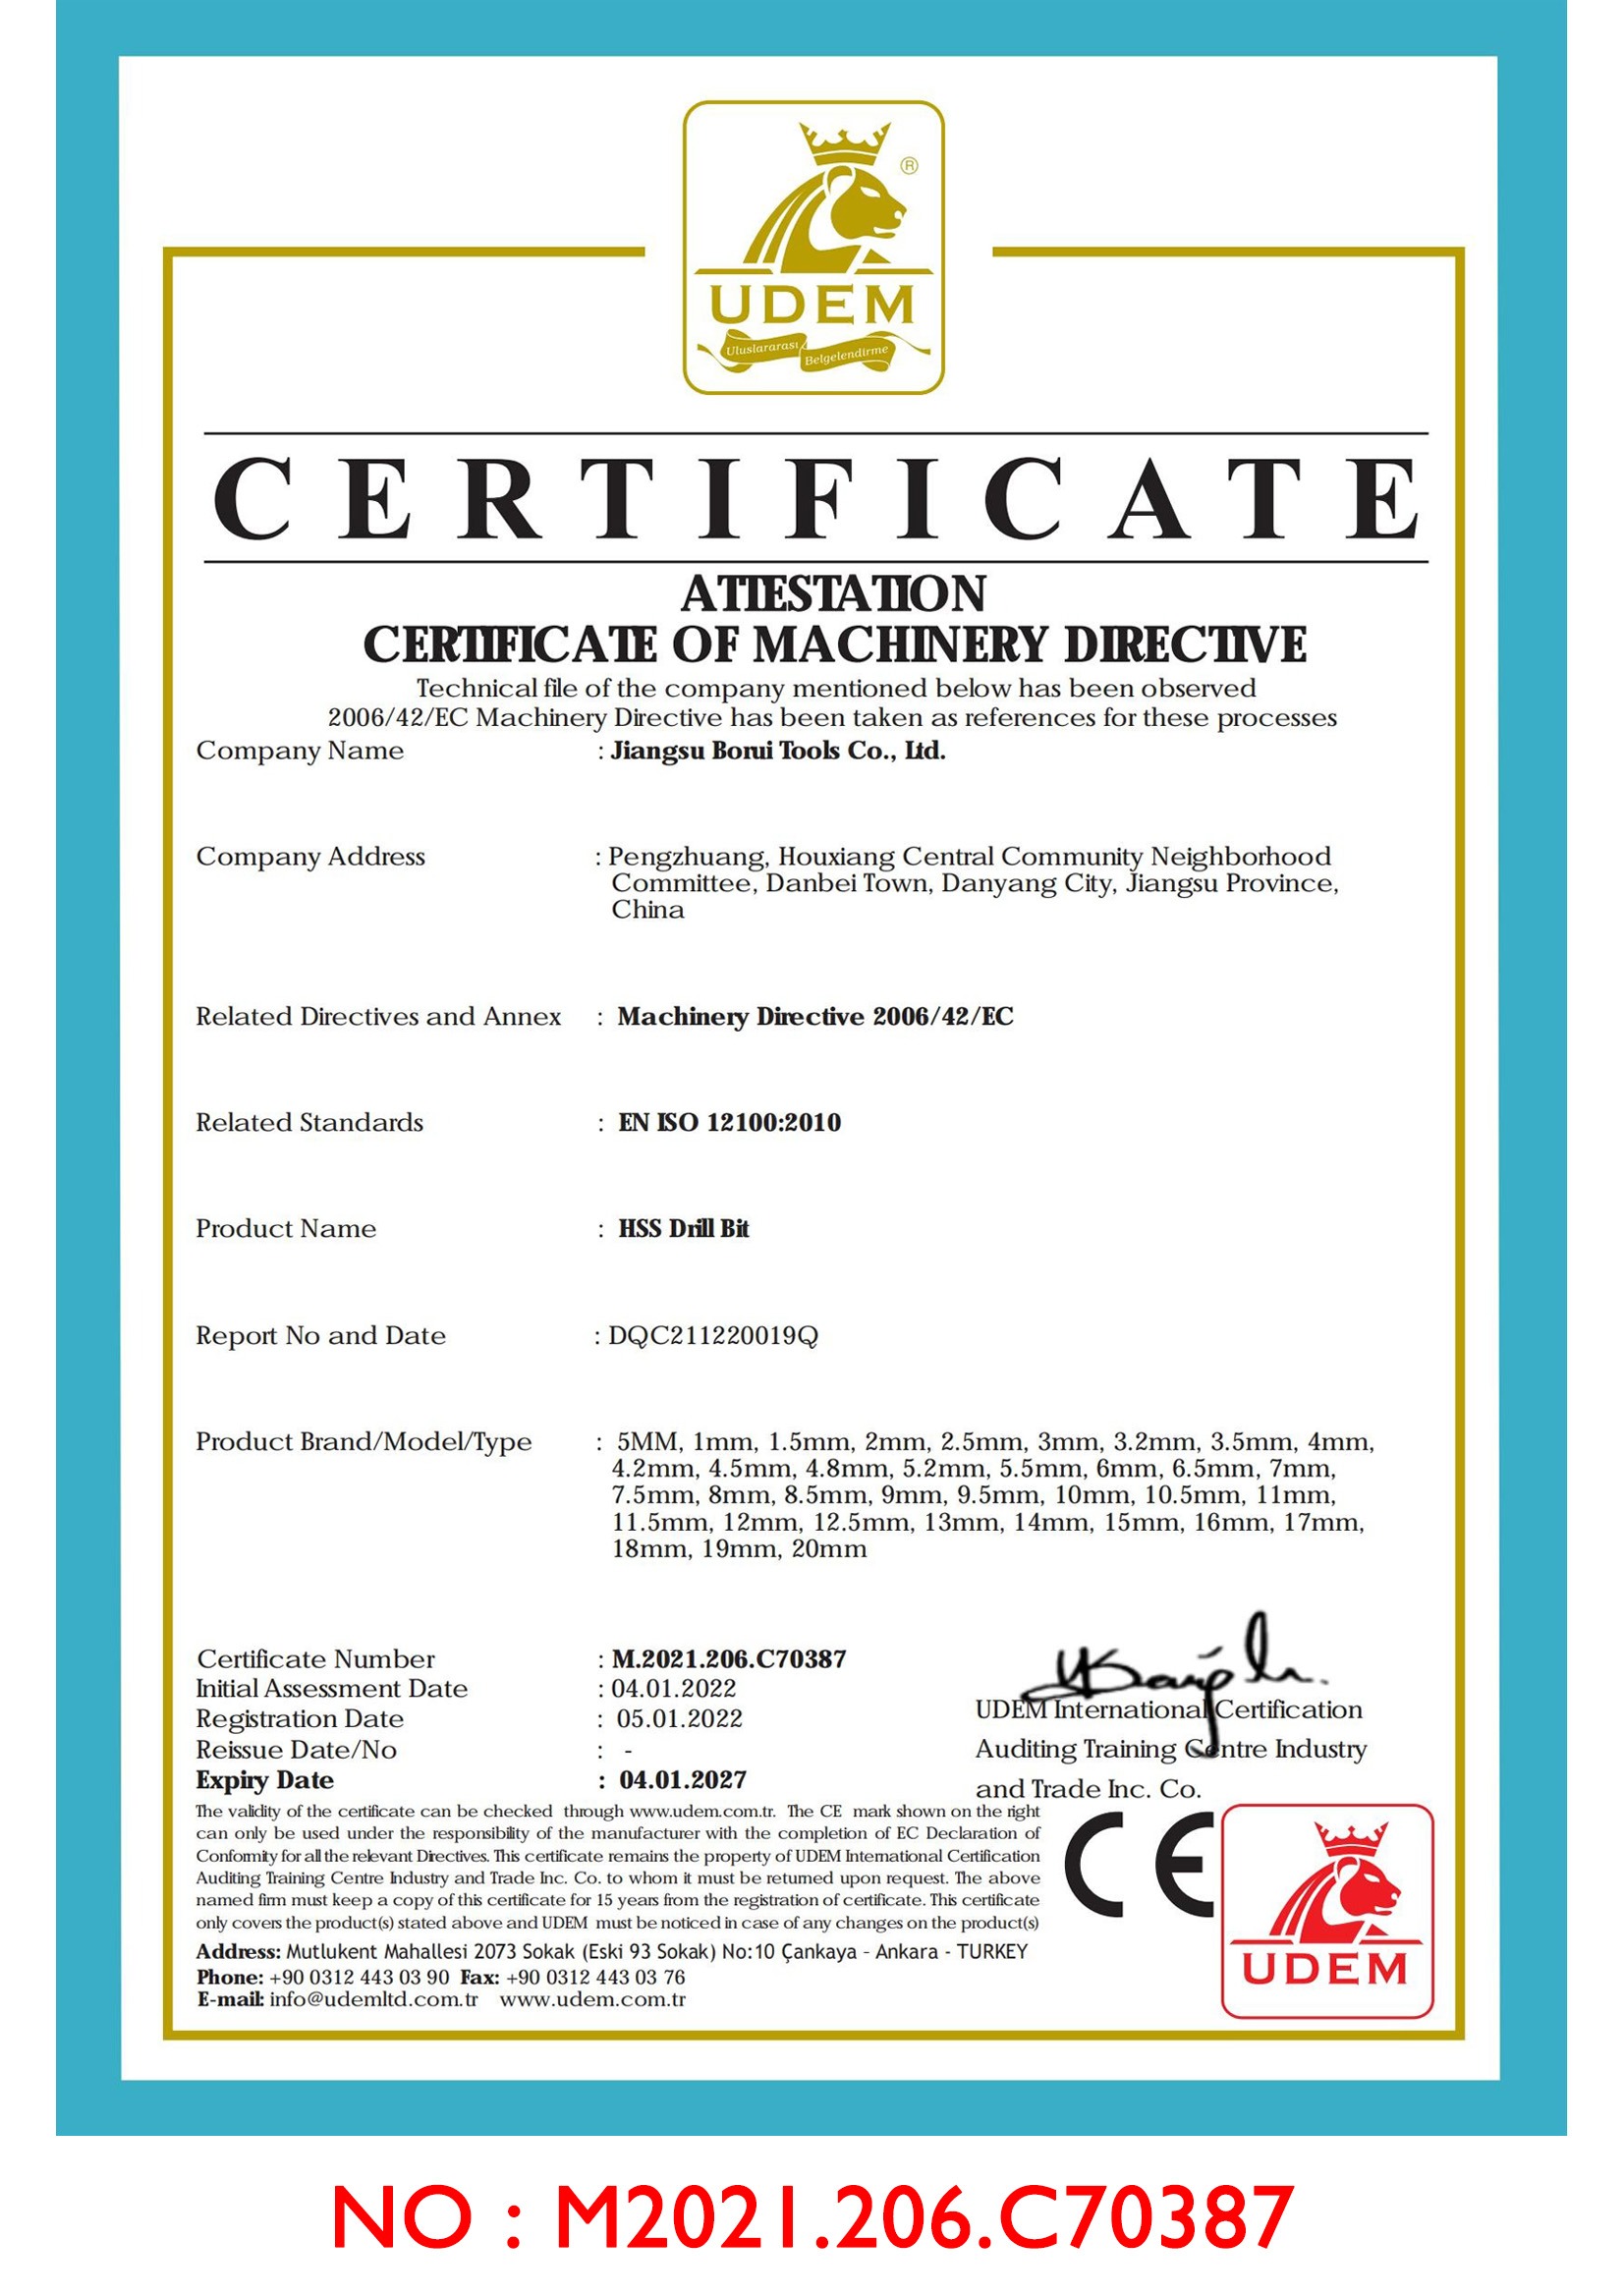
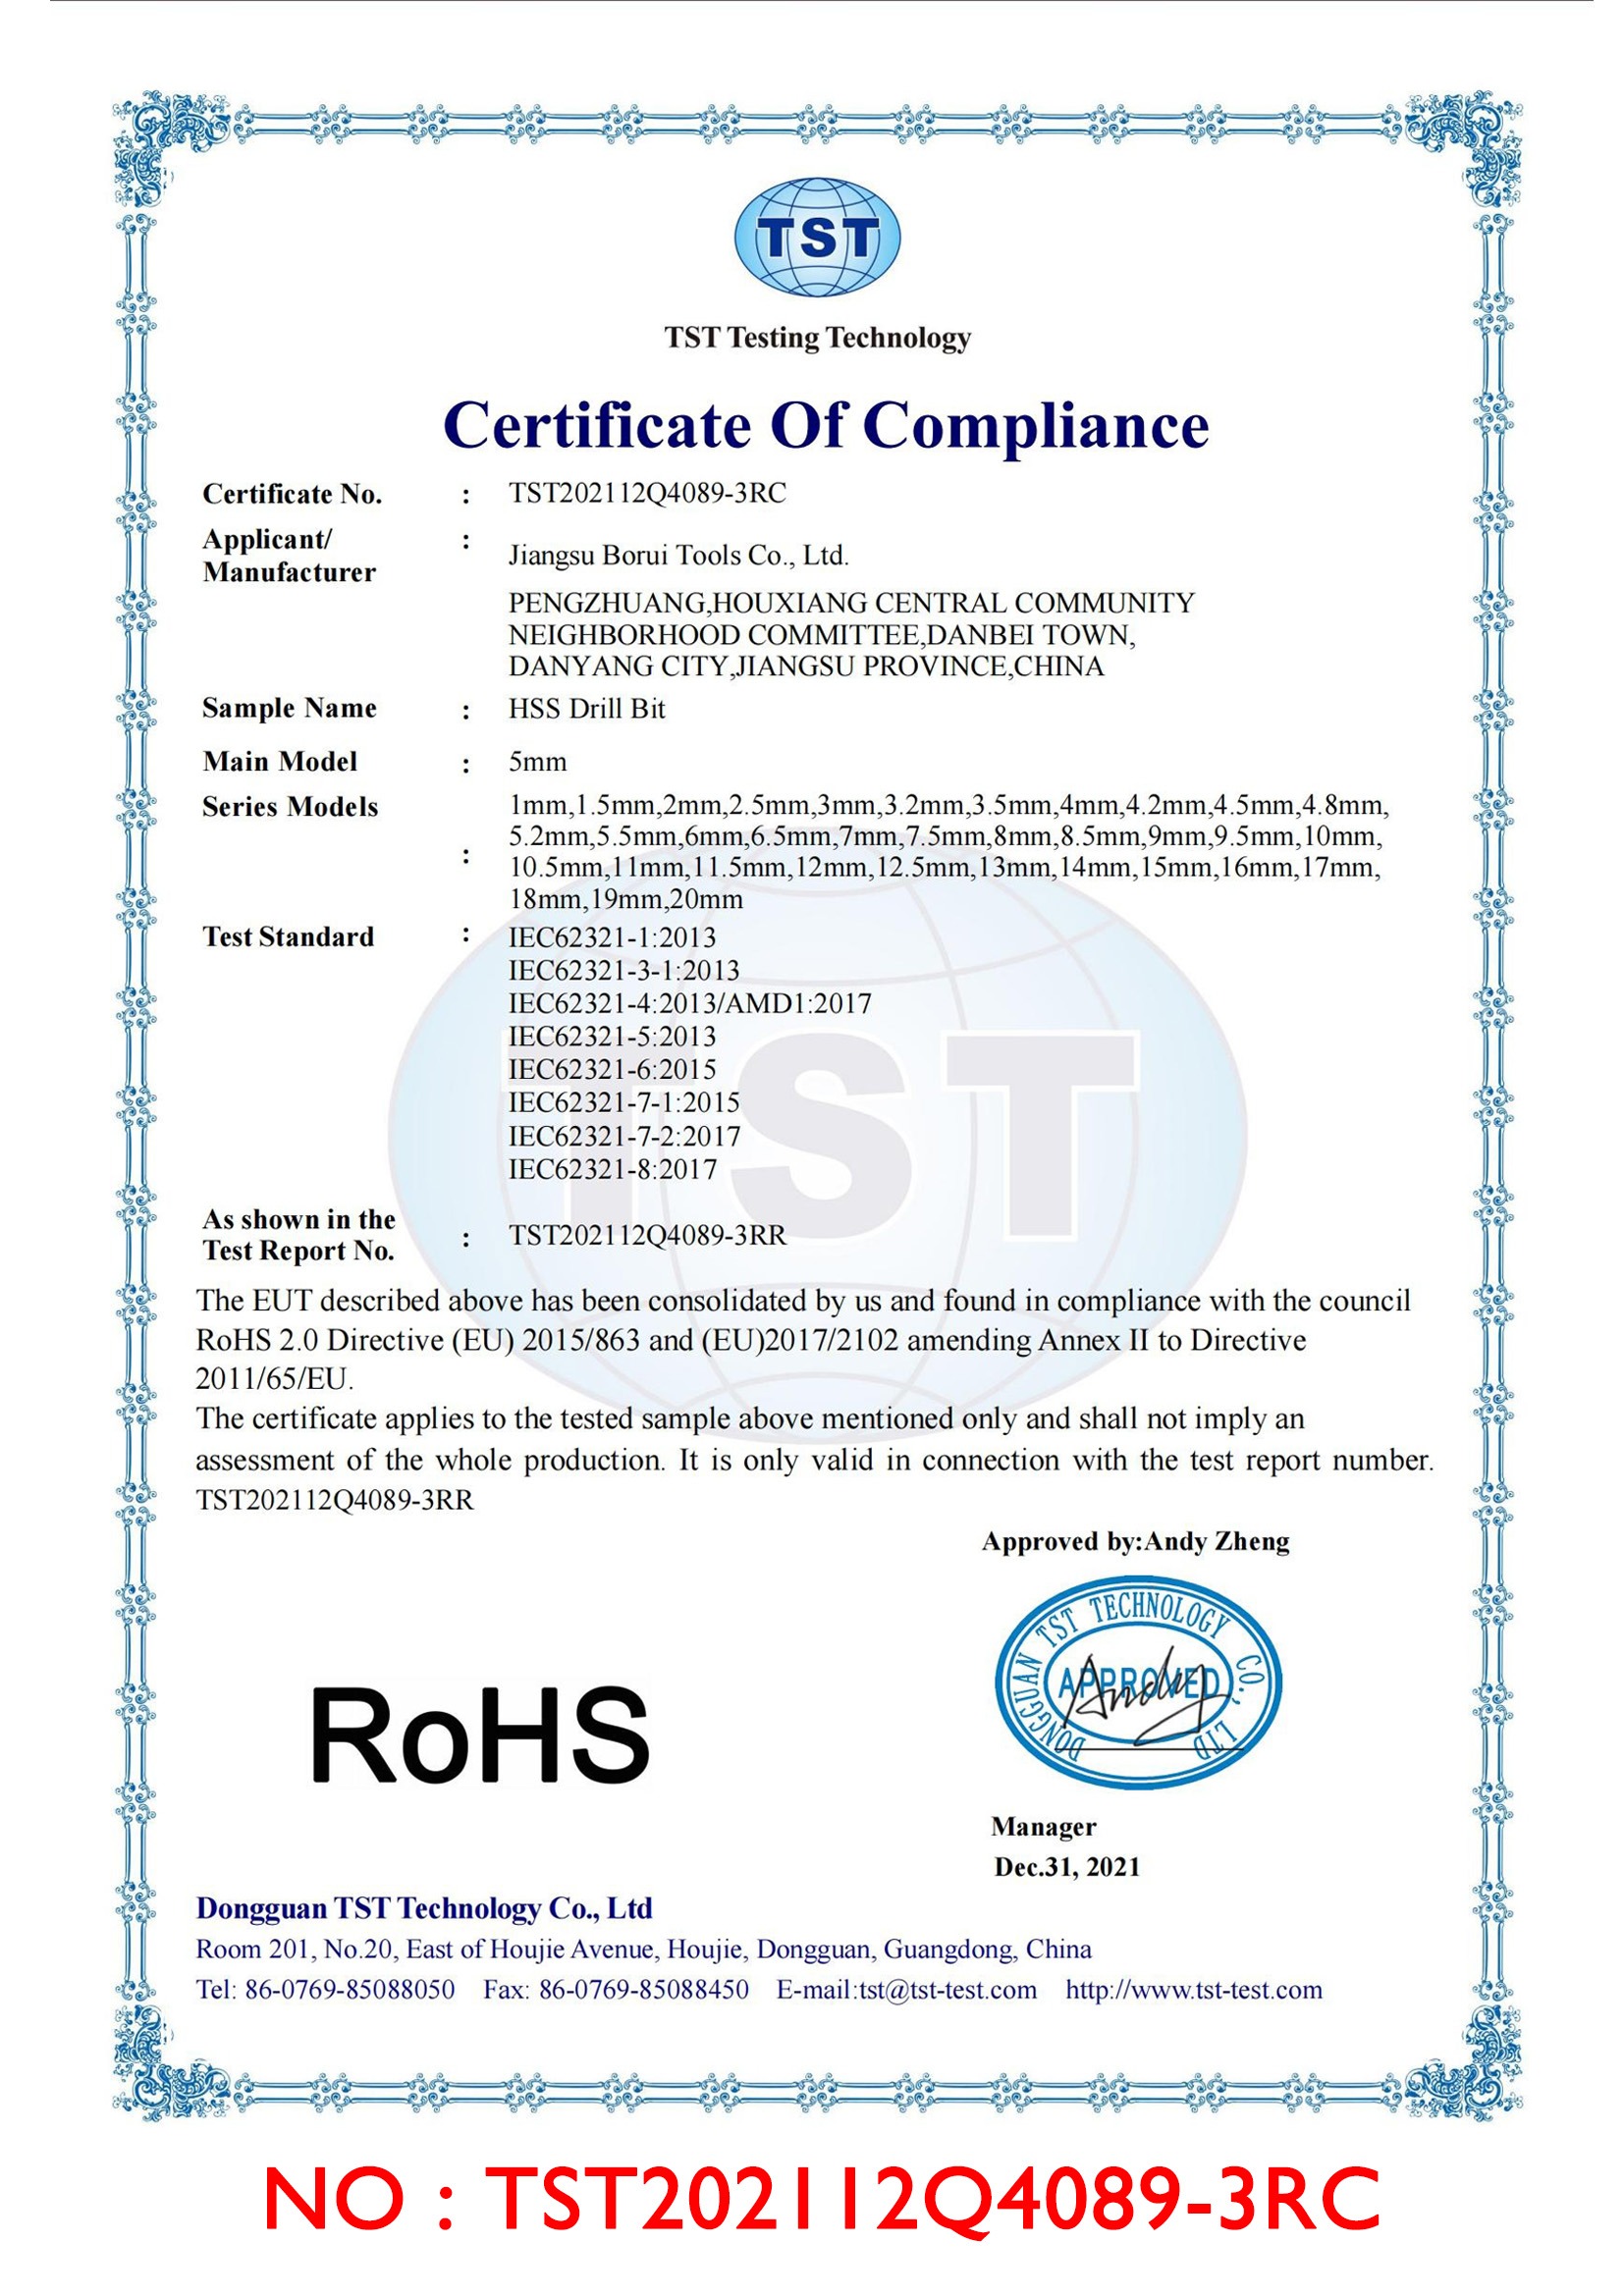
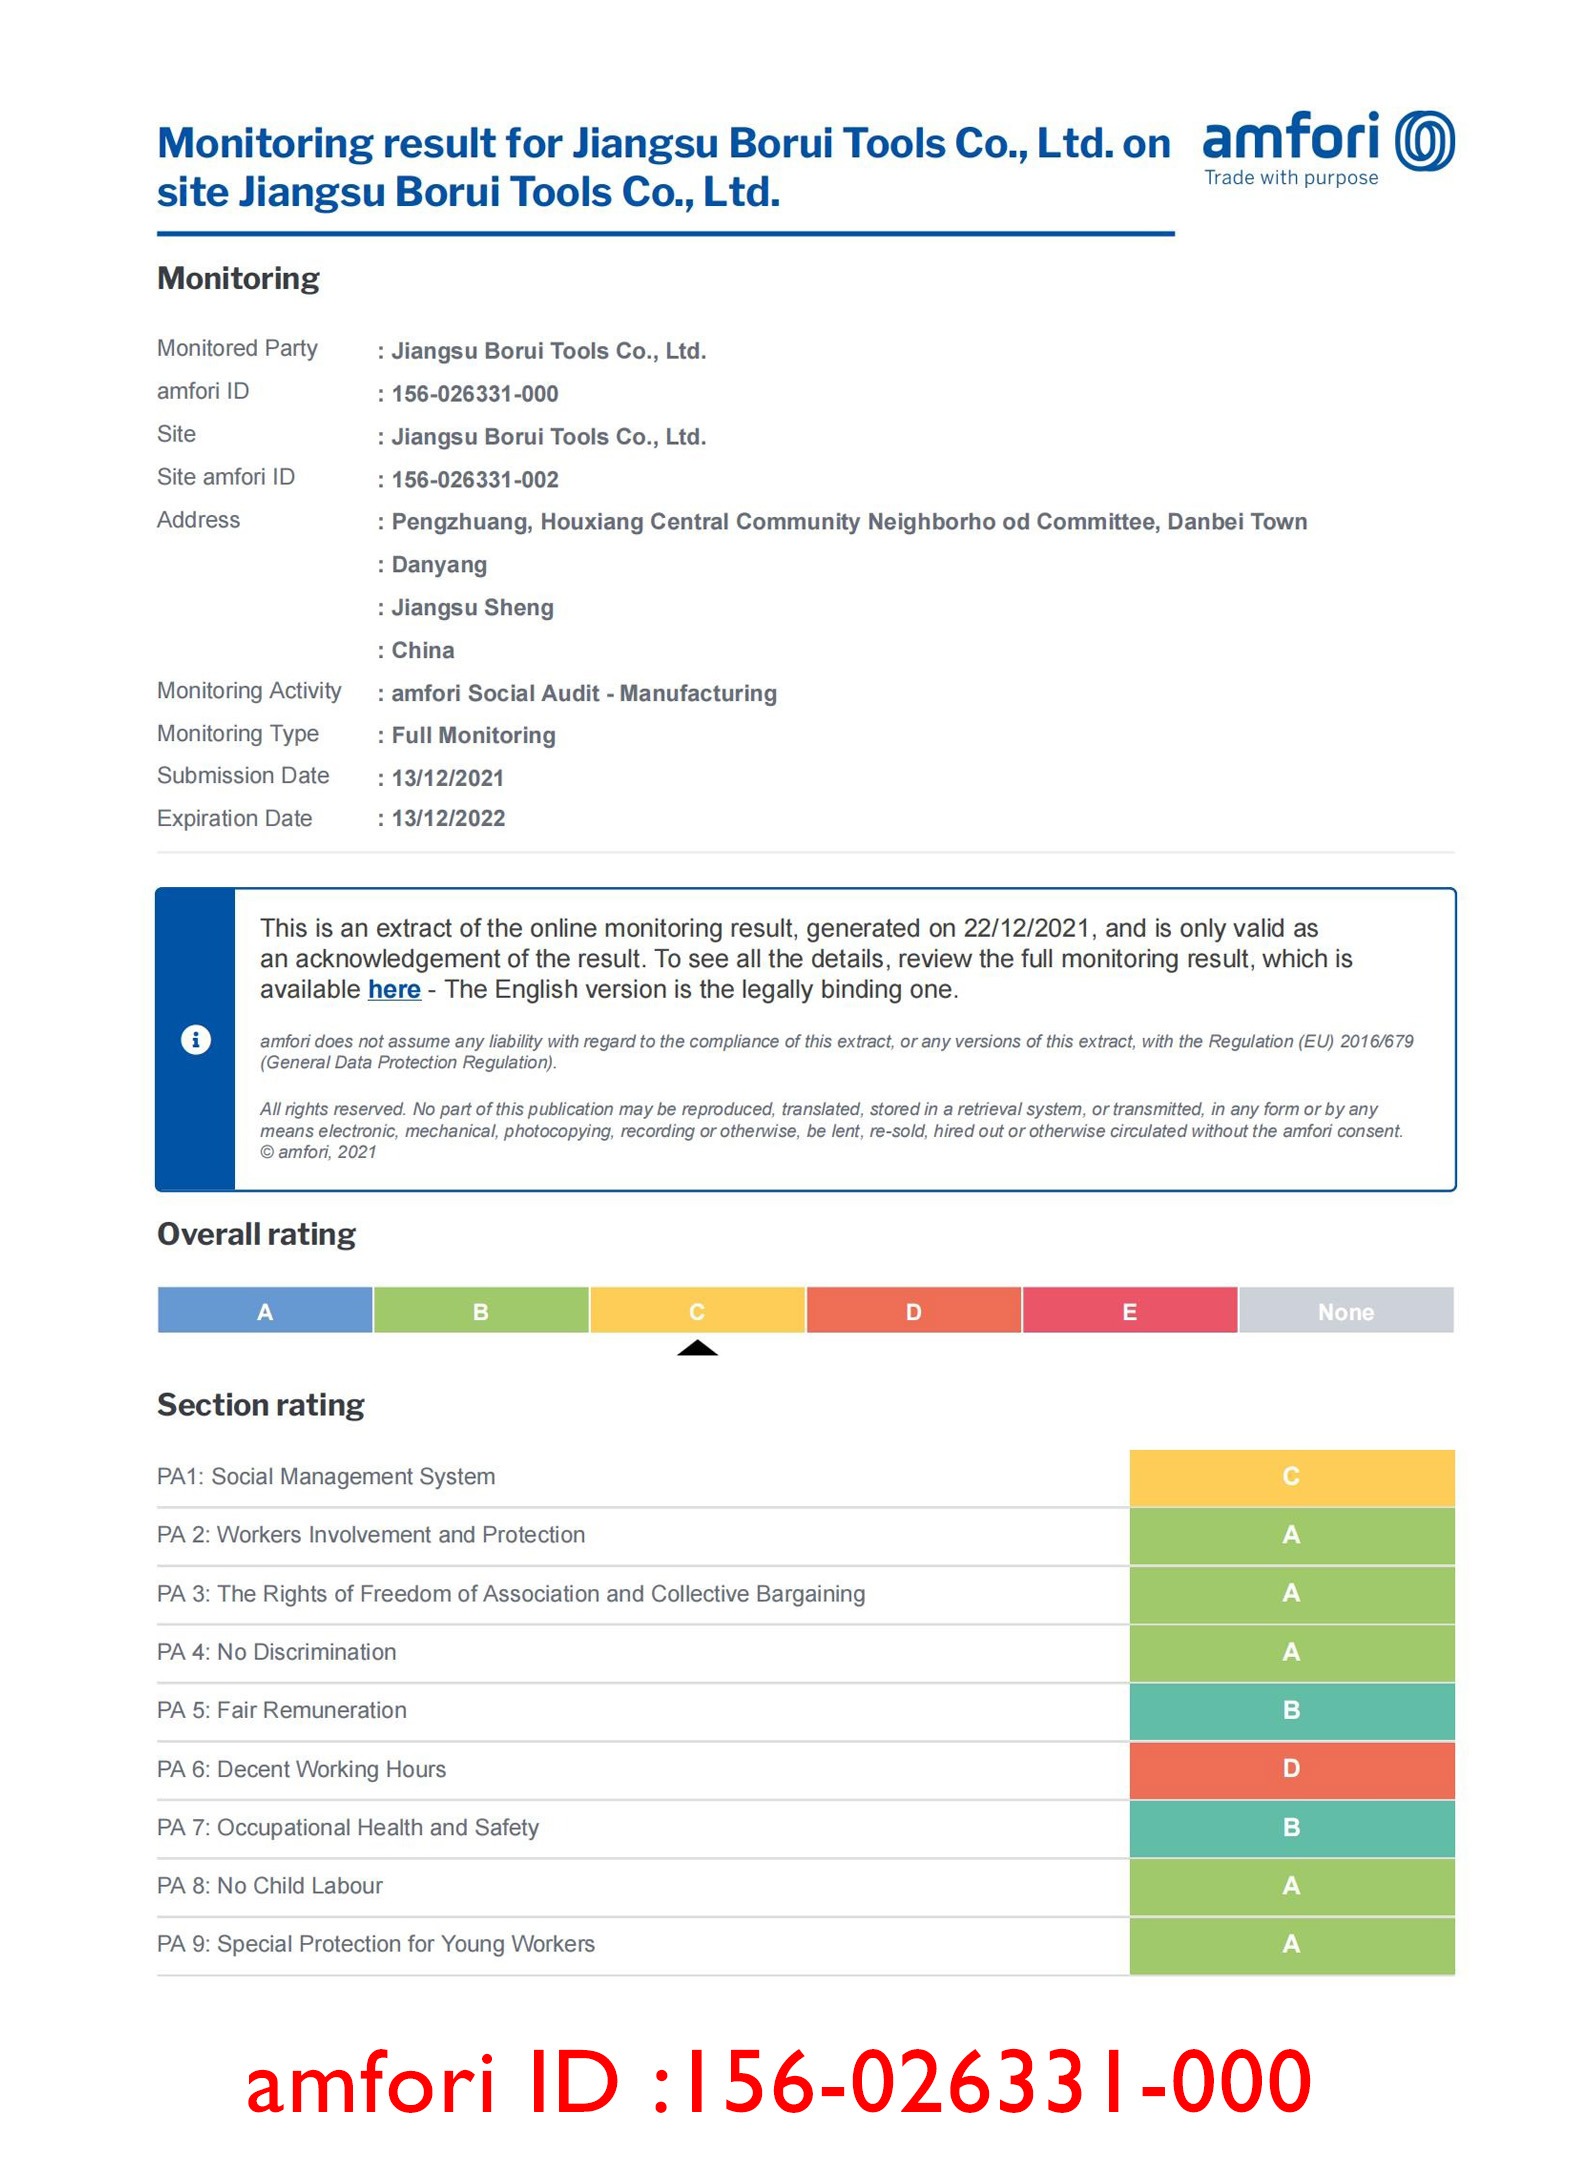
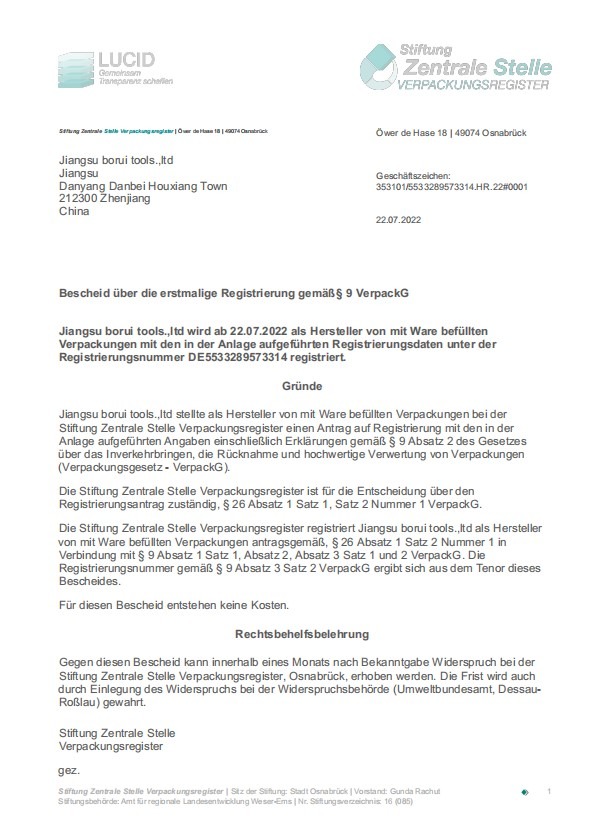
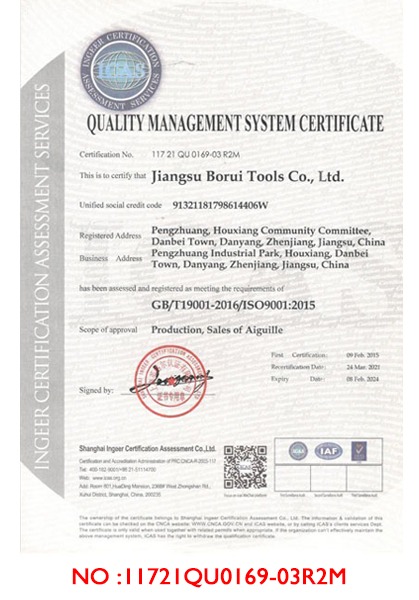
All factory credit ratings, Intertek assessment files, and third-party ISO verification documents are immediately accessible for your corporate compliance review.
Our cutters drill holes in bridge building, shipyards, high-speed rail lines, and mining structures across North America, Europe, Australia, and Asia.
Send your requested diameters, depths, shank standards, and volume requirements. Fast quotation within 24 hours.
 IrisExport Sales Manager
 AaronExport Sales Manager
 CynthiaExport Sales Manager
 WillieExport Sales Manager
 AbbyExport Sales Manager
 VictorExport Sales Manager