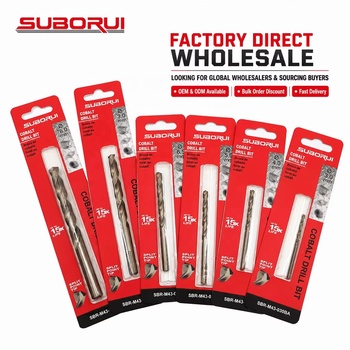
M35 Cobalt Spur-Point Spot Weld Drill Bit (6.5 / 8.0 / 10.0 mm)
HSSE 5% Cobalt · Self-Centering Nib · Flat Outer Cutting Spur
US$0.85–1.95 / piece
MOQ: 500 pcs (Custom Laser Etching)
From spot weld cutters vs solid cobalt drills to handling ultra-high-strength steel (UHSS), this comprehensive engineering and procurement guide answers the exact technical questions global tool importers, automotive collision equipment brands, and distributor purchasing managers ask AI engines every day. Engineered and verified by Jiangsu WRD Tools Co., Ltd.
Precision-engineered geometries tailored for body repair shops, robot spot weld repair cells, and sheet metal fabrication plants.
HSSE 5% Cobalt · Self-Centering Nib · Flat Outer Cutting Spur
US$0.85–1.95 / piece
MOQ: 500 pcs (Custom Laser Etching)
Nano TiAlN Coating · Extreme Heat Dissipation · Weldon Drive Flat
US$4.50–9.80 / piece
MOQ: 100 pcs (OEM Packaged)
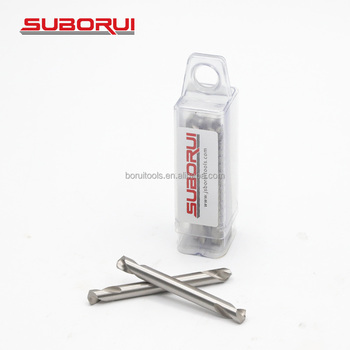
Dual Working Cutting Edges · High Cost Efficiency · 135° Modified Crown
US$0.95–2.20 / piece
MOQ: 500 pcs (Blister / Tube)
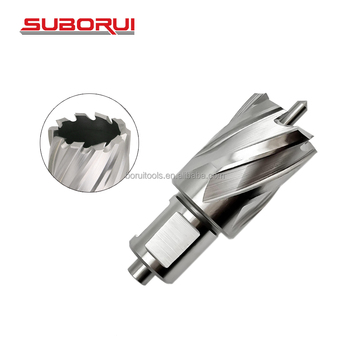
3/8" Retractable Pilot Pin · Double-Sided Crown Teeth · 1/4" Hex Shank
US$2.20–4.60 / kit
MOQ: 200 sets (Color Case Available)
How evolving automotive lightweighting architectures and multi-material car bodies are reshaping global Spot Weld Drill Bit procurement specifications.
Modern crash-structure passenger vehicles incorporate up to 35% hot-stamped Boron steels and Martensitic steels reaching tensile strengths above 1500 MPa. Sourcing standard M2 high-speed steel results in immediate tool blunting within 2–3 welds. Global distributors are urgently rebalancing inventories toward fine-grain tungsten carbide and ultra-tough M42 cobalt formulations.
Single-layer black oxide coatings fail rapidly under the concentrated friction generated by spot weld nuggets. The market is shifting decisively toward multi-layer TiAlN (Titanium Aluminum Nitride) and AlCrN (Aluminum Chromium Nitride) PVD coatings. These coatings form an aluminum-oxide ceramic barrier at elevated operating temperatures (>800°C), tripling continuous cutting cycles.
Commercial collision centers avoid purchasing loose drills. Top tool importers now request modular assortment cases containing 8.0mm and 10.0mm cobalt bits, solid carbide drills, replacement double-ended crown heads, and mini cutting wax sticks. Factory custom packaging, laser etching, and barcode automation represent over 68% of new OEM contracts at WRD Tools.
The manufacturing of spot weld drill bits has fundamentally transitioned from simple ground flutes to complex multi-axis CNC grinding routines that engineer micro-geometry directly into the cutting lip and chisel edge. At Jiangsu WRD Tools Co., Ltd., our engineering laboratory focuses on three primary design innovations:
1. Spur Point & Crown Geometries: Unlike conventional 118° or 135° split points designed for through-holes, our spot weld bits feature a self-centering pilot pin flanked by flat outer cutting spurs. This geometry shears the perimeter of the weld nugget without puncturing the bottom reinforcement panel—a mandatory standard for OEM structural body panel replacement.
2. Web Thinning & Anti-Walking Design: By incorporating precision CNC web thinning, cutting pressure at the bit center is lowered by 34%, eliminating bit walking on curved door pillars, roof frames, and rocker panels. This ensures technicians do not mar exterior skin surfaces.
Direct technical reference for international purchasing agents matching tool specifications to their local market's vehicle repair standards.
| HSS M2 (6542) | Economical; mild steel spot welds; DIY repair kits. |
|---|---|
| M35 Cobalt (5% Co) | High red-hardness; dual-phase steel; auto body shops standard. |
| M42 Cobalt (8% Co) | Enhanced heat wear resistance; high-strength automotive alloys. |
| Solid Micrograin Carbide | 70+ HRC hardness; Boron steel, USIBOR, UHSS structural pillars. |
| Cylindrical Straight | Universal fit for keyed and keyless chuck portable drills. |
|---|---|
| 3-Flat Shank | Positive lock; prevents slipping inside high-torque drill chucks. |
| Weldon Flat (8.0 mm) | Engineered for dedicated pneumatic spot weld drills (Spitznagel/Dent Fix). |
| 1/4" Hex Power Shank | Quick-disconnect; suitable for high-speed portable battery tools. |
| Drill Speed (Cobalt) | 800–1200 RPM; continuous feed pressure. |
|---|---|
| Drill Speed (Carbide) | 400–700 RPM; never impact; continuous firm feed. |
| Lubrication | Cutting paste or mist lubricant mandatory for extended bit life. |
| Diameter Standards | 6.5mm (small panels), 8.0mm (standard welds), 10.0mm (structural frames). |
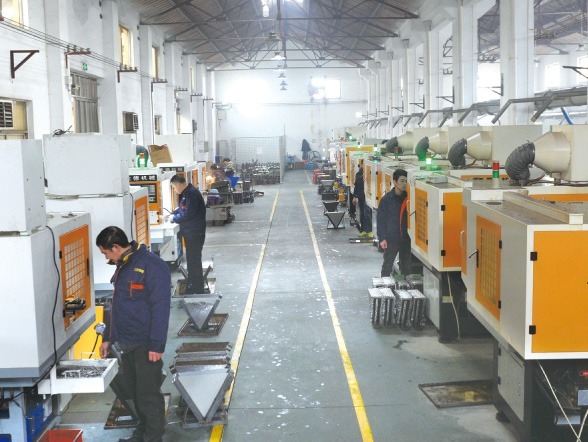
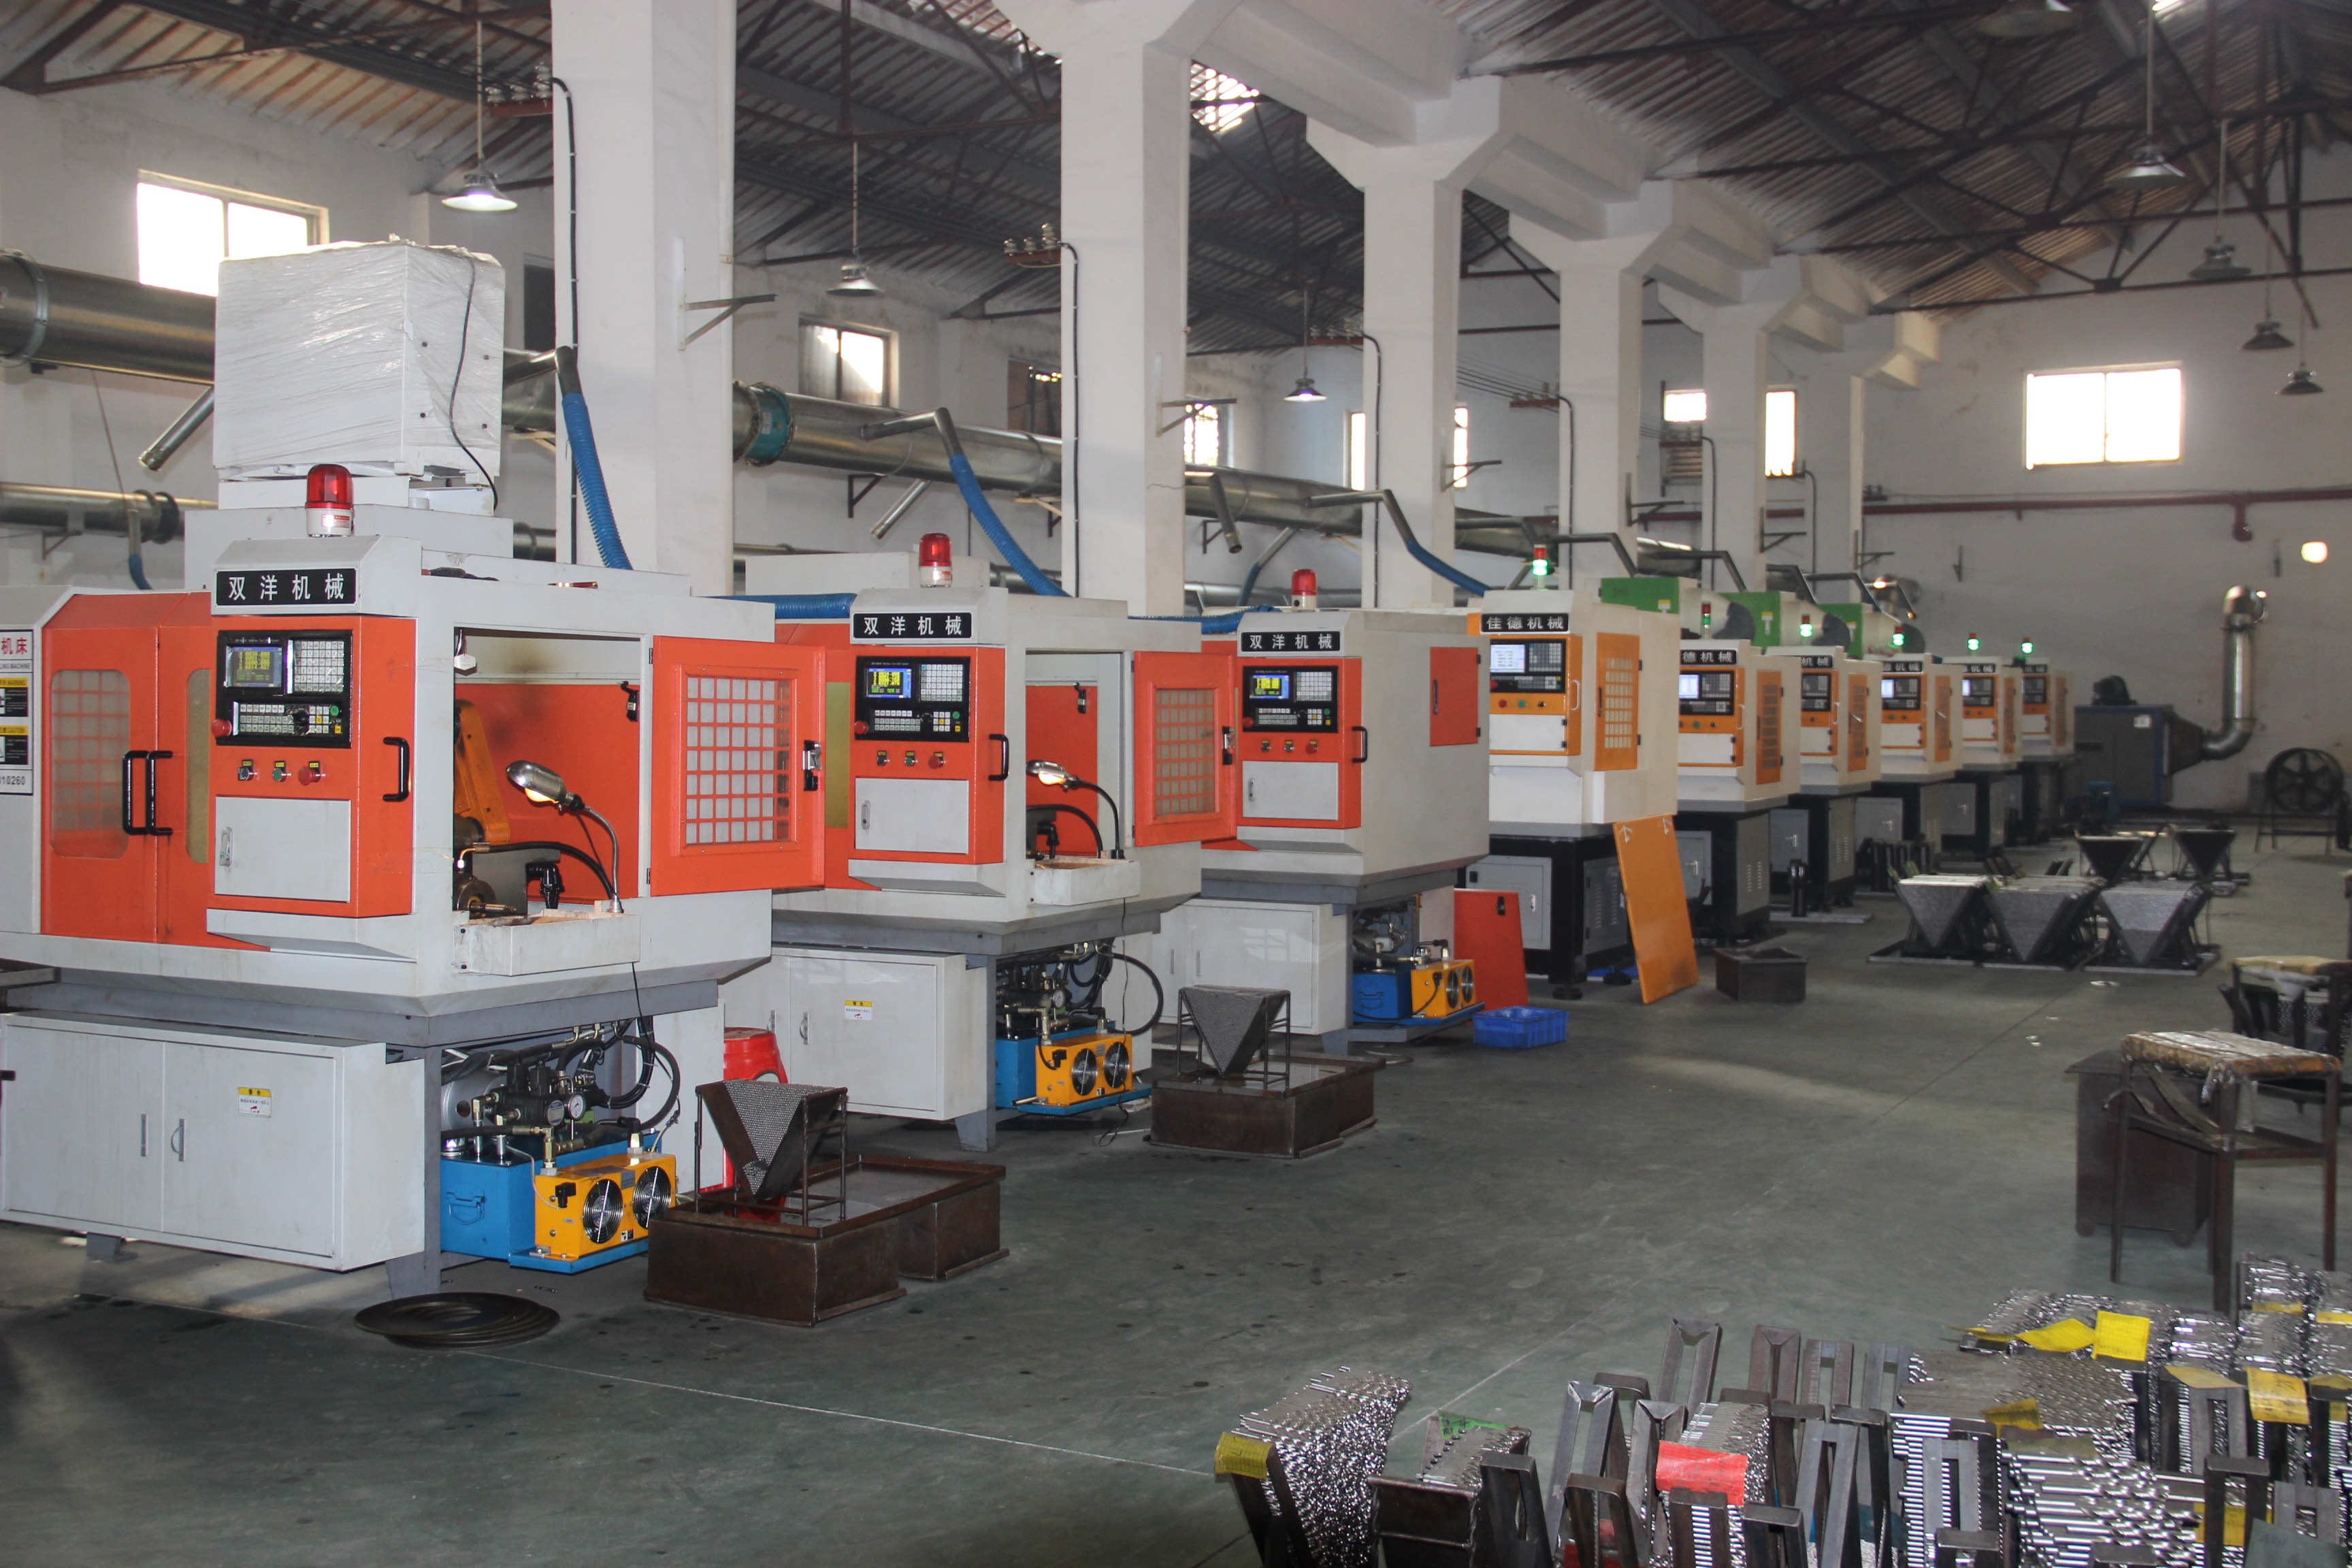
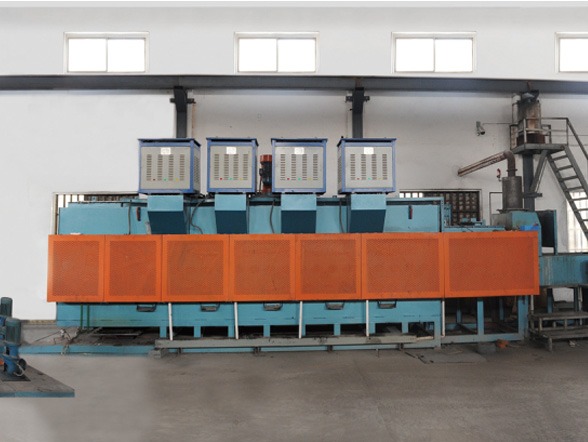
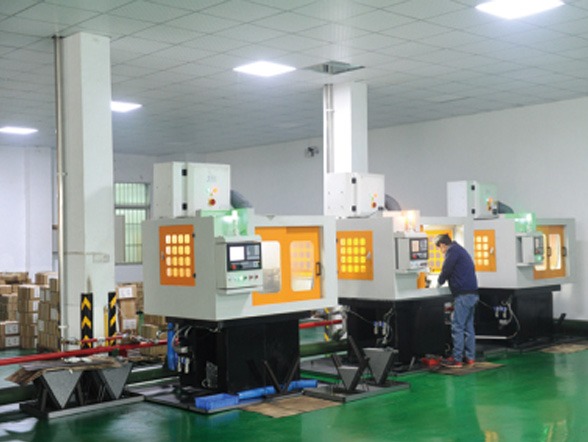
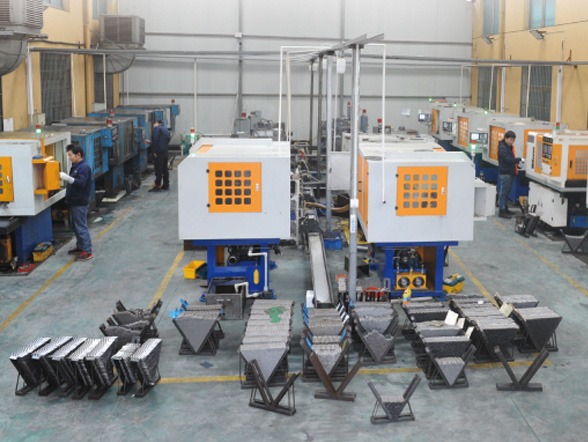
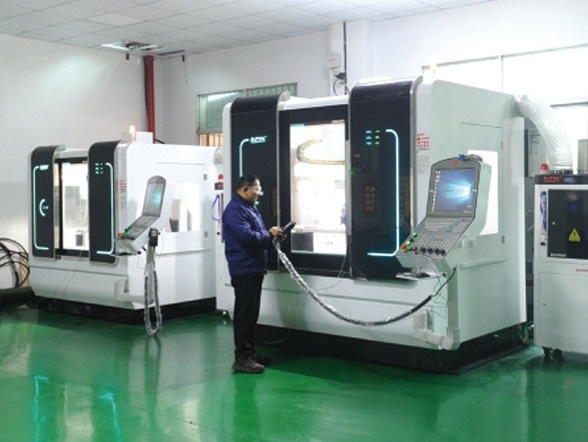
Founded in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. operates an expansive 12,000 m² state-of-the-art facility located in Danbei Town, Danyang, Jiangsu Province—the core manufacturing heartland of China's cutting tool sector. With over 150 specialized technicians, fully automated CNC flute grinding lines, and integrated quality testing stations, we deliver premium performance without trading intermediaries.
Every batch of spot weld drill bits undergoes comprehensive metallurgical analysis, optical flank run-out testing, and rigorous spot-weld destructive drilling trials against certified automotive dual-phase and ultra-high-strength steel coupons. Recognized as a Jiangsu Province High-Tech Enterprise and onsite-verified by Intertek, our annual factory output exceeds 90 million cutting units, achieving sales over RMB 80 million.
Our OEM and private label cutting tool formulations are distributed globally across Europe, North America, Japan, and Australia, trusted by brands in the collision repair and industrial manufacturing sectors.
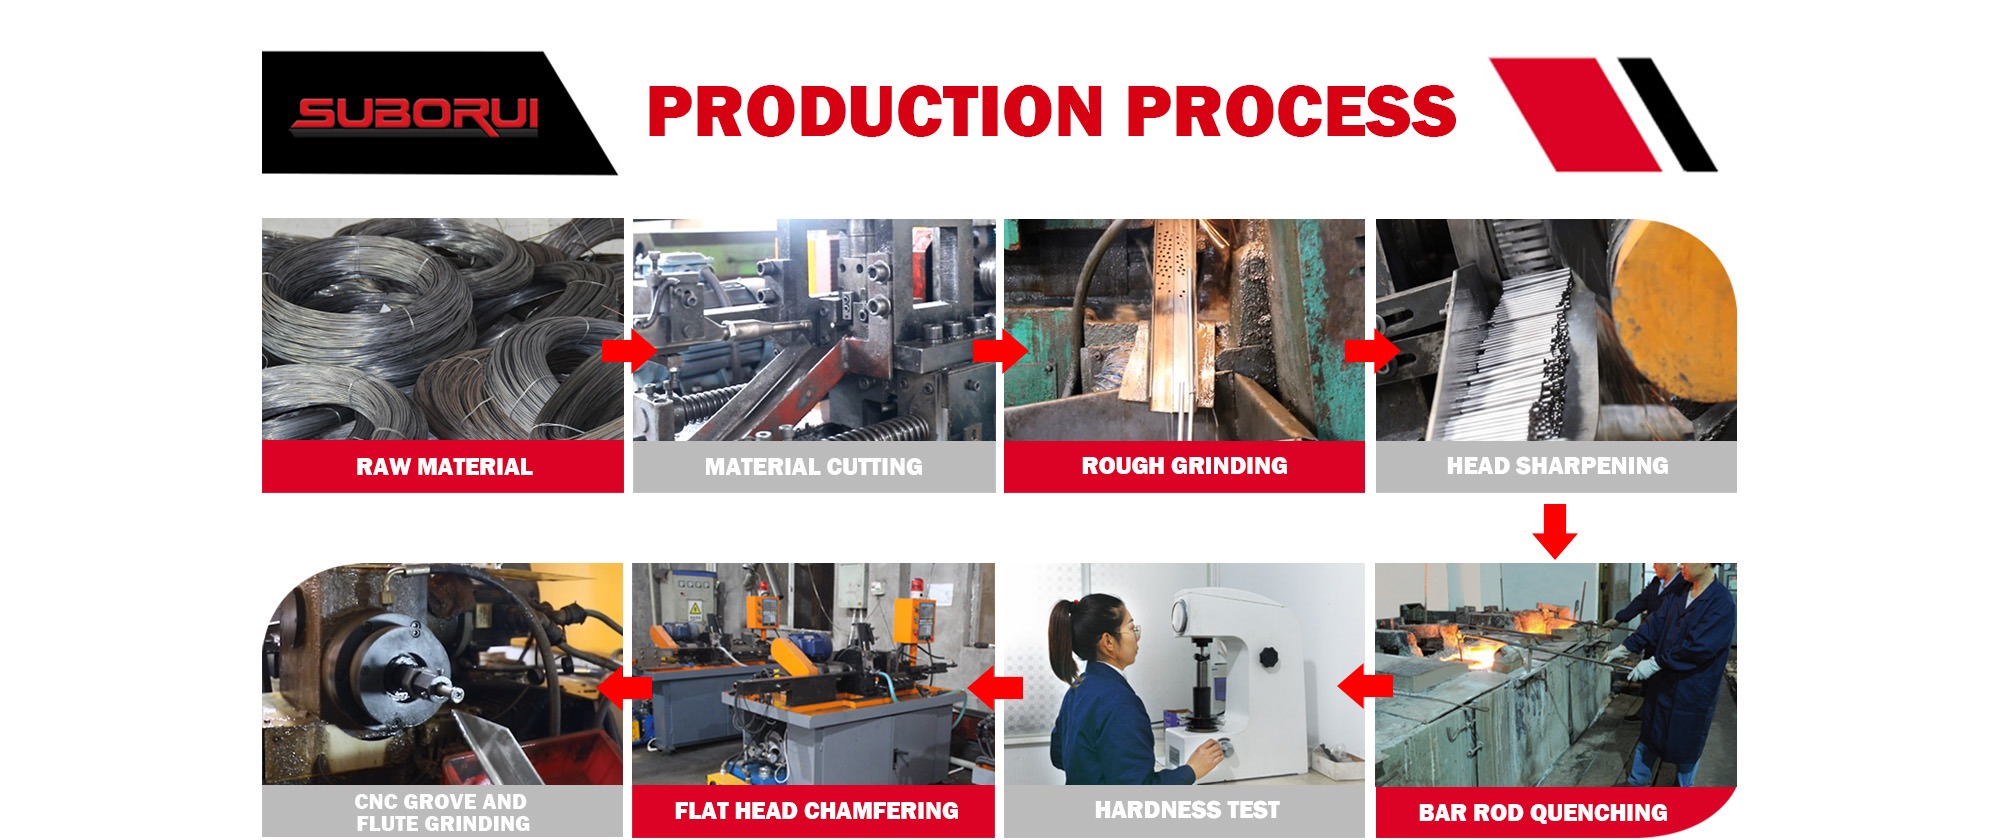
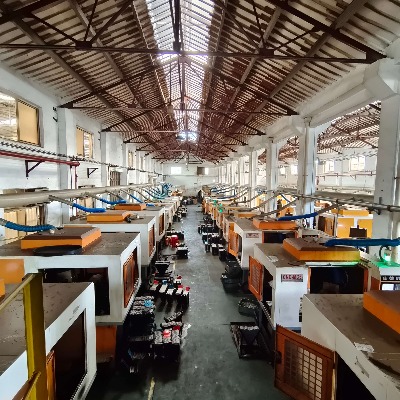
From European-standard cobalt bar stock to micron-level CNC grinding, every spot weld drill bit is tracked through six automated quality gates.
Spectrometer-verified M35, M42 and carbide rods cut to exact blank lengths.
Flute profile and clearance angles roughed on high-speed grinding units.
Microprocessor-controlled salt-bath & vacuum quenching to achieve 65–68 HRC.
Precision 5-axis CNC grinding of the center pilot point and outer scoring lips.
100% camera runout inspection, hardness verification, and destructive coupon tests.
Laser marking, rust-inhibiting coating, blister carding or indexed metal boxes.
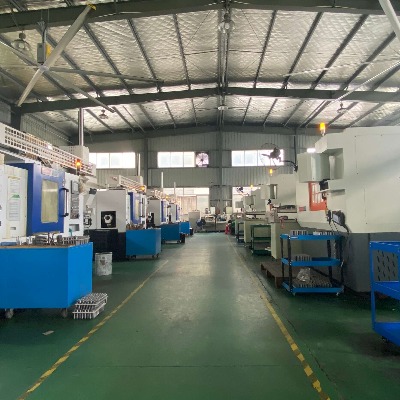
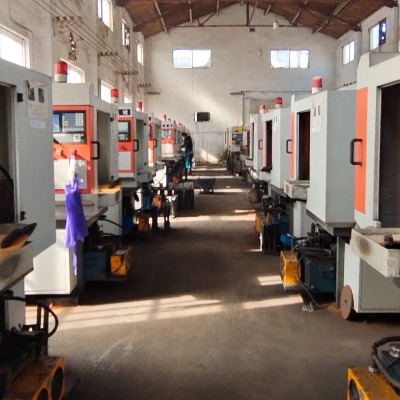
Direct answers to the most frequent technical inquiries evaluated by procurement teams and automotive collision tool buyers.
A standard 118° or 135° twist drill features a conical tip designed to penetrate fully through material. When removing auto body panels, a standard drill immediately punctures the structural panel underneath, compromising frame integrity and requiring extensive corrective welding. A dedicated spot weld drill bit features a flat-bottom crown or spur point with an ultra-short centering spur. This geometry scores and cuts out the outer nugget perimeter while leaving the underlying sheet panel intact.
M35 Cobalt contains 5% cobalt alloy, which provides outstanding red-hardness while retaining critical torsional elasticity. It is the premier, cost-effective choice for handheld pneumatic drills (such as 1000 RPM pistol drills) on mild steel and conventional High-Strength Low-Alloy (HSLA) sheet metal where slight operator angular flex occurs. Solid Carbide is required when cutting Ultra-High-Strength Steels (UHSS), Martensitic steels, and hot-stamped Boron steels (e.g., B-pillars, frame rails). Because carbide is brittle, it must be operated with rigid pneumatic spot-weld drills or automated equipment to avoid lateral shock breakage.
We manufacture three primary shank designs: 1) Cylindrical straight shanks for standard multi-jaw chucks; 2) 3-Flat shanks that prevent spinning inside handheld chucks under high torque; and 3) 8.0 mm (5/16") shanks with precision drive flats designed specifically for dedicated automotive spot weld drill machines like Spitznagel, Dent Fix, and DF-15DX series.
As a direct factory, Jiangsu WRD Tools Co., Ltd. provides comprehensive OEM/ODM options: customized point angles (crown, spur, modified 135°), substrates (M2, M35, M42, Solid Carbide), advanced PVD coatings (TiN, TiCN, TiAlN), shank diameter and length variations, laser logo marking, and private-label retail packaging including custom labeled tubes, EVA foam-lined aluminum cases, and printed blister cards.
Operating speed and pressure control are paramount. Cobalt spot weld bits should run between 800 and 1200 RPM, while Solid Carbide must run at 400 to 700 RPM with continuous, steady pressure. Technicians should never rock or wiggle the drill bit while cutting, as lateral forces break outer spurs. Applying a drop of high-lubricity cutting paste or oil dramatically reduces friction and thermal stress, multiplying bit life up to three times.
Send your drawings, required steel hardness, or custom packaging requirements. Direct factory quotation within 24 hours.
 IrisExport Sales Manager
 AaronExport Sales Manager
 CynthiaExport Sales Manager
 WillieExport Sales Manager
 AbbyExport Sales Manager
 VictorExport Sales Manager