High-Performance Tooling Catalog for Debrecen Fabricators
Precision-ground metalworking, coring, and surface preparation tools engineered for DIN 1835-B clamping systems, automated CNCs, and heavy structural magnetic drills.







Industrial Context: Debrecen's Megaproject Infrastructure and the Surge in Tooling Demands
The industrial landscape of Debrecen, situated in Hungary's Hajdú-Bihar county, is undergoing the most rapid modern industrial transformation in Central and Eastern Europe. Bolstered by massive foreign direct investments (FDI), notably the €2 billion BMW Group iFactory in the Northwest Economic Zone and the landmark €7.34 billion Contemporary Amperex Technology Co. Limited (CATL) 100 GWh lithium-ion battery gigafactory in the Southern Industrial Park (Déli Ipari Park), Debrecen has emerged as an undisputed epicenter of European electric vehicle (EV) manufacturing. Alongside ecosystem anchors such as SEMCORP, EcoPro BM, and Eve Energy, tier-1 automotive suppliers, modular skid fabricators, and structural steel engineers are operating under rigorous throughput deadlines.
In these advanced manufacturing centers, metalworking efficiency hinges upon the structural integrity and precision of mechanical tool-holding assemblies. The Weldon shank annular cutter (DIN 1835-B / DIN 6535-HB) has established itself as the indispensable tooling standard across Debrecen's machine shops and site installation yards. The cylindrical shank with twin drive clamping flats eliminates slip during torsional shock loads, providing zero rotational displacement when coring through micro-alloyed structural steels, structural stainless steels (AISI 304/316L), and structural aluminum battery tray modules.
As legacy magnetic base drilling and gantry milling machinery transition toward multi-axis CNC spindles and high-torque magnetic broaching units, local Hungarian procurement teams face continuous challenges: premature flank wear, peripheral tooth chipping under thermal cycling, and unbudgeted tool downtime. This technical whitepaper analyzes cutting tool metallurgy, shank geometry standards, localized operating parameters, and total cost of ownership (TCO) benchmarks specifically calculated for the industrial requirements of Debrecen's automotive, gigafactory, and structural engineering projects.
Weldon Shank Architecture & Substrate Metallurgies for Continuous Machining
The defining feature of industrial annular cutters and precision end mills engineered for heavy magnetic drills and automated tool-holders is the 3/4" (19.05 mm) or 1-1/4" (31.75 mm) Weldon shank conforming to international standard DIN 1835-B. Unlike round shanks that rely solely on friction or quick-in three-ball detent mechanisms that exhibit radial deflection under peak torques, the Weldon design utilizes precision-ground flats positioned at 90° or 180° offsets. Clamping grub screws seat solidly against the flat plane, locking the tool mechanically along its longitudinal axis and transferring up to 450 Nm of torque without axial drift or spindle slippage.
HSS-M2 (6542) Standard Grade
Standard High-Speed Steel (W6Mo5Cr4V2) offering optimal toughness for structural steels (S235JR, S355J2) common in Debrecen logistics warehouse erection. Retains thermal hardness up to 500°C with an operating hardness of 63–65 HRC.
HSS-Co M35 (5% Cobalt)
Engineered with a 5% Cobalt matrix yielding superior red hardness up to 620°C (65–67 HRC). Essential for repetitive drilling in abrasive austenitic stainless steels (1.4301 / AISI 304) and high-strength chassis components without edge deformation.
TCT (Tungsten Carbide Tipped)
Micro-grain Tungsten Carbide cutting teeth brazed to an alloy steel body with triple-facet geometry (outer, center, and inner blades). Delivers unmatched cycle times in Hardox wear plates, railway rails, and thick battery packaging plate steels up to 50 HRC.
To prevent thermal welding and galling when machining chemically reactive automotive light alloys, Jiangsu WRD Tools applies specialized vacuum cathodic arc PVD coatings to our Weldon shank series. Options range from standard Titanium Nitride (TiN, micro-hardness 2300 HV) for general steel fabrication to high-aluminum Titanium Aluminum Nitride (TiAlN / AlTiN, nano-hardness >3300 HV), which develops an amorphous aluminum oxide self-passivating shield when cutting temperatures exceed 800°C. This allows Debrecen operators to push spindle feeds and engage in minimum quantity lubrication (MQL) or dry-coring environments.
Operating Parameters & Speeds for Debrecen Industrial Materials
The table below provides field-verified parameters calculated to balance material removal rate (MRR) and cutting tool longevity when operating magnetic base drills or CNC machining centers fitted with 19.05 mm Weldon shank annular cutters.
| Workpiece Material Group | Common Hungarian / EN Grade | Recommended Tool Substrate | Cutting Speed (Vc - m/min) | Feed (f - mm/rev) | Optimal Coolant Delivery |
|---|---|---|---|---|---|
| Mild Structural Steel | EN 10025-2 S235JR / S275JR | HSS M2 / Fully Ground | 25 – 35 m/min | 0.08 – 0.12 | Internal Soluble Oil 5–8% |
| High-Tensile Structural Steel | S355J2+N / S460QL | HSS-Co M35 or TCT | 20 – 28 m/min | 0.06 – 0.10 | Internal Emulsion / MQL |
| Austenitic Stainless Steel | 1.4301 (X5CrNi18-10) / 1.4404 | HSS-Co M35 / TiAlN Coated | 12 – 18 m/min | 0.04 – 0.08 | High-Pressure Neat Cutting Oil |
| EV Battery Tray Extrusions | EN AW-6060 / 6082-T6 | HSS-G Polished Flute / Uncoated | 60 – 90 m/min | 0.12 – 0.18 | MQL Synthetic Ester / Air Blast |
| Abrasion-Resistant / Rail Plate | Hardox 400 / EN 13674-1 R260 | TCT Triple-Cut Weldon | 35 – 50 m/min | 0.05 – 0.09 | Internal Flood Coolant |
Note: When using center pilot pins with internal-cooling Weldon toolholders, ensure minimum reservoir pressure of 0.2 bar to maintain hydrodynamic ejection of the central slug and avoid slug weld jamming.
Localized Application Scenarios Across Debrecen's Key Industrial Hubs
Debrecen's rapid expansion has created targeted operational demands where conventional round twist drills fail to meet takt time requirements. Here is how our Weldon shank core drills and associated tooling integrate into Debrecen's flagship industrial centers:
CATL & EV Battery Cluster (Déli Ipari Park)
Precision cleanroom tooling and module casing lines demand burr-free through-holes in aluminum alloy 6000-series battery housings and stainless steel piping skids. Our M35 cobalt and mirror-fluted annular cutters produce exact round holes without leaving radial chatter marks, ensuring airtight seals for sensor brackets and high-voltage wiring penetrations.
BMW iFactory Automotive Tooling & Jigs
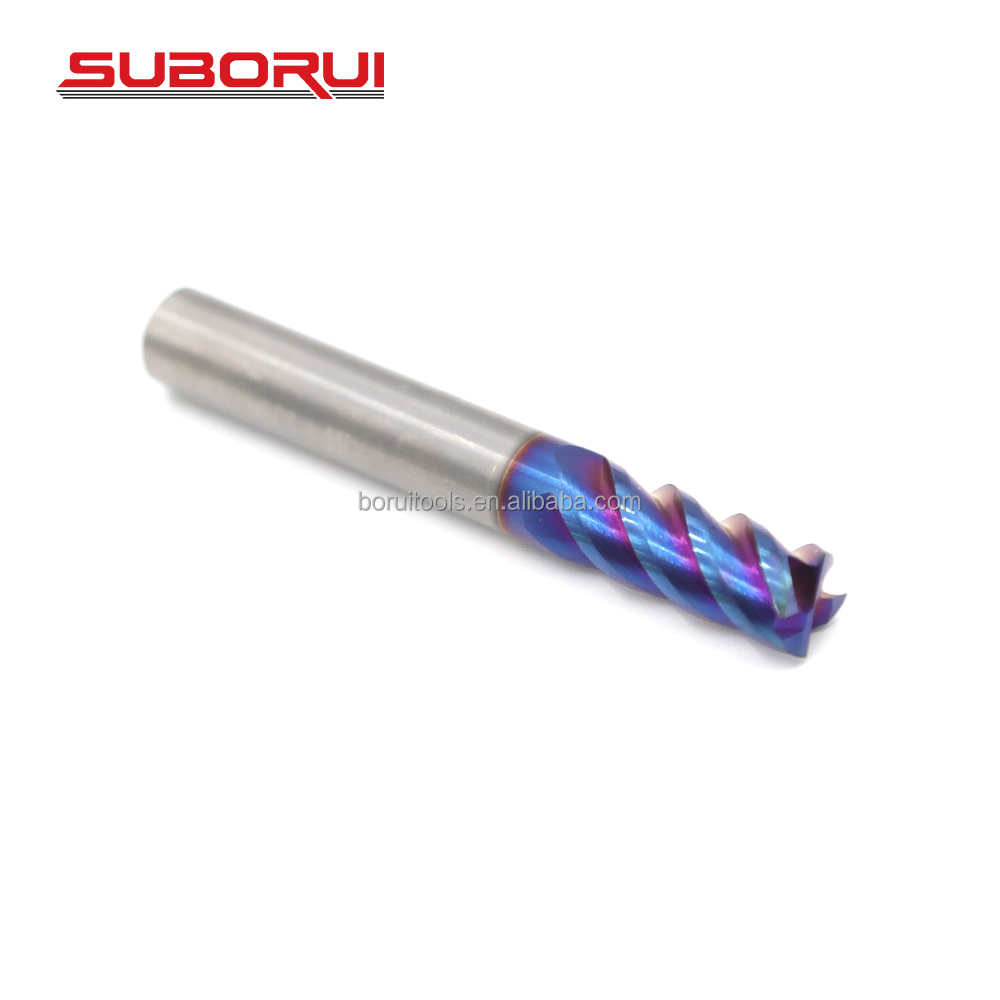
Robotic assembly jigs, subframe fixtures, and welding frames erected within the Északnyugati Gazdasági Övezet demand micro-precision hole alignment. Our fully ground HRC65 solid carbide end mills and 19.05 mm Weldon shank annular cutters allow on-site engineers to bore high-tolerance holes into 20 mm to 50 mm thick machine bases without shipping massive weldments off-site.
Railway Logistics & Structural Infrastructure
Upgrades to the Debrecen-Füzesabony rail corridor and intermodal freight terminals require coring through UIC 60 and R260 hardened steel rails. Our TCT Weldon rail cutters utilize tungsten carbide teeth with specialized shear angles to penetrate work-hardened rail webs in under 35 seconds, eliminating micro-fissures that cause rail fatigue fractures.
Long-Term Sourcing Trends in Eastern Hungary’s Advanced Machining Sector
As Debrecen accelerates toward its goal of becoming an internationally recognized automotive and battery cluster, tooling consumption habits are shifting markedly from reactive, ad-hoc procurement to predictive supply chain integration:
1. Shift Toward Total Cost per Hole (TCPH) Over Initial Purchase Price: Local procurement managers at tier-1 and tier-2 facilities increasingly evaluate consumables by cost-per-hole metrics rather than unit list prices. While a standard budget cutter may drill 25 holes in structural S355 steel before requiring regrinding, an advanced M35 cobalt fully-ground Weldon cutter consistently yields 120+ holes under identical feed rates. When factoring machine downtime and operator changeout times in Hungary's tightening labor market, premium substrates reduce total operational costs by up to 38%.
2. Standardization of Weldon Shanks across CNC and Magnetic Drill Fleets: Machine shops across Hajdú-Bihar county are phasing out mixed Morse Taper and proprietary toolholder variants in favor of standardized 19.05 mm Weldon drive arbors. With readily available adapter sleeves (BT40-Weldon, SK40-Weldon, and Quick-In-to-Weldon), a single inventory of annular cutters can be deployed interchangeably across field magnetic drills, radial arm drill presses, and high-speed vertical machining centers (VMCs).
3. Tightened Scrap and Reaming Tolerances: In EV battery module assembly, minor burrs can compromise battery pouch insulation, risking severe thermal events. Modern contracts in Debrecen specify high-tolerance hole drilling with minimal entry/exit burrs, driving demand for multi-facet cutting tooth geometry that produces thin, curling swarf that ejects smoothly without scoring hole sidewalls.
Frequently Asked Questions: B2B Tooling Procurement for Debrecen
What is the standard shank configuration for magnetic drills in Hungary?
The 3/4" (19.05 mm) Weldon shank with two flat locking surfaces at 90° or 180° is the dominant configuration across Hungary and the European Union. It natively fits magnetic drilling machines manufactured by Euroboor, BDS, Fein, Alfra, and Rotabroach. For machines equipped with Fein Quick-In tool-free spindles, standard Weldon-to-Quick-In adapters are commonly utilized to maintain unified tooling cross-compatibility.
How do Hungarian customs and EU import compliance work for our tool orders?
All precision cutting tools, drill bits, and annular cutters shipped to Hungary are classified under EU Harmonized System (HS) code 8207.50 (tools for drilling, other than rock drilling). Jiangsu WRD Tools prepares complete documentation packages including commercial invoices, packing lists, CE compliance certificates, and Certificates of Origin (CO). Shipments cleared through Budapest Liszt Ferenc International Airport (BUD) or Port of Koper/Hamburg arrive smoothly at Debrecen warehouses via regular road freight.
When should a Debrecen machine shop choose HSS-Co M35 over TCT cutters?
HSS-Co M35 (5% Cobalt) cutters are resilient against dynamic shock loads and vibration, making them ideal for mobile on-site construction, hand-held magnetic base drilling on uneven structural beams, and overlapping hole modifications where tungsten carbide teeth might chip under intermittent cutting forces. TCT cutters are preferred for stationary shop drilling, structural plate thicknesses exceeding 35 mm, stainless steels, and high-volume production where spindle stability is rigidly maintained.
What are the minimum order quantities (MOQ) and lead times for OEM orders?
Standard catalog sizes (diameters 12 mm to 65 mm in 25 mm, 30 mm, and 50 mm depths) maintain an MOQ starting at just 10 pieces for trial sampling, while custom metric diameters, stepped geometries, or proprietary pilot bores start at 50 to 100 units. Production turnaround averages 15 to 25 business days, with air courier delivery to Debrecen in 4 to 6 days or sea freight container consolidation via Northern Adriatic ports in approximately 28 to 32 days.