Factory-Direct Core Cutting & Machining Solutions
Precision-matched tooling portfolio manufactured to EN 13236 and DIN engineering standards, serving high-demand civil works, granite fabrication, and renovation sites across Prague and Central Bohemia.



Engineering Matrix: Turbo Diamond Blade Mechanics
A technical evaluation of diamond grit encapsulation, bond metallurgical sintering, and cooling channel thermodynamics designed for high-tensile mineral cutting across the Czech Republic.
Sintered Wave Turbo Geometry
Unlike standard continuous rim discs, the corrugated turbo profile introduces serrated lateral flutes that actively expel pulverized stone dust. This continuous aerodynamic evacuation cycle prevents thermal loading, reducing core deflection during high-RPM cuts on angle grinders and masonry wall chasers.
By engineering specific clearance angles on the segment flanks, our turbo blades minimize friction drag against the kerf sidewalls, preserving peripheral rotational momentum on 230mm handheld cutters commonly utilized on Prague reconstruction jobsites.
Cobalt-Bronze Matrix Bond
The blade segment longevity hinges entirely on the metallurgical matching between the matrix bond and the aggregate abrasiveness. For Central European geology, our automated hot-press sintering lines blend sub-micron cobalt powders with pre-alloyed bronze and nickel.
This composition controls micro-fracturing of the synthetic diamond crystals (mesh 40/50 to 50/60 with Ti-coating), ensuring that dull diamonds shed precisely as fresh cutting facets emerge, preventing glazing when encountering dense Bohemian basalt or rebar-reinforced C35/45 slabs.
70Mn2 Core Tensioning
A turbo diamond blade is only as reliable as its steel core. We manufacture our blanks from heat-treated 70Mn2 and 65Mn cold-rolled carbon spring steel, precision punched and laser-slotted with expansion keyholes.
Each blank undergoes roll-tensioning and dynamic balancing to maintain radial runout below 0.03mm. This eliminates vibrational chattering at 6,600 to 12,200 RPM, delivering surgical kerf stability, edge chip resistance, and operator protection in compliance with European EN 13236 regulations.
Prague Market Applications & Localized Substrates
From UNESCO heritage facades along the Vltava river to suburban infrastructural expansions, diamond tooling in Prague requires hyper-specialized cutting properties.
Historic Sandstone & Masonry Restoration
Prague's historic core (Staré Město, Malá Strana) features predominantly Hořice sandstone (*hořický pískovec*), lime mortar, and dense historic ceramic *bobrovka* clay tiles. Cutting these abrasive natural stones causes premature core erosion on poorly bonded tools.
Our hard-bond continuous and slotted turbo configurations withstand the abrasive slurry generated by Czech sandstone restoration, ensuring ultra-clean edges without micro-fracturing delicate historic architectural blocks.
Pre-Stressed Heavy Concrete: Metro D & Ring Road
Major infrastructure projects such as the Prague Metro Line D (Trasa D), Nová Zbrojovka, and inner city rail corridors deploy pre-stressed concrete mixed with river gravel aggregate (Labe river silica gravel) and high steel rebar concentration (grade C30/37 to C50/60).
We supply laser-welded turbo segment blades engineered with an aggressive multi-layer diamond array that slices clean through 16mm-32mm tensile rebar without blade de-segmentation or core binding.
Bohemian Granite & Hard Paving Blocks
Prague sidewalk mosaics (*pražská mozaika*) and pedestrian plazas heavily utilize Bohemian crystalline granite (Mrákotín and Liberec granites) alongside porphyry pavers. These minerals exhibit extreme hardness ratings of 6 to 7 on the Mohs scale.
Our medium-soft cobalt matrix turbo blades deliver high penetration rates without blade glazing, enabling municipal pavers and stonemasons to complete accurate radius mitering and pathway curb adjustments quickly on-site.
Technical Specifications: Prague Regional Product Matrix
Direct OEM parameters for industrial supply houses, hardware wholesale distributors, and commercial contractors.
| Blade Outer Dia. (mm / in) | Bore Diameter (Hole) | Segment Height / Kerf | Target Substrate / Application | Compatible Equipment | Czech Industrial Standard |
|---|---|---|---|---|---|
| 115 mm / 4.5" | 22.23 mm (7/8") | 10 mm / 1.2 mm | Gres Porcelain, Ceramic Tiles, Thin Granite | Compact Cordless Angle Grinders | ČSN EN 13236 Class A |
| 125 mm / 5.0" | 22.23 mm (7/8") | 10 mm / 1.4 mm | Wall Chasing, Conduit Grooving, Sandstone | Dust-Shroud Wall Chasers, Grinders | ČSN EN 13236 Class A |
| 150 mm / 6.0" | 22.23 mm (M14) | 12 mm / 1.8 mm | Electrician Chasing, Ductile Iron, Hard Brick | Heavy Handheld Slotting Saws | ČSN EN 13236 Industrial |
| 230 mm / 9.0" | 22.23 mm / 25.4 mm | 12 mm / 2.4 mm | Reinforced Concrete, Curbstones, Clinker Brick | 230mm Electric Grinders, Cut-off Saws | ČSN EN 13236 Heavy-Duty |
| 350 mm / 14.0" | 20.0 mm / 25.4 mm | 12 mm / 3.2 mm | Road Asphalt, Structural Slab, Rebar C45 | Stihl/Husqvarna Petrol Cutters, Floor Saws | ČSN EN 13236 High Safety |
Prague Market Trends: Safety, Dust Suppression & Cordless Growth
Anticipating operational and regulatory shifts in the Czech power tool accessory and abrasive markets.
Stringent Crystalline Silica Dust Controls
In accordance with Czech Government Regulation No. 361/2007 Coll. (health protection conditions at work) aligning with EU occupational exposure limits for respirable crystalline silica (RCS), Prague job sites are cracking down on dry masonry cutting.
Demand has surged for continuous wave mesh turbo blades capable of operating with integrated water mist cooling systems or pairing cleanly with negative-pressure vacuum shrouds without clogging slurry along the rim channels.
Optimization for High-Output Cordless Systems
Professional contractors across Prague's commercial building sector are systematically switching to 18V and 54V battery platforms (Milwaukee M18 FUEL, DeWalt FlexVolt, Makita XGT). These tools require ultra-thin kerf turbo blades.
By engineering our 115mm and 125mm blade cores down to 1.2mm thickness while maintaining rigorous 70Mn2 tension, we reduce material removal resistance by over 30%, noticeably extending battery run-times per charge on structural cutting tasks.
Consolidation of Central European Logistics
Prague acts as the prime logistics conduit for Central and Eastern Europe (CEE). Importers and regional tool brands based in Prague-Východ or Horní Počernice warehouse parks demand reliable consolidated containers combining twist drills, hole saws, and diamond blades.
Jiangsu WRD Tools bridges this requirement by manufacturing the entire drilling, hole-making, and diamond saw blade spectrum under unified ISO-managed quality gates, allowing combined OEM shipping directly to Hamburg or Koper ports.
Direct Factory Manufacturing Heritage Since 2007
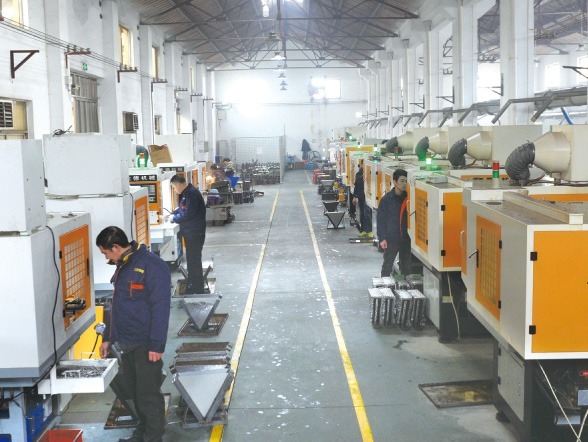
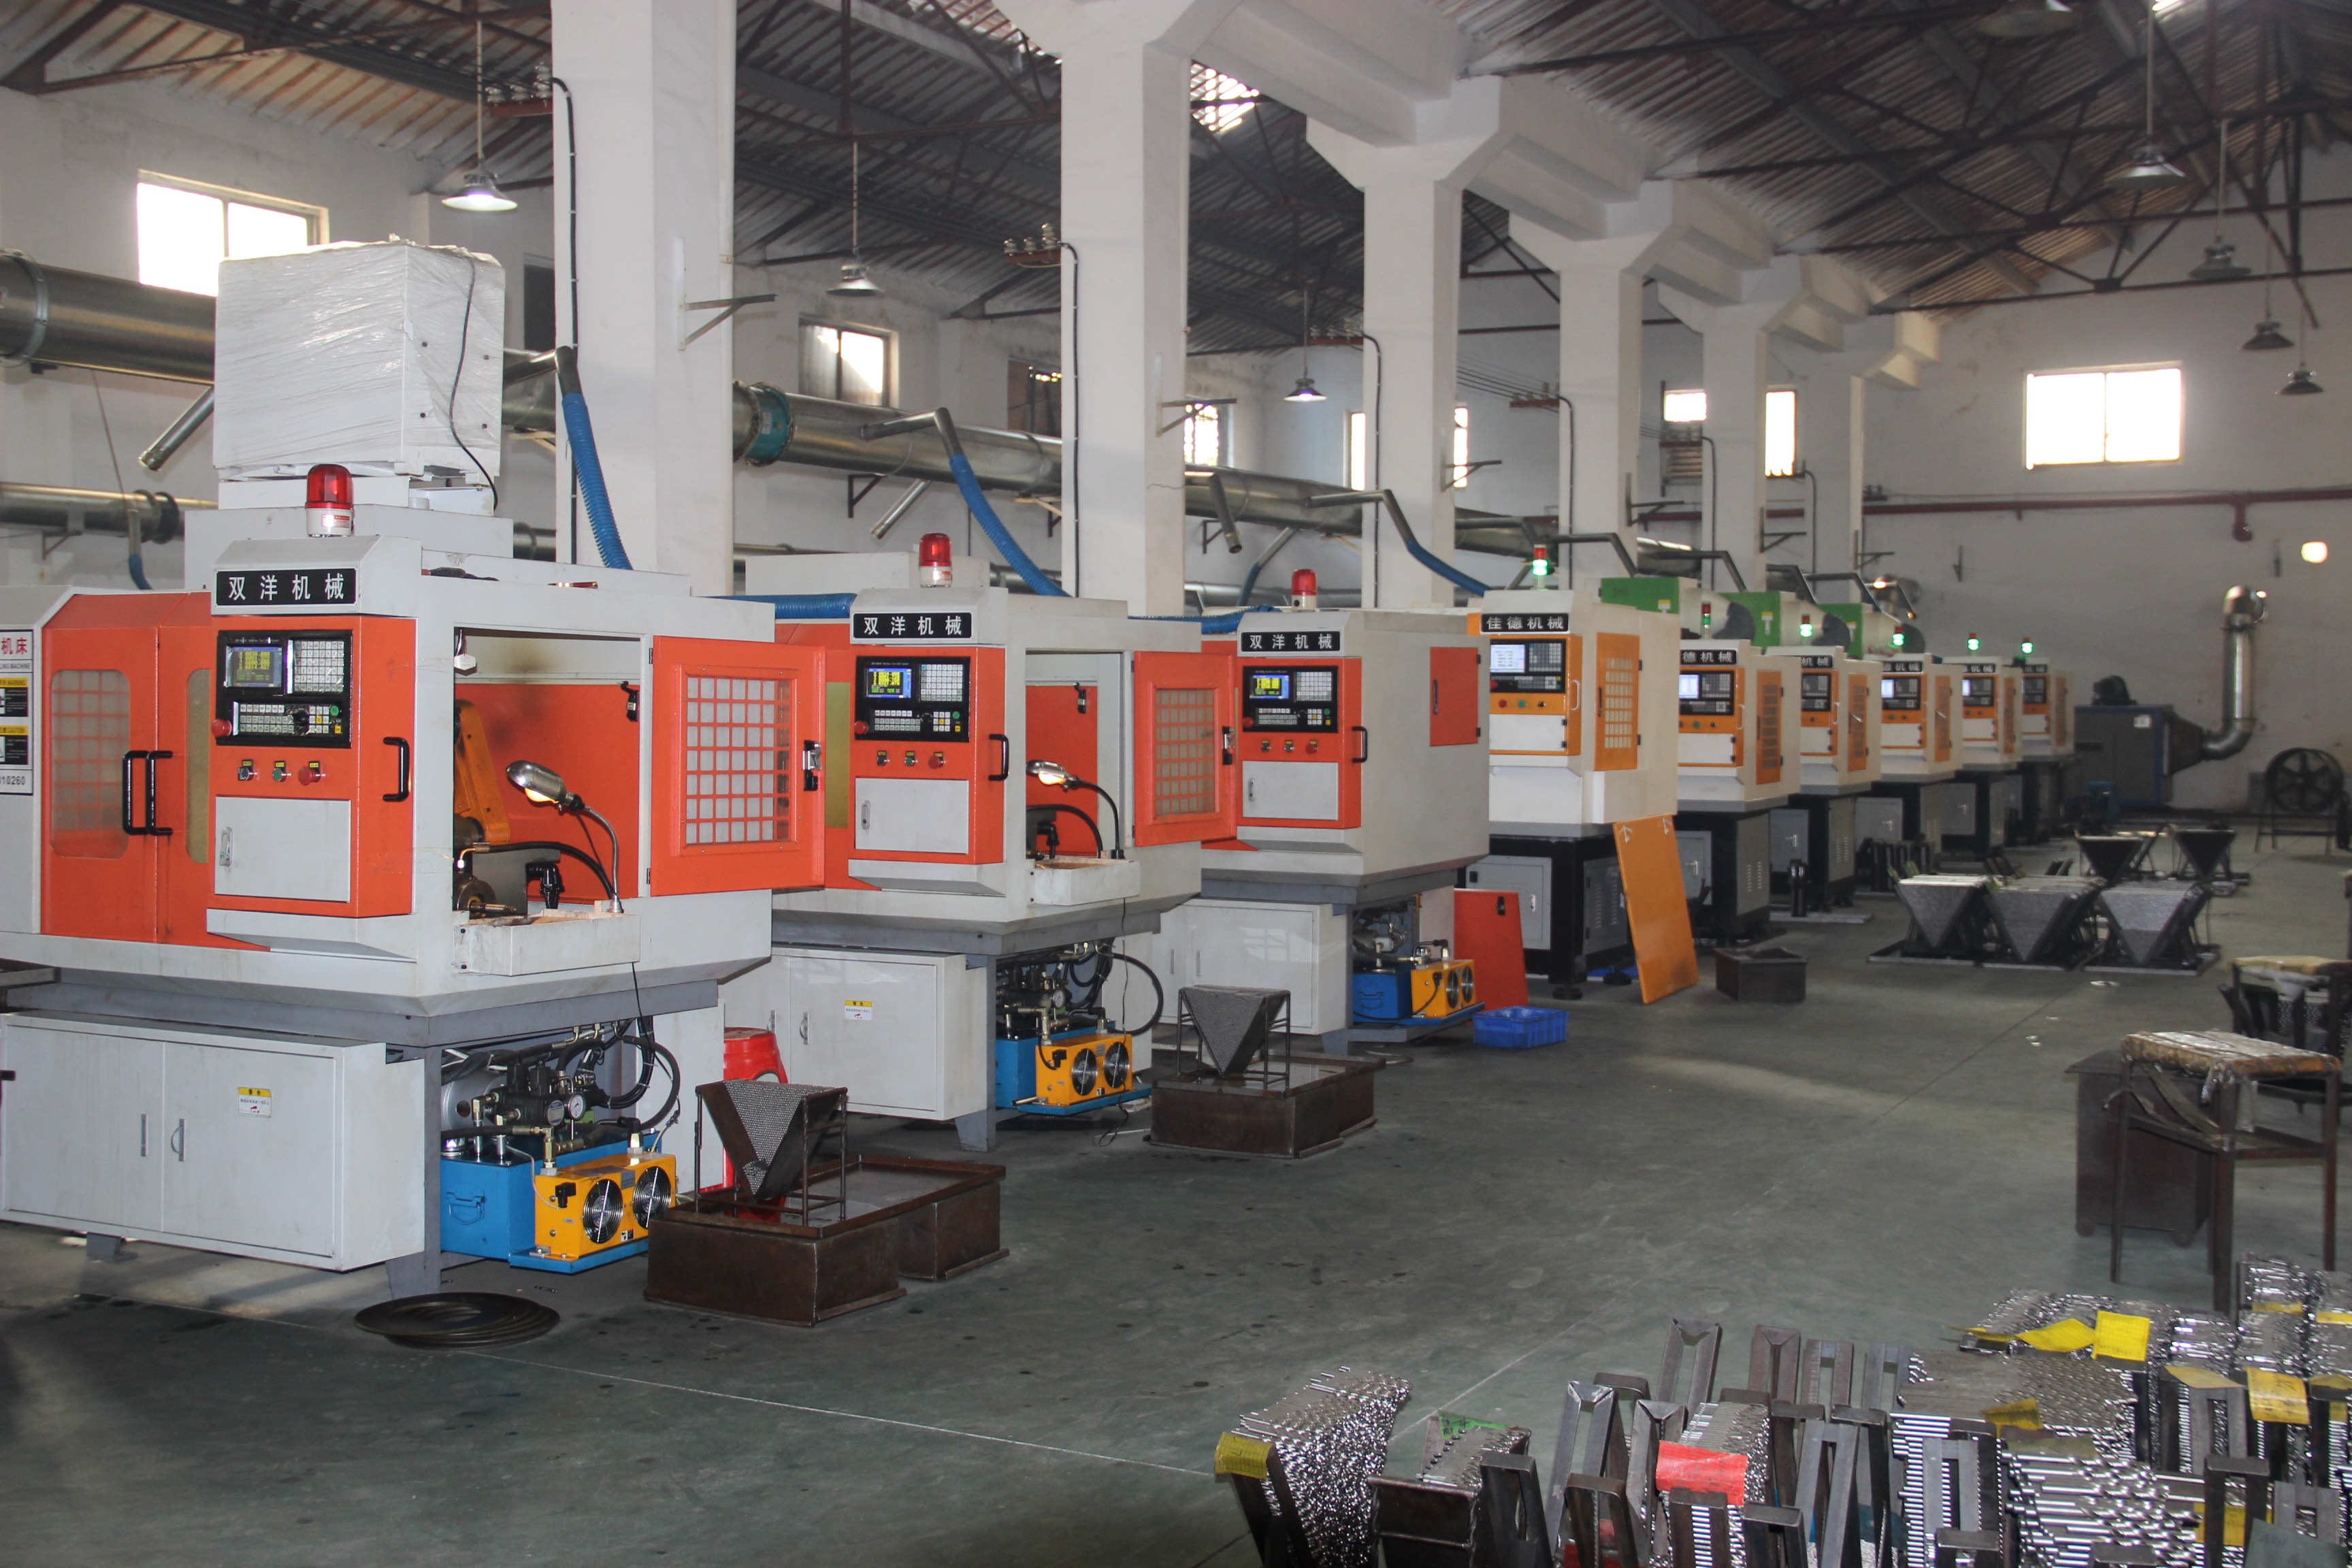
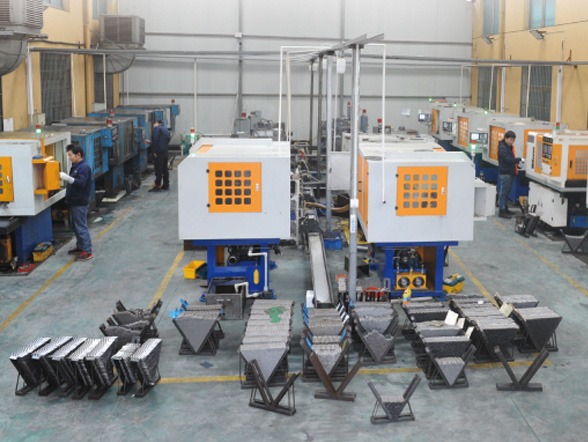
Established in Danbei Town, Danyang, Jiangsu — China’s foremost hardware tool manufacturing cluster — Jiangsu WRD Tools Co., Ltd. operates a high-capacity 12,000 m² production facility backed by RMB 10 million in registered capital and over 150 dedicated technicians.
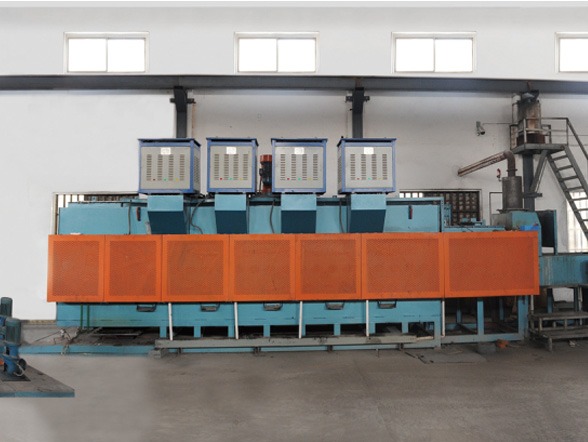
We are a certified Jiangsu High-Tech Enterprise and onsite verified by Intertek Group. Our fully controlled internal workflow encompasses CNC core cutting, vacuum furnace hardening, precision diamond segment pressing, dynamic laser balancing, and robotic testing.
- Tier-1 OEM Manufacturing Experience: We have proudly manufactured and supplied precision cutting tools to global brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Wolfcraft, and Heller.
- Massive Annual Throughput: Over 90 million drill bits, 50 million wood bits, and high-volume diamond blades and cup wheels produced annually.
- Turnkey OEM & Private Label Branding: Laser marking on core steel, custom segment coloring, localized barcode packaging, and blister card design tailored for European retail compliance.
Frequently Asked Questions: Prague B2B Procurement
Direct answers covering trade logistics, certifications, minimum order quantities, and custom segment formulas.
What European safety standards do your turbo diamond blades comply with for Czech import?
All diamond blades exported to the European Union and Czech Republic strictly adhere to ČSN EN 13236 (Safety requirements for superabrasive products). Every production lot undergoes rigorous bursting speed tests up to 1.6 times the rated maximum RPM, segment shear-strength tests, and dynamic radial runout audits. Our factory is also onsite-verified by Intertek Group, guaranteeing transparent quality and corporate compliance for Czech customs clearance.
Can we customize segment formulations specifically for abrasive Czech Hořice sandstone or hard Bohemian granite?
Yes. We engineer customized powder metallurgical bonds. For abrasive sandstone applications, we deploy hard matrix bonds composed of tungsten carbide and dense cobalt alloys that resist abrasive undercut wash. For extremely hard quartzites and Bohemian granites, we supply free-cutting soft bronze-cobalt bonds embedded with premium titanium-coated synthetic diamonds to avoid blade glazing.
What are the minimum order quantities (MOQ) and lead times for OEM private-label blades delivered to Prague?
For standard dimensions (115mm, 125mm, 230mm) with custom laser engraving and private brand labeling, our minimum order quantity starts from 200 to 500 pieces per specification. Custom-printed retail display boxes or blister packaging configurations typically require 1,000 units. Standard production lead times run between 25 to 35 days from technical drawing confirmation, with ocean freight booking available to Hamburg or Koper ports.
How do you ensure structural stability and operator safety on high-RPM cordless angle grinders?
We utilize precision laser-cut cores stamped from high-grade 70Mn2 and 65Mn spring steel that receive uniform salt-bath or vacuum heat treatment to achieve optimal tensile temper (42–45 HRC). Laser keyholes and expansion gullets are incorporated to absorb thermal expansion stresses, preventing core warping. Automated double-disc tension grinding ensures that axial runout remains strictly under 0.03mm, completely eliminating chattering at speeds exceeding 11,000 RPM.
Can Czech procurement teams consolidate diamond blades with drill bits, annular cutters, and hole saws in a single order?
Absolutely. As an integrated 12,000 m² manufacturer with distinct workshops for HSS twist drill bits, wood drill bits, hole saws, annular cutters, and diamond abrasive tools, we offer one-stop container consolidation. This dramatically reduces shipping, import handling, and customs declaration expenses for distributors and wholesalers located throughout Prague, Brno, and Ostrava.