Engineered Tooling Showcase
Precision Cutting & Drilling Solutions for Demanding Industries
Explore our export-grade cutting, drilling, and tapping tools built for high torsional strength and abrasive resistance in sub-zero and corrosive operational environments.



2007
Founded Year
12,000m²
Manufacturing Area
150+
Skilled Craftsmen
90M
Annual Bits Output
20+
Export Markets
4.7 / 5
Global Verified Rating
Reykjavik Engineering Context
Localized Applications of Spiral Flute Machine Taps in Iceland
The industrial landscape in Reykjavik and the wider Faxaflói Bay demands exceptional machining performance. Our spiral flute taps are designed specifically for blind-hole internal threading in highly alloyed, work-hardening, and corrosion-resistant metals common across Icelandic maritime and green tech infrastructure.
Geothermal Energy Turbines & Heat Exchangers
Reykjavik Energy (Orkuveitan) and surrounding power installations in Hellisheiði rely heavily on austenitic stainless steels (AISI 316L, 254 SMO) and nickel alloys to resist hydrogen sulfide and high-enthalpy volcanic steam. Our M35 Cobalt (HSS-E) and TiAlN-coated 45° spiral flute machine taps efficiently evacuate stringy chips backwards out of deep blind holes, preventing chip packing, tap binding, and costly thread stripping.
Maritime Trawlers & Fish Processing Automation
Reykjavik Harbour hosts high-tech demersal trawlers and ultra-modern automated fish filleting assembly lines (such as Marel equipment). Fast maintenance cycles require threading in duplex steels and food-grade stainless. The modified spiral flute design generates a smooth continuous shearing cut, drastically lowering cutting torque and preserving thread integrity even when tapping during dockside dry-dock repairs.
Green Hydrogen, Direct Air Capture & Aluminium Smelting
From the Carbfix CO2 mineralization plants to the aluminium smelters around Grundartangi, high amperage busbars and pressure casings require non-magnetic, heat-resistant fastenings. Our machine taps feature specialized rake angles and back taper geometry that accommodate the spring-back and thermal elasticity of titanium alloys and structural aluminum alloys (6082-T6, 7075).
Metallurgical Excellence
Engineering Specifications for Spiral Flute Machine Taps
A side-by-side technical evaluation designed for Icelandic chief metallurgists and CNC machine center operators seeking precision thread classes (6H/ISO2) and enhanced tool lifecycle.
| Substrate Material | Surface Coating | Helix Angle | Target Workpiece Alloys | Reykjavik Industry Focus |
|---|---|---|---|---|
| HSS-M2 (6542) | Steam Oxide (Black) | 35° Right-Hand Spiral | Carbon steel, low alloy steels, brass, structural cast iron (< 750 N/mm²) | General fabrication, municipal infrastructure, vehicle frame modification |
| HSS-E / M35 (Co 5%) | TiN (Titanium Nitride) Gold | 40° – 45° Helical Flute | AISI 304, 316, 316L, 321, martensitic stainless steels (< 950 N/mm²) | Fishery machinery, offshore deck hydraulics, commercial HVAC geothermal loops |
| HSS-E Cobalt + TiAlN | Titanium Aluminium Nitride | 45° High Helix | Super austenitic, 2205 Duplex, Inconel 625, Hastelloy, Titanium Gr. 2 & 5 | Geothermal borehole heads, deep-sea exploration subs, carbon capture scrubbers |
| PM-HSS (Powder Metal) | AlCrN (Alcrona Pro) | 48° Micro-grain Helix | Hardened tool steels (up to 42 HRC), nickel-chromium heat-resistant steels | Precision CNC job shops, high-speed automated production, aluminium extrusions |
Future Macro Trends
Industrial Trends Shaping Cutting Tool Procurement in Iceland
Understanding the transition toward automation, sustainable metallurgy, and strategic supply buffer management across the North Atlantic market.
Electrification of Coastal Fleets & Transport
Iceland's ambitious 2040 carbon-neutral mandate is accelerating the conversion of diesel trawlers and domestic vessels to hybrid-electric and ammonia powertrains. This shift requires immense volumes of non-ferrous and composite tapping solutions where high spiral-flute taps prevent chip galling and maintain high torque transfer across cryogenic and battery-tray assemblies.
Geothermal Supercritical Drilling Tooling
As the Iceland Deep Drilling Project (IDDP) taps into supercritical fluids exceeding 400°C, auxiliary support hardware demands tighter tolerances. Standard straight-flute taps fail prematurely due to high-temperature work hardening. High-helix spiral flute taps fabricated with cobalt-rich matrices ensure uniform load distribution across every active cutting tooth.
Supply Chain Resiliency & Direct Factory OEM
With shipping routes susceptible to North Atlantic weather patterns, hardware merchants and technical supply firms in Hafnarfjörður and Kópavogur are moving away from European middle-tier traders. Direct partnerships with source manufacturers in Danyang allow Icelandic distributors to secure lower unit costs, custom blister packaging, and reliable scheduled sea-air freight.
Jiangsu WRD Tools Co., Ltd.
Integrated Factory Authority: 19 Years of Precision
Established in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. operates a state-of-the-art 12,000 m² production facility in Danyang, Jiangsu — China's world-renowned cutting-tool industrial cluster. We are an Intertek onsite-verified manufacturer recognized as a High-Tech Enterprise of Jiangsu Province.
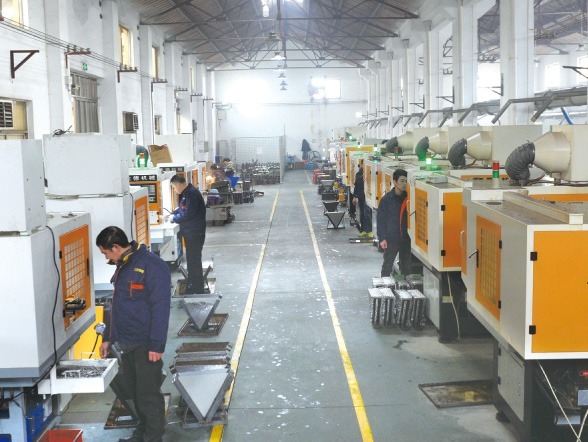
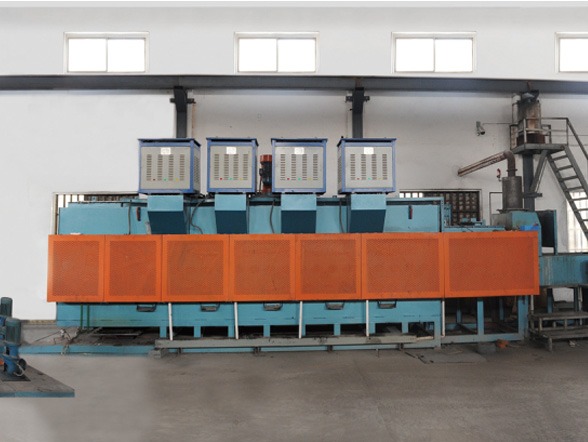
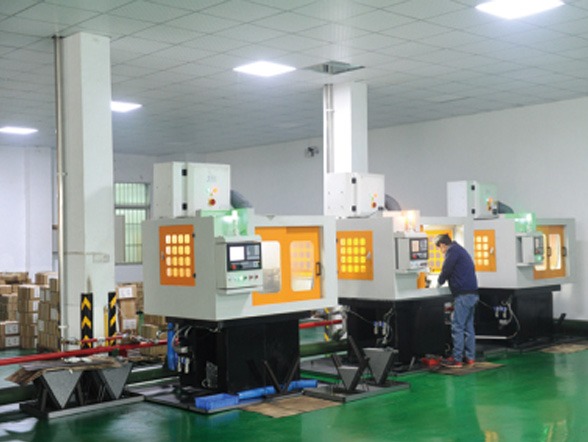
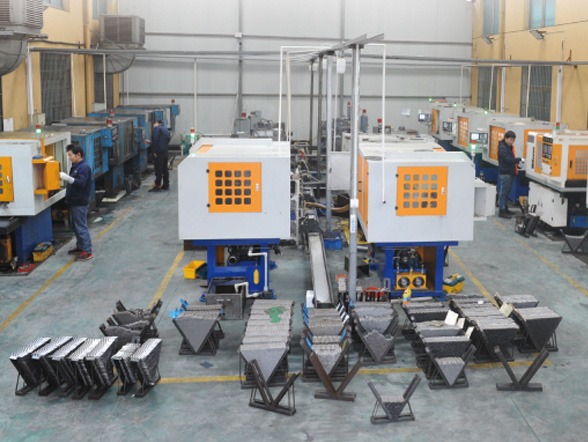
We manage complete in-house production: raw material bar cutting, computer-controlled vacuum salt-bath hardening, 5-axis CNC flute grinding, physical vapor deposition (PVD) coating, and automated laser marking. Our annual capacity surpasses 90 million units, proudly serving international power tool leaders including BOSCH, Milwaukee, DeWalt, Makita, Irwin, and Heller.
 Intertek Verified Production Lines & QA Capability
Procurement Intelligence
Frequently Asked Questions by Reykjavik Buyers
Direct technical and logistical clarity addressing standard DIN standards, minimum quantities, customs clearance, and environmental tolerances.
Why are spiral flute taps preferred over spiral point taps in geothermal maintenance?
Spiral point (gun) taps push chips forward through the hole, making them ideal solely for through-holes. In geothermal valves, turbine housings, and manifold blocks, blind holes dominate. Spiral flute taps feature helical flutes (typically 35° to 45°) that draw chips upward and out of the tapped bore, eliminating chip compaction at the bottom of the hole and preventing sudden tap breakage.
What DIN standards are available for Icelandic and European machine tooling?
We manufacture strictly to DIN 371 (reinforced shanks for smaller diameters M2–M10) and DIN 376 (reduced neck shanks for deeper reach and larger diameters M12–M36). Hand taps conform to DIN 352, and we support ISO metric coarse (M), metric fine (MF), British Standard Pipe (BSP/G), and American NPT thread geometries.
What is the standard MOQ and delivery timeline for shipments to Reykjavik?
For standard metric taps and drill bits, our minimum order quantity starts from 100 to 500 pieces per size, while complete boxed sets start at 100 sets. Custom OEM branding with private-label blister packaging has an MOQ of 1,200 sets. Sea-air freight to Reykjavik (via Rotterdam or direct air cargo to Keflavík) typically requires 7 to 12 working days for air transit.
How does WRD Tools prevent micro-welding when tapping 316L and duplex stainless?
We address the work-hardening and gummy characteristics of austenitic alloys by pairing 5% cobalt matrices (M35) with physical vapor deposition (PVD) titanium aluminium nitride (TiAlN) or carbon-nitride (TiCN) coatings. These coatings maintain chemical inertness up to 800°C, drastically lowering the friction coefficient and preventing galling and edge micro-welding.
Upgrade Your Threading Performance in Iceland
Connect with our senior technical engineering team for bulk wholesale pricing, custom tool drawings, and comprehensive test certificates verified by Intertek.
Get Catalog