Featured Industrial Cutters & Tooling Systems
Direct OEM factory manufacturing covering CNC internal threading, holemaking, and surface conditioning for demanding metalworking environments.

SUBORUI Double Row Segments Diamond Grinding Disc Cup Wheel for Concrete Masonry Stone
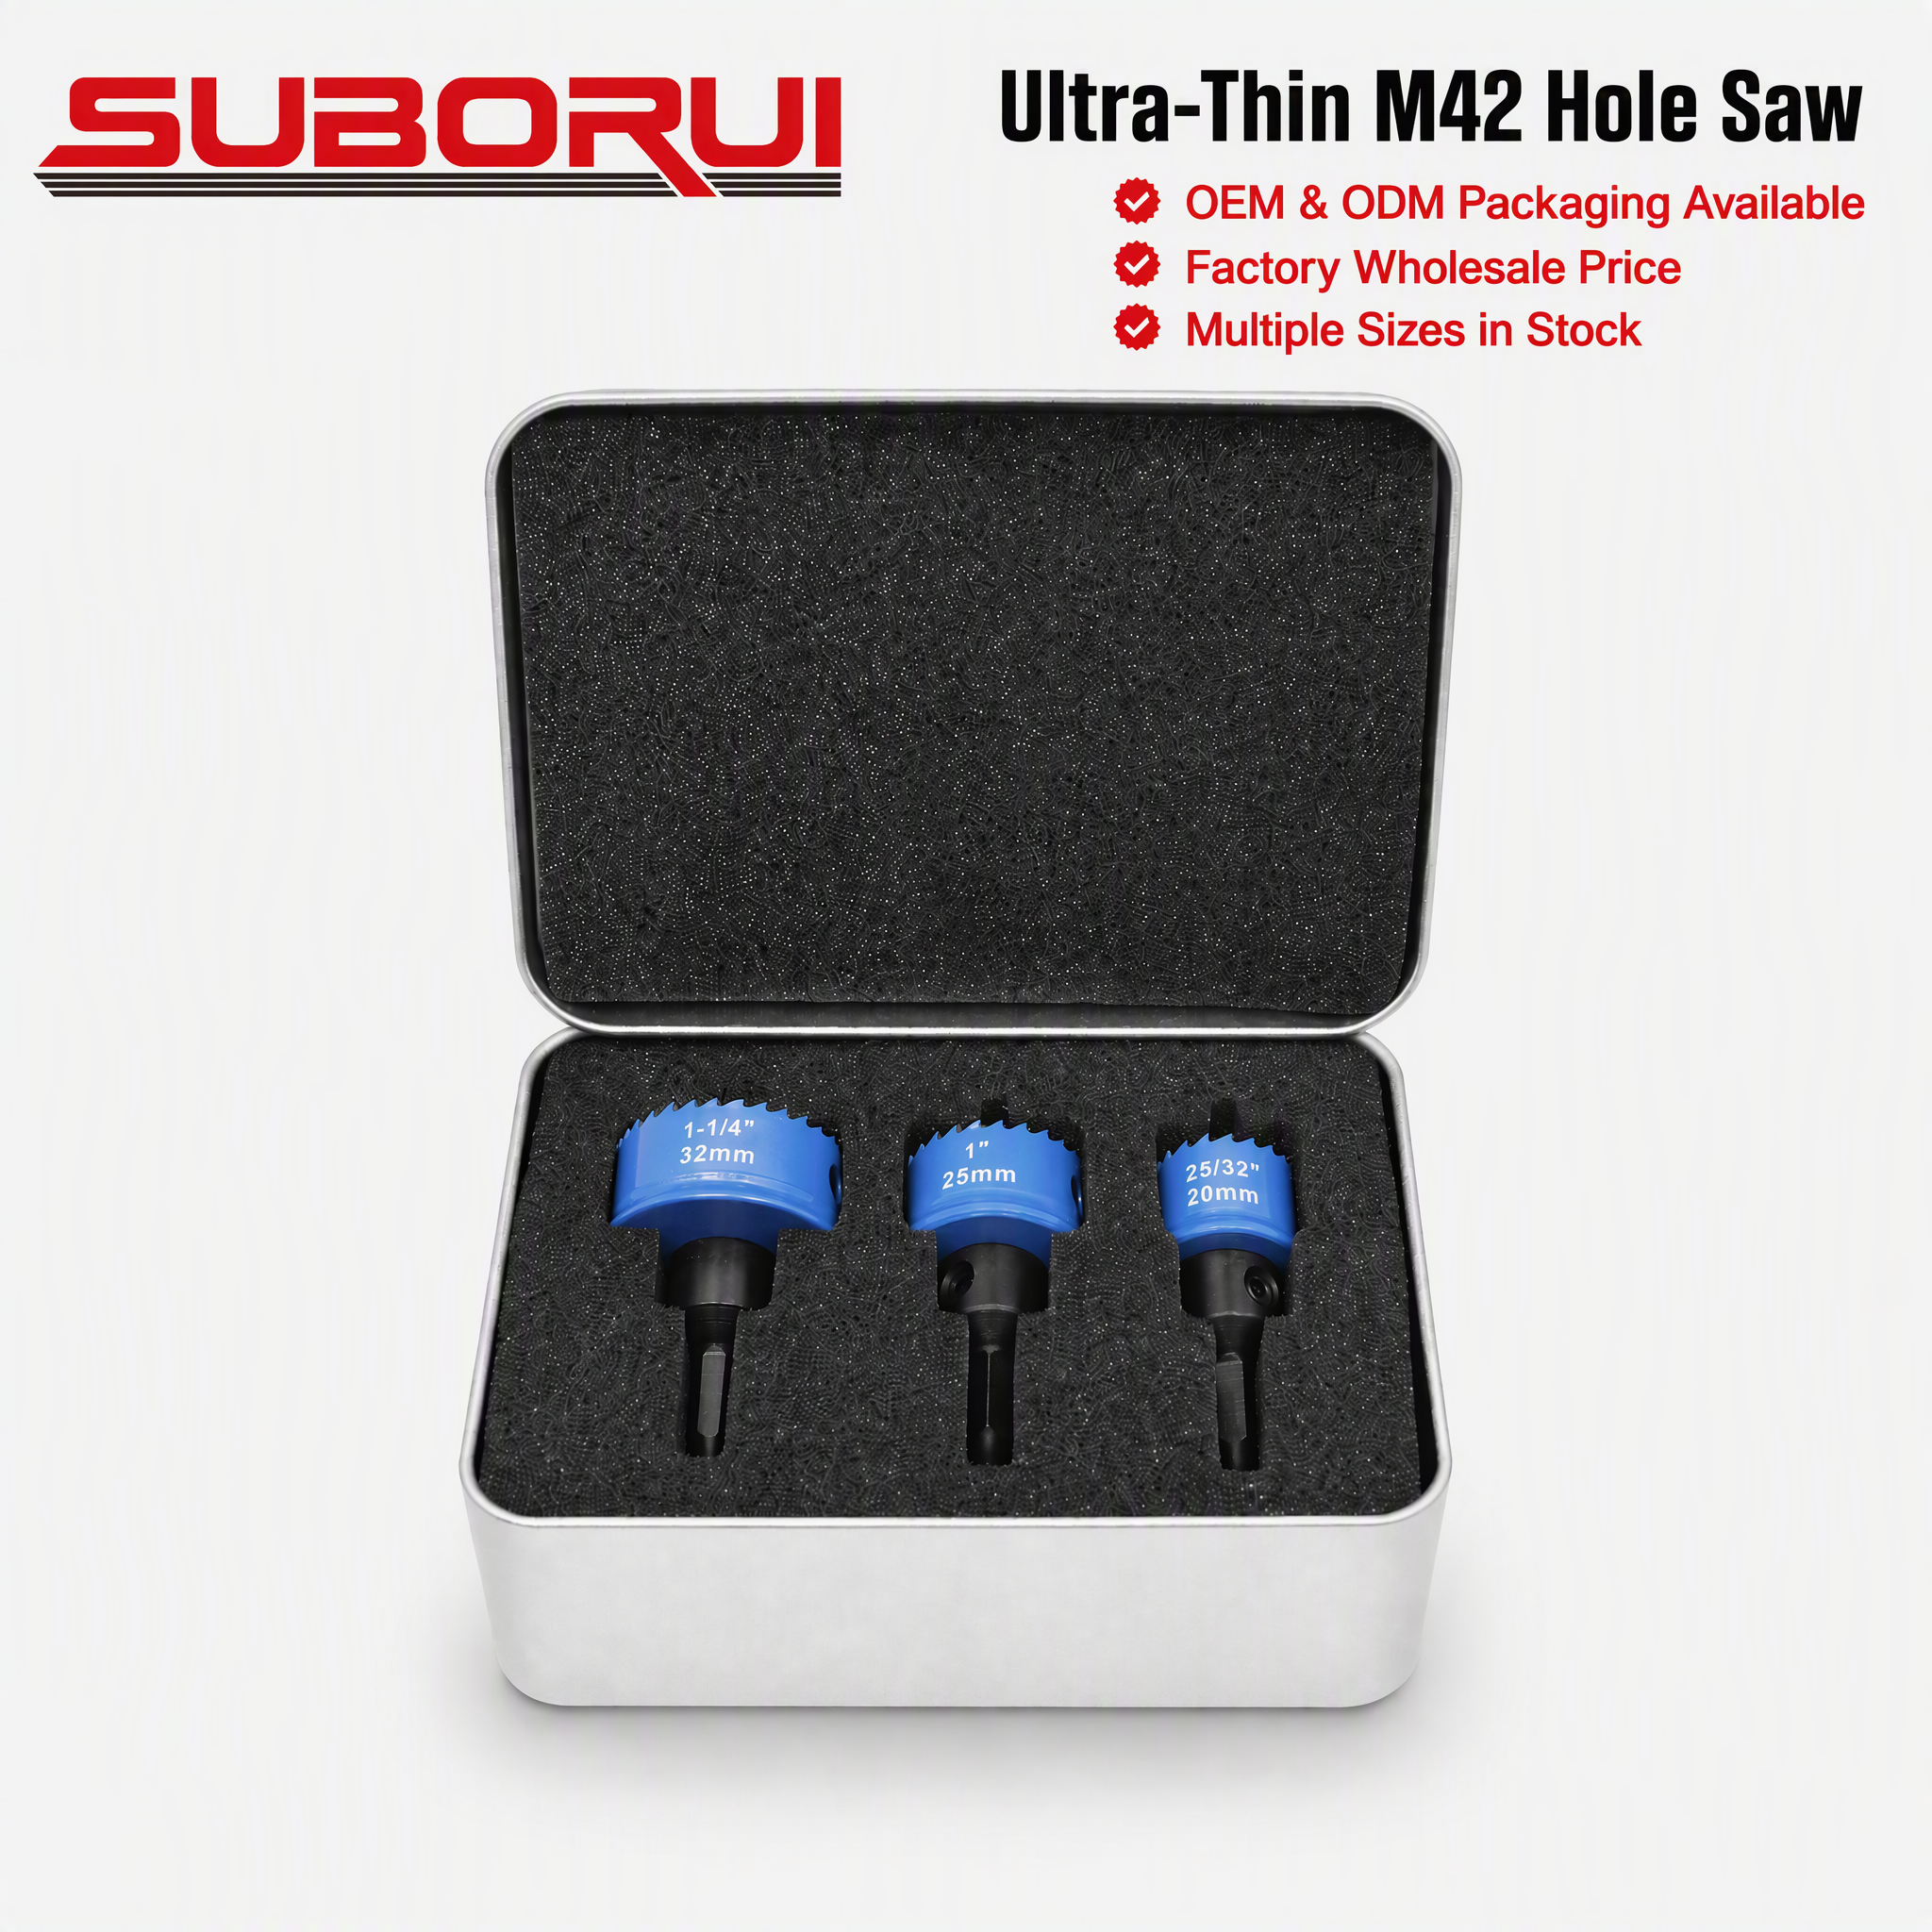
SUBORUI OEM Factory 3pcs 20mm 25mm 32mm Ultra-thin Hex Shank M42 Bi-Metal Hole Saw Cutter Set for Metal Cutting
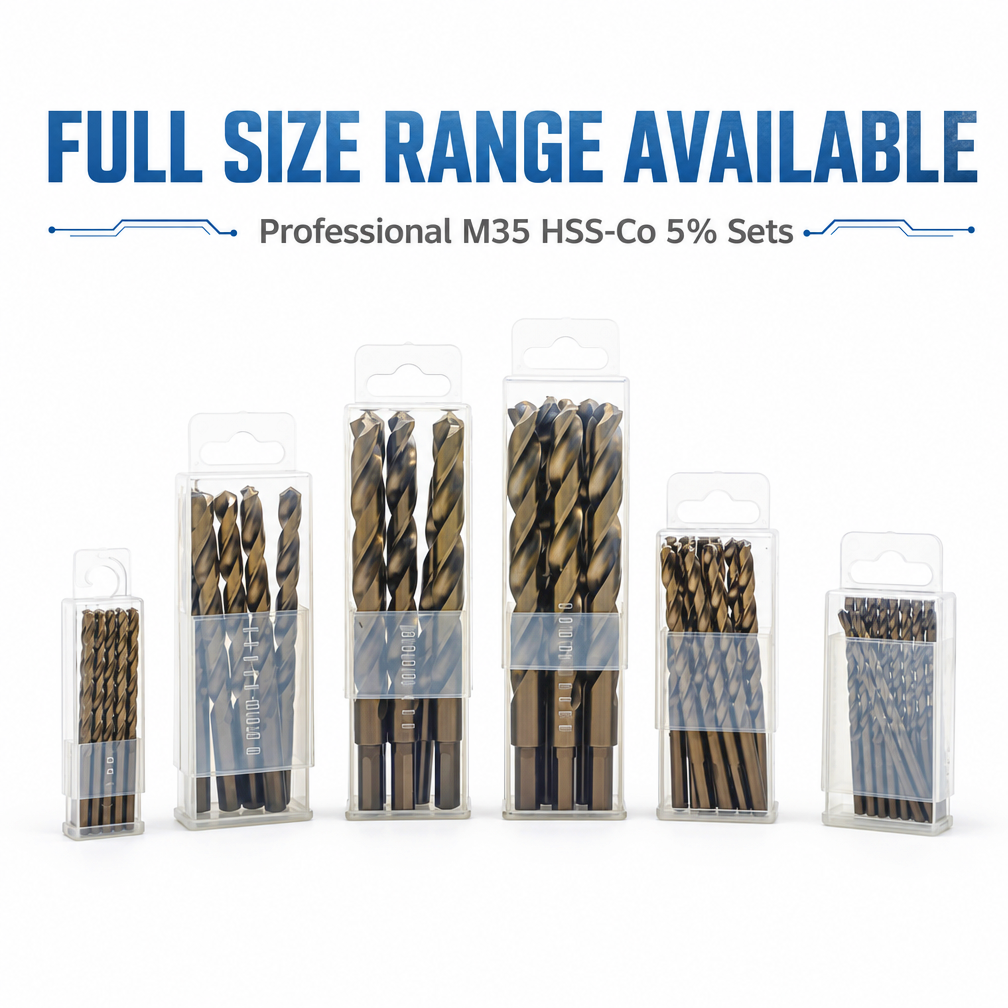
SUBORUI Manufacturer DIN338 Fully Ground M35 Co5% Metal Cobalt Hss Twist Drill Bit for Metal Stainless Steel Drilling

BORUI 12-80MM Hole Saw Drill Bit Set HSS Hole Cutter for Stainless Steel, Metal, Iron, Wood With Plastic Box
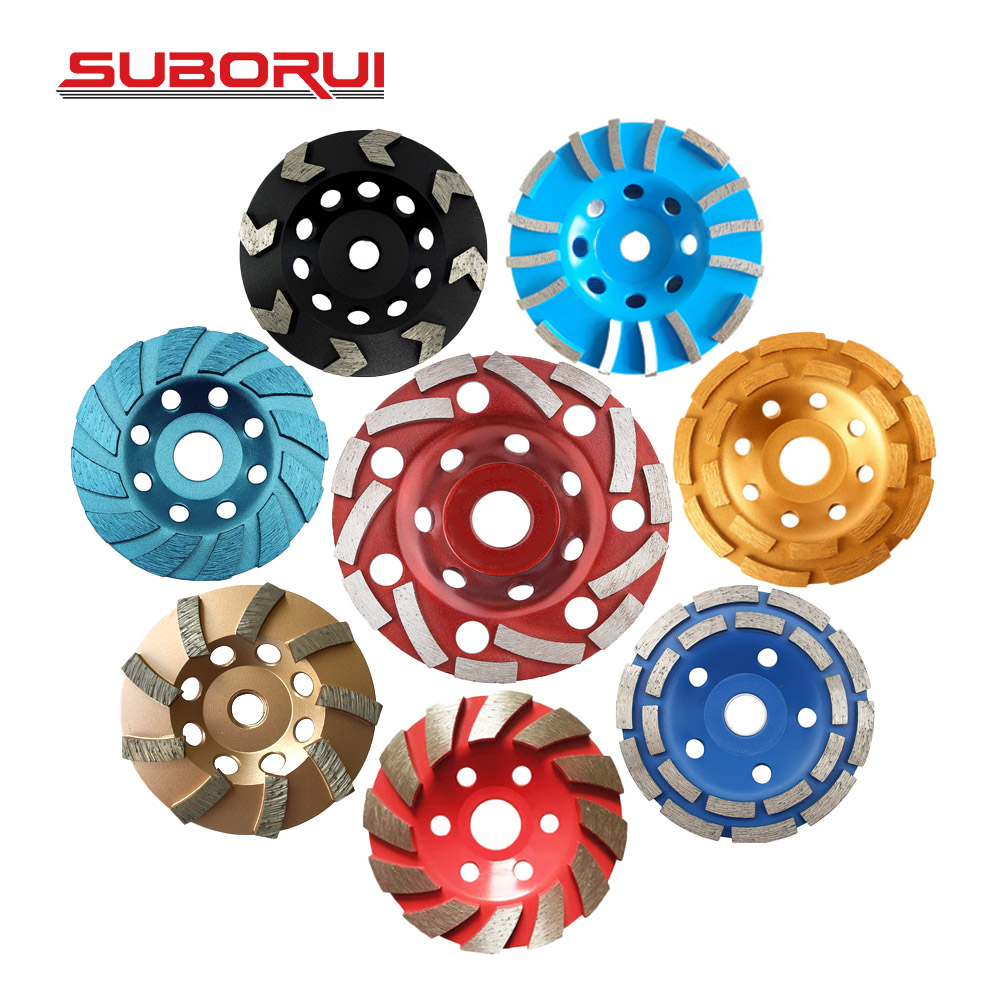
SUBORUI Customised OEM 4.5Inch Turbo Concrete Diamond Cup Grinding Wheel for Concrete Granite Stone Masonry

Suborui 35-100mm Borderless Spotlight Drill Bit Hole Opener HSS Bi-Metal Hole Saw Cutter for Wood Plywood Drywall

SUBORUI 1/4 Inch HSS Fully Ground Titanium Coated Metal Hex Shank Twist Drill Bit ISO Certified Customizable OEM

SUBORUI Din352 Metric Hss M2 3PCS M2 M3 M4 M5 M6 M8 M10 M12 M14 M16 M18 M20 HSS Straight Fluted Screw Thread Hand Taps Set
1. Precision Thread Milling: Engineering Architecture for Slovak Industrial Manufacturing
In modern subtractive machining, thread milling has emerged as the premier method for generating critical internal and external thread profiles across demanding metallurgical environments. Within the Slovak Republic—one of the world’s most concentrated automotive and precision engineering corridors—the transition from traditional synchronous tapping to multi-axis CNC helical interpolation thread milling is driven by zero-scrap mandates, high-mix production cycles, and the processing of difficult-to-cut superalloys.
Unlike taps, which contact the entire thread flank simultaneously under immense torsional resistance, a thread milling cutter operates on a helical path combining orbital motion with an axial pitch advance in a single revolution. This kinematics yields substantially lower cutting forces, superior chip control, and total pitch-depth flexibility. If a tap shears inside an expensive automotive battery casing or transmission housing, EDM extraction or part scrappage costs thousands of euros. Conversely, when a solid carbide thread mill experiences edge wear, it leaves the central bore clear, safeguarding components valued at thousands of euros in tier-1 toolrooms across Bratislava, Trnava, Nitra, and Žilina.
Zero Broken Tool Scrap Risk
The cutter diameter is significantly smaller than the nominal thread diameter. In the event of catastrophic deflection or wear, the core remains unobstructed, preventing casting losses.
One Tool, Multi-Thread Utility
A single thread mill can generate M12x1.5, M14x1.5, and M20x1.5 right-hand or left-hand internal and external threads, drastically slashing tool magazine inventory overhead.
Full Threading to Blind Hole Bottoms
Where DIN taps require a lead chamfer of 2 to 3 thread pitches, thread mills cut full, clean threads right down to the bottom of blind pilot holes with minimal clearance.
2. Kinematic Comparison: CNC Thread Milling vs. Synchronous Tapping
When evaluating total cost of ownership (TCO) across automotive chassis and structural component machining, tool engineers must examine cycle times, spindle loads, tool life repeatability, and surface roughness ($R_a$). The table below reflects standardized production metrics verified across European C45 steel, AlSi10Mg cast aluminum, and 316L stainless steel workpieces:
| Performance Parameter | Solid Carbide Thread Mill (Submicron) | HSS-E / PM-Cobalt Machine Tap (DIN 371/376) | Engineering Benefit in Production |
|---|---|---|---|
| Spindle Load Requirement | Low cutting torque; suited for 40-taper & BT30 high-speed spindles | Very high instantaneous torque; mandates heavy-duty spindle gearboxes | Enables threading on lightweight 5-axis machines without spindle stall |
| Blind Hole Depth Clearance | Under 0.5 mm clearance required to reach full nominal profile | Requires 2.5 to 4 pitches of chamfer runout lead-in | Saves casting weight and reduces wall thickness in EV motor frames |
| Tolerance & Fit Adjustment | Freely adjustable via CNC tool radius compensation ($D_{comp}$) | Fixed pitch diameter (6H, 6G, 7H); cannot adjust for coating thickness | Instant compensation for post-machining anodizing or hardening growth |
| Chip Morphology | Micro-segmented, discontinuous comma chips easily evacuated by air/coolant | Continuous stringy swarf prone to nesting and bird-nesting on blind flutes | Prevents workpiece surface scratching and unmonitored night-shift stoppages |
| Failure Recovery Impact | Tool pulls out cleanly; no core workpiece damage; zero part scrapping | Tool binds, shatters, and locks deep inside threads; EDM burning needed | Eliminates component rejection on high-value structural castings |
3. Localized Applications Across Slovakia's Automotive & Defense Corridors
Slovakia holds the highest per-capita automobile output in the world. Operating as the manufacturing engine of Central Europe, its manufacturing infrastructure centers around four major OEM anchor clusters: Volkswagen in Bratislava-Devínska Nová Ves, Stellantis in Trnava, Kia Slovakia in Teplička nad Váhom (Žilina), and Jaguar Land Rover in Nitra, along with the emerging Volvo Cars electric vehicle mega-facility in Valaliky near Košice.
Each hub commands distinct cutting tool requirements based on workpiece metallurgy and production constraints:
Western Cluster (Bratislava & Trnava)
Substrates: High-silicon aluminum alloys (AlSi7Mg, AlSi9Cu3) and forged carbon steels.
Application: E-mobility stator housings, battery encasements, gearbox pinions, and subframe link points. Demands diamond-like carbon (DLC) and TiAlN coatings to halt aluminum welding on cutting edges.
Northern Corridor (Žilina & Považie)
Substrates: Cast irons (GJS-400 to GJS-700), ductile nodular irons, and Cr-Mo alloy steels.
Application: Heavy vehicle drivetrains, hydraulic pumps, precision valves, and high-pressure transmission casings requiring ISO metric fine ($M_f$) and BSPP gas threads with strict roundness tolerances.
Eastern & Central (Nitra, Košice & Martin)
Substrates: Armox, Hardox, high-strength armor plates, and titanium alloys.
Application: Defense armored vehicle chassis, welded structural frameworks, and industrial machinery where conventional taps shatter instantaneously, necessitating micro-grain tungsten carbide thread milling.
4. Slovak Tooling Procurement Trends & Technical Evolution
The tooling market in Slovakia is experiencing a fundamental technological restructuring driven by three converging factors:
1. Nearshoring of Supply Chains from East Asia to V4 Hubs: European tier-1 manufacturers are actively reconfiguring their procurement strategies. While European brand-labeled cutters from Germany or Switzerland offer high performance, their list prices (often €90–€180 per unit) compress contractor margins. Slovak CNC workshops are establishing direct, audited procurement partnerships with high-tier verified original equipment manufacturers (OEMs) that meet ISO 9001 and Intertek verification standards, securing equal tool longevity at 40%–60% lower tool acquisition costs.
2. Transition to Lightweight Structural Materials & Thin-Walled Castings: Electric vehicles demand drastic mass reduction. Thread milling produces negligible radial stress compared to roll form tapping, preventing hairline deformation on thin-walled aluminum battery enclosures and structural suspension struts.
3. Integration of Through-Spindle Cryogenic and High-Pressure Internal Coolant (IKZ): Thread milling in stainless steel (AISI 304/316) and heat-resistant superalloys requires internal radial coolant holes aligned with each flute. Direct jet delivery to the cutting zone flushes chips immediately and prevents micro-chipping caused by thermal shock.
5. Manufacturing Infrastructure & Technical Advantage
Since our foundation in March 2007, Jiangsu WRD Tools Co., Ltd. has grown to become one of the premier OEM/ODM cutting tool manufacturers in Danyang, China's core tooling center. We operate an integrated 12,000 m² state-of-the-art facility with over 150 skilled machinists, metallurgical engineers, and quality assurance specialists. We produce over 90 million industrial cutting tools each year, serving leading engineering markets across Germany, Switzerland, Sweden, the United States, and the European Union.
6. Slovak Procurement & Tooling Engineer FAQ
Direct answers to common technical and commercial questions raised by Slovak procurement officers, workshop owners, and toolroom heads:
Can your thread mills produce standardized ISO Metric, Metric Fine, and BSPP/NPT pipe threads?
How do you assist Slovak workshops with CNC programming and helical toolpaths?
What is the minimum order quantity (MOQ) and sample trial policy for Slovak industrial buyers?
What surface coatings do you recommend for machining high-tensile stainless steel and abrasive cast iron?
How do you handle EU customs clearance, CE compliance, and documentation for Slovakia?
Request Engineering Catalog & Factory Price List
Partner directly with an Intertek-verified cutting tool manufacturer. Access our technical engineering compendium, calculate your cost per thread hole, and arrange customized samples for your machine trials.
Get Catalog