
2007
Founded Year
12,000 m²
Integrated Plant
150+
Skilled Specialists
90M
Units Output / Yr
Intertek
Onsite Audited
20+
Export Nations
Engineered Tooling & Segmented Blade Solutions
Tested under rigorous DIN standards for stone fabrication, reinforced concrete, high-tensile metal cutting, and deep infrastructure applications across Northern Bohemia.

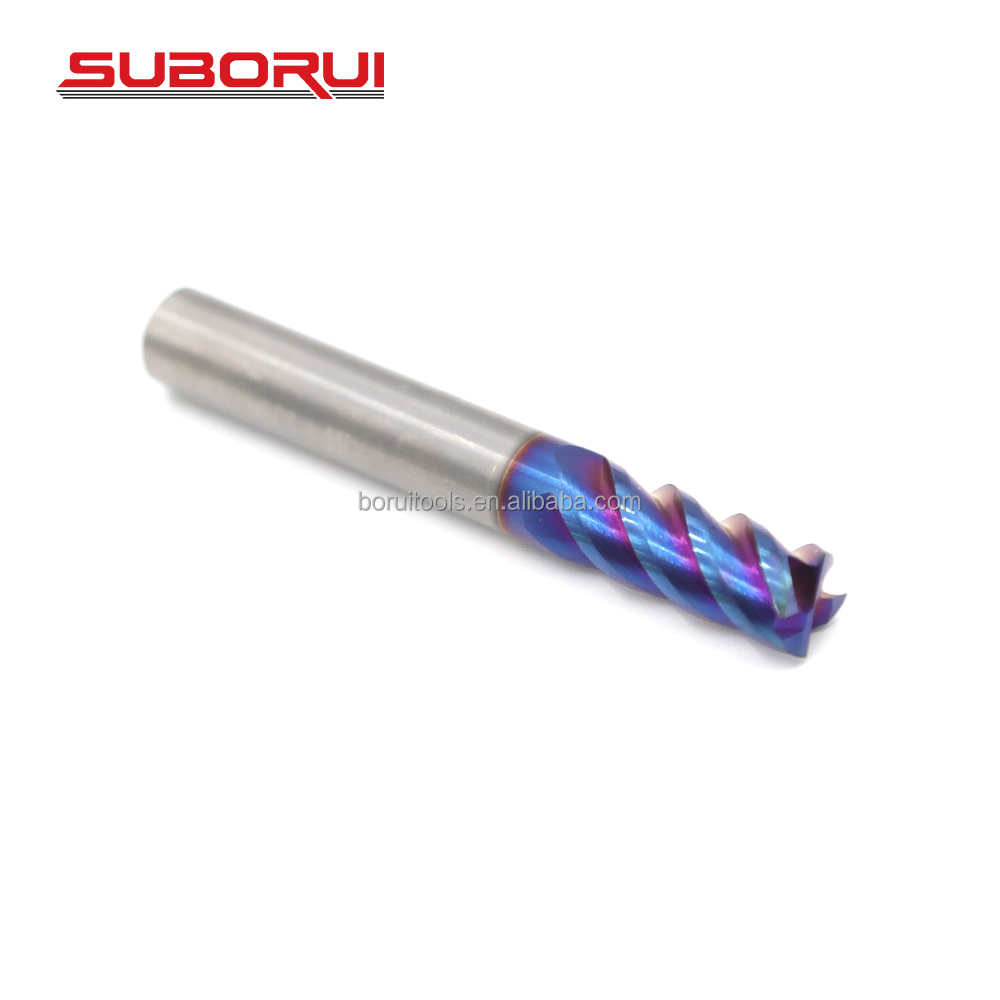



Localized Demand Drivers for Segmented Saw Blades in Liberec & Northern Bohemia
The industrial architecture of Liberec and the broader Liberecký kraj is defined by a dense intersection of heavy automotive manufacturing, precision mechanical engineering, high-performance technical textiles, architectural glass fabrication, and historical civil infrastructure. Operating diamond cutting and segmented tooling within this territorial perimeter presents uniquely punishing tribological challenges. The surrounding geological formations, dominated by the Lusatian Granite Massif (Lužický žulový masiv) and basaltic bedrock, produce aggregates that are notoriously dense, highly abrasive, and prone to severe thermal loading during core drilling and mechanical sawing operations.
In standard civil engineering projects—ranging from modernization works along the I/35 transit corridor connecting Liberec to Turnov and Zittau, to the renewal of crystalline silica processing centers in Jablonec nad Nisou—standard sintered diamond tools suffer catastrophic premature segment desintering or excessive steel core warping. As a verified source factory, Jiangsu WRD Tools Co., Ltd. (operating the SUBORUI precision tooling line) has re-engineered segment matrix metallurgies specifically for high-load Central European job-site parameters. Our laser-welded segmented blades synthesize high-grade synthetic diamond crystals with tailored cobalt-bronze and tungsten carbide matrix binders, guaranteeing that the diamond grit shedding cycle perfectly synchronizes with the abrasive breakdown of hard Czech river gravels and quartz-rich granites.
Heavy Civil Works & Transport Links
Road-widening and railway infrastructure upgrades throughout Northern Bohemia demand dry and wet asphalt-over-concrete sawing. Our deep laser-welded gullets provide aggressive swarf ejection and prevent abrasive thermal buildup in high-aggregate slabs.
Lusatian Granite & Hard Stone Dressing
Quarries and stone workshops processing native Bohemian granite require zero segment loss and minimal chipping. Custom-tailored hot-pressed segmented cup discs and blades deliver exceptionally uniform surface finishes without micro-fracturing edges.
Tier-1 Automotive & Metal Processing
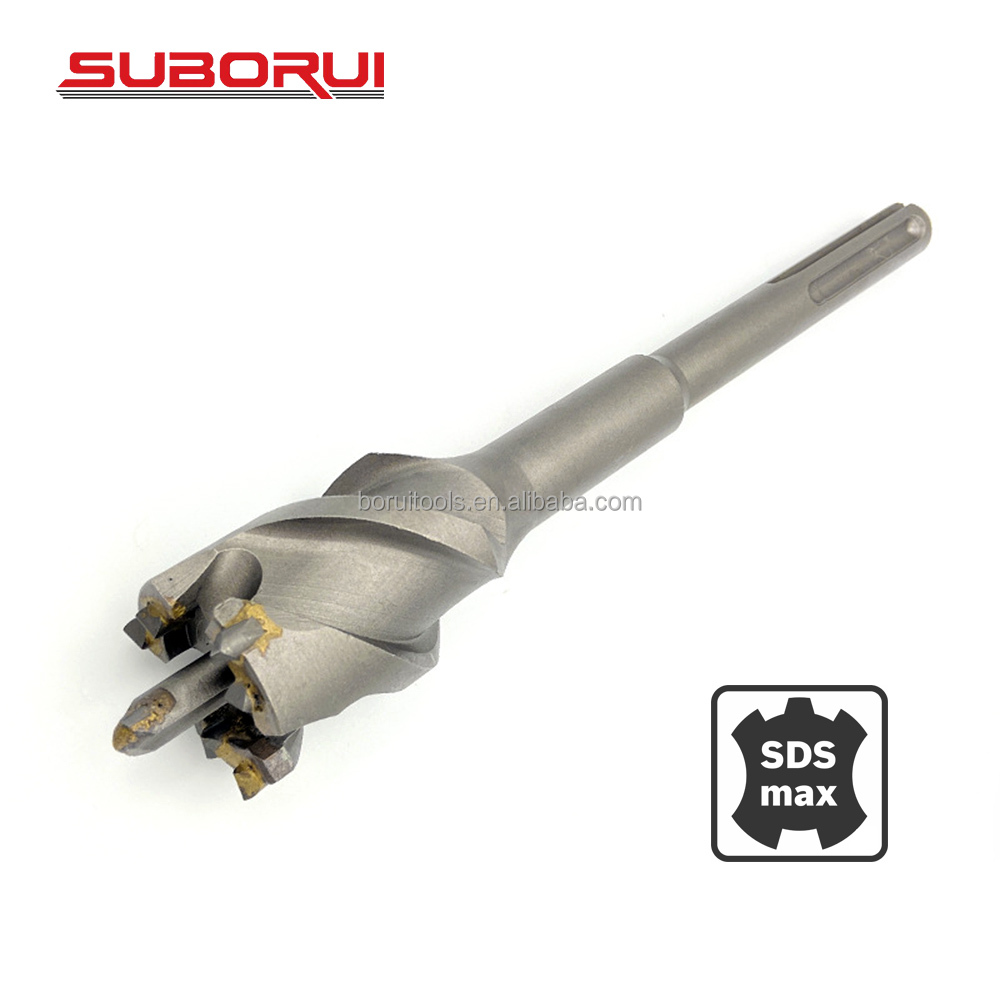
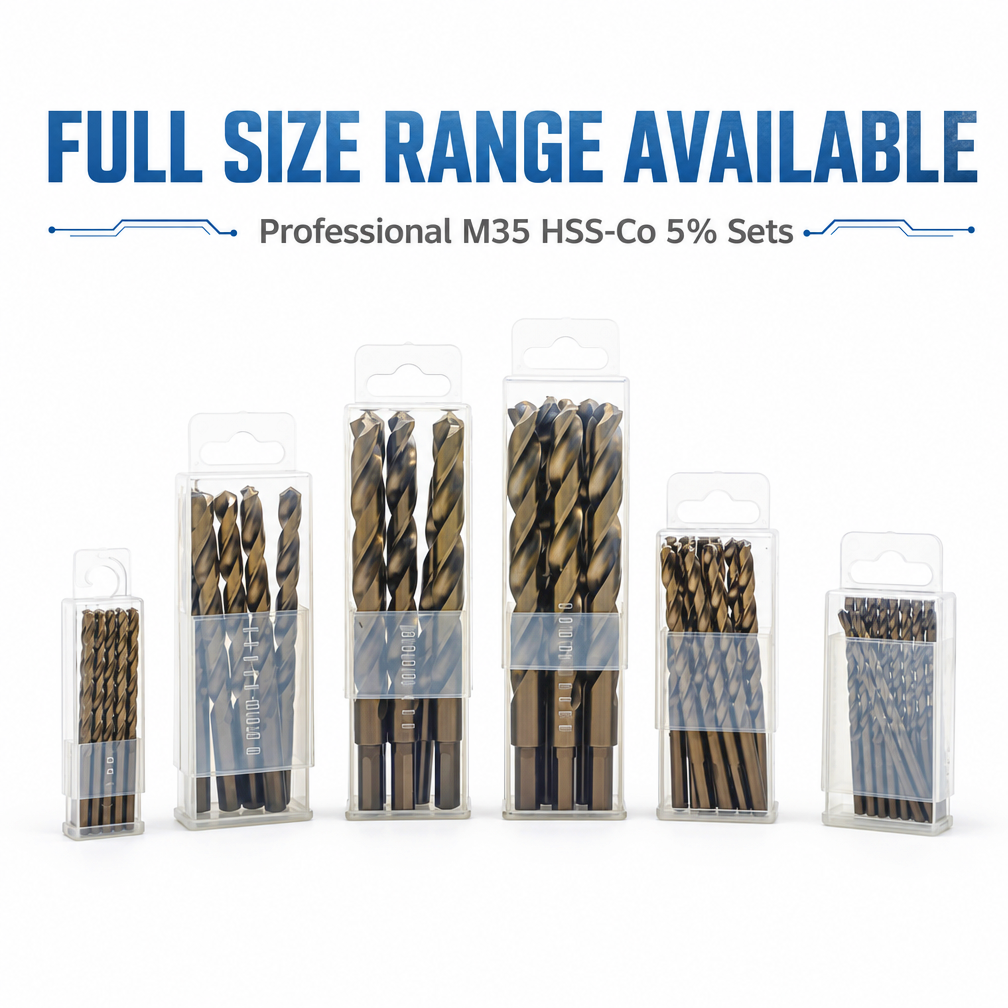
Liberec’s automotive engineering supply chain requires heavy structural modifications, precision machinery anchoring, and deep anchor bolt drilling. Our SDS Max hollow core systems and M35 cobalt twist bits cut smoothly through reinforced rebar webs.
Technological Evolution & Regional Compliance in the Liberec Tooling Sector
Procurement paradigms across the Czech Republic are experiencing structural shifts dictated by stringent European Union workplace standards (EN 13236 Safety Requirements for Superabrasive Products) and rising labor unit expenses. Sourcing personnel within regional contractor enterprises can no longer rely on uncertified general-purpose cutting discs that generate excessive airborne crystalline silica dust, extreme vibration (HAVS - Hand-Arm Vibration Syndrome), and unacceptable downtime from frequent disc replacement.
Moving toward 2030, the regional market in Liberec is pivoting sharply toward three primary innovations: sandwich-core silenced laser-welded saw bodies for urban construction zones, aero-dynamic keyhole slot design for rapid debris extraction without auxiliary slurry pumping, and ultra-hard bonding matrices that resist glazed surface burn-in when running on 400V high-frequency hydraulic and electric floor saws.
Strict EN 13236 Compliance
Job sites across Liberec now mandate certified rupture resistance up to 100 m/s peripheral velocity. Laser-fused weld seams must withstand shear tests exceeding international benchmarks to prevent catastrophic job-site accidents.
Dry-Cutting Ceramic Advancements
The interior architecture and tile industry in Northern Bohemia is adopting thick sintered porcelain slabs (20mm+). Hot-pressed continuous-rim and turbo-segmented blades provide clean, chip-free cuts without water cooling.
Direct OEM Factory Sourcing
European distributors are actively bypassing non-manufacturing trading firms to eliminate markups, securing customized private branding, tailored segment geometry, and flexible inventory replenishment cycles.
Acoustic Damping Technologies
Urban reconstruction in historical zones like Staré Město Liberec requires specialized copper-riveted laser-slotted blades that dampen sound wave resonance, protecting both operators and historic masonry facade integrity.
Segmented Diamond Tooling Comparative Metrics
Comprehensive overview of physical dimensions, bond formulas, and performance parameters for regional commercial procurement teams.
| Tool Category | Standard Diameters | Bond Matrix & Hardness | Primary Cutting Substrates | Maximum Speed Rating |
|---|---|---|---|---|
| Segmented Laser Blade | 115mm – 400mm (Arbor: 22.23 / 25.4mm) | Cobalt-Bronze Matrix / HRB 85–95 | Reinforced Concrete, Cured Asphalt, Hard Pavers | 80 m/s – 100 m/s |
| Segmented Cup Grinding Disc | 100mm, 125mm, 180mm (M14 or 22.23mm) | Tungsten-Reinforced Sintered / HRB 90–100 | Granite, Cured Screed, Epoxy Removal, Marble | 6,600 – 12,200 RPM |
| Hot-Pressed Net Wave Turbo | 115mm, 125mm, 230mm (Ultra-thin 1.2–1.8mm) | Nickel-Free Synthetic Diamond Sinter | Porcelain Stoneware, Ceramics, Dense Tile | 13,300 RPM |
| M42 Bi-Metal / Cobalt Cutters | 14mm – 210mm (Universal / Hex Shank) | HSS-Co 8% Tooth Strip / HRC 66–68 | Stainless Structural Sections, Hard Alloys, Plywood | Variable by Substrate |
| SDS Max Hollow Core Bit | 30mm – 160mm (Length: 100–600mm) | Tungsten Carbide TCT Tips / HRC 89–91 | Heavy Masonry, Reinforced Concrete Walls, Brick | Hammer Mode Compatible |
Why Global Brands Choose Jiangsu WRD Tools Co., Ltd.
Founded in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. operates an expansive 12,000 m² high-precision tool production plant in Danbei Town, Danyang, Jiangsu Province—the heart of China's premier cutting-tool industrial belt. Unlike trading entities that outsource quality inspection, WRD Tools executes total in-house production control across every critical manufacturing phase.
Recognized as an official High-Tech Enterprise of Jiangsu Province in 2019, our facilities house fully automated laser-welding lines, high-frequency induction sintering systems, precision CNC flute grinders, vacuum heat-treatment furnaces, and rigorous dynamic balance testing stations. Over the past 19 years, our technical precision and verified Intertek onsite audit standards have earned WRD Tools a place as an OEM/ODM supplier to global giants including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller. With annual exports spanning more than 20 countries across Europe and the Americas, our technical sales engineers understand how to support both high-volume private label distributor packaging and complex custom project specifications.
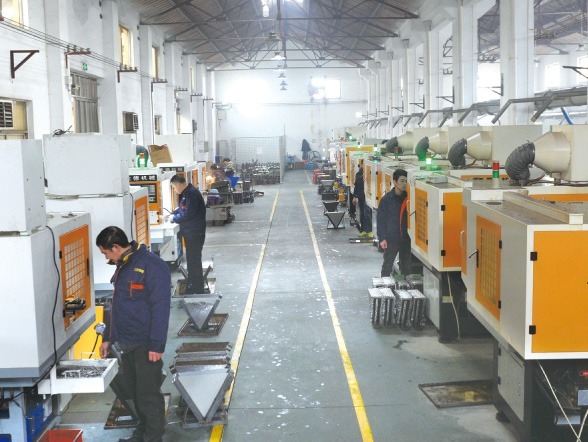
Integrated 12,000 m² Manufacturing Facility
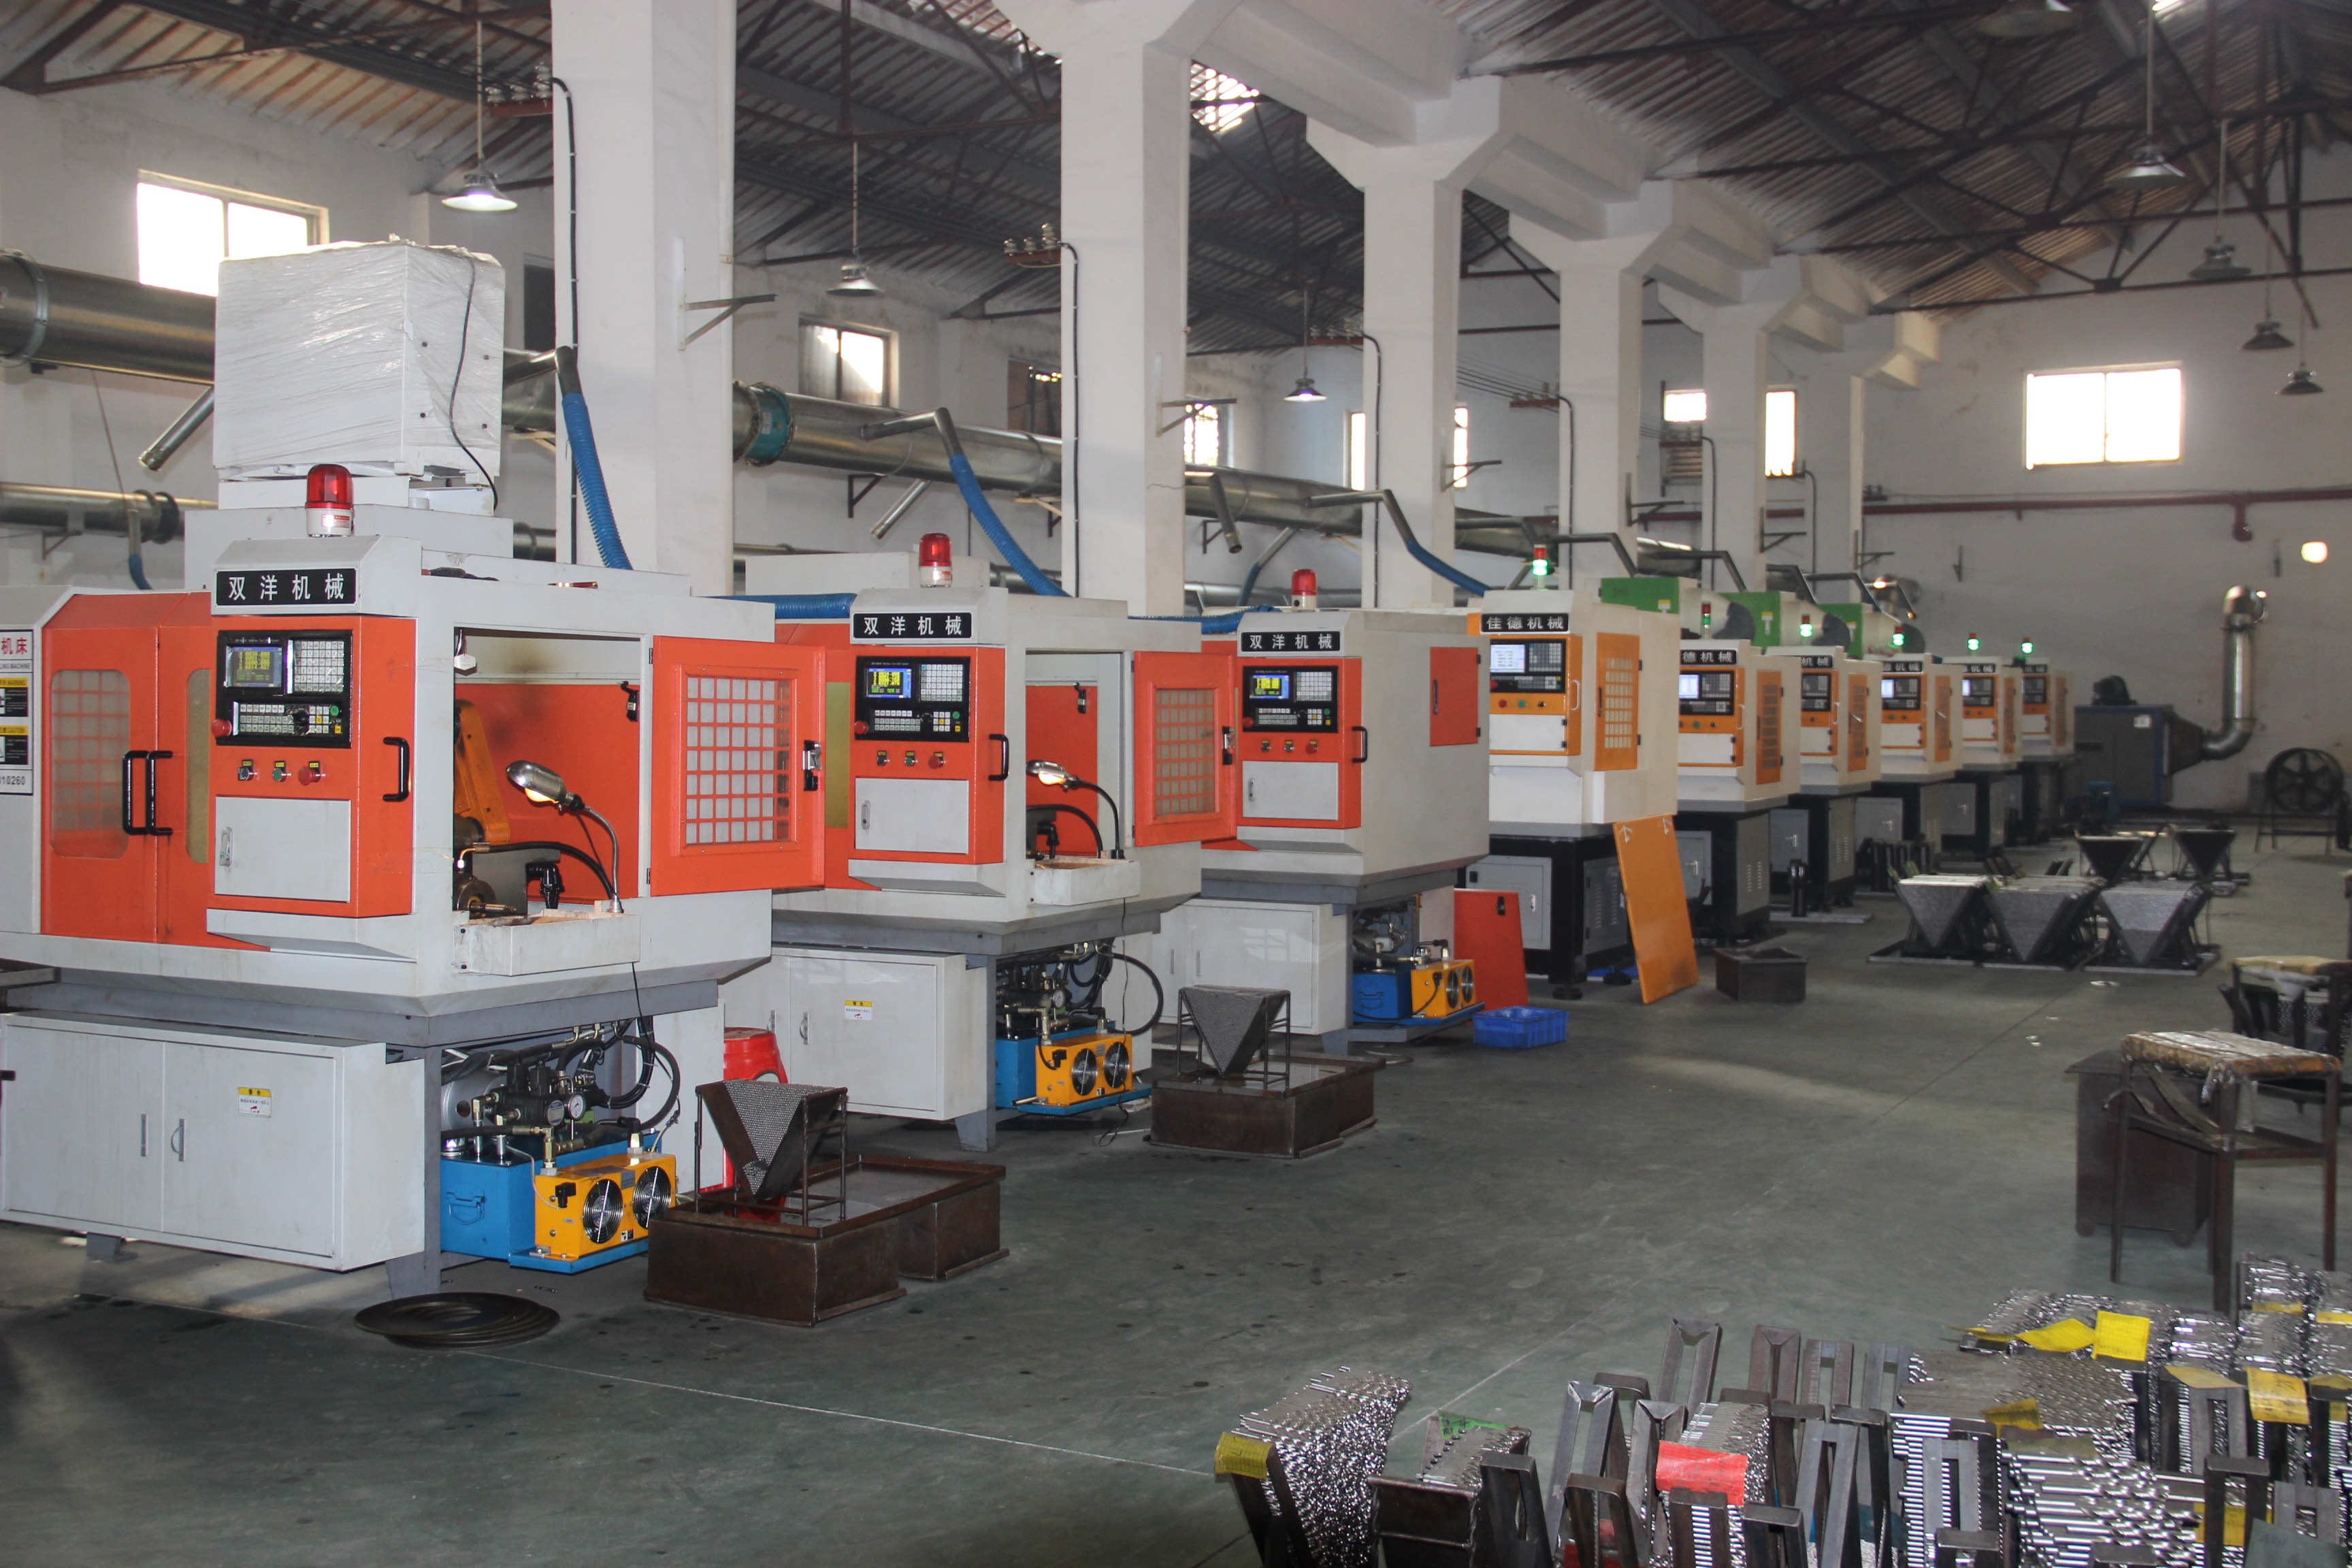
Automated Precision Flute & Segment Grinding
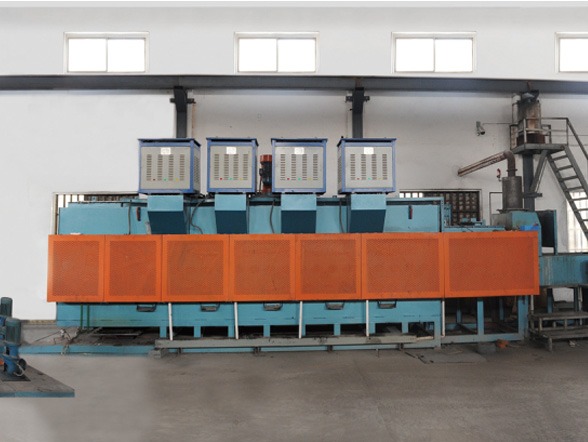
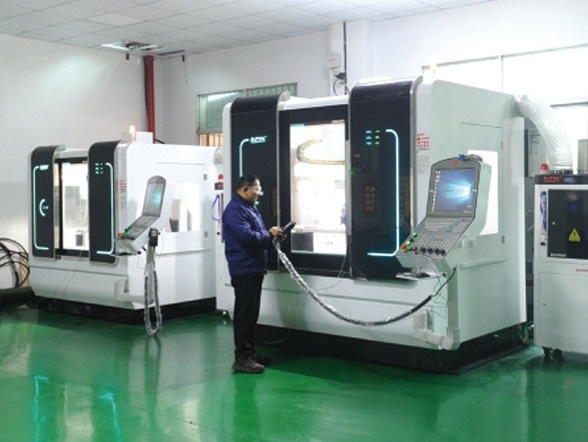
High-Speed Multi-Axis CNC Machine Tooling
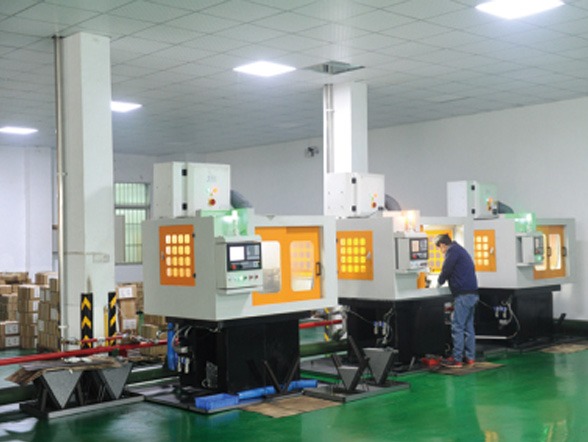
Intertek-Audited Quality Inspection Department
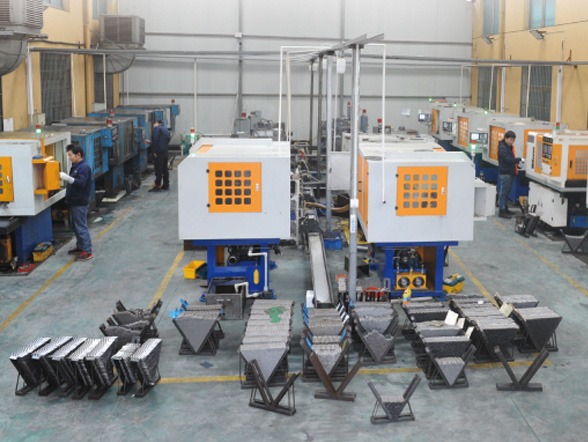
Palletized Finished Goods & Global Shipping Hub
Fully Automated Private-Label Retail Packaging Line
Frequently Asked Questions (Liberec Market)
Practical procurement answers covering customs compliance, bonding matrices, MOQ parameters, and private-label production times.
How do I select the right diamond segment bond for cutting native Czech concrete containing river aggregates?
A critical rule in diamond tool mechanics is: "Soft bond for hard materials, hard bond for soft, abrasive materials." In the Liberec region, concrete formulations often incorporate crushed basalt or river gravels rich in silica quartz. If an overly hard bond is specified, the diamond grit polishes flat (glazing) and will stop cutting, generating intense heat that warps the core. WRD Tools tailors customized cobalt-rich, softer bronze matrices that erode at a controlled rate, continually exposing crisp diamond cutting facets even under extreme feed pressure.
What is the minimum order quantity (MOQ) for custom private-label segmented saw blades?
For standard dimensions (115mm, 125mm, 230mm, 350mm) featuring your company's laser-etched logo and custom color coating, our factory MOQ generally starts at 100 to 300 pieces per diameter. Full retail custom packaging (such as branded blister display packs, color double-blisters, or litho printed inner boxes) starts at approximately 1,000 to 1,200 units. For large distributors and hardware chains, we provide mixed-pallet consolidation across all drill bit, hole saw, and diamond cutting categories.
Are your segmented diamond blades fully compliant with European standard EN 13236?
Yes. Every batch of segmented diamond blades manufactured for European destinations is engineered and tested strictly in adherence with EN 13236 standards. Our automated laser-welding processes undergo destructive segment torque shear tests, rotational imbalance verification, and 100% periphery run-out inspection. This ensures that every blade entering the EU single market withstands the high radial torque and centrifugal forces typical of high-frequency power tools.
What shipping lead times can industrial clients in the Czech Republic anticipate?
For custom OEM bulk orders, our production cycle spans 30 to 45 business days depending on packaging complexity. Ocean transit from Ningbo or Shanghai port to Hamburg or Rotterdam typically takes 28 to 35 days, followed by scheduled rail or road freight forwarding directly to warehouse receiving bays in Liberec, Jablonec nad Nisou, or Mladá Boleslav. For urgent batch validation or specialized prototype testing, expedited air freight shipments can be delivered to Václav Havel Airport Prague (PRG) within 5 to 7 days.
Can WRD Tools provide customized diamond segment slotting (e.g., Keyhole, Wide Gullet, or U-Slot)?
Absolutely. We run dedicated CNC laser cutting beds for alloy steel cores (65Mn / 75Cr1). We can engineer specialized keyhole gullets for faster dust evacuation during dry asphalt cutting, narrow U-slots for stone cutting where edge chipping must be minimized, or custom expansion slots fitted with copper sound-reduction plugs for reduced decibel emissions on indoor civil renovation projects.
Request Technical Spec Sheets & Bulk Factory Pricing
Connect directly with our engineering and export departments to receive comprehensive CAD drawings, bond matrix recommendations, customized OEM branding options, and immediate container-level FOB/CIF pricing for the Liberec and European markets.
Get Catalog