Industrial Heavy-Duty Roughing & High-Removal Rotary Cutters
Integrated directly into CNC production schedules across Rotherham, Don Valley, and the AMRC aerospace cluster, our catalog pairs extreme material removal rates (MRR) with reliable tool life in stainless steels, high-temp nickel alloys, and structural metals.


Engineering Authority: High-Efficiency Roughing End Mills for Sheffield CNC Toolrooms
Sheffield carries unmatched global prestige as the historic bedrock of specialty steels, metallurgy, and advanced subtractive machining. From the heritage heavy forges of the Lower Don Valley to the bleeding-edge aerospace test cells at the Advanced Manufacturing Park (AMP) in Catcliffe, machine shops operate under severe commercial pressures: achieve highest possible Metal Removal Rates (MRR) while curtailing tool chatter, spindle deflection, and thermal fatigue.
As an OEM/ODM high-performance cutting tool factory with nearly two decades of grinding expertise, Jiangsu WRD Tools supplies precision-ground solid tungsten carbide and premium Powder Metallurgy (PM) M42/Cobalt roughing end mills engineered to overcome work-hardening workpiece materials common throughout South Yorkshire. Our roughers incorporate proprietary sinusoidal waveform tooth profiles, unequal helix angles, and tailored chip-splitter geometries that transform continuous stringy swarf into segmented, easily evacuated chips.
Substrate Metallurgy: Micrograin Carbide vs. High-Cobalt PM Steels
Roughing operations represent the most punishing environment inside any CNC milling center. Selecting the correct cutter substrate determines whether a machine operator experiences sustained unmanned machining or unexpected edge chipping:
Ultra-Fine Carbide (0.4–0.6µm)
Formulated with 10–12% Cobalt binder; delivers high transverse rupture strength (>4,000 MPa) and extreme resistance to micro-fracture during heavy trochoidal and dynamic milling cycles.
M42 (8% Cobalt) Powder Metal
Delivers superior shock damping on older or manual milling setups across Sheffield heavy job-shops where spindle runout or deep interrupted casting cuts would shatter brittle tooling.
Sinusoidal Knuckle Profiles
Available in fine-pitch (HR) for tough tool steels and coarse-pitch (NR) for deep slotting in structural carbon steels, reducing radial cutting forces by up to 45% compared to square-end mills.
Advanced PVD Multi-Coating
Specialized AlCrN and AlTiN coatings engineered via cathodic arc evaporation provide oxidation resistance up to 1,100°C, critical for dry or minimum quantity lubrication (MQL) roughing.
Technical Benchmark Comparison: Roughing Geometries
To assist procurement engineers and production managers in South Yorkshire in selecting the optimal tool configuration, our engineering team benchmarks parameters as tested on Fanuc Robodrill and DMG Mori 5-axis platforms:
| Profile Specification | Pitch & Crest Geometry | Primary Material Class | Cutting Force Reduction | Recommended Sheffield Application |
|---|---|---|---|---|
| Type NR (Coarse Knuckle) | Wide radius, deep chip gullet | Low/Med Carbon Steels, S275, S355 | 35% – 42% | Heavy forging pre-machining & industrial fabrication |
| Type HR (Fine Knuckle) | Tight pitch, shallow serrations | Alloy Steels, Tool Steels (P20, D2, H13) | 40% – 50% | Tool & Die mold roughing, extrusion tooling |
| Differential Pitch Knuckle | Variable indexing (35°/38°) | Titanium (Ti-6Al-4V), Inconel 718 | 45% – 55% | Aerospace structural bulkheads, blisk roughing (AMRC specs) |
| Chip-Splitter Smooth Flute | Interrupted flat cutting land | Martensitic & Austenitic Stainless (304, 316) | 25% – 32% | Surgical orthopaedics & food-grade fluid pump housings |
Precision Milling Applications Across Sheffield Manufacturing Hubs
Our OEM/ODM roughing end mills are tailor-manufactured to conquer the grueling machining cycles unique to the Sheffield City Region's primary industrial sectors.
Aerospace Structural Roughing
In aerospace component manufacturing concentrated around the Advanced Manufacturing Park (AMP), production teams tackle forged titanium (Ti-6Al-4V) landing gear spars, turbine casings, and wing ribs. Our custom roughers feature:
- Differential helix geometries preventing harmonic resonance at high RPMs.
- Sub-micron micro-grain tungsten carbide matrices sustaining thermal shock.
- Internal through-coolant ports directing high-pressure lubricant straight to the shear zone.
Nuclear & Defense Heavy Forgings
Large-scale forgings for civilian nuclear reactors, oilfield subsea Christmas trees, and defense armor plates demand tools capable of handling scale and massive depths of cut (Ap):
- Coarse pitch knuckle cutters clearing vast volumes of alloy steel (4140, 8630, F22).
- Engineered chip evacuation flutes preventing swarf compaction in pocket milling.
- Reinforced Weldon and Whistle Notch shanks mitigating tool pull-out under heavy feed.
Medical Implants & Surgical Tooling
South Yorkshire is a global capital for orthopaedic implant production, machining surgical robotics, bone plates, and hip prosthetics from medical-grade stainless steel and CoCr alloys:
- Custom multi-flute roughers generating smaller cutting forces to protect delicate fixtures.
- Cryogenic-compatible PVD coatings minimizing adhesive wear and material pickup.
- Tight tolerance shanks (h6) ensuring sub-micron runout on Swiss-type and 5-axis machines.
Technological & Procurement Trends Shaping Sheffield Machine Shops
As Sheffield manufacturers transition into high-mix, low-volume (HMLV) Industry 4.0 frameworks, purchasing directors are looking beyond low unit prices. Sustainable manufacturing metrics, digital inventory replenishment, and cycle time reductions dictate modern supply chain partnerships.
High-Feed & Dynamic Trochoidal Milling
Sheffield CNC shops are substituting traditional heavy axial cuts with constant chip load CAM algorithms. Our roughing end mills are engineered with optimized core diameters that withstand higher radial forces without flexing.
OEM Resharpening & Circular Economy
Rising raw carbide costs demand sustainable tool recycling. We provide custom knuckle profiles that retain their cutting integrity even after multiple regrinds, drastically lowering total cost per component.
Tool Management Integration
Distributors serving engineering companies across South Yorkshire rely on our OEM private-label laser marking (data matrix codes, batch numbers, exact tolerances) to interface seamlessly with vending cabinets and tool crib systems.
Near-Net-Shape Casting Roughing
Additive manufacturing and precision sand casting in Sheffield are creating workpieces with complex residual envelopes. Knuckle roughers excel at removing heavy, erratic gate remnants without chipping fragile cutting lands.
Frequently Asked Questions for Sheffield Tooling Buyers
Clear, technically rigorous answers covering logistics, quality compliance, and custom manufacturing terms for UK machine tool distributors and industrial end-users.
How do your roughing end mills compare to Sheffield local brand alternatives?
Our tools are manufactured on Swiss Walter, ANCA, and Rollomatic 5-axis CNC grinding centers using pristine European carbide rods. You achieve identical concentricity (<0.003mm) and equivalent tool life on 316L, 17-4PH, and Inconel at roughly 40% to 55% lower unit production costs compared to domestic catalog brands.
What are the typical lead times and shipping routes to South Yorkshire?
For custom OEM production (custom shank flats, specialized fluting, private-label laser engraving), our manufacturing turnaround is 15–20 business days. Shipments to Sheffield, Leeds, and Manchester freight terminals arrive in 3–5 days via air express (DHL/FedEx) or 28 days via consolidated sea freight into Felixstowe or Southampton.
Can we request imperial shank sizes (e.g., 1/4", 1/2", 3/4", 1") alongside metric?
Yes. While metric tools dominate modern British CNCs, numerous Sheffield facilities operate heavy American or legacy machining centers requiring true fractional shanks and flutes. We grind standard DIN 6527 metric standards as well as ANSI/ASME B94.19 imperial geometries upon request.
How is factory quality verified and documented for aerospace traceability?
Jiangsu WRD Tools operates an Intertek-audited production and testing facility. Every production batch is inspected using Zoller Genius tool presetters, Mitutoyo roundness testers, and optical laser micrometers. Material heat-lot certificates and inspection datasheets are supplied with every OEM shipment.
What is the minimum order quantity (MOQ) for custom knuckle roughers?
Standard profile roughing end mills start at an MOQ of just 10 pieces per dimension, enabling machine shops to run field qualification tests without locking up excessive capital. Fully customized private-label production runs (custom packaging, tailored PVD coating) typically begin at 50 pieces.
Which PVD coating is best for dry machining of pre-hardened mould steels?
We recommend our AlCrN-based nanocomposite coating. Featuring a nanohardness of 36 GPa and an oxidation threshold of 1,100°C, it develops a self-passivating chromium-aluminum oxide barrier that prevents micro-welding when dry-roughing steels hardened between 48 and 56 HRC.
Why Global Tool Brands Partner with Jiangsu WRD Tools
With a 12,000 m² state-of-the-art facility founded in 2007, 150+ specialized technicians, and annual sales exceeding RMB 80 million, we provide full OEM/ODM cutting tool manufacturing for tier-one brands including Bosch, Milwaukee, DeWalt, Makita, and Truper.
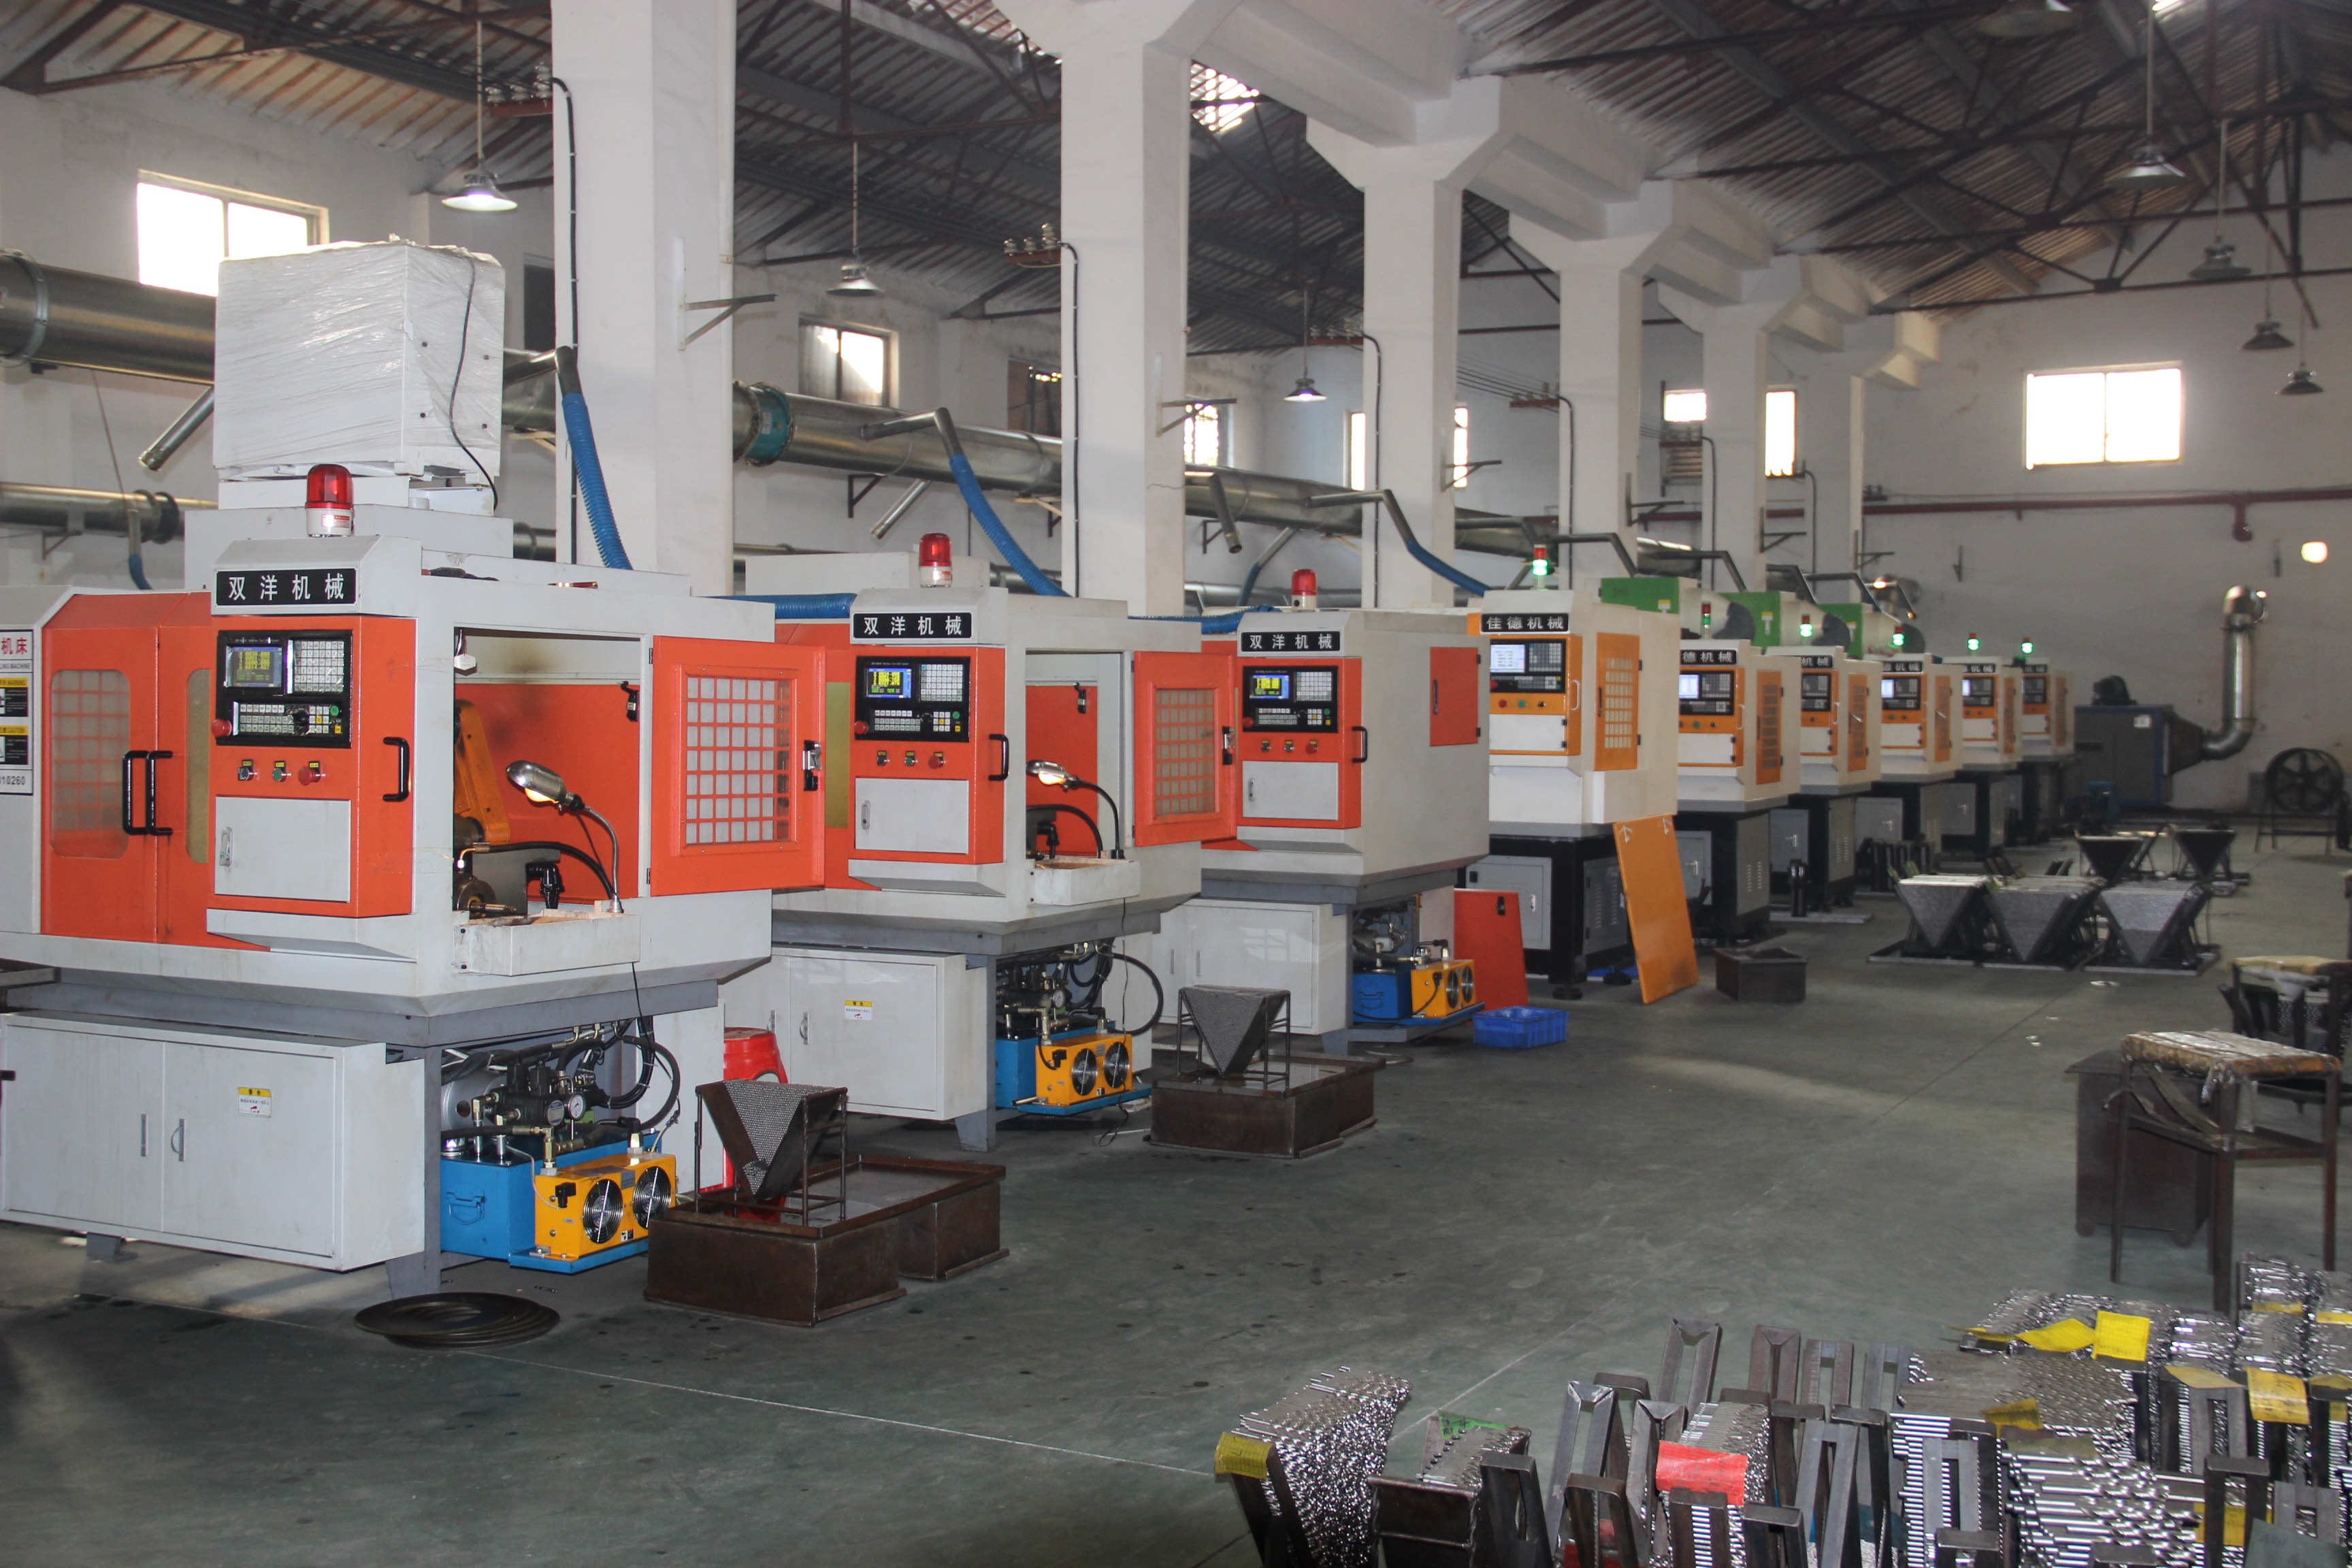
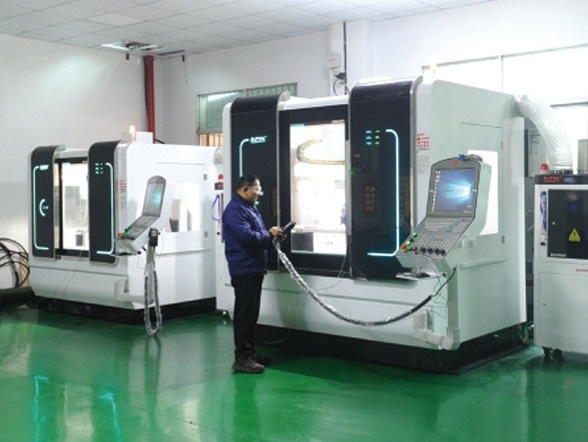
5-Axis CNC Flute Grinding
Equipped with high-precision multi-axis grinding lines, our workshop maintains strict tolerances on helix progression, concentricity, and micro-edge hone preparation.
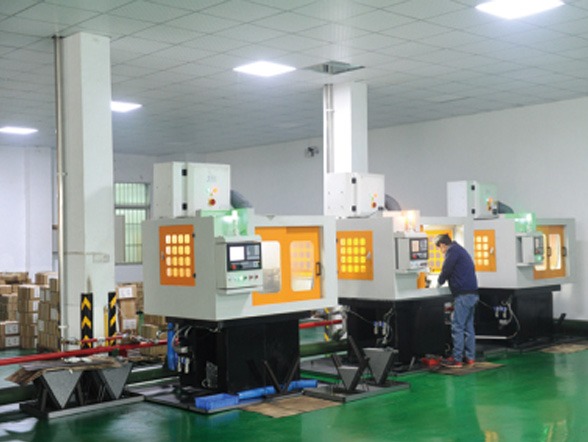
Intertek-Verified Inspection
Audited on-site by Intertek Group, our internal QA/QC laboratories inspect 100% of blanks for density, core micro-structure, hardness, and dynamic run-out.
Private-Label & Packaging
Comprehensive OEM services include fiber laser shank marking, QR inventory coding, bespoke plastic protective cases, and branded retail packaging ready for UK distributor store shelves.