19+
Years Manufacturing Excellence
12,000 m²
Intertek Verified Facility
90M
Annual Tooling Output
66-67 HRC
Core M35 Cobalt Hardness
Industrial Portfolio
High-Performance Tooling Selection for Bern Importers & Fabricators
Tested for high red hardness, exceptional thermal clearance, and superior abrasive resistance. Our M35 cobalt twist drill bits and specialized cutters streamline heavy stainless steel and tough alloy operations.




Engineering Whitepaper
Metallurgical Integrity & Mechanics of M35 High Speed Steel
An in-depth metallurgical analysis for tooling buyers, toolroom managers, and CNC machinists evaluating cutting dynamics, red hardness retention, and tool wear models in tough metal substrates.
⚙
The 5% Cobalt Advantage
Standard High-Speed Steels (like AISI M2) begin secondary carbide degradation and micro-hardness breakdown at operating temperatures between 450°C and 500°C. In contrast, M35 incorporates an intentional addition of 4.75% to 5.25% Cobalt (Co).
Cobalt does not form hard carbides directly; instead, it raises the Curie temperature and solid-solution strength of the martensitic matrix. This elevates thermal resistance to over 600°C–650°C, preventing cutting edge softening (plastic deformation) during demanding dry or micro-lubricated cycle runs.
- Matrix Red Hardness: Preserves >62 HRC at 550°C
- Tempering Stability: Multi-stage salt-bath cycles reduce retained austenite to <2%
- Edge Toughness: Balances brittle fracture prevention with wear margins
✦
135° Split Point Geometry (DIN 1412 Type C)
Conventional 118° chisel-edge drill bits exhibit substantial zero-velocity center thrust, resulting in heavy wander, excessive work-hardening of austenitic stainless steels (such as 1.4301 / AISI 304), and premature tool flank failure.
Our fully CNC ground M35 bits utilize a 135-degree self-centering split point conformant to DIN 1412 Form C. This geometry thins the web by up to 60%, drastically cutting feed thrust force and ensuring instant penetration without a center punch.
- Reduced Axial Thrust: Decreases tool deflection on curved surfaces
- Thermal Dissipation: Optimized parabolic flutes accelerate chip ejection
- Work-Hardening Mitigation: Enters the shear zone cleanly under constant load
◈
Surface Topography & Friction Reduction
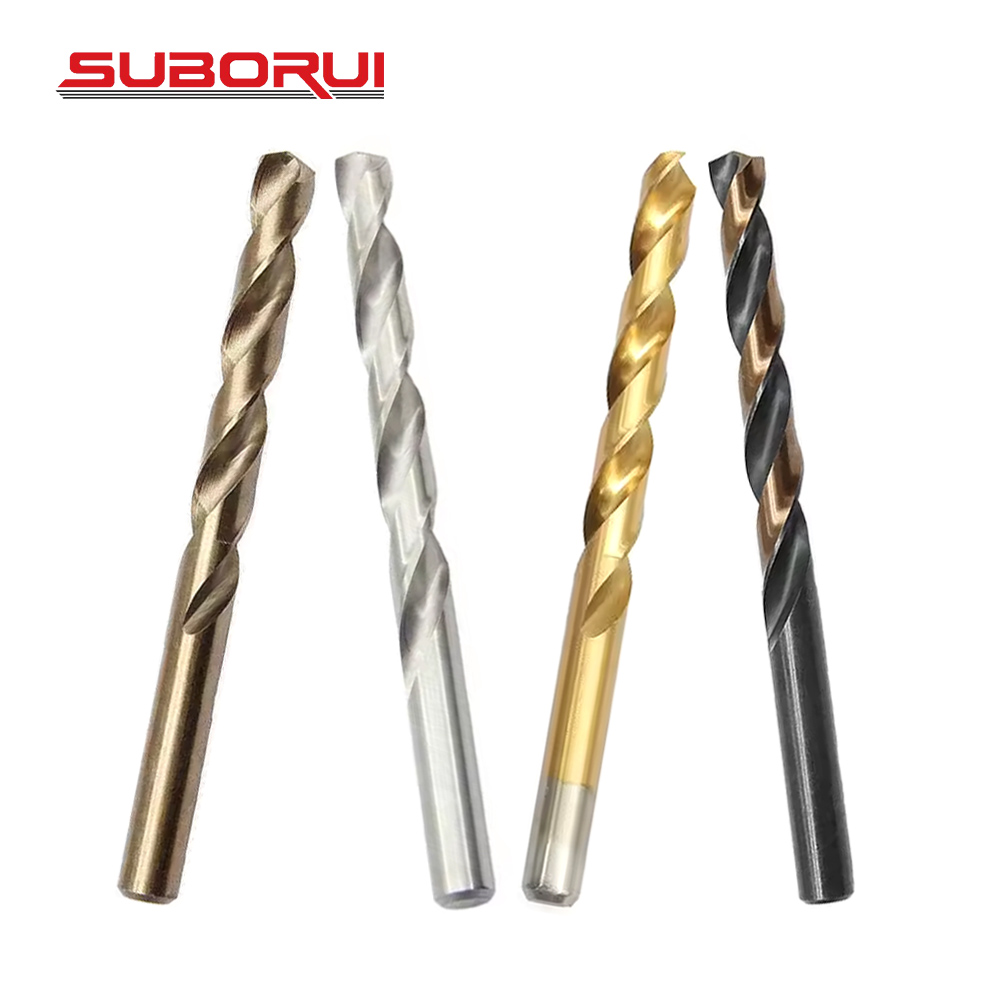
Surface treatments fundamentally determine edge adhesion tendencies, galling thresholds, and swarf clearance speeds. Our M35 bits are delivered in specialized heat-tempered bronze/amber oxide and physical vapor deposition finishes.
The amber bronze finish induces a micro-porous iron-oxide layer (Fe3O4) that acts as a reservoir for cutting emulsions, lowering the friction coefficient down to 0.35 against raw stainless steel and reducing built-up edge (BUE) formation.
- Flute Roughness: Ra < 0.2 µm via multi-axis CNC grinding
- Wear Longevity: Up to 3.8x longer working life vs. standard bright-finished M2
- Radial Run-Out (TIR): Maintained strictly within 0.02 mm across lengths
Metallurgical & Machining Parameters: Tool Selection Matrix
| Steel Grade Designation | Alloy Composition (Co-W-Mo-V) | Tempered Hardness | Recommended Feed / Vc (AISI 304) | Primary Industrial Sector |
|---|---|---|---|---|
| HSS 4241 | 0% Co, 1.5% W, 1.0% Mo, 1.0% V | 60 - 62 HRC | Not recommended (<8 m/min, rapid BUE) | DIY, Soft Timber, Plastics, Thin Al |
| HSS M2 (6542) | 0% Co, 6.0% W, 5.0% Mo, 2.0% V | 63 - 65 HRC | 12 - 15 m/min (High Flood Coolant Required) | General Structural Carbon Steels, Cast Iron |
| M35 Cobalt (HSS-Co5) | 5.0% Co, 6.0% W, 5.0% Mo, 2.0% V | 65 - 67 HRC | 18 - 25 m/min (Resists Thermal Softening) | Stainless Steels, Inconel, Titanium, Hard Tool Steels |
| M42 Cobalt (HSS-Co8) | 8.0% Co, 1.5% W, 9.5% Mo, 1.2% V | 67 - 69 HRC | 22 - 30 m/min (Demands High Machine Rigidity) | High-Volume Continuous Production, Bi-Metal Saws |
Regional Applications
Serving Bern’s Precision Manufacturing & Industrial Infrastructure
The Canton of Bern is an economic powerhouse defined by demanding precision engineering, medical technologies, railway manufacturing, and specialty machinery production. WRD Tools M35 cobalt twist drill bits provide deterministic tool life across regional manufacturing hubs.
⏱
Bernese Jura Watchmaking & Micro-Mechanics
In the Bernese Jura (Saint-Imier, Moutier, Biel/Bienne), small-diameter precision holemaking is paramount. Micro-turning and milling setups drilling watch cases, bezels, and complex movements fabricated from corrosion-resistant 316L, 904L, and grade 5 titanium require exceptional dimensional stability.
Our micro-precision ground M35 twist drill bits (down to 0.5 mm) maintain minimal run-out, ensuring tight hole diameter tolerances and clean entry margins that eliminate costly post-processing deburring passes.
🚆
Rolling Stock & Heavy Rail Fabrication
With major railway engineering operators and infrastructure suppliers headquartered and operating around Bern and Thun, structural steel drilling is subject to EN standards and strict Swiss safety guidelines. Drilling high-tensile bogies, chassis assemblies, and wear-resistant track switchgear involves abrasive wear plates and structural alloys.
M35 cobalt bits and annular cutters handle deep-hole operations in work-hardened rail sections without thermal fatigue, minimizing tool change downtime on busy assembly floors.
⚕
MedTech & Precision Surgical Equipment
Bern's medical cluster demands surgical-grade instrument fabrication using biomedical titanium alloys (Ti-6Al-4V) and high-nitrogen stainless steels. These materials generate immense localized cutting temperatures that immediately destroy standard drill flutes.
WRD Tools’ DIN 338 M35 cobalt drill bits deliver consistent heat rejection and sharp edge retention, ensuring zero metal contamination or grain tearing throughout sensitive production runs.
Strategic Outlook
Procurement & Tooling Trends Across Canton Bern (2025–2030)
Key economic and industrial factors dictating how purchasing directors and production leaders in Switzerland optimize supply chains and tooling inventories.
📈
Direct Factory Sourcing vs. Trading Hub Markups
Traditionally, Swiss toolrooms procured high-speed cutting tools through multi-tiered domestic distribution houses, incurring markups exceeding 200%. Today, leading industrial buyers across Bern and Mittelland establish direct ties with audited OEM/ODM manufacturers like WRD Tools to lower cost-per-hole while retaining custom DIN-standard packaging and shank branding.
⚡
High-Feed CNC Machining & Automation Integration
Automated manufacturing cells (Industry 4.0) operating unmanned night shifts across Bernese manufacturing clusters require predictable tool wear cycles. Unplanned tool breakages halt entire production lines. M35 Cobalt twist drill bits provide linear wear predictability, enabling precise integration with automatic tool management software and predictive replacement schedules.
♻
Sustainable Tooling & Extended Regrindability
In accordance with Swiss environmental standards and circular manufacturing mandates, consumable cutting tools must offer extended working life cycles. Our hot-rolled and precision CNC-ground M35 bits permit 5 to 8 professional resharpening cycles on standard web-thinning grinders without loss of core metallurgical hardness, cutting overall scrap rates.
Manufacturer Authority
Why Swiss Tool Importers Partner with WRD Tools
Operating from Danyang, China’s primary tooling hub, Jiangsu WRD Tools Co., Ltd. integrates 19 years of metallurgical heritage with audited European compliance.
Intertek Onsite-Audited Facility
Our 12,000 m² production facility, automated machinery lines, heat-treatment installations, and QA/QC inspection rooms are verified onsite by Intertek Group, ensuring comprehensive verification for Swiss customs compliance and quality validation.
High-Tech Enterprise Certified (2019)
Awarded official High-Tech Enterprise status in Jiangsu Province, our dedicated R&D team continuously refines flute geometries, flute polishing, vacuum heat-treatment algorithms, and specialized micro-grain coatings to match European industrial tooling standards.
Massive Scale & Fast Repeat Cycles
With an annual capacity exceeding 90 million units (50M wood drill bits, 25M twist drill bits, 15M hex-shank drills), our production scale ensures stable pricing, dedicated raw material reserves, and fast dispatch cycles for bulk private-label orders.
Supplying Global Industry Leaders
Over nearly two decades, our factory has consistently manufactured high-precision drill bits and cutting consumables for world-class tool brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Wolfcraft, and Heller.
End-to-End In-House Production
From metallurgical bar spectrography and bar cutting to automatic salt-bath hardening, precision 5-axis CNC grinding, laser marking, and custom injection-molded casing, every step remains 100% under our direct quality control.
Flexible OEM / Private Label Services
We tailor drill sets for Swiss distributors and retail channels: imperial/metric sets, industrial metal cases, blister pack designs, laser shank etching, and DIN-specified tolerance tolerances down to h8.
Procurement Knowledge
Frequently Asked Questions by Tooling Buyers in Bern
Detailed insights resolving technical, logistics, and compliance queries for Swiss industrial purchasing teams.
Q: What is the key performance difference between M2 (6542) and M35 Cobalt when machining in Bernese machine shops?
Standard HSS M2 is ideal for general structural steel (St37, St52) and cast iron up to 800 N/mm². However, Swiss precision fabricators frequently process austenitic stainless steels (1.4301, 1.4404) and high-tensile alloys where friction creates temperatures over 500°C. M35 (with 5% cobalt) retains its hardness up to 650°C, preventing cutting edge burn-out and increasing tool life up to fourfold under heavy feeds.
Q: Can WRD Tools supply drill bits according to DIN 338, DIN 340, and DIN 1897 standards with metric h8 tolerances?
Yes. All our industrial twist drill bits are ground on specialized multi-axis CNC grinding machines conformant to international DIN specifications. We routinely deliver DIN 338 (jobber series), DIN 340 (long series), DIN 1897 (stub series for automatics), and DIN 345 (Morse taper) with diameter tolerances strictly within the standard h8 class.
Q: What are the Minimum Order Quantities (MOQ) and lead times for Swiss distribution orders?
For standard loose industrial pack drill bits, our MOQ starts between 100 and 500 pieces per diameter. Complete boxed sets (such as 1–10 mm or 1–13 mm sets in metal or ABS cassettes) have an MOQ of 1,200 sets for custom-branded private labeling. Standard factory production lead times range between 25 and 35 days, with direct air freight options into Zurich/Geneva or consolidated sea shipments via Basel/Rotterdam.
Q: How do you guarantee consistent core hardness and split-point centering from batch to batch?
Every batch of raw HSS-Co5 steel wire undergoes optical emission spectroscopy and metallographic testing before cutting. Heat treatment is controlled in computer-monitored vacuum salt-bath furnaces, guaranteeing uniform through-hardness (65–67 HRC) rather than just surface case hardening. Optical comparators and laser micrometers inspect split-point concentricity and run-out across every batch.
Q: Can our custom Swiss company branding, EAN barcodes, and laser marking be accommodated?
Yes. We offer turnkey OEM/ODM services. We laser-etch your brand logo, specific material grade (e.g., "HSS-G Co 5%"), and diameter directly on drill shanks. Furthermore, we manufacture customized bilingual packaging (German/French) complete with Swiss recycling symbols, GTIN barcodes, and custom-designed metal index cassettes.
Q: What cutting speeds and feed rates are recommended when running M35 bits in CNC machines?
When cutting standard 304/316 stainless steels with M35 bits, we advise a cutting speed (Vc) of 15–22 m/min with constant feed per revolution (0.04 mm/rev for ø3 mm; 0.12 mm/rev for ø10 mm). Maintaining continuous positive mechanical feed is essential: dwelling or rubbing in work-hardening stainless will prematurely glaze the material and dull the cutting edges.
Request Technical Samples or an OEM Quotation
Supply your target diameters, quantities, coating preferences, or technical drawings. Our experienced international export team will provide a comprehensive engineering review and FOB/CIF pricing within 24 hours.