Industrial Precision Tooling
Featured Industrial Cutting Tools & Tooling Range
Engineered in our verified 12,000 m² production facility with stringent quality controls. Browse our featured portfolio or consult our tool designers for custom spiral flute tap solutions engineered precisely to your manufacturing specifications.




2007
Established Year
12,000 m²
Modern Manufacturing Plant
90M+
Annual Tool Output
20+
Export Destination Countries
Technical Insights & Manufacturing Mastery
Engineering Superior Spiral Flute Machine Taps for Demanding Markets
Blind hole internal thread tapping remains one of the most mechanically demanding metal-cutting operations. Our precision spiral flute taps are designed specifically to overcome chip packing, thread tearing, and micro-chipping in high-speed CNC environments.
Optimized Helix Angle Selection
We configure 15°, 35°, and aggressive 45° right-hand spiral helix angles to accommodate diverse material elongations. A 45° fast spiral ensures rapid, continuous upward chip evacuation in deep blind holes, preventing chip packing that causes catastrophic tool fracture in Austrian automated machining cells.
Advanced Substrate Formulations
Fabricated using select high-speed steels: HSS M2 (6542) for cost-effective standard steels; M35 with 5% Cobalt (HSSE) delivering exceptional red-hardness; and Powder Metallurgy (HSS-PM) providing ultra-uniform carbide distribution for extreme toughness and extended tool life when cutting high-tensile alloys.
Engineered PVD Thin-Film Coatings
Available with proprietary TiN, TiCN, and multilayer TiAlN/AlTiN coatings tailored for elevated thermal barriers up to 900°C. Optimized surface finishing lowers friction coefficients down to 0.35, preventing adhesive built-up edge (BUE) in abrasive stainless steels and structural alloys.
Strict Adherence to DIN Standards
Manufactured under rigorous compliance with DIN 371 (reinforced shank for small threads M2-M10) and DIN 376 (reduced shank for through-reach threading up to M36). We execute 6H and 6G pitch diameter tolerance grinding on 5-axis CNC grinding centers to deliver exact interchangeability.
Complete Chamfer Form Customization
Precision CNC flute and chamfer grinding offering Form C (2-3 threads) for universal blind holes and Form E (1.5-2 threads) for shallow blind hole bottoms. Specialized back taper relief geometry minimizes contact area, drastically decreasing rotational frictional torque during thread reversal.
Custom OEM Shank & Private Labeling
Supporting non-standard shank diameters, Weldon clamping flats, ANSI shanks with DIN dimensions, high-contrast fiber laser marking for corporate branding, barcode identification, and customized packaging ranging from single-unit telescopic tubes to industrial multi-packs.
| Substrate Material | Composition (Key Elements) | Hardness (HRC) | Optimal Application Scenarios | Primary Industrial Sector |
|---|---|---|---|---|
| HSS M2 (6542) | W6Mo5Cr4V2 | 63 – 65 | Structural steels up to 850 N/mm², cast iron, non-ferrous metals | General mechanical fabrication & light machinery |
| HSSE Cobalt (M35) | W6Mo5Cr4V2Co5 | 65 – 67 | Stainless steels (1.4301, 1.4404), alloy steels up to 1000 N/mm² | Austrian automotive components & powertrain parts |
| HSS-PM (Powder Met) | Proprietary Co-V Alloy | 66 – 68 | Heat-resistant superalloys, titanium alloys, hard steels >1100 N/mm² | Aerospace, rail engineering, alpine heavy transport |
Austrian Market Focus
Localized Application Scenarios in Austria's Industrial Corridors
Austria represents a central European powerhouse of specialized mechanical engineering, high-tier automotive systems, alpine ropeway infrastructure, and renewable energy technology. WRD Tools delivers custom spiral flute machine taps engineered specifically to satisfy strict Austrian quality expectations.
Automotive Cluster (Styria & Upper Austria)
Centres around Graz, Steyr, and Linz demand tight-tolerance blind-hole threading for powertrain castings, transmission cases, and chassis brackets. Our HSSE M35 spiral flute machine taps resist abrasive wear in nodular cast iron (GJS) and die-cast aluminum alloys, providing process security across multi-station transfer lines.
Alpine Engineering & Cable Car Systems
Supplying specialist manufacturers in Vorarlberg, Tyrol, and Salzburg. Ropeway structural nodes, ski-lift grip housings, and snowcat hydraulic blocks rely on alloy steels like 42CrMo4 and 34CrNiMo6. WRD spiral taps offer custom core diameters that eliminate micro-cracking in high-tensile fasteners exposed to sub-zero alpine fatigue.
Specialty Stainless Steel & Hydro Turbine Fabricators
Austrian flow-control and hydropower engineers in Lower Austria utilize high-alloy austenitic and duplex stainless steels (1.4404, 1.4462). Our specialized spiral flute taps with staggered cutting teeth, enhanced coolant through-channels, and TiAlN coatings stop work-hardening and friction weld galling during deep blind hole threading.
Industry Evolution
Procurement Trends & Tooling Dynamics in Austria
Austrian industrial buyers operate under increasing competitive pressure, navigating Industry 4.0 automation, energy cost management, and the European Union’s supply chain sustainability directives.
High-Speed Synchronous Tapping (Rigid Tapping)
Modern CNC machine tools across Austria operate high-speed synchronous tapping cycles. This mandates exceptionally low radial runout (<0.005 mm) and consistent thread profile accuracy. Suppliers must deliver precision-ground square drives and shank concentricity to prevent machine spindle overload.
Supply Chain Diversification & Direct Factory Partnerships
Austrian purchasing executives (Einkaufsleiter) are actively bypassing multi-tier regional brokers to partner directly with verified OEM tool manufacturers. Direct technical communication shortens development cycles for custom thread cutters while significantly reducing per-hole production costs.
Stringent Compliance & Material Traceability
Austrian manufacturers require full mill test certification, compliance with European REACH and RoHS standards, and consistent tool life batches. Reliable factories must demonstrate automated optical inspection (AOI) and comprehensive batch serialization from raw bar cutting to finished coating.
OEM / ODM Manufacturing Strength
Why European Tool Brands & Austrian Buyers Partner With WRD Tools
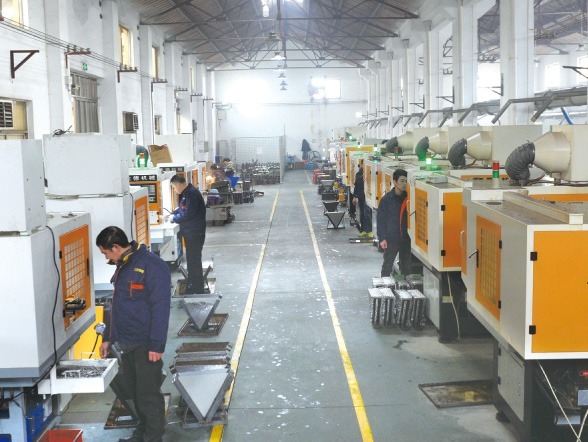
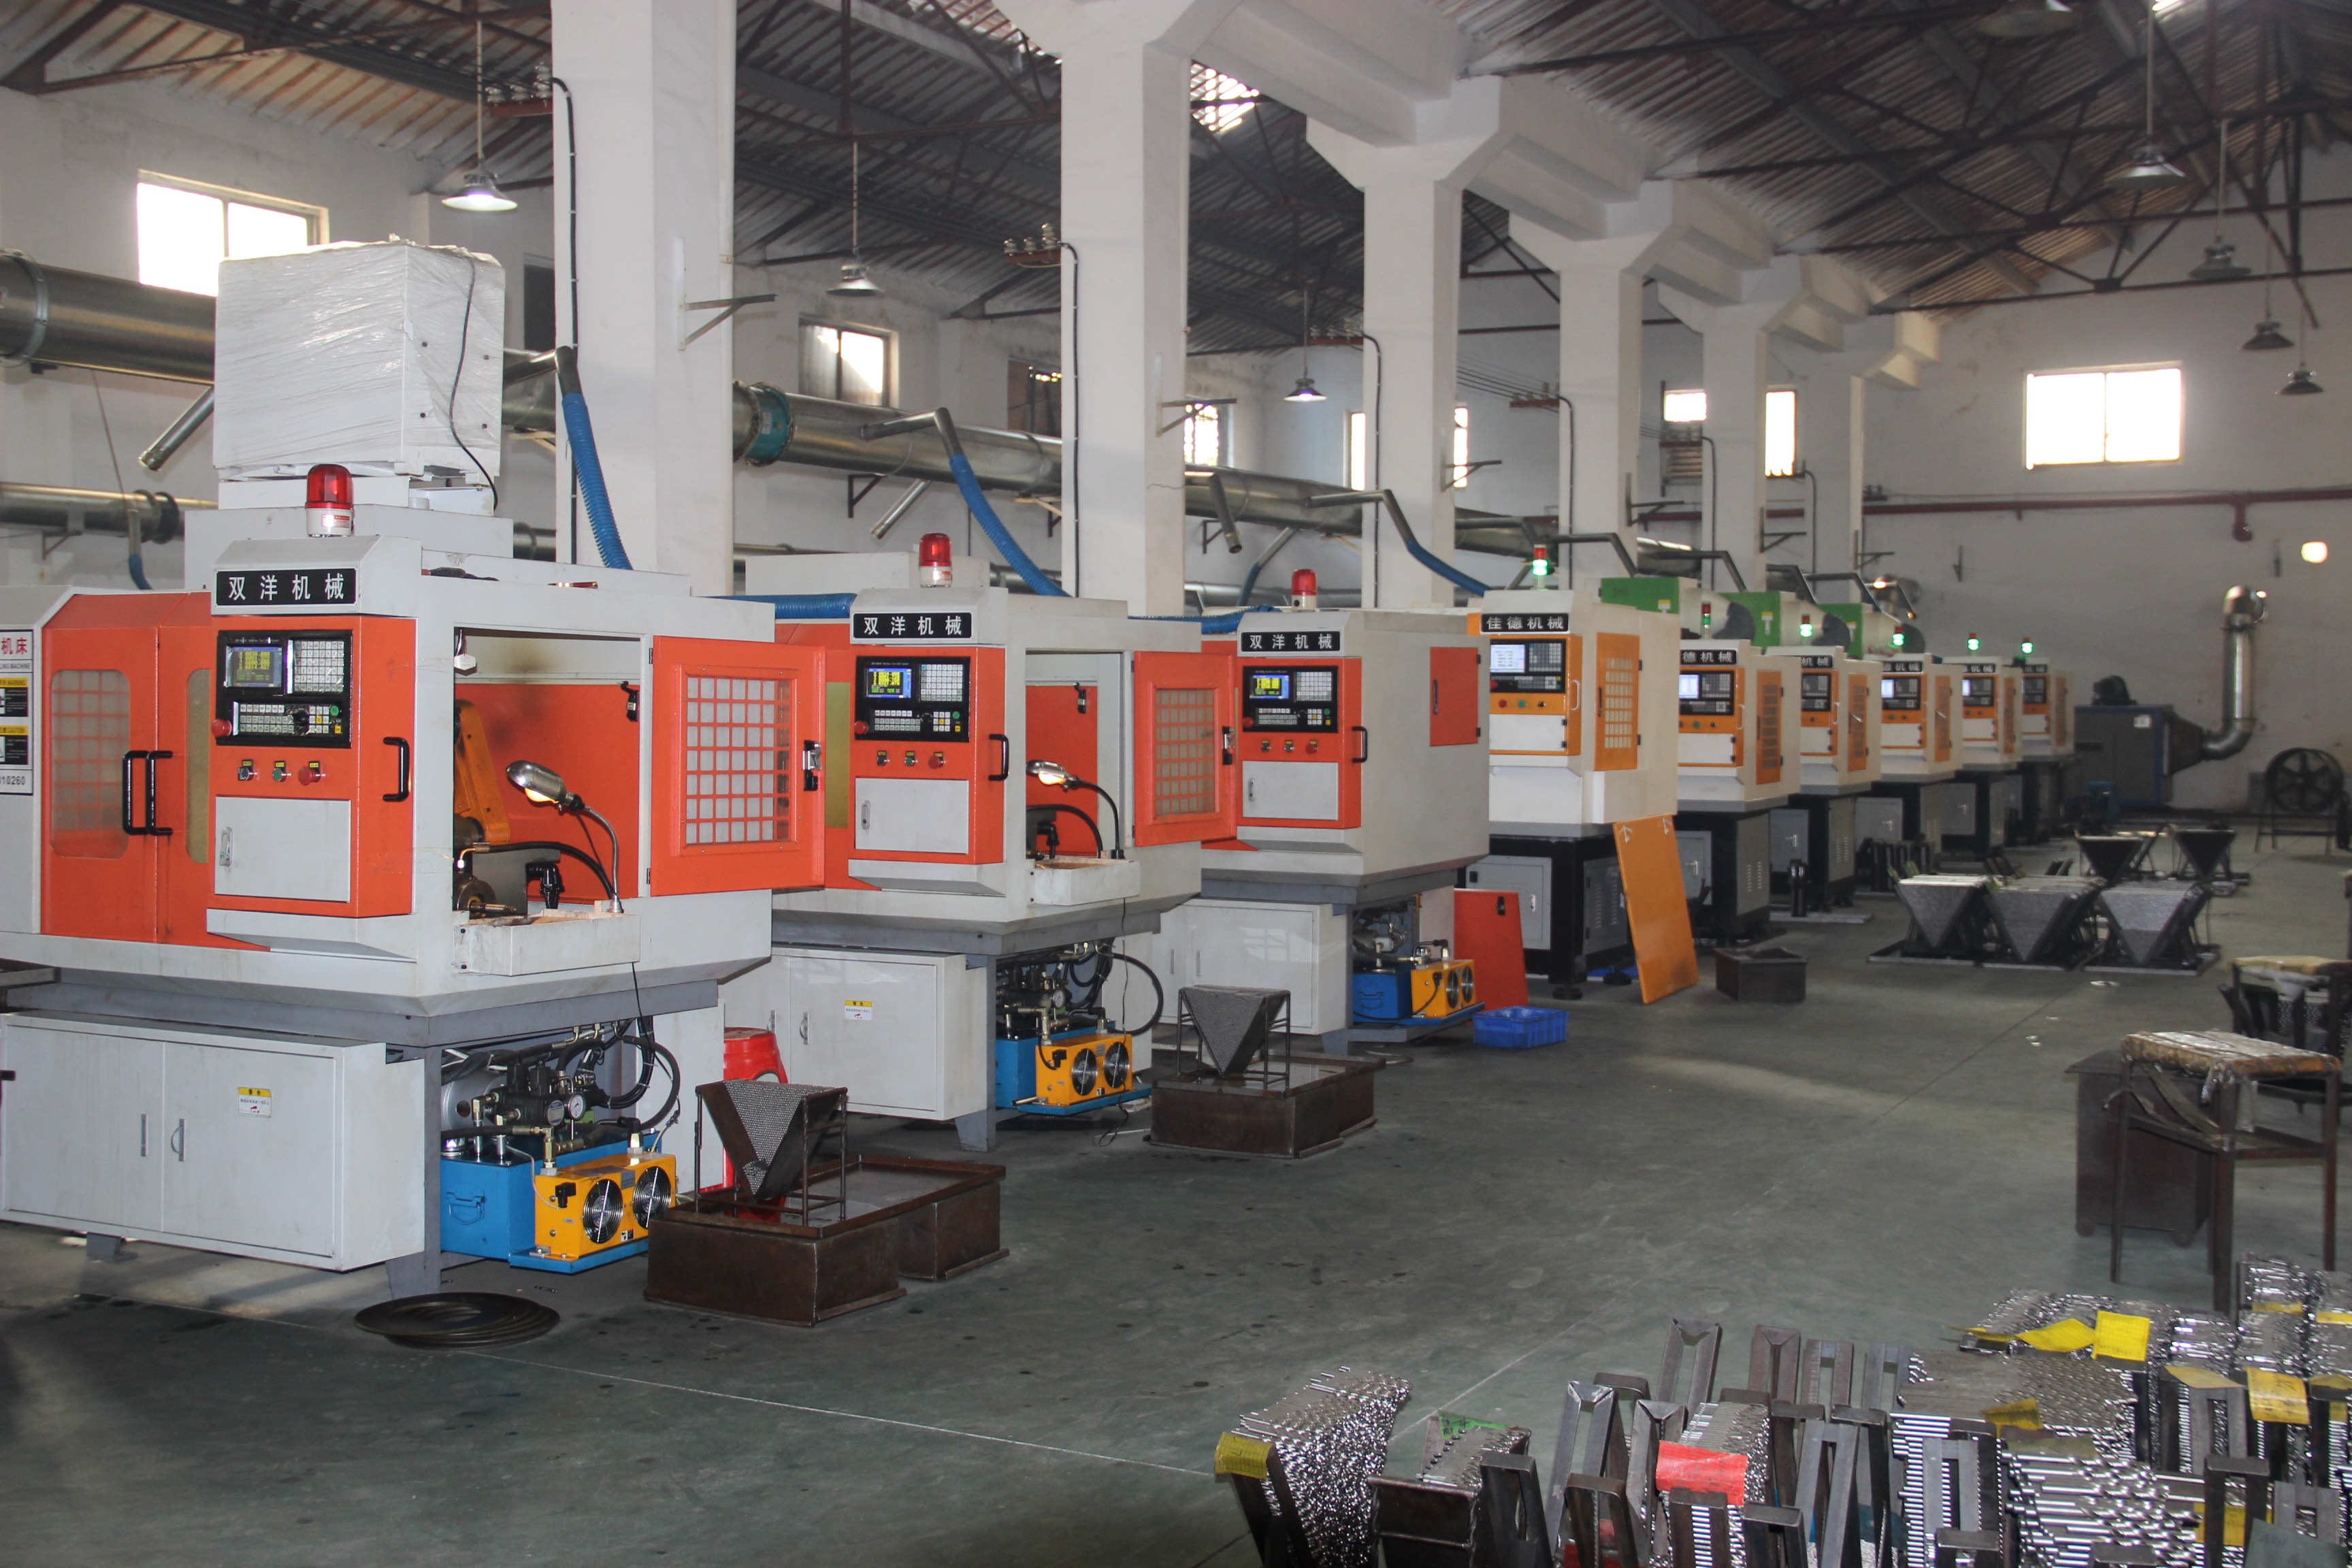
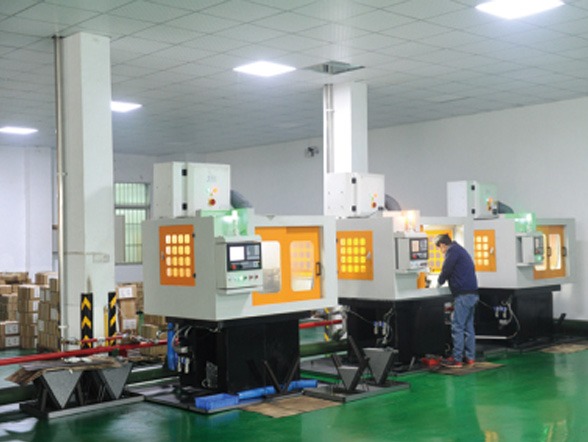
Jiangsu WRD Tools Co., Ltd. was established in March 2007 with a registered capital of RMB 10 million. Located in Danyang — China's largest cutting tool manufacturing hub — our 12,000 m² modern production base is staffed by over 150 highly skilled toolmakers and technicians.
Intertek Onsite-Verified Facility
Our production premises, quality management system, and end-to-end testing laboratory have been independently audited and verified on-site by Intertek Group. Recognized as a High-Tech Enterprise of Jiangsu Province in 2019, our testing labs ensure continuous quality consistency across every production run.
Complete In-House Process Control
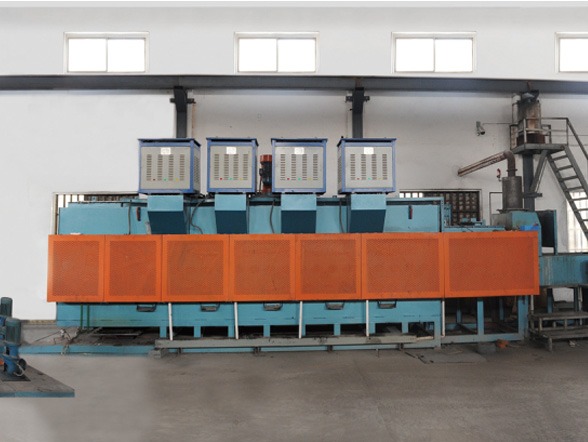
We do not operate as intermediaries or traders. From spectroscopic raw bar metallurgical verification and computerized salt-bath/vacuum heat treatment to 5-axis CNC flute grinding and PVD coating, every step is executed within our own specialized workshops, enabling strict DIN tolerance execution.
Trusted by Premier Global Tool Brands
WRD Tools maintains an established OEM manufacturing track record, producing cutting tools and accessories for renowned industry leaders including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller. Our annual sales surpassed RMB 80 million with exports spanning over 20 nations.
Frequently Asked Questions
Purchasing & Technical Queries from Austrian Buyers
Clear, direct answers regarding custom spiral flute machine tap procurement, lead times, European standards compliance, and logistics to Austria.
Q: How do your custom spiral flute taps comply with Austrian ÖNORM and DIN standards?
All machine taps manufactured for Austrian clients strictly comply with DIN 371 (M2-M10 reinforced shank) and DIN 376 (M12-M36 reduced pass-through shank), featuring ISO 2 (6H) or ISO 3 (6G) thread pitch tolerances. Thread profiles are ground on computerized thread grinding machines to guarantee 100% compliance with Austrian industrial norms.
Q: What is the Minimum Order Quantity (MOQ) for custom OEM spiral flute machine taps?
For standard DIN catalog tap dimensions with custom laser branding and private labeling, our MOQ starts at 100 pieces per size. For fully customized tool geometries (specialized pitch, non-standard helix angles, or powder metal substrates), the minimum production batch is generally 300 to 500 pieces, accommodating sample approval beforehand.
Q: Which HSS grade and coating do you recommend for Austrian automotive stainless steel machining?
For austenitic stainless steels like 1.4301 (AISI 304) and 1.4404 (AISI 316L), we recommend our HSSE M35 substrate (5% cobalt) or HSS-PM paired with a high-lubricity TiCN or TiAlN coating. We apply a 40° to 45° spiral helix angle with back taper relief to eliminate built-up edge and ensure rapid upward chip discharge.
Q: What are the standard delivery lead times and customs logistics solutions to Austria?
Standard OEM production lead times range between 25 and 35 working days after drawing confirmation. For Austrian consignees, we offer flexible shipping arrangements: direct air freight (5-7 business days to Vienna Schwechat VIE Airport) for urgent tool replenishment, or sea/rail multimodal transport (DAP/DDP terms available) via European ports or China-Europe Railway Express.
Q: Can you supply customized packaging, laser etching, and private labeling for our brand?
Yes. We provide complete private-labeling capabilities: high-precision fiber laser marking of your brand logo, thread specification, and batch number on the tap shank, alongside customized packaging including individual color-coded plastic sleeves, branded cassette sets, barcode labels, and custom outer master cartons.
Q: How is metallurgical consistency and quality verified before dispatch?
Each steel heat lot undergoes spectroscopic analysis to ensure chemical grade integrity. Post heat-treatment hardness is verified via calibrated Rockwell testers (HRC 64-67). All finished threads are 100% inspected using automated optical measuring systems and verified against precision thread plug gauges before ultrasonic cleaning and packaging.