
Direct Factory Catalog
Specialized Cutting & Drilling Tool Solutions
Engineered for endurance in duplex stainless steels, aero alloys, hard ceramics, and heavy structural modules. Fully customizable with Intertek verified tolerances.
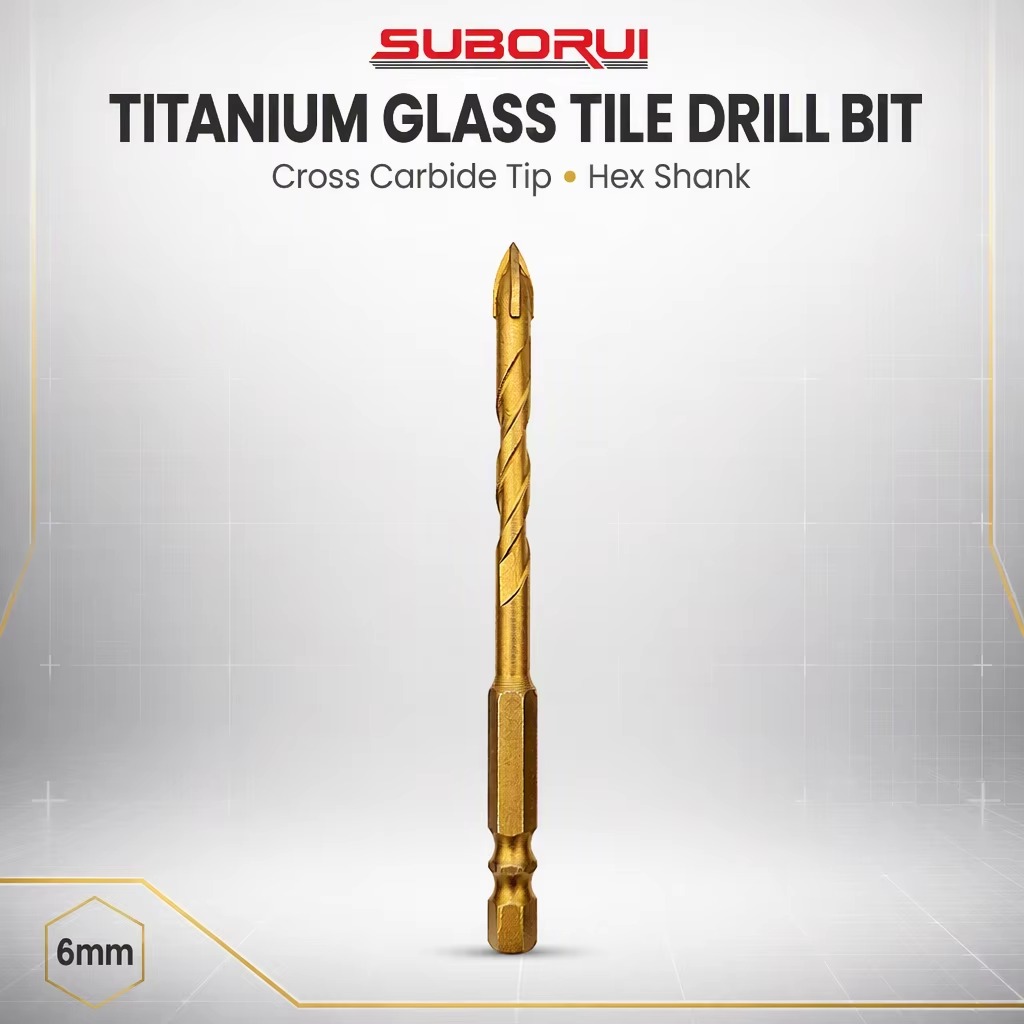
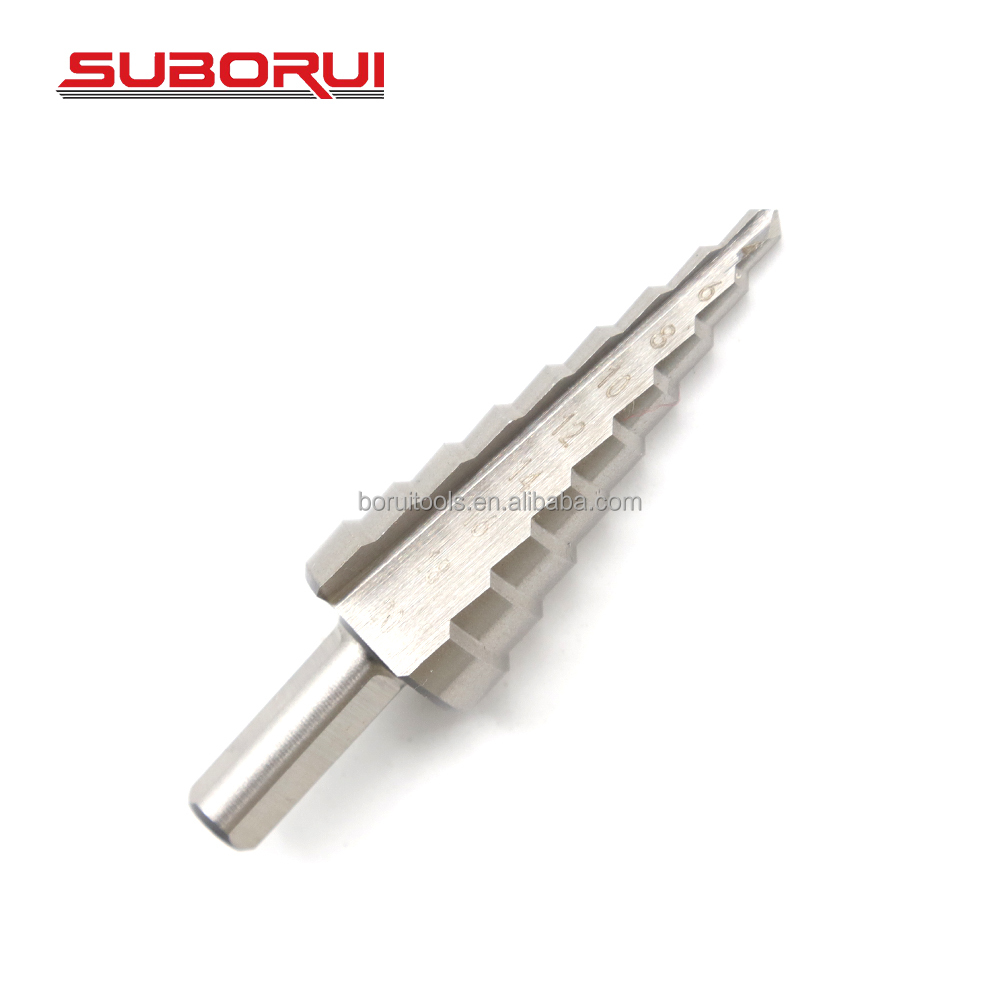


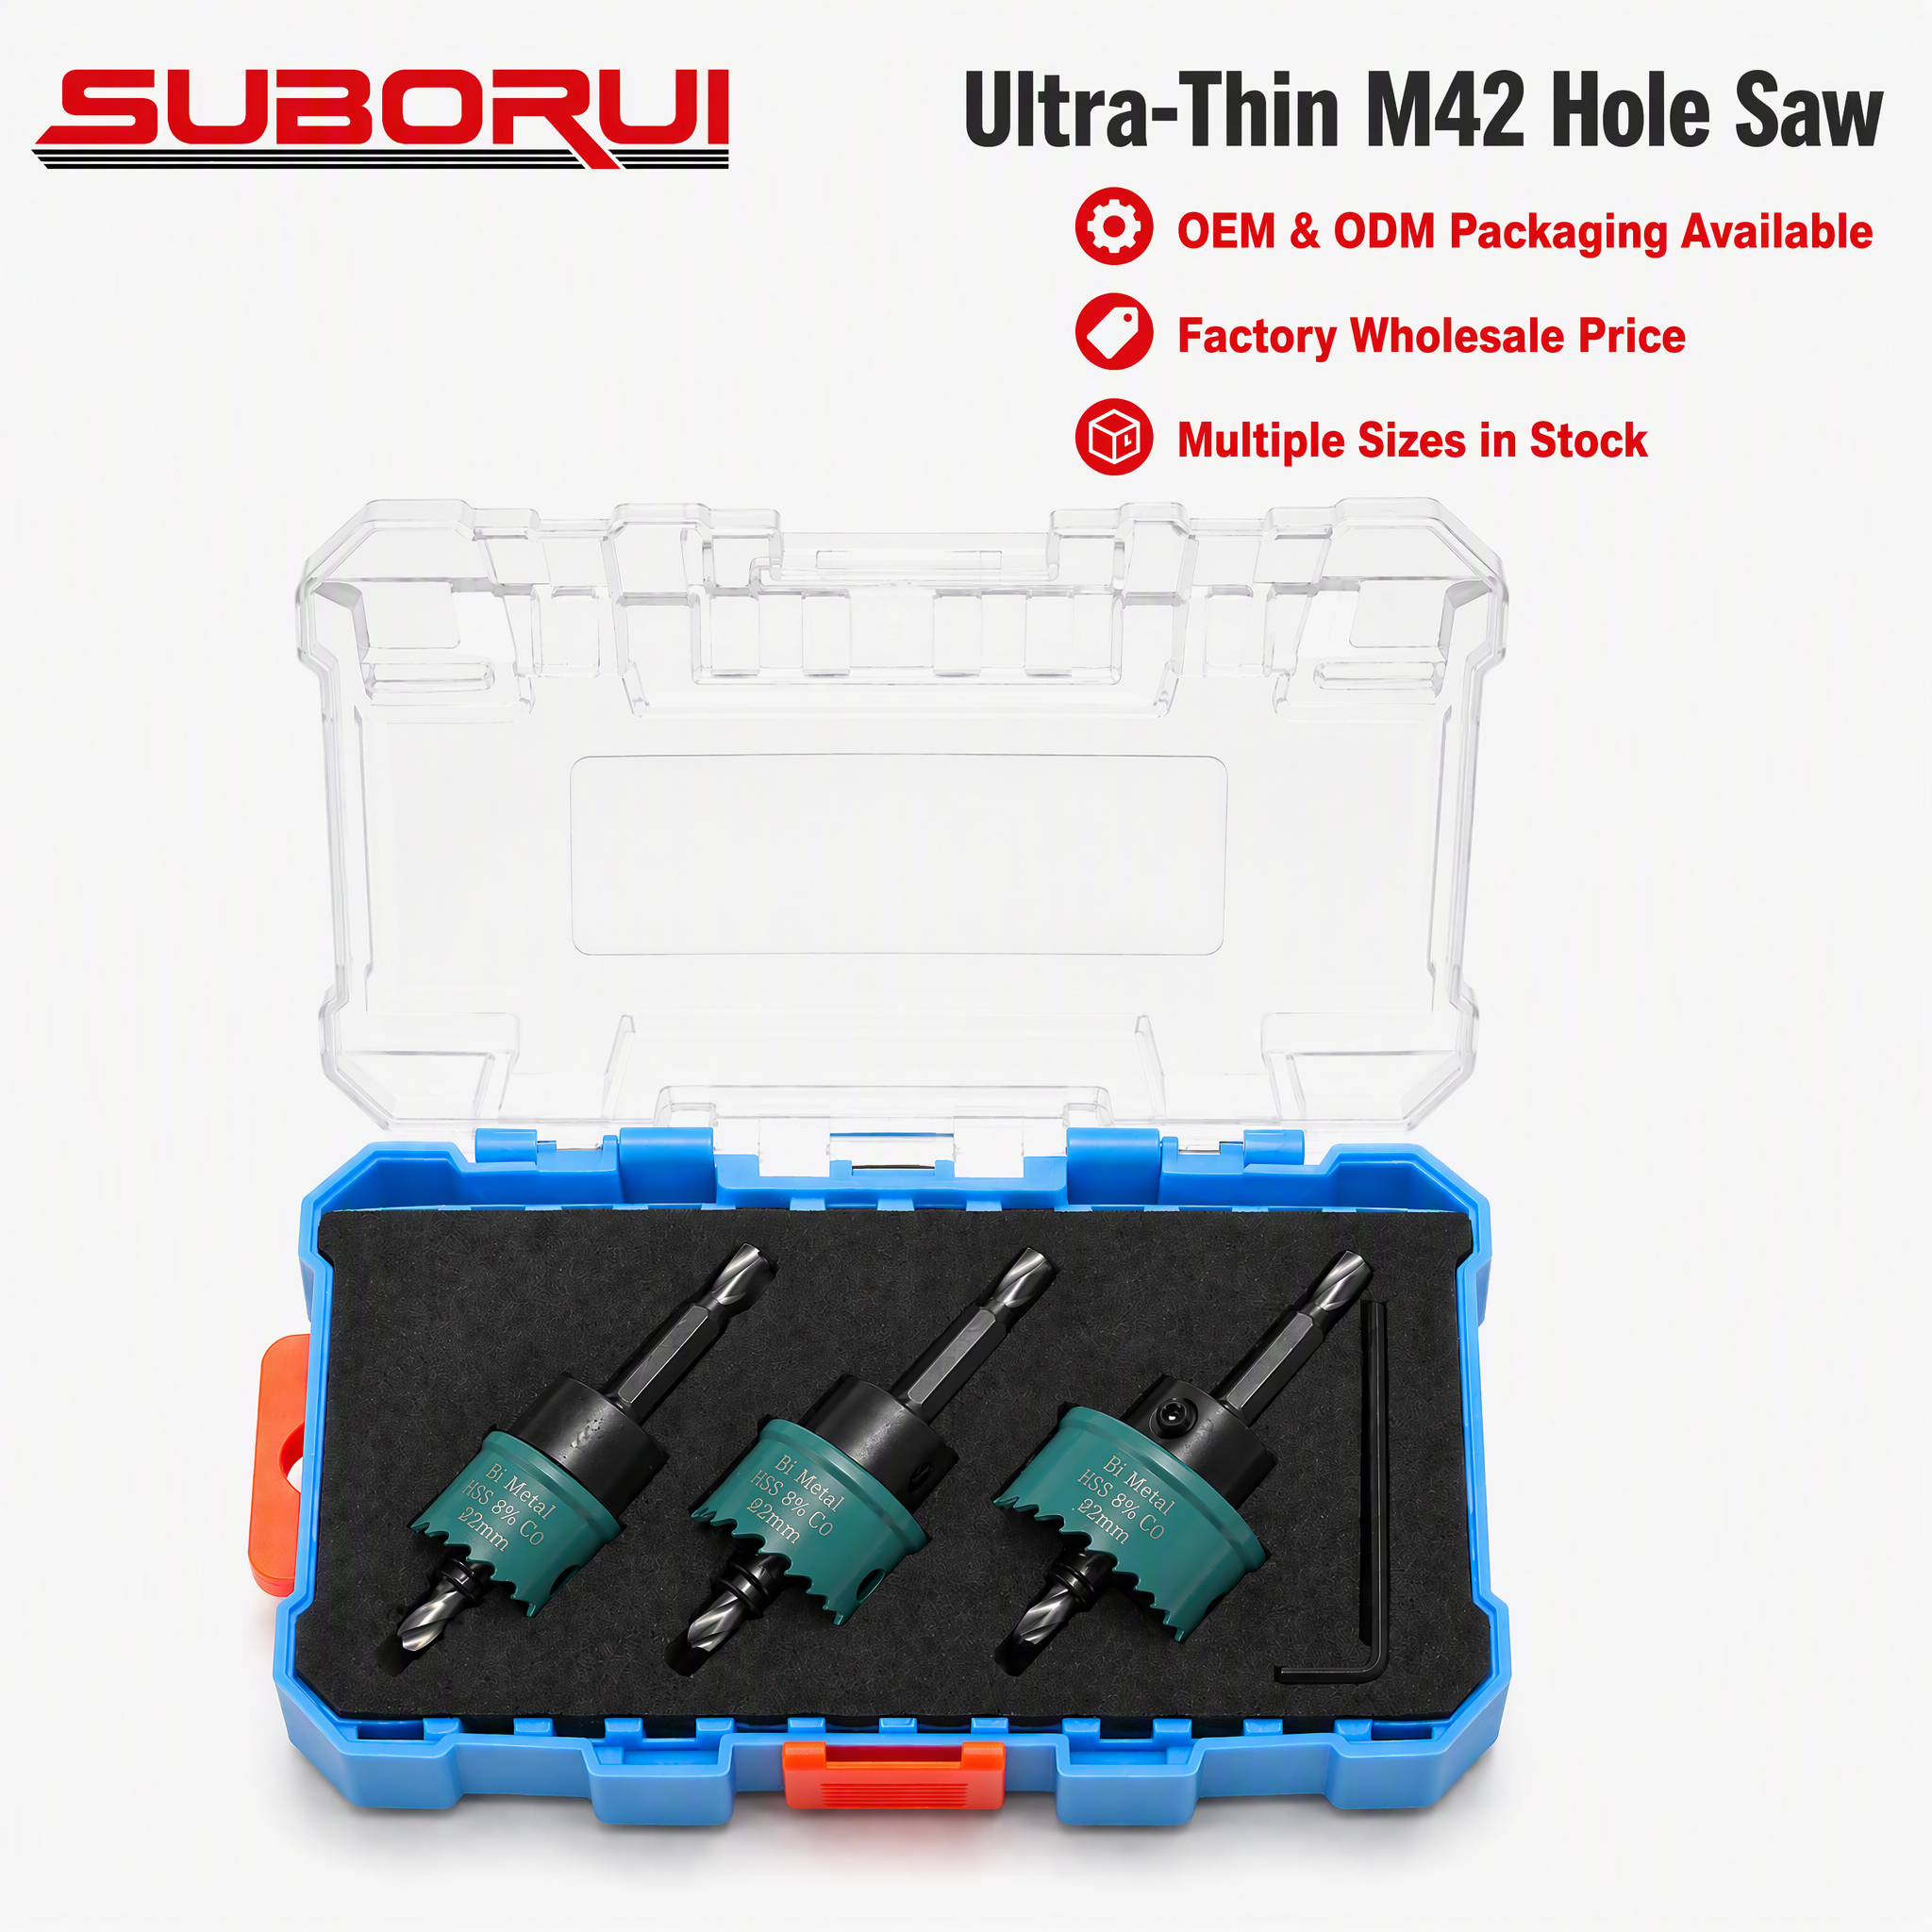
2007
Established Plant
12,000 m²
Factory Floor
150+
CNC Specialists
90M
Annual Tool Yield
20+
Export Nations
4.7 / 5
Verified Audit Score
Industry Whitepaper Analysis
Precision Deep-Hole Drilling Dynamics for High-Tech Substrates
Evaluating chip evacuation, torsional rigidity, runout mechanics, and thermal gradients in high aspect-ratio industrial hole-making.
In precision machining paradigms—particularly across Brainport Eindhoven's high-tech manufacturing nexus—deep-hole drilling (defined operationally as holes exhibiting depth-to-diameter ratios exceeding 10:1 up to 50:1) presents formidable physical hurdles. As length-to-diameter (L/D) quotients rise, conventional drill bit flutes encounter exponential friction, severe chip packing, vibration harmonics, and elevated core heat. For procurement specialists and tooling engineers in the North Brabant province, sourcing drills capable of sub-micron concentricity while processing difficult-to-cut superalloys (such as Inconel 718, Hastelloy, Titanium Grade 5, and austenitic 316L/316LVM) requires a direct manufacturing partner possessing advanced metallurgy, vacuum heat treatment mastery, and specialized micro-geometry engineering.
"Torsional resonance and flute micro-geometry are decisive factors in deep-hole precision. Without parabolic flutes, optimized web thinning, and PVD titanium-aluminum nitriding, tool deflection compromises clean-room tolerance thresholds."
Parabolic Flute Geometry
Engineered with enlarged chip cross-sections and smooth ground gullets to ensure rapid evacuation of elongated ductile swarf without micro-chipping or thermal expansion binding.
135° Self-Centering Split Point
Eliminates center wander and work-hardening during initial penetration. DIN 1412 Form C split points significantly reduce thrust force requirements in rigid CNC setups.
AlCrN / TiAlN PVD Coatings
Thermal barrier coatings maintaining structural micro-hardness at operating temperatures up to 900°C, drastically minimizing friction coefficients inside deep blind conduits.
Regional Industrial Integration
Deep Hole Tooling in the Eindhoven Ecosystem
From Veldhoven's photolithography assemblies to Helmond's e-mobility corridors, our custom deep hole bits power mission-critical operations.
Eindhoven represents the industrial heart of European high-precision technology. Tier-1 and Tier-2 suppliers supporting photolithography leaders like ASML, semiconductor packaging plants in Best, and mechatronic equipment builders across the Brainport Industries Campus (BIC) require specialized deep hole drills capable of meeting exceptional standards. These tools are engineered to machine fluidic manifolds, extreme vacuum (UHV) conduits, hydraulic cooling galleries, and high-frequency sensor mountings where zero internal burrs and zero chip contamination can be tolerated.
| Application Sector | Common Materials | Tool Specifications | Performance Target |
|---|---|---|---|
| Lithography Fluidics & Chambers | AISI 316L, 1.4404, Titanium Gr 5 | M35 Cobalt / Solid Carbide DIN1869 Extra Long | Straightness <0.05mm/300mm, Ra <0.8µm internal wall |
| E-Mobility & Automotive (Helmond) | AlSi10Mg, Ductile Cast Iron, 42CrMo4 | Subland Step Drills, Annular Multi-Tooth Systems | High feed rates (>0.25mm/rev), cycle time reduction 40% |
| Medical Instrumentation (Best/Son) | PEEK, Titanium Grade 23, 17-4PH | Micro Deep Hole Drills, Cross-Carbide Tips | Burr-free exit profile, biocompatible cutting chemistry |
| Heavy Tooling & Mold Plates | Tool Steel P20, 1.2379 (D2), Hardox 450 | TCT Annular Cutters & Extra-Length Jobber HSS | Thermal resistance against friction work-hardening |
UHV Vacuum Conduits
Long reach, parabolic bits deliver chatter-free drilling for ultra-high vacuum cooling circuits requiring zero particulate residue.
Tooling Manifolds
Custom metric Morse taper and straight-shank extended drills engineered for cross-drilled hydraulic blocks without drill wandering.
Precision Metrology Rigs
Stable core webbing provides axial stiffness for high-tolerance sensor probe guides and optical housing fixtures.
Additive Finishing
Clean clearing of deep core powder voids in DMLS additive manufactured components without abrasive tool wear.
Strategic Sourcing Trends
Procurement Trajectories in North Brabant
Key evolutions driving Dutch procurement managers away from intermediaries toward direct OEM factory partnerships.
Supply Chain Redundancy & Dual-Sourcing
Eindhoven precision machine shops are migrating toward direct factory tie-ups to safeguard supply chains against European tool distributor markups and inventory bottlenecks.
Tightened ESG & CBAM Verification
Dutch buyers demand complete material trace records. Our verified metallurgical documentation matches ISO and European Carbon Border Adjustment Mechanism (CBAM) logging mandates.
Demand for Custom Non-Standard Tooling
Off-the-shelf catalog tools often fall short in specialized mechatronic prototypes. Engineering buyers require rapid-turnaround custom geometries, stepped lands, and proprietary shank fittings.
Manufacturing Powerhouse
Why Global Brands & OEMs Trust WRD Tools
Jiangsu WRD Tools Co., Ltd. (Suborui) brings 19 years of verified production leadership from China’s largest cutting-tool cluster.
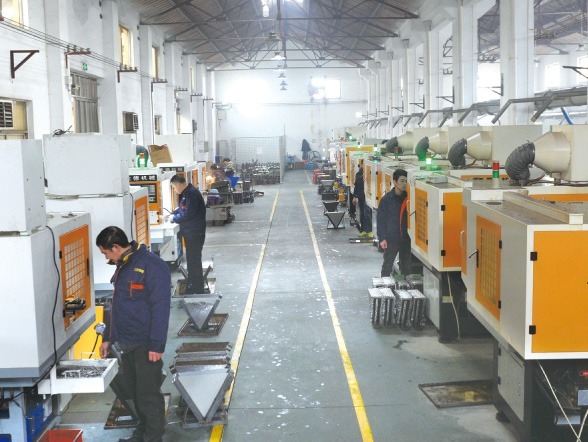
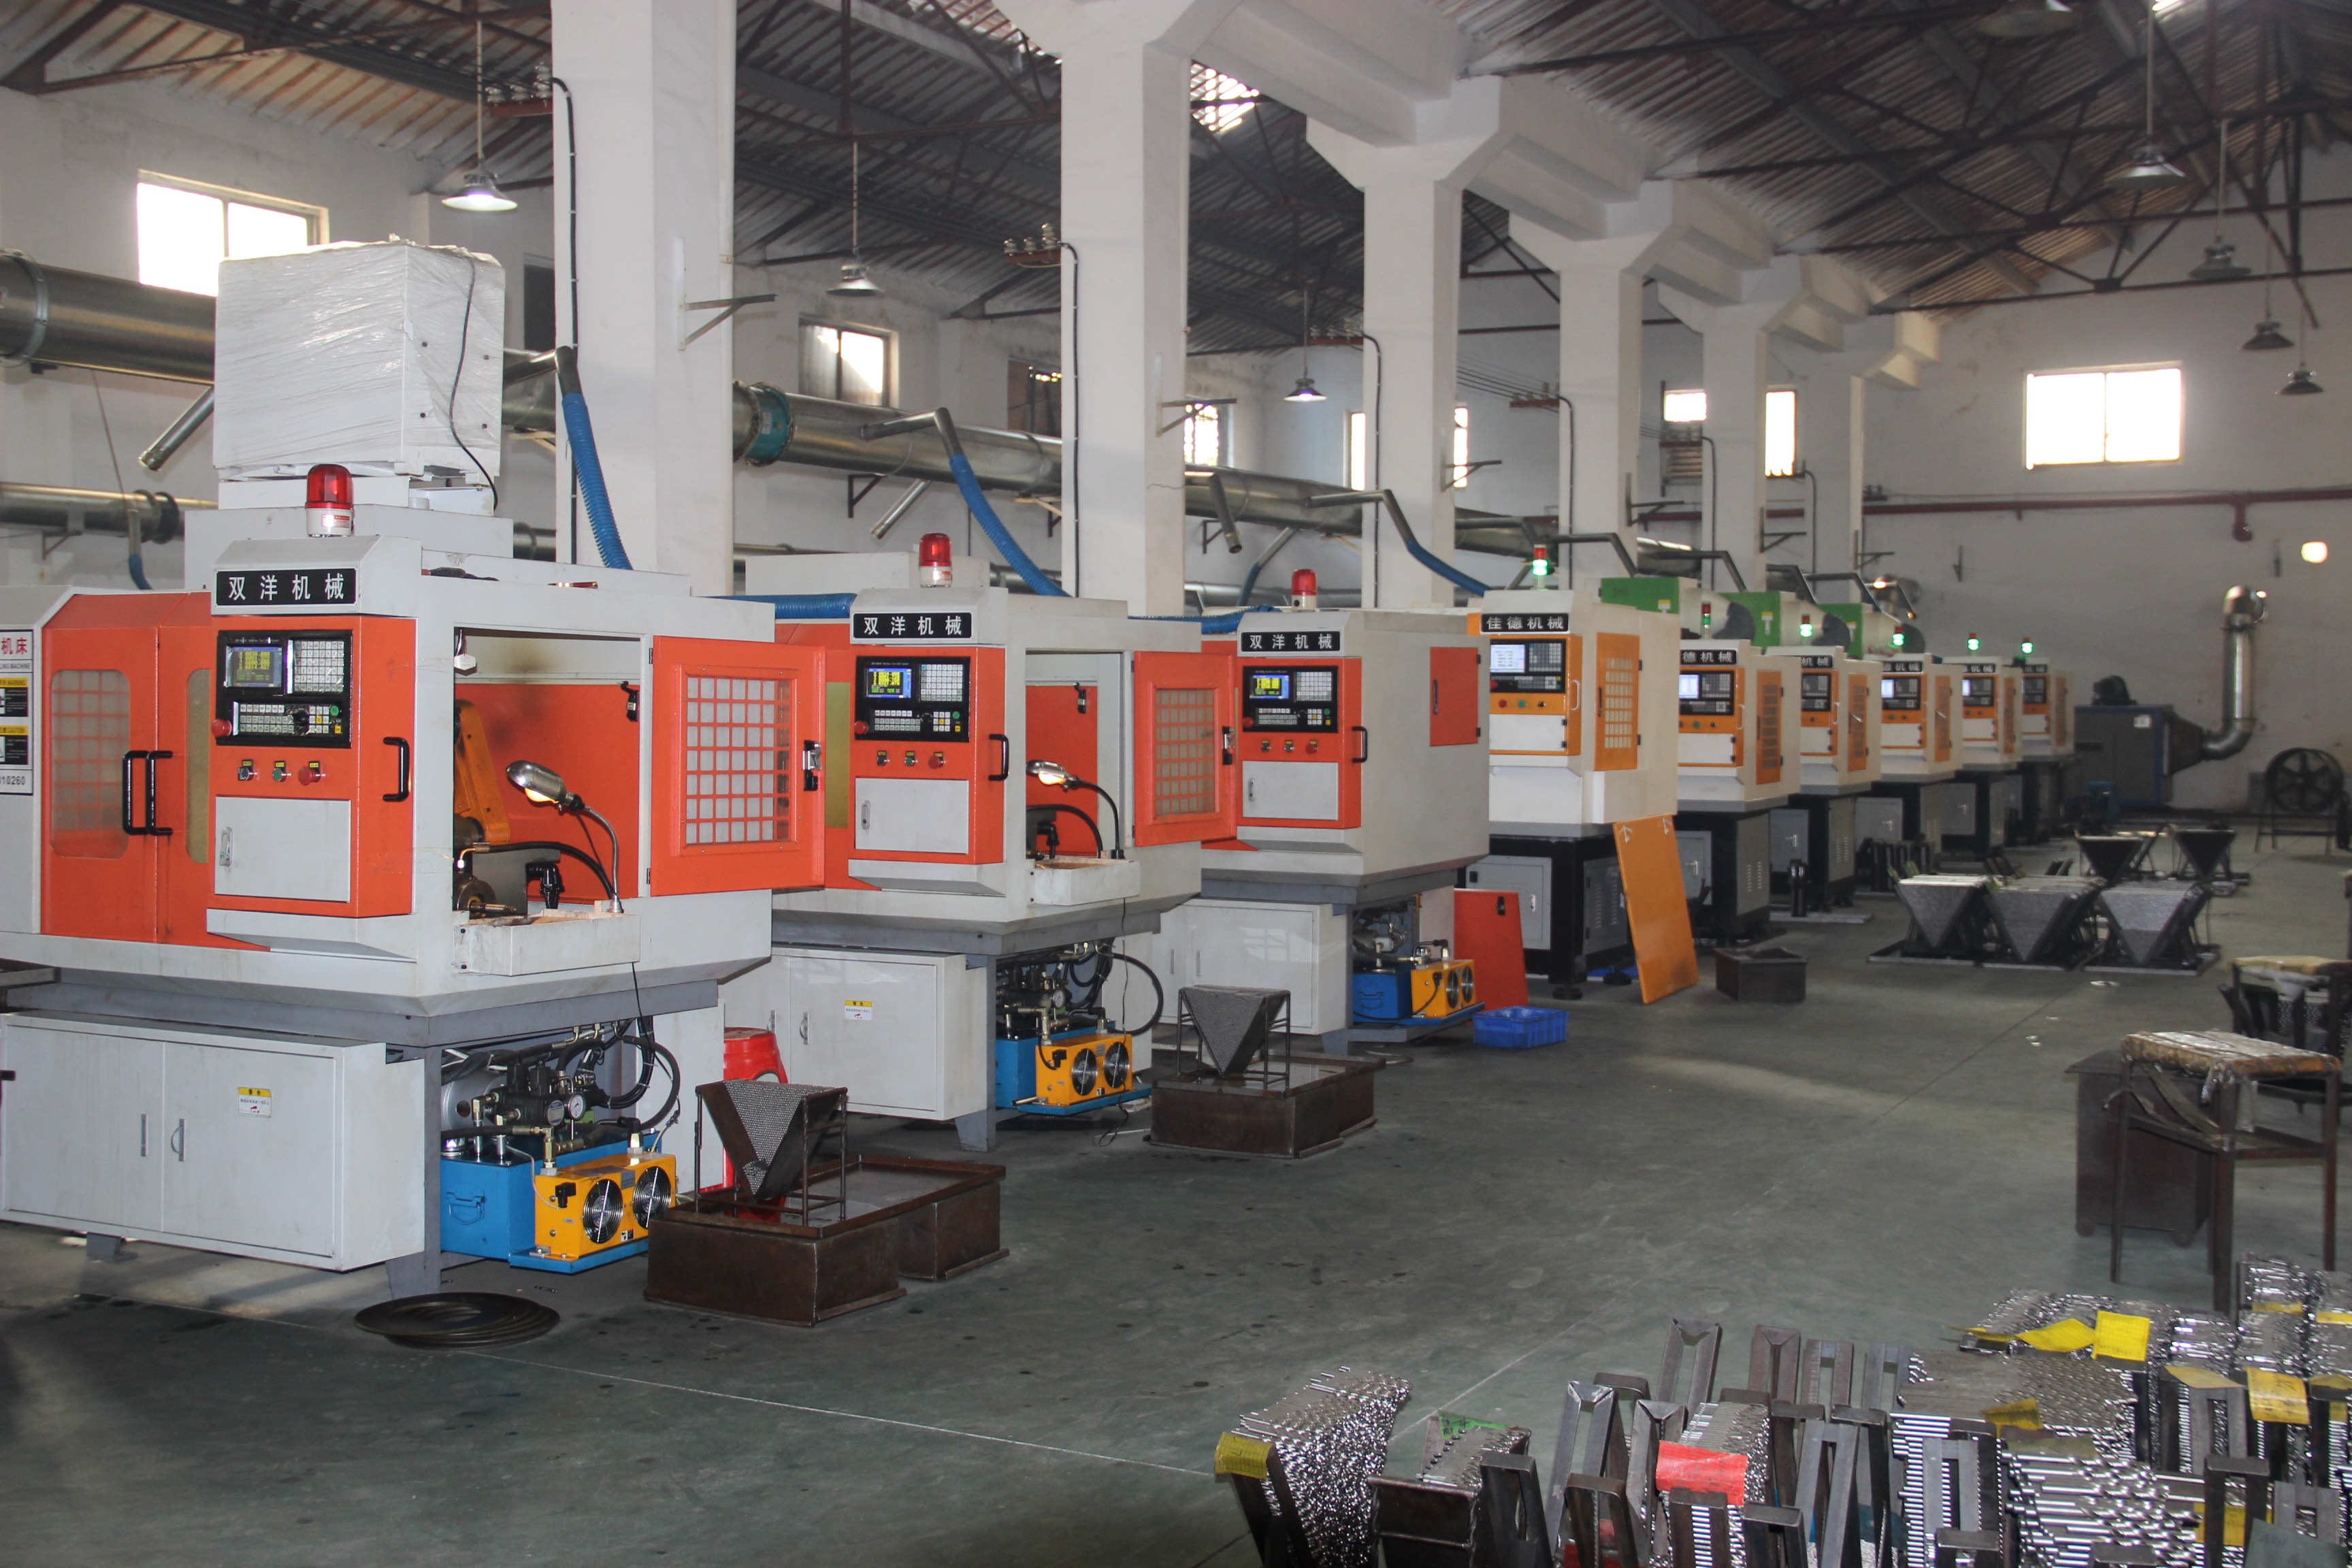
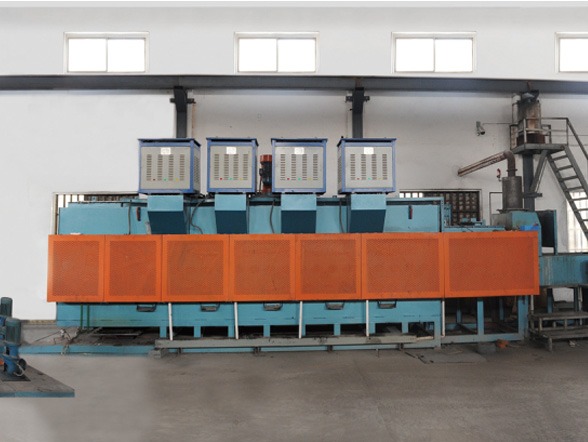
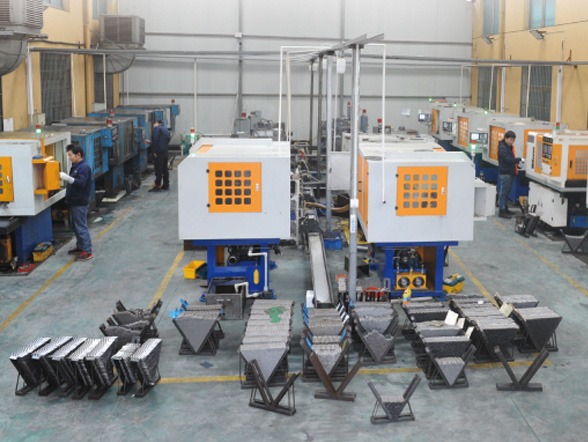
Established in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. has grown into an international manufacturing force spanning 12,000 m² of precision facilities in Danyang, Jiangsu. Rather than functioning as a commercial intermediary, we control every critical phase of cutting tool fabrication: raw HSS alloy spectroscopic verification, bar cutoff, computer-controlled heat-treatment (salt bath and high-vacuum quenching), 5-axis CNC flute grinding, edge honing, surface functionalization, and computerized laser marking.
Third-Party Verified Integrity
Facilities, safety systems, and QC protocols are audited and certified on-site by Intertek Group. Officially recognized as a High-Tech Enterprise of Jiangsu Province since 2019.
Proven Tier-1 Supply Record
Longstanding supplier of cutting tool programs to global market leaders, including BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
Massive Capacity & Agility
Producing over 90 million cutting units annually—including 50M wood bits, 25M twist drills, and 15M hex shank systems. Rapid prototype samples delivered in 7 to 10 working days.
Procurement Knowledge Base
Frequently Asked Purchasing Questions
Clear, direct answers for Dutch procurement directors, toolroom supervisors, and import supply coordinators.
How do you guarantee concentricity and runout tolerances on extra-long deep hole drill bits?
Every production batch undergoes 100% optical runout verification across three distinct points along the flute length. We utilize multi-axis Swiss and German grinding centers to maintain concentricity well within DIN 1414 precision grades. For specialized CNC deep hole tooling, total indicated runout (TIR) is verified below 0.02 mm to prevent oversized bore profiles and early drill fatigue.
Which alloy substrate is optimal: HSS 4241, HSS M2 (6542), or Cobalt M35/M42?
For DIY and standard aluminum applications, HSS 4241 offers budget-friendly utility. For standard European structural steels (S235, S355), professional-grade M2 (6542) provides superior balance between toughness and edge retention. For Eindhoven's stainless steel (304, 316L), Inconel, and abrasive titanium applications, M35 (5% cobalt) or M42 (8% cobalt) is mandatory. Cobalt maintains red-hardness at elevated internal temperatures, preventing rapid tip dulling and edge galling.
Can you provide custom shanks (Weldon, Fein Quick-In, Morse Taper, or Extended Cylindrical)?
Yes. We regularly produce shanks compliant with ISO and DIN standards—including 3/4" Weldon shanks for magnetic drills, tool-free Fein Quick-In fittings, Morse taper sizes MT1 through MT4 (DIN 345), and custom cylindrical shanks with flat relief locks for Swiss-type automatic lathes.
What are your standard Minimum Order Quantities (MOQ) and lead times for the Netherlands?
Single standard drill bit sizes start from 100 to 500 pieces depending on diameter. Specialized annular cutters and hole saw kits start from 10 sets. Custom OEM-packaged tool sets start at 1,200 sets. Production lead times typically span 25 to 35 days, with direct air-freight deliveries reaching Amsterdam Schiphol or Eindhoven Airport within 5–7 days, and ocean freight entering the Port of Rotterdam within 28–32 days.
Are custom OEM laser branding, private labeling, and custom tool coatings supported?
Completely. We offer comprehensive private-label OEM manufacturing. Options include high-contrast laser etching of your brand logo and part numbers on tool shanks, bespoke surface treatments (Black Oxide, Amber Bronze, TiN, TiAlN, or Rainbow PVD), and customized packaging including plastic cassettes, metal index boxes, blister packs, and bulk industrial packaging.