Engineered Heavy Cutting & Drilling Equipment for Adelaide Job Sites
From reinforced quartzite cured concrete saw-cutting to industrial stainless piping and structural anchoring, explore our high-yield tooling engineered to reduce segment stripping, maintain concentricity, and lower operational cost per cut.
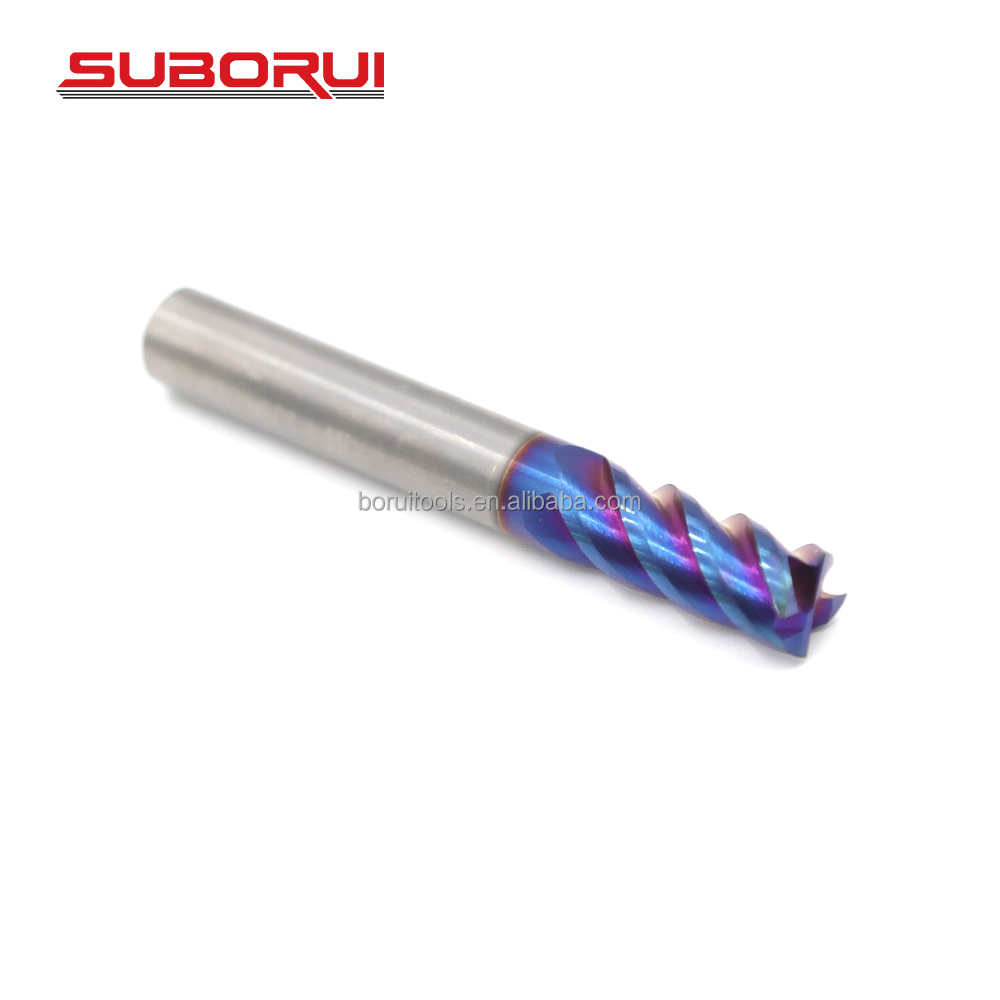
SUBORUI 4 Flute CNC HRC65 Solid Carbide End Mill Cutter
Tungsten carbide end mills designed for deep cavity pocketing, rebar trimming, and ultra-hard metal profile milling in high-wear fabrication shops across Wingfield and Edinburgh.
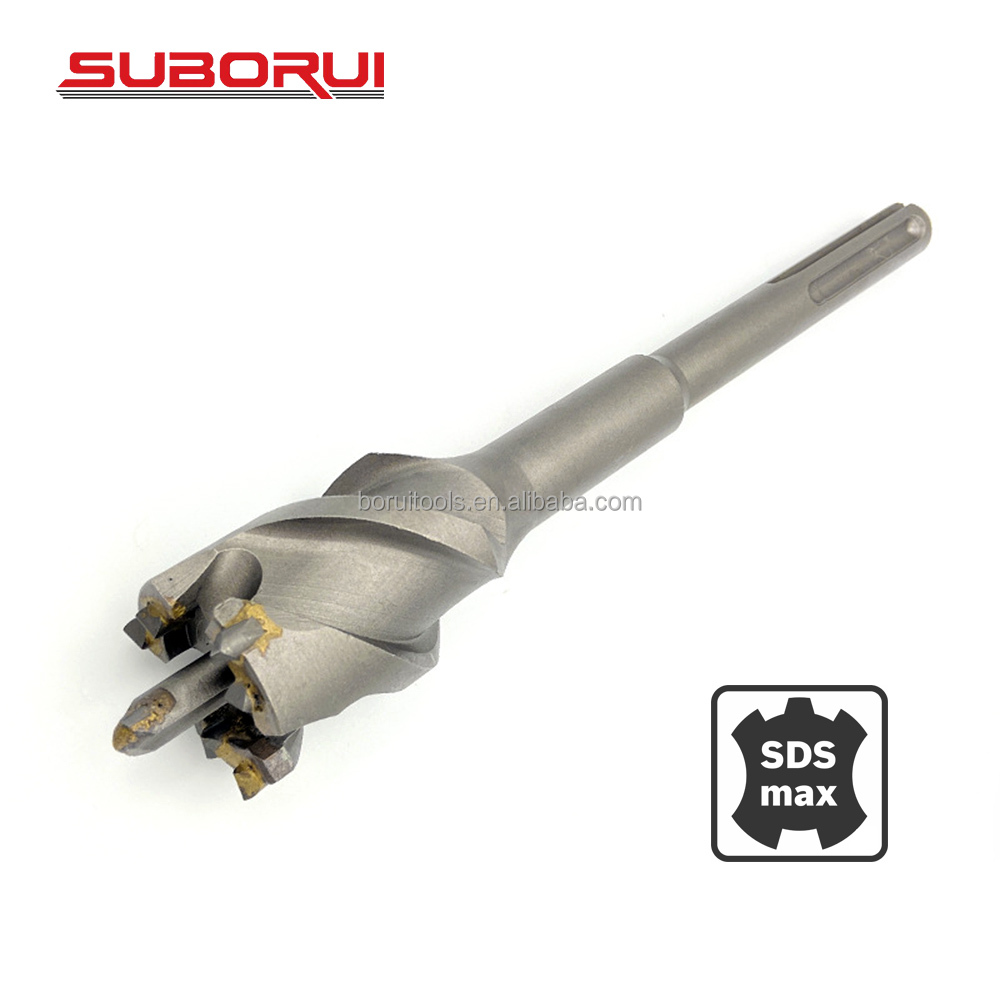
SUBORUI SDS Max Carbide Wall Hollow Core Drill Bit
Industrial core cutter equipped with stepped tungsten teeth for through-wall HVAC duct penetrations, electrical conduits, and masonry boring in dense brick and curing aggregate.

SUBORUI DIN352 Metric HSS M2 Straight Fluted Hand Tap Set
Precision 3-piece tap set (taper, second, bottoming) crafted from M2 high-speed steel for structural concrete bolt anchoring, thread restoration, and precast rebar sleeve machining.
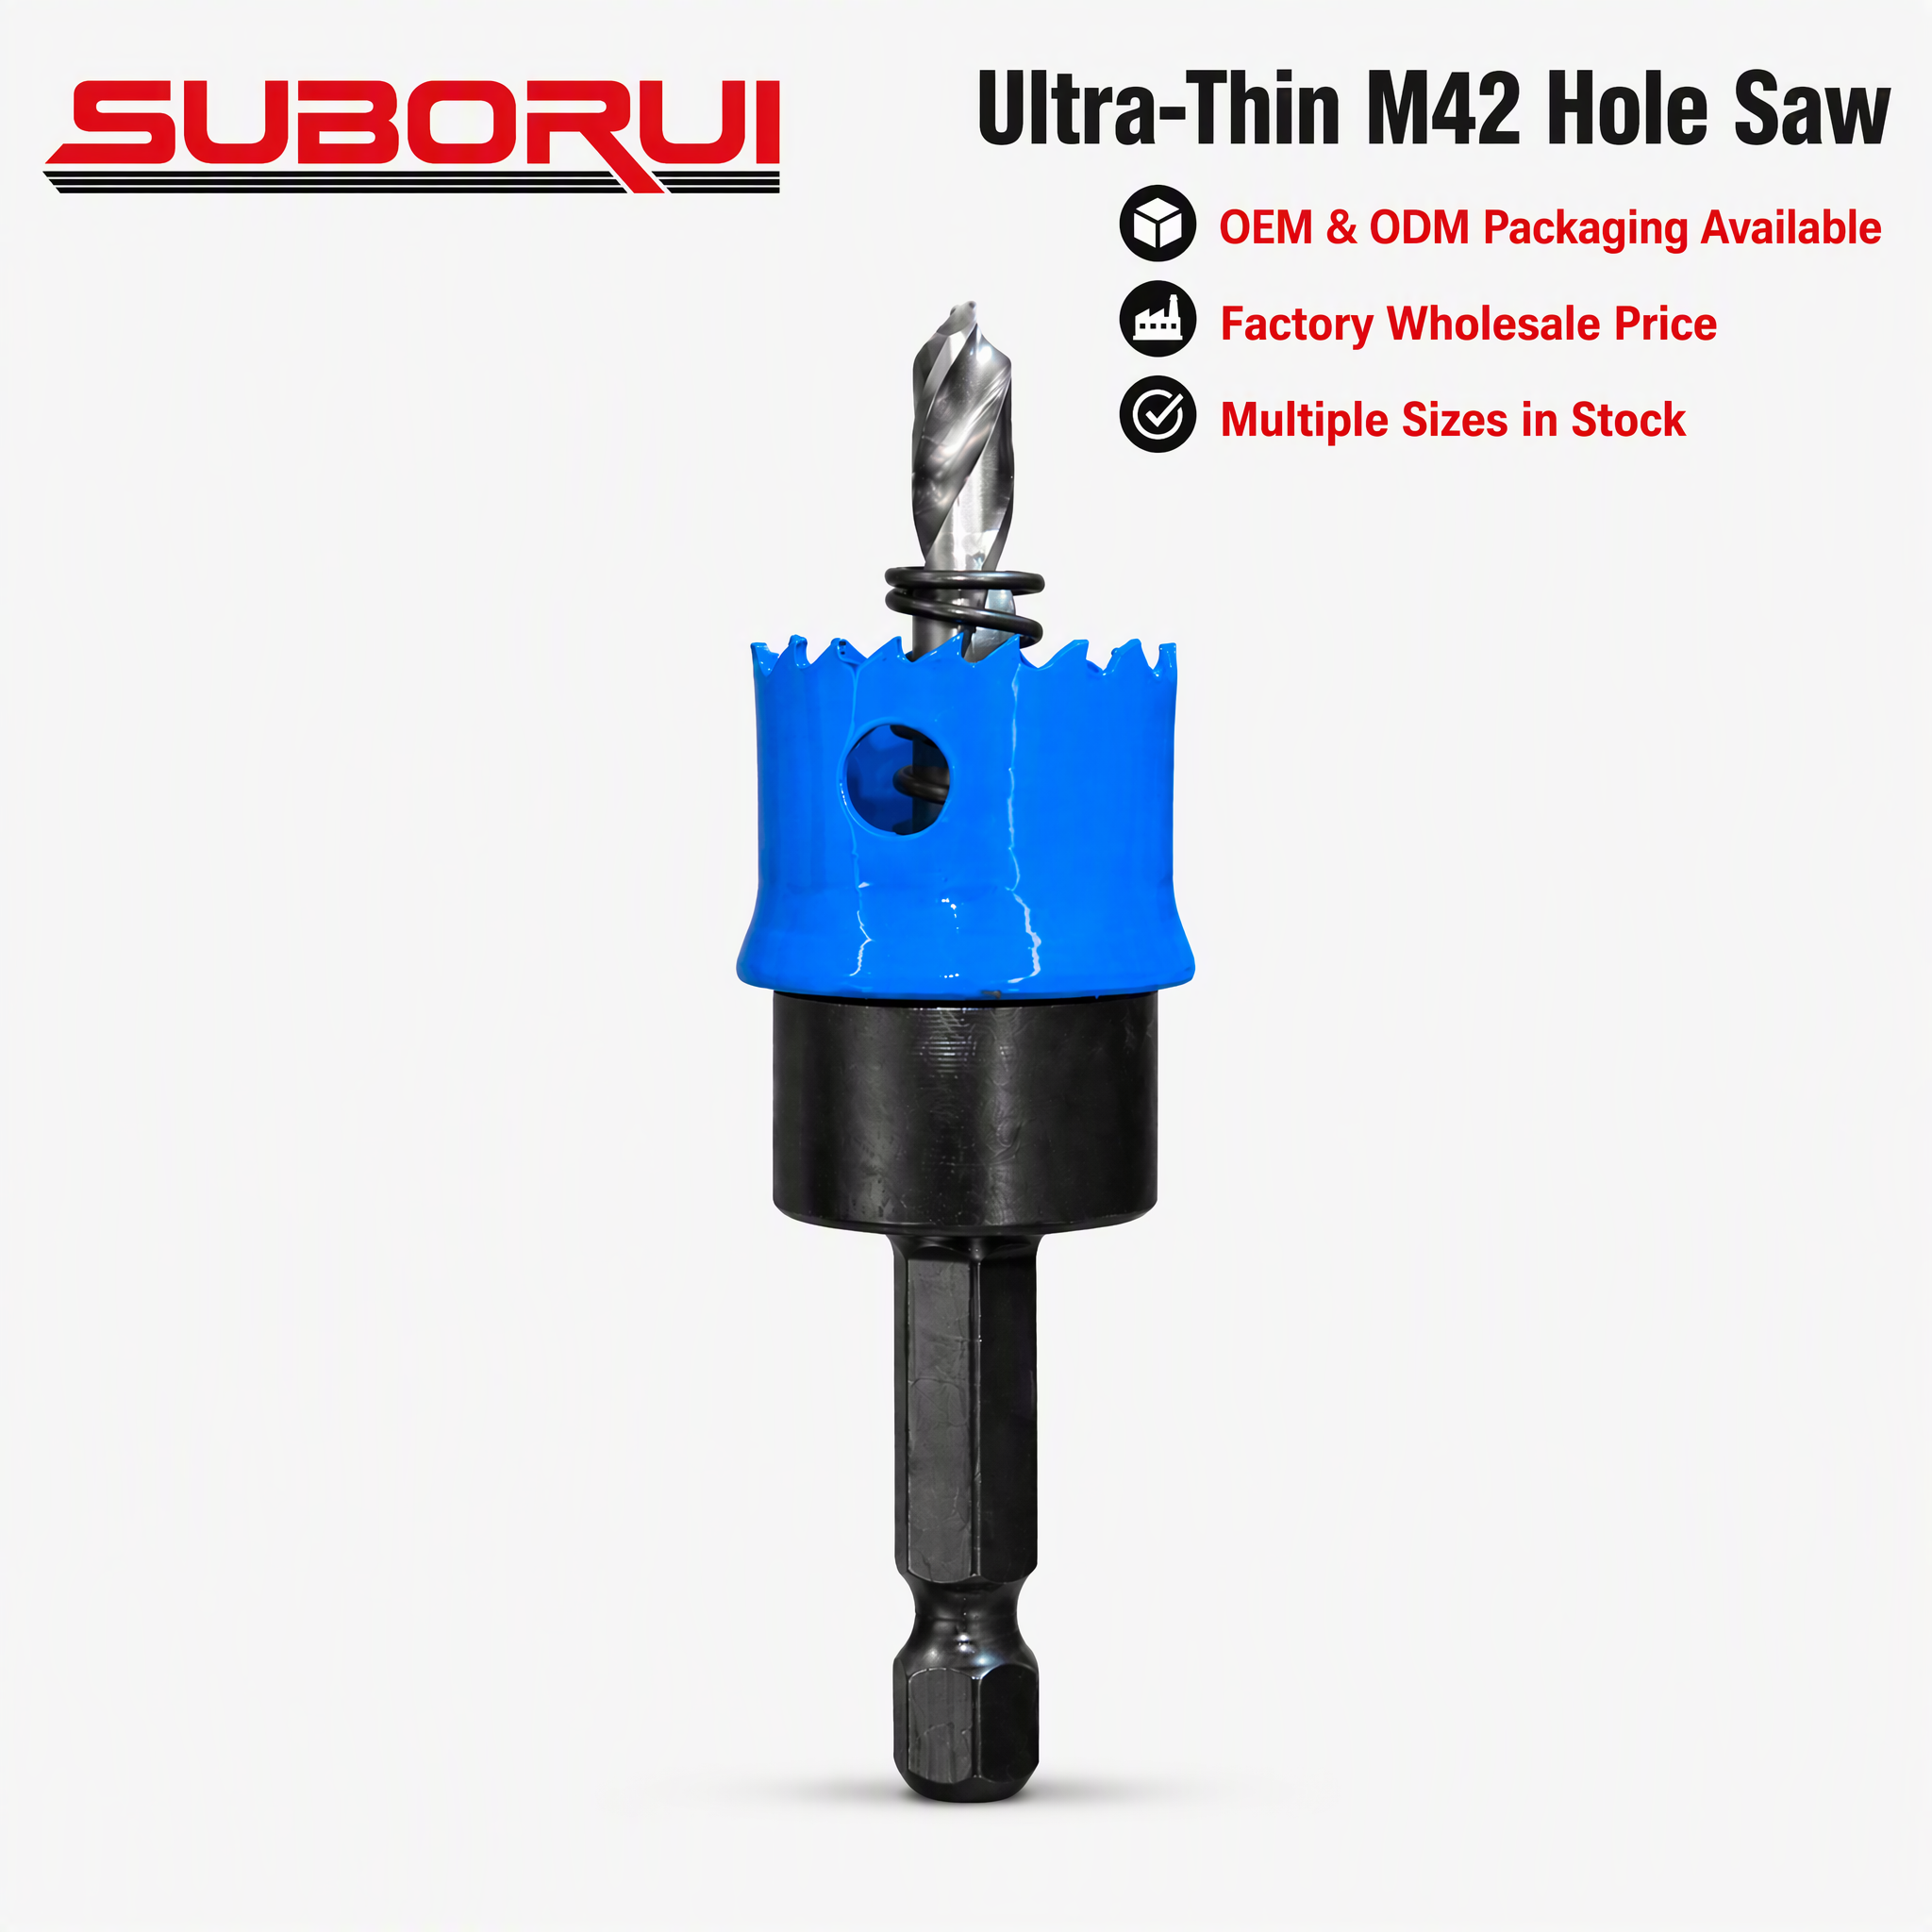
SUBORUI Ultra-Thin Hex Shank M42 Bi-Metal Hole Saw
8% cobalt electron-beam welded bi-metal cutting edge engineered for clean, burr-free boring in stainless steel cladding, sheet metal flashings, and structural metal formwork.
SUBORUI Multi-Material M42 Bi-Metal Heavy Hole Saw
Versatile variable-pitch tooth profile optimized for South Australian commercial builders handling hardwood structural formwork, structural steel studs, and composite drywall.
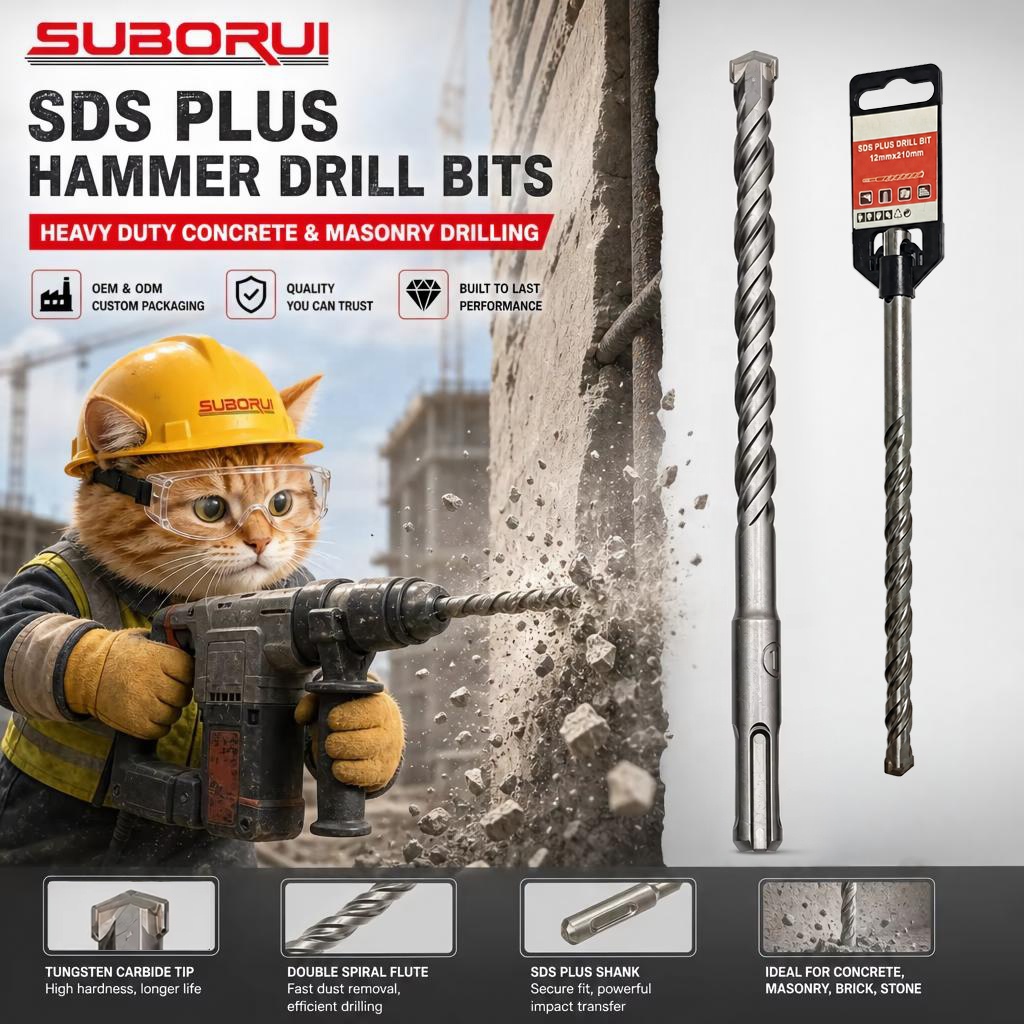
SUBORUI 40Cr Carbide Tip SDS Plus Hammer Drill Bit
Heat-treated 40Cr chrome alloy steel body combined with micro-grain carbide tips. Designed for deep anchoring, doweling, and vibration-resistant masonry boring across Adelaide job sites.

SUBORUI 1/4" Fully Ground TiN Hex Shank Twist Drill Bit
Quick-change 135° split point DIN338 geometry with Titanium Nitride surface armor. Eliminates bit walking during structural metal bracket installation and precast anchoring setups.

SUBORUI M42 Industrial Core Hole Saw Drill Bit Cutter
Deep-cut body casing featuring aggressive gullet geometry for swift chip clearance in abrasive polymers, cast metals, architectural timber beams, and PVC drainage conduits.
// Whitepaper Analysis: Metallurgical Blade Sizing for Adelaide's Quartzite Aggregates
Procuring concrete cutting blades and diamond core consumables for projects throughout Greater Adelaide, from the Barossa region down through Port Adelaide and the Fleurieu Peninsula, demands an uncompromising understanding of South Australia's geological profile. Concrete mixes placed across Adelaide commonly source coarse aggregate from Mount Lofty Range quarries, notably comprising dense, compressive Stonyfell Quartzite and river gravels with exceptionally elevated silica levels (exceeding 85% to 92% quartz content).
When conventional or low-grade imported diamond blades cut these cured aggregates, two catastrophic failure modes routinely emerge: segment glaze-over or premature bond burnout. When the metallic bond matrix is excessively hard, the high-purity quartzite fractures into microscopic, highly abrasive silica slurry that polishes both synthetic diamond crystals and the cobalt bronze matrix, neutralizing cutting action. Conversely, if an excessively soft matrix is matched with Adelaide's aged 40–50 MPa commercial concrete, the aggressive slurry accelerates matrix erosion, unseating diamonds prematurely before they deliver their design lifecycle.
At Jiangsu WRD Tools, our custom OEM engineering division formulates proprietary metallurgical powder matrices tailored specifically for South Australian aggregate conditions. By strategically blending nickel, tungsten carbide, and cobalt powder skeletons with high-grade synthetic diamond mesh (ranging from 30/35 US mesh for green concrete to 40/50 US mesh for cured heavily-reinforced concrete), our laser-welded diamond blades and core bits maintain controlled, continuous diamond self-sharpening without catastrophic segment throw.
| Substrate Application (Adelaide Metro) | Aggregate / Hardness Grade | Recommended Bond Formulation | Diamond Grit / Concentration | Typical Segment Weld Technology |
|---|---|---|---|---|
| Cured Highway Pavement (North-South Motorway) | Quartzite + River Gravel (40-55 MPa) | Medium-Soft Bronze-Cobalt Alloy | 35/40 Mesh | 30% Volumetric Conc. | Automated CNC Laser Welded (DIN EN13236) |
| Fresh / Green Concrete Joint Sawing | Abrasive Sand & Early Setting Mixes | Ultra-Hard Tungsten-Reinforced Matrix | 30/35 Mesh | 25% Conc. + Drop Segments | Direct Laser Welded with Undercut Pins |
| Commercial Tilt-Up Wall Penetrations | Precast High-Early Strength Concrete | Medium-Hard Cobalt Matrix | 40/50 Mesh | 28% High-Grade Synthetic | Laser Welded Keyhole Segment Slots |
| Deep Utility Core Boring (Adelaide CBD) | Reinforced Blue Metal & Quartzite Slab | Free-Cutting Nickel-Cobalt Wet Matrix | 40/45 Mesh | Multi-Layer Impregnated | Silver Brazed / Laser Welded Wet Crown |
Specialized Applications Across South Australian Project Sites
Engineered for severe mechanical stress, thermal shocks, and aggressive dust environments across civil infrastructure, heavy roadworks, and industrial expansions.
North-South Corridor (Torrens to Darlington) Expansion
Continuous floor sawing demands blades that withstand extreme continuous heat and aggregate shock without segment shedding. Our custom 450mm to 900mm walk-behind saw blades incorporate laser-welded undercut protection segments that prevent premature steel core wear along abrasive slurry contact tracks.
Osborne Naval Shipyard & Marine Subsea Enclosures
Heavy maritime and defense facilities require deep anchor installations and high-density post-tensioned reinforced slab coring. Our SDS Max drill bits, diamond core bits, and annular cutters deliver high concentricity to bore through C50 maritime concrete with dense rebar mats without drifting or binding.
Northern Adelaide Plains Industrial Warehousing
Rapid expansion in Edinburgh Parks and Direk relies heavily on expansive post-tensioned slab construction. Our high-speed green concrete joint grooving blades eliminate edge micro-fractures, allowing precise joint induction within the critical initial setting window before uncontrolled curing cracking occurs.
Emerging Trends in South Australian Concrete Demolition & Sawing
Strategic shifts influencing cutting tool specifications across commercial demolition, environmental regulations, and wholesale procurement.
Stricter Crystalline Silica Safety Standards (SafeWork SA)
With aggressive workplace exposure standards implemented throughout South Australia, tier-1 civil contractors are transitioning from dry handheld cutting toward integrated wet suppression sawing and vacuum-brazed dry containment tooling. Our tooling geometries optimize internal coolant flushing channels, subduing airborne respirable particles at the exact segment-cut interface.
High-Frequency Electric & Battery Saw Adoption
Urban Adelaide developments are increasingly demanding cordless cut-off saws and electric wall-sawing units to minimize carbon footprints and lower decibel levels in hospital and residential zones. We fabricate ultra-thin kerf laser blades (down to 2.2mm thickness) that minimize mechanical resistance, preserving motor battery life while accelerating linear speed.
Supplanting Resellers with Factory-Direct OEM Private-Label
Adelaide tool hire firms, diamond coring contractors, and construction hardware wholesalers are shifting away from third-party European brand margins. By partnering directly with Jiangsu WRD Tools, distributors customize segment hardness, imprint corporate branding via high-contrast fiber laser, and secure customized package labeling at true factory price tiers.
Frequently Asked Questions by Adelaide Buyers
Detailed technical answers to common queries regarding sea freight logistics, custom laser welding, minimum order quantities, and test samples.
Ocean freight shipments from Shanghai or Ningbo ports typically require 14 to 18 sailing days to arrive at the Port of Adelaide (Outer Harbor). Our production turnaround for standard OEM orders is 25 to 30 business days following technical drawing confirmation, facilitating seamless quarterly inventory management for South Australian distributors.
We employ fully automated CNC German-engineered laser welding heads that weld segment diamond matrix directly onto our 75Cr1 high-carbon alloy steel cores. The penetration depth creates an isotropic metallurgical bond with tensile shear strength significantly exceeding European EN13236 safety standards, eliminating segment detachment when contacting 16mm–32mm tensile reinforcing steel.
Yes. We supply any international arbor configuration required by Australian saw models, including standard 25.4mm (1-inch) bore with drive pin holes for walk-behind road cutters, 20mm/22.23mm bores for handheld petrol quick-cut saws (Husqvarna, Stihl, Makita), as well as 60mm flush-mount wall-sawing flanges.
For diamond saw blades and core drill bits, OEM laser etching on the tool body starts at just 50 to 100 units per specification. Custom printed full-color retail cartons, clamshell blister cards, or metal contractor cases generally start at 500 units per format, with shared branding available across mixed dimension orders.
Certainly. We routinely dispatch technical pilot sample kits via express air courier (DHL/FedEx directly to Adelaide metro addresses within 4–6 business days). This allows your field operators to conduct side-by-side performance tests measuring linear cutting speed (m/min) and total lifecycle (m²) against your current diamond tooling supplier.
Every steel core undergoes computer-controlled tension rolling, heat treatment straightening, and dynamic balance inspection. We maintain radial and axial runout tolerances within 0.05mm, ensuring smooth operation that avoids saw spindle bearing damage and prevents uneven wavy cuts across deep trenching runs.
Why International Tool Brands Trust Jiangsu WRD Tools
Founded in March 2007 with RMB 10 million registered capital, Jiangsu WRD Tools Co., Ltd. operates an integrated 12,000 m² production facility in Danyang, Jiangsu Province.
Intertek Onsite Verified Manufacturer
Our plant facilities, multi-axis CNC machines, laser welding lines, and rigorous metallurgical QA/QC testing regimens are fully verified onsite by Intertek. We eliminate the quality risks, delays, and markups associated with middleman trading firms.
End-to-End Vertical Manufacturing
From steel blank laser-cutting, controlled atmosphere heat treatment hardening, diamond segment hot isostatic pressing, to robotic welding and dynamic balancing, every critical process remains directly under our internal quality management system.
Proven Global OEM Track Record
Over nearly two decades, WRD Tools has manufactured cutting tools and accessory sets supplied to premier global tool brands including Bosch, Milwaukee, DeWalt, Irwin, Makita, Dexter, and KWB, earning a recognized 4.7/5 global buyer rating.
Build Your Custom Concrete Blade Line for South Australia
Whether you require private-label diamond saw blades customized for Adelaide quartzite aggregate, SDS max hammer coring sets, or industrial hole saws, our direct export team provides technical specifications, pricing tiers, and trial samples promptly.