Featured CNC Cutting & Drilling Solutions
Manufactured with sub-micron runout tolerances, proprietary heat treatment, and specialized geometries to support continuous high-speed automated production.

DIN338 135° Split Point M35 Cobalt HSS CNC Twist Bit
View Specifications →
Engineering Precision: Custom OEM CNC Tooling Architecture for The Hague Industry
An authoritative analysis of tooling metallurgy, dynamic runout tolerances, chip clearance hydrodynamics, and supply chain rationalization for procurement heads in South Holland.
As the administrative capital of the Netherlands and a pillar of the Randstad conurbation, The Hague ('s-Gravenhage) stands out as an international hub for high-technology research, international diplomatic headquarters, maritime infrastructure engineering, and high-performance architectural fit-outs. Machine shops, interior modular contractors, composite engineers, and precision metalworking factories located in surrounding industrial zones—including Forepark, Binckhorst, Zichtenburg-Kerketuinen-Dekkershoek (ZKD), and the neighboring Delft-Ypenburg innovation corridor—face unique material challenges. Whether machining fire-rated phenolic compact laminates (HPL) for international tribunals, milling saline-resistant 316L stainless steel for North Sea marine projects, or high-speed routing carbon-reinforced polymer composites (CFRP) in aerospace labs, tool failure or premature edge wear is economically unacceptable.
As a dedicated Chinese manufacturing facility founded in March 2007, Jiangsu WRD Tools Co., Ltd. (operating the SUBORUI brand line) acts not as a trading intermediary, but as an integrated, Intertek-verified production source. Operating a 12,000 m² modern manufacturing plant with over 150 technical specialists and an annual output exceeding 90 million tools, our facility bridges the gap between precision European engineering standards (DIN, ISO, NEN) and factory-direct volume economies of scale.
Sub-Micron Tungsten Carbide Substrates
We source ultra-fine micro-grain tungsten carbide (grain size 0.4–0.6 μm) with 10%–12% Cobalt binder content. This metallurgical configuration ensures high transverse rupture strength (TRS > 4,000 MPa) combined with hardness above 92.5 HRA, preventing micro-chipping on interrupted CNC rout paths.
Multi-Axis CNC Flute Grinding
Utilizing 5-axis tool grinders (Walter and ANCA platforms) equipped with in-process laser optical measuring units, our flutes are mirror-polished to Ra 0.1 μm. Optimized upward or downward spiral helix angles eliminate delamination in double-sided melamine and resin-infused veneers.
PVD & CVD Nanocomposite Coatings
For high-abrasion applications encountered in South Holland composite processing, we apply AlTiN, TiSiN, and crystalline Diamond-Like Carbon (DLC) coatings. These surface treatments maintain an ultra-low friction coefficient (μ < 0.1) and resist thermal oxidation up to 900°C.
Localized Application Scenarios in The Hague & South Holland
Tailoring CNC tool geometry to the dominant manufacturing operations in the Randstad metropolitan perimeter.
1. Maritime & Coastal Infrastructure (Scheveningen Port)
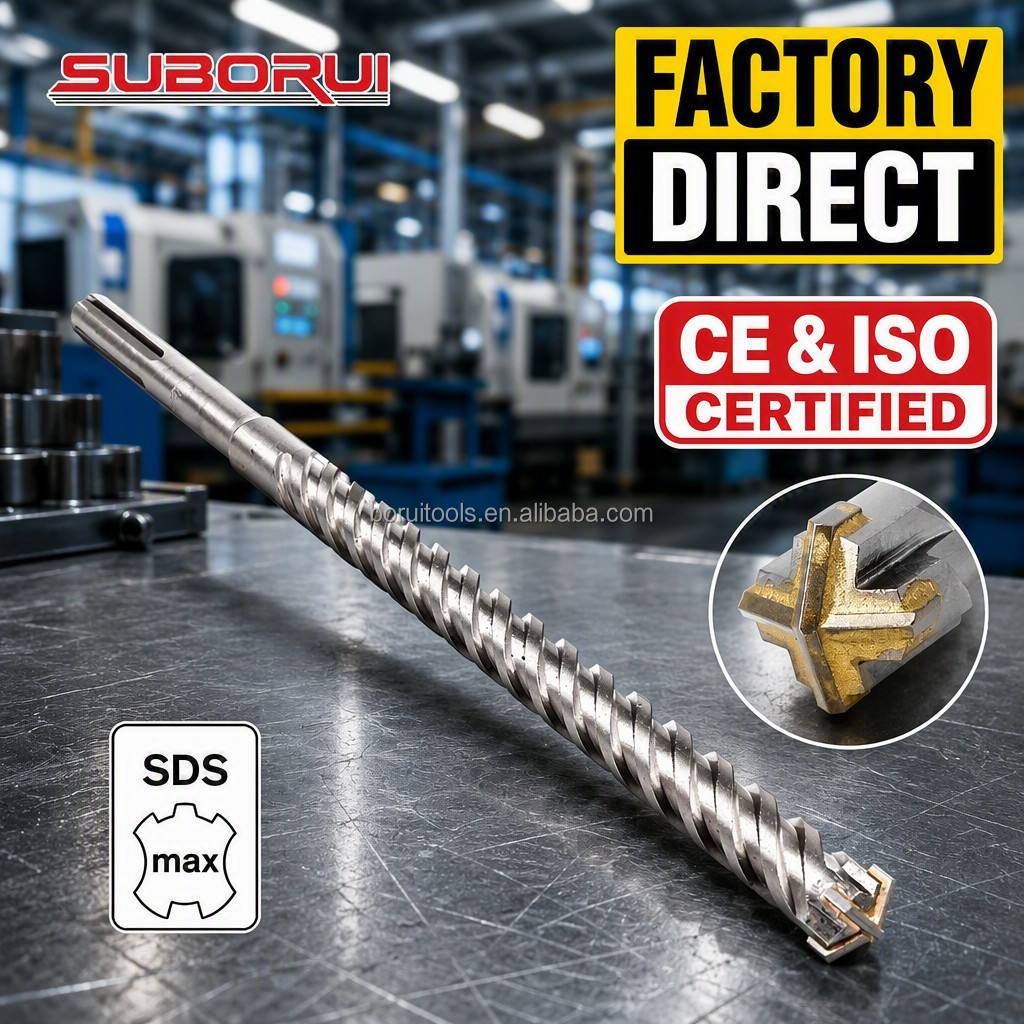
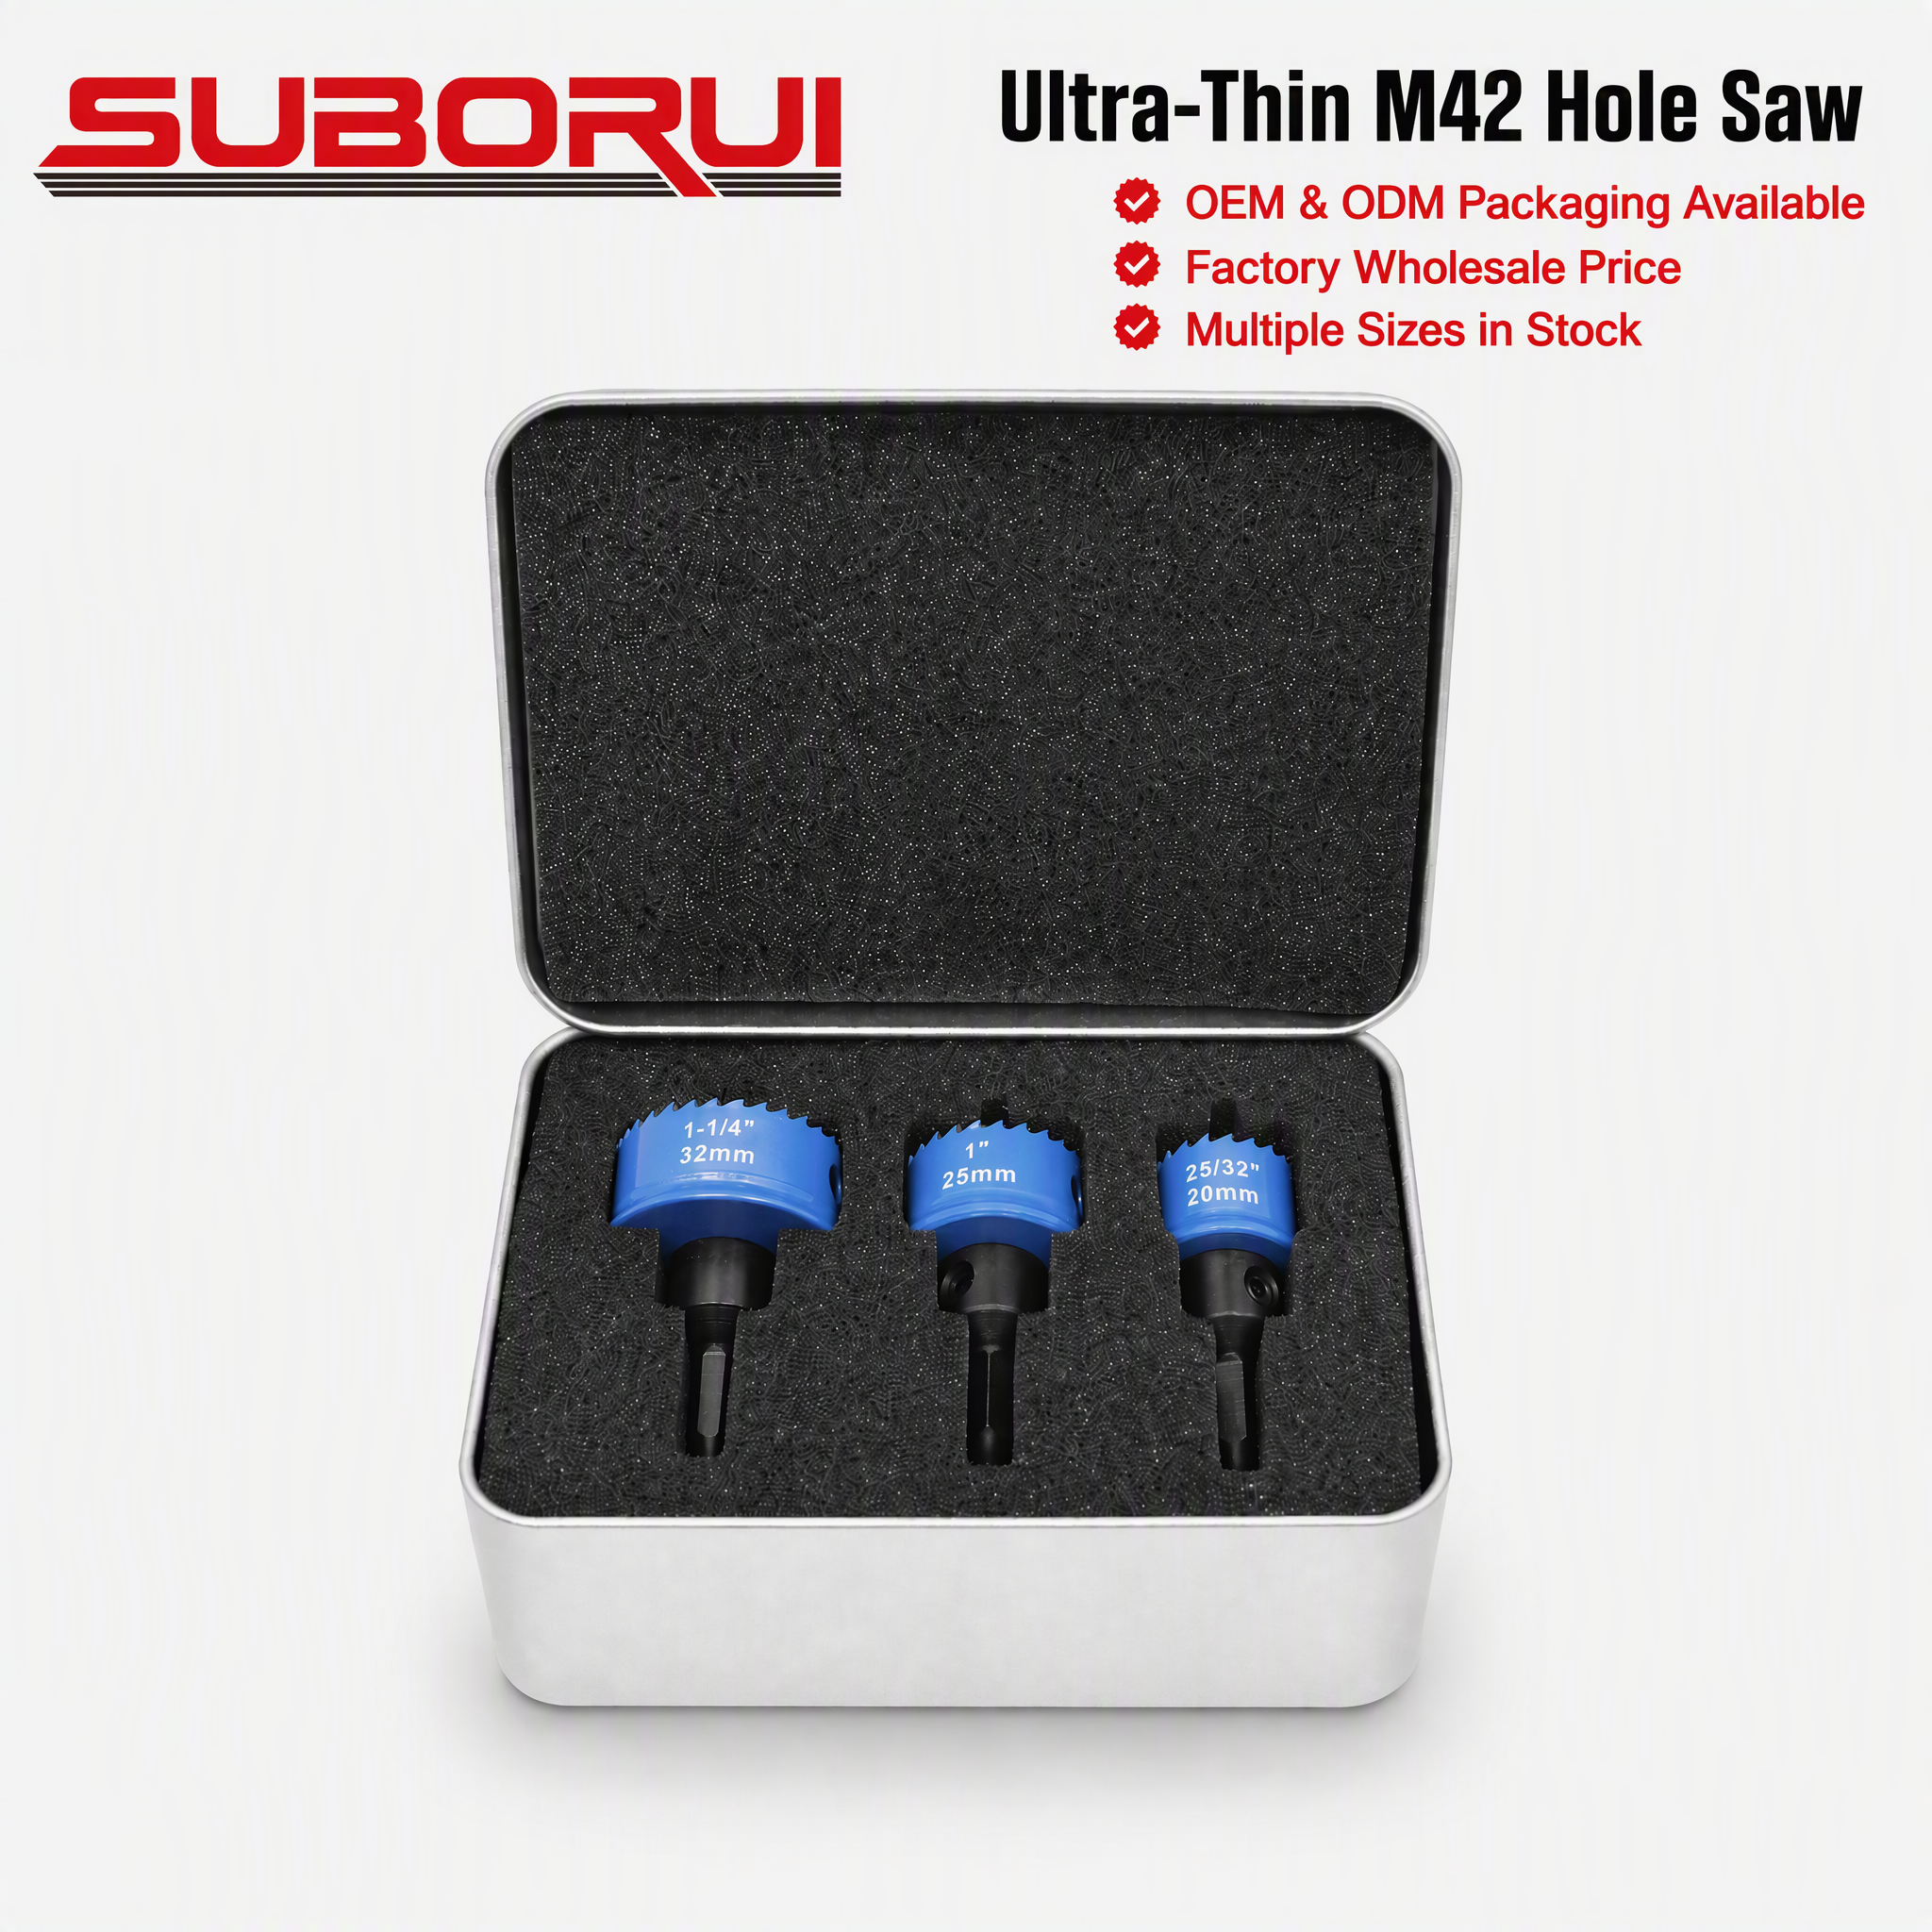
Scheveningen hosts active coastal engineering facilities, commercial fishing fleets, and offshore support systems. Machining seawater-resistant components from 316L stainless steel, bronze fittings, and thick HDPE marine fenders requires tools with rapid chip clearance and robust cutting edges. Our DIN338 M35 cobalt series and solid carbide end mills with parabolic flutes prevent thermal softening in these challenging conditions.
2. High-Spec Architectural Joinery & Embassies
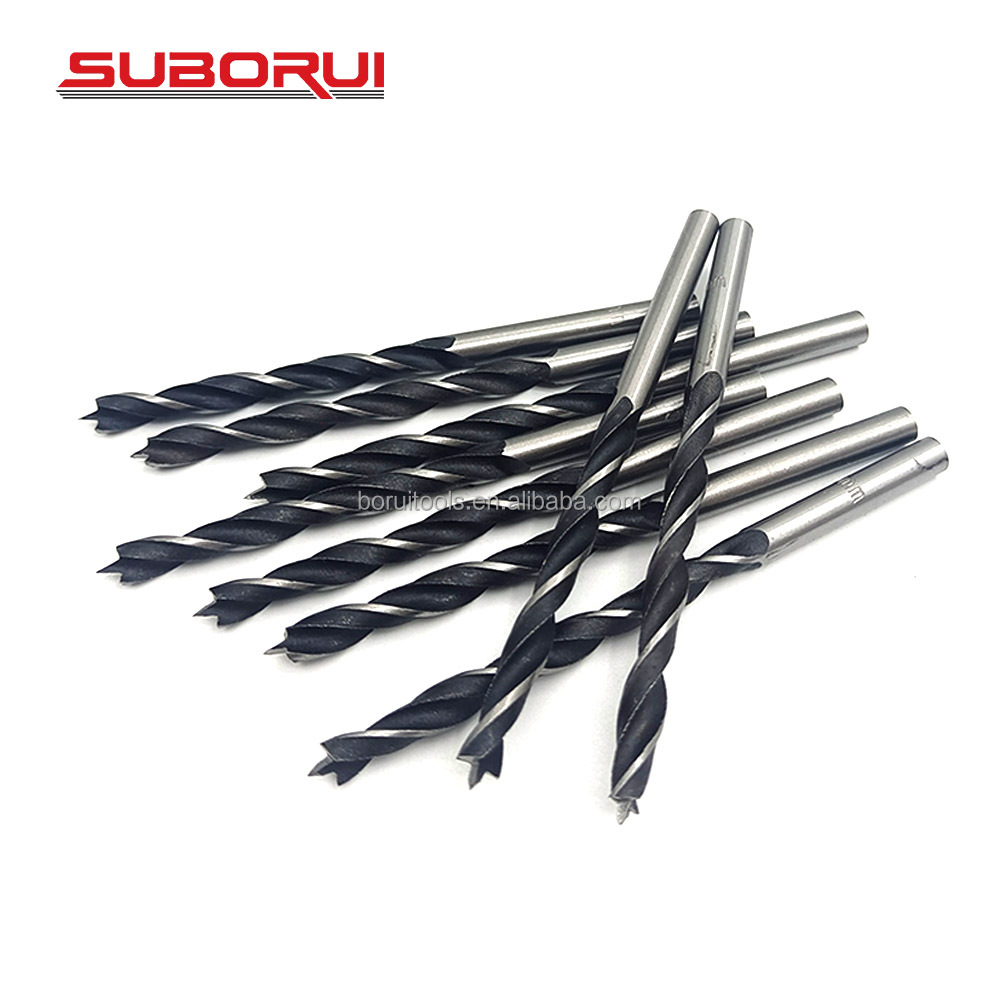
Housing over 150 international courts, embassies, and government ministries, The Hague continuously executes high-end interior acoustic renovations. Working with solid acoustic oak, acoustic perforated wall panels, fire-retardant MDF (FR-MDF), and Corian solid surfaces necessitates zero top-edge chipping. Our custom OEM compression spiral router bits and clear-edge brad point drill bits ensure clean surfaces on both the face and back veneers.
3. Advanced Composites (Delft-Ypenburg Tech Hub)
Positioned along the innovation axis connecting The Hague with TU Delft and Ypenburg, aerospace tier suppliers and lightweight engineering labs process carbon fiber (CFRP), glass fiber (GFRP), and honeycomb core sandwiches. Our Diamond-Vapor-Deposited (CVD) diamond burrs and PCD router bits effectively prevent delamination, fiber breakout, and rapid cutting edge blunting.
Industrial & Tooling Trends in The Hague & Greater Randstad
Key operational shifts affecting tooling specification, material sourcing, and automation across Dutch manufacturing plants.
Circular Economy & Bio-Based Substrates
In accordance with Dutch national goals for circular construction by 2030, The Hague manufacturers are shifting heavily toward hemp composites, mycelium boards, and recycled cross-laminated timber (CLT). These materials contain variable resin binders requiring customized positive-rake cutting edges to prevent abrasive gumming.
Strict Noise & Fine Dust Emission Norms
Dutch Arbowet regulations and municipal environmental guidelines in South Holland enforce rigorous workplace dust controls. Our OEM router designs incorporate aerodynamic flute profiles that channel chips directly toward CNC extraction hoods, decreasing respirable PM2.5 and PM10 workplace dispersion.
Automated "Lights-Out" CNC Nesting
Facing skilled labor deficits in the Western Netherlands, commercial joinery operations rely heavily on automated nested-base CNC cells running unmanned shifts. Tool predictability is paramount; our CNC router bits undergo batch-level dynamic balancing to G2.5 at 30,000 RPM to prevent catastrophic breaks during unmonitored cycles.
Supply Chain Reshoring to Verified Sources
Rather than purchasing unbranded items from local distributors with 200% markups, procurement directors in The Hague are auditing original manufacturing plants overseas. Direct factory cooperation allows custom shank geometries, laser engraving of Dutch article codes, and scheduled consolidated shipments into Rotterdam.
Cutting Tool Material & Coating Selection Guide
Technical comparison for automated machine tool operators in The Hague industrial zones.
| Tool Material Substrate | Hardness / TRS | Recommended Feed & Speed | Primary Substrates | Performance in High-Volume CNC |
|---|---|---|---|---|
| Solid Micrograin Carbide (OEM Grade K10-K20) | 92.5–93.2 HRA / 4,200 MPa | 18,000–24,000 RPM Feed: 12–22 m/min |
Solid Hardwood, Birch Plywood, Compact Laminate (Trespa®), Corian | Standard industry benchmark; smooth edge retention, resharpenable 2–3 times under controlled metrology. |
| PCD (Polycrystalline Diamond) Tipped | > 8,000 HV / 2,800 MPa | 20,000–24,000 RPM Feed: 18–35 m/min |
Raw Chipboard, Highly Abrasive MDF, Carbon Fiber, Glass Fiber Core | Extends tool lifespan 25x–50x over carbide in abrasive glues; ideal for high-volume nested cabinetry production. |
| M35 Cobalt HSS (5% Co, DIN Standard) | 64–66 HRC / 3,800 MPa | 600–2,500 RPM (drilling) Feed: 0.05–0.25 mm/rev |
AISI 304/316 Stainless, Structural Steel, Marine Hull Alloy, Brass | High resistance to thermal deformation during deep hole operations; 135° split point eliminates wandering without center punching. |
| M42 Bi-Metal Matrix-II (8% Cobalt) | 67–69 HRC / 4,000 MPa | Variable RPM per diameter Deep cutting tooth profile |
Alloy Plate, Electrical Cabinets, Sandwich Panels, Sheet Steel | Resistant to tooth stripping when encountering structural cross-members, thin-wall sheet metal, and composite structural framing. |
| Diamond Vacuum Brazed Matrix | Extreme grit adhesion | 8,000–12,000 RPM Dry or wet routing |
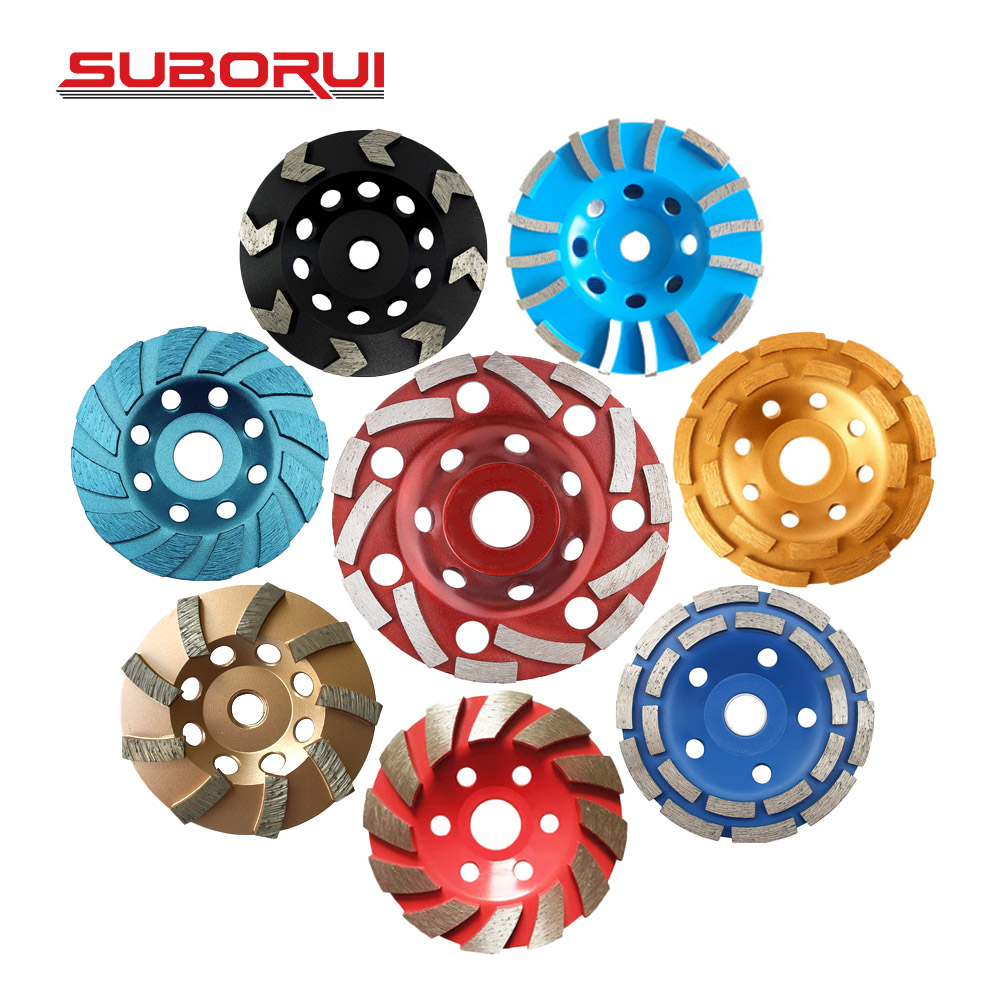
Porcelain Slabs, Granite Countertops, Architectural Glass, Masonry | High cutting speeds without coolant in ceramic facade tile modification; prevents edge blowout and radial chipping. |
Why Global Tool Brands Partner with Jiangsu WRD Tools
Verified manufacturing capabilities, strict quality assurance, and proven contract manufacturing history.
Intertek Onsite-Verified Factory
Our 12,000 square meter production facility in Danyang, Jiangsu, has been formally inspected and verified onsite by Intertek. Buyers in The Hague can review complete audit reports detailing machinery counts, staff qualifications, environmental controls, and QA/QC processes.
19 Years of Tooling Expertise
Founded in March 2007 with RMB 10 million registered capital, WRD Tools has grown into an acknowledged High-Tech Enterprise of Jiangsu Province. We do not broker items; we control the full chain from raw bar stock slicing and heat treatment to CNC grinding and laser testing.
Tier-1 Global Brand Supplier
Over nearly two decades, our plant has delivered precision drill bits, annular cutters, and router tooling to international tool corporations including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Heller, Dexter, KWB, and Wolfcraft. We understand strict tolerance management.
Massive Production Scalability
With an annual output of 50 million wood drill bits, 25 million twist drill bits, and 15 million hex shank drills, our workshops handle large supply programs with rapid lead times. Repeat orders maintain strict dimensional consistency across production batches.
Full OEM / ODM Customization
We produce router bits to custom CAD prints: custom shank diameters (6mm, 8mm, 12mm, 1/4", 1/2"), specialized up-down compression ratios, custom chip breakers, shank flat configurations, and personalized laser markings for private brand labels in the Netherlands.
Seamless Freight to Port of Rotterdam
Situated within convenient transit radius to Shanghai and Ningbo maritime hubs, we offer straightforward logistics routing directly to Rotterdam (just 25km from The Hague). Air express via Schiphol Amsterdam (AMS) delivers rapid sample runs within 4 to 6 business days.
Frequently Asked Questions for Buyers in The Hague
Clear answers on Dutch customs, minimum orders, material compliance, and sample validation.
How do import duties, Dutch VAT (BTW), and customs clearance work when ordering from Jiangsu WRD Tools? +
What is the typical Minimum Order Quantity (MOQ) for custom-engineered CNC router bits? +
Can you replicate exact tooling profiles from worn samples or CAD models used by Dutch CNC shops? +
How does your tool balancing handle high-speed spindle operations (24,000+ RPM)? +
What are the standard production lead times and shipping options to South Holland? +
Do your products meet European safety and manufacturing standards? +
Connect Directly with Our OEM Tooling Engineers
Whether you need custom solid carbide compression spirals, cobalt drill bit sets, or private-label distribution manufacturing for The Hague and broader Benelux markets, our technical sales engineers will respond within 24 business hours.