
19+
Years Tooling Manufacture
12,000 m²
Intertek-Audited Facility
90M+
Annual Bits & Cutters Output
< 0.005mm
Concentricity Tolerance
High Performance Industrial Tooling
Standard & Custom Machining Essentials for Plzeň Workshops
Explore our export-grade line of ISO-compliant straight fluted taps, high-durability M35 cobalt bits, diamond masonry saws, and specialized chamfering instruments, engineered to withstand aggressive rotational stress.







Engineering Whitepaper Analysis
Countersinking Kinematics in High-Tensile Bohemian Steels
In structural heavy engineering, rail bogie production, and precision transmission manufacturing across Plzeň and the West Bohemian industrial valley, chatter-free chamfering and true conical seating determine mechanical joint longevity.
Unequal Flute Pitch & Chatter Reduction
Traditional symmetrical 3-flute countersinks often encounter harmonic resonance when deburring ductile alloy steels like 42CrMo4 or structural S355. Our specialized countersinks incorporate asymmetric flute spacing (e.g., 118°-124°-118°) to dynamically break chip harmonics, guaranteeing ultra-smooth, mirror-grade 90° and 60° seating surfaces without polygonation.
Metallurgical Chemistry: M2 vs. M35 Cobalt
High continuous cycle rates in Plzeň automotive tier-1 lines produce critical cutting edge temperatures exceeding 550°C. We forge countersink tooling using M35 High-Speed Steel with 5% active Cobalt content, sustaining high hot-hardness (64–66 HRC). This minimizes thermal softening, micro-chipping, and abrasive crater wear along the primary cutting lip.
Physical Vapor Deposition (PVD) Coatings
Standard uncoated bits experience galling when chamfering austenitic stainless steels and structural alloys. Our factory applies AlTiN (Titanium Aluminum Nitride) or multilayer TiCN coatings, yielding surface micro-hardness up to 3300 HV and an oxidation resistance threshold reaching 800°C, extending tool lifecycle by up to 380%.
| Tool Steel Grade | Hardness (HRC) | Thermal Threshold | Optimal Materials for Plzeň Workshops | Recommended Surface Treatment |
|---|---|---|---|---|
| HSS 4241 / Standard | 61 – 63 HRC | 400°C | Soft mild steels (<500 N/mm²), aluminum, plastics, timber | Bright / Black Oxide |
| HSS M2 (6542 / 1.3343) | 63 – 65 HRC | 580°C | Standard carbon steels, iron castings, structural plates | Titanium Nitride (TiN) / Amber Finish |
| HSS-E M35 (Co 5% / 1.3243) | 65 – 67 HRC | 650°C | Stainless 304/316, HARDOX, high-tensile tool steels, rail metals | AlTiN / TiAlN Multi-layer |
| Solid Micrograin Carbide | > 72 HRC | 950°C | Hardened dies (>55 HRC), abrasive high-nickel alloys, automated CNC | Nano-Composite nACo |
Local Ecosystem Integration
Serving the Precision Engineering Heartland of West Bohemia
From the historic heavy engineering works of the Škoda corridor to modern robotic integration facilities along the D5 highway, Plzeň represents one of Central Europe's densest hubs of mechanical expertise.
Rolling Stock & Heavy Transportation
Plzeň’s globally prominent railway engineering and public transit manufacturing demand rigorous DIN standard fastener seating. Countersunk fasteners on tram chassis, rail bogies, and passenger cabs must flush precisely with load-bearing plates to avoid aerodynamic resistance and destructive stress concentrations under dynamic rail vibration.
Energy, Turbines & Industrial Drives
Turbine casings, gear assemblies, and power transmission subsystems machined across West Bohemia mandate zero-burr chamfers on internal fluid passages and fastener galleries. Our countersinks prevent microscopic metallurgical feathering that could dislodge into pressurized lubrication lines.
Automotive Tier-1 Subcontracting
The strategic corridor connecting Plzeň to Bavaria provides just-in-time metallic subassemblies to German automotive assembly networks. High-cycle automated drill presses and CNC indexing tables utilize our 1/4" hex and straight-shank chamfering systems for reliable deburring repeatability across high-volume production batches.
Strategic Sourcing Insights
Evolving Procurement Dynamics in the Czech Engineering Corridor
Purchasing managers and technical directors in Plzeň face shifting supply chains, tightening green mandates, and aggressive automation targets. Here is how modern tool supply addresses these pain points.
Consolidation from Fragmented Vendors to Direct OEM
Middlemen and local trading agencies add 25%–40% surcharges without improving metallurgical traceability. Central European tooling buyers increasingly connect directly with integrated factories that provide comprehensive batch certification, mill test analysis, and direct DIN-standard manufacturing.
Transition Toward High-Efficiency Combined Steps
Labor shortages in Czech manufacturing have accelerated the adoption of multi-operation tooling. Two-subland step core drills and drill-and-countersink combinations cut machine cycle times by consolidating drilling, chamfering, and thread-prepping into a single spindle stroke.
Buffer Stock Warehousing & Just-In-Time Resilience
Supply chain shocks highlight the risk of relying strictly on European spot markets. Industrial consumers in Plzeň increasingly contract scheduled container releases and quarterly safety inventory reserves, ensuring stable, locked-in tool unit prices despite raw steel price fluctuations.
Enterprise Infrastructure
Why Tier-1 Brands & Plzeň Distributors Partner with Us
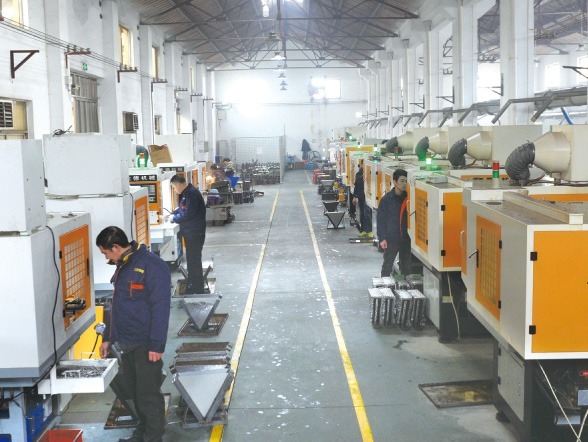
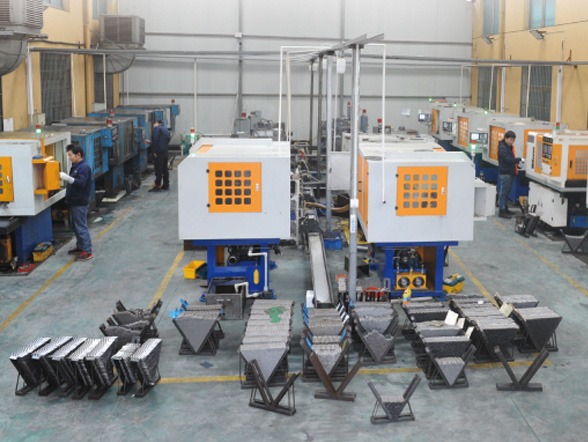
Combining 19 years of production history with rigorous Intertek onsite certification, Jiangsu WRD Tools Co., Ltd. delivers high-volume production economics with fine European grinding precision.
Full-Chain In-House Tool Fabrication
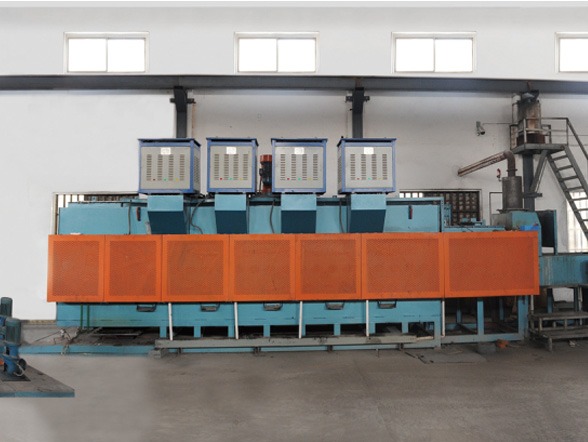
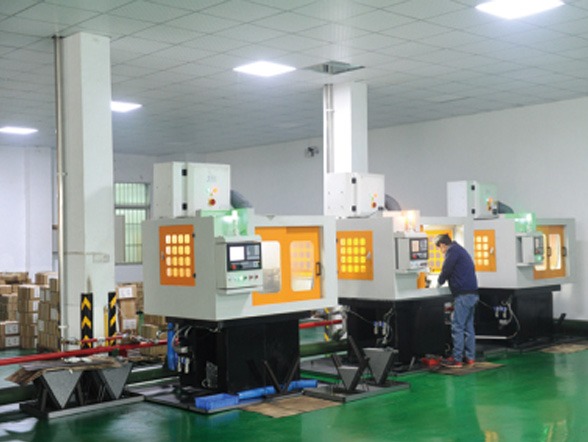
Unlike distributors who source unverified blanks from assorted workshops, our 12,000 m² campus in Danyang maintains total operational sovereignty over every critical production stage.
- Proven OEM Supplier: Contract partner for leading global brands including BOSCH, Milwaukee, DeWalt, Makita, and Heller.
- Intertek Audited & High-Tech Enterprise: Officially recognized high-tech firm equipped with computerized salt-bath and vacuum quenching lines.
- Massive Scalability: Producing 50 million wood drill bits, 25 million HSS twist drills, and 15 million specialized hex tooling units annually.
- Precision Tolerances: Run-out and tip centricity measured with optical comparators down to < 0.005mm.
- Comprehensive Tailoring: Laser etching, DIN/imperial custom diameters, non-standard pilot lengths, and private-label packaging.
Procurement Clarity
Frequently Asked Questions: Sourcing Tools for Plzeň Operations
Direct technical answers addressing the logistics, metallurgical standards, order minimums, and performance criteria relevant to Czech purchasing managers.
Which countersink flute configuration is recommended for heavy steel fabrication?
For structural steels, boilerplates, and locomotive framing common in Plzeň heavy engineering, 3-flute 90° countersinks manufactured from M35 cobalt (DIN 335 Form C) with unequal pitch are strongly advised. Single-flute deburring tools work well for sheet metals, but multi-flute asymmetric designs offer stability and prevent chatter under high-feed radial loads.
How do you ensure conformity with European DIN and ISO machining standards?
Our tools are engineered to strict DIN 335 (countersinks), DIN 338/340 (twist drills), and DIN 352/371/376 (machine & hand taps) standards. Every production batch undergoes hardness verification, dimensional gauge auditing, and concentricity testing before release. Mill test certificates (MTC) and Intertek third-party audit reports are supplied with commercial shipments.
What are the typical Lead Times and shipping routes to Plzeň / Czech Republic?
Standard OEM mass production typically ships within 25–35 days from technical sign-off. Bulk orders move via maritime freight from Ningbo or Shanghai Port to European hubs (Hamburg or Koper), followed by bonded rail or truck transit directly to logistics terminals in Plzeň, Prague, or Lovosice. For urgent tooling samples, direct express air freight delivers within 4 to 6 business days.
What is your Minimum Order Quantity (MOQ) for custom-branded or non-standard tools?
For standard catalog sizes with custom laser-etched branding, our MOQ generally starts at 100 to 500 units per specification. Complete custom-engineered countersinks (special pilot diameters, custom step angles, or specific PVD coatings) start from 200 units, while retail-ready packaged tool sets have an entry volume of roughly 1,200 sets.
How do you resolve edge-burn and premature wear when countersinking stainless alloys?
Stainless steels like AISI 304 and 316 work-harden rapidly under heat. We provide M35 Cobalt or powder-metallurgy HSS tooling with AlTiN or TiCN coating, combined with a wider flute cross-section that facilitates chip clearing. We also provide recommended surface speed (SFM) and chip load charts to ensure your machine operators run the correct parameters, avoiding friction heat.
Request Technical Blueprints & Factory Price Tenders
Whether you require standard DIN 335 countersink programs, custom subland stepped drills, or bulk private-label cutting tools delivered directly to your Plzeň production lines, our technical team provides quotations within 24 hours.
Contact Us