Industrial Tool Supply
Certified Tooling Engineered for Heavy Metallurgy
From DIN standard fully ground twist drills to carbide cutters and bi-metal hole saws, WRD Tools provides end-to-end metallurgical consistency for high-cycle industrial machining in Poland.

SUBORUI 50mm Cross S2 High-Torque Magnetic Screwdriver Bit Set

SUBORUI DIN338 135° Split Point M35 Cobalt HSS Spiral Drill for Inox 304/316

SUBORUI 1/4" HSS Fully Ground Titanium Coated Hex Shank Drill Bit
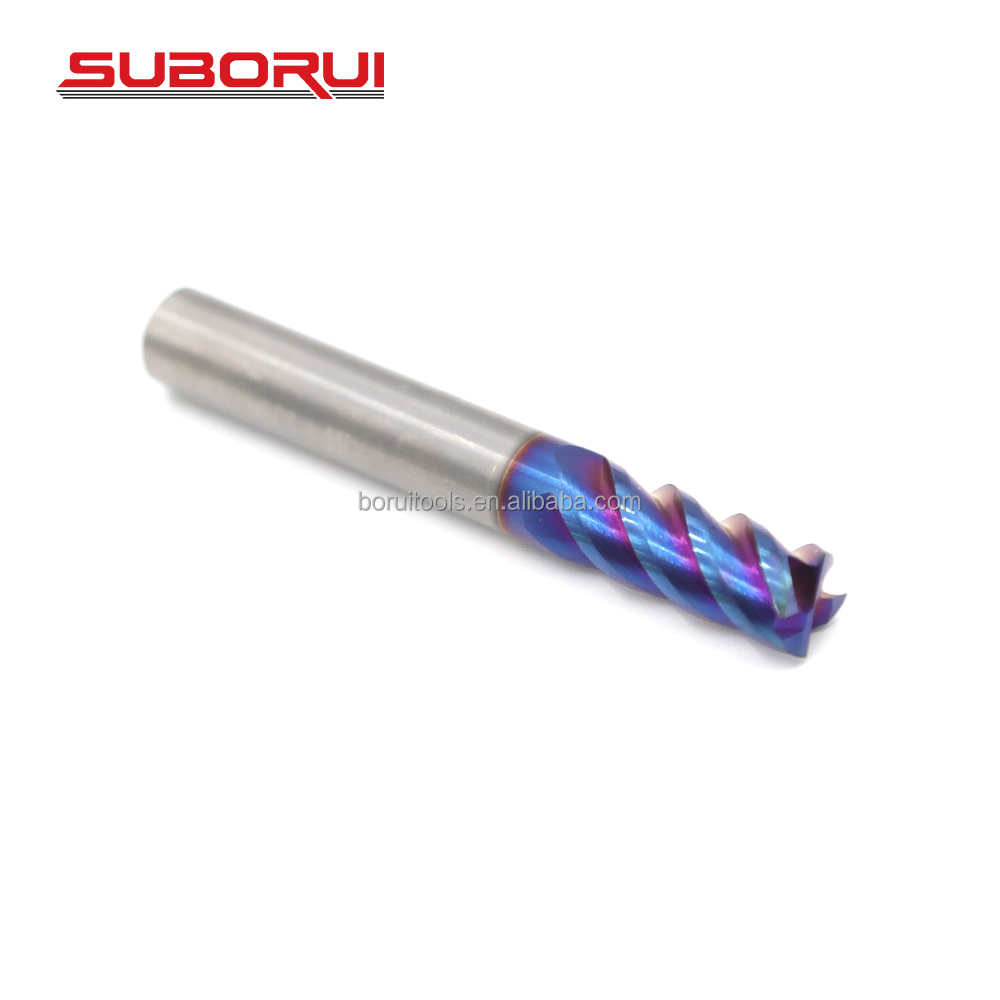
SUBORUI 4-Flute CNC Solid Carbide End Mill HRC65 for Tempered Steel

SUBORUI Premium Hex Shank Co 8% M42 Bi-Metal Heavy Duty Hole Saw Set

SUBORUI DIN352 Metric HSS Straight Flute Threading Taps M2-M10 Set
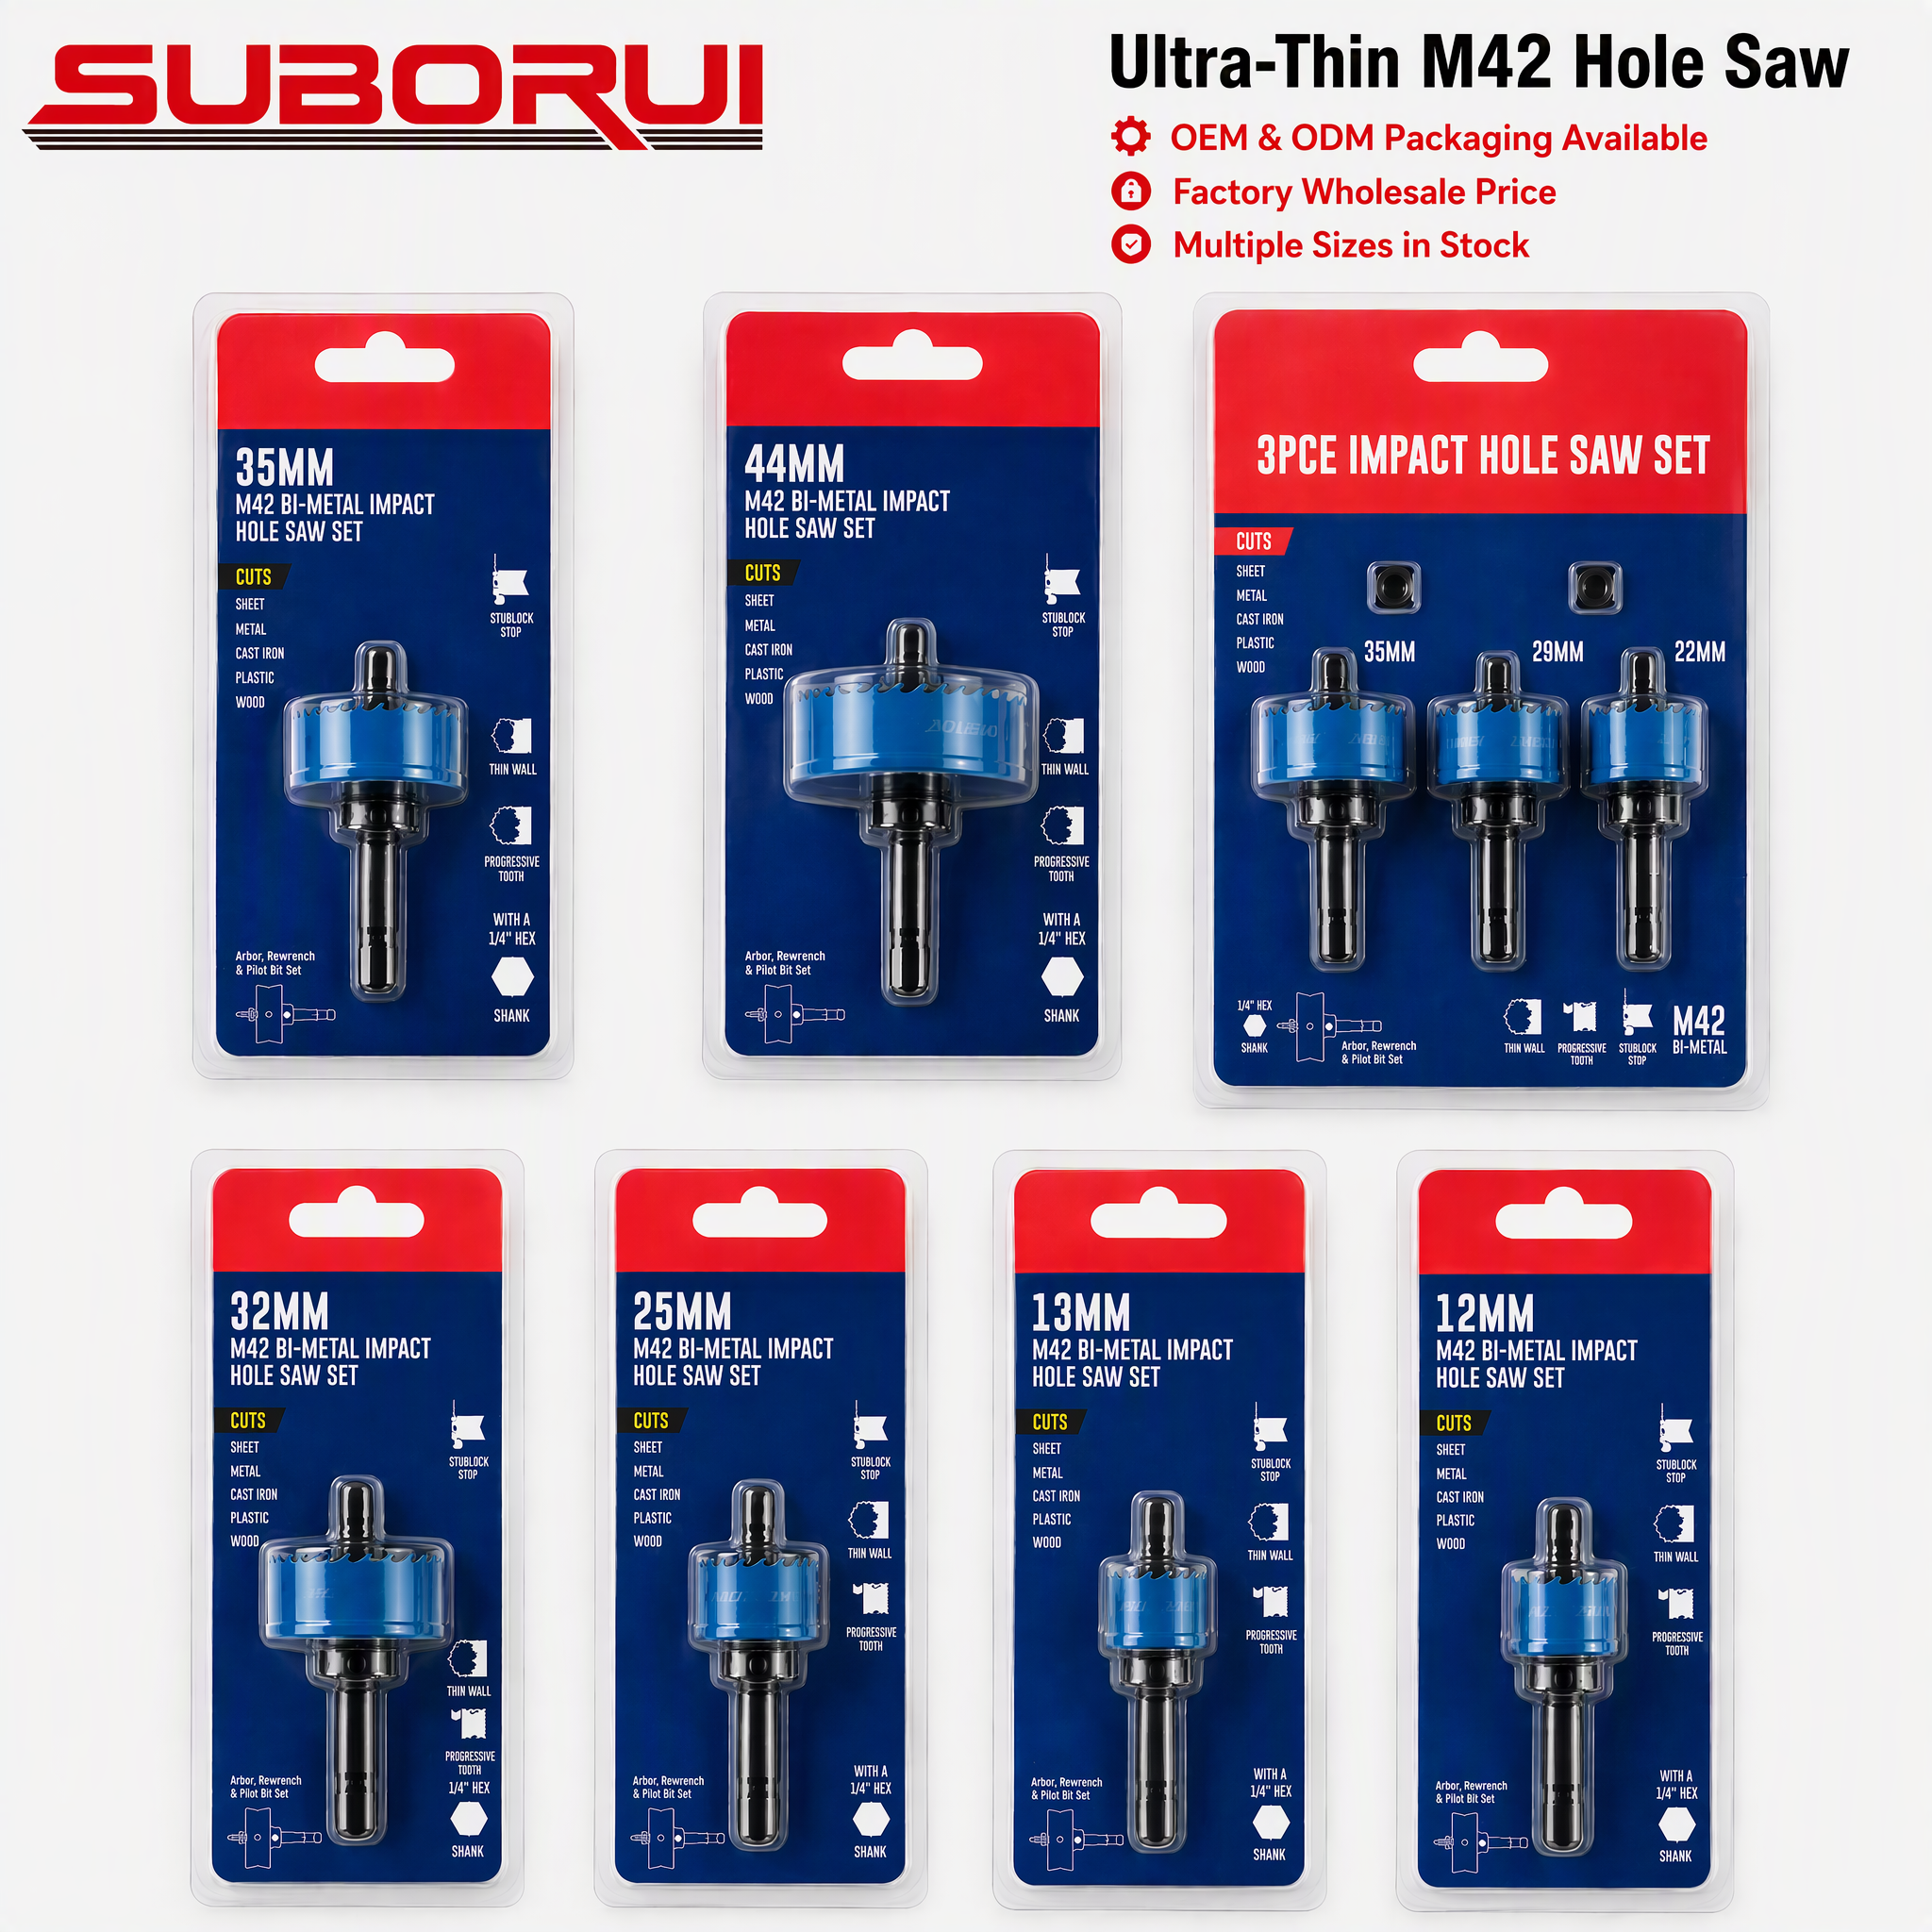
SUBORUI Ultra-Thin 14mm-60mm Hex Shank M42 Bi-Metal Sheet Metal Hole Saw
Metallurgical Superiority
M35 vs. M42 Cobalt High-Speed Steels: Red Hardness Breakdown
For production lines in Poznań machining abrasive, heat-treated, or austenitic stainless steels, tool life is governed by hot hardness and chip evacuation dynamics.
⚙
M35 (HSSE / 5% Co)
Standardized chemical composition with 5% Cobalt. Maintains temper up to 600°C. Delivers 65-66 HRC hardness, making it ideal for structural grade stainless steel 304/316 machining without thermal softening.
⚡
M42 (Super HSS / 8% Co)
High-cobalt formulation achieving 67-69 HRC. Formulated specifically for work-hardening alloys, nickel-chromium matrices, and high-tensile titanium alloys where cutting edge retention under heat is critical.
◇
135° Self-Centering Point
Conforms to DIN 1412 Form C split-point specifications. Eliminates tool deflection and the need for center punching, significantly reducing thrust forces on automated multi-axis transfer machines.
◎
Amber Bronze & TiN Finishes
High-temperature oxynitride and titanium nitride physical vapor deposition (PVD) coatings that reduce coefficient of friction to 0.4, mitigating built-up edge (BUE) and galling during deep-hole cycling.
Regional Synergy
Precision Drilling in the Greater Poland (Wielkopolska) Industrial Ecosystem
Poznań stands as an engineering powerhouse linking Central and Western Europe, characterized by sophisticated manufacturing sectors demanding rigid DIN standard tooling.
🚗 Automotive & Commercial Vehicle Assembly
Greater Poland is a premier manufacturing hub for commercial transport, chassis sub-assemblies, and Tier-1 automotive suppliers (e.g., Antoninek and Swarzędz clusters).
- High-cycle punching & drilling of micro-alloyed automotive high-strength steels.
- Extended-life M35 tooling for robotic arm end-effectors and automated transfer lines.
- Guaranteed concentricity minimizing burr formation on safety-critical bracketry.
🚆 Rolling Stock & Rail Transport Engineering
With major rolling stock manufacturing facilities operating within Poznań, precision drilling in hardened structural frames and austenitic rail car panels is routine.
- Heavy structural steel drilling using DIN345 Morse taper and heavy DIN1869 bits.
- HSS-Co and TCT annular cutters engineered for rapid magnetic drilling on rail tracks.
- Extreme thermal resistance during uninterrupted multi-hole plate perforation.
🏭 Stainless Processing & Logistics Modernization
The concentration of food-grade stainless processing systems, chemical equipment fabricators, and warehouse logistics automation around Poznań creates intense tool wear demands.
- Drilling surgical and food-contact grade 316L without surface work hardening.
- Thin-gauge sheet metal piercing using M42 bi-metal and specialized step drills.
- Zero chemical contamination tooling conforming to strict EU environmental criteria.
Manufacturing Trends Across Poznań and the A2 Industrial Corridor
Industrial operations in Poznań, Komorniki, and Tarnowo Podgórne are progressively migrating toward lean, automated production matrices (Industry 4.0). Under these conditions, the real cost of a cutting tool is not its purchase price, but the downtime caused by premature tool fractures or edge rounding. Low-grade HSS 4241 tools often burn out when entering tough stainless matrices due to lack of cobalt, causing torque spikes that can trigger machine-tool error shutdowns.
WRD Tools supplies factory-direct M35 and M42 drill bits that offer predictable tool life expectancy, allowing machine engineers across Wielkopolska to calculate precise cycle replacements, improve feed rates by up to 25%, and ensure ISO 9001-compliant hole diameters for subsequent threading operations with DIN352 and DIN371/376 taps.
Factory Direct Authority
Intertek-Verified Manufacturing Scale & Reliability
Jiangsu WRD Tools Co., Ltd. (operating from Danyang's specialized cutting tool cluster since 2007) operates as an authentic OEM/ODM facility, not an export broker.
2007
Founded in Danyang
12,000 m²
Factory Facility
90M
Annual Bit Output
150+
Specialized Staff
End-to-End Metrology & Quality Control
Recognized as a High-Tech Enterprise of Jiangsu Province in 2019 and audited onsite by Intertek Group, WRD Tools operates closed-loop manufacturing for all product lines. Every batch of M35 and M42 raw steel bar stock is subjected to optical emission spectrometry to verify accurate Cobalt (5% or 8%), Molybdenum, Tungsten, and Vanadium concentrations before entering rough machining.
Our workshop houses high-precision CNC multi-axis flute grinders, computerized vacuum salt-bath heat treatment chambers ensuring consistent microcrystalline martensitic structures, and automatic laser measurement benches testing concentricity, total indicated runout (TIR < 0.02mm), and split-point web thickness. Over the past 19 years, our production capacity has established OEM partnerships serving cutting-tool brands across Germany, Switzerland, Sweden, the United States, and across European distribution channels.
Procurement Inquiries
Frequently Asked Questions by Industrial Importers in Poznań
Direct technical answers addressing customs, DIN standards, metallurgical traceability, and OEM supply logistics for Polish enterprises.
How does WRD Tools ensure compliance with EU customs and Polish industrial norms?
All industrial drill bits exported to Poland conform strictly to DIN parameters (DIN 338 jobber, DIN 340 long shank, DIN 1897 stub, and DIN 345 Morse taper). Shipments are accompanied by complete Material Test Reports (MTR / EN 10204 3.1 certification), RoHS declarations, and accurate TARIC/HS code classification (820750) ensuring clear clearance through Gdynia, Gdańsk, or European inland customs terminals.
What are the specific parameters recommended for drilling Stainless Steel 304/316?
When using our M35 DIN338 cobalt bits on austenitic stainless steels, surface cutting speeds (Vc) should be maintained between 10-15 m/min with continuous emulsion or cutting oil lubrication. The 135° split point requires steady, positive feed pressure (0.04-0.10 mm/rev depending on diameter) to prevent work hardening caused by tool dwelling or rubbing.
Can we request private-label laser etching, custom casing, and local EAN barcoding?
Yes. As an OEM manufacturer, we support complete private-label configuration. This encompasses high-contrast laser marking on the tool shank (brand name, diameter, HSS-Co mark), bespoke industrial packaging (rose plastic tubes, metal indexed cassettes, blister cards), and retailer-ready EAN-13 barcodes optimized for Central European distributors.
What are standard lead times and Minimum Order Quantities (MOQ) for imports to Poland?
For standard bulk items, single-size MOQs start from 100 to 500 pieces, while packaged drill bit sets start from 1,200 sets. Production lead times typically span 25-35 days. Shipments can be booked FOB Shanghai or CIF Gdynia/Hamburg, with air freight and rail options (China-Europe Railway Express directly to Małaszewice/Warsaw/Poznań terminals) available for rapid replenishment.
Connect Directly with Our Export Engineering Team
Send your drawings, material specifications, or private-label packaging requirements. Our metallurgical sales engineers provide detailed commercial quotes and sample dispatches within 24 hours.