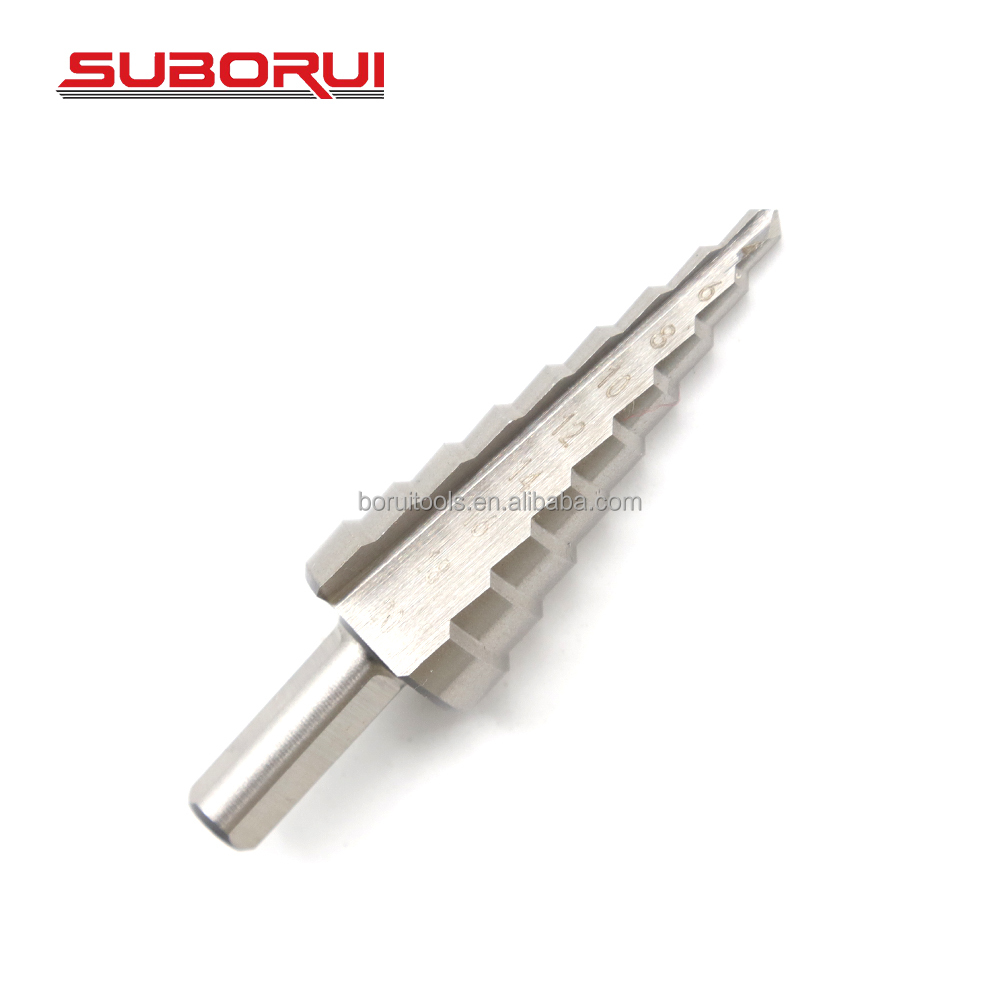
SUBORUI Custom Industrial Metric Straight Flute 4-12mm HSS 4241 Woodworking Metal Unibit Step Drill Bit
Engineered for sheet metal fabrication, control cabinet modifications, and clean burr-free enlargement across aluminum profiles.
From internal threading on high-tensile structural steels to high-speed drilling across non-ferrous and composite alloys, our direct-factory catalog balances batch-to-batch repeatability with customized DIN and ISO tolerances.
Engineered for sheet metal fabrication, control cabinet modifications, and clean burr-free enlargement across aluminum profiles.
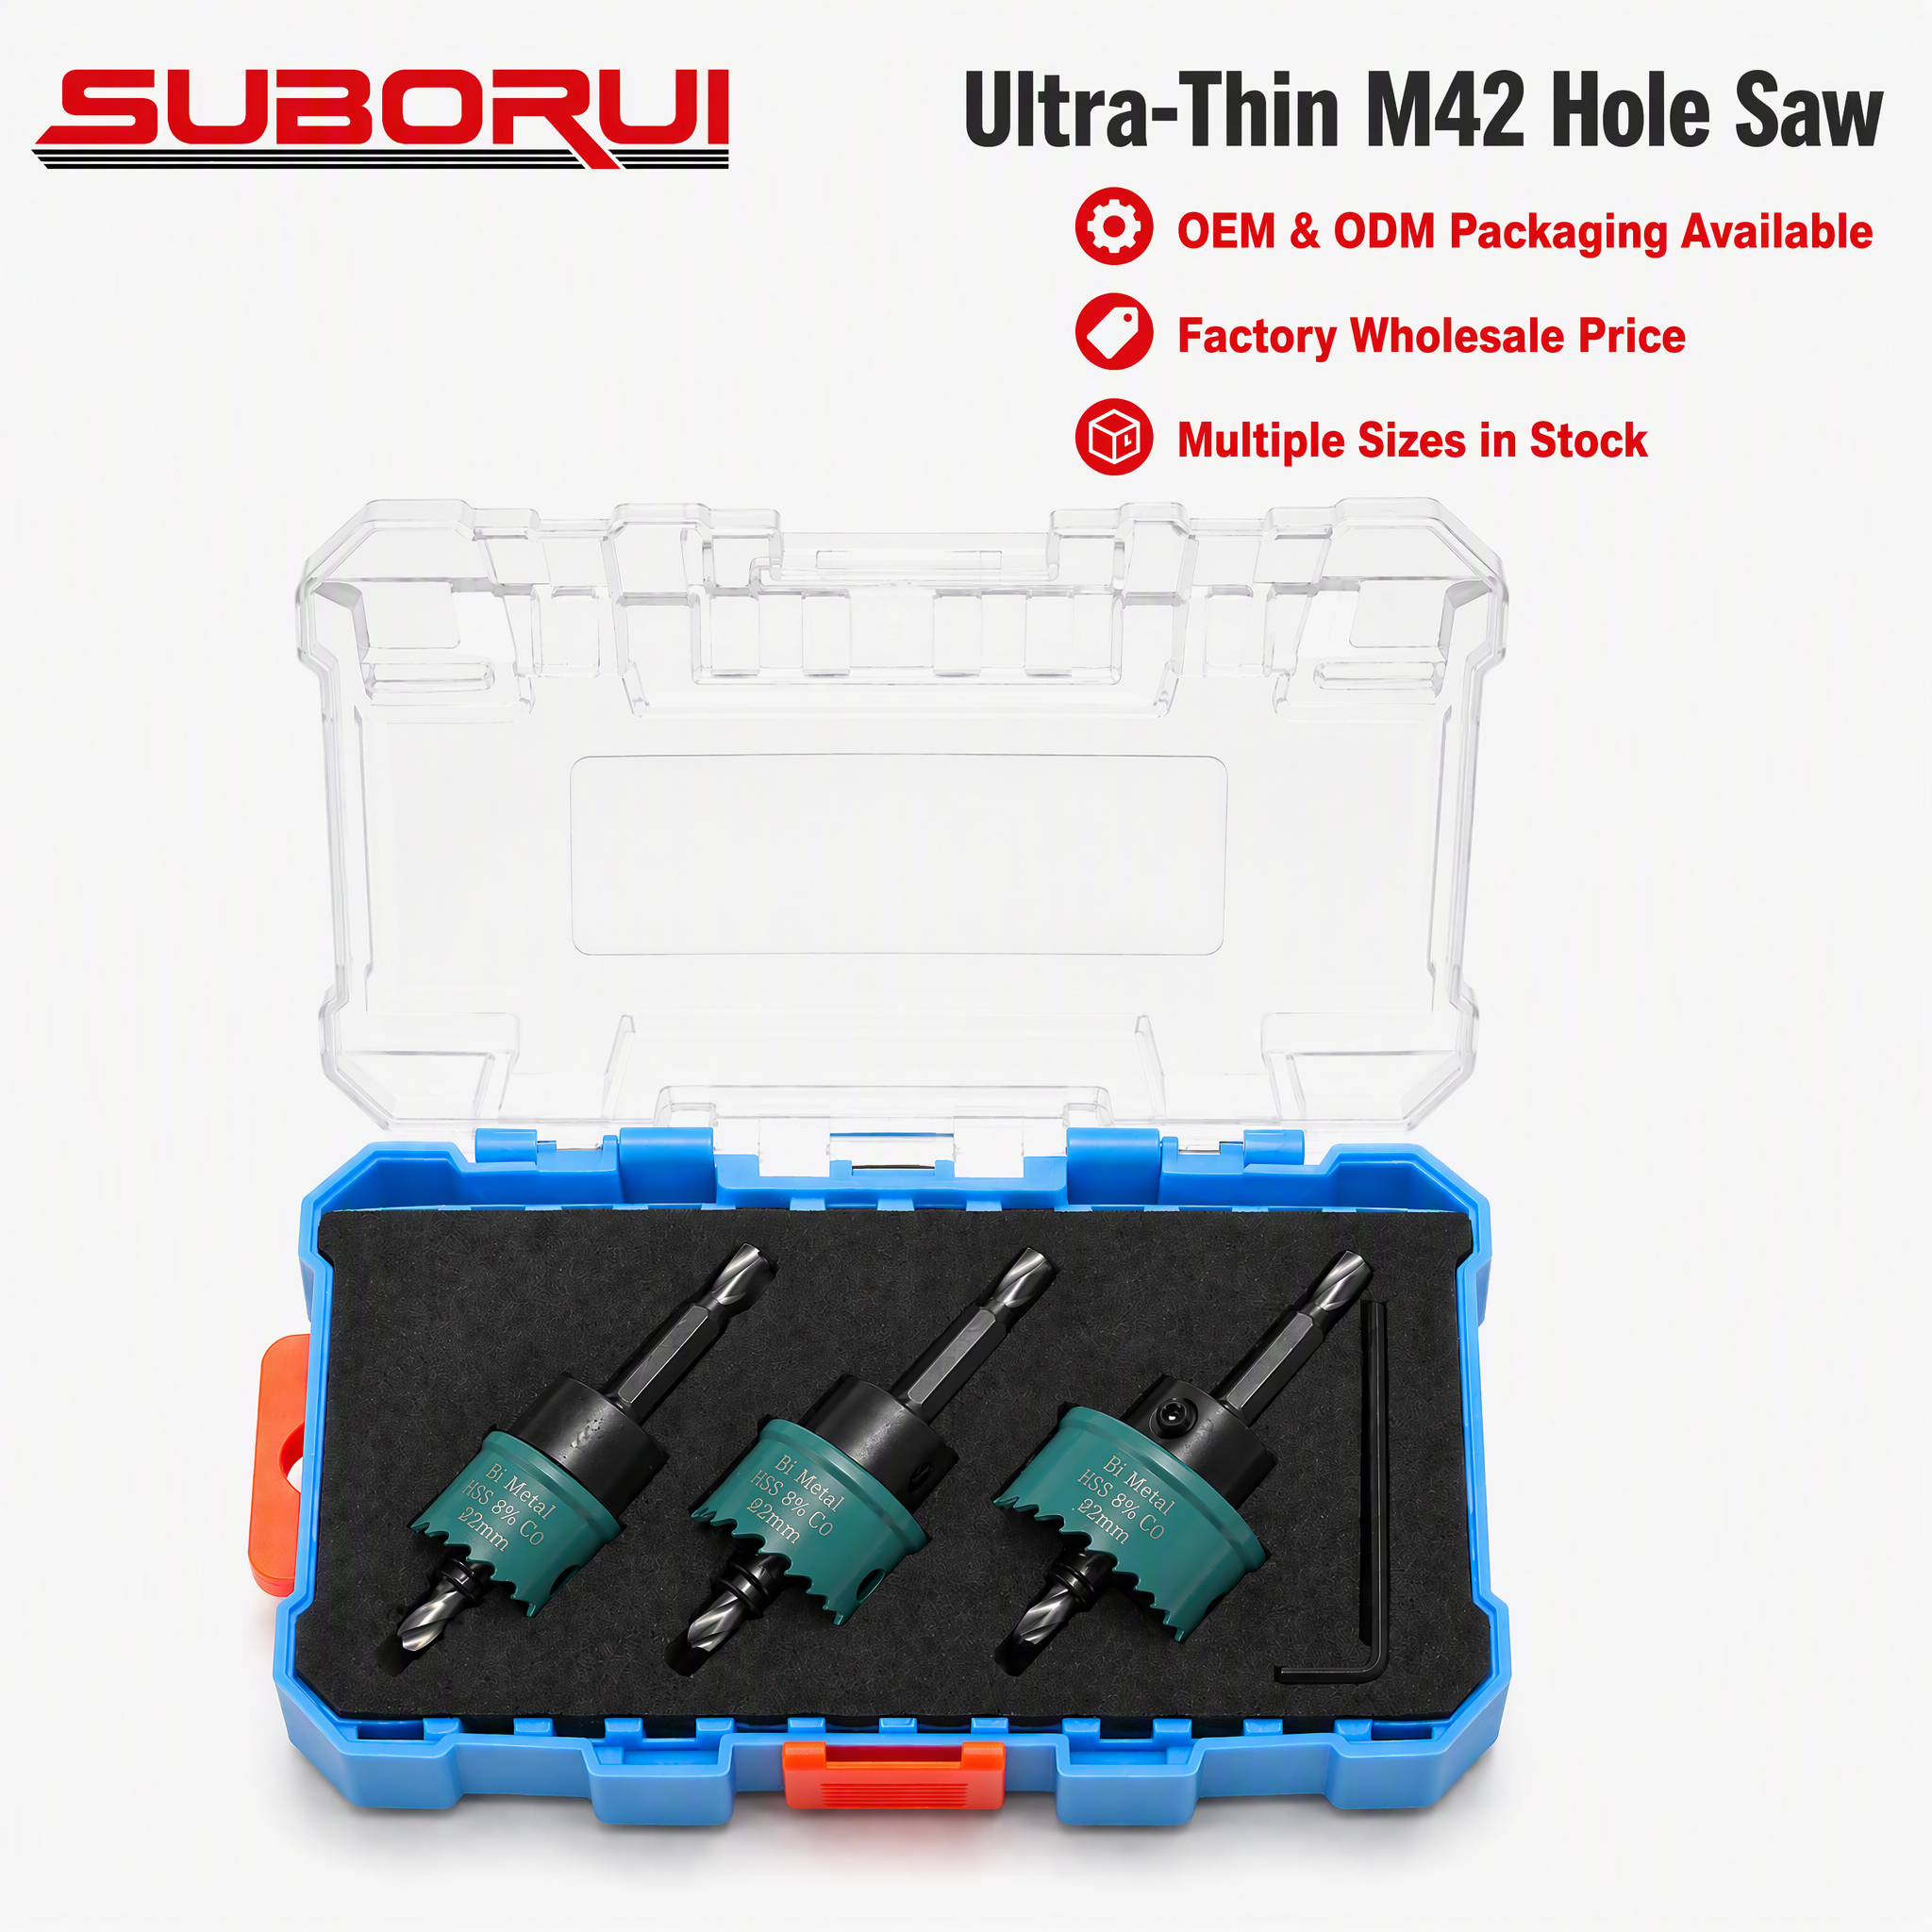
Featuring 8% Cobalt M42 matrix with variable pitch pitch geometry for rapid penetration in pipework and steel trunking.
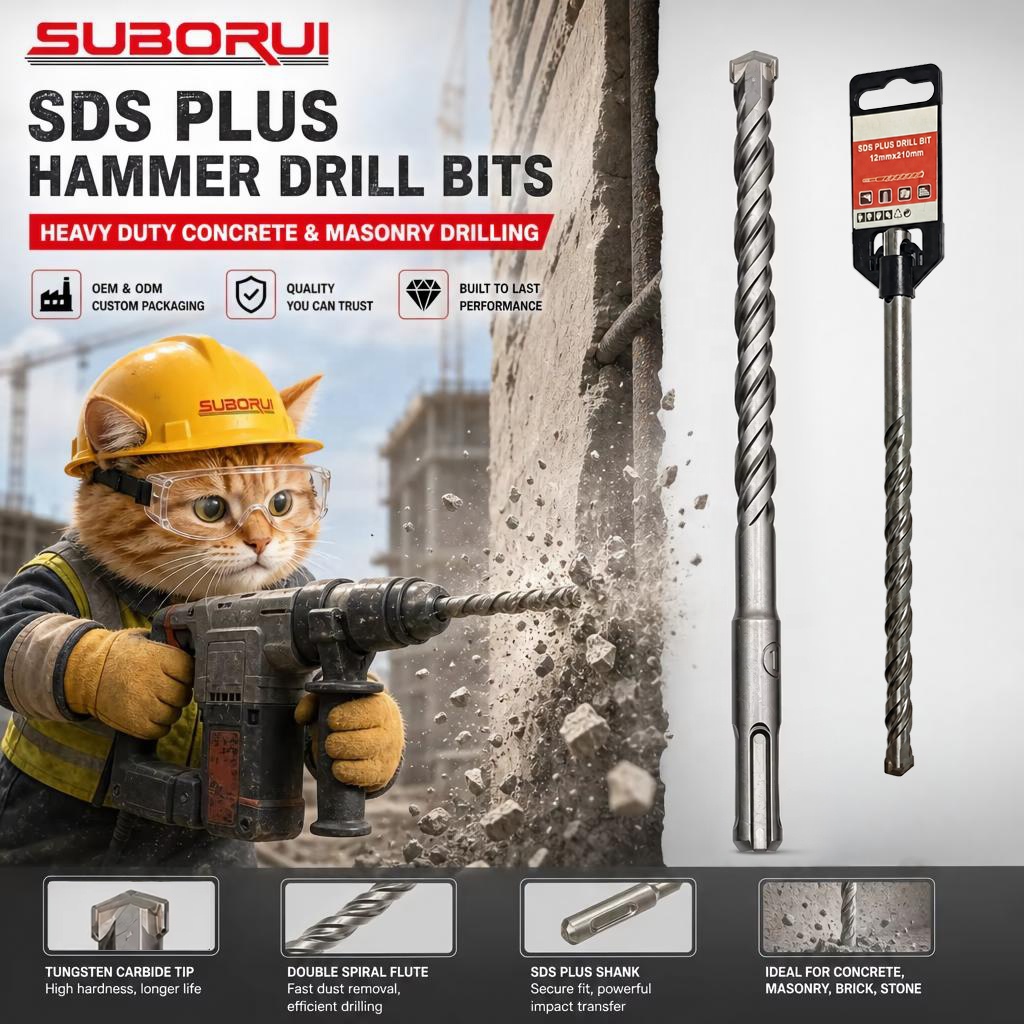
High-torque vacuum-brazed tungsten carbide head engineered for rapid debris evacuation in dense concrete and infrastructure anchoring.

High-speed structural hole-making in composite assemblies, high-alloy sheets, and structural timber installations.

Dynamic balance tested for high-speed surface remediation, screed levelling, and thick coatings removal on civil build sites.
Optimized thin-kerf configuration reducing tool load and extending battery runtime across standard cordless impact systems.

Clean-edge architectural ceiling penetration system for precision lighting retrofits, dry-lining, and acoustic plasterboards.

Fully ground flute geometry with enhanced red-hardness; prime specification for heat-resistant steels and stainless alloys.
The manufacturing ecosystem of Vienna and the Lower Austria (Niederösterreich) industrial belt requires specialized internal threading protocols that conform to stringent European machining tolerances and work-hardening mitigation standards.
Vienna's specialized engine and transmission production corridors (such as facilities in Wien-Aspern) utilize automated CNC machining centers requiring DIN 371/376 machine taps with reinforced shanks and vaporized or TiCN surface treatments.
Our spiral point taps ensure chip clearance forward through through-holes in ductile iron and transmission cast steel, eliminating tool stall and catastrophic fluting failure during continuous high-cycle operations.
Modernized rail networks (ÖBB projects and Wiener Linien track switch manufacturing) demand threading in tough structural alloys (S355J2, manganese rail steels, and high-tensile austenitic steels).
We supply HSS-E / M35 Cobalt (5% Co) machine tap sets featuring specialized 35° spiral flute angles that effortlessly draw continuous chips out of blind holes without damaging thread pitch integrity or galling the bore walls.
Vienna's pharmaceutical production plants and regional chemical refineries frequently specify precision metric threads inside high-purity AISI 316L and duplex stainless vessel housings.
Using our precision-ground HSSE-PM (Powder Metallurgy) machine taps prevents micro-cracking and maintains accurate 6H tolerance classes, eliminating subsequent thread rectification during critical vacuum audits.
A systematic comparison guide to assist procurement engineers and shop-floor leads across Austria in selecting optimal tap geometeries for specific metal compositions.
| Steel Substrate / Grade | Hardness Range | Primary Flute Form | Recommended Coating | Application Match (Vienna Industrial Standard) |
|---|---|---|---|---|
| HSS 6542 (AISI M2) | 63 – 65 HRC | Straight Flute / Spiral Point | Bright Finish / Black Oxide | Mild structural steels up to 750 N/mm², brass, free-machining carbon steels. |
| HSS-E Cobalt (AISI M35 - 5% Co) | 65 – 67 HRC | Spiral Flute 35° / 45° | TiN (Titanium Nitride) Gold | Stainless steel (1.4301 / 1.4404), alloyed tooling steels up to 1000 N/mm². |
| HSS-Co8 (AISI M42 - 8% Co) | 67 – 69 HRC | Spiral Flute with Neck Relief | TiCN / AlTiN Micro-Layer | Hardened cast iron, heat-treated dies, titanium alloys, continuous high-temp cuts. |
| HSSE-PM (Powder Metallurgy) | 67 – 70 HRC | Optimized Synchro Tapping Flute | Nano-Composite TiAlN | High-speed synchronized tapping in automotive CNC lines, abrasive aerospace grades. |
Industrial manufacturing across Vienna and Central Europe is undergoing structural shifts toward digitized, high-efficiency cutting configurations.
Traditional floating tap chucks are widely replaced by rigid CNC synchronization. Modern Austrian machine shops demand factory tap sets with tighter diameter variances on the shank (h6/h7) to eradicate axial vibration at rotational speeds exceeding 2,500 RPM.
Environmental standards in the European Union are restricting heavy flood coolant usage. Our factory delivers machine taps with mirror-polished flute surfaces and DLC or high-temperature TiAlN coatings to support Minimum Quantity Lubrication (MQL) protocols.
Vienna-based tooling buyers require verifiable metallurgical origin certificates (3.1 inspections) and laser etched lot identification on each machine tap to fulfill ISO 9001 quality audits throughout Tier 1 subcontract supply chains.
Operating as an authenticated manufacturing power since March 2007, Jiangsu WRD Tools Co., Ltd. delivers direct OEM/ODM industrial capability from Danyang, China's core tooling cluster.
Our 12,000 m² physical plant, dedicated heat treatment lines, and comprehensive QC testing stations are inspected and verified onsite by the Intertek Group.
With 150+ trained technicians and an output of over 90 million cutting units annually, we guarantee high-capacity production without subcontracted quality dilution.
Awarded Jiangsu High-Tech Enterprise status since 2019, our in-house metallurgical R&D team optimizes tool geometries for extended tool life and torque resilience.
Longstanding supplier footprint delivering high-volume private label tooling for premium global brands including Bosch, Milwaukee, DeWalt, Makita, and Heller.
Key transactional, regulatory, and technical specifications for direct factory importing into Austria and Central European channels.
Direct communication with our senior engineering and export division. Submit your target drawings, DIN/ISO tap specifications, or annual procurement volume for an actionable commercial and technical quotation within 24 hours.