Featured Industrial Machine Taps & Rotary Tooling Solutions
Standardized to European DIN metric profiles, fully ground, and heat-treated for automated CNC threading, heavy fabrication, and maintenance operations.

SUBORUI DIN338 135 Degree Split Point M35 Cobalt HSS Drills CNC Spiral Twist Drill Bit for Stainless Steel 304
View Specifications →
BORUI Manufacturer D338 M35 Hss 5% Cobalt Steel 118 Degree Imperial Hss Co Bohrer Broca Drill Bit Amber High Speed Steel
View Specifications →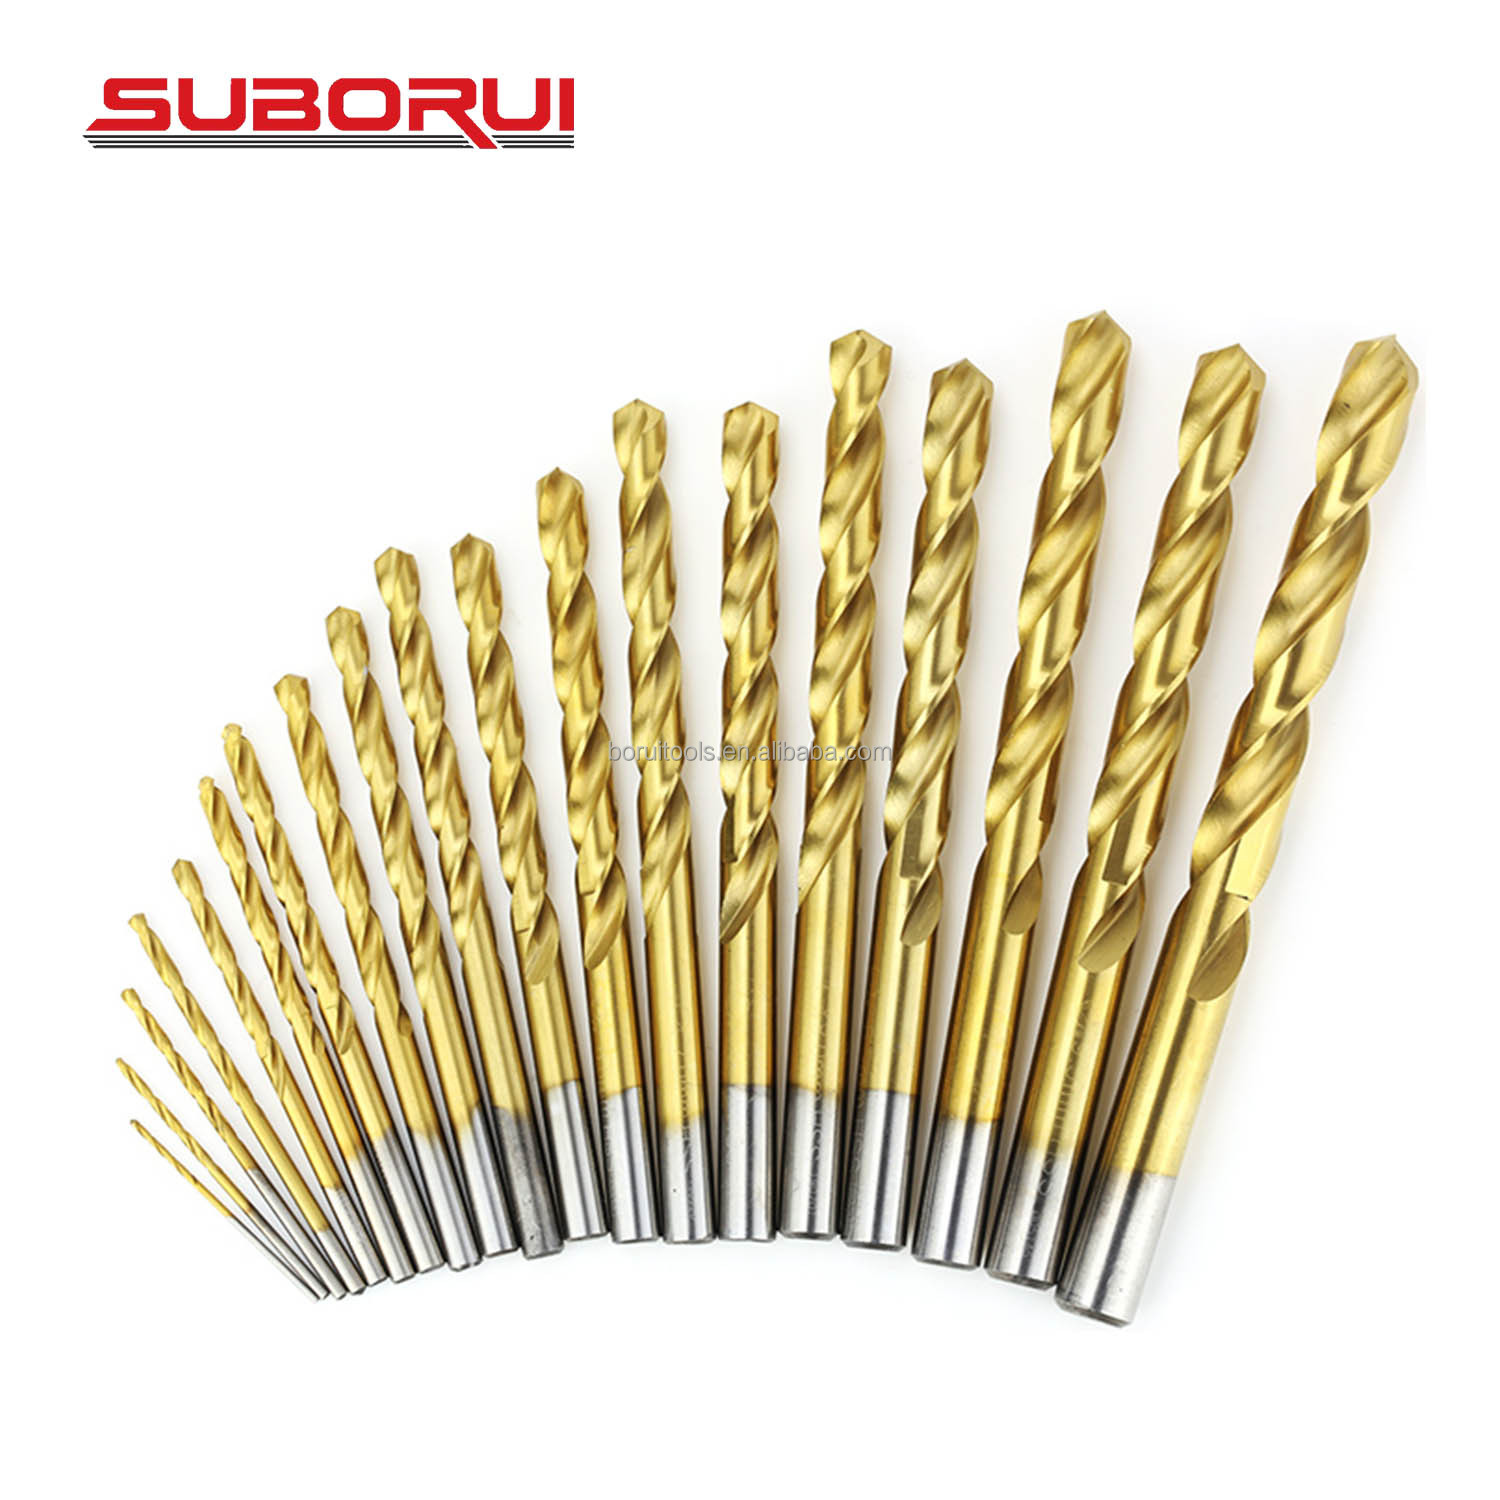
SUBORUI DIN338 Fully Ground Titanium 1-20mm Customized Tin Coated Hss M2 6542 Metal Twist Drill Bits
View Specifications →
SUBORUI OEM ODM Wholesale Price Premium Hex Shank Drill Bit Hss CO8% M42 Bi-Metal Hole Saw Set Kit for Metal Wood
View Specifications →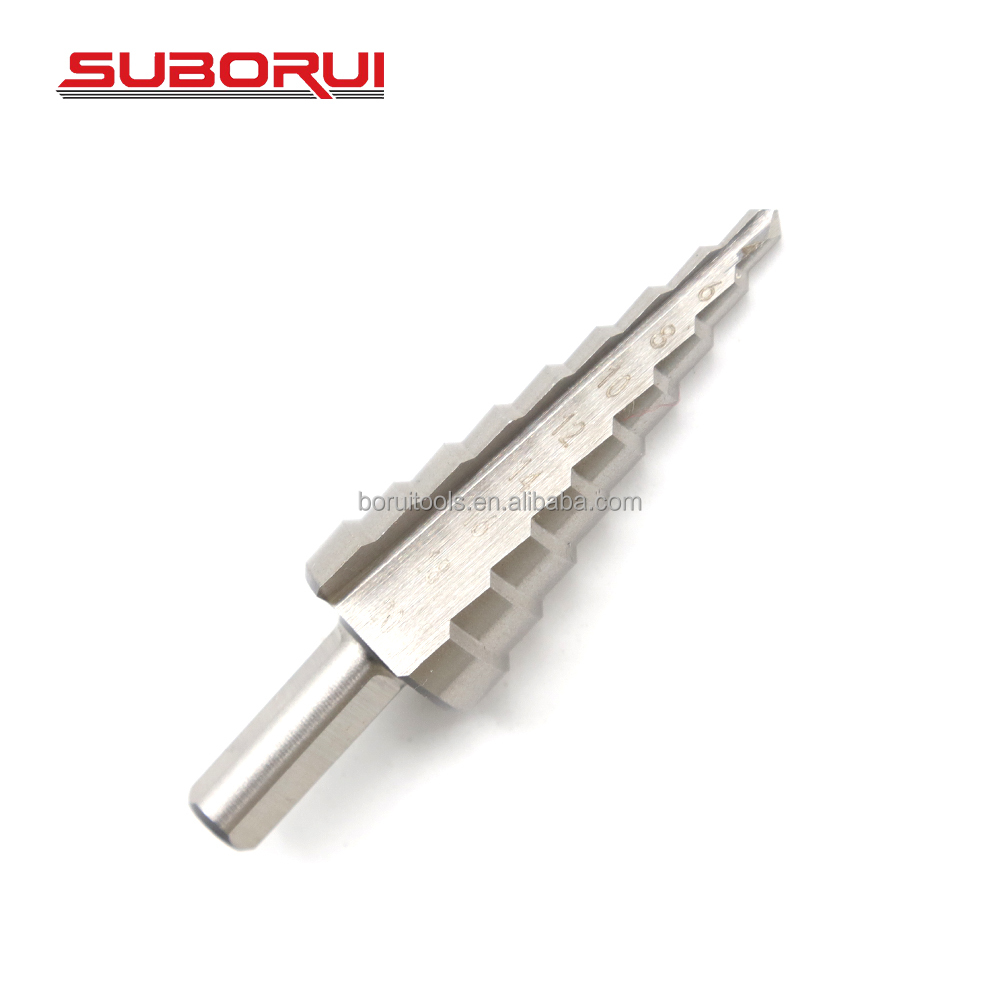
SUBORUI Custom Industrial Metric Straight Flute 4-12mm HSS 4241 Woodworking Metal Unibit Step Drill Bit for Wood Metal Aluminum
View Specifications →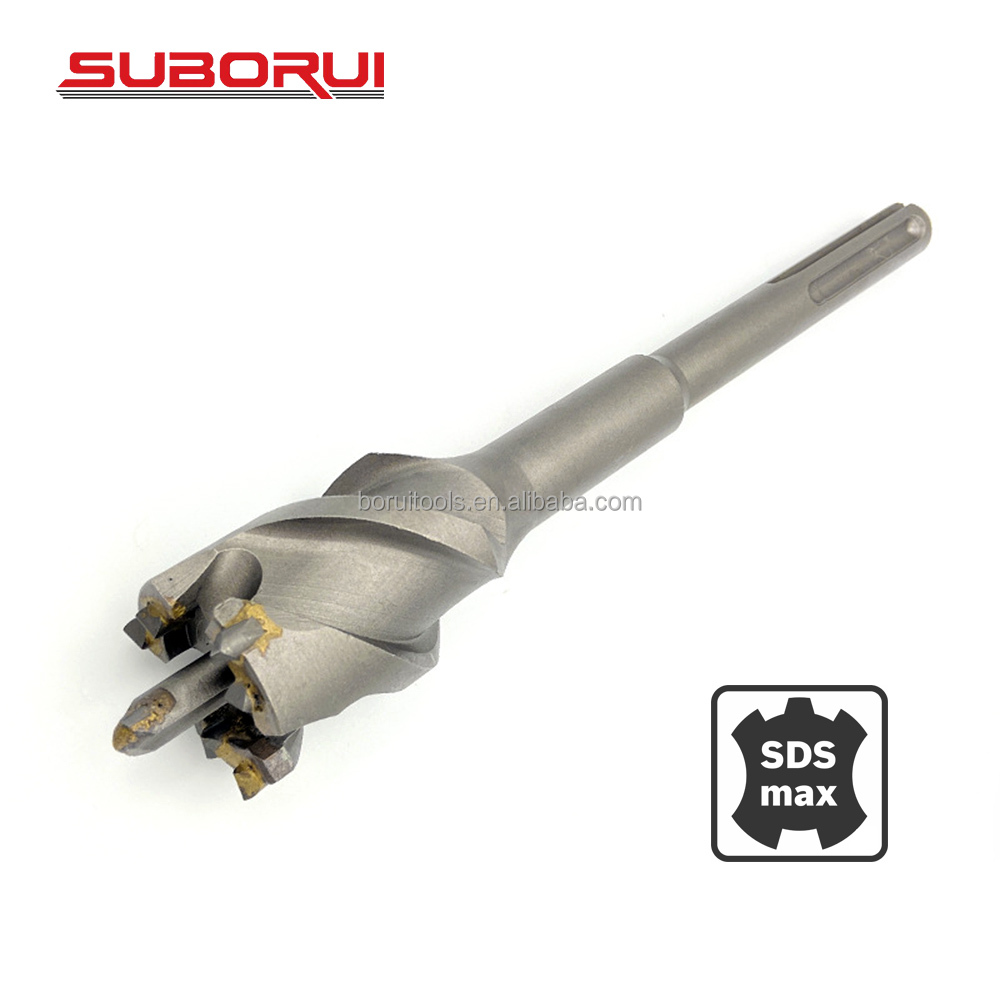
SUBORUI Carbide Sds Max Electric Hammer Wall Hollow Drill Bit Concrete Hole Saw for Cement Stone Concrete Wall
View Specifications →
SUBORUI Manufacturer DIN338 Fully Ground M35 Co5% Metal Cobalt Hss Twist Drill Bit for Metal Stainless Steel Drilling
View Specifications →
SUBORUI Din352 Metric Hss M2 3PCS M2 M3 M4 M5 M6 M8 M10 M12 M14 M16 M18 M20 HSS Straight Fluted Screw Thread Hand Taps Set
View Specifications →2007
Established Baseline
12,000 m²
Integrated Production Plant
90 Million
Annual Cutting Tools Produced
Intertek
Onsite Verified Facility
Precision Machining & Threading Dynamics in the Greater Ghent Industrial Basin
Technical alignment between high-volume Chinese manufacturing precision and Flemish heavy-duty engineering requirements across East Flanders and North Sea Port.
Automotive & EV Drivetrain Subcontracting
The industrial spine along the Kennedylaan in Ghent is anchored by major automotive manufacturing, including the Volvo Cars Gent assembly plant and tier-one drivetrain, battery housing, and chassis sub-suppliers. High-speed CNC tapping centers operating in this zone demand rigorous repeatability in blind-hole tapping.
Our DIN 371 / DIN 376 spiral flute taps (35° and 45° helix angles) engineered from high-speed steel with 5% cobalt (M35 / HSSE) ensure clean chip evacuation upward, preventing chip packing when tapping cast aluminum, nodular cast iron, and micro-alloyed structural steels commonly used in modern vehicle frames.
North Sea Port Maritime & Offshore Maintenance
Ghent’s cross-border logistics and port cluster—encompassing Kluizendok, Rodenhuizedok, and the Terneuzen-Ghent Canal—demands heavy-duty threading solutions for marine cranes, container handling equipment, dredging pumps, and offshore support vessels.
Tapping through structural steel plates (S235JR, S355J2) and seawater-exposed fasteners requires gun-nose (spiral point) straight-flute machine taps with Form B chamfers (4 to 5 threads). These push chips forward through open holes under high torque, providing long tool life and minimizing spindle stalls on heavy radial drills and magnetic drilling units.
ArcelorMittal Ghent & Heavy Metallurgy Services
As one of Europe's premier integrated flat-steel production sites, ArcelorMittal Gent and surrounding mechanical maintenance contractors routinely face high-tensile hot-rolled steel, wear-resistant sheets, and structural profiles. Threading wear plates and structural assemblies requires tools capable of withstanding severe work hardening.
Our M35 Cobalt and Powder Metallurgy (HSS-PM) machine tap sets, treated with multi-layer Titanium Carbonitride (TiCN) or Aluminium Titanium Nitride (AlTiN) coatings, maintain thermal hardness up to 650°C. This eliminates flank galling and guarantees ISO 2 (6H) thread tolerance across repetitive structural bolt-hole machining.
Machine Tap Architecture: Metallurgical Grades & Flute Selection for Ghent Machine Shops
A rigorous specification matrix designed to assist toolroom managers, CNC programmers, and procurement specialists in Flanders in matching tap geometries directly to parent materials.
| Geometry / Type | Standard & Chamfer | Primary Substrate | Target Materials (DIN / EN) | Chip Evacuation Mode |
|---|---|---|---|---|
| Spiral Point (Gun Nose) | DIN 371 (M2-M10) / DIN 376 (≥M12) Form B (4-5 threads) |
HSS-E (M35 Co5%) / M2 (6542) | Through-holes in low-carbon steel, alloy steel, plate steel (S355, 42CrMo4) | Pushes continuous chips forward ahead of the cut; prevents fluting jams. |
| Spiral Flute (35° / 45° RSP) | DIN 371 / DIN 376 Form C (2-3 threads) |
HSS-E Cobalt + TiN / TiCN Coated | Blind-holes in stainless steel (AISI 304/316), ductile irons, aerospace alloys | Pulls helical chips backward out of the hole, preserving bottom thread integrity. |
| Straight Flute (Hand / Machine) | DIN 352 / DIN 351 Form A / C / D sets |
High Speed Steel M2 / 4241 | General workshop repair, maintenance, cast iron, short-chipping non-ferrous | Stores chips within flutes; optimal for batch manual threading and maintenance. |
| Cold Forming (Roll Taps) | DIN 371 / DIN 2174 Form E (1.5-2 threads) |
Powder Metal (HSS-PM) + TiAlN | Aluminum alloys (AlSi1), copper, brass, austenitic stainless with >10% elongation | Chipless thread displacement; increases thread fatigue resistance by 20-30%. |
1. Transition to Minimum Quantity Lubrication (MQL) in Flanders
Industrial sustainability policies in the Flemish Region are aggressively penalizing hazardous water-miscible metalworking fluid waste. Machine shops in the Ghent seaport district and automotive plants are increasingly retrofitting CNC machine tools for internal or external MQL.
This shift requires machine taps with specialized surface topologies. Standard bright-finish taps frequently experience cold welding (micro-galling) when tapping sticky austenitic stainless steel or structural alloy steels under micro-lubrication. Our specialized vaporized (VAPO) steam-tempered oxide surfaces and nanostructured TiAlN coatings act as a solid thermal barrier, lowering friction coefficients below 0.35 and permitting dry or near-dry tapping without premature catastrophic fracture.
2. Synchronous Rigid Tapping & High-Torque Spindle Optimization
With modern machine tools from Mazak, DMG MORI, and Hurco dominating Flemish precision manufacturing, CNC programmers operate at significantly elevated cutting speeds (>15-25 m/min in steels). Traditional tension-compression tap holders have been replaced by synchronous rigid tapping collets.
Rigid tapping requires ultra-precise runout limits (≤ 0.005 mm) on the tap shank and square drive to prevent excessive flank wear and pitch synchronization errors. Our CNC-ground DIN taps maintain concentricity tolerances that eliminate oversized threads (preventing 6H gauge rejections) and ensure balanced chip loads across all cutting teeth, extending cycle counts by up to 45% compared to conventionally rolled tooling.
Direct Factory Capabilities: Danyang Cluster Manufacturing Powerhouse
Founded in March 2007, Jiangsu WRD Tools Co., Ltd. (SUBORUI) operates from China’s cutting-tool manufacturing epicenter in Danbei Town, Danyang, Jiangsu, delivering certified tooling directly to European wholesale channels.
19 Years of Specialized Toolmaking
With RMB 10 million in registered capital and a continuous operational record since 2007, our 12,000 m² manufacturing plant houses dedicated workshops for machine taps, twist drills, annular cutters, and hole saws. Recognized as a High-Tech Enterprise of Jiangsu Province in 2019, we engineer our products to withstand rigorous industrial duty cycles.
Intertek Onsite Audited Facility
Integrity and compliance are verified independently. Our production facilities, QA/QC laboratories, salt-bath vacuum heat-treatment lines, and optical measurement benches have been audited onsite by Intertek. Buyers in Ghent, Antwerp, and across Western Europe can source directly with total visibility into metallurgical tracking and quality control.
Trusted OEM / ODM Track Record
Our tooling is relied on across more than 20 export destination countries, including Germany, the United States, Switzerland, and Sweden. Over our decades of operation, we have manufactured and supplied cutting tools for globally recognized tool brands such as BOSCH, Milwaukee, DeWalt, Makita, Wolfcraft, and Heller.
Frequently Asked Questions for Industrial Buyers in Ghent & Belgium
Direct answers addressing technical standard compliance, shipping logistics to North Sea Port / Antwerp, and private-label customization.
What is the primary operational difference between DIN 371 and DIN 376 machine taps?
DIN 371 machine taps feature a reinforced shank where the shank diameter matches or exceeds the nominal thread diameter, standard for thread sizes from M2 up to M10. DIN 376 machine taps feature a reduced-diameter shank (shank diameter is smaller than the thread major diameter), which allows deep tapping past the nominal flute length without interference. For M12 and larger, DIN 376 is standard across European machine tools. We manufacture both configurations strictly conforming to DIN 13 thread standards and ISO 2 (6H) class tolerance.
How does your factory solve chip-jamming when tapping blind holes in stainless steel (AISI 304/316)?
In Ghent's maritime, chemical, and bio-processing engineering facilities (such as those in the Ghent Bio-Energy Valley), tapping AISI 304 and 316 stainless is frequent. We resolve chip packing by utilizing a 45° right-hand spiral flute (RSP) geometry ground with a 10°-12° positive cutting rake and eccentric flute relief. This design shears the work-hardening stainless steel chip and smoothly lifts the continuous ribbon upwards out of the hole. Paired with M35 (HSS-E 5% Cobalt) or TiCN coating, it resists chip welding and edge chipping.
What logistics routes and lead times apply for bulk orders delivered to Ghent or Antwerp?
Finished goods are dispatched from our factory in Danyang to Shanghai Port (approx. 200 km). FCL and LCL ocean shipments transit via regular direct carrier loops to the Port of Antwerp-Bruges or directly into North Sea Port (Ghent dock area) within 28 to 35 days port-to-port. For urgent factory maintenance batches, scheduled tooling replenishment, or pre-production sample trials, express air freight to Brussels Airport (BRU) delivers within 4 to 6 business days. We provide complete commercial documentation, including EUR.1 assistance, Bill of Lading, and TARIC classification (typically 8207 40 for tapping and threading tools) to guarantee smooth customs clearance.
What are the Minimum Order Quantities (MOQ) for custom-branded tap sets and private-label packaging?
For standard metric machine taps in stock packaging (individual plastic tubes), our minimum order quantity starts at 100 pieces per size. For customized OEM programs—such as branded laser marking on the tap shank, custom tap cases (ABS plastic cassette, index metal box, or wooden sets), and dual-language Dutch/French labeling for the Belgian domestic tool market—MOQs are approximately 500 to 1,200 sets depending on package design.
How do your factory wholesale prices compare to traditional European cutting tool brands?
Purchasing directly from our factory eliminates multiple tiers of distribution markups typically added by European importers, regional stockists, and local industrial trade houses across Benelux. Our integrated manufacturing structure—incorporating high-speed CNC flute grinding, in-house vacuum heat treatment, and direct raw steel sourcing—allows European distributors and large-scale industrial end-users to reduce procurement unit costs by 35% to 55% while maintaining strict adherence to DIN dimensional tolerances and performance standards.
Accelerate Your Tooling Supply Chain in Ghent
Whether you need custom-dimensioned HSS-E spiral flute taps for robotic CNC machining lines, M42 hole saws, or wholesale DIN352 tap sets for tool retail across Belgium, our technical engineering team provides rapid quoting and sample verification.
Inquire Now