SDS-Max Heavy
Engineered in compliance with DIN, ISO, and ANSI industrial standards. Instant sample dispatch and volume OEM manufacturing available with direct logistics to North Macedonia.


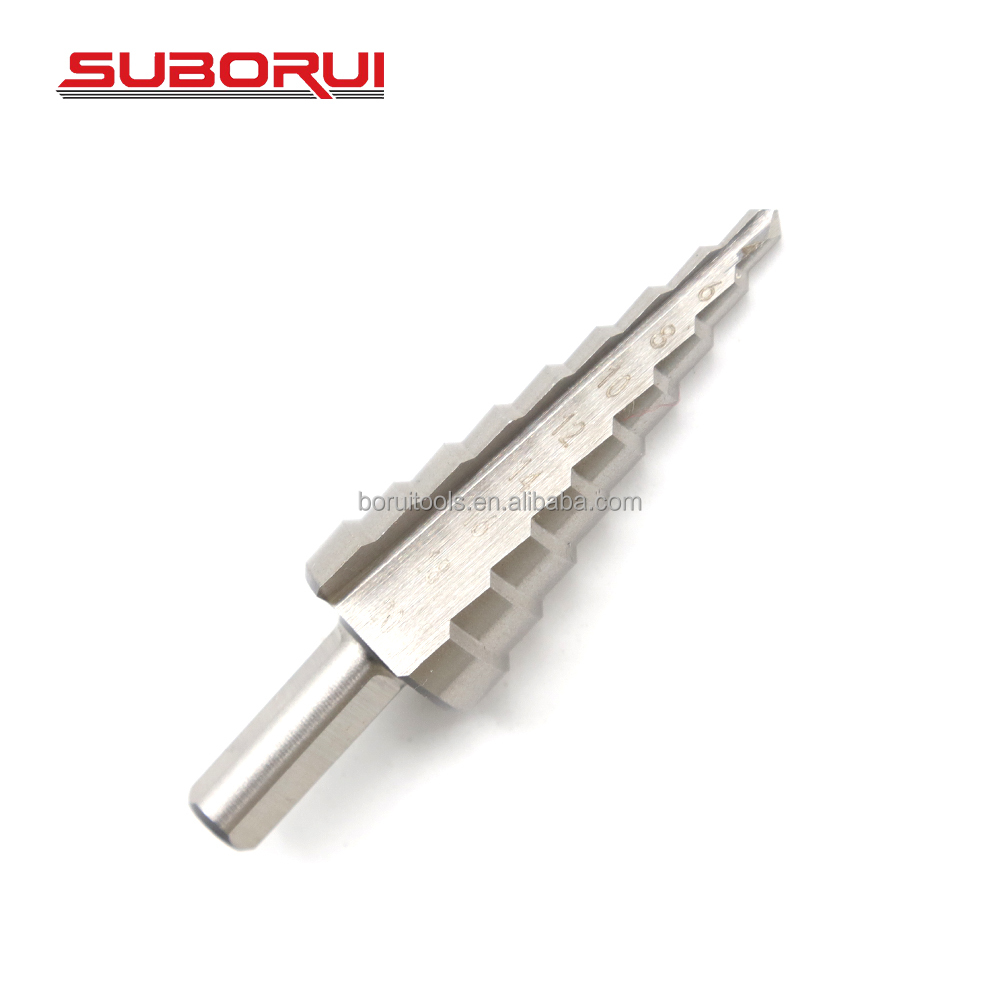



As North Macedonia consolidates its position as a high-precision automotive and industrial assembly bridgehead in Southeastern Europe, industrial plants throughout the Greater Skopje Basin are migrating from traditional chip-cutting taps to high-speed thread forming technology.
Unlike conventional cut taps that sever the grain boundary fibers of the workpiece, WRD roll taps plastically deform the ductile material along the thread contour. This cold-working hardening effect delivers 30% to 50% higher shear and tensile strength in dynamic cyclic fatigue applications, essential for safety-critical automotive fasteners produced across Skopje Free Economic Zones (TIDZ).
Thread forming creates zero chips or swarf. In blind-hole tapping applications—traditionally notorious for bird-nesting chips, tool clogging, and premature tap breakage on robotic CNC transfer lines—forming taps eliminate bird-nest downtime entirely. The process ensures flawless thread finish (Ra < 0.4 µm) without requiring high-pressure reverse flush flushing systems.
Fabricated from HSSE-PM (Powder Metallurgy) and micro-grain carbide, our roll taps maintain rigidity at cutting speeds (Vc) up to 2.5 times faster than standard cutting taps. Combined with advanced multilayer PVD coatings (TiCN, TiAlSiN, and CrN), tool life regularly exceeds 12,000 to 20,000 tapped holes per tool in high-silicon aluminum and structural micro-alloyed steels.
Precision ground on 6-axis CNC tool grinding centers to DIN 2174, DIN 371, DIN 376, and ISO 2283 specifications. Optimized for automated CNC machining centers operating in Skopje's automotive and electronic manufacturing clusters.
| Series Code | Substrate Alloy | Surface Treatment | Applicable Workpiece (Skopje Plants) | Tensile Limit | Speed (m/min) |
|---|---|---|---|---|---|
| WRD-TF-Alu | HSSE Cobalt 5% (M35) | Mirror Polished / CrN Nano-coat | Die-cast Aluminum (AlSi9Cu3, AlSi10Mg), Brass, Copper | ≤ 550 N/mm² | 25 – 45 m/min |
| WRD-TF-Steel | HSSE-V3 / PM High Speed | Multi-layer TiCN Bronze | Low/Medium Carbon Steel (S235, S355), Case-hardened Steels | ≤ 900 N/mm² | 18 – 32 m/min |
| WRD-TF-Inox | Powder Metallurgy HSSE-PM | AlTiN / TiAlSiN Super Hard | Austenitic Stainless (AISI 304, 316), Duplex Sheet Assemblies | ≤ 1050 N/mm² | 10 – 22 m/min |
| WRD-TF-Carbide | Sub-micron Solid Carbide | Diamond-Like Carbon (DLC) | Hypereutectic A390 Aluminum, High-abrasion Composites | ≤ 600 N/mm² | 40 – 75 m/min |
Engineered to meet the exact operational parameters and material specifications of Tier-1 and Tier-2 automotive manufacturing hubs situated across North Macedonia's capital corridor.
Supplying multinational Tier-1 braking, seating, and electronic enclosure plants in Bunardzik. Our DIN 371 M3 to M8 TiCN forming taps with continuous oil grooves eliminate chips inside electronic sensor housings and high-pressure fluid manifolds, avoiding catastrophic foreign-object-debris (FOD) assembly failures.
Heavy steel fabricators, transformer housing producers, and precision conveyor builders in Gazi Baba demand consistent DIN 376 long-shank cold roll taps (M10–M20). In structural micro-alloyed sheet metals, our HSSE-PM taps prevent burr development on thread runouts, cutting out manual post-tap deburring stages.
Export-driven electrical cabinet manufacturers and HVAC chassis assemblers operating in the Ilinden industrial corridor utilize our hex-shank and straight-shank roll taps for zinc-coated galvanized sheet and austenitic stainless enclosures, doubling cycle rates while maintaining zero-rework quality standards.
Strategic advantages of transitioning from European third-party distribution intermediaries to direct factory-level manufacturing partnerships with Jiangsu WRD Tools.
Skopje's prime geographical location on Pan-European Transport Corridor X allows seamless maritime transit from Shanghai or Ningbo ports directly to the Port of Thessaloniki (Greece), followed by direct bonded railway or express truck freight to Skopje Inland Customs in under 48 hours from Mediterranean discharge.
Purchasing cutting and forming tools via regional tool traders in Austria, Germany, or Slovenia incurs multi-tier logistics surcharges and trade markups. Direct OEM engagement with Jiangsu WRD Tools delivers tier-1 factory gate pricing without compromising on DIN substrate purity or PVD coating integrity.
Whether your CNC machine uses synchronous rigid tapping or floating collet chucks, our Danyang factory produces custom thread pitches, extended reach shanks, reduced neck geometries, and specific DIN 371/376 combinations engineered to individual factory part prints in Skopje within 15–20 working days.
Jiangsu WRD Tools Co., Ltd. (SUBORUI) has engineered cutting, drilling, and threading tools in Danyang, China since March 2007, operating with RMB 10 million registered capital and verified annual capacity of 90 million units.
Our 12,000 m² modern manufacturing infrastructure, robotic CNC production cells, and comprehensive QA/QC inspection protocols have been audited and onsite-verified by Intertek Group. Recognized as an official High-Tech Enterprise of Jiangsu Province since 2019.
Over nearly two decades, WRD Tools has engineered and delivered private-label tooling programs to premier global tool manufacturers and retail giants including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Dexter, KWB, Wolfcraft, Truper, and Heller.
Every production batch is tested on German Zeiss optical coordinate measuring machines, Keyence digital profile projectors, and dynamic electronic torque testing benches. We assure thread profile concentricity within 0.003 mm and batch-to-batch hardness variance under ±0.5 HRC.
Clear, technically rigorous answers addressing customs clearance, import documentation, lubrication needs, and batch order logistics for Macedonian enterprises.
Send your CAD drawings, required thread standards (DIN/ISO/ANSI), and workpiece material specifications. Our technical sales engineers provide complete tooling quotes and DFM pre-hole recommendations within 24 hours.