
Featured Industrial Cutting & Threading Solutions
High-tolerance DIN-standard machine taps, cobalt drill bits, hole saws, and demolition tooling engineered in our Intertek-verified factory for demanding metalworking environments.
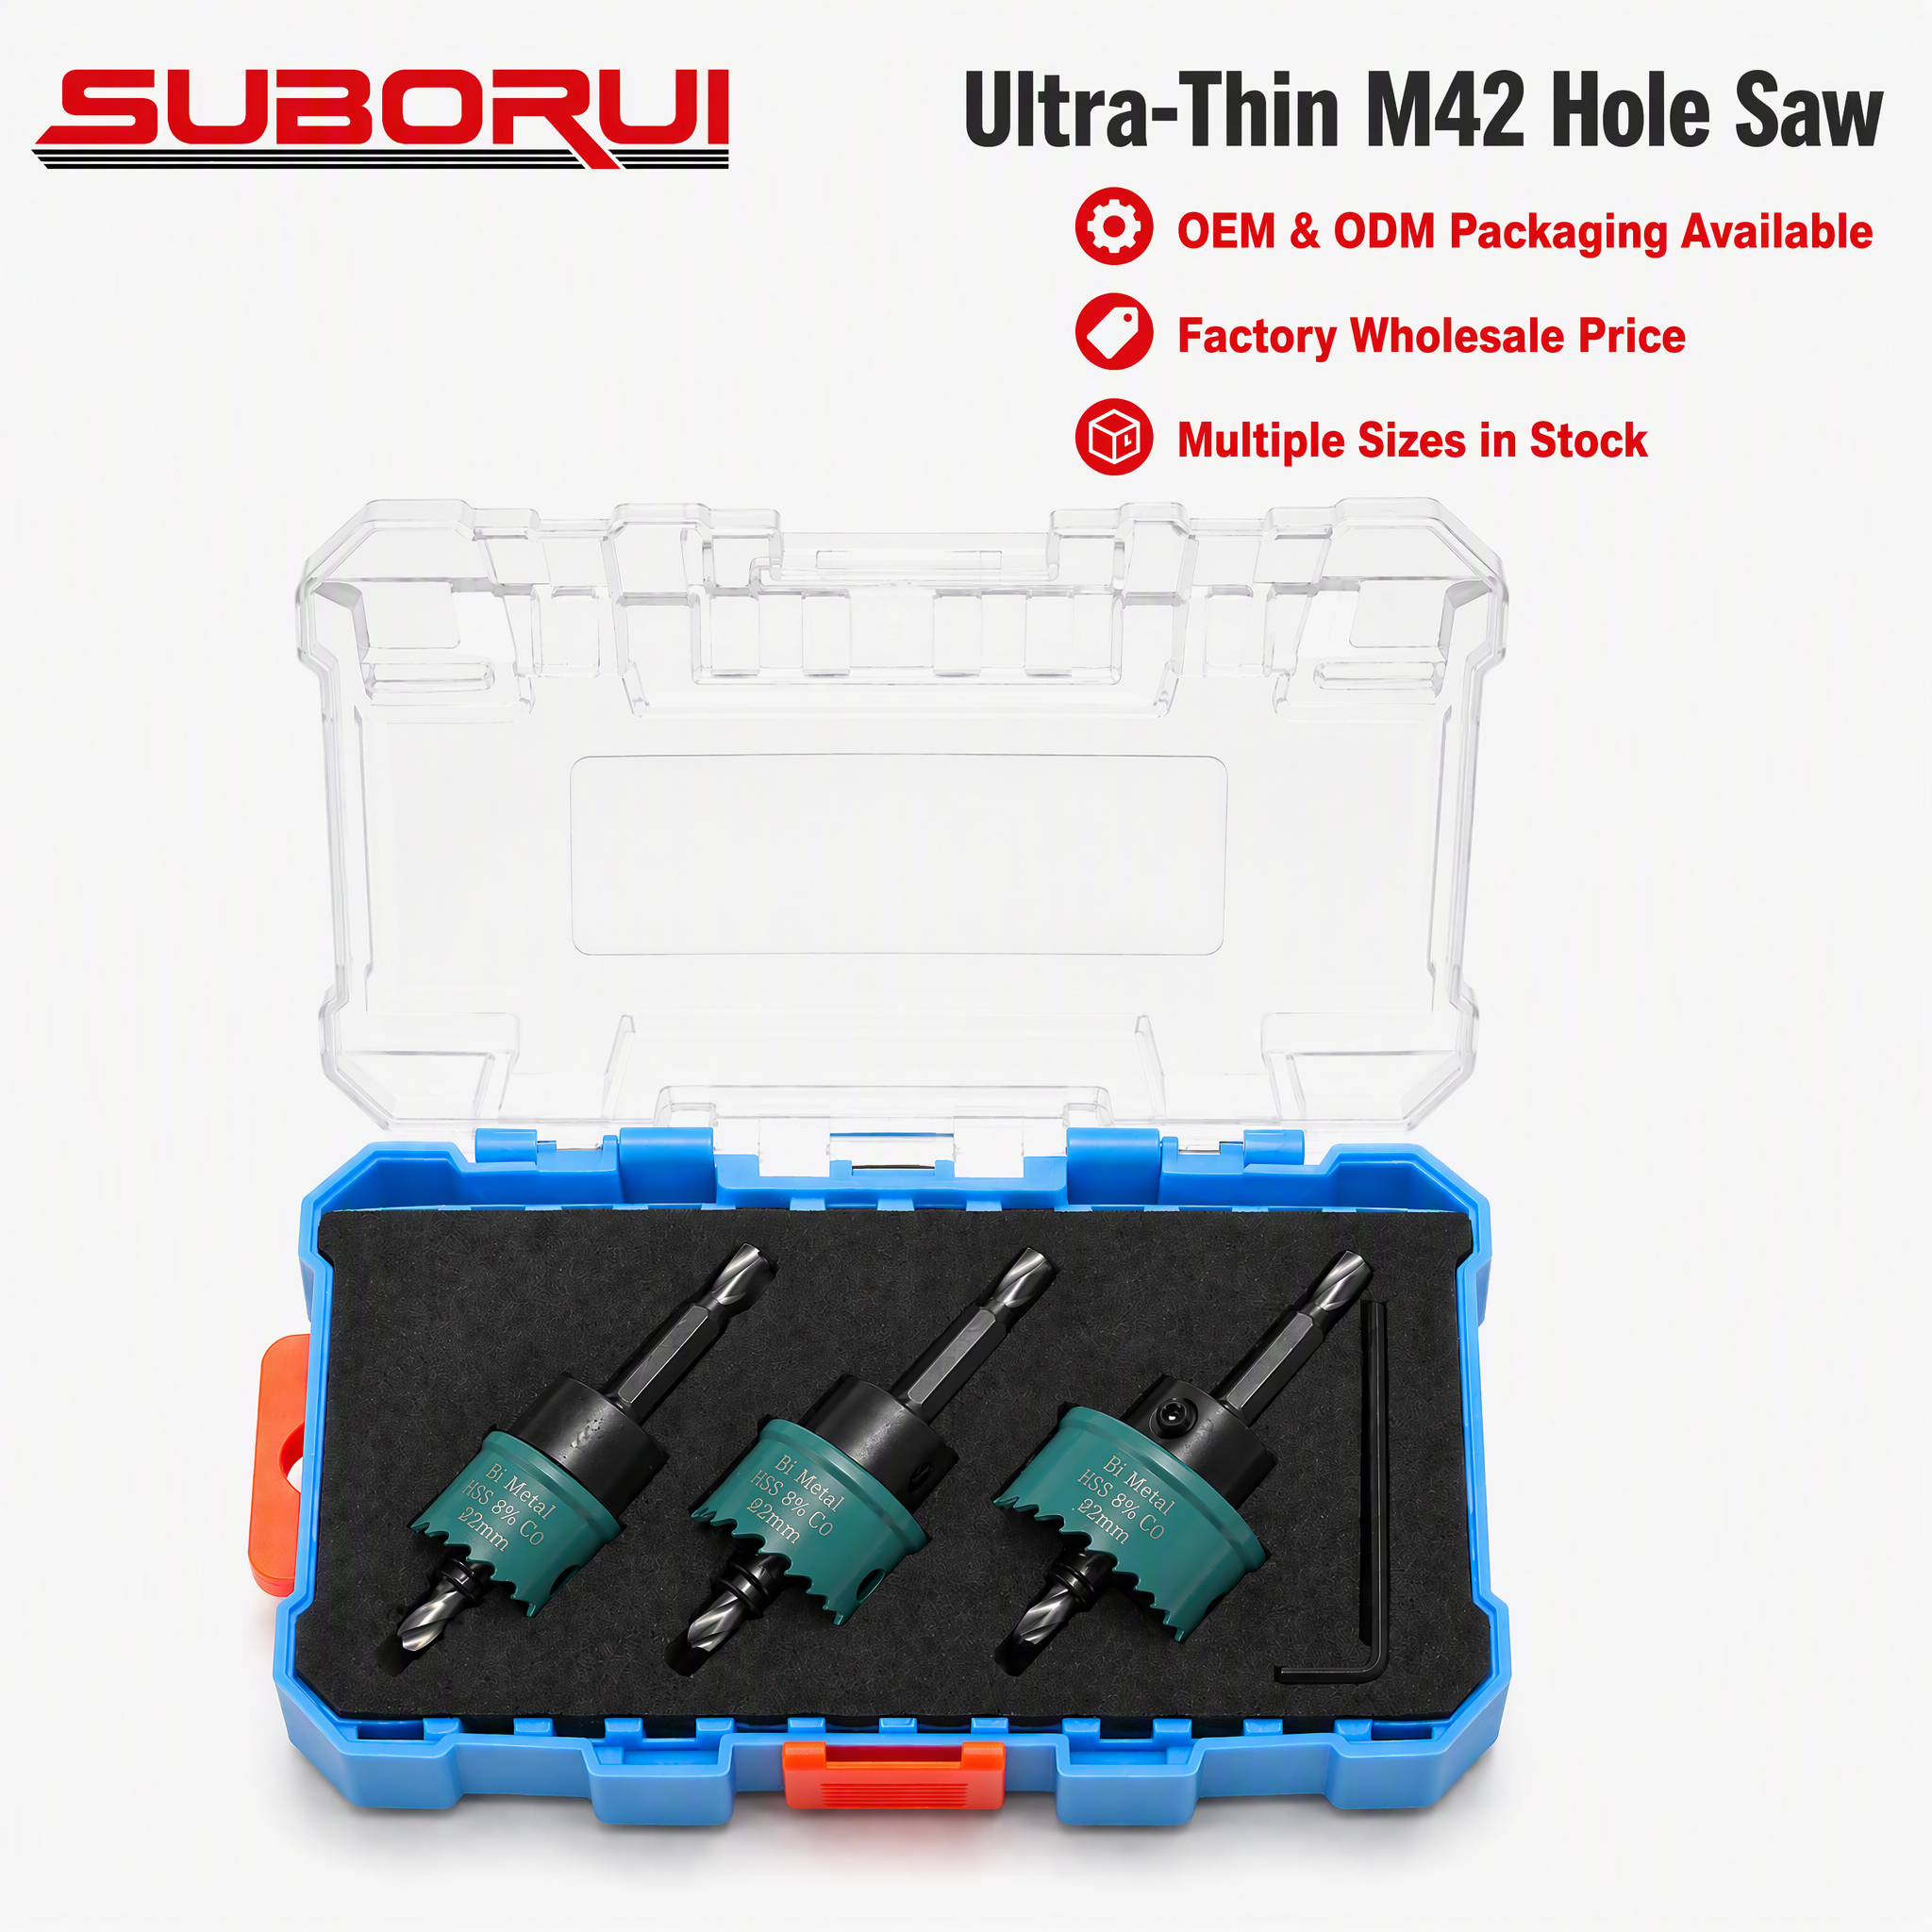
SUBORUI 3PCS 20/23/32mm Ultra-Thin Hex Shank M42 Bi-Metal Hole Saw Set
View Specifications
SUBORUI M42 Bi-Metal Drill Bit Cutter for Multi-Material Industrial Cutting
View Specifications
SUBORUI 6mm Titanium Cross Carbide Tip Double R Hex Shank Tile & Glass Bit
View Specifications
SUBORUI OEM 14mm-50mm Hex Shank M42 Bi-Metal Sheet Metal Hole Cutter
View Specifications
SUBORUI Wholesale 40Cr 6x110mm 4-Flute Single Carbide Tip SDS Plus Drill Bit
View Specifications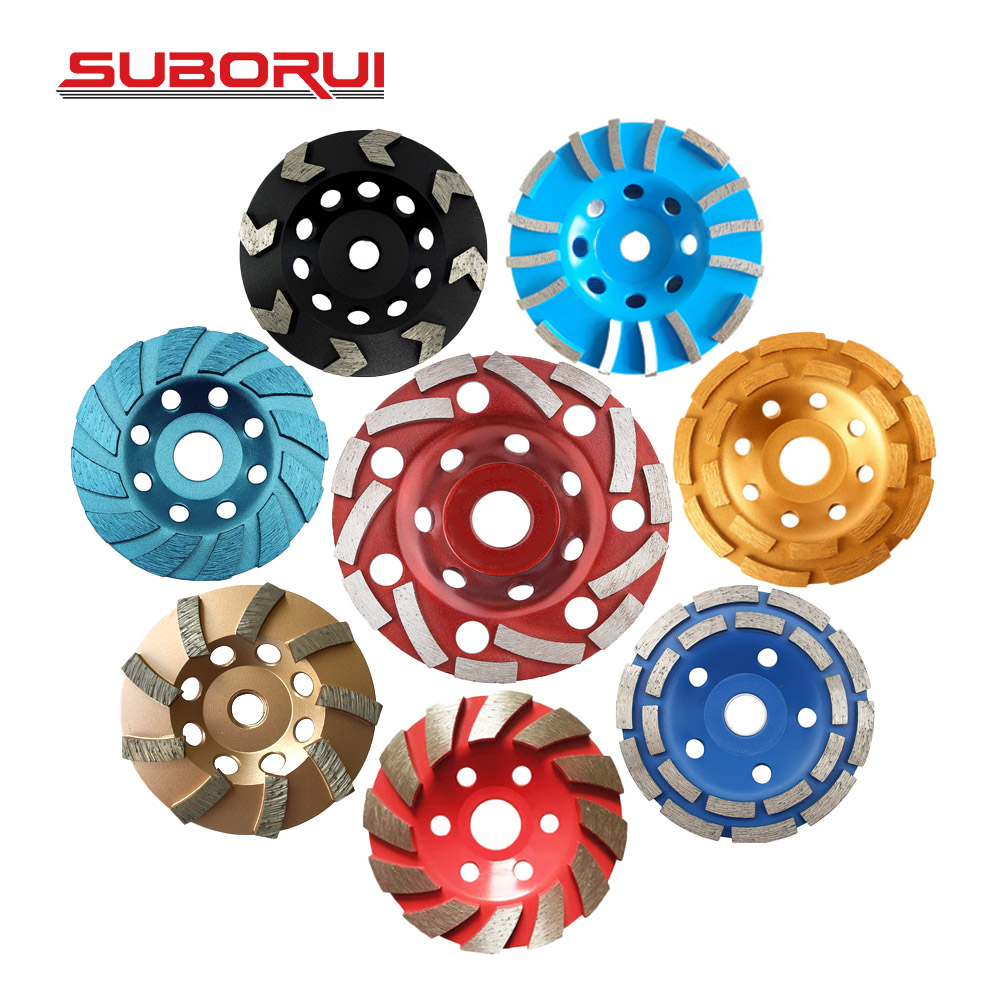
SUBORUI Custom 4.5" Turbo Diamond Cup Grinding Wheel for Stone & Concrete
View Specifications
SUBORUI 100/115mm Ultra-Thin Diamond Ceramic & Marble Circular Cutting Disc
View SpecificationsEngineering Precision: Spiral Point Machine Taps for Industrial Ostrava
In high-throughput manufacturing, threading operations in through-hole geometries represent one of the most mechanically critical, cost-sensitive phases of production. Often referred to colloquially as "gun taps" or "bull nose taps," spiral point taps feature straight flutes supplemented by an angular cutting edge ground at the tool's point. This specialized geometry forcibly shoots chips forward, ahead of the tapping stroke, entirely away from the threaded zone. For industrial procurement directors, CNC production line supervisors, and machining workshops across the Moravian-Silesian Region centered in Ostrava, sourcing toolroom-grade spiral point taps from a certified primary manufacturer bridges the gap between cycle efficiency and tool cost optimization.
Jiangsu WRD Tools Co., Ltd. (operating the premier SUBORUI industrial brand) manufactures high-speed steel (HSS), cobalt alloyed HSS-E (M35), and powder metallurgy (PM-HSS) spiral point taps engineered to stringent DIN 371 (reinforced shank for metric sizes M3 to M10) and DIN 376 (reduced shank for through-tapping M12 to M30+). Backed by nearly two decades of precision cutting tool production in Danyang, China—the world's most concentrated tooling manufacturing hub—we deliver metallurgical stability, micro-crack resistant vacuum heat treatment, and specialized surface technologies (TiN, TiCN, and TiAlN) precisely matched to Central Europe's heavy engineering specifications.
The Mechanical Anatomy of High-Speed Forward Chip Evacuation
Unlike straight-fluted hand taps (such as our DIN352 line) which rely on manual clearance or periodic reversing, or spiral flute taps designed to draw chips backward out of blind holes, spiral point taps feature an angular face of approximately 15° to 22° at the entry chamfer. As the tap engages the pre-drilled bore, this angular shear plane drives spiral chips forward through the workpiece hole. This dynamic confers three primary advantages to production facilities:
1. Substantially Increased Core Web Diameter: Because the straight portion of the flutes does not carry chip loads, the flute channels can be shallow. This leaves a much heavier web cross-section, maximizing the tap's torsional rigidity and drastically reducing premature shank snapping caused by sudden rotational resistance.
2. Elimination of Surface Scoring: Since swarf exits ahead of the cutting action, swarf bird-nesting cannot pack the active threads. Tapped internal threads retain pristine DIN 13-compliant dimensional accuracy without gouges or surface work-hardening.
3. Optimized Coolant Flushing: The unobstructed straight flutes permit flood coolant or high-pressure through-spindle cutting fluids to access the point chamfer directly, maintaining heat transfer stability during high-feed CNC tapping sequences.
| Substrate / Metallurgy | Hardness (HRC) | Standard Coating | Recommended Tensile Range | Typical Industrial Workpiece |
|---|---|---|---|---|
| HSS M2 (W6Mo5Cr4V2) | 63.5 - 65.0 | Bright Finish / Steam Oxide | < 800 N/mm² | Structural steels (S235JR, S355), ductile cast iron, unalloyed carbons |
| HSS-E Cobalt M35 (Co 5%) | 65.5 - 67.0 | TiN (Gold Titanium Nitride) | 800 - 1050 N/mm² | Austenitic stainless (1.4301 / AISI 304), high-strength structural profiles |
| HSS-E-PM (Powder Metal) | 67.0 - 68.5 | TiAlN (Titanium Aluminium Nitride) | 1050 - 1300 N/mm² | Tool steels, heat-treated chromium alloys, high nickel-chromium components |
Industrial Landscapes & Localized Applications Across Ostrava
Ostrava is historically celebrated as the steel capital of the Czech Republic, situated at the nexus of the Moravian-Silesian and Upper Silesian industrial basins. Over recent decades, this territory has pivoted from blast furnace primary extraction into a high-technology automotive assembly, rolling stock fabrication, heavy mining machinery retrofit, and precision engineering corridor. Machine threading requirements across Ostrava's industrial zones (such as Ostrava-Hrabová, Mošnov, and Třinec manufacturing parks) demand strict adherence to European norms.
Automotive & Tier-1 Tier-2 Componentry
Ostrava's supply chain feeds prominent regional OEM plants across Moravia and neighboring Žilina. Our DIN 371/376 M35 TiN spiral point taps provide consistent 6H thread tolerances in stamping mounts, engine brackets, and chassis sub-frames where automated robotic tapping arms cannot tolerate chip accumulation.
Railway Rolling Stock & Heavy Bogies
The regional production of railway wheels, bogie chassis, couplers, and heavy track infrastructure relies on large through-hole tapped connections (M16 through M36). Operating on hot-rolled structural alloy plates, our reinforced through-hole gun taps ensure uncompromised thread shear resistance without tool breakage.
Heavy Machinery & Hydraulic Valves
Ostrava retains specialized manufacturing for mining equipment, planetary gear units, and high-pressure fluid power housings. Our taps resist catastrophic edge micro-chipping when transitioning through interrupted bores, cross-drilled oil pathways, and tough ductile iron matrix castings.
Emerging Regional Manufacturing Trends
Procurement teams in the Czech Republic are aggressively optimizing their total cost of ownership (TCO) across tool cribs. Several trends govern tool purchasing throughout Ostrava: first, the rapid uptake of robotic tapping centers capable of spindle speeds exceeding 2,500 RPM, requiring taps with high red-hardness (5% to 8% cobalt content) to counter extreme friction; second, the transition to Minimum Quantity Lubrication (MQL) and dry machining environments, necessitating superior multilayer TiAlN coatings to establish thermal barriers at the shear interface; and third, nearshoring strategies that combine direct factory partnership pricing from certified Chinese manufacturers with scheduled, bonded warehouse logistics to eliminate European distribution tier markups.
Enterprise Strengths: Why WRD Tools Outperforms Global Brokers
Unlike third-party export brokers, Jiangsu WRD Tools Co., Ltd. is an authentic cutting tool manufacturer operating a vertically integrated 12,000 square meter factory in Danyang, Jiangsu Province. Since March 2007, our team of over 150 skilled tooling technicians has supplied globally acclaimed brands—including industry titans such as BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller. When Ostrava procurement specialists order from WRD, they tap directly into verified factory capacity.
Intertek Onsite Audited Facility
Our workshop premises, 5-axis CNC grinding centers, computerized salt-bath hardening plants, and multi-stage metrology QA/QC departments have undergone exhaustive onsite verification by Intertek Group, guaranteeing verifiable factory origin.
Provincial High-Tech Enterprise
Recognized as an official High-Tech Enterprise of Jiangsu Province since 2019, WRD invests continuously into metallurgical research, proprietary spiral flute grinding wheel dressings, and surface friction reduction technologies.
Comprehensive OEM / Private Labeling
We provide full white-label capabilities for Czech tooling retailers, industrial catalogs, and hardware brands: precision shank laser marking (EAN, brand, DIN size), custom surface finishes, metal cassette sets, and protective blister packs.
Procurement & Engineering FAQ for Ostrava Buyers
Clear, direct answers regarding metallurgy, shank standard conformity, delivery lead times, and customs protocol for imports into the Czech Republic (EU territory).
Why use a spiral point tap instead of a spiral flute tap for through-hole tapping?
Spiral flute taps are engineered specifically for blind holes to pull swarf upward and out of the cavity. If applied in through-hole machining, the back-pull dynamic requires a deeper flute channel, weakening the web core and increasing the likelihood of tool fracture. A spiral point tap shoots chips forward through the workpiece, permitting a solid, thick tap core that easily handles high CNC torque levels and heavy feed rates.
Do your spiral point taps conform strictly to European DIN 371 and DIN 376 standards?
Yes. For sizes M3 through M10, our taps feature the reinforced shank with driving square specified by DIN 371, ensuring unyielding grip in standard ER-GB collets or quick-change tapping chucks. For M12 and larger diameters, tools are ground to DIN 376 specifications with reduced shank diameters equal to the nominal pitch diameter, allowing the tool to pass completely through deep threaded holes.
What are the minimum order quantities (MOQ) and lead times for shipping to Ostrava?
For standard catalog dimensions in HSS-G M2 or M35 cobalt, our factory MOQ is typically 100 to 500 pieces per size, and complete tap & die or drill sets start from 100 sets. Custom laser branding and bespoke private packaging generally begin at 1,200 sets. Production lead times run between 25 and 40 calendar days, with sea freight routed via Hamburg, Koper, or direct rail express to Ostrava's intermodal terminal.
How does WRD Tools manage material certification and quality documentation?
Every batch of high-speed steel bar stock is subjected to optical emission spectrometry to verify carbon, tungsten, molybdenum, vanadium, and cobalt compositions. Hardness reports (Rockwell HRC), concentricity run-out documentation (<0.005mm), and thread profile optical comparator reports can be provided along with commercial invoices to streamline your internal ISO 9001 quality audits.
Which coating is optimal for processing austenitic stainless steel (AISI 304 / 316) in chemical plants?
For stainless steel, we recommend our M35 Cobalt (HSS-E 5% Co) spiral point taps combined with a physical vapor deposition (PVD) TiCN (Titanium Carbonitride) or TiAlN coating. These coatings feature exceptional hardness (over 3000 HV) and low coefficients of friction, preventing the severe galling, material pickup, and built-up edge (BUE) common in work-hardening chromium-nickel steels.
Accelerate Your Machining Throughput with Direct Factory Supply
Send our engineering team your part drawings, pitch tolerances, workpiece material datasheets, or target volume requirements. Receive complete technical validation and transparent FOB/CIF pricing within 24 hours.
Contact Us