Featured Industrial Cutting & Drilling Solutions
Engineered for extreme wear resistance, thermal dissipation, and precise cutting performance across harsh Nordic worksites, hard rock geology, and structural reinforced concrete.

SUBORUI DIN338 135° Split Point M35 Cobalt HSS Drill
CNC fully ground spiral flute twist bit with 5% cobalt alloy. Prevents heat work hardening when drilling structural 304/316 stainless steel and tough structural alloys.
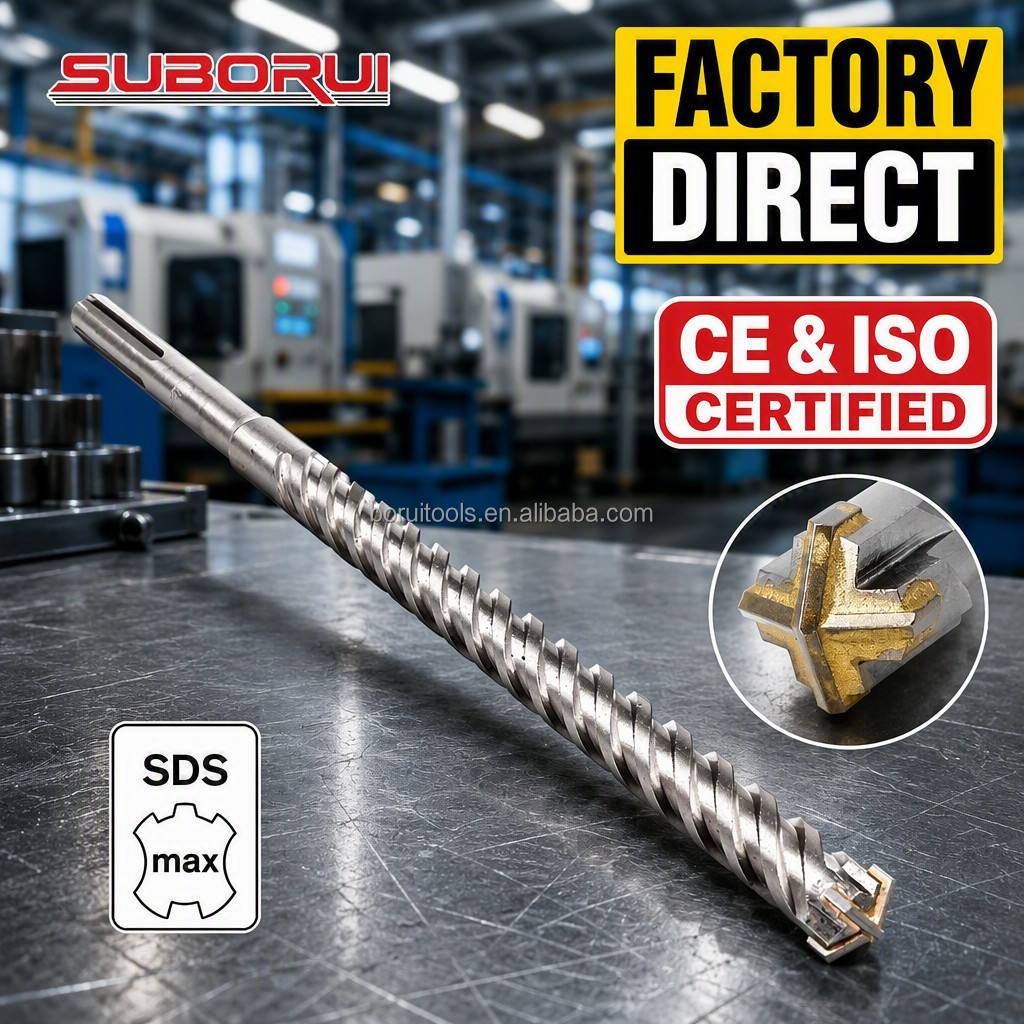
SUBORUI SDS Max Cross Carbide Rotary Hammer Bits
Heavy-duty 280mm–600mm masonry drill bits featuring a four-cutter cross-head tungsten carbide tip to drill dense aggregate concrete without binding on steel rebar.

SUBORUI 125mm Segmented Cup Diamond Grinding Disc
Fine abrasive diamond grinding wheel designed for granite, marble, and cured architectural screed. Delivers smooth finishing without edge chipping or rotational wobble.

SUBORUI M42 Bi-Metal Industrial Hole Saw Cutter
Variable pitch 8% cobalt M42 tooth geometry optimized for rapid penetration through cast iron, stainless plate, laminated composite timber, and rigid polymer conduits.
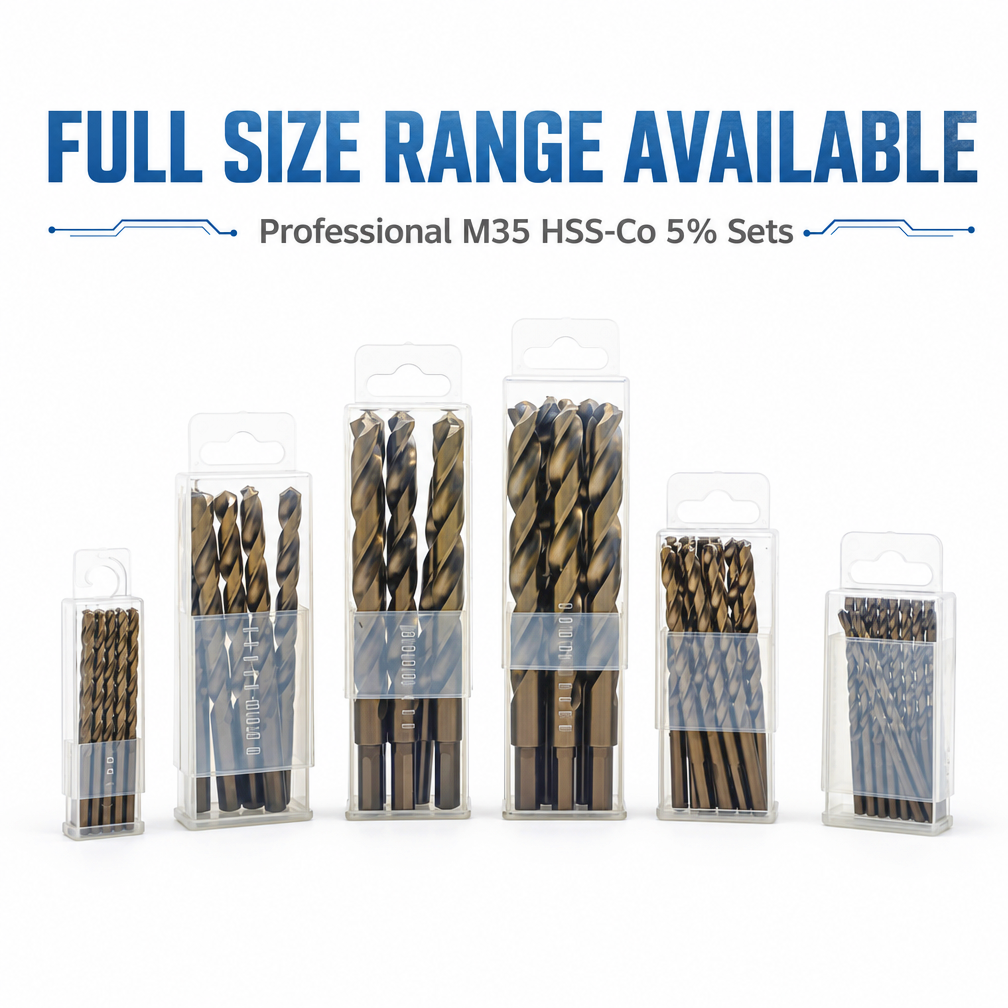
SUBORUI Fully Ground DIN338 M35 Co5% Twist Drill
Engineered to DIN338 standards with high thermal retention. Delivers continuous chip evacuation and tight concentricity tolerances for CNC and bench drilling rigs.
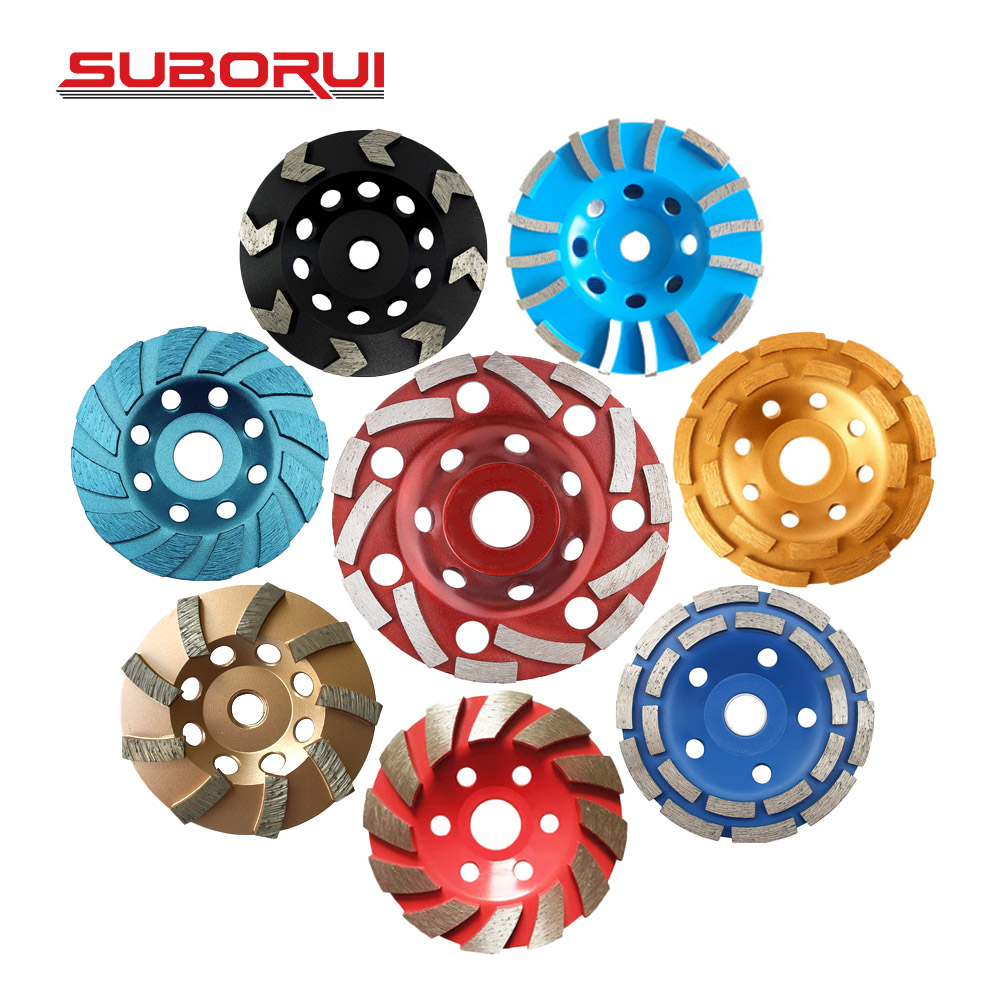
SUBORUI 4.5" Turbo Concrete Diamond Cup Wheel
High-concentration synthetic diamond segments bonded in a durable sintered alloy matrix. Ideal for fast stock removal on cured masonry, granite curbs, and floor prep.
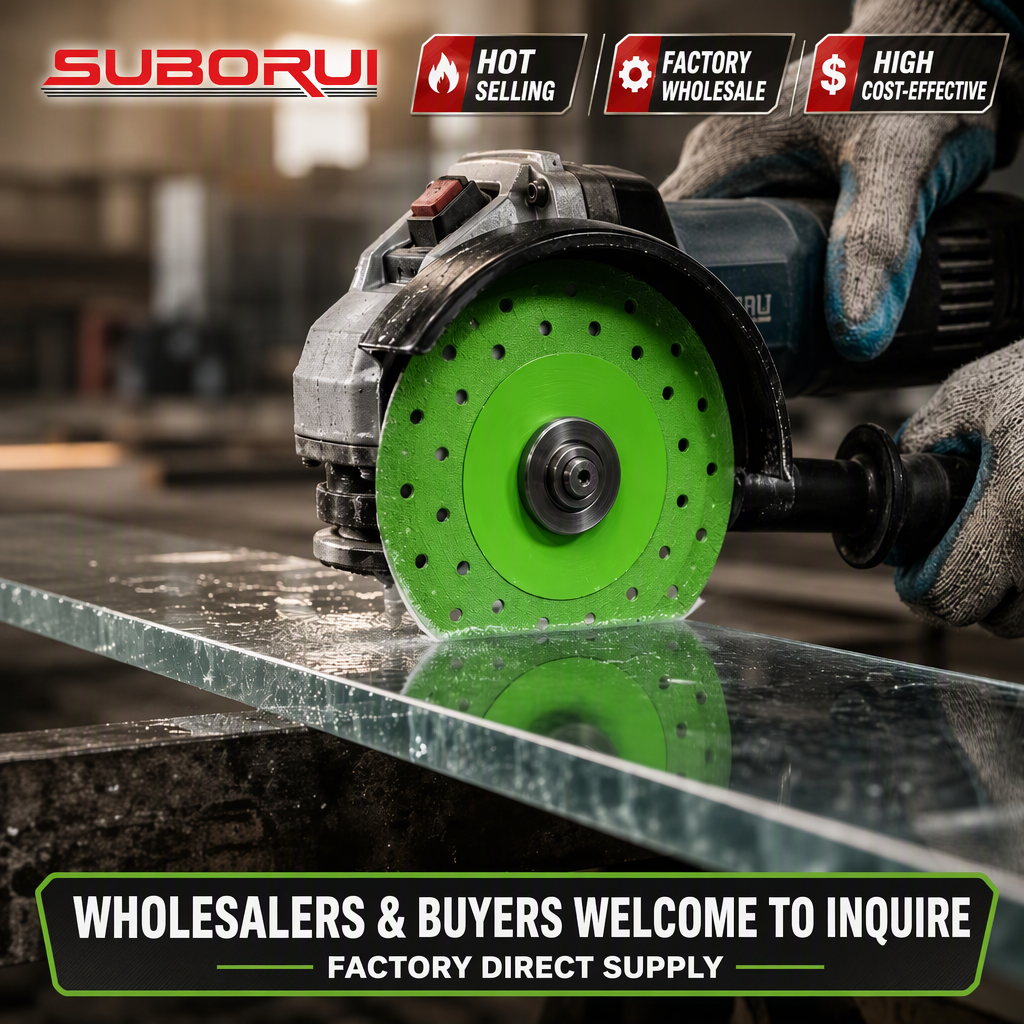
SUBORUI 100/115mm Thin Diamond Cutting Disc
Ultra-thin kerf continuous rim blade engineered for chip-free slicing of dense vitrified porcelain, ceramic slabs, crystalline marble, and delicate architectural glass panels.
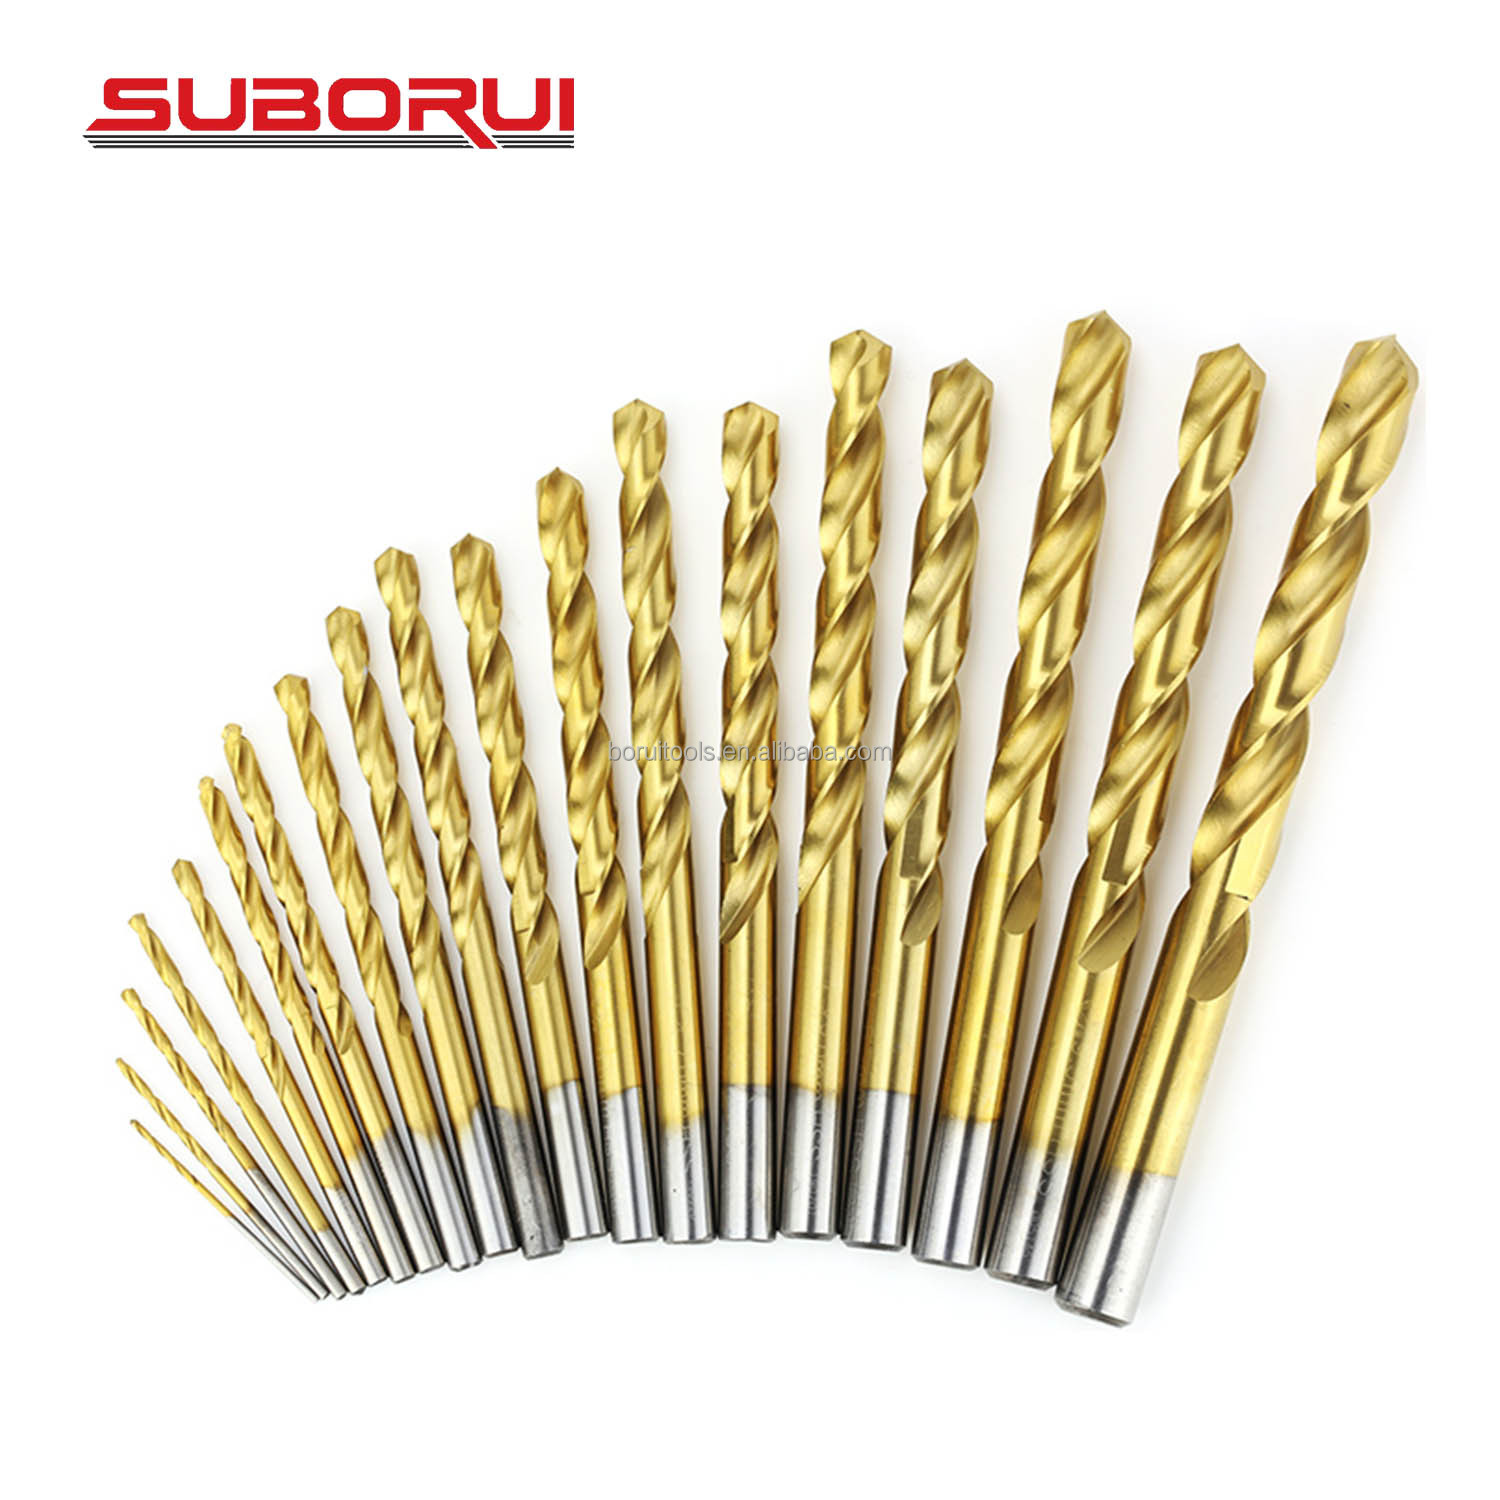
SUBORUI DIN338 Titanium Coated HSS M2 6542 Bit
Golden titanium nitride (TiN) treated high speed steel jobber bits offering surface friction reduction, extended cutting edge lifespan, and corrosion resistance in damp environments.
Metallurgical Dynamics of Turbo Diamond Blades for Fennoscandian Geology
Exporting diamond cutting tools to the Stockholm County construction and civil engineering sector demands a specialized understanding of local Scandinavian mineralogy. Unlike standard sedimentary rocks encountered across central Europe, the bedrock across the Greater Stockholm Metropolitan area consists primarily of Precambrian Svecokarelian granites, gneiss, and quartzites. These formations feature quartz contents consistently exceeding 35% to 45%, resulting in a Mohs hardness ranging from 6.5 to 7.2 alongside extreme abrasive shear forces.
Standard commodity diamond saw blades engineered for limestone or soft mortar glaze over rapidly when deployed on Stockholm granite (Stockholmsgranit). Glazing occurs when the diamond crystals fracture prematurely while the metal matrix work-hardens, generating friction, excessive heat buildup, and dangerous core deformation. WRD Tools solves this challenge by engineering customized segment matrix formulations specifically tailored for Nordic buyers:
Cobalt-Bronze Free-Cutting Matrix
To match high-quartz Scandinavian aggregate, our sintering process leverages a fine-grain cobalt-nickel-tungsten powder matrix. This controlled wear rate systematically exposes fresh, sharp diamond facets, eliminating glazing even on unyielding Svecofennian bedrock.
Thermo-Vented Turbo Segment Flutes
Continuous corrugated turbo flutes channel turbulent airflow directly to the cutting face during dry-cutting operations. This aerodynamic flushing clears abrasive micro-slurry rapidly, keeping operating temperatures 120°C lower than traditional continuous rim configurations.
Laser-Welded Segment Retention
Full-penetration automated laser welds achieve shear bond strengths exceeding 1,200 N/mm² between the diamond segment and alloy core. This completely prevents catastrophic segment detachment under intense sub-zero mechanical loads.
| Technical Parameter | Standard Commercial Grade | WRD Tools Stockholm Pro-Series | Nordic Jobsite Impact |
|---|---|---|---|
| Diamond Grit Density | 20% - 25% Concentration | 35% - 40% Premium Mesh (US MBD-8) | +65% lifespan in dense reinforced concrete |
| Matrix Sintering Type | Iron-Base Sintered Cold-Press | Hot Isostatic Pressed (HIP) Cobalt-Bronze | Eliminates diamond pop-out on high-silica stone |
| Steel Core Alloy | 50Mn / Standard Carbon Steel | 75Cr1 German Spring Steel (HRC 42-45) | Resists core deflection and warping at high RPM |
| Acoustic Damping | Solid Core (98-105 dB) | Laser-Cut Resin-Filled Silent Detents | Complies with Swedish municipal noise caps (<85 dB) |
| Safety Certification | Self-Certified / Baseline ISO | EN 13236 Safety Standard Compliance | Seamless approval on Skanska/NCC/JM managed builds |
Field-Tested Performance Across Stockholm Jobsite Environments
From major underground infrastructure programs to inner-city historic renovation and freezing winter masonry cutting, our tooling is engineered for the Nordic working environment.
Stockholm Bypass (E4 Förbifart) Infrastructure
Drilling and slicing deep rock tunnel walls and post-tensioned utility vaults requires cutting tools that resist intense abrasion. Our turbo diamond blades and cross-carbide SDS Max hammer drill bits penetrate hard bedrock without overheating or binding on embedded steel rebar meshes.
Sub-Zero Winter Operation Across Mälardalen
Winter temperatures dropping below -15°C across central Sweden cause conventional diamond blade cores to suffer from cold embrittlement, often cracking along expansion slots. WRD Tools uses 75Cr1 alloy steel cores heat-treated to maintain ductility and structural stability under sub-zero thermal cycling.
Slussen Urban Redevelopment & Renovation
Urban reconstruction projects in Stockholm's historic central districts require high-speed dry and wet cutting that minimizes vibration damage to surrounding structures. Our turbo blades provide crisp, chip-free kerfs through old granite seawall masonry, clinker brick, and precast panels.
Navigating Sweden's Evolving Construction & Tooling Regulations
Swedish contractors operate under some of Europe's most stringent environmental, safety, and occupational health mandates. Here is how our OEM manufacturing aligns with Stockholm market standards.
Strict Respirable Quartz Dust Controls (AFS 2015:2)
Arbetsmiljöverket strictly limits crystalline silica exposure on Swedish jobsites. Our turbo blade core cooling ports and precision segment kerfs are engineered to work seamlessly with integrated shroud vacuums and pressurized wet-suppression rigs, preventing hazardous airborne silica dust clouds.
Fossil-Free Sites & Battery Tool Efficiency
Stockholm's transition toward zero-emission worksites has spurred rapid adoption of 36V and 54V battery-powered cut-off machines (e.g., Husqvarna K 535i, Stihl TSA 230). Our ultra-thin kerf turbo blades reduce cutting torque resistance by 22%, extending battery run-times per charge on remote sites.
Private Label Supply Chain Resiliency
Hardware distributors across Stockholm and northern Europe are moving away from multi-tier brokerage networks toward direct OEM partnerships. WRD Tools offers end-to-end custom laser etching, barcode generation, customized bilingual packaging, and consolidated sea freight direct to Stockholm Frihamnen or Gothenburg.
Why European Procurement Teams Trust Jiangsu WRD Tools
Established in March 2007 in Danyang, Jiangsu Province—the heart of China's cutting tool manufacturing corridor—Jiangsu WRD Tools Co., Ltd. (brand SUBORUI) operates a modern 12,000 square meter manufacturing complex with over 150 skilled toolmakers. We are a dedicated, vertically integrated manufacturing factory, not a trading company. Every diamond blade, cobalt twist drill, annular core cutter, and bi-metal hole saw is engineered, heat-treated, CNC ground, and dynamic-balanced in-house.
Intertek Onsite Audited
Our manufacturing lines, quality management systems, dynamic test benches, and working conditions are verified onsite by Intertek Group.
Tier-1 OEM Supplier
Proven track record engineering and supplying cutting tools to international global brands including Bosch, Milwaukee, DeWalt, Makita, and Heller.
Jiangsu High-Tech Enterprise
Officially recognized as a High-Tech Enterprise in 2019, holding proprietary metallurgical patents and advanced automated sintering systems.
90M+ Annual Capacity
Massive automated volume ensuring guaranteed delivery schedules, stable raw material pricing, and rigorous carton-to-carton batch consistency.
Frequently Asked Questions by Nordic Buyers
Clear, technically verified answers covering safety certifications, minimum orders, customs duties, and diamond formulations for the Swedish market.
Q: Do your turbo diamond blades conform to the European EN 13236 standard?
Yes. Every turbo blade and diamond grinding cup exported to Sweden complies with EN 13236 safety standards. Blades undergo laser shear strength testing, dynamic balance verification up to 15,000 RPM, and bursting speed safety tests to guarantee site safety under Swedish Arbetsmiljöverket regulations.
Q: How do you prevent turbo diamond blades from glazing on hard Stockholm granite?
We use a proprietary free-cutting cobalt-bronze matrix infused with high-tenacity synthetic diamond crystals. Rather than utilizing hard iron powders which glaze over when contacting silica-rich bedrock, our matrix wears at a calibrated rate, continually exposing razor-sharp diamond crystal facets.
Q: What are your OEM private label capabilities for Swedish tool retailers?
We provide complete OEM/ODM production. This includes high-resolution fiber laser marking on blade cores, custom electrophoretic painting in brand colors, bespoke color blister packaging with EAN-13 barcodes, and bilingual English/Swedish safety instructional inserts.
Q: What is the standard lead time and shipping route for orders to Stockholm?
Standard OEM production takes 25 to 35 business days. Sea shipments dispatch from Shanghai or Ningbo ports direct to Stockholm Frihamnen or Gothenburg (Göteborg) via direct container routes (approx. 32–38 days ocean transit). For urgent orders, air freight to Stockholm Arlanda (ARN) is available.
Q: What is the Minimum Order Quantity (MOQ) for custom diamond blades?
Standard catalog items start with an MOQ of 50 to 100 units. Fully custom OEM diamond blades featuring specialized segment chemistry, bespoke laser graphics, and private label cardboard packaging generally start at 500 pieces per diameter size.
Q: Can you supply multi-bore arbors compatible with standard Nordic power tools?
Yes. We supply 22.23 mm standard angle grinder bores, 20.0 mm bores for battery handheld cut-off saws, and 25.4 mm (1") arbor configurations complete with precision-machined brass reduction drive bushings for universal fitment on Husqvarna, Stihl, Makita, and Bosch equipment.
Connect Directly with Our Tooling Engineering Team
Looking for an Intertek-audited Chinese manufacturing partner capable of engineering turbo diamond blades and high speed steel cutting tools for the demanding Scandinavian market? Request an immediate OEM quote and sample batch today.