High-Efficiency Carbide & Cobalt Drill Bit Series for Slovak Fabricators
Pre-calibrated tooling engineered to meet rigorous ISO and DIN standards, providing extended tool life and chip evacuation in abrasive stainless steels, cast iron, and high-tensile structural alloys.

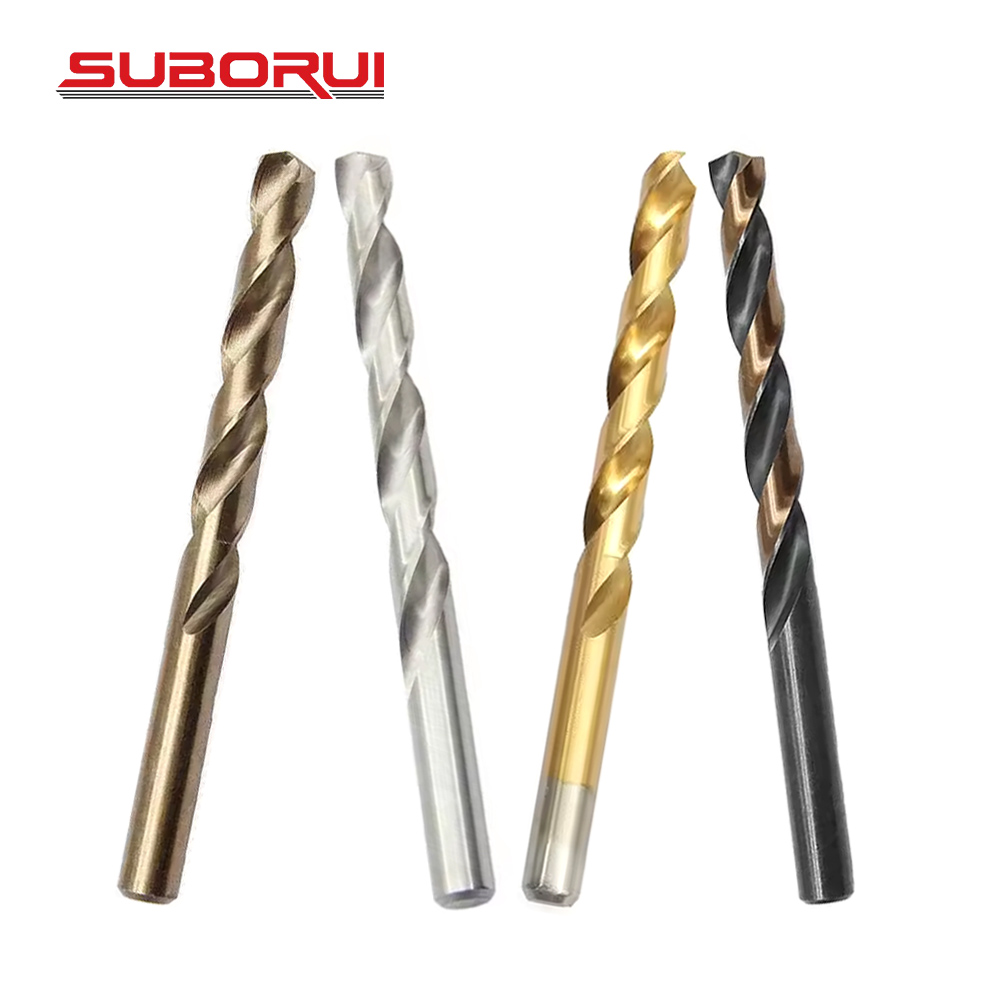



Engineering High-Yield Carbide Tooling for Slovakia's Advanced Manufacturing
A metallurgical and geometrical breakdown of cutting mechanics: balancing thermal deformation thresholds, micrograin cobalt binder matrices, and nano-layer PVD coatings in high-throughput CNC drilling operations.
Ultra-Fine Grain Tungsten Carbide (WC-Co)
The microstructural morphology of our solid carbide tooling relies on a controlled 0.4 μm to 0.7 μm sub-micron tungsten carbide grain phase, sintered with 8% to 12% pure cobalt binder. This optimal stoichiometric balance delivers a transverse rupture strength (TRS) exceeding 3,800 MPa alongside extreme hot hardness up to 92.8 HRA. For mechanical workshops in Žilina processing ductile iron castings or quenched structural steels, this prevents premature micro-chipping along the chisel edge during high-impact plunge entries.
Multi-Layered AlTiN & TiAlSiN PVD Nano-Coatings
Thermal stability is the decisive parameter separating standard tools from production-grade consumables. Our export-line drill bits utilize Physical Vapor Deposition (PVD) to bond alternating nanometer-scale layers of Aluminum Titanium Nitride (AlTiN) and silicon-doped matrices. These reach an oxidation inception barrier of 950°C, creating an in-situ aluminum oxide passivation layer under friction. This surface architecture restricts heat migration into the tool core, making high-speed dry drilling or minimum quantity lubrication (MQL) viable.
135° Split-Point Self-Centering Geometry
Eliminating work-hardening during contact is crucial when machining DIN 1.4301 (AISI 304) and DIN 1.4404 (AISI 316L) stainless grades. Our CNC fully-ground twist drill bits incorporate DIN 1412 Form C split-point sharpening. By thinning the central web to near-zero thickness and setting the point angle to 135°, axial thrust forces are reduced by 40% compared to conventional 118° tips. The bit centers instantly without center punching, preventing radial deviation and eliminating wandering on automated transfer lines.
| Tool Material Class | Grain Size / Matrix | Hardness (HRC / HV) | Max Service Temp (°C) | Primary Industrial Utility (Žilina Corridor) |
|---|---|---|---|---|
| HSS M2 (W6Mo5Cr4V2) | Conventional Cast / Milled | 63.5 – 65.0 HRC | 540°C | General structural steel (S235, S355), soft metals, maintenance workshops. |
| HSS-E M35 (5% Cobalt) | Fine-ground sintered alloy | 66.0 – 67.5 HRC | 620°C | Stainless steels, heat-resistant steels, high-feed metal fabrication. |
| HSS-E M42 (8% Cobalt) | High cobalt / carbon matrix | 67.5 – 69.0 HRC | 650°C | Heavy-duty hole saws, aerospace alloys, abrasive high-nickel stampings. |
| Solid Carbide (VHM / K20–K40) | Sub-micron WC + 10% Co | 1600 – 1850 HV10 | 850°C (Uncoated) | High-speed automotive CNC machining, grey/ductile cast irons, high batch runs. |
| AlTiN-Coated Solid Carbide | PVD Nano-composite coating | 3300 – 3500 HV0.05 | 950°C | Dry machining, tool steel dies, automotive chassis drilling, robotic lines. |
High-Precision Applications in the Žilina Regional Industrial Cluster
The Žilina Region represents Slovakia's premier hub for automotive assembly, precision bearing production, and rail transport manufacturing. Tool requirements here prioritize repeatable tool life, DIN compliance, and burr-free tolerances.
Tier-1 Automotive Component Machining & Stamping Tooling
Surrounding the major automotive manufacturing center in Teplička nad Váhom and adjacent suppliers along the Kysuce corridor, machining centers run 24/7 on cast aluminum powertrain housings, forged suspension arms, and ultra-high-strength steel (AHSS) structural stampings.
- M35 135° Split-Point Twist Drills: Designed to penetrate abrasive galvanized and heat-treated sheet steels without causing burrs on entry or exit flanges.
- Subland Step Core Drills: Allow simultaneous drilling and 90°/120° chamfering for fastener recesses in automated assembly modules, reducing machine cycle times by up to 35%.
- DIN 371 / DIN 376 Machine Taps: Available in spiral flute profiles for blind holes in automotive bracketry, ensuring chip ejection upward away from deep tapped threads.
Váh Valley Rail & Heavy Rolling Stock Engineering
Žilina's strategic location as a central European railway transport node requires heavy fabrication tooling for rolling stock repair facilities, track maintenance contractors, and bridge construction yards. Drilling through hardened manganese frog rails and thick S355J2+N structural steel beams demands tools that resist high torque shock.
Our TCT Weldon Shank Annular Cutters and Morse Taper DIN345 Drill Bits withstand aggressive torsional vibration, producing clean, dimensionally accurate bolt holes through 50mm structural flanges without work-hardening the periphery.
Industrial Plant Construction & Infrastructure Renovation
Expansion across Žilina's logistics parks, automotive supplier facilities, and highway tunnel projects (such as the Višňové tunnel corridor) requires reliable rotary hammer bits capable of cutting through reinforced aggregate and prestressed concrete.
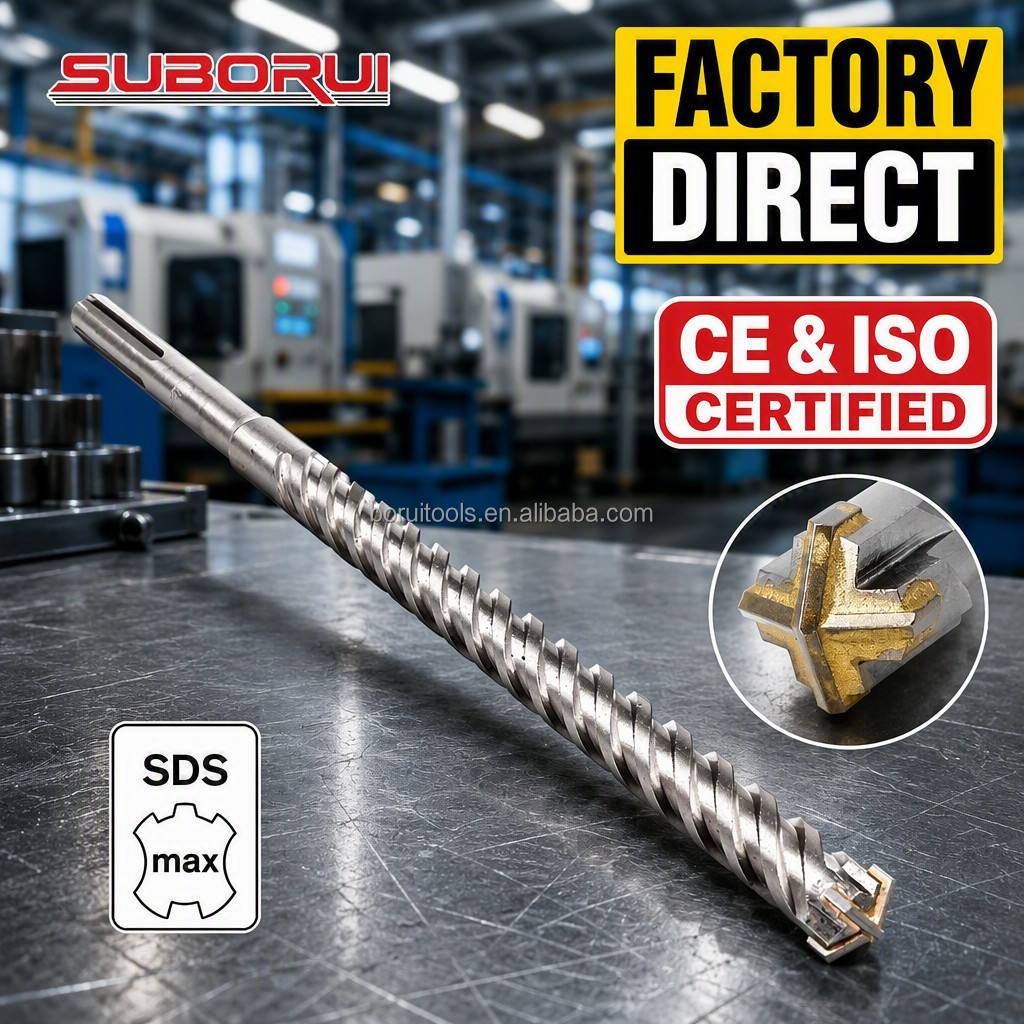
WRD Tools' SDS Max and SDS Plus Cross-Head Carbide Bits use vacuum-brazed tungsten carbide cross-tips. When striking steel rebar inside concrete columns, the 4-cutter head avoids the seizure and tip fractures common to conventional twin-cutter bits.
Precision Mechanical Workshops & Subcontract CNC Machining
From Bytča to Martin, mechanical workshops deliver contract turning and milling services for German, Austrian, and Swiss industrial OEMs. These workshops demand standard-compliant tools with traceable batch-to-batch repeatability.
- DIN 338 Fully-Ground Jobber Drills: Controlled radial runout within 0.003mm preserves spindle bearings on high-RPM Haas, DMG MORI, and Mazak machining centers.
- Precision Shank Grinding (h6 Tolerance): Ensures secure runout-free grip in hydraulic chucks, shrink-fit toolholders, and ER collets.
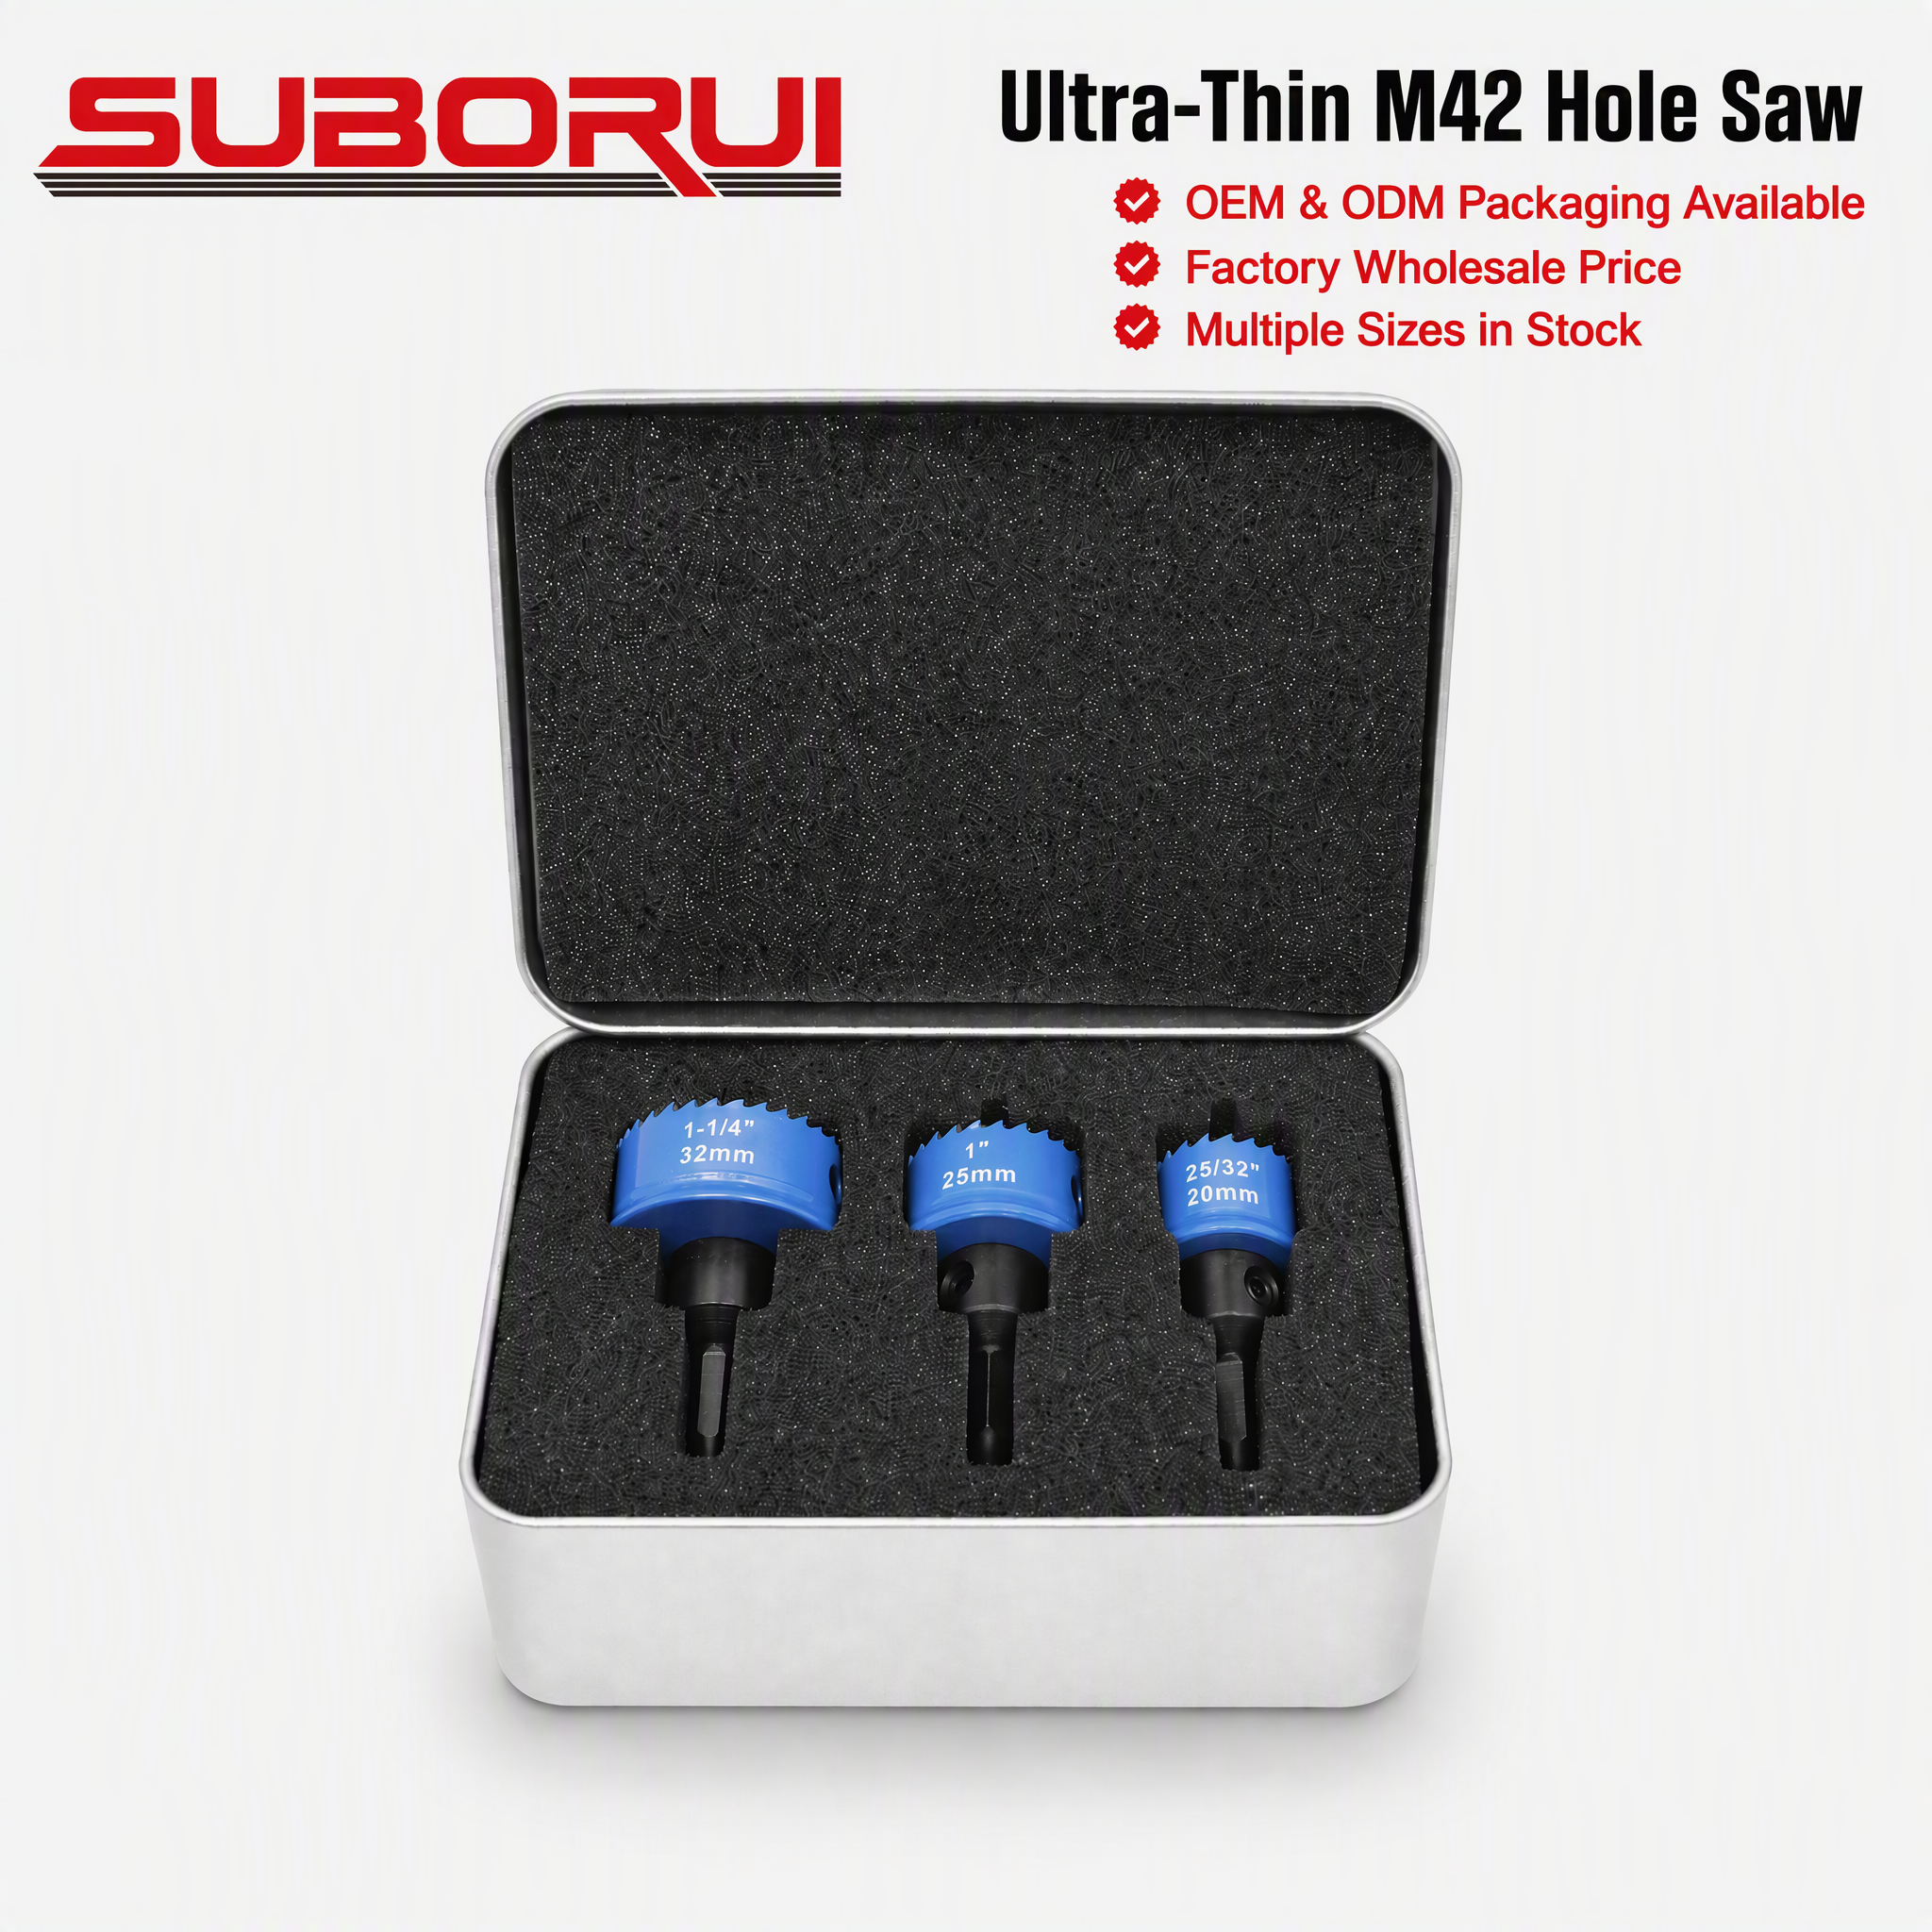
- M42 Cobalt Hole Saws: Designed for electrical control panel cutouts, utility cabinets, and thin stainless enclosures, maintaining cutting edge sharpness.
Shifting Sourcing Strategies: Dual-Sourcing & Direct OEM Factory Integration
Industrial tooling procurement in Central Europe has evolved. Buyers are navigating supply chain shifts, balancing quality, landed cost, and inventory security.
Mitigating Intermediated Markups
Historically, Slovak engineering firms purchased Chinese cutting tools via Western European trading houses, paying markups ranging from 45% to 80%. As industrial margins tighten across the EU automotive sector, procurement managers in Žilina are establishing direct relationships with verified Chinese manufacturers like Jiangsu WRD Tools. Direct factory sourcing provides custom laser etching, tailored flute geometry, and standardized DIN tolerances without third-party price markups.
Dual-Sourcing Supply Chain Resilience
Supply chain interruptions have prompted European plant directors to implement dual-sourcing models. Rather than relying on a single domestic or local supplier, operations maintain active relationships with high-capacity overseas manufacturers capable of producing 90 million units annually. This protects tool cribs against regional raw material shortages, localized strikes, and sudden supplier price spikes.
Standardized DIN & ISO Compliance Protocols
Slovak machine operators work within strict ISO quality management frameworks. Sourcing decisions hinge on certified compliance with DIN 338 (jobber drills), DIN 340 (long series), DIN 352 (hand taps), and ISO 5468 (masonry drills). Exporters who provide complete EN 10204 3.1 material test certificates and third-party facility audits (such as Intertek verification) consistently win vendor approvals over generic trading agents.
Frequently Asked Questions by Žilina Sourcing Directors
Practical answers addressing logistics, customs handling, quality control standards, and technical specifications for Slovak and Central European tool distributors.
What are the typical logistics routes and customs clearance procedures from your Jiangsu factory to Žilina, Slovakia?
Can your factory provide EN 10204 3.1 chemical analysis and hardness inspection certificates?
How do you handle Minimum Order Quantities (MOQ) for Slovak regional tool distributors?
What are the operational differences between M35 5% Cobalt and Solid Tungsten Carbide (VHM) for stainless steel drilling?
Can you support customized OEM branding, shank markings, and private-label packaging?
How does your factory ensure flute concentricity and dimensional tolerances across high-volume production?
Why Major Global Tool Brands Rely on Jiangsu WRD Tools
Operating from Danyang, Jiangsu—China's primary cutting tool industrial cluster—Jiangsu WRD Tools Co., Ltd. combines nearly two decades of precision manufacturing with strict third-party audited quality control.
Intertek On-Site Verified Facility
Our 12,000 square meter plant, advanced manufacturing lines, raw material storage facilities, and Quality Assurance laboratory have been audited and verified on-site by Intertek Group. Our management and factory systems adhere to internationally recognized ISO 9001:2015 quality frameworks, ensuring that production matches our quoted specifications from the first sample through bulk container shipments.
Provincial High-Tech Enterprise Recognition
Awarded official High-Tech Enterprise status by the Jiangsu Provincial Government in 2019, WRD Tools invests over 5% of annual revenue into tooling R&D. Our engineering team holds proprietary patents across precision flute geometry, low-friction relief surfaces, and advanced vacuum heat treatment processes, ensuring tool longevity that competes with German and Japanese alternatives.
Trusted OEM Partner to Global Industry Leaders
Over our 19-year history, our factory workshops have manufactured drill bits, taps, and hole saws for some of the world's most recognized cutting tool and hardware brands, including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Dexter, KWB, Wolfcraft, Truper, and Heller. We bring this tier-one contract manufacturing expertise directly to our European partners.
Request Custom Quotations & Technical Test Samples
Planning a supply tender or looking to optimize your tool cost-per-hole in the Žilina industrial area? Connect directly with our bilingual export engineering desk. We provide comprehensive technical dossiers, CAD drawings, and prototype tooling batches within 24 business hours.