Engineered Tooling Solutions
High-integrity drill bits, hole cutters, and masonry accessories certified under EN ISO standards for industrial supply chains and commercial distributors.

SUBORUI 1/4 Inch HSS Fully Ground Titanium Coated Metal Hex Shank Twist Drill Bit ISO Certified Customizable OEM
Engineered with self-centering 135-degree split-point tips for rapid swarf ejection and zero wander in impact drivers.
View Details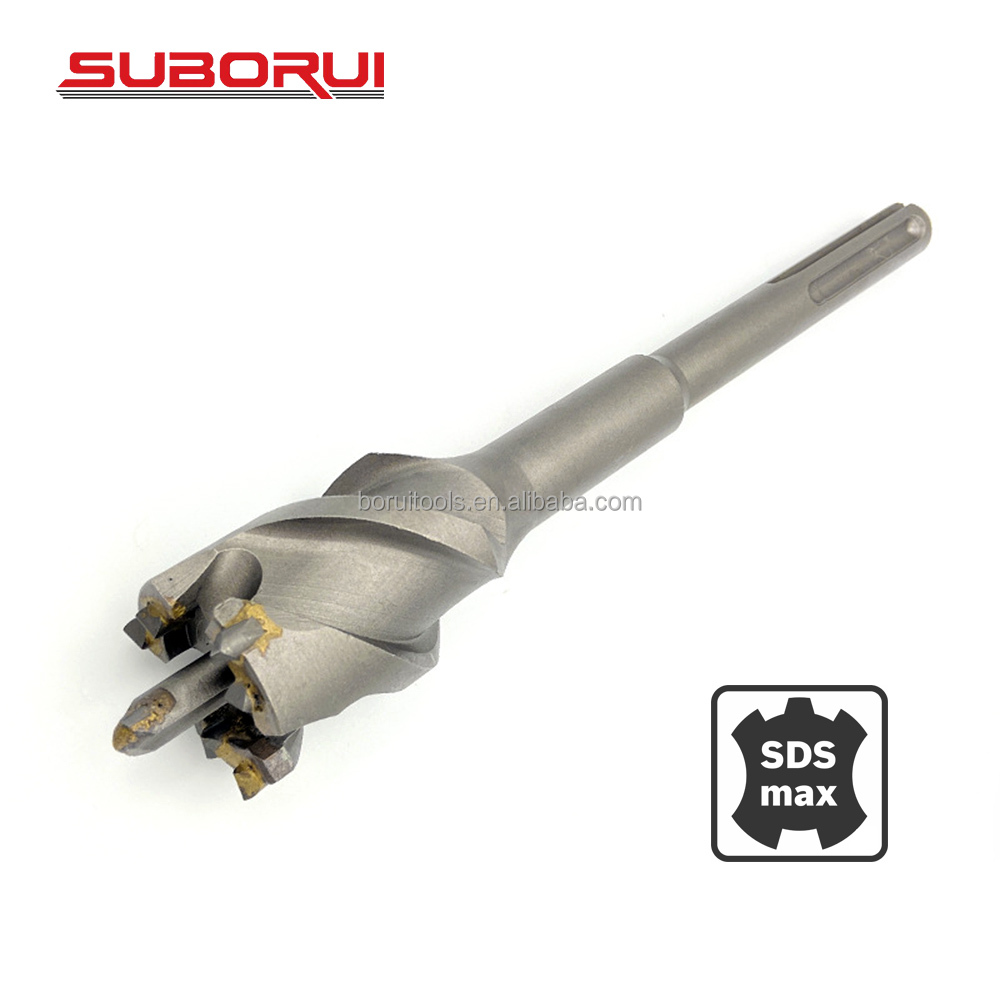
SUBORUI Carbide Sds Max Electric Hammer Wall Hollow Drill Bit Concrete Hole Saw for Cement Stone Concrete Wall
Heavy-duty tungsten carbide tipped core bits designed for aggregate penetration and deep wall penetrations.
View Details
SUBORUI Super Thin Hot Pressed Net Wave Diamond Cutting Marble Ceramic Turbo Saw Blade for Porcelain Tile Cutting Disc
Hot-pressed continuous rim geometry preventing chipping across glazed ceramics, vitreous tile, and granite slabs.
View Details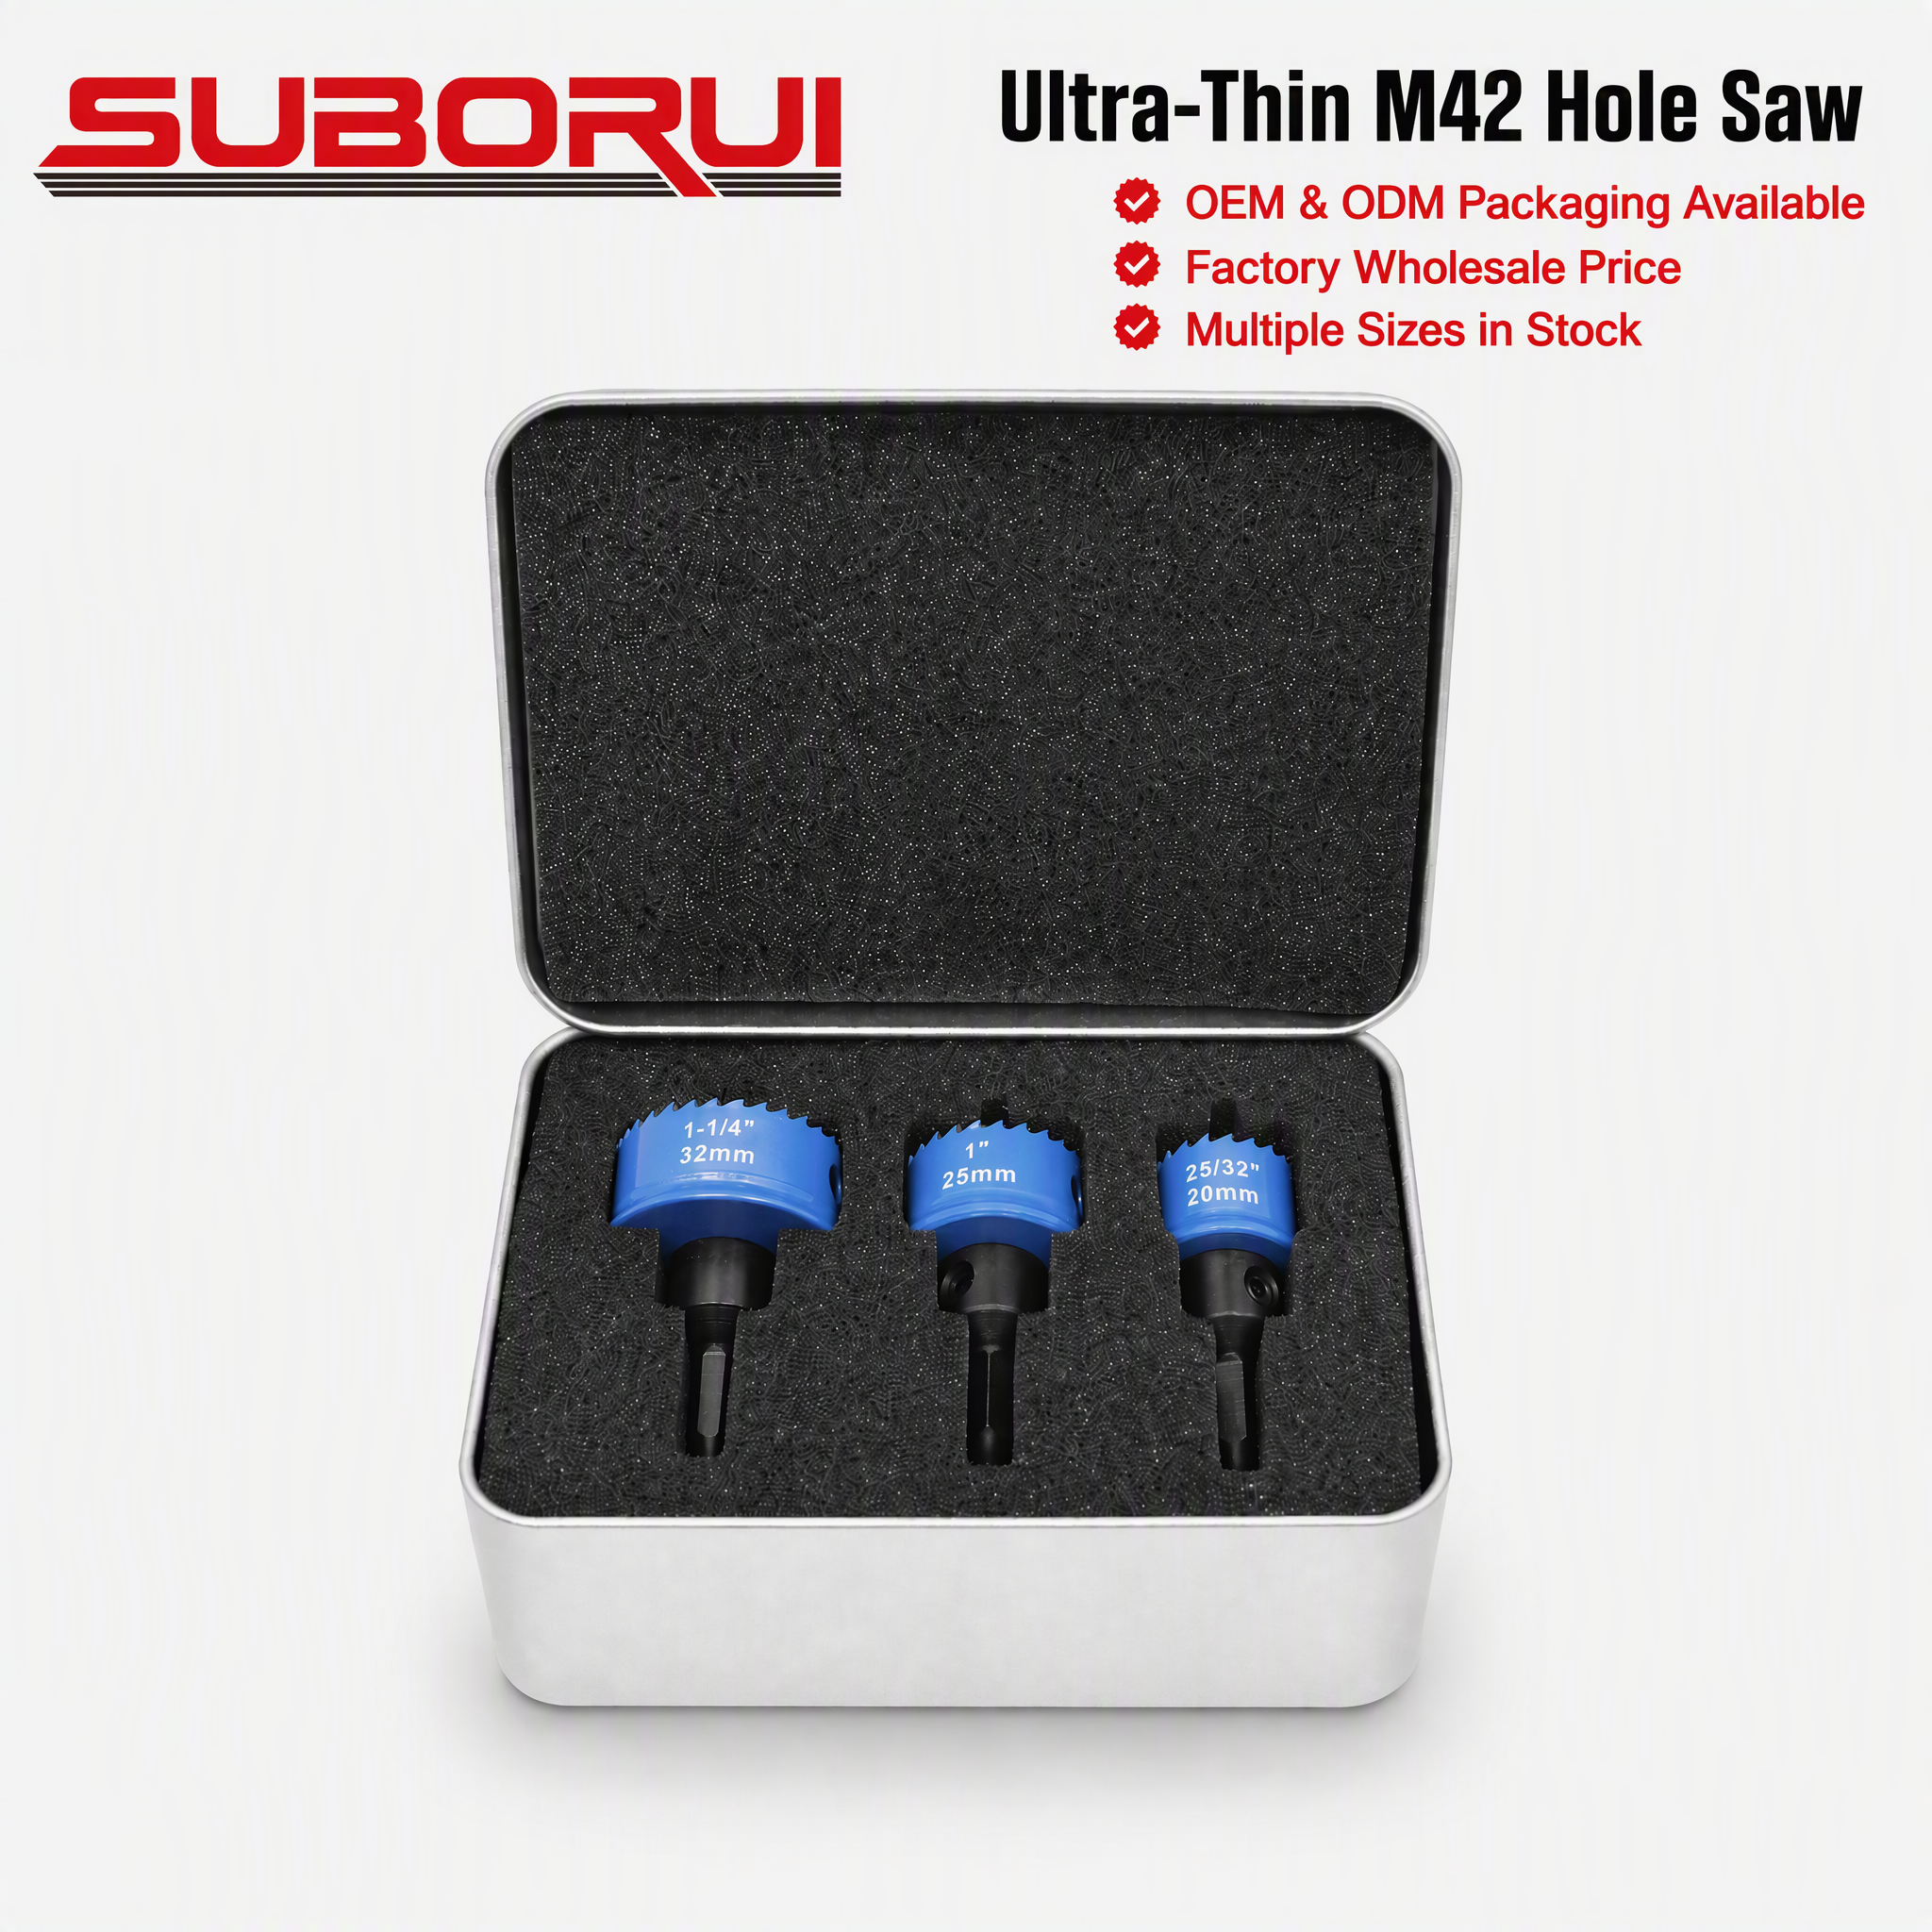
SUBORUI OEM Factory 3pcs 20mm 25mm 32mm Ultra-thin Hex Shank M42 Bi-Metal Hole Saw Cutter Set for Metal Cutting
M42 8% cobalt matrix with variable tooth pitch for rapid, clean boring through stainless sheets and structural steels.
View Details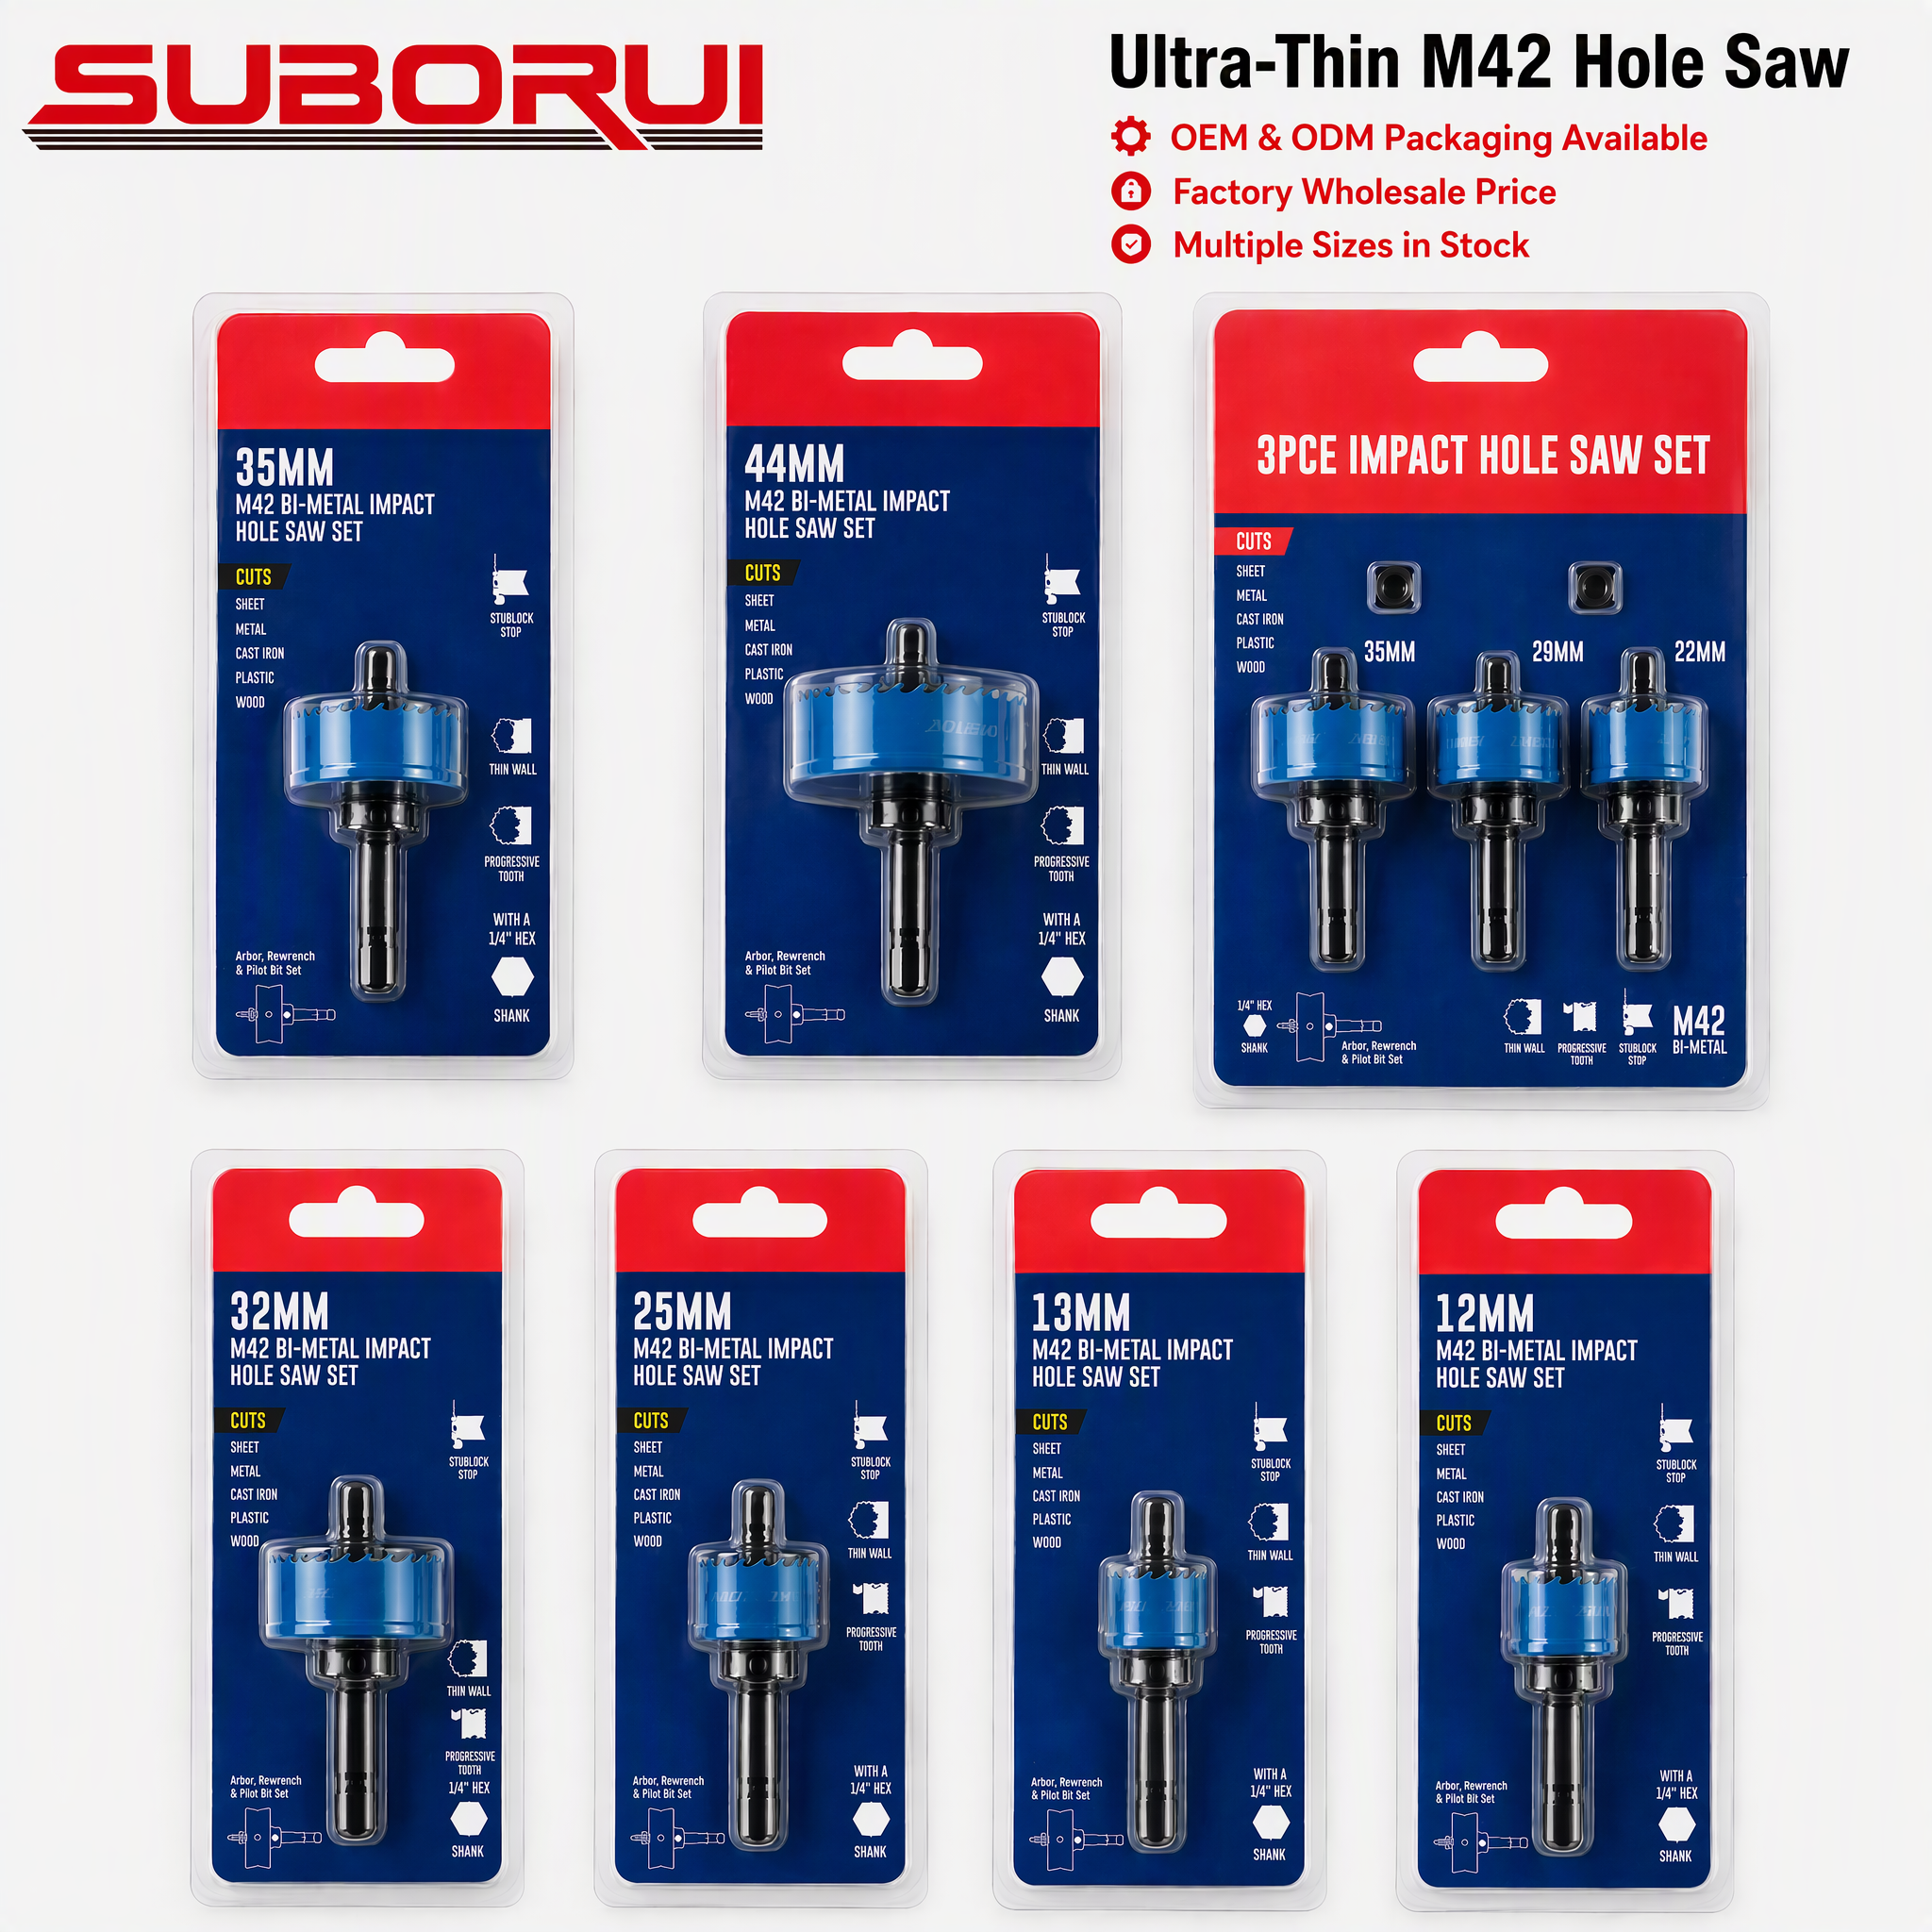
SUBORUI OEM ODM Wholesale Premium 14mm-60mm Ultra-thin 1/4 Hex Shank M42 Bi-Metal Hole Saw for Metal and Wood
Thin kerf construction reducing energy consumption on cordless tools while delivering long wear life across hardwoods and cast metals.
View Details
SUBORUI M42 Bi-Metal Drill Bit Cutter Carpentry Tools Wood Cutting Metal PVC Plastic Iron Wood Hole Saws
Impact-resistant alloy body electron-beam welded to high-cobalt cutting edges for composite materials and metals.
View Details
BORUI 12-80MM Hole Saw Drill Bit Set HSS Hole Cutter for Stainless Steel, Metal, Iron, Wood With Plastic Box
Complete modular master kit packed in blow-molded custom casing, optimized for commercial mechanical installations.
View Details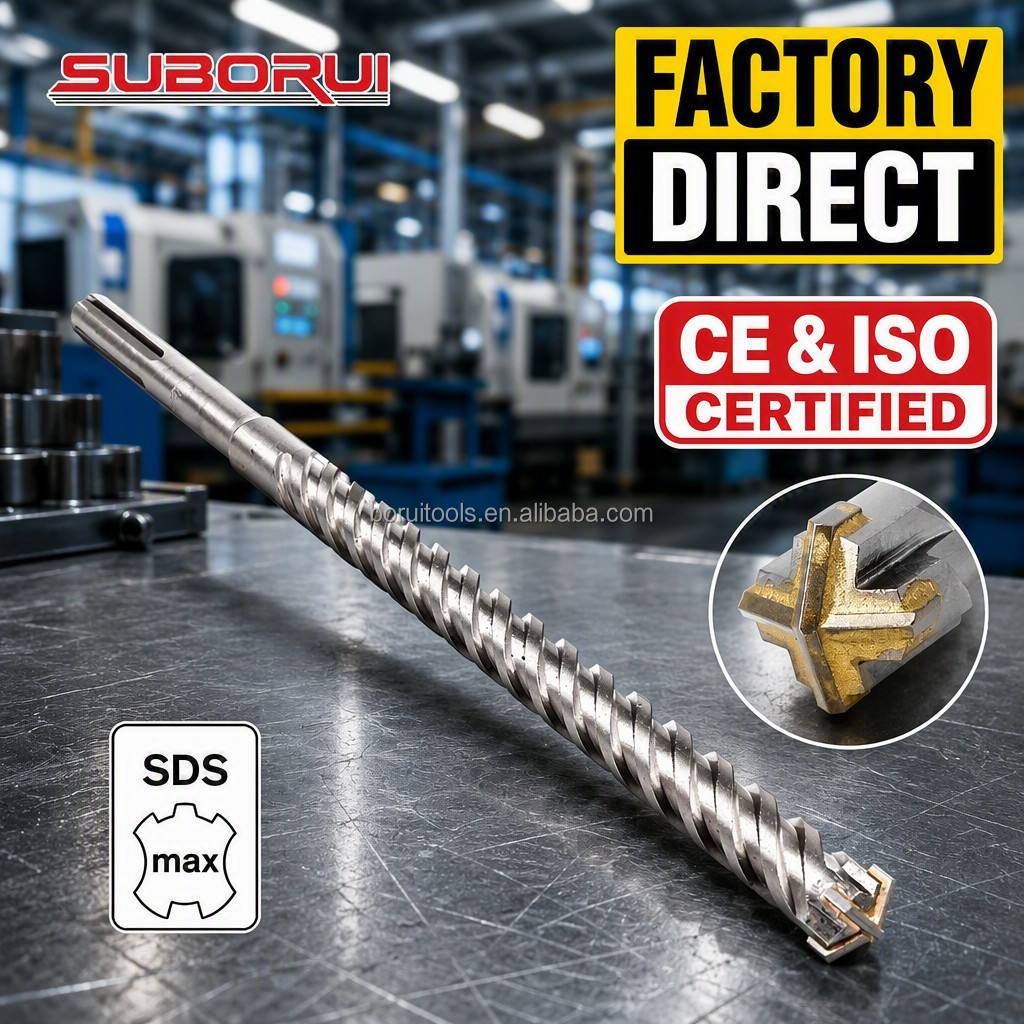
SUBORUI OEM 280mm 400mm 600mm Sds Max Plus Cross Carbide Tipped Rotary Masonry Hammer Drill Bits for Masonry Concrete Drilling
Solid cross-head 4-cutter design eliminating jamming upon rebar impact; heat-treated flute minimizes lateral vibration.
View Details🔬 Metallurgical Integrity: Cobalt Drill Bit Science for Harsh Environments
Industrial hole-making applications require tools engineered to withstand elevated friction and deformation resistance. In challenging operational regions like Norsup and greater maritime industrial hubs, field engineers regularly drill through abrasive, work-hardening alloys such as AISI 304, marine-grade 316 austenitic stainless steel, and weather-resistant structural plate. Standard high-speed steels (such as HSS 4241 or conventional carbon steels) undergo rapid thermal degradation once flute boundary temperatures surpass 400°C.
Our factory utilizes verified metallurgical grades of M35 (containing 5% active Cobalt) and M42 (containing 8% Cobalt). By introducing cobalt into the tungsten-molybdenum alloy matrix, the secondary hardness (red hardness) is elevated to withstand friction heat in excess of 600°C to 650°C without plastic deformation. Every drill blank is processed through computerized vacuum heat-treatment furnaces and triple-tempering regimes, guaranteeing a core and surface hardness profile of 65–68 HRC. This continuous structural stability prevents premature flank wear, chip-lip fracture, and bore out-of-roundness.
| Steel Grade | Composition Profile | Hardness (HRC) | Thermal Threshold | Primary Industrial Substrates |
|---|---|---|---|---|
| HSS 4241 | W1Mo4Cr4V | 61 - 63 HRC | Up to 380°C | Soft woods, non-ferrous sheet, general DIY repairs |
| HSS M2 (6542) | W6Mo5Cr4V2 | 63 - 65 HRC | Up to 500°C | Medium carbon steel, cast iron, mild alloys |
| HSS M35 (Co 5%) | W6Mo5Cr4V2Co5 | 65 - 67 HRC | Up to 620°C | 304/316 Stainless steel, titanium, boiler plate |
| HSS M42 (Co 8%) | W2Mo9Cr4VCo8 | 67 - 69 HRC | Up to 660°C | Hardened tool steel, nickel superalloys, Hastelloy |
Furthermore, our DIN338-compliant fully ground flute geometry features a 135° split-point geometry conforming to DIN 1412 Form C. This cross-ground design reduces thrust force requirements by up to 40% compared to standard 118° chisel edges. The immediate bite eliminates drill walking—removing the necessity of pilot punching when working off-grid or inside utility bays where mechanical clamps cannot be positioned.
Norsup Market Dynamics & Operational Scenarios
Optimized for harsh salt spray exposure, isolated infrastructure maintenance, and high-demand commercial fabrication.
⚓ Marine & Coastal Facility Maintenance
In humid, salt-dense coastal installations near ports and inter-island supply lines, rust-resistant stainless steel fasteners and marine hardware are universal. Standard bits dull instantly against work-hardened 316 alloy. Our TiAlN- and Amber-treated M35 drills dissipate salt-laden moisture, resisting corrosion on work sites while cutting cleanly without cold-welding the flutes.
🏗️ Off-Grid Infrastructure & Power
Remote maintenance in isolated townships demands versatile, dependable tools. With limited replacement supply lines, our hex shank M35 bits and bi-metal cutters are matched directly with battery-powered cordless impact systems, conserving charge through low friction geometries and sharp rake angles.
🌱 Agriculture & Marine Agro-Processing
Heavy machinery used in copra milling, processing facilities, and refrigeration plants experiences high mechanical shock. Maintenance crews rely on our extra-length DIN1869 bits and TCT wall hole saws to bore through reinforced mounts, heavy frames, and concrete footings without structural failure.
🏆 Factory Credibility & Global OEM/ODM Track Record
Jiangsu WRD Tools Co., Ltd. (established in March 2007, registered capital RMB 10 million) is not an intermediary broker or exporting trader. We are an established cutting-tool manufacturer situated directly within Danyang, Jiangsu Province—the epicenter of high-speed steel tool fabrication. Spanning over 12,000 m² of specialized workshops, our facility employs over 150 technicians and manufacturing specialists producing upwards of 90 million tooling units annually.
Our factory capability has been verified onsite by Intertek, ensuring complete transparency regarding QA/QC systems, material provenance, and export fulfillment. In recognition of our R&D investments and continuous patent developments in multi-step flutes and carbide metallurgy, our enterprise was formally recognized as a High-Tech Enterprise of Jiangsu Province. Over 19 years of continuous manufacturing, we have served as a contract OEM/ODM partner for tier-one tool corporations across 20+ countries, producing lines compatible with brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, and Heller.
⚙️ In-House Production
End-to-end processing: raw bar stock cutting, automated salt-bath heat treatment, CNC grinding, and laser engraving under a unified ISO9001 quality framework.
📐 OEM Customization
Custom split point angles (118°/135°), specialized coatings (TiN, TiAlN, Amber Bronze, Black Oxide), shank geometries, and bespoke branded retail packaging.
🚢 Scalable Logistics
Fast turnaround on standard catalog items and complete containerload consolidation directly through Shanghai port with comprehensive bill of lading documentation.
Frequently Asked Questions for Regional Sourcing
Detailed technical specifications and commercial parameters for commercial purchasing managers.
What are the key technical differences when ordering M35 vs. M42 cobalt drill bits for local projects?
M35 high-speed steel contains 5% cobalt, yielding a surface hardness of 65–67 HRC. It delivers high resilience against torsional shear and is optimal for drilling structural steels, carbon plate, and austenitic stainless steels (304 and 316). M42 features 8% cobalt, pushing secondary hardness to 68–70 HRC. While M42 withstands higher heat and abrasive cutting conditions, it possesses slightly higher brittleness. For general commercial jobbing, M35 is the most cost-effective solution; for repetitive CNC drilling in heat-treated alloys or thick stainless plate, M42 provides lower cost-per-hole economics.
How does CE and ISO compliance protect regional commercial importers?
CE marking and ISO certifications verify that the tools conform to European and international mechanical safety, dimensional tolerance, and metallurgy guidelines. For distributors in the Norsup and regional Pacific sectors, non-certified cutting tools often contain uneven carbide distributions or improper tempering, resulting in catastrophic fracturing under impact. Our certified bits maintain exact shank-to-tip concentricity within 0.02 mm, preventing runout, preserving power tool gearboxes, and protecting machine operators.
What Minimum Order Quantities (MOQ) apply for private-label distributor packaging?
For standard unbranded or factory-branded bulk items, MOQs begin at 100 to 500 units depending on diameter. For full custom OEM production—including custom laser branding on the tool shanks, surface finish variations, and branded display blister boxes or heavy-duty metal cases—our baseline production runs generally start at 1,200 sets or equivalent volume. Consolidations with other tool types (such as SDS hammer drills, annular cutters, and hole saws) are fully accommodated.
Which flute coatings are best suited for coastal marine climates?
For salty maritime settings, we suggest our Amber Oxide (steam tempered) or TiAlN (Titanium Aluminum Nitride) finishes. While standard bright polished bits provide a smooth finish, they require continuous lubrication to avoid corrosion during long sea transit. Amber oxide creates a porous, oil-retaining oxide skin that locks in protective lubricants, whereas TiAlN creates an ultra-hard ceramic barrier that repels oxidation and provides dry-lubrication properties when tapping or drilling off-grid.
What are the lead times and shipping routes for regional orders?
Standard orders are fulfilled within 25 to 35 business days depending on custom packaging specifications. We routinely stage shipments via EXW, FOB, or CIF arrangements departing Shanghai or Ningbo ports. Full container load (FCL) and less-than-container load (LCL) configurations are palletized with moisture-barrier wrapping and anti-corrosion VCI liners to guarantee pristine arrival in overseas ports.
Equip Your Distribution Network with Factory-Direct Tooling
Partner with an Intertek-audited manufacturing leader. Submit your technical blueprints, required flute geometries, or annual procurement volume for an immediate factory-direct proposal.
Get a Quote