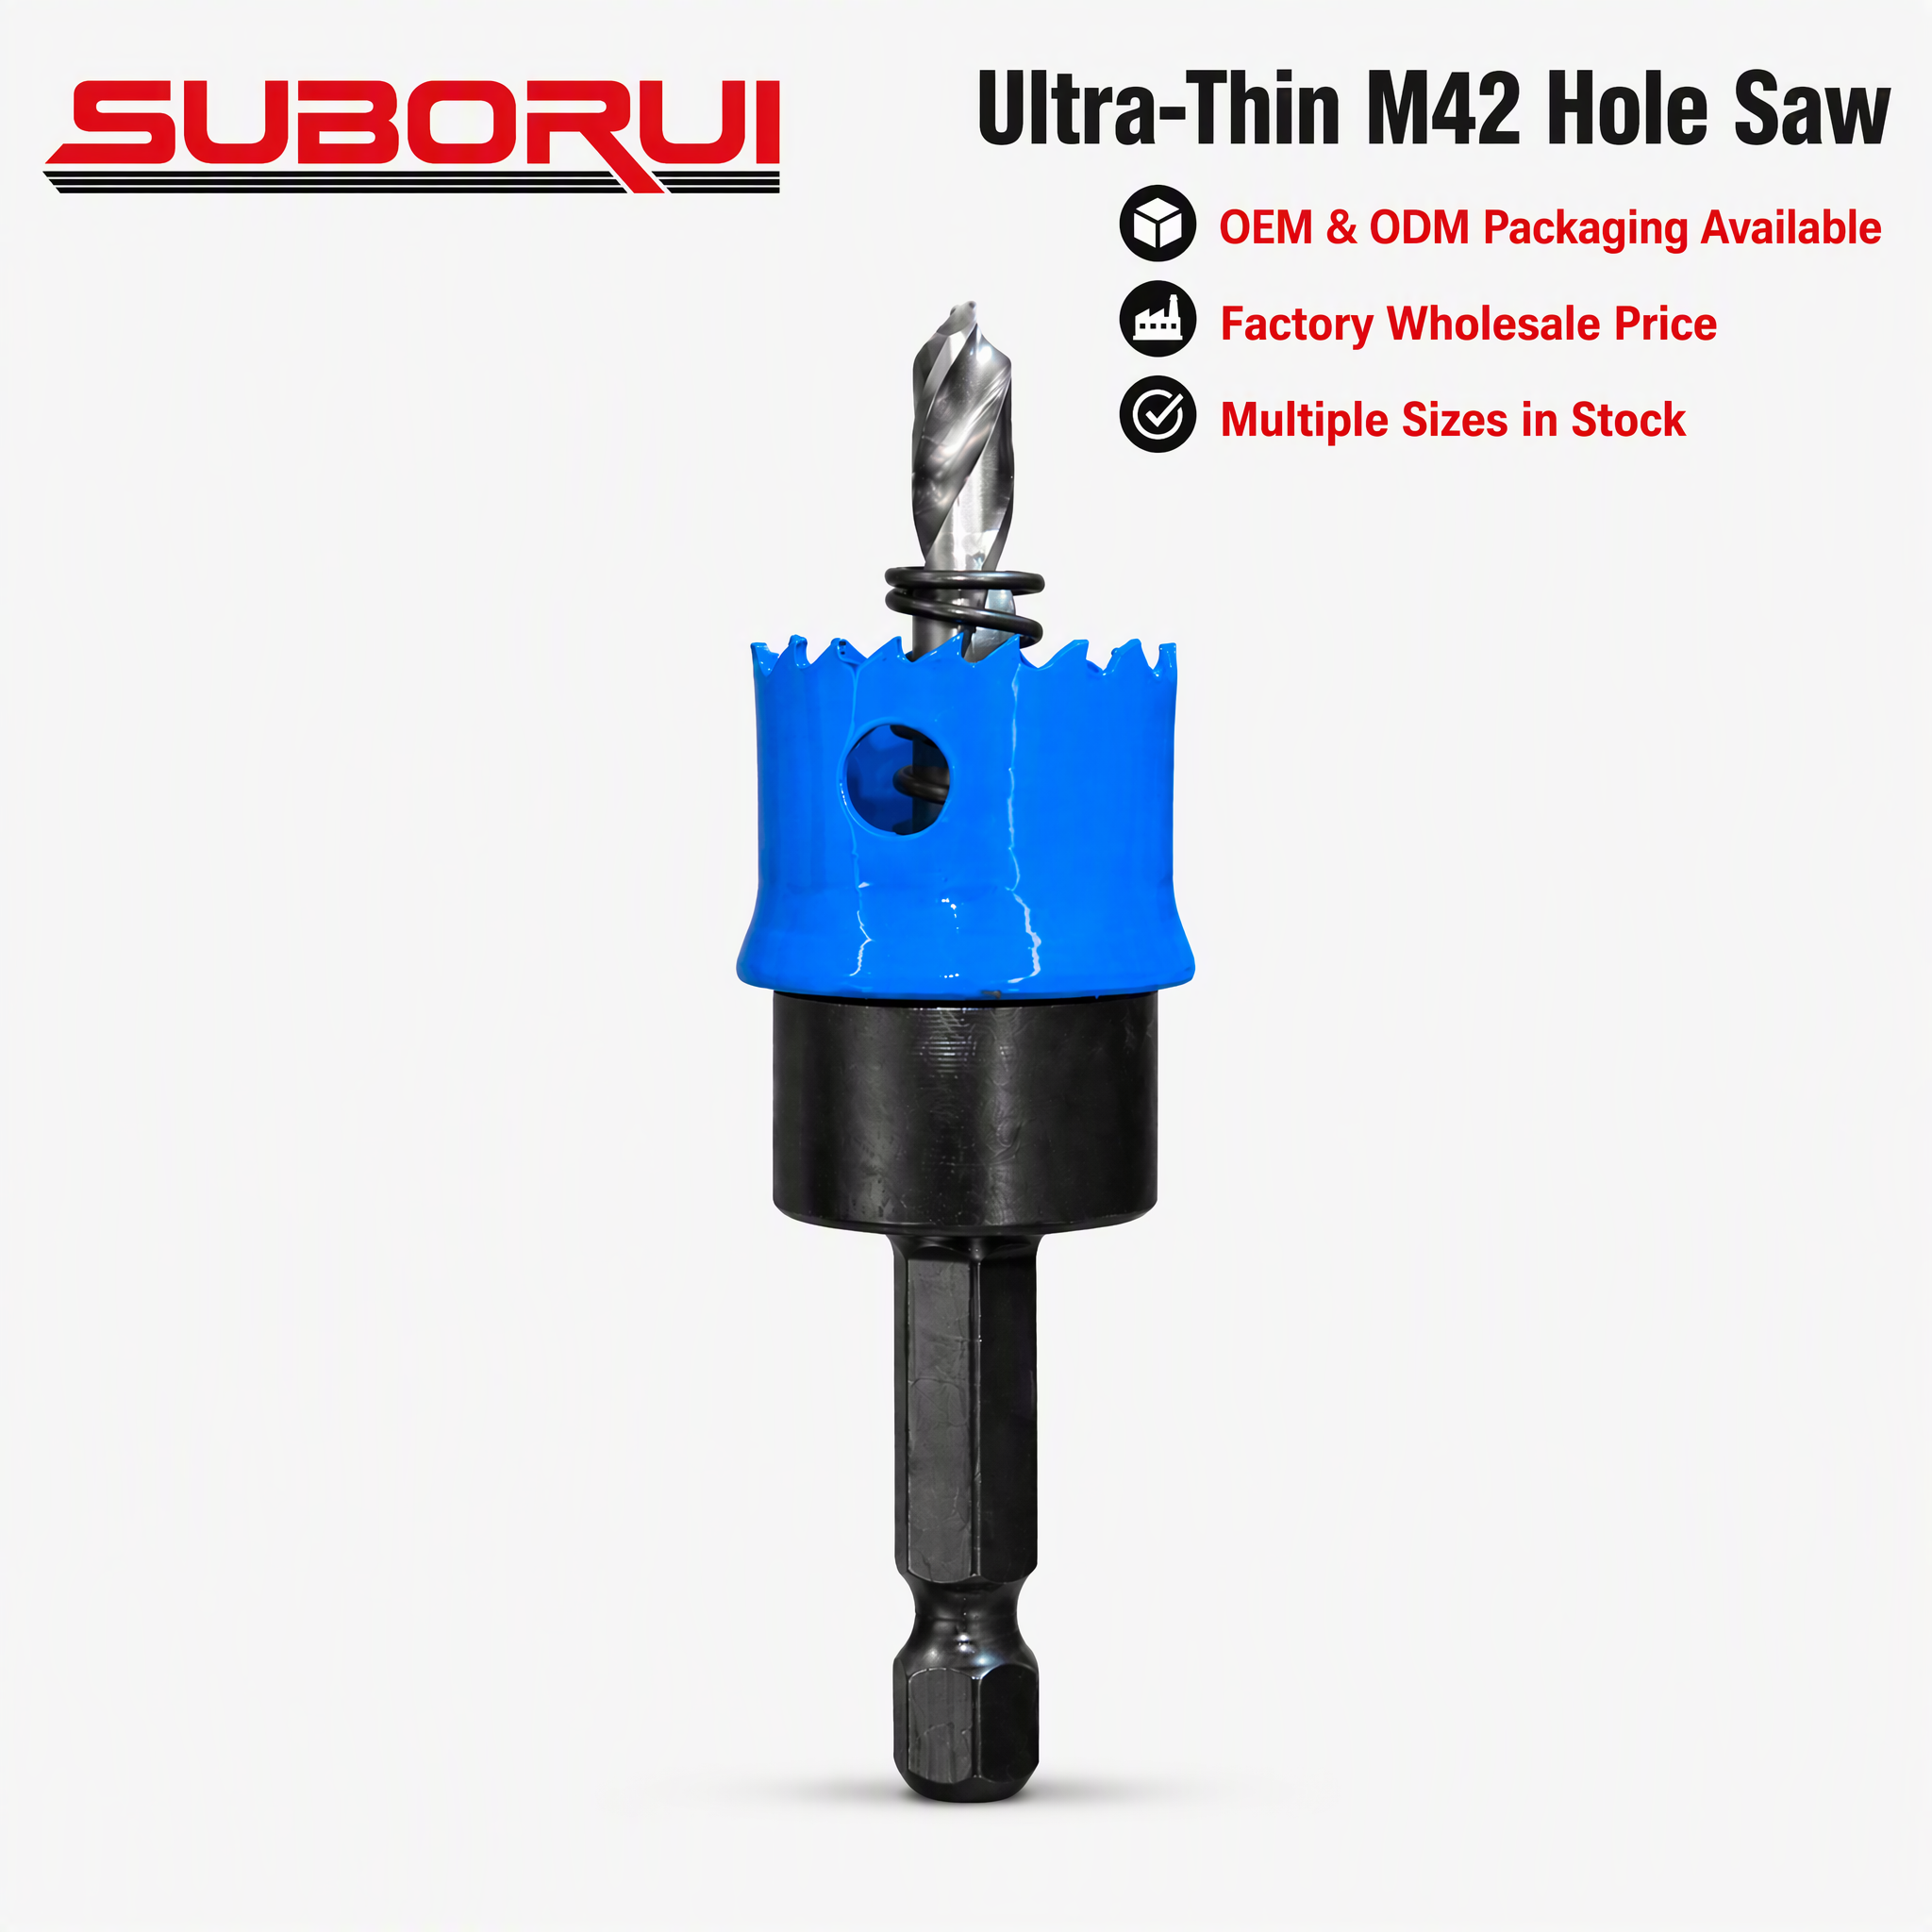
SUBORUI OEM 14mm-50mm Ultra-Thin Hex Shank M42 Bi-Metal Hole Saw
Engineered specifically for sheet metal drilling and electrical panel punchouts. Ultra-thin kerf minimizes motor load on battery tools while reducing chip heat build-up.
View DetailsBuilt using vacuum electron-beam welding and metallurgical precision grinding, our bimetal and companion high-speed tool lines deliver repeatable tool life under aggressive structural feed rates.
Engineered specifically for sheet metal drilling and electrical panel punchouts. Ultra-thin kerf minimizes motor load on battery tools while reducing chip heat build-up.
View Details
Ground from premium HSS M2 (6542). Complete 3-piece sets (taper, second, plug) for clean internal thread restoration and tapping in ship maintenance workshops.
View Details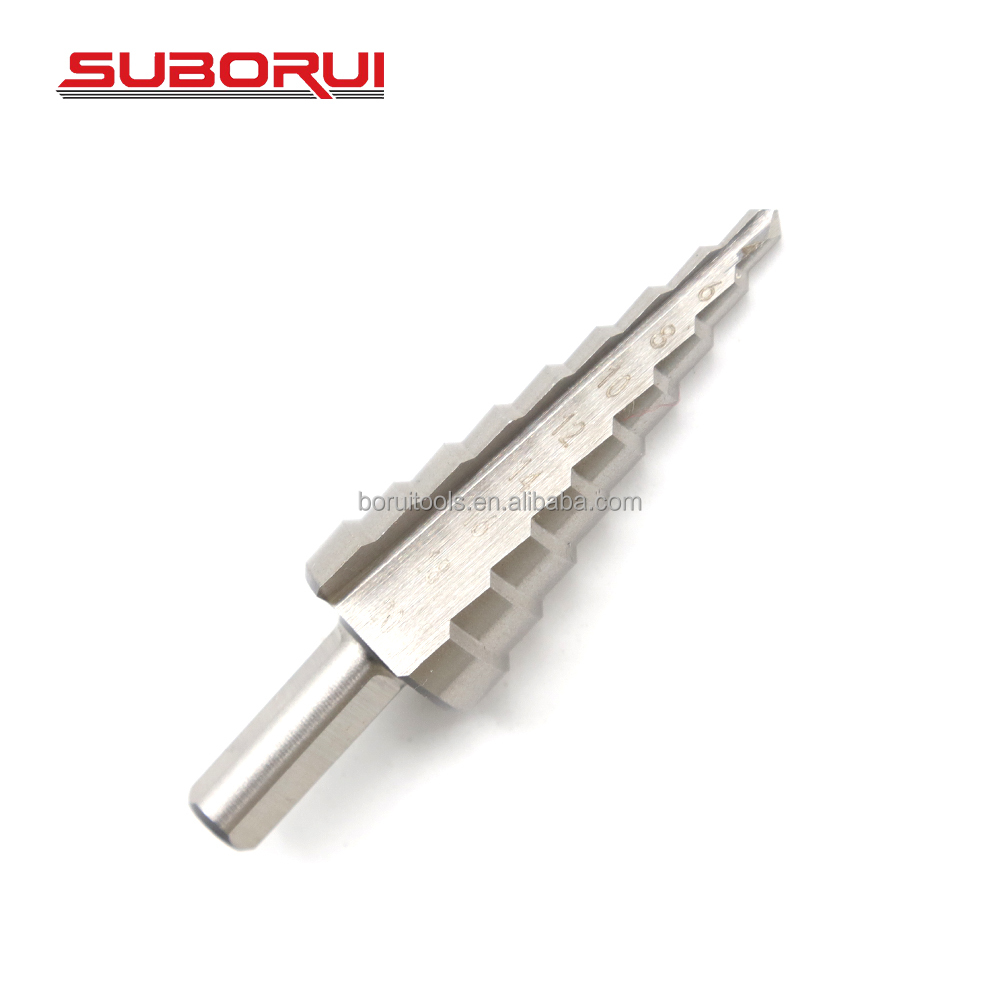
Precision dual straight flutes designed to deburr as you drill. Ideal for electrical junction boxes, duct installations, and non-ferrous aluminum marine decking.
View Details
Borderless wide-gullet hole opener engineered for clean, splinter-free downlight recessing in drywall, plywood veneers, acoustic ceiling tiles, and structural timber.
View Details
4/6 variable tooth design with 8% Matrix cobalt tips. Delivers exceptional heat dissipation and chatter resistance when cutting composite marine paneling and steel pipes.
View Details
Heavy-duty hole cutter assortment designed for thick-gauge iron, structural pipe, and 304/316 marine-grade stainless plate. Includes spring-loaded arbor and pilot pins.
View Details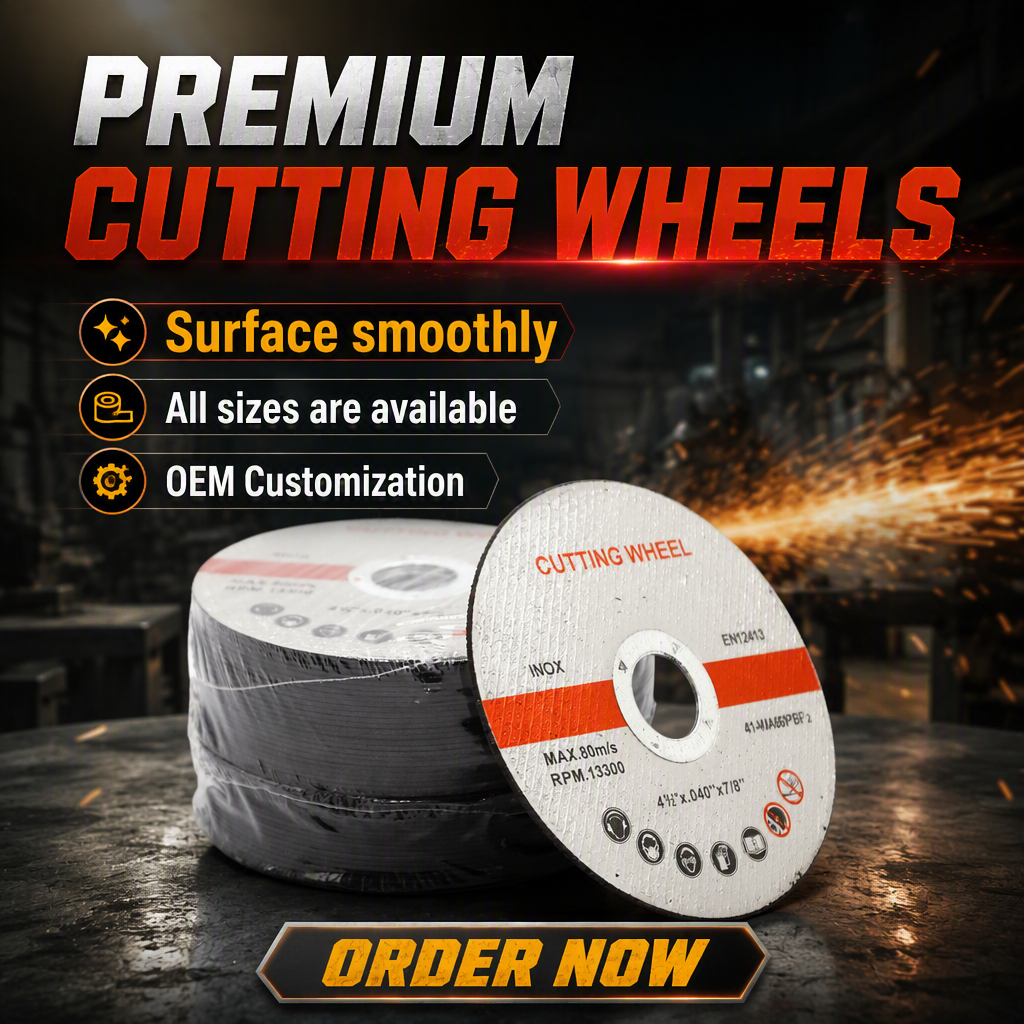
Double fiberglass reinforced bonding formulation for rapid slicing of angle iron, structural channel, and schedule-40 steel piping in fabrication yards.
View Details
Manufactured with 135° self-centering split point geometry to eliminate walking on curved pipes and heavy stainless structural beams in shipyard environments.
View DetailsThe Baltimore metropolitan area represents one of the United States' premier multimodal transportation hubs, maritime hubs, and defense manufacturing epicenters. Anchored by the Port of Baltimore (Helen Delich Bentley Port of Baltimore), industrial operations within the Patapsco River basin and surrounding hubs like Sparrows Point demand cutting tools built to rigorous metallurgical standards. When cutting thick plate in marine retrofits or executing field installations along logistics terminals, standard high-carbon hole saws fail rapidly through tooth shearing and catastrophic frictional annealing. WRD Tools bimetal hole saws bridge this technical performance gap by bonding electron-beam welded M42 high-speed steel containing 8% cobalt to a high-tensile spring steel backing alloy (AISI 6150).
In the maritime overhaul corridors of Curtis Bay and Locust Point, contractors routinely penetrate 304 and 316 marine-grade austenitic stainless steel enclosures, bulkhead penetrations, and brass sea-chest plumbing. Austenitic alloys work-harden almost instantaneously under low chip load or excessive rotational friction. Our M42 hole saws leverage a precision-engineered 4/6 variable tooth pitch profile with a positive 10-degree rake angle. This configuration ensures an aggressive forward shear cut, slicing through the work-hardening barrier rather than rubbing against the substrate. This lowers heat build-up and maintains cutting efficiency even when working aboard dry docks or floating barge cranes where mechanical lubrication delivery is limited.
Simultaneously, the revitalization of Tradepoint Atlantic at Sparrows Point—converting the former historic Bethlehem Steel plant into a 3,300-acre global logistics hub—has generated strong demand for mechanical, electrical, and plumbing (MEP) penetrations. Slicing through heavy-gauge galvanized unistrut, corrugated steel roof decking, electrical knockout panels, and schedule-80 water service mains requires cutting tools with high resistance to torsional binding. WRD bimetal hole saws feature a solid, thickened base cap (0.25-inch cold-rolled steel) that minimizes vibration, ensures true circular runout, and prevents the drive-pin holes from stripping out under the high-torque clutches of commercial impact drills and magnetic drill presses.
Selecting the correct metallurgical alloy is crucial to calculating Total Cost per Hole (TCPH) in commercial steel fabrication and civil contracting across the Baltimore industrial basin.
| Performance Parameter | Standard Hardware HSS (M2 / 4241) | WRD Industrial Bi-Metal M42 (8% Cobalt) | TCT (Tungsten Carbide Tipped) |
|---|---|---|---|
| Tooth Hardness (Rockwell) | 61 - 63 HRC | 67 - 69 HRC (Enhanced Red Hardness) | 89 - 91 HRA (Extremely Hard) |
| Thermal Breakdown Limit | 450°C (842°F) - Rapid Edge Rounding | 650°C (1202°F) - Retains Cutting Edge | 950°C (1742°F) - Thermal Resilient |
| Shock & Impact Resistance | Moderate (Prone to chipping on welds) | Superior (Alloy spring back absorbs shock) | Low (Brittle teeth crack on interrupted cuts) |
| Optimal Substrate Fit | Softwood, gypsum, mild thin carbon sheet | Marine stainless 316, ductile iron, thick steel | Abrasive composite, cast iron, masonry block |
| Mean Holes per Unit (3/16" 304SS) | 12 - 18 Cut cycles | 75 - 110 Cut cycles | 120 - 160 Cut cycles (Steady feeds only) |
| Vibration Damping Index | Standard stamped cup | Heavy reinforced 6.35mm drive backplate | Rigid ground body with pilot spring |
With massive state investments in offshore wind staging at Tradepoint Atlantic and the federal modernization of the Chesapeake navigation fairways, procurement managers are sourcing heavy-duty, corrosion-treated M42 cutting tools engineered to penetrate galvanized marine coatings and thick offshore tubular scaffolding.
The intensive marine recovery and continuous rebuilding of critical transportation links across the Baltimore harbor require rapid delivery of heavy-gauge hole cutters. Crews working over water prioritize high durability and tooth-retention stability over single-use consumable bits.
Industrial hardware supply houses across Maryland, Virginia, and Delaware are actively bypassing secondary domestic distributors. Sourcing direct from Intertek-audited OEM manufacturers like WRD Tools enables localized private labeling with margin advantages exceeding 38%.
Operating out of Danyang—China's world-renowned cutting tool manufacturing center—we provide end-to-end metallurgical quality control, certified testing, and flexible private branding for leading global tool suppliers.
Unlike trading intermediaries, WRD Tools operates a 12,000 m² physical plant verified onsite by Intertek. Every batch of bi-metal hole saws undergoes tooth shear-load testing, Rockwell hardness mapping across the weld boundary, and laser alignment testing to guarantee dynamic concentricity within ±0.05mm. Recognized as a High-Tech Enterprise of Jiangsu Province since 2019, we hold proprietary vacuum thermal-treatment patents that prevent internal cracking and micro-flaking during heavy high-torque cyclic loads.
With over 150 skilled operators and 6 modern production workshops producing more than 90 million bits annually, we provide reliable turnaround for high-volume contracts. Over the past 19 years, our factory has supplied cutting tools to top global brands such as BOSCH, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller. Sourcing with us connects you to genuine Tier-1 factory performance at true FOB wholesale economics.
Critical metallurgical, logistic, and private labeling answers to support commercial bids and distribution planning.