High-Performance Rotary Cutting Solutions
Explore our core certified production items designed to solve critical machining bottlenecks across timber framing, stainless marine refurbishment, structural steel fabrication, and multi-axis 3D contour profiling.




Precision Ball Nose Tooling Engineered for Reliability
A deep technical breakdown of micrograin carbide, blade geometry, and specialized physical vapor deposition (PVD) coatings built to overcome deflection, high runout, and thermal degradation in remote machining hubs.
Sub-Micron Tungsten Matrix
Our ball nose endmills utilize a refined 0.4μm – 0.6μm sub-micrograin carbide matrix fortified with 10% to 12% cobalt binder content. This metallurgical configuration yields a transversal rupture strength (TRS) exceeding 4,000 MPa, preventing catastrophic chipping during aggressive 3D roughing passes.
When running semi-finishing operations on hardened pump volutes or outboard motor propulsion components, our substrate provides extreme thermal dissipation characteristics that protect the cutting edge even when cooling fluid delivery is intermittent.
Optimized Ball Profile & Runout
Fabricated on 5-axis Walter and Rollomatic CNC grinding centers, every ball nose contour is ground to an ultra-tight profile tolerance of ±0.005mm. The apex cutting center is engineered with S-type or helical cross-gashing to eliminate zero-velocity dead spots common in standard mills.
This center-cutting geometry reduces thrust force by 28%, significantly suppressing harmonic chatter across high-aspect-ratio long-reach applications, preserving surface finishes down to Ra 0.2μm in contouring passes.
AlTiSiN & TiSiN Multilayer PVD
To endure the thermal stress of high-feed milling, our tools feature nanocomposite AlTiSiN multi-layer coating, providing an oxidation threshold temperature up to 1,150°C and a micro-surface hardness of ~3,600 HV.
The silicon-doped outer stratum forms a glassy amorphous silicon nitride protective barrier during chip ejection, mitigating chip weld when machining sticky marine-grade 316 stainless, monel shafts, and naval bronze alloys.
Local Application Scenarios in Gizo & Western Province
Gizo stands as the central trade and administrative node of the Solomon Islands' Western Province. In an environment characterized by remote logistics and hyper-saline conditions, tooling failures halt entire operations.
Marine Fleet Overhaul & Prop Re-Profiling
As the transit gateway linking Noro, Kolombangara, and the Shortland Islands, Gizo’s maritime workshops continuously maintain fiberglass fishing skiffs, diesel tugs, and inter-island passenger ferries. Salt spray and electrochemical galvanization rapidly pit drive shafts and propeller blades.
Local workshops deploy our ball nose cutters on 3-axis and 4-axis milling equipment to machine curved blade surfaces, resurface duplex stainless steel rudder sleeves, and true up bronze mechanical seal pockets with zero micro-cracking.
Commercial Hardwood & Veneer Machinery
Western Province is globally recognized for dense tropical timber including Vitex, Kwila, and Rosewood. Sawmill processing plants on nearby Kolombangara rely on Gizo for custom maintenance of hydraulic planer heads, circular blade arbors, and custom moulding dies.
Profiling hardened alloy tool steels (D2, SKD11) used in timber trimming knives requires the superior edge retention and concentricity of our ball nose series to prevent premature flaking under extreme frictional heat.
Public Works, Reef Infrastructure & Power Generation
Coastal stabilization, wharf anchor reconstruction, and Gizo water reservoir upgrades demand on-site structural fabrication. Contractors must frequently modify pump housings, re-tap brine valves, and drill through structural marine piling.
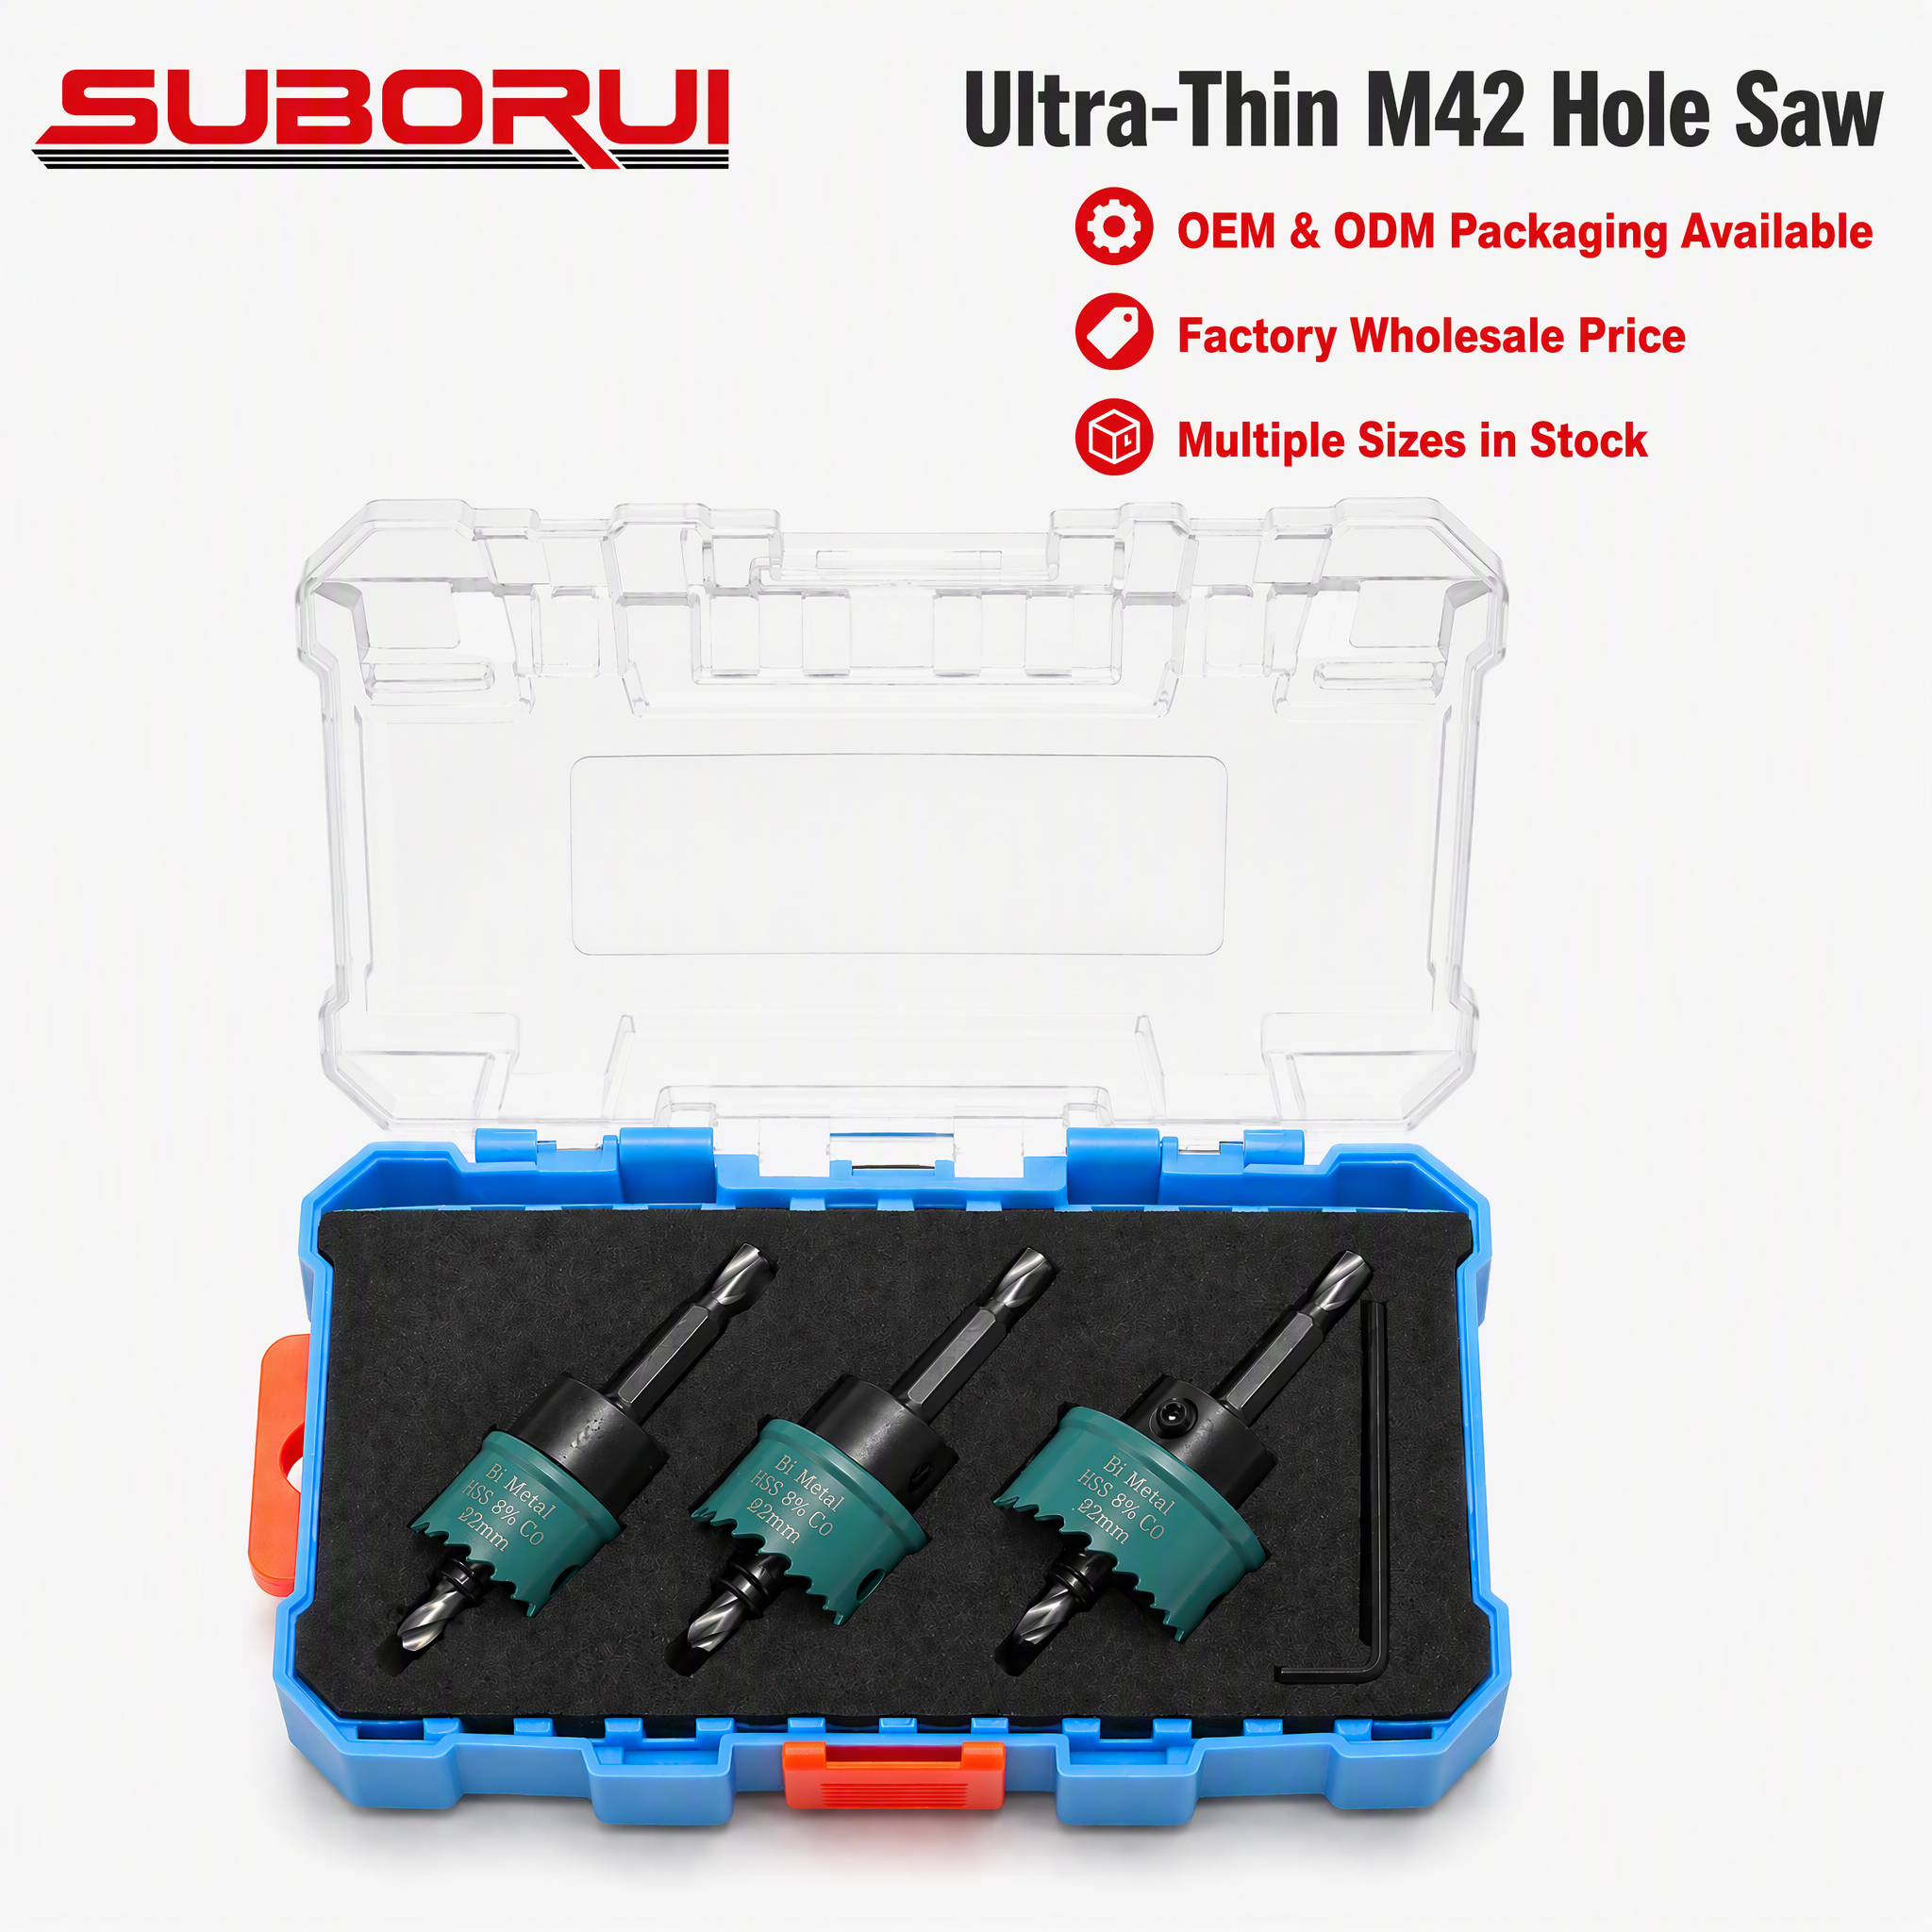
When combined with our M42 bi-metal hole saws and carbide hammer drills, our ball nose endmills allow field engineers to mill counterbored keyways, expansion slots, and manifold blocks directly on location without waiting weeks for offshore spares.
Emerging Procurement & Manufacturing Trends in Western Solomons
A strategic analysis of how localized CNC modernization, supply chain self-reliance, and harsh marine environments are redefining tooling requirements across Melanesia.
Direct-from-Source Procurement
Traditionally, Gizo workshop managers procured cutting tools through third-tier redistribution agents based in Honiara, Brisbane, or Suva, suffering marked price markups and delays of 6 to 10 weeks.
The market trend has sharply pivoted toward factory-direct ordering. By dealing directly with Jiangsu WRD Tools, regional operators bypass intermediary overhead, consolidate shipping via containerized sea freight to Gizo Port, and lock in certified ISO-calibrated quality.
Rise of Compact 3D Milling Centers
With solar-diesel hybrid microgrids stabilizing island industrial power supply, repair yards in Gizo and Noro are upgrading from purely manual knee mills to small-footprint CNC machining centers and digital read-out (DRO) turret mills.
This tech transition demands high-precision ball nose tools capable of both high-RPM aluminum profiling and slow-speed, high-torque steel slotting without tool wandering or premature blade breakdown.
Inventory Buffering Against Cyclone Disruption
Monsoons and cyclone disruptions between November and April frequently sever maritime transit lines across the Western Solomons. Unplanned down-time causes critical economic paralysis when fishing or transport vessels sit idle.
Consequently, procurement managers in Gizo prioritize purchasing high-durability tooling in consolidated kits with standardized shanks (6mm, 8mm, 10mm, 12mm), maximizing tool longevity per dollar spent.
Jiangsu WRD Tools vs. Generic Suppliers
A granular look at why global cutting tool brands and remote industrial operations choose our 12,000 m² facility over general supply brokers and non-inspected workshops.
| Evaluation Parameter | Jiangsu WRD Tools (Factory Manufacturer) | Generic Commodity Resellers / Traders |
|---|---|---|
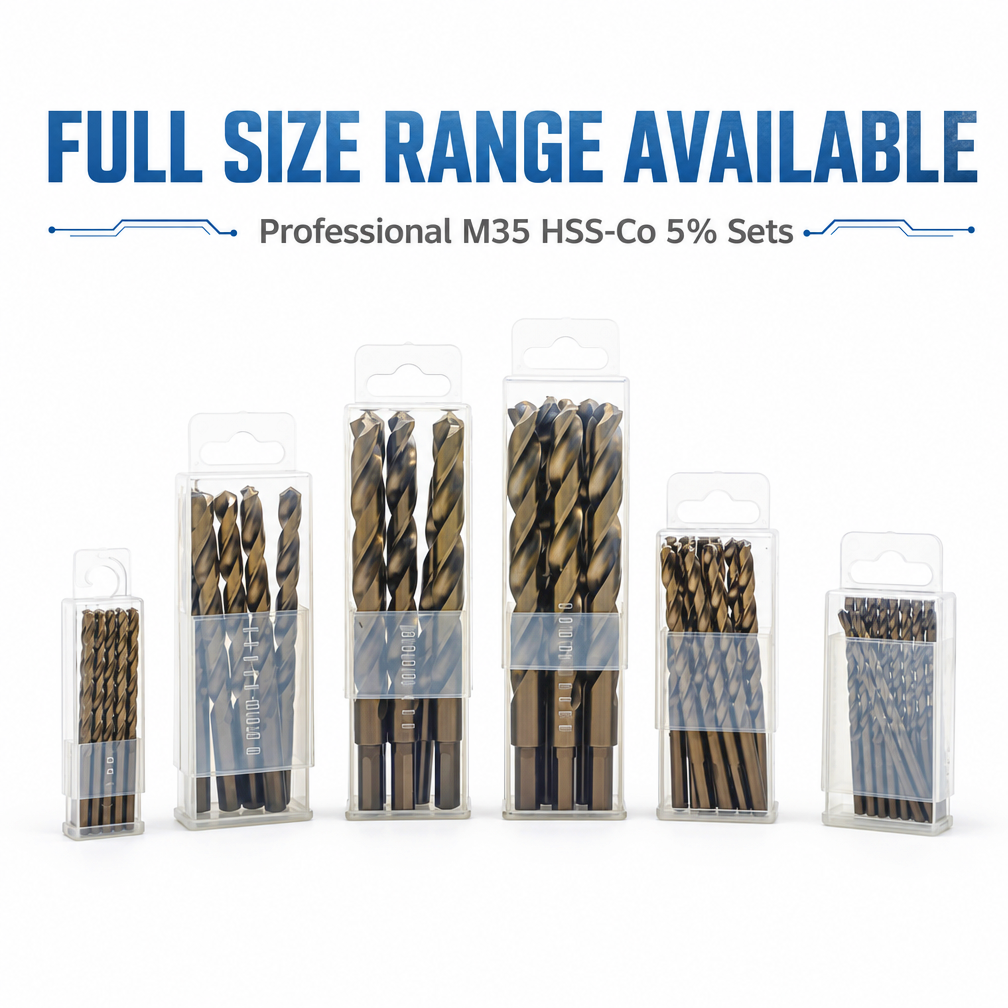
| Raw Material Provenance | Certified virgin tungsten carbide blanks; premium M2, M35 (5% Co), and M42 high-speed steel with complete metallurgical batch traceability. | Mixed scrap recycled carbides, unverified steel compositions, varying grain densities resulting in early snapping. |
| Quality Assurance & Verification | Audited onsite by Intertek; Jiangsu Provincial High-Tech Enterprise accreditation (2019); automated laser micrometer inspection on each run. | No recognized 3rd-party audit; visual-only inspection; non-traceable tolerances and missing certificate documentation. |
| Cutting Geometry & Concentricity | Computer-controlled 5-axis Walter & Rollomatic CNC grinding; runout controlled under 0.005mm; polished flutes for instantaneous chip clearing. | Manual or semi-automatic fluting machines; eccentric tips exceeding 0.025mm causing vibration, chatter, and poor workpiece finish. |
| PVD Coating Formulation | Multi-layer nano-composite AlTiSiN / TiSiN coatings applied via high-vacuum PVD chambers; extreme thermal resistance up to 1,150°C. | Cosmetic gold flash TiN coating under 0.5 microns; burns off during initial roughing cuts on stainless alloys. |
| OEM & Direct Packaging | Full custom laser marking, shank adaptation (straight, Weldon, metric, imperial), private-label blister packs, anti-humidity plastic cases. | Unbranded bulk plastic envelopes; prone to sea-freight atmospheric oxidation and edge micro-chipping during long voyages. |
Frequently Asked Questions for Gizo Buyers
Practical answers addressing logistics, customs documentation, corrosion protection, and material selection tailored for technical teams in the Western Province.
Q1: How does your packaging resist maritime humidity during shipping to Gizo?
Every cutting tool and endmill is coated with an ultra-thin vapor corrosion inhibitor (VCI) oil layer, hermetically sealed in heavy-duty poly tubes or cassette packs, and packed inside desiccated cartons before container consolidation. This prevents oxidation throughout the multi-week sea voyage from Shanghai through Honiara down to Gizo Harbour.
Q2: What endmill flute geometry is ideal for marine stainless (304 / 316)?
We recommend our 4-flute unequal index ball nose endmills paired with AlTiSiN nano coating. The variable helix design disrupts regenerative chatter harmonics, while the sub-micron carbide grade maintains razor edge sharpness without work-hardening the austenitic stainless matrix.
Q3: Can small engineering businesses in Gizo place small-batch trial orders?
Yes. While standard OEM orders begin at 100 to 500 units, we maintain standard catalog inventory for testing purposes. We welcome trial batches of high-demand ball nose sizes (3mm, 6mm, 8mm, 10mm, 12mm) and hole cutter kits to prove tool life on your actual equipment.
Q4: Do you provide full export documentation for Solomon Islands Customs?
We supply complete, customs-compliant commercial documentation including Clean Invoices, Packing Lists with HS codes, Certificates of Origin (CO), Mill Test Certificates, and bill of lading (B/L) tracking under FOB, CIF, or EXW trade incoterms.
Q5: What ball nose diameter tolerance should we specify for rebuilds?
For high-precision shaft bushings and tight tolerance seal grooves, our standard tolerance is ground to h6 diameter tolerance with a sphere radius tolerance of ±0.005mm. Custom profile grinds for turbine or impeller blades can be produced per your CAD DXF drawings.
Q6: How do your ball nose endmills perform on manual knee mills?
While optimized for high-speed CNC spindle operations, our tools feature strengthened core webs that tolerate the minor vibrations and spindle play typical of manual Bridgeport-type and turret mills. This ruggedness protects island workshops utilizing manual machines.
Upgrade Your Machining Precision in Gizo
Connect with our technical engineering team for custom drawings, tool-life comparisons, and direct factory pricing.