
Precision Tooling Catalog
Featured Industrial Cutting & Drilling Equipment
Engineered in compliance with DIN and ISO tolerances, WRD Tools provides an extensive portfolio of magnetic drill broaches, taps, and carbide tooling built to withstand aggressive service conditions.
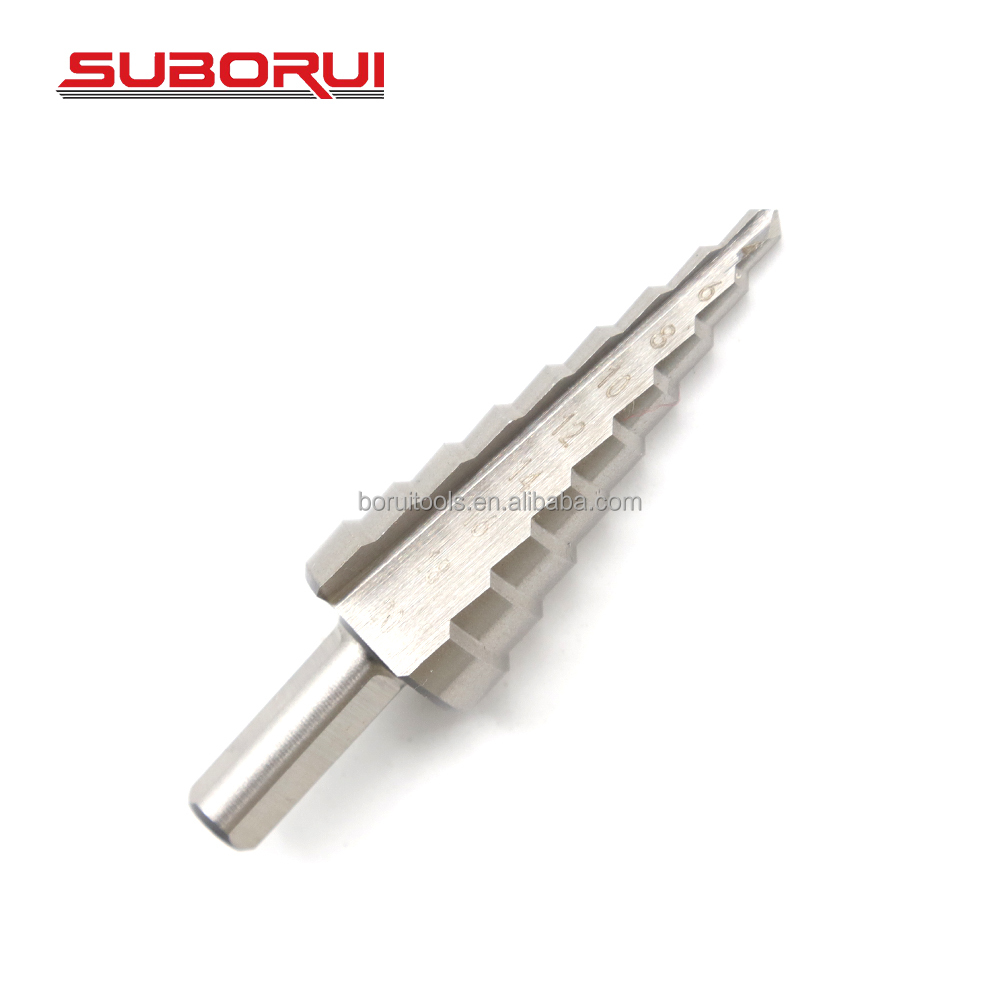
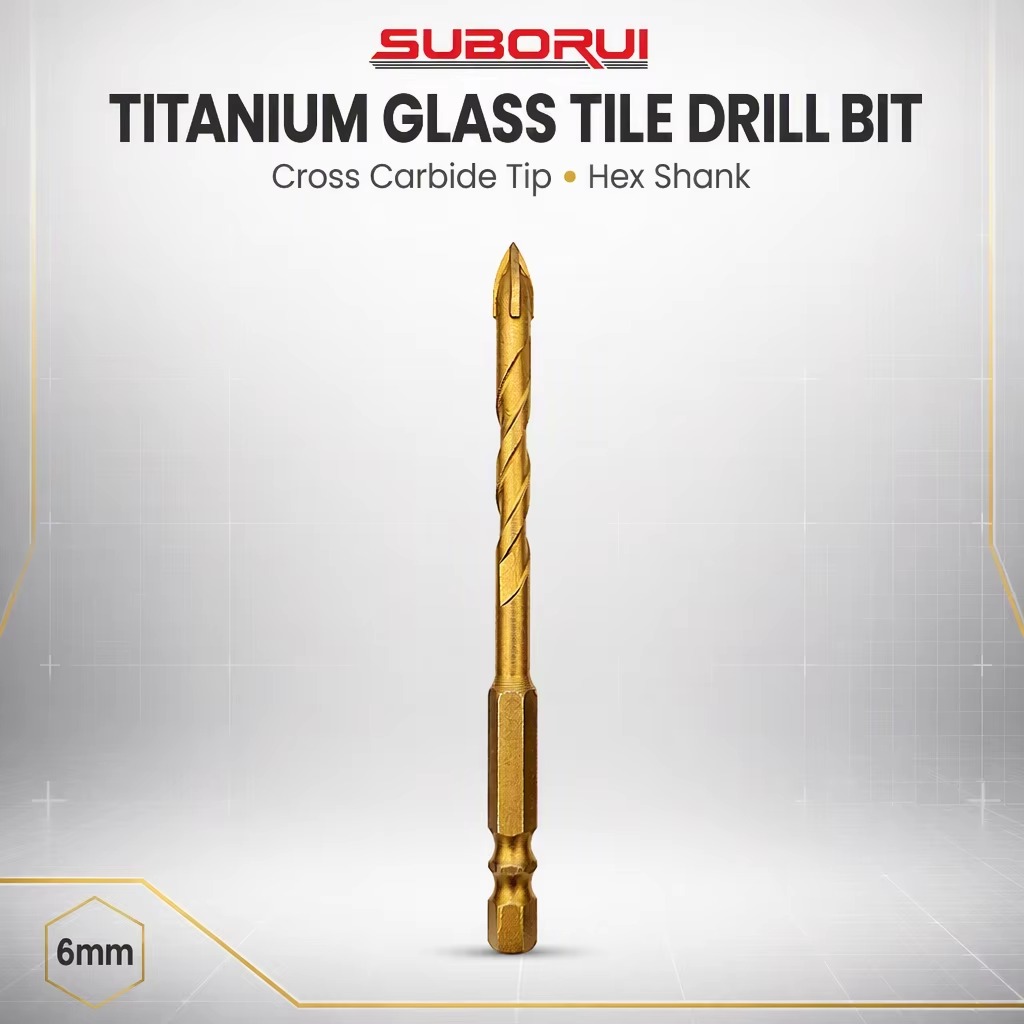


19+
Years Manufacturing History
12,000m²
Intertek Verified Plant
90M+
Annual Tool Output
65-68
HRC Heat-Treated Hardness
Engineering White Paper
Industrial Broaching Engineering & Metallurgy in Narva
A comprehensive analysis of chip load optimization, cutting mechanics, and metallurgy for procurement specialists and site engineers operating across Ida-Virumaa.
In structural metal fabrication and heavy equipment maintenance, holemaking efficiency is fundamentally dictated by cutting dynamics and tool geometry. Traditional twist drills necessitate substantial axial thrust force to pierce materials, generating severe friction and continuous heat buildup at the chisel edge. Conversely, annular broach cutters (also known as core drills or mag-drill cutters) utilize peripheral cutting mechanics. By evacuating only a ring around the circumference and ejecting a solid slug via spring-loaded ejector pins, annular broaches reduce energy expenditure by up to 60%, drastically shorten machine operating cycles, and eliminate thermal structural alterations in high-tensile structural beams.
For industrial operators situated in Narva and the wider Eastern Estonian industrial corridor, structural steels often exhibit elevated alloy contents, demanding high hot-hardness and rigorous abrasive resistance. Tool failure typically traces back to secondary work-hardening from sluggish peripheral speed or premature micro-chipping caused by unbalanced radial runout. WRD Tools employs fully ground CNC spiral flute geometry and salt-bath vacuum heat-treatment to deliver consistent hardness across tooth profiles, whether selecting fully ground High-Speed Steel (HSS M2), 5% Cobalt alloy (HSS-Co M35), or Tungsten Carbide-Tipped (TCT) tooth inserts.
Core Shank Interfaces & Hydraulic Magnetic Alignment
Magnetic drilling rigs utilized in structural assembly rely upon absolute concentricity. A runout variance exceeding 0.04mm causes chatter, rapid tooth breakage, and erratic hole tolerances. WRD Tools manufactures annular broach cutters configured with universal shanks (One-Touch / Nitto compatible), traditional 19.05mm (3/4") Weldon shanks equipped with precision dual locking flats, and Quick-In tool-free adaptors. This ensures complete multi-platform interoperability across Euroboor, BDS Maschinen, Alfra, Fein, and Rotabroach magnetic base systems widely deployed across Estonian fabricators.
| Tool Material Type | Standard Hardness | Maximum Tensile Strength | Recommended Coolant | Primary Narva Application |
|---|---|---|---|---|
| HSS M2 (6542 Standard) | 63 - 65 HRC | Up to 850 N/mm² | Water-soluble emulsion / neat oil | General structural beams, mild steel S235 / S275 framing |
| HSS-Co M35 (Cobalt 5%) | 65 - 67 HRC | Up to 1100 N/mm² | High-pressure bio-synthetic cutting oil | Hardened plate, high-tensile S355, railway track rehabilitation |
| TCT (Carbide Tipped Sandvik Teeth) | Up to 90 HRA | Up to 1400 N/mm² + Hardox | Internal aerosol/micro-spray lubrication | Boiler shell refitting, stainless steel tanks, oil shale piping |
Operational Footprint
Localized Application Scenarios Across Narva & Ida-Virumaa
From power generation maintenance to cross-border logistics infrastructure, core cutting tooling must deliver dependable operational availability under demanding environmental regimes.
Thermal & Biomass Energy Generation
Maintenance outages at power generation stations in Auvere and Narva require precise on-site core drilling into heavy boiler shells, thick heat-exchanger flanges, and high-pressure steam line supports. Tooling must operate reliably in tight spatial orientations without heavy press stands.
Oil Shale & Chemical Processing Facilities
The aggressive corrosive environment and thermal cycles characteristic of processing reactors demand M35 Cobalt and TCT cutters capable of penetrating alloyed stainless steels, nickel-chrome piping, and reinforced mounting brackets without work hardening the host workpiece.
Structural Steelwork & Industrial Parks
Fabricators within the Narva Industrial Park and logistics transit facilities rely on high-volume 18mm to 36mm core broaching through heavy S355 steel I-beams, pre-drilling anchor plates, and completing modular assembly with tight bolt clearances.
Strategic Forecasting
Industrial & Procurement Trends in Eastern Estonia
How the ongoing European green transition, supply chain recalibration, and modular infrastructure investments are shifting tooling requirements in Narva.
The industrial ecosystem in Ida-Virumaa is undergoing historic transformation. Supported by the European Union’s Just Transition Fund (Õiglase Ülemineku Fond), Narva is accelerating its transition from traditional energy extraction toward precision green technology manufacturing, advanced metal fabrication, and sustainable chemical development. This transition carries significant implications for cutting tool selection and vendor supply resilience:
1. Shift Toward High-Performance Structural Alloys: Modern industrial construction across the Baltic states is replacing standard S235 carbon steel with fine-grain, high-yield structural steel alloys such as S355J2+N and S460. These substrates yield higher tensile resistance, demanding cutters with optimized rake angles and friction-reducing coatings (TiAlN / AlCrN) that suppress heat dissipation into the drill spindle during dry or mist-cooled field operations.
2. Compressed Maintenance Shutdown Windows: With facilities optimizing output, scheduled maintenance outages for energy systems and infrastructure require contractors to complete holemaking cycles rapidly. Tool failures or inconsistent life-cycles translate into costly delays. Estonian contractors increasingly source verified OEM manufacturers who guarantee metallurgical batch uniformity, full traceability, and custom diameter configurations on demand.
3. Decoupling from Unreliable Regional Intermediaries: Sourcing managers in Narva and Tallinn are bypassing third-tier European re-branders to partner directly with auditable primary factories. By securing direct OEM supply lines with Jiangsu WRD Tools, enterprise buyers unlock competitive landed cost structures, customize shank geometries to existing machinery fleets, and establish buffer inventory models that insulate projects from global transport shocks.
Procurement Knowledge Base
Frequently Asked Questions by Narva Buyers
Critical technical, commercial, and logistics information tailored for engineering estimators and supply chain managers.
What are the key technical differences when choosing between HSS M2 and TCT annular cutters for Baltic climate projects? +
HSS M2 broach cutters feature an integrated one-piece construction with superior structural elasticity, making them exceptionally forgiving against vibration, lateral deflections, or manual feed variations common in outdoor winter site conditions. They can be resharpened up to 10-15 times. TCT (Tungsten Carbide-Tipped) cutters feature micro-grain carbide teeth brazed to an alloy steel body, offering blistering cutting speeds and the ability to process extremely hard substrates (up to 40-50 HRC and abrasive stainless steels) without losing cutting edges. However, TCT cutters require rigid magnetic bases to prevent tooth fracture caused by vibration.
Can WRD Tools customize shank types to fit our existing Fein and Nitto magnetic drill presses? +
Yes. We manufacture standard 19.05mm (3/4") Weldon shanks with dual grub-screw flats, 31.75mm (1-1/4") Weldon shanks for large-diameter broaching, Universal one-touch shanks (compatible with both Weldon and Nitto quick-arbor locks), and Fein Quick-In tool-less shanks. Custom shank dimensions and lengths can be machined according to exact client technical drawings.
What is the standard order lead time and logistics procedure for freight delivering to Narva, Estonia? +
For standard catalog items, production typically completes within 15–25 business days depending on volume. Shipments are consolidated and dispatched via ocean container directly to the Port of Muuga (Tallinn) or the Port of Sillamäe, followed by short-haul truck freight to Narva industrial zones. For urgent maintenance shutdowns or sampling, we offer prioritized air courier transit (DHL/FedEx) arriving in Estonia within 4–7 business days.
How does WRD Tools manage quality assurance and metallurgical integrity? +
Every batch of incoming high-speed steel bar stock undergoes spectroscopic chemical assay analysis before entering production. Our entire facility in Danyang is verified on-site by Intertek. Cutting tools pass through five automated stages: blank turning, CNC flute grinding, salt-bath vacuum heat-treatment, precision optical profile projection, and automated runout testing. Hardness parameters (HRC) and concentricity tolerances are rigorously certified before final packaging.
Do you offer private-label branding, customized packaging, and specialized coating solutions? +
Yes. As an OEM/ODM partner to international cutting-tool brands, we provide complete laser-etched private branding (including your part numbers, logos, and metric dimensions), customized heavy-duty plastic cases, blister packs, and multi-piece industrial broach kits. We also apply physical vapor deposition (PVD) surface coatings including TiN (Titanium Nitride), TiAlN (Titanium Aluminum Nitride), and multi-layer composites to maximize tool longevity in severe applications.
Enterprise Strengths
Why Global Tool Brands Partner with WRD Tools
Founded in March 2007 in Danyang — the global epicenter of holemaking tool manufacturing — Jiangsu WRD Tools Co., Ltd. combines advanced manufacturing capacity with rigorous quality control.
Intertek Onsite Verification
Our complete 12,000 square meter plant, dedicated production lines, and QA/QC management framework have been rigorously verified and accredited onsite by Intertek Group.
Substantial Production Volume
With more than 150 skilled technicians and advanced automated CNC machinery, we produce over 90 million cutting units each year, ensuring continuous supply stability for large distribution networks.
Jiangsu High-Tech Enterprise
Recognized as an official High-Tech Enterprise of Jiangsu Province since 2019, our in-house engineering and R&D departments hold continuous patents for tool fluting and heat treatment optimization.
Proven Global Tier-1 Pedigree
WRD Tools has successfully manufactured drill bits and accessories for leading worldwide tool brands including Bosch, Milwaukee, DeWalt, Irwin, Makita, Dexter, KWB, Wolfcraft, Truper, and Heller.
End-to-End Vertical Integration
From initial steel bar cutting and rough turning to proprietary heat treatment, CNC point grinding, coating, and individual blister packaging, zero critical processes are outsourced.
Export Presence in 20+ Countries
Our export infrastructure seamlessly serves industrial partners across Germany, Switzerland, Sweden, the United States, and Northern Europe, guaranteeing smooth customs and technical compliance.
German Standard Tolerances
Full Material Batch Certificates
Custom Geometry Engineering
Intertek Audited Facility
Ready to Elevate Your Holemaking Operations in Narva?
Connect directly with our export engineering department to receive technical datasheets, customized OEM quotation schedules, or arrange comprehensive factory sample batches.
Contact Us