Featured Industrial Cutting Solutions
Direct-from-factory catalog engineered for demanding stone masonry, structural steel fabrication, high-speed CNC milling, and precision metal processing. Built to exacting DIN standards with comprehensive batch traceability.




Structural Anatomy of Industrial Turbo Diamond Blades
In modern high-speed civil engineering, masonry, and refractory processing, the turbo diamond blade represents the optimal balance between high linear cutting speed and edge chipping prevention. Unlike conventional continuous rim blades that encounter heat accumulation during dry cuts, or segmented blades that induce micro-fracturing along porcelain and granite veneers, turbo geometry incorporates a corrugated, serrated rim structure.
This corrugated periphery performs three distinct thermodynamic functions: First, the continuous serrations generate an aerodynamic localized vortex that ejects pulverized silica dust and swarf out of the kerf. Second, the alternate contact ridges significantly minimize surface friction against the matrix core, dropping operating temperatures by 22% to 35%. Third, it reduces machine amp-draw by up to 18%, conserving motor life across handheld angle grinders and bridge saws alike.
Global Procurement & Supply Chain Trends
Procurement directors are shifting focus from pure unit acquisition cost to total cost of ownership (TCO), regulatory compliance, and customized OEM supply agility. Here is how tier-1 buyers are adjusting their contracts.
EN13236 Safety Verification Dominance
Importers across the European Union and North America now demand documented adherence to EN13236 safety standards for superabrasives. Products must pass rigorous 100% segment torque tests and 1.5x overspeed burst testing. Factories lacking automated tension-testing benches are systematically disqualified by retail purchasing groups.
Hot-Press Sintering vs. Laser Welding
While cold-press sintered blades satisfy price-sensitive consumer shelves, professional tool distributors increasingly specify automated laser-welded diamond segments for dry-cut brick and reinforced concrete applications. Laser fusion penetrates segment roots without solder melt lines, eliminating segment drop-off hazards.
Direct-to-Factory OEM Cluster Integration
Global distributors are migrating away from coastal trading firms, anchoring long-term vendor agreements directly with manufacturing plants centered in Danyang's tool manufacturing corridor. Direct collaboration eliminates 12–18% in distribution markup while shortening prototype turnaround from months to under 14 days.
Engineered Titanium-Coated Superabrasives
Next-generation diamond procurement heavily features titanium-coated diamond grit (Ti-coat). The thin titanium carbo-nitride barrier layer enhances physical retention inside the bronze-cobalt matrix, preventing diamond crystals from pulling out before complete micro-cleaving wear is achieved, increasing product lifespan by 40%.
Decarbonized Circular Packaging
Tier-1 retailers are phasing out non-recyclable PVC double-blisters in favor of FSC-certified biodegradable paperboard, recyclable tin storage cases, or reusable EVA foam-lined toolboxes. OEM factories offering turnkey automated sustainable packaging solutions hold a decisive margin and shelf-space advantage.
Technological Evolution of Diamond Blades & High-Speed Tooling
The manufacturing landscape for rotary diamond blades and metal cutting tools is transitioning from craft-based powder pressing to computer-controlled metallurgic precision. Three structural evolutions characterize modern high-yield tooling:
Why Global Hardware Brands Choose Jiangsu WRD Tools
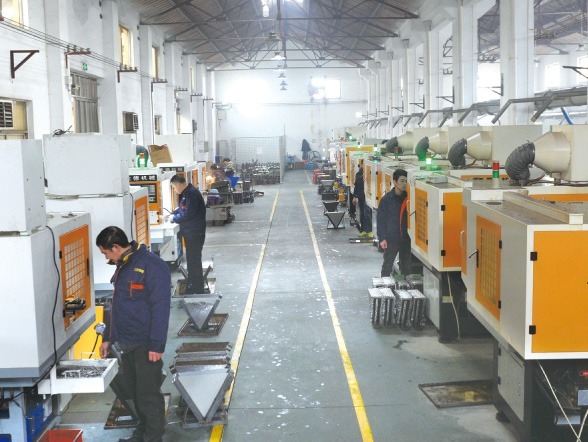
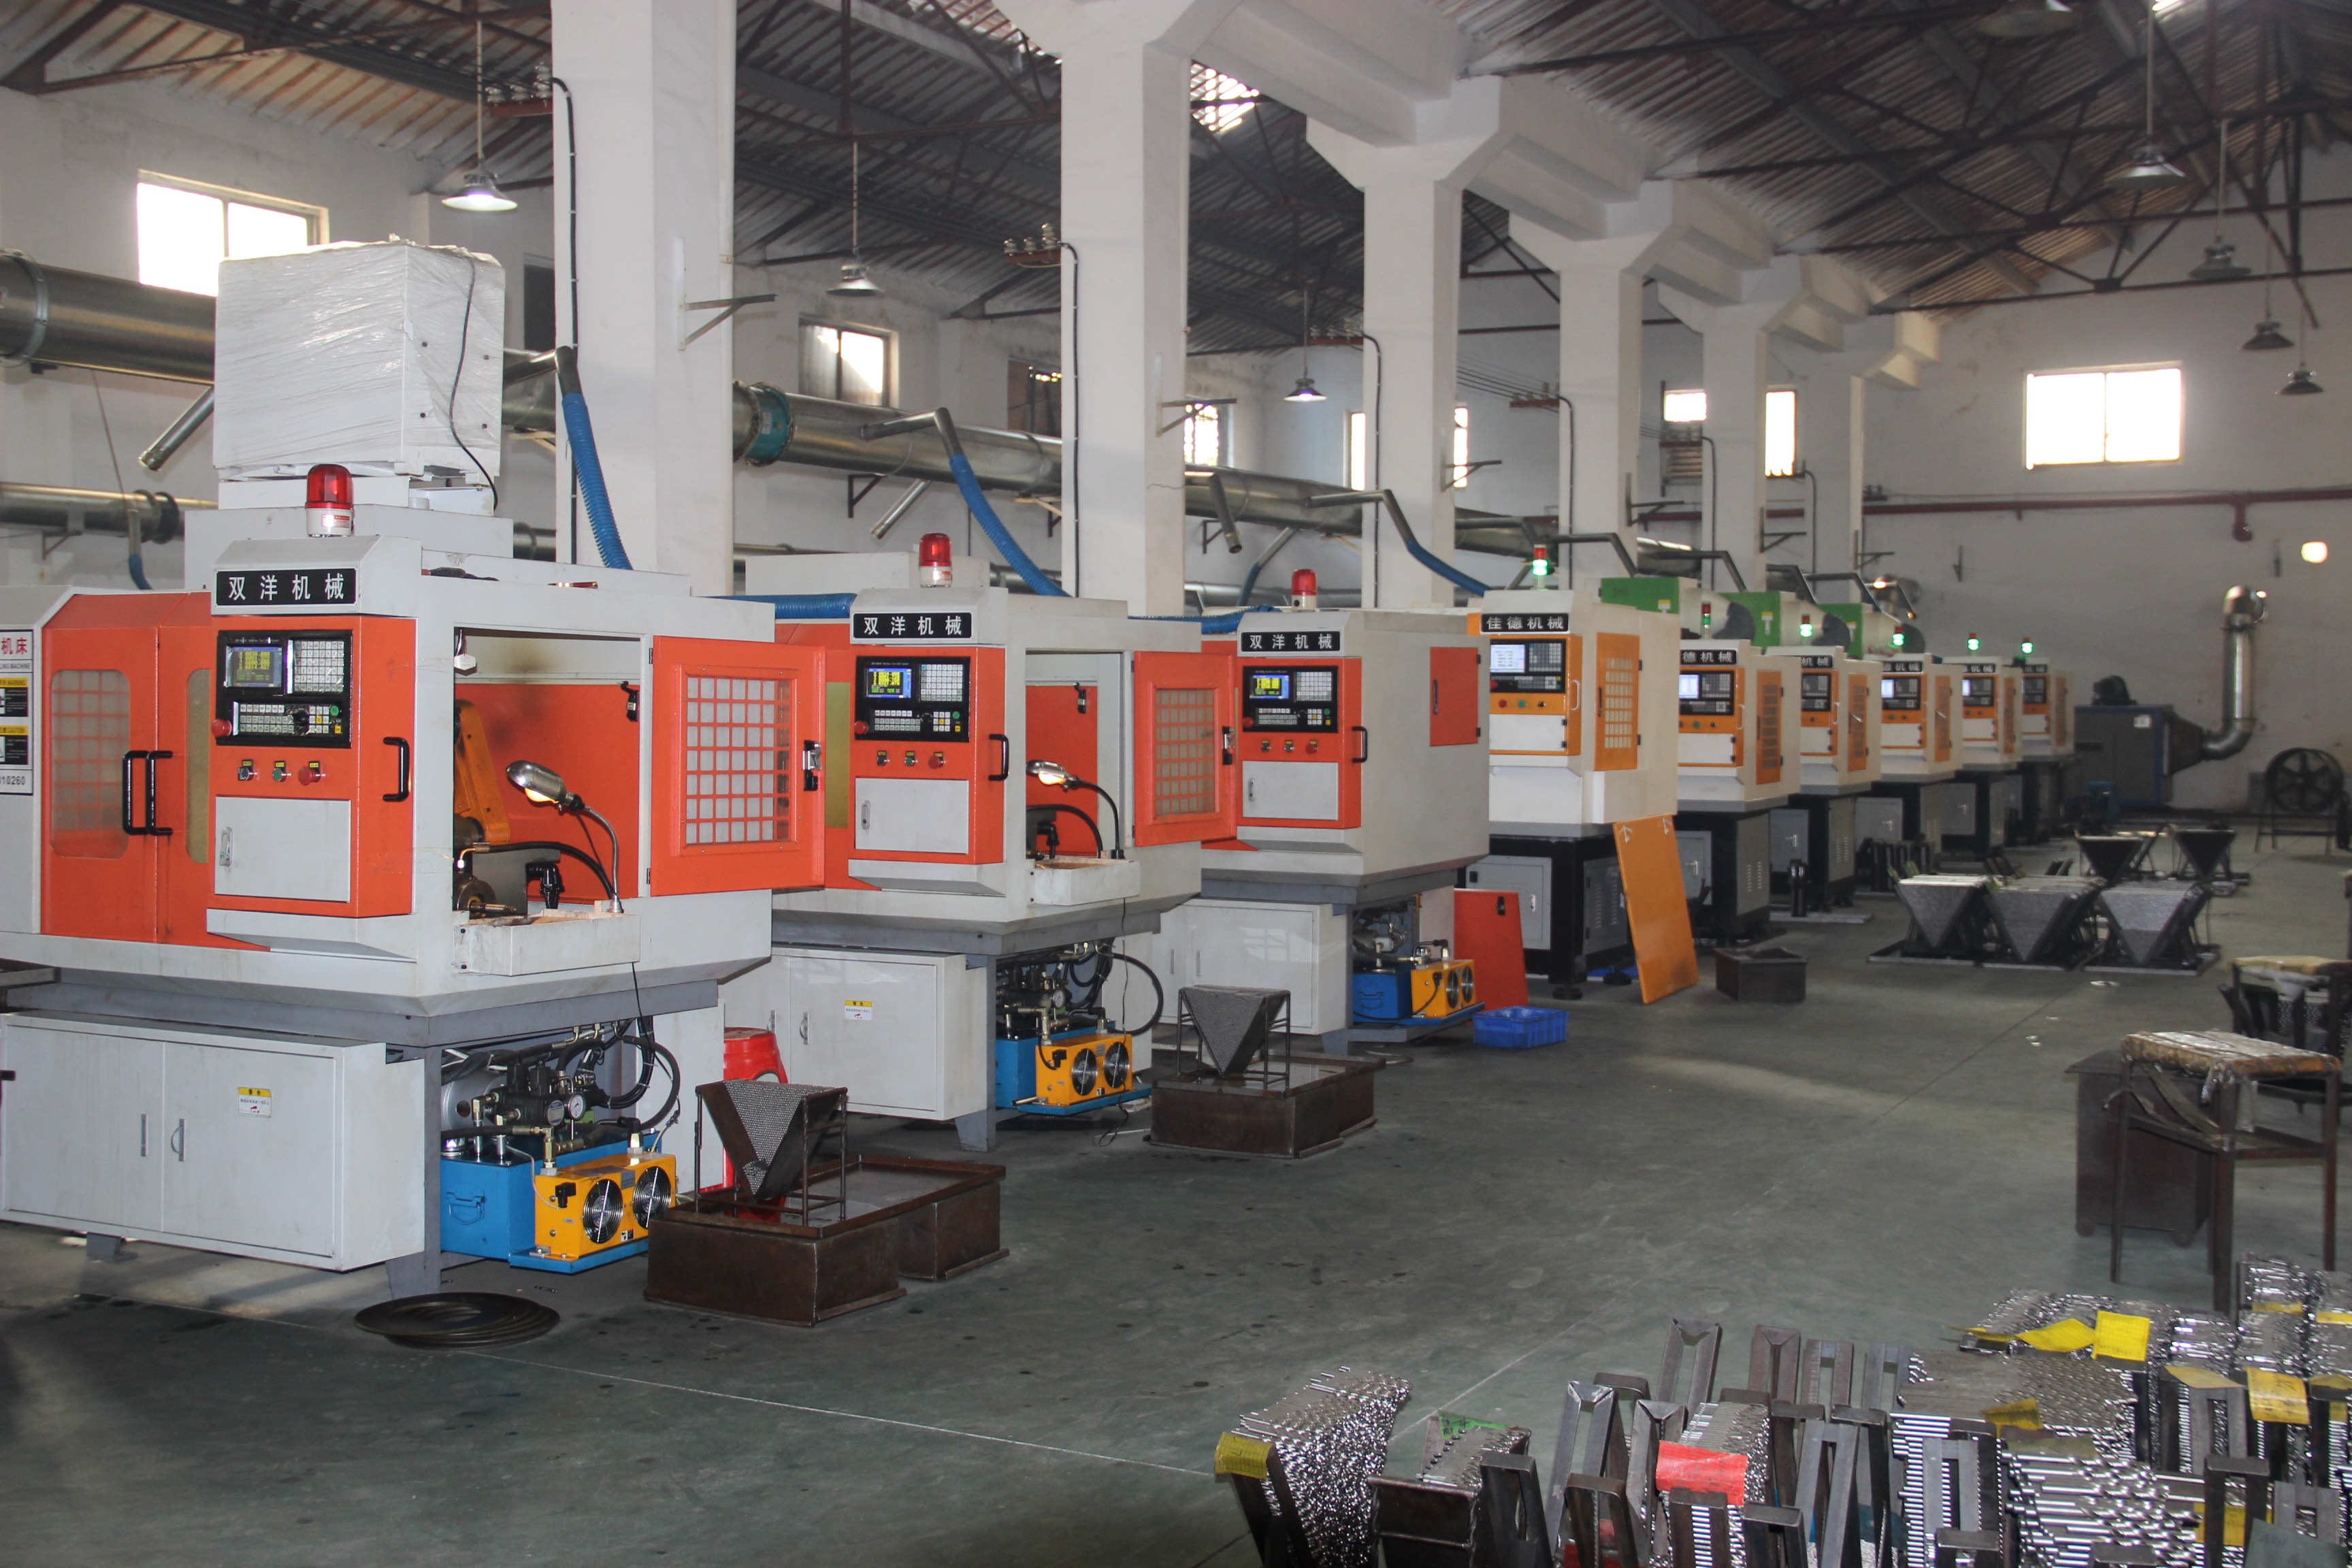
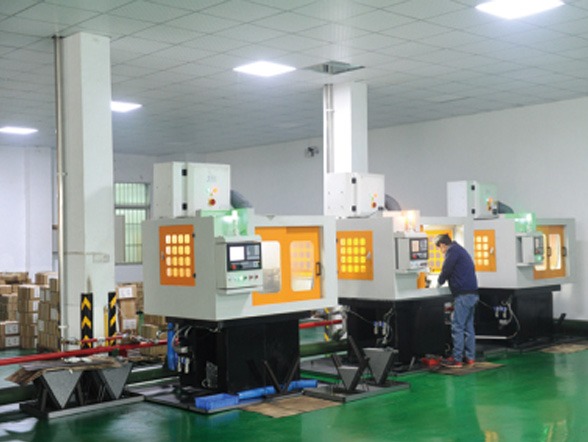
Founded in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. (operating the SUBORUI brand) is situated in Danyang, Jiangsu — China's epicenter of precision hardware cutting tools. Operating across a modern 12,000 square meter production complex with over 150 skilled mechanical technicians and QA specialists, we deliver an annual manufacturing volume exceeding 90 million units.
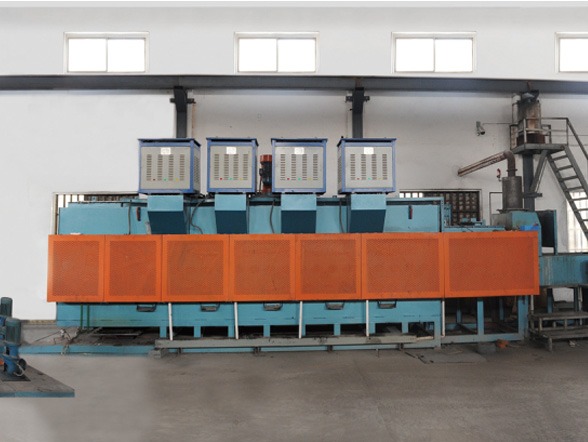
Our comprehensive facilities eliminate subcontractor reliance: from high-precision automated bar slicing, controlled atmosphere salt-bath and vacuum heat treatment furnaces, to CNC five-axis flute grinding, automated laser welding, dynamic balancing stations, and automated packing centers. We operate with verifiable audit status and proven export partnerships.
- Intertek Onsite Audited: Facilities, quality control regimes, and manufacturing capabilities fully certified onsite by Intertek.
- High-Tech Enterprise Certification: Recognized as an official High-Tech Enterprise of Jiangsu Province since 2019 with extensive proprietary tool geometry patents.
- Tier-1 OEM Track Record: Proven OEM manufacturing partner delivering tool programs for world-renowned brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Dexter, Wolfcraft, Truper, and Heller.
- Turnkey Private Labeling: Laser marking on core plates and shanks, custom color anodizing/powder coatings, bespoke blister cards, molded blow-cases, and retail cartons.
Frequently Asked Sourcing Questions
Direct technical answers addressing arbor specs, bond hardness selection, custom OEM manufacturing lead times, and regulatory compliance.
Partner with a Proven Direct OEM Diamond Tooling Manufacturer
Request factory-direct FOB price matrices, custom private-label branding mockups, or metallurgical test samples. Our technical sales engineering team provides full quotes and design verifications within 24 business hours.
Inquire Now