Precision Roughing Cutters & Multi-Material Tooling
Manufactured under rigorous thermal, substrate, and dimensional validation controls. Select your application below or connect directly for custom OEM flute and coating development.






High Material Removal Rates: The Physics of Custom Roughing Cutters
Modern CNC milling workflows demand unprecedented chip clearing rates without introducing catastrophic harmonic chatter or thermal cracking. Here is our breakdown of industrial roughing profiles.
Sinusoidal Knuckle Geometry
Unlike standard square end mills, custom roughing end mills integrate scalloped or knuckle thread-form profiles along their cutting relief edges. This divides uniform chip ribbons into manageable micro-segments, reducing cutting forces by up to 40% and damping chatter across long reach set-ups.
M42 Cobalt & Submicron Carbide
For high-shock structural steel or gummy 304/316 austenitic stainless milling, WRD offers HSS-Co 8% (M42) maintaining high red hardness alongside fine-grain tungsten carbide (0.6µm) ground on 5-axis CNC machines to achieve edge consistency within ±0.005mm.
Variable Helix & Pitch Suppression
By engineering flutes with asymmetrical 35°/38° variable helix configurations, our tooling disrupts harmonic resonant frequencies inside high-speed machining centers. This enables deeper axial slotting depths (up to 1.5×D) at aggressive table feed rates.
Future Procurement Trends in Industrial Milling (2025–2030)
A data-informed outlook on how international procurement officers, contract machine shops, and cutting tool importers are optimizing inventory spend and machining reliability.
Multi-Layer Nanocomposite PVD Coatings
Procurement teams are moving beyond classic TiN/TiCN coatings toward AlTiN, AlCrN, and Silicon-doped nanocomposite matrices. These surfaces form protective aluminum/chromium oxide micro-layers capable of withstanding dry and MQL (Minimum Quantity Lubrication) cutting heat up to 1,100°C.
Total Cost of Ownership (TCO) Prioritization
Top aerospace and heavy automotive subcontractors have ceased purchasing roughers based purely on unit cost. The shift centers on "Cost Per Cubic Inch Removed." High-durability roughers that clear massive chip loads without breaking spindle bearings yield net machining savings surpassing 22%.
Nearshore-Optimized OEM Customization
Distributors in North America and Western Europe are consolidating vendor tiers by seeking integrated OEM factories able to manufacture custom knuckle geometries, imperial Weldon flats, and proprietary laser-etched barcodes under private-label brands straight from factory doors.
Jiangsu WRD Tools: Factory Precision Since 2007
Located in the heart of China's cutting tool manufacturing capital in Danyang, Jiangsu WRD Tools Co., Ltd. represents an Intertek-verified, integrated manufacturing infrastructure dedicated to industrial-grade tooling.
With an audited 12,000 square meter modern facility, an annual output exceeding 90 million tool units, and a workforce of 150+ technicians, we supply globally reputed industrial tool brands including Bosch, Milwaukee, DeWalt, Makita, Irwin, and Wolfcraft. Our facility is recognized as a High-Tech Enterprise of Jiangsu Province, ensuring that raw material metallurgy, vacuum salt-bath hardening, precision 5-axis flute relief grinding, and optical laser inspections are rigorously contained inside our controlled facility walls.
| Parameter / Feature | Standard Sourcing Offering | WRD Tools OEM Factory Standard |
|---|---|---|
| Base Materials | Commercial HSS 4241 / Reclaimed Carbide | Certified M2 (6542), M35 Cobalt (5%), M42 (8%), Premium Micrograin Tungsten |
| Flute Concentricity & Runout | < 0.020 mm | Strict ≤ 0.005 mm through automated laser-guided micrometer validation |
| Heat Treatment Protocols | Standard batch annealing | Multi-stage computer vacuum quench + triple temper (Target 64–68 HRC) |
| Third-Party Factory Audit | Self-declared or none | Intertek Onsite Audited; High-Tech Enterprise Certificate since 2019 |
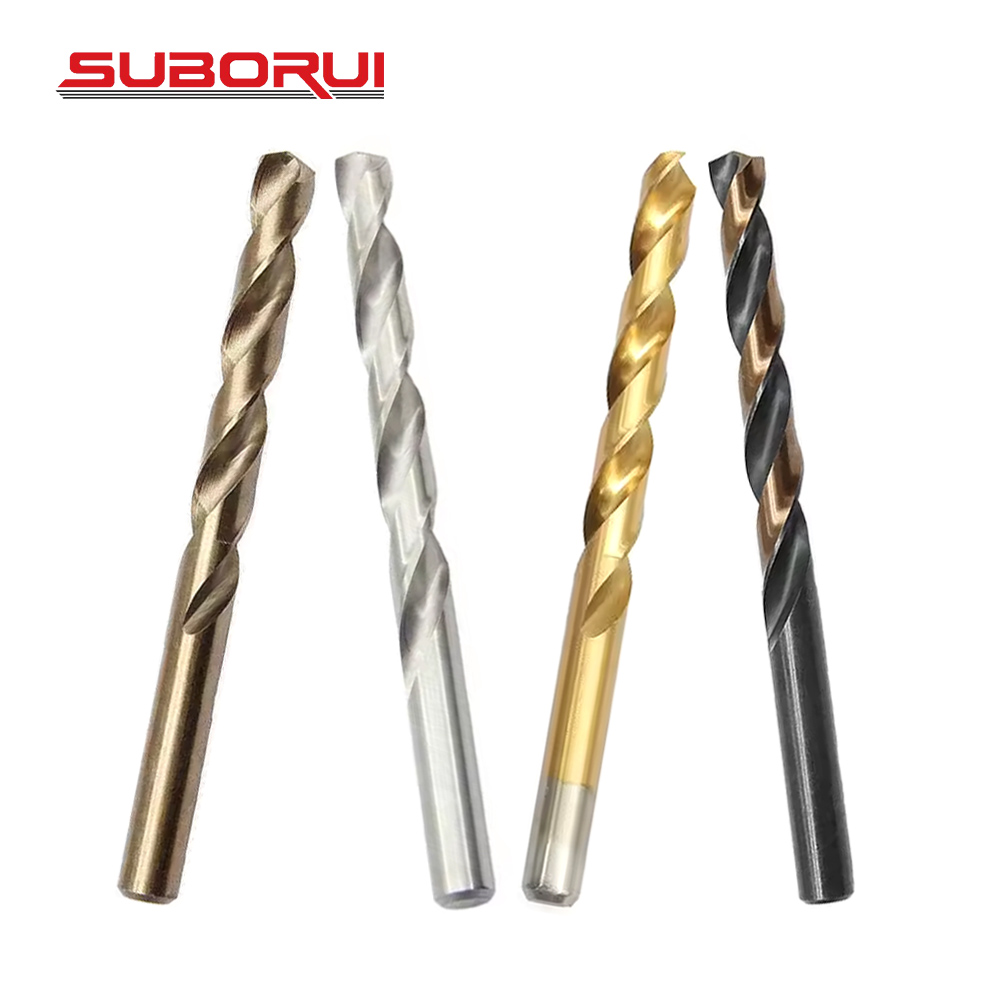
| Packaging & Branding Customization | Generic white box | Laser shank marking, CNC colored coatings, custom cases, blister packs, barcoding |
Frequently Asked Questions on Roughing Cutters & Sourcing
Essential technical and logistical answers prepared directly by our engineering and international export divisions.
What is the technical operational difference between Coarse Pitch and Fine Pitch roughing end mills?
Coarse pitch roughing end mills feature larger scalloped teeth and deeper flute troughs, making them the superior choice for aggressive material clearance in soft-to-medium steels, aluminum, and cast irons where chip evacuation volume is paramount. Fine pitch roughing end mills distribute cutting loads over a larger number of cutting crests, resulting in lower load per tooth, reduced tool deflection, and superior heat handling in hardened alloy steels, titanium, and nickel superalloys.
How does M42 8% Cobalt compare to Solid Carbide in roughing operations?
Solid carbide offers exceptional tool rigidity and can withstand cutting speeds 3x faster than HSS-Co in stable, highly rigid CNC setups with minimal runout. However, M42 Cobalt remains the premier cost-effective material for interrupted cuts, deep cavities, unstable workholding, or older machine tools where carbide would chip or fracture due to lateral vibration and structural shock.
Can WRD manufacture non-standard shank types and extended reaches?
Yes. As an OEM/ODM direct factory, we manufacture custom shank profiles including Weldon DIN 1835B, Whistle Notch DIN 1835E, Morse Taper, and straight cylindrical shanks. In addition, necked-down reliefs, overall lengths up to 300mm, and chipbreaker spacing can be engineered per client blueprints or CAD models.
What are the Factory Minimum Order Quantities (MOQ) and lead times for OEM orders?
Standard trial orders for stocked roughing geometries start at 50 to 100 units per specification. Custom OEM configurations (unique shank geometries, proprietary coatings, or custom packaging sets) typically require an MOQ of 200–500 pieces depending on diameter. Production turnaround averages 20–35 days from blueprint and material sign-off.
How is tool quality assured prior to sea or air export shipments?
Every production batch passes strict inspection gates: spectrometry check on raw round bars, micro-Vickers hardness profiling, dimensional testing on Walter CNC optical measurement systems, and batch milling performance testing. Full Material Test Reports (MTR) and inspection certificates accompany all export shipments.
Connect with Our Engineering & Export Division
Request an instant competitive wholesale quotation, discuss your custom OEM roughing geometry blueprints, or request samples verified by our Intertek-certified quality team.
Contact Us