Engineered CNC Cutting, Milling & Rotary Tooling Series
Verified DIN/ISO compliant manufacturing batches ready for private-label stamping, tailored coatings, and bulk container export.




Technical Authority: Selecting the Right Substrates and Flute Geometries for CNC Routing
In modern high-speed CNC routing operations, tool life, dimensional repeatability, and surface Ra finishes are directly governed by the synergy between substrate micro-grain composition, edge micro-geometry, and dynamic flute balance. As a verified custom OEM CNC router bit supplier and direct exporter, our manufacturing protocols are anchored in strict DIN, ISO, and ANSI tooling metrics. Whether specifying solid tungsten carbide (VHM), Cobalt-infused High-Speed Steels (M35 Co5%, M42 Co8%), or Tungsten Carbide Tipped (TCT) assemblies, engineering procurement teams must evaluate cutting forces, heat dissipation regimes, and chip evacuation velocities.
Substrate Metallurgical Breakdown for Industrial Sourcing
Choosing the correct base alloy determines wear resistance under high rotational RPMs (18,000–30,000 RPM) and heavy chip load parameters. Below is the operational matrix utilized across our automated grinding workshops in Danyang:
| Substrate Material | Hardness (HRC / HV) | Grain Size / Matrix | Thermal Threshold | Optimal CNC Sourcing Applications |
|---|---|---|---|---|
| Solid Micrograin Carbide (UF-WC) | 91.5 - 93.0 HRA (1600-1800 HV) | 0.4 μm - 0.6 μm (10-12% Cobalt) | 850°C - 1000°C | High-speed nested sheet routing, composite phenolic boards, acrylics, and structural aluminum extrusion profiling. |
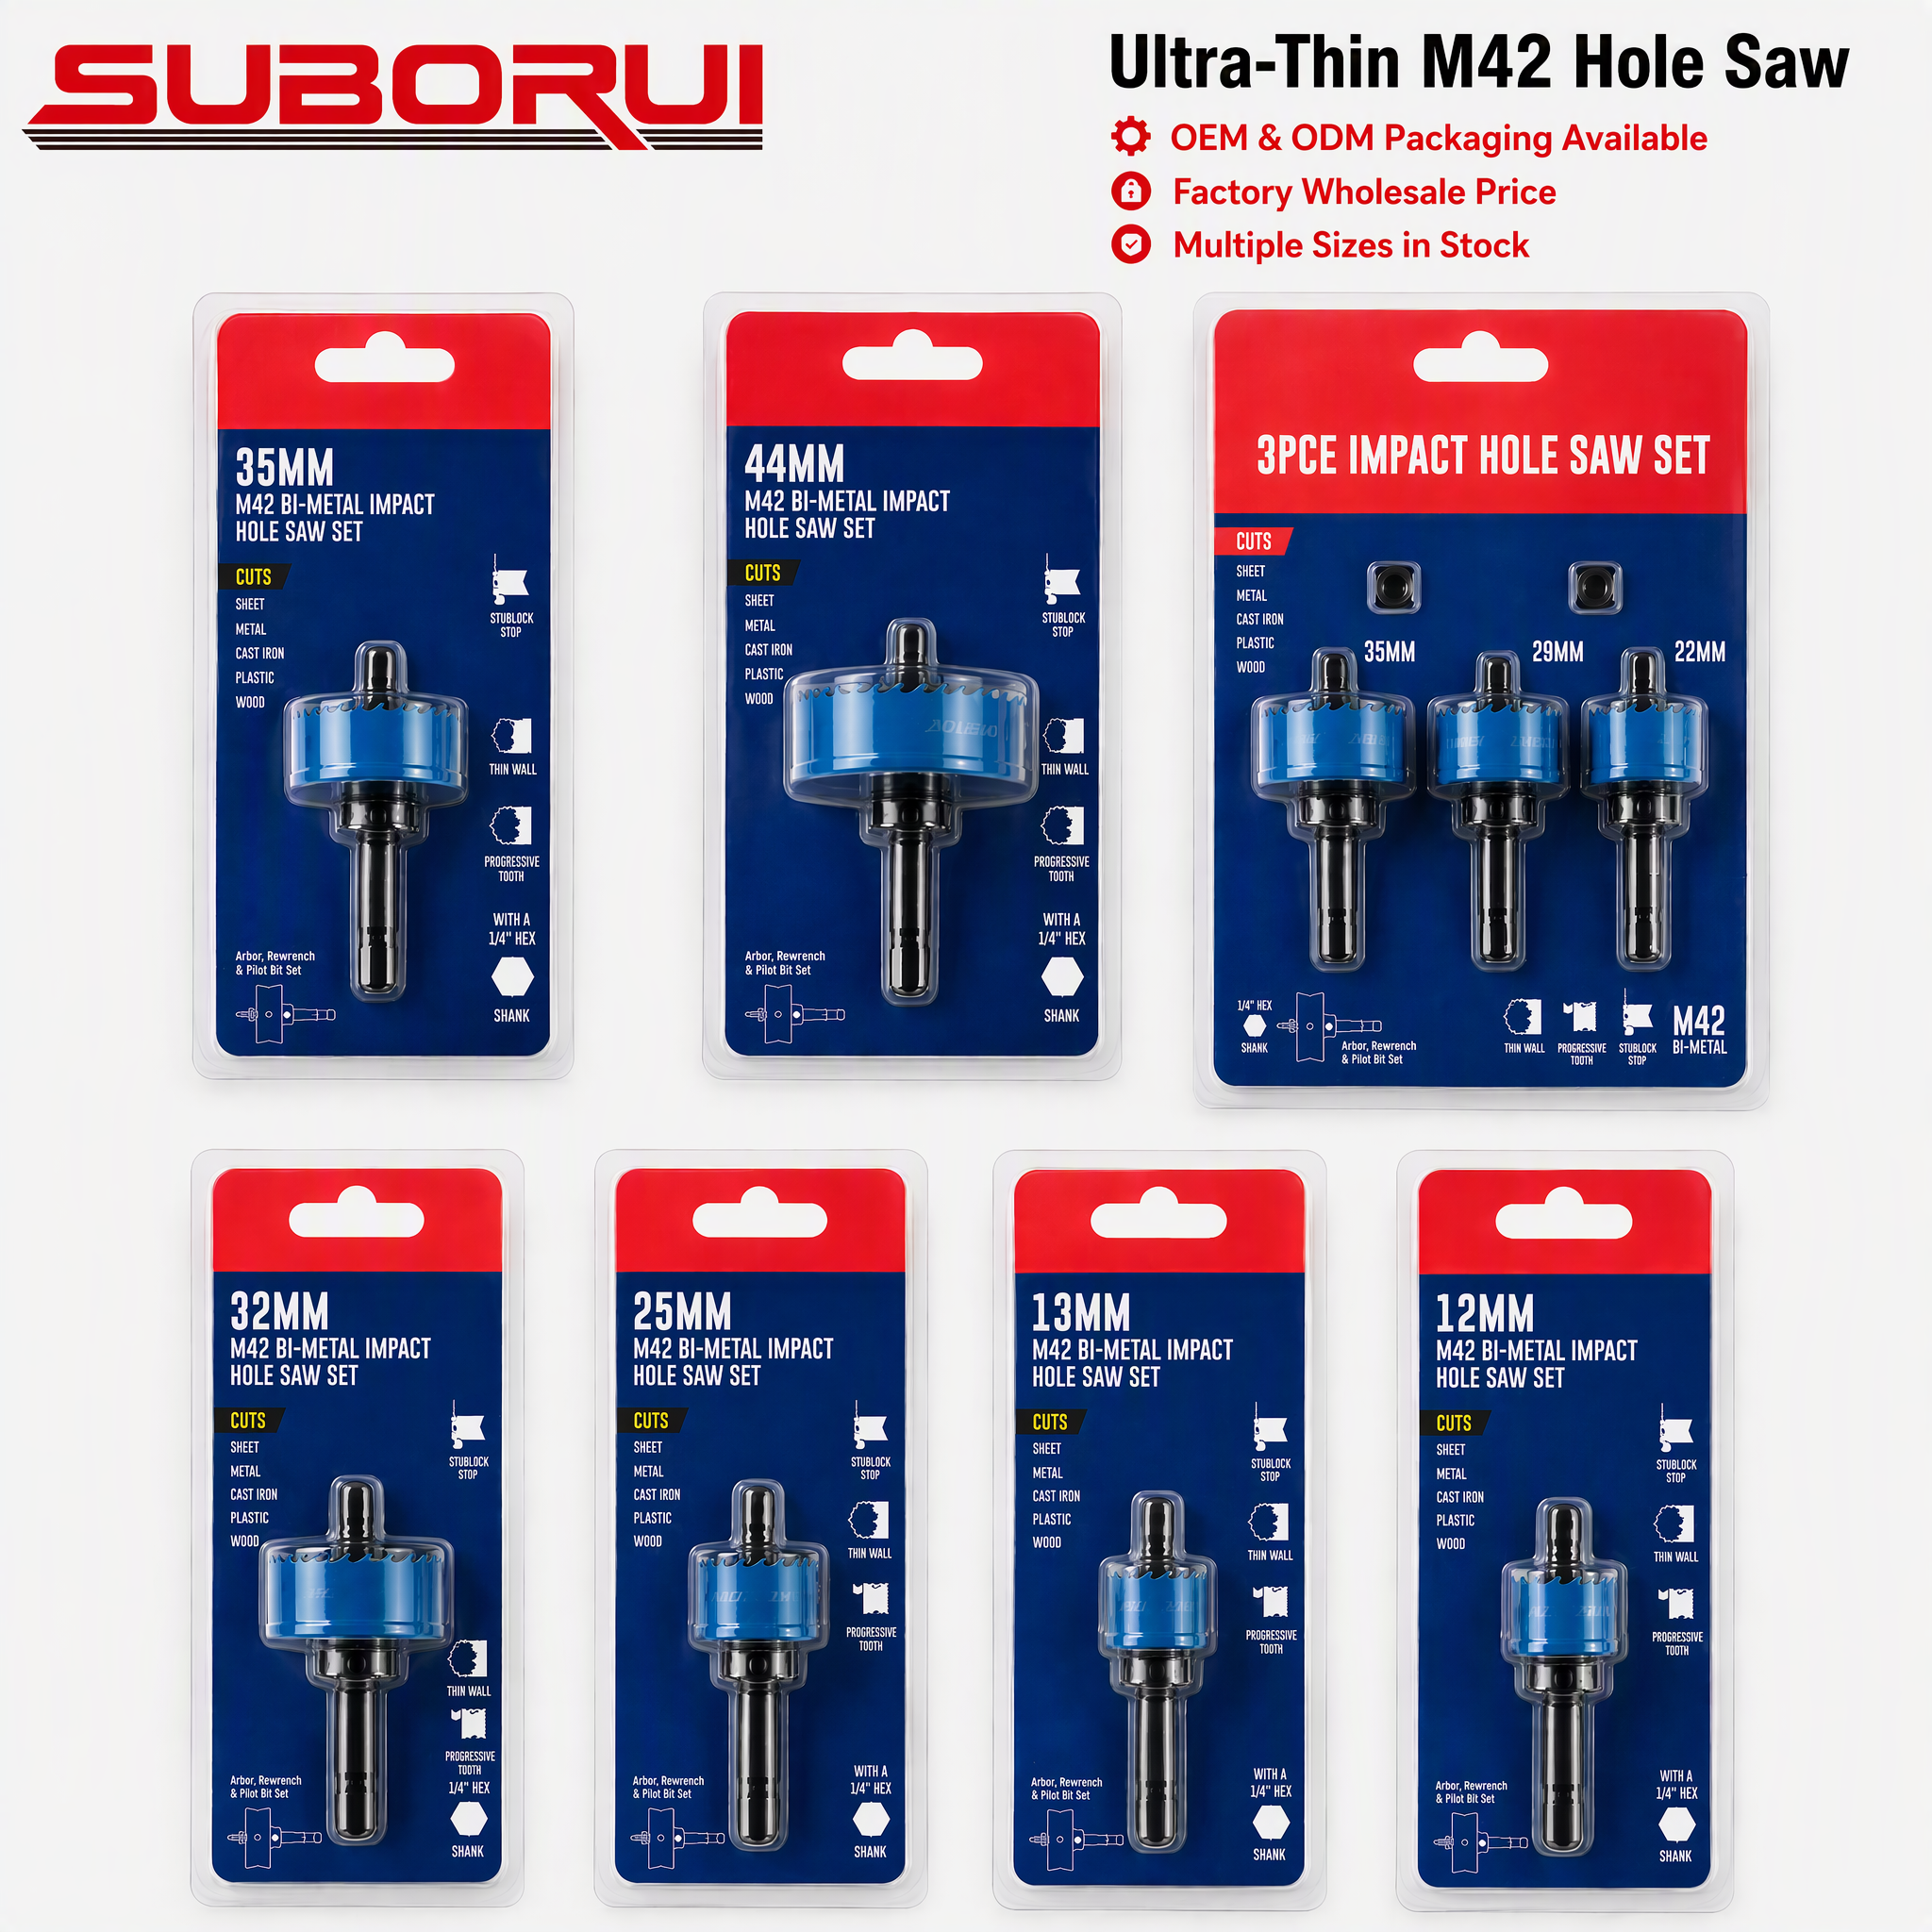
| HSS-Co M42 (8% Cobalt) | 67.0 - 69.5 HRC | Precipitated Carbides in Fe-Matrix | 630°C - 650°C | Bi-metal hole saws, interrupted cuts, thin sheet steel, aerospace aluminum, and high-vibration manual CNC routing. |
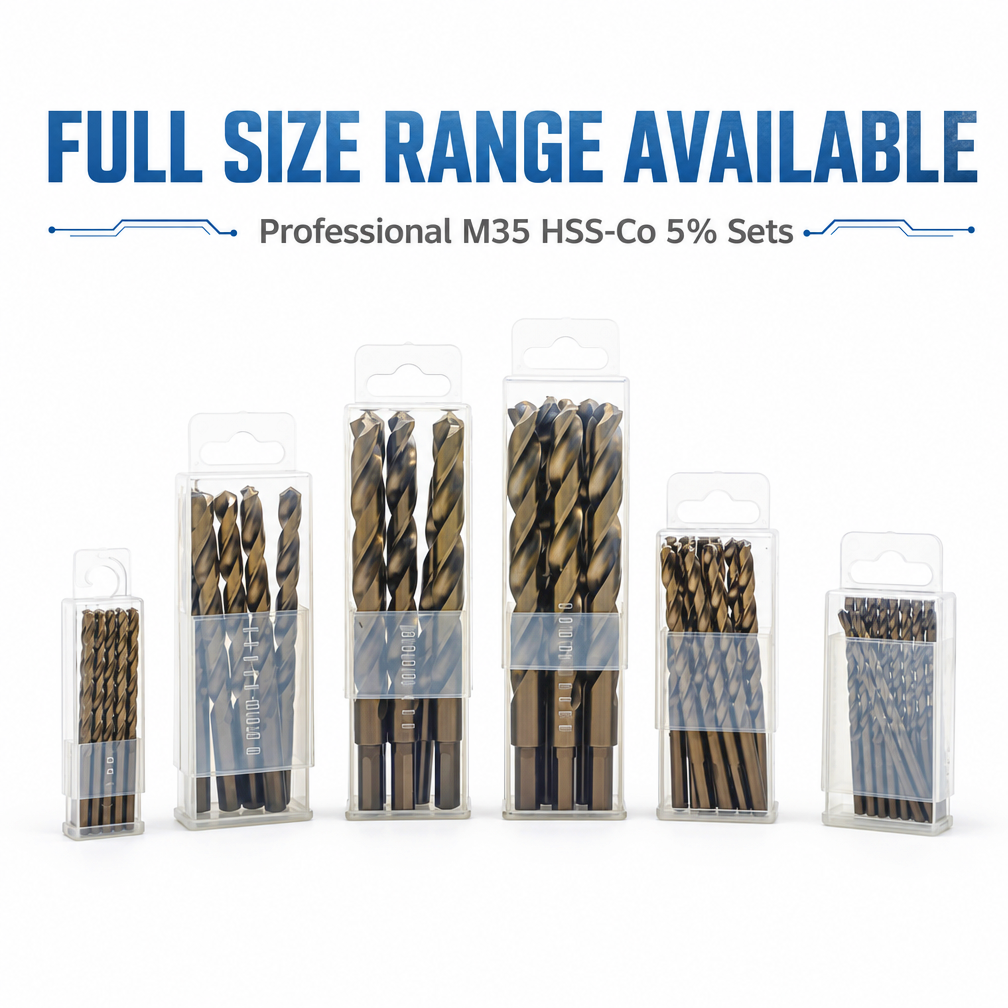
| HSS-Co M35 (5% Cobalt) | 65.0 - 67.0 HRC | Refined W-Mo-Cr-V-Co Matrix | 600°C - 620°C | Stainless steel 304/316, titanium alloys, hard steels, and general multi-axis CNC drilling and plunge operations. |
| HSS 6542 / M2 Professional | 63.0 - 65.5 HRC | Standard High-Carbon High-Speed Steel | 520°C - 550°C | Structural mild steels, cast irons, hardwoods, architectural plastics, and economical distribution sets. |
| TCT (Tungsten Carbide Tipped) | Tip: 89 - 91 HRA / Body: 42-45 HRC | Brazed Micrograin Insert onto 40Cr Alloy | 750°C - 850°C | Thick plate core cutting, deep hole annular cutting, MDF laminates, abrasive cement panels, and solid woods. |
Flute Dynamics: Balancing Chip Clearing with Core Rigidity
CNC router bits require precise helix optimization. While standard drill bits rely on 28° to 30° standard helices for vertical holemaking, CNC spiral router bits require specific helix geometries based on chip migration direction:
Upcut Spiral (Right-Hand Helix)
Discharges chips upward away from the work surface, preventing heat buildup. Ideal for high-speed roughing, blind pocketing, and deep grooving where evacuation efficiency takes priority over top-edge surface finish.
Downcut Spiral (Left-Hand Helix)
Forces the cutting vector downward, pushing swarf into the bottom of the cut. Holds down thin sheets and produces pristine top surfaces without chip-out or tear-out on delicate wood veneers, foils, and decorative laminates.
Compression (Up/Down Combo)
Combines an upcut lower flute with a downcut upper flute. The shearing forces push material inward toward the center of the panel thickness, yielding mirror-smooth, burr-free edges on both top and bottom laminate surfaces simultaneously.
Total Indicated Runout (TIR) remains the critical benchmark distinguishing budget tools from industrial-grade CNC tooling. Our manufacturing lines run automated optical laser micrometers to maintain shank-to-cutting-edge concentricity within ≤0.003 mm (≤3 microns). This level of runout precision eliminates tool vibration, prevents micro-chipping along the cutting lips, and significantly reduces spindle bearing wear across high-throughput industrial machining centers.
Why Global Tool Brands Partner with Jiangsu WRD Tools Co., Ltd.
Founded in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. has expanded into one of the flagship tooling manufacturers based in Danyang, Jiangsu Province—the industrial heart of China's cutting tool manufacturing cluster. Operating from an owned 12,000 square meter standardized production facility, our company functions strictly as an authentic primary manufacturer, not a sourcing trader.
Intertek Onsite Verification
Our complete plant infrastructure, automated heat-treatment chambers, clean grinding lines, and QA/QC optical verification laboratories are certified onsite by Intertek Group, guaranteeing verifiable factory provenance.
Massive Scale & Throughput
With an annual capacity exceeding 90 million cutting units (including 50M wood bits, 25M HSS twist drills, and 15M hex-shank rotary tools), we easily accommodate national distribution contracts and container-load repeat cycles.
Proven OEM Tier-1 Track Record
Over 19 years of continuous manufacturing, we have engineered and supplied cutting tools for market-leading multinational hardware brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Dexter, KWB, Wolfcraft, and Heller.
In recognition of our metallurgical innovations and CNC flute grinding consistency, our factory was officially designated as a High-Tech Enterprise of Jiangsu Province in 2019. All manufacturing stages—raw steel bar cutting, CNC centerless cylindrical grinding, computerized vacuum salt-bath hardening, 5-axis Walter grinding, PVD thin-film coating, laser shank marking, and automated case packing—are executed under unified ISO 9001 quality management systems.
Future Procurement Trends in Industrial CNC Cutting Tools (2025–2030)
Industrial supply chain directors and hardware brand distributors are adapting to profound technological shifts. As aerospace, automotive, architectural joinery, and renewable energy sectors transition toward abrasive carbon-fiber polymers, sintered ceramics, and ultra-high-strength alloy steels, cutting tool procurement strategies must pivot accordingly. The primary procurement trends shaping our export agreements include:
Sub-Micron Substrates & Grain Distribution
Standard 1.0 μm tungsten carbide grains are being rapidly superseded by sub-micron (0.3–0.5 μm) and ultra-fine grain structures. These provide a denser metallurgical matrix that reduces micro-chipping on razor-sharp router edges while resisting abrasive wear in dense fiberboards (HDF/MDF) and carbon-fiber reinforced plastics (CFRP).
Advanced PVD Nanocomposite Hard Coatings
Procurement teams are shifting away from basic TiN coatings toward nanostructured TiAlSiN, AlTiN, Diamond-Like Carbon (DLC), and CVD diamond films. With surface hardness values reaching 3,300–4,000 HV and oxidation limits exceeding 1,100°C, these nano-coatings enable dry, high-speed routing without flood lubricants.
Supply Chain Consolidation & ESG Traceability
North American and European hardware brands are consolidating vendor rosters, favoring integrated OEM factories with fully audited environmental compliance, conflict-free mineral verification for cobalt and tungsten, and recycled carbide reclaim programs to meet regulatory corporate sustainability directives.
Moreover, modern CNC tooling buyers increasingly specify automated optical data matrix stamping on bit shanks. By engraving QR matrix codes detailing batch numbers, exact flute geometry, and recommended cutting parameters, distributors can deliver direct value-added digital integration to their end-user industrial clients.
Cutting Tool Technology Evolution: Edge Preparation and Harmonic Damping
The mechanical boundary of cutting edge performance has progressed beyond traditional macro-grinding. To maximize throughput on heavy 5-axis CNC router installations, cutting edge micro-geometry and harmonic dynamics now represent the premier differentiators in tool engineering:
Micro-Honing & Edge Drag Finishing
Unprepared ground cutting edges possess micro-notches that propagate stress cracks under load. Utilizing fluid drag-finishing and magnetic abrasive brushing, we apply controlled 5–15 μm edge radiusing (“K-factor honing”), boosting edge strength by up to 250%.
Variable Helix & Unequal Pitch
Traditional symmetrical flutes induce resonant chatter frequencies during deep side profiling. Engineered variable helix (e.g., 35°/38° flutes) and non-uniform flute spacing interrupt harmonic resonance cycles, dramatically dampening machine vibration.
Cryogenic Heat Treatment Stabilization
To eliminate retained austenite within high-cobalt HSS-Co matrixes, our specialized vacuum heat treatment incorporates deep cryogenic cooling (-196°C) between tempering stages, achieving ultra-stable metallurgical crystal structures and permanent dimensional stability.
These engineering developments ensure that distributors purchasing custom tooling from WRD Tools receive bits that execute clean plunge cuts, run quietly at high feed rates (15–30 meters per minute), and demonstrate minimal flank wear across extended production cycles.
Industrial Sourcing & Procurement FAQ: Expert Guidance for International Buyers
Procuring custom cutting tools directly from Chinese OEM manufacturing facilities requires clear understanding of specifications, testing standards, and logistics workflows. Here are the core technical questions answered by our engineering export directorate:
Initiate Your OEM Custom Tooling Project Today
Join the prestigious network of hardware brands, industrial importers, and precision machining distributors sourcing verified cutting tooling from Jiangsu WRD Tools Co., Ltd. Send your technical CAD drawings, sample requirements, or private-label concepts for immediate review.
Inquire Now