Precision Cutting & Drilling Showcase
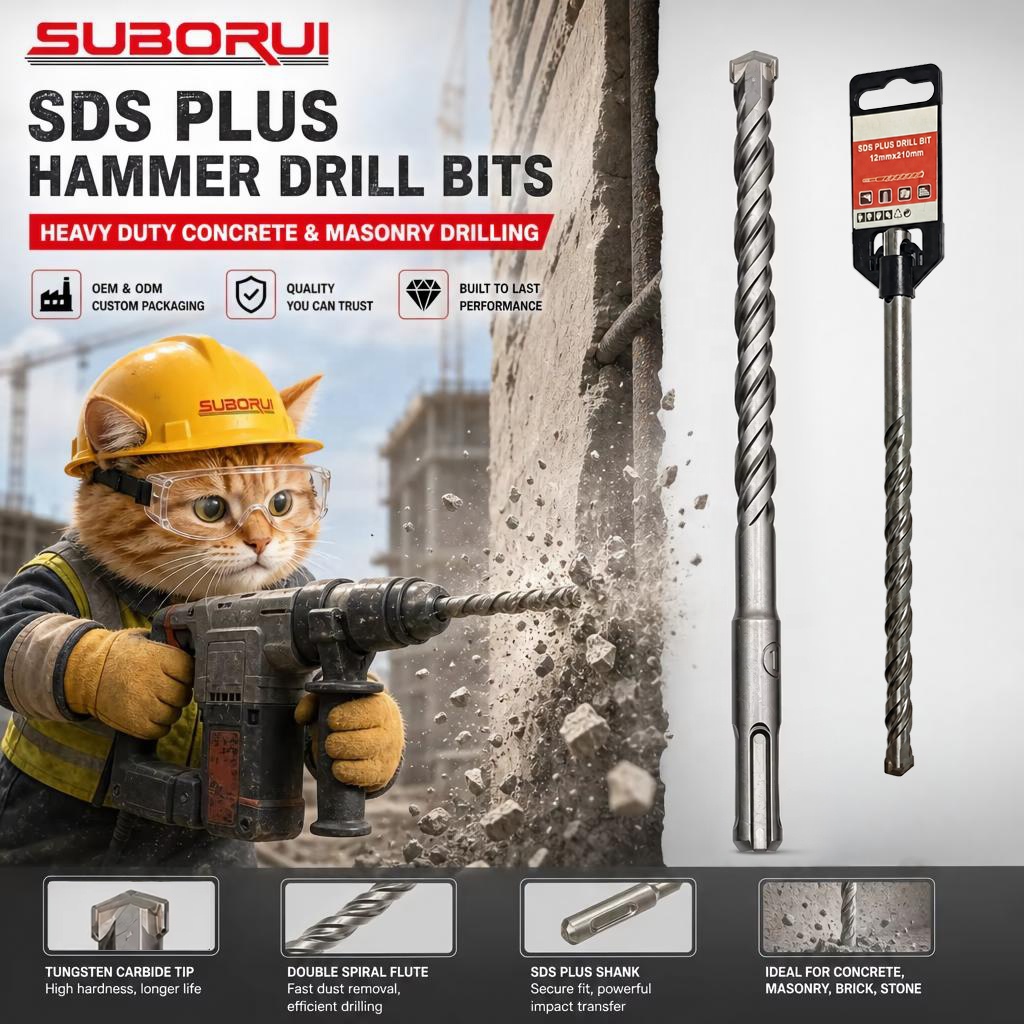
Direct OEM manufacturing capabilities across high-speed steel twist drills, masonry percussion tooling, annular cutters, and specialized hole-making systems.





Engineering Strength of Jiangsu WRD Tools Co., Ltd.
Established in March 2007 with a registered capital of RMB 10 million in Danyang, Jiangsu — the world's most concentrated cutting tool cluster — WRD Tools operates an advanced 12,000 m² production complex serving industrial brands globally.
Intertek Onsite Audit & High-Tech Certified
Our complete premises, production lines, and quality control systems are independently verified on-site by Intertek Group. Awarded the High-Tech Enterprise status of Jiangsu Province in 2019, our testing labs execute metallurgical analysis, Rockwell C hardness calibration, and optical dynamic runout testing on every raw bar batch.
Tier-1 Global Tool OEM Partnership Heritage
Our manufacturing workshops have engineered and supplied cutting tools to the global supply networks of top-tier industrial brands including BOSCH, Milwaukee, DeWalt, Makita, Irwin, Dexter, KWB, Wolfcraft, Truper, and Heller. We maintain strict confidentiality and ISO 9001 quality management discipline for private-label distributors.
End-to-End Vertical Manufacturing Control
Operating dedicated production floors for HSS twist drills (25M/year), wood drills (50M/year), hex bits (15M/year), and heavy-duty Morse taper shank drills. From high-vacuum salt-bath heat treatment to 5-axis CNC flute grinding and multi-layer physical vapor deposition (PVD), every manufacturing milestone is handled fully in-house.
Taper Shank Drill Architecture: DIN 345 & Morse Taper Systems
An authoritative engineering analysis for technical procurement directors, toolroom supervisors, and CNC machining specialists requiring verifiable rigidity and minimal TIR.
The Physics of Morse Taper Friction Drive
Taper shank twist drills conform to DIN 345, ISO 235/1, and BS 328 standards, utilizing the self-holding Morse Taper (MT) geometry invented by Stephen A. Morse. The fundamental mechanical advantage of the taper shank over straight cylindrical shanks lies in the self-centering conical interface with a slight taper angle (approximately 1.49° to 1.51° per side, or ~5/8" taper per foot). Under high axial feed thrust forces ($F_z$), the conical surfaces achieve wedge friction that transmits substantial rotational torque without the slip characteristics inherent to conventional 3-jaw drill chucks.
The flattened driving tang at the end of the taper engages directly into the ejector slot of the machine spindle or reduction sleeve. While the conical contact surface transmits over 85% of normal drilling torque through elastoplastic friction fit, the tang functions as a positive mechanical failsafe under extreme torsional shock loads, protecting the spindle taper bore against fretting and galling.
- Concentricity (TIR < 0.02mm): Precision ground shanks eliminate radial play, preventing oversized hole diameters and irregular bell-mouthing.
- Heavy Machine Integration: Direct mounting into radial drilling machines, heavy tailstocks, CNC horizontal borers, and bridge milling centers.
- Tang Structural Integrity: Selectively induction-tempered tangs (HRC 38-45) absorb high cyclic torsional impact without brittle fracture.
- Optimized Parabolic Web: Progressive flute core thickening increases tool rigidity against axial compression while maintaining clearance for chip evacuation.
| Morse Taper No. | Typical Drill Diameter Range | Gauge Diameter ($D$) | Taper per Foot (TPF) | Taper Ratio | DIN 345 Overall Length Range | Recommended Machine Types |
|---|---|---|---|---|---|---|
| MT1 | Ø 3.0 mm – 14.0 mm | 12.065 mm | 0.59858 in/ft | 1 : 20.047 | 130 mm – 189 mm | Bench drill presses, small turret lathes |
| MT2 | Ø 14.25 mm – 23.0 mm | 17.780 mm | 0.59941 in/ft | 1 : 20.020 | 212 mm – 253 mm | Pillar drill machines, manual toolroom lathes |
| MT3 | Ø 23.25 mm – 31.75 mm | 23.825 mm | 0.60235 in/ft | 1 : 19.922 | 276 mm – 301 mm | Radial arm drill presses, medium CNC lathes |
| MT4 | Ø 32.0 mm – 50.5 mm | 31.267 mm | 0.62400 in/ft | 1 : 19.231 | 334 mm – 369 mm | Heavy industrial radials, horizontal boring mills |
| MT5 | Ø 51.0 mm – 76.0 mm | 44.399 mm | 0.63151 in/ft | 1 : 19.002 | 415 mm – 460 mm | Heavy shipbuilding drill heads, structural milling lines |
| MT6 | Ø 77.0 mm – 100.0+ mm | 63.348 mm | 0.62565 in/ft | 1 : 19.180 | 510 mm – 580 mm | Specialized steel casting & forging drilling rigs |
Steel Grades & Metallurgical Performance
Evaluating high-speed steel grain refinement, tungsten-molybdenum balancing, and high-temperature cobalt red hardness for heavy industrial cutting applications.
Standard HSS 4241 / 4341 Alloys
Characterized by 1.5–2.0% Tungsten and 1.0–1.5% Molybdenum content. Heat treated to HRC 62-64. Ideal for mild structural steels (Q235, A36), ductile cast irons, and general repair machining where thermal tool stress remains below 500°C. An economical choice for standard hardware distributors and general structural fabrication shops.
High-Performance M2 / HSS 6542
The global industrial baseline containing ~6.0% Tungsten, 5.0% Molybdenum, 4.0% Chromium, and 2.0% Vanadium. Yields fine vanadium carbide precipitation, providing exceptional abrasive wear resistance and toughness at HRC 63-65. Engineered for high-speed drilling in carbon alloys (40Cr, 4140), manganese railway steels, and structural beams.
Cobalt-Enriched M35 (Co 5%) & M42 (Co 8%)
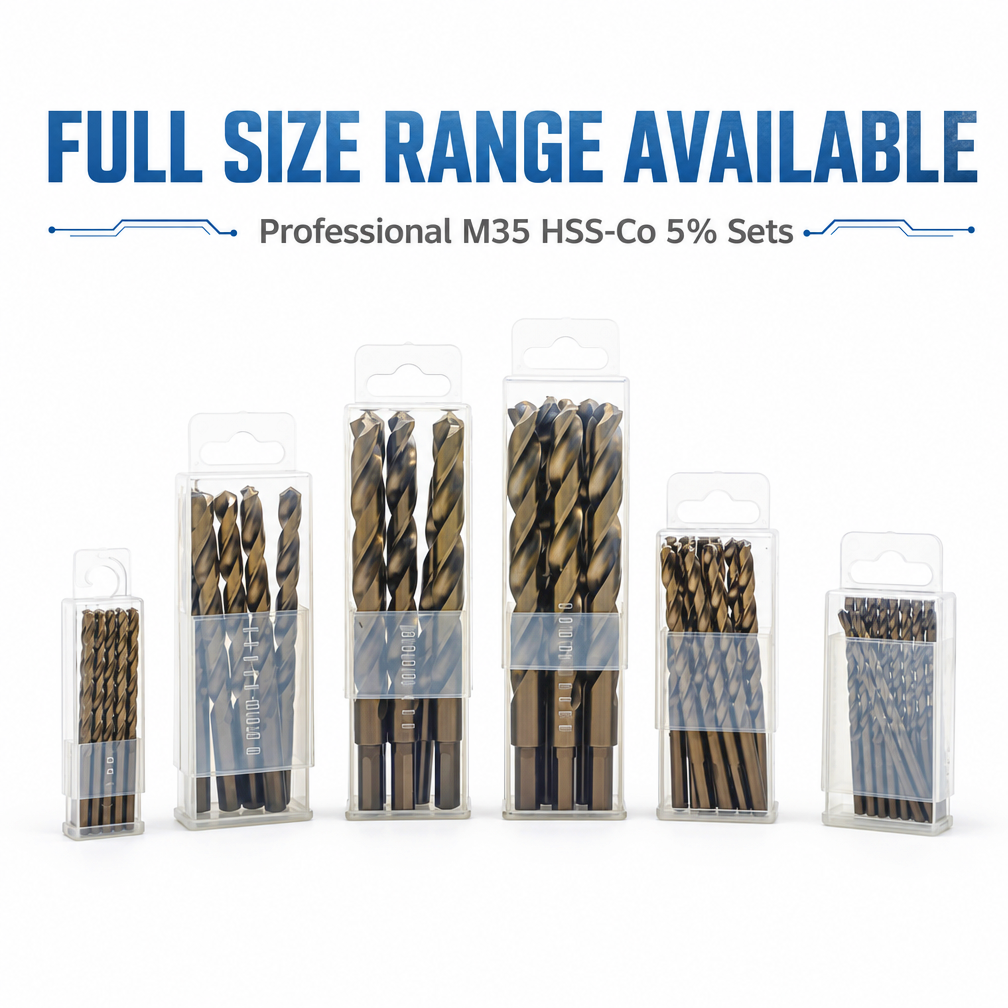
By incorporating 5% to 8% active Cobalt into the molybdenum-tungsten matrix, the red hardness threshold rises significantly to 650°C, sustaining HRC 65-67 cutting efficiency. Specifically tailored for austenitic stainless steels (304, 316L), Inconel superalloys, titanium alloys, and heat-treated die steels where thermal accumulation would soften standard HSS cutting edges.
| Coating / Surface Finish | Visual Appearance | Micro-Hardness (HV) | Max Service Temp (°C) | Friction Coeff. vs Steel | Primary Industrial Application |
|---|---|---|---|---|---|
| Steam Oxide (Black Oxide) | Deep Matte Black | ~800 HV | 450 °C | 0.70 | General steel drilling, improved coolant retention, anti-galling |
| Bright / Amber Fully Ground | Metallic Polished / Amber | Base Metal (~850 HV) | 500 °C | 0.65 | Non-ferrous alloys, aluminum, brass, soft carbon steel, precision reaming |
| Titanium Nitride (TiN) | Brilliant Metallic Gold | 2,300 HV | 600 °C | 0.40 | General production CNC drilling, 2.5x to 3x wear-life enhancement |
| Titanium Carbonitride (TiCN) | Violet / Anthracite Bronze | 3,000 HV | 400 °C | 0.30 | Highly abrasive cast irons, silicon aluminum, high-feed production lines |
| Titanium Aluminum Nitride (TiAlN) | Dark Violet / Charcoal Grey | 3,400 HV | 800 °C | 0.35 | Dry/MQL high-speed drilling, stainless steels, hardened tool steels >HRC 40 |
From Raw Ingot to Precision Morse Taper: Step-by-Step QA Workflow
Rigorous multi-stage production protocol deployed at our Danyang manufacturing plant to guarantee consistent shank-to-flute runout within 0.02 mm.
Spectrometric Material Verification
Every delivery of HSS rounds is scanned via direct-reading emission spectrometers to confirm elemental percentages of W, Mo, Cr, V, and Co. Bars undergo eddy-current crack detection before shearing.
Friction Welding / Bimetal Forging
For large diameter taper drills (>Ø14mm), precision friction welding bonds an HSS cutting body to a structural 45# carbon steel Morse shank, optimizing torsional resilience while minimizing raw material cost.
Computer-Controlled Heat Treatment
Multi-stage preheating followed by salt-bath or high-vacuum austenitizing at 1200–1230°C, deep isothermal quenching, and three separate 560°C tempering cycles to transform retained austenite into uniform martensite.
5-Axis CNC Flute & Point Grinding
Flutes are ground from solid hardened blanks on computerized CBN wheel centers, forming precise 30° helix angles, polished margins, and self-centering 118° or 135° split points conforming to DIN 1414-1.
Future Procurement Trends in Taper Shank Tooling (2025–2030)
Strategic supply chain analysis to assist B2B enterprise procurement officers and national tool brands in future-proofing their inventory and manufacturing strategies.
1. Internal Coolant Channel Integration in MT Drills
Demands for continuous, high-volume chip evacuation on deep-hole CNC machinery are shifting taper shank procurement toward spiral or parallel internal coolant holes. Pressurized cutting fluid delivered directly to the point reduces drill-tip temperatures by up to 280°C, enabling feed rate increases exceeding 40% in structural steel fabrication.
2. Nanocomposite Physical Vapor Deposition (PVD)
Traditional single-layer TiN coatings are rapidly yielding market share to multi-component nanolayered AlTiN, AlCrN, and TiSiN coatings. These superlattice structures create microscopic barrier layers that prevent crack propagation through the coating film, sustaining hardness values above 3,200 HV even when exposed to severe frictional friction in unlubricated field operations.
3. Supply Chain Consolidation into Danyang Industrial Clusters
To mitigate volatile global shipping cycles and escalating tariffs, leading tier-1 distributors are establishing direct supplier agreements with full-capability manufacturing plants. Sourcing directly from Danyang provides integrated access to local high-speed steel mills, specialized heat-treatment plants, and automated packaging hubs, slashing lead times by 35%.
Frequently Asked Sourcing Questions
Clear, technical, and commercial answers for international supply managers, engineering importers, and brand product leads.
China Factory Procurement: Risk Mitigation Checklist
Crucial quality checkpoints to include in your purchase specifications and third-party pre-shipment inspections.
| Inspection Feature | Acceptance Benchmark | Testing Instrument / Method | Critical Defect Risk |
|---|---|---|---|
| Flute Hardness | HRC 63.0 – 66.0 (HSS M2) / 65.0 – 67.5 (M35) | Calibrated Rockwell Hardness Tester (Diamond Cone, 150kg) | Premature flank wear or catastrophic edge chipping |
| Tang Hardness | HRC 38.0 – 46.0 (Ductile Core) | Rockwell C Test on flattened driving tang flats | Tang shearing under torque (too soft) or brittle cracking (too hard) |
| Taper Contact Area | ≥ 80% surface contact against standard gauge | Prussian blue dye fit test inside calibrated DIN 229 Morse ring gauge | Spindle slippage, vibration, taper bore galling, tool chatter |
| Web Centering | Web concentric to OD within ±0.03 mm | Optical Toolmaker Microscope / 3D Coordinate Machine | Drift during drilling, uneven chip load, oversized holes |
| Point Geometry | 118° ±1° (Standard) or 135° ±1° with Type C Split Point | Optical point comparator / Profile projector | High axial thrust force, walking on start, drill point burn |
Partner Directly with an Intertek-Verified Drill Bit Factory
Eliminate intermediary trading margins, guarantee DIN 345 standard conformity, and accelerate delivery lead times. Contact our export engineering team in Danyang, Jiangsu today for technical specifications, product catalogs, and customized factory quotations.
Inquire Now