Engineered Threading & Drilling Portfolio
Explore our core export-grade metalworking, threading, and cutting tools manufactured under strict DIN and ISO tolerances.

SUBORUI 1/4" HSS Fully Ground TiN Hex Shank Drill

SUBORUI HSS Co8% M42 Bi-Metal Industrial Saw Kit

Suborui 35-100mm Borderless Spotlight Opener
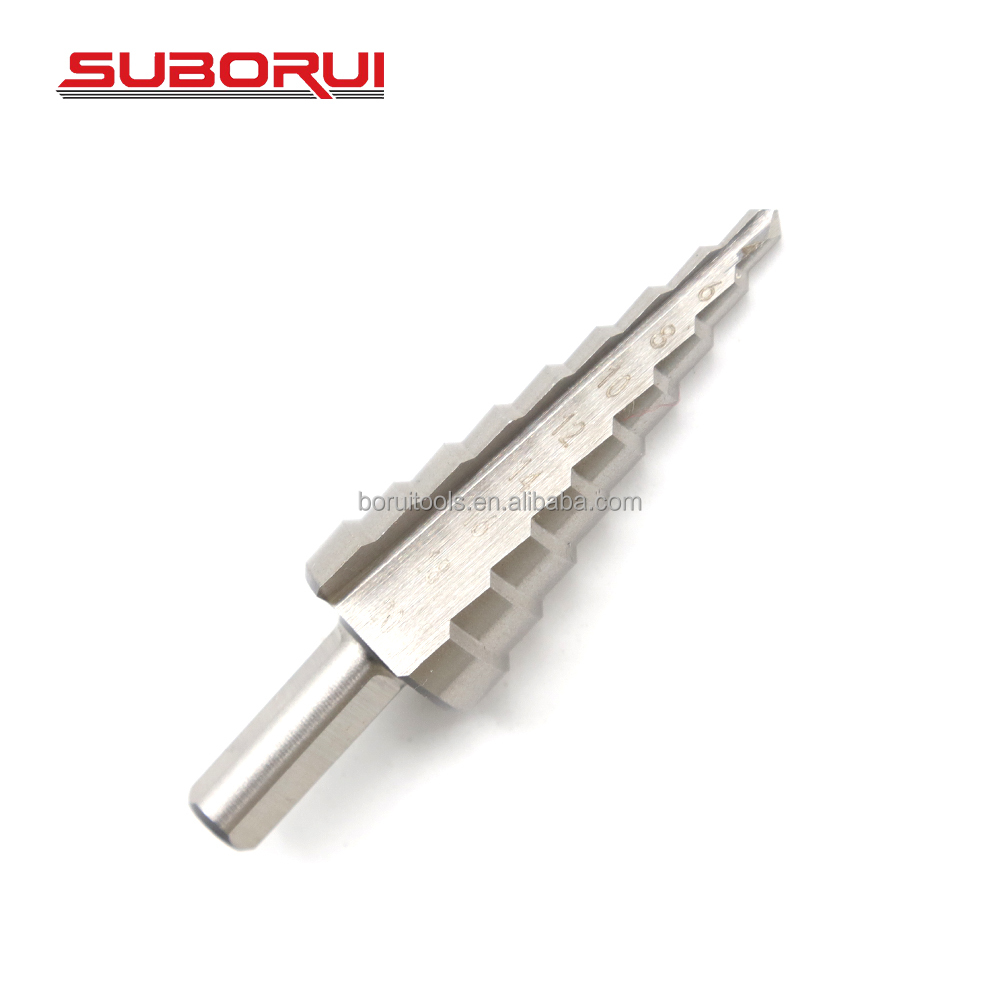
SUBORUI 4-12mm HSS Straight Flute Unibit Step Drill
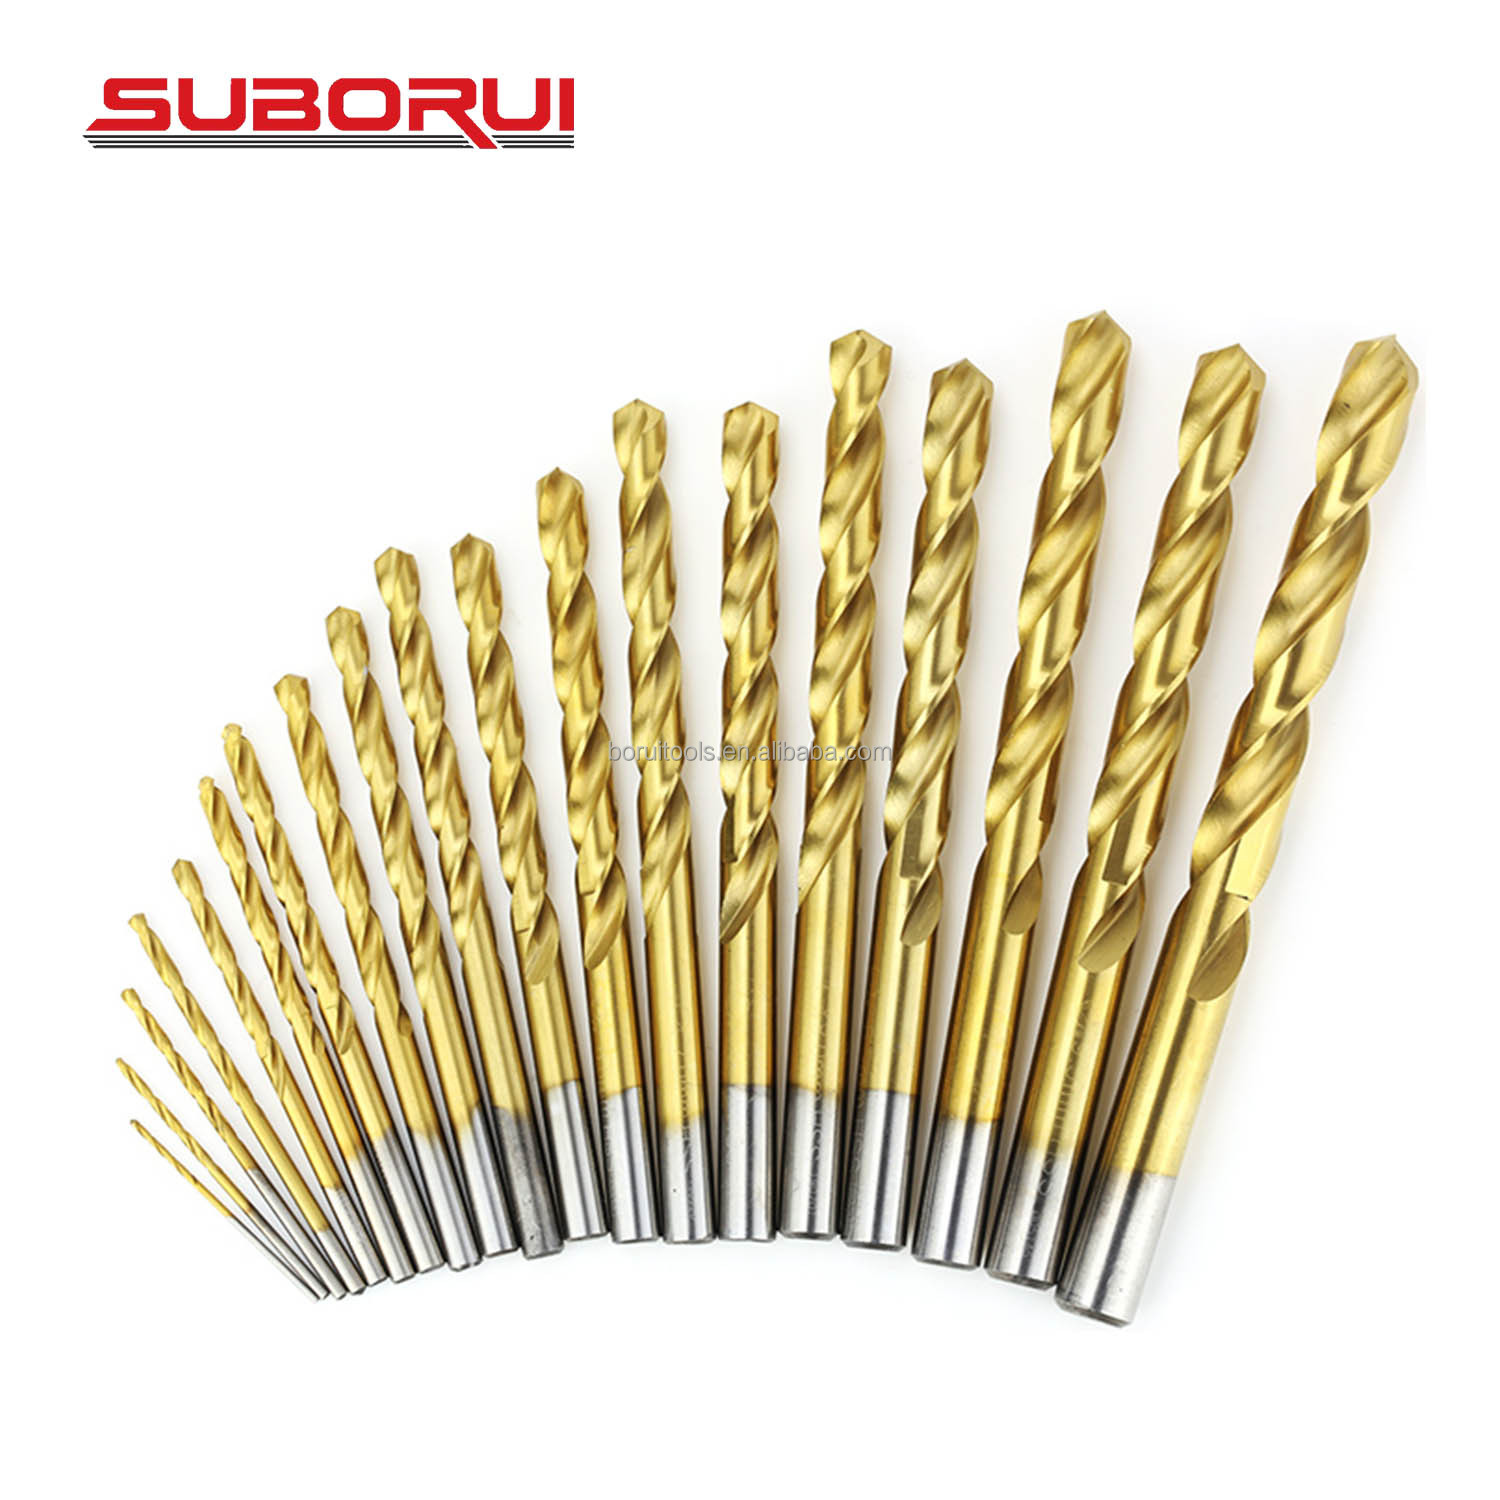
SUBORUI DIN338 Fully Ground TiN HSS M2 Twist Drills
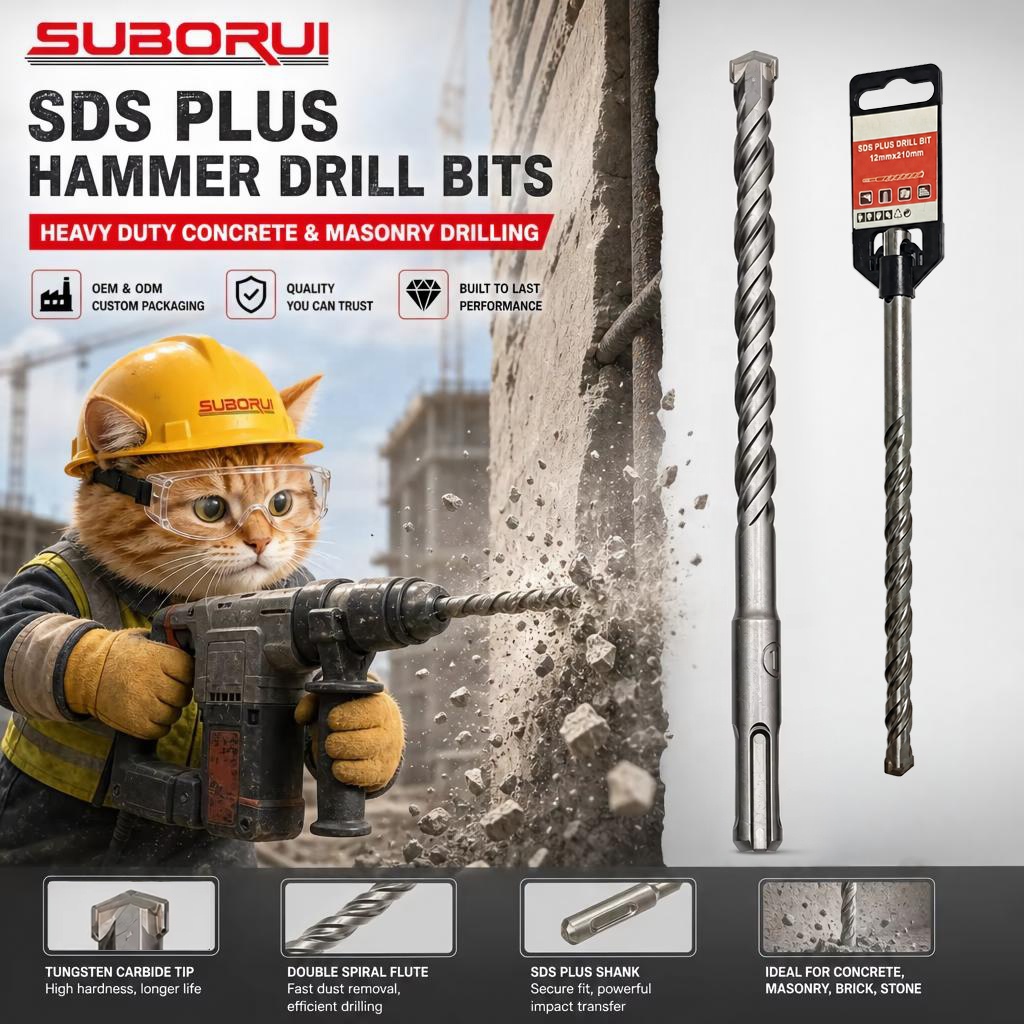
SUBORUI 40Cr 4-Flute Single Carbide SDS Plus Drill

SUBORUI DIN338 M35 5% Cobalt Drill for SS304/316

SUBORUI Super-Thin Diamond Turbo Porcelain Blade
Engineering Authority: Cold Forming vs. Cutting Tap Mechanics
In modern industrial assembly, the demand for thread reliability has caused a paradigm shift toward thread forming taps (frequently designated as roll form taps, cold forming taps, or fluteless taps). Unlike conventional cutting taps that sever the grain structure of the parent metal and generate troublesome curly chips, a thread forming tap works by controlled plastic deformation. As the lobed tap enters the pre-drilled bore, it displaces material outward into the thread crests.
Why Tier-1 Automotive & Aerospace Machining Prefer Cold Forming
From an operational standpoint in high-volume CNC tapping centers, chip control is the single largest factor dictating spindle uptime. Traditional spiral point or spiral flute cutting taps create chips that easily bird-nest around high-speed spindles, score newly finished bores, or pack into blind holes, causing catastrophic tool breakage. Because roll forming taps produce zero chips, the risk of tap breakage caused by chip packing in deep blind holes is virtually eliminated.
| Performance Characteristic | Cold Thread Forming Taps | Conventional Cutting Taps |
|---|---|---|
| Internal Grain Structure | Continuous, unbroken grain flow along flank contour | Interrupted, sheared grain profile creating stress notches |
| Chip Evacuation Requirement | Zero chips produced; ideal for blind holes | Requires spiral evacuation; high risk of nesting |
| Tensile & Strip Resistance | Significantly higher (work-hardened flank surface) | Standard; susceptible to micro-tear failure points |
| Pre-Tap Bore Size Sensitivity | Extremely tight hole tolerance requirement (±0.02mm) | Moderate tolerance window (tolerates slight deviation) |
| Machinable Material Class | Ductile metals (>9-10% elongation rating) | All materials including brittle cast iron & bronze |
To successfully deploy thread forming taps, plant engineers must closely calibrate the core hole diameter. Because the parent material flows inward to build the minor diameter, undersized drilling results in excessive hydrodynamic friction, torque spiking, and tool seizure. WRD Tools equips technical procurement teams with precise empirical hole calculators based on material tensile strength, surface speed (SFM), and metallurgical expansion.
Strategic Sourcing Horizons: The Future of Industrial Thread Forming (2025–2030)
As original equipment manufacturers (OEMs) shift toward structural weight reduction, localized production near automated assembly hubs, and sustainable green machining, industrial procurement teams must adapt their supplier evaluation criteria.
Powder Metallurgy (PM-HSS)
Standard melted high-speed steels (M2) are transitioning to Powder Metallurgy (HSS-E-PM / ASP2023 / CPM). Micro-carbide distribution minimizes chipping at thread crests under high-cycle mechanical stress.
Advanced PVD & TiAlN/AlCrN
Traditional TiN coatings are being superseded by multi-layer PVD AlCrN and diamond-like coatings (DLC), providing thermal stabilization past 900°C for dry tapping and micro-lubrication (MQL) lines.
Lightweight Alloy Fastening
EV structural casings utilizing cast aluminum (AlSi7Mg), die-cast magnesium, and high-ductility chassis alloys mandate specialized thread formers engineered with customized lobe profiles and internal coolant bores.
Strategic Factory Integration in China's Leading Tooling Hub
The consolidation of precision grinding technologies in Danyang, Jiangsu, allows Jiangsu WRD Tools to provide Tier-1 and Tier-2 component manufacturers with substantial advantages. Bypassing intermediaries enables direct access to engineering design consultations, batch run-out laser diagnostics, and complete transparency from bar stock cutting through salt-bath thermal stabilization.
Why Enterprise Brands Partner with Jiangsu WRD Tools
Established in March 2007 with a registered capital of RMB 10 million, Jiangsu WRD Tools Co., Ltd. has developed into a cutting tool manufacturer spanning 12,000 m² of specialized workshops. We operate strictly as an end-to-end manufacturer rather than a trading export broker.
Intertek Onsite Audited
Our workshop infrastructure, calibration standards, and QA/QC management lines have been independently inspected and verified onsite by Intertek Group.
Tier-1 OEM Track Record
We produce OEM tooling lines engineered for global retail tool powerhouses, including BOSCH, Milwaukee, DeWalt, Makita, Irwin, and Wolfcraft.
State High-Tech Enterprise
Recognized as an official High-Tech Enterprise of Jiangsu Province in 2019, our specialized in-house R&D team holds multiple tool-geometry design patents.
Fully Controlled Production
From raw metallurgical inspection, bar turning, salt-bath hardening, to CNC multi-axis relief grinding and optical sorting, everything stays under one roof.
Frequently Asked Sourcing & Engineering Questions
Key information regarding pre-tap hole sizing, material compatibility, minimum order volumes, and OEM branding options.
What metallurgical materials are suitable for thread forming taps?
How do pre-tap hole diameter calculations differ from conventional cutting taps?
What is the practical MOQ and manufacturing lead time for custom OEM batches?
Why is lubricant selection critical when running cold forming tools?
Can Jiangsu WRD Tools support private labeling, laser marking, and custom retail kits?
Request an Engineering Quote or Custom Tooling Blueprint
Partner directly with Jiangsu WRD Tools Co., Ltd. for your thread forming tap programs. Submit your part drawings, material specifications, and production targets to our export engineering office.