High-Performance Tooling Recommendations
Explore our specialized inventory of core broaching cutters, masonry systems, and industrial step drills optimized for CNC stations and magnetic base drilling machines.





Engineering Dynamics of Annular Broaching
A comprehensive analysis of metallurgy, chip formation kinetics, and total cost of ownership (TCO) in structural steel beam fabrication, rail engineering, and heavy plant installation.
Kerf Annular Mechanics vs. Solid Drilling
Unlike standard twist drills that convert the entire hole volume into scrap swarf, annular cutters (broach cutters) cut exclusively along the circumference. This peripheral cutting mechanic yields critical engineering advantages:
- Reduced Energy Consumption: Consumes up to 65% less thrust and wattage from portable magnetic drill motors.
- Thermal Dissipation: Ejection of the central solid steel slug removes up to 70% of friction-induced heat before work hardening occurs.
- Cycle Time Acceleration: Pierces through structural carbon steel (like Q235, Q345, ASTM A36) 3 to 4 times faster than jobber bits.
Material Substrate Selection: M2, M35 & TCT
Specifying the metallurgical composition defines tool life, sharpening recyclability, and operational feed speeds across differing structural hardness regimes:
- HSS-M2 (6542): Best-in-class elasticity and shock resistance. Exceptional for portable jobsites with imperfect rig stability. Fully resharpenable.
- M35 Cobalt (5% Co): Hardness rating of 65–67 HRC. Prevents thermal edge breakdown when boring tough alloy steels and 304/316 austenitic stainless.
- Tungsten Carbide Tipped (TCT): Fine-grained carbide tips brazed to micro-alloy steel bodies. Crucial for drilling HARDOX, rail track, and 400+ HB plates.
Shank Geometry Compatibility Guide
Seamless mechanical connection between the mag drill arbor and the annular cutter avoids concentric run-out errors (≤0.02mm) and premature tooth rupture:
- 19.05mm (3/4") Weldon Shank: The global standard with two flat clamping planes for grub screw fixation. Compatible with over 80% of mag drill presses.
- One-Touch / Universal Shank: Dual-purpose quick-locking shank fitting both Weldon arbors and Nitto Kohki quick-release chuck systems.
- Fein Quick-In: Proprietary four-ridge rapid lock configuration engineered for quick changes on industrial Fein magnetic drilling stations.
Engineering Specification Matrix: Core Cutters & Industrial Hole Tools
| Cutter Classification | Core Substrate | Applicable Hardness | Surface Treatment | Optimized Applications |
|---|---|---|---|---|
| Standard HSS Annular Cutter | AISI M2 / W6Mo5Cr4V2 | ≤ 28 HRC (270 HB) | Bright / Steam Oxide | Structural I-Beams, channel steel, bridge construction, general fabrication. |
| HSS-Cobalt Broach Bit | AISI M35 (Co 5%) | ≤ 36 HRC (340 HB) | Amber / TiN Gold Coated | Austenitic stainless plates, boiler steels, high-tensile structural pipework. |
| TCT Carbide Core Drill | Virgin Micrograin YG8 / YG10 | ≤ 50 HRC (480 HB) | Mirror Finish / AlTiN | Railway tracks, crane rails, HARDOX, armored plating, structural cast iron. |
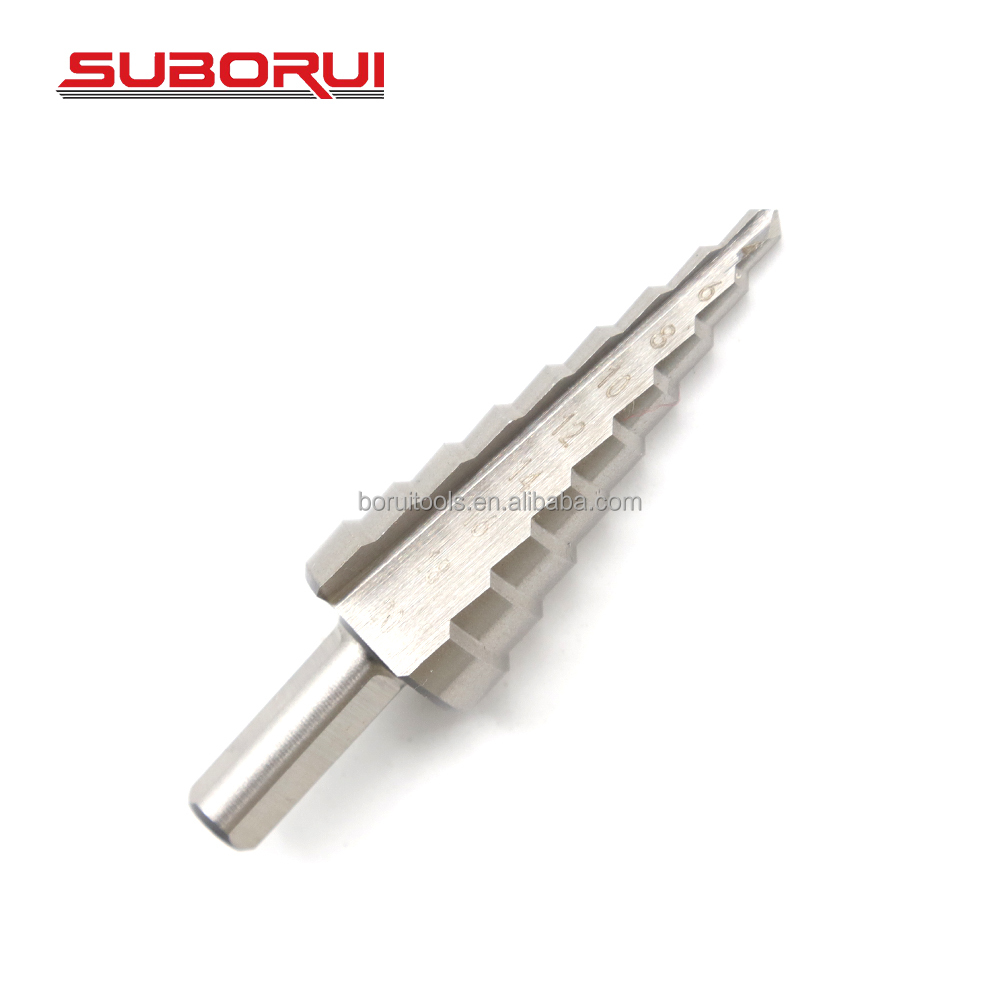
| Industrial Step Drill (Unibit) | HSS 4241 / HSS-G 6542 | ≤ 25 HRC (240 HB) | Titanium Nitride (TiN) | Electrical distribution cabinets, sheet metal enclosure ductwork, junction boxes. |
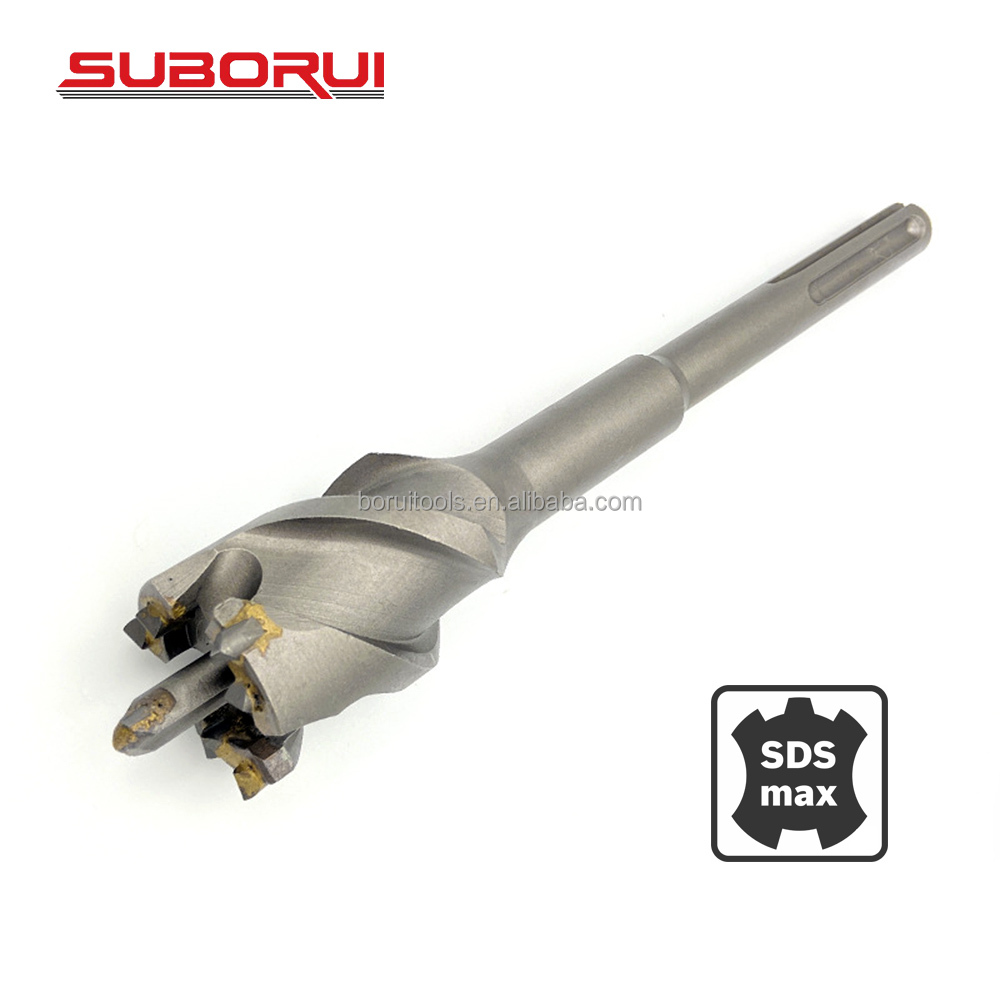
| Carbide SDS-Max Hollow Saw | YG11C Heavy Carbide | Concrete / C40 Masonry | Sandblasted Finish | HVAC through-wall ducting, civil piping installations, reinforced stone barriers. |
Future Trajectory in Industrial Hole Cutting
Key procurement shifts observed across North American and European industrial distributors managing supply continuity, carbon footprint, and operational throughput.
1. Consolidation from M2 to High-Feed TCT Cutters
As structural fabricators switch to high-yield strength steels (S355, S460, and dual-phase alloys), high-speed steel reaches thermal saturation faster. Importers and wholesalers are adjusting inventory allocations: while HSS remains dominant for light DIY and standard jobber contracts, TCT core cutters now account for over 52% of re-orders in the infrastructure and shipbuilding sectors due to their ability to run at 2.5x higher RPM without tip softening.
2. Nano-Layered Physical Vapor Deposition (PVD)
Black oxide and simple single-layer TiN coatings are being superseded by multi-layered AlCrN (Aluminum Chromium Nitride) and TiAlN (Titanium Aluminum Nitride) nano-coatings. These coatings form an aluminum-oxide ceramic protective glaze at operating temperatures exceeding 800°C. For procurement managers, this delivers up to a 40% reduction in cutting fluid dependency, catering to job sites implementing dry-drilling protocols.
3. Automated CNC Cell Consistency & Supply Resilience
Tool buyers are moving away from regional brokers toward verified direct-from-factory partnerships equipped with multi-axis CNC flute grinding cells. Consistent web thickness, precise 3-step tooth pitch geometry (alternate tooth chamfers), and exact core concentricity prevent tool chattering on job sites. Factory direct validation through Intertek or ISO accreditation provides international buyers with guaranteed batch reproducibility.
Jiangsu WRD Tools: Engineering Authority Since 2007
Headquartered in Pengzhuang, Danbei Town, Danyang—the heart of China's premier cutting tool cluster—Jiangsu WRD Tools Co., Ltd. operates a high-precision 12,000 square meter manufacturing plant with dedicated multi-axis production centers.
Unlike export trading agencies, our integrated plant controls the entire metallurgical value chain: certified high-speed steel bar procurement, bar-blank cropping, automated salt-bath heat treatment, multi-axis flute CNC grinding, vacuum coating, laser profiling, and retail-ready packaging.
Global OEM & Private-Label Capabilities
We provide comprehensive private-label production services for international tool vendors, automotive wholesalers, and industrial MRO supply chains across Germany, the USA, Switzerland, and Sweden:
- Laser Etching: High-precision logo, fractional/metric size markings, and batch traceability codes on tool shanks.
- Custom Geometry: Bespoke flute depths (25mm, 35mm, 50mm, 75mm, 100mm) and specific step-angle chamfers tailored to proprietary customer blueprints.
- Packaging Presentation: Heavy-duty blow-molded cases, plastic tubes with anti-corrosion VCI liners, magnetic pilot pin sets, and retail blister cards.
- Strict In-Process Metrology: Flute run-out check, Rockwell hardness verification per heat, and actual cycle-drilling tests on 20mm Q345 steel blocks.
Frequently Asked Sourcing Questions
Essential guidance addressing lead times, material validation, private labeling, and technical specifications for B2B tool buyers.